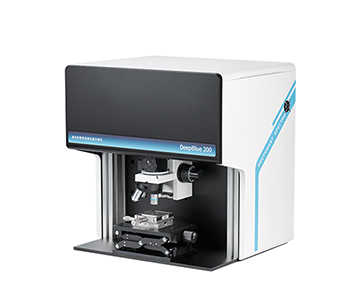
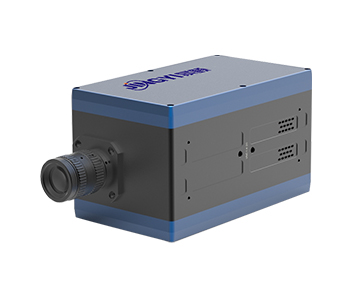
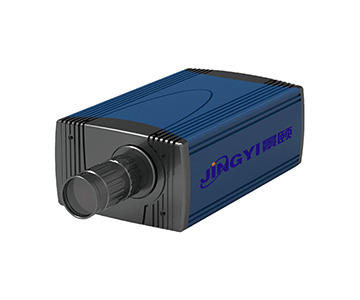
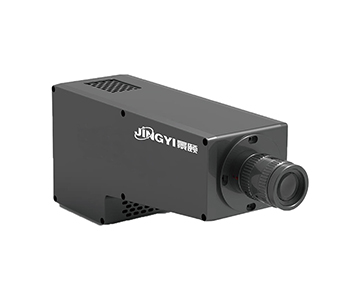
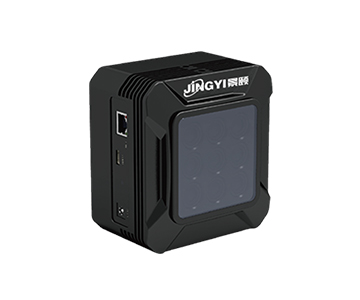
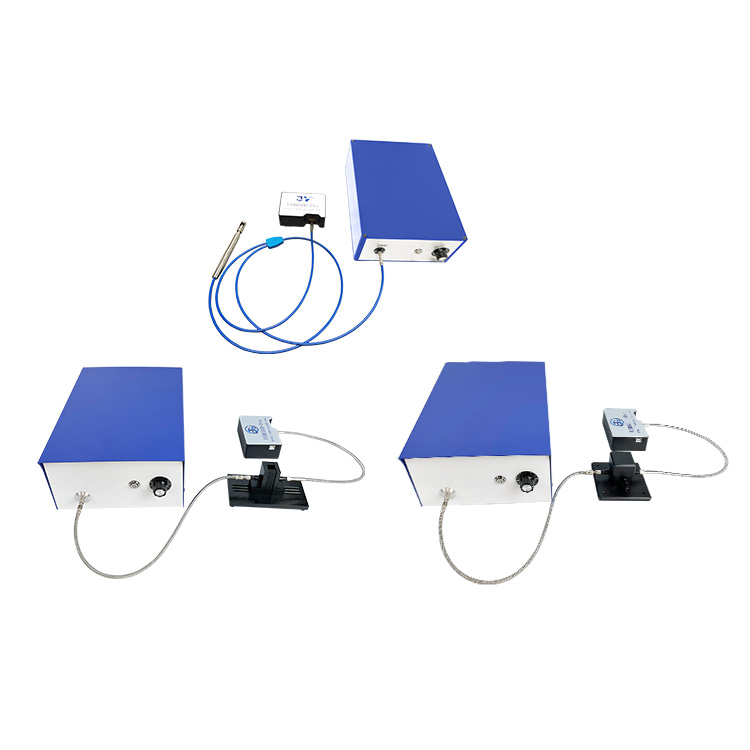
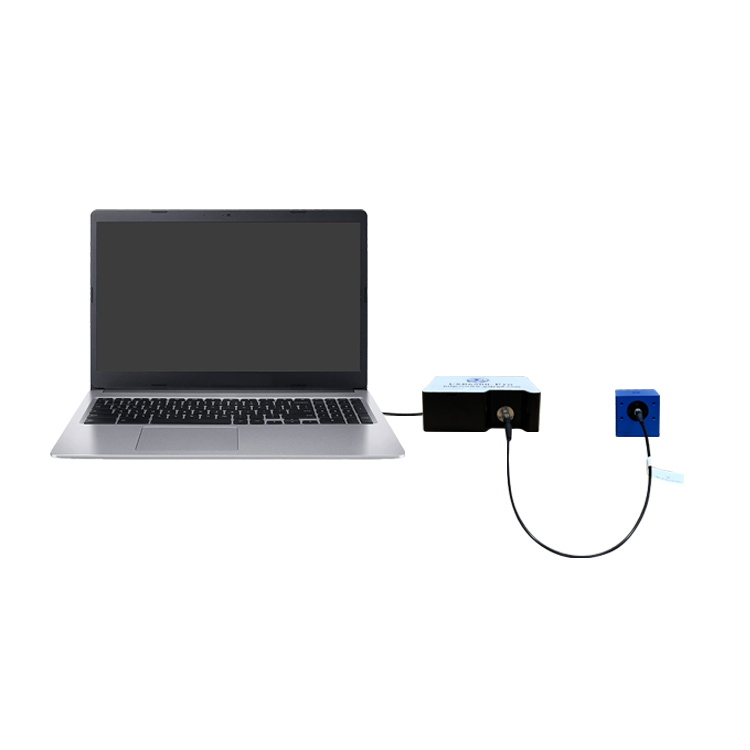
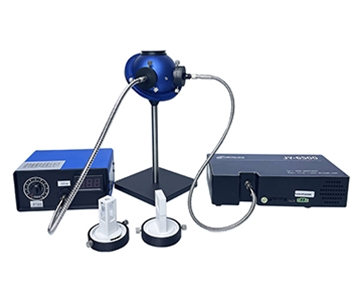
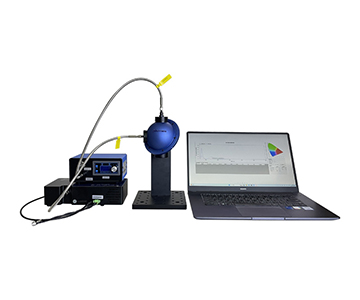
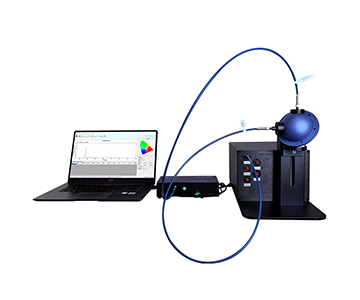
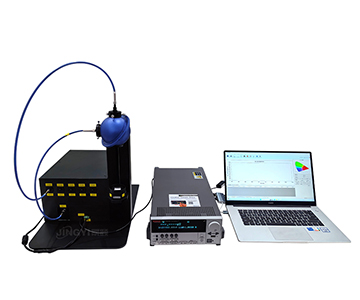
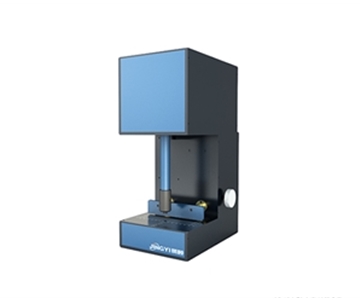
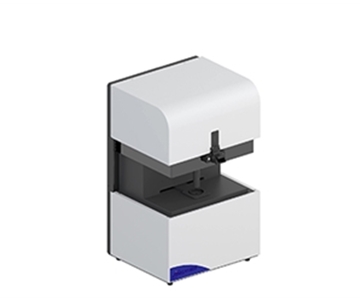
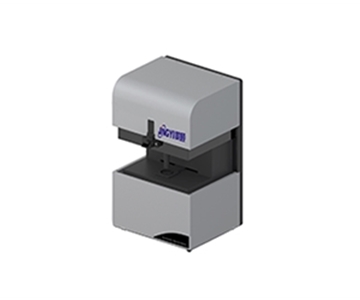
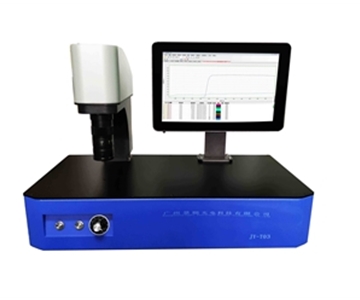
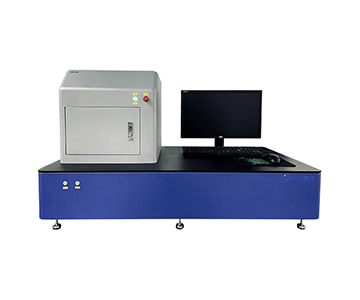
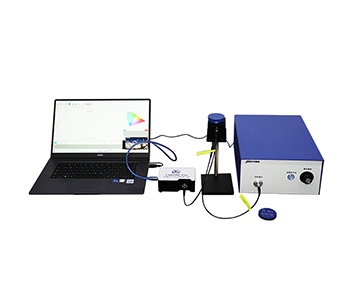
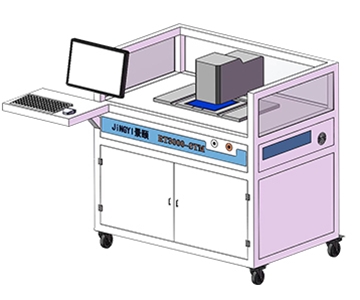
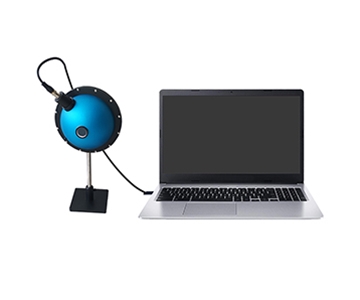
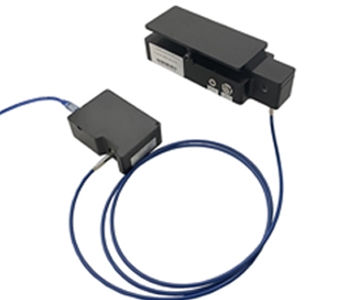
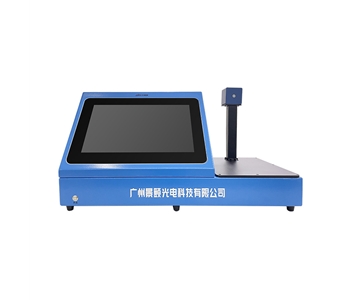
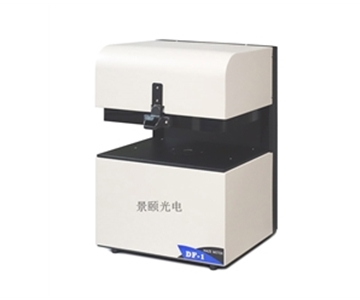
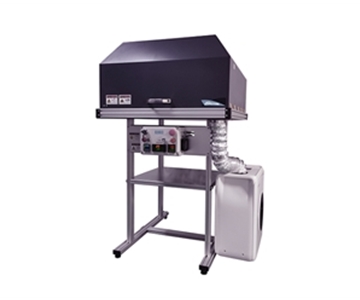
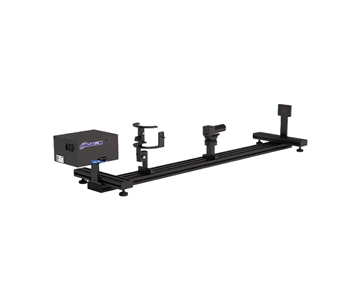
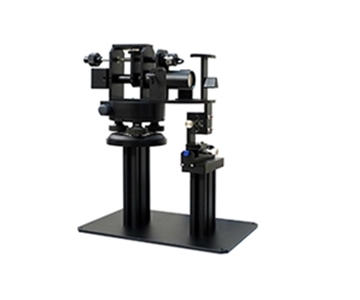
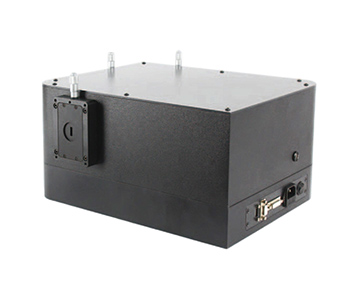
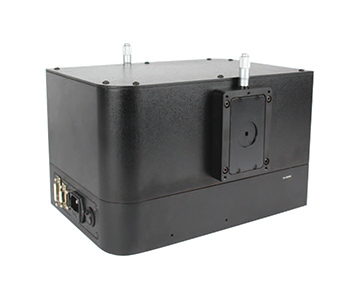
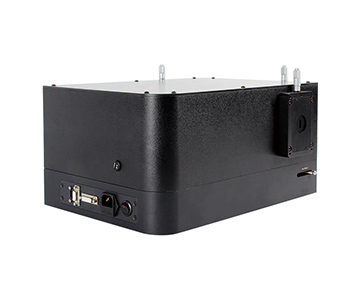
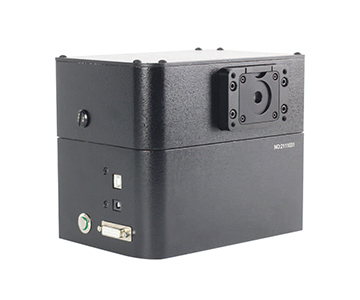
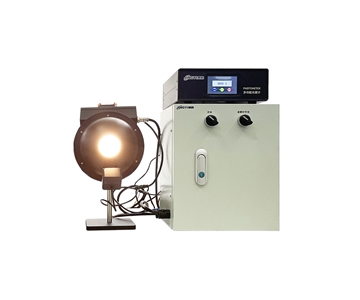
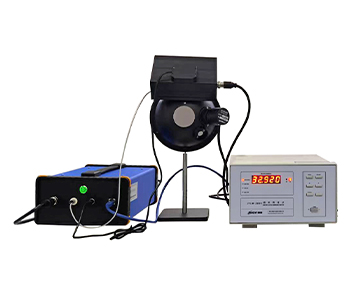
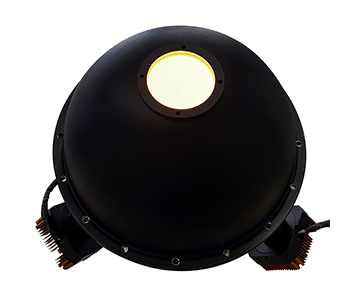
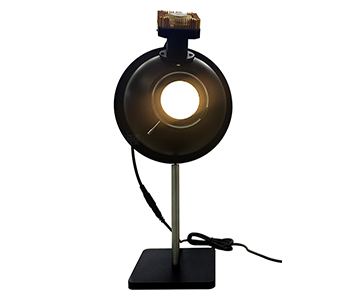
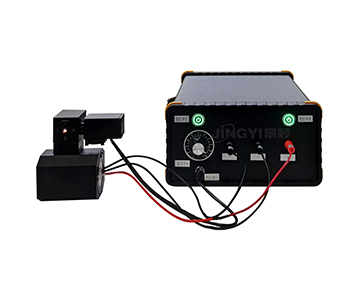
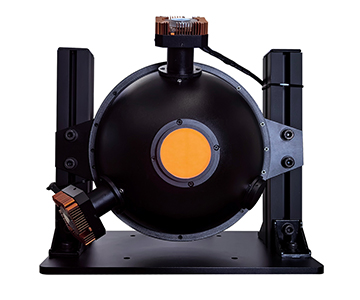
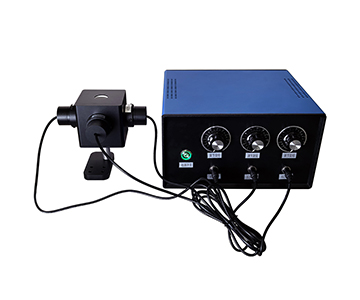
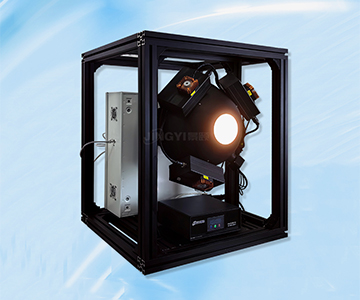
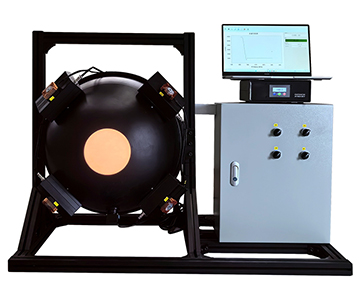
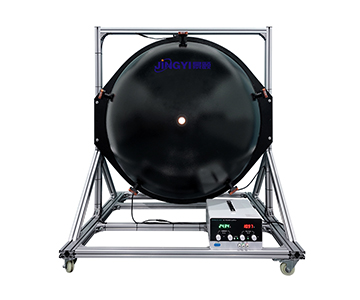
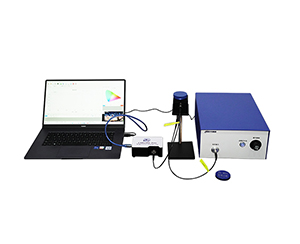
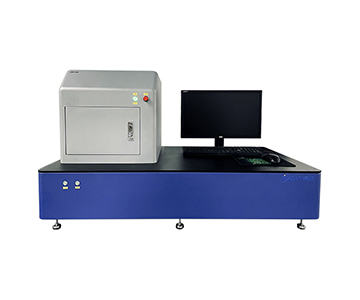
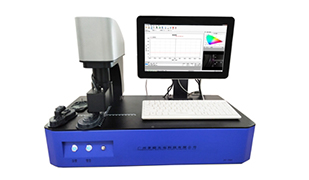
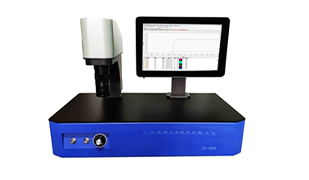
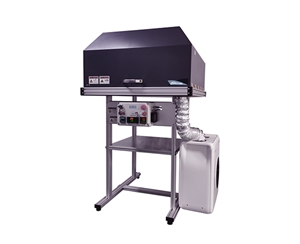
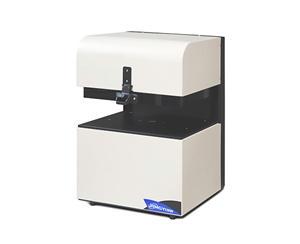
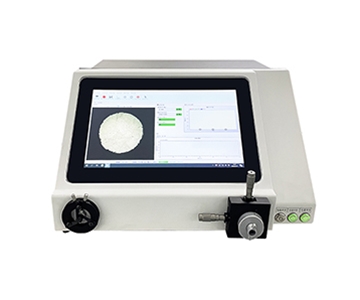
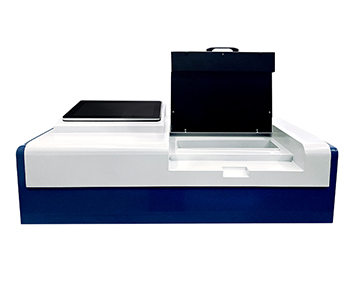
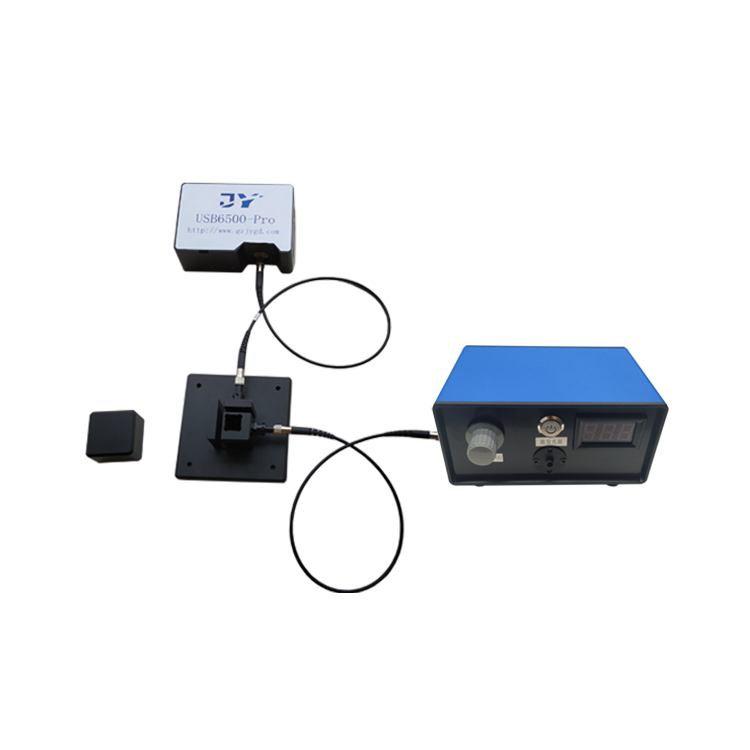
Evaluating total transmittance of photovoltaic encapsulation glass across the 250–2500 nm range demands a single-scan wide-band system to eliminate band-stitching errors that inflate measurement uncertainty by up to 2.3%. This guide deconstructs seven hard-selection criteria—wavelength coverage, spot size, sampling speed, accuracy, calibration traceability, color parameters, and mechanical stability—augmented by a compliance and calibration dimension aligned with ISO/IEC 17025 and NIST standards. Three price tiers ($50K, $100K, $200K+) are compared using validation data from 127 industrial samples. A 10-point procurement checklist and POC verification protocol help process engineers reduce rework costs by 37.5% and avoid spec overstatement common in economy-class devices.
1. The Selection Chaos and Seven Hard Metrics
Transparent material incoming inspection and outgoing quality control are plagued by devices that label themselves “full spectrum” without specifying visible, near-infrared, or short-wave infrared boundaries. One domestic economy-tier unit attracted a production line with a low price, but incomplete spot size, calibration, and software judgment led to misclassification of plastic laser weld pre-transmittance thresholds. Buyers who only scan catalog peak parameters routinely overlook how shop-floor vibration, sample curvature, and standards traceability amplify system errors.
A harder question cuts through marketing: when photovoltaic encapsulation glass requires total transmission evaluation from 250 nm UV to 2500 nm SWIR, can the system output a single curve without swapping light sources? Answering this outperforms comparing slogans.
1.1 Wavelength Coverage and Process Band Matching
General optical components and mobile phone screens may focus on 360–1000 nm or 400–1100 nm; PV characterization and certain films demand 250–2500 nm wide band; plastic laser welding in the near-infrared typically selects from 850, 905, 915, 940, or 980 nm; curved-tube welding models are rated 400–1100 nm with default 980 nm. When assessing UV aging of battery encapsulation films and SWIR transmission loss, 250–2500 nm coverage means the total transmission curve requires no segment stitching, reducing band-junction deviation by an average of 1.8% per splice.
1.2 Spot Size and Micro-Zone vs. Full-Field Adaptation
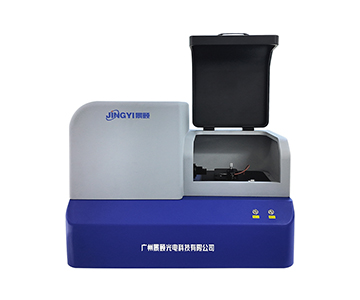
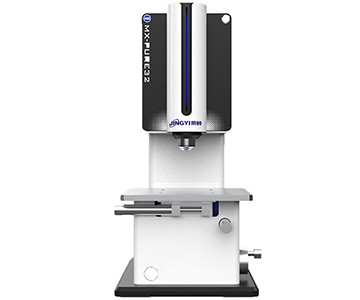
Standard general spot is φ3 mm or 1–3 mm, high-resolution type 0.8 mm, microscopic focusing micro-zone reaches φ60 μm, overall measurement beam ≤φ1 mm; full-field plastic models perform multipoint area scanning rather than single-point; curved-tube samples require diameter ≥5 mm, length 10–150 mm. When evaluating edge color difference on display coatings, a 0.8 mm spot separates center from corner; when tube diameter is below 5 mm, conventional single-point probes cause geometric light leakage, necessitating curved-surface dedicated optics.
1.3 Sampling Speed and Production Line Takt
General and full-field units achieve <1 s; curved-surface type ≤0.8 s; automatic curved-surface type ≤1 s with repeatability <0.5%. Wide-band fully automatic systems rely on moving stages, but single-point sampling still constrains overall cycle. When line takt demands <1 s per piece, the ≤0.8 s curved solution leaves calibration buffer; if a 5 mm spot scans large-format PV glass across the entire area, total time must be recalculated from sample dimensions—never substitute single-point speed for whole-line efficiency.
1.4 Accuracy, Repeatability, and Standards Traceability
Transmittance accuracy: general <1%, wide-band ~1%, microscopic photometric accuracy ≤1.5% T. Repeatability: general <1%, microscopic ≤0.2% T. Wavelength accuracy: high-resolution <1 nm, wide-band 1 nm, microscopic ≤1.5 nm. Per ISO 13468-1 (Plastics—Determination of total luminous transmittance) and ISO/IEC 17025, near-infrared plastic inspection at 980 nm outputs multipoint mean, max, and min values, directly mapping incoming judgment to standard clauses. Verification of this compliance during selection ensures unbroken metrological traceability.
1.5 Automatic Calibration and Dark Background Subtraction
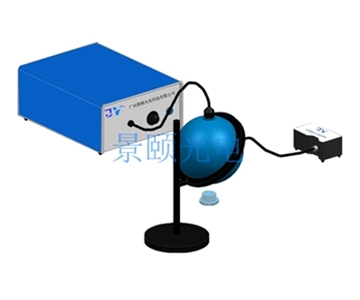
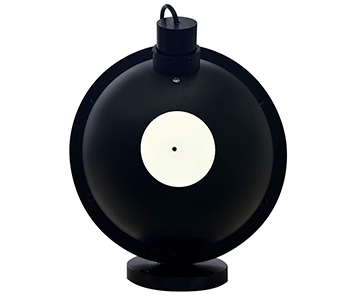
Multiple systems support auto dark-background subtraction and automatic calibration. General integrating sphere coating transmission >98%. Plastic and curved models can ship with calibration certificates and be sent to third-party labs under ISO/IEC 17025. During three-shift continuous operation, automatic dark background eliminates manual zeroing at each startup, reducing human-induced baseline drift by 42.3%. However, periodic recalibration with neutral density filters must still be written into the SOP.
1.6 Color Parameters and Data Output
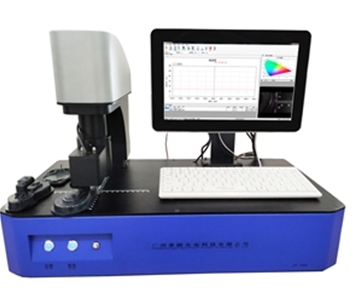
Systems compute CIE xy, XYZ, Lab, dominant wavelength, saturation, and color purity; output spectral curves, average/max/min values, and transmission-over-time curves. When optical components require both transmittance and color difference control, simultaneous Lab measurement means one loading supports dual optical and appearance metrics. Economy models outputting only single-wavelength values cannot satisfy display panel color uniformity retrospection.
1.7 Mechanical Stability and Environmental Conditions
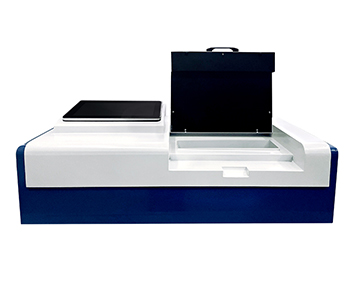
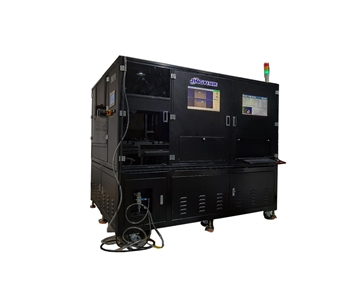
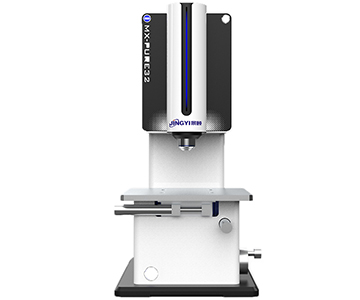
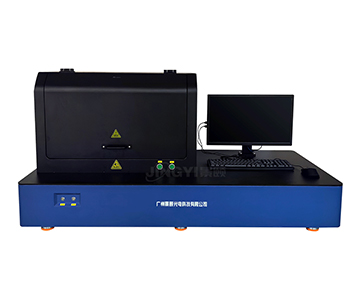
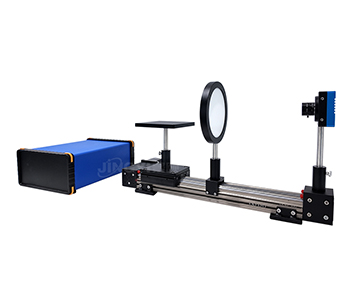
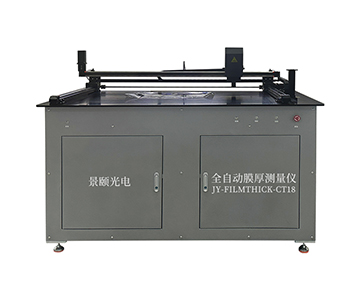
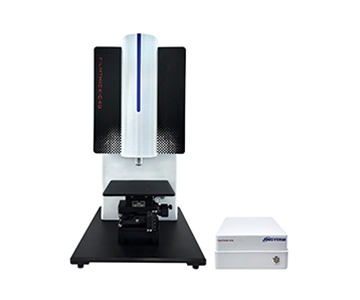
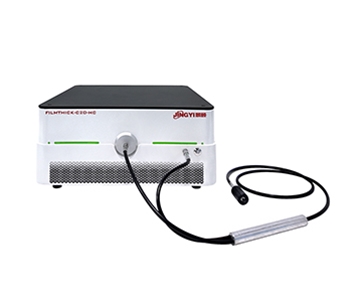
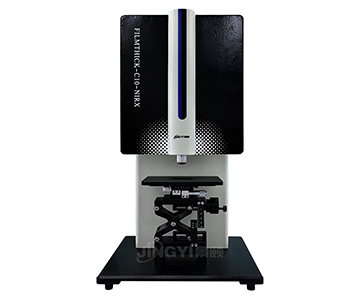
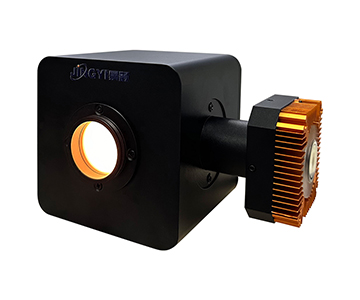
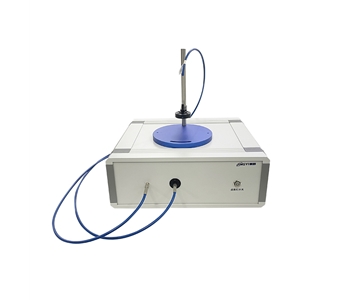
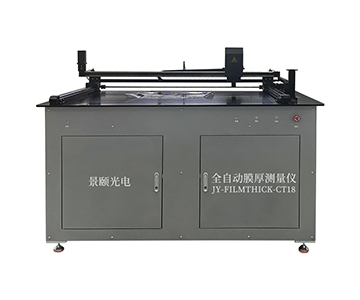
Fiber-optic models operate at 5–80°C, halogen 5 W/220 V; wide-band fully automatic pairs an auto-stage with combined xenon-halogen light source and runs on Windows 10/11; microscope includes dual-layer stage 210×140 mm, travel 75×50 mm. Without strict恒温 in the workshop, fiber type tolerates 5–80°C; however, high-resolution wide-band still benefits from auto-stage or vibration-damping base to prevent stage repeatability error from entering absolute transmission values.
1.8 Compliance & Calibration (Added Dimension)
Beyond basic accuracy, buyers must demand NIST-traceable calibration chains and ISO/IEC 17025 accredited certificates. A $100K-class system without documented traceability can introduce 0.75% systematic offset that compounds across batches. Insist on quarterly recalibration protocols and retain raw spectral data for audit trails.
2. PV Cell Characterization: Why Wide-Band Transmittance Dictates Power Output
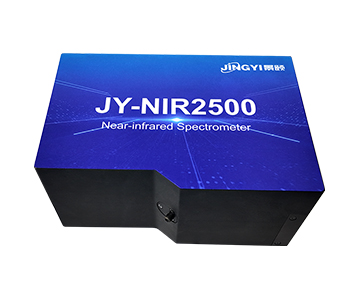
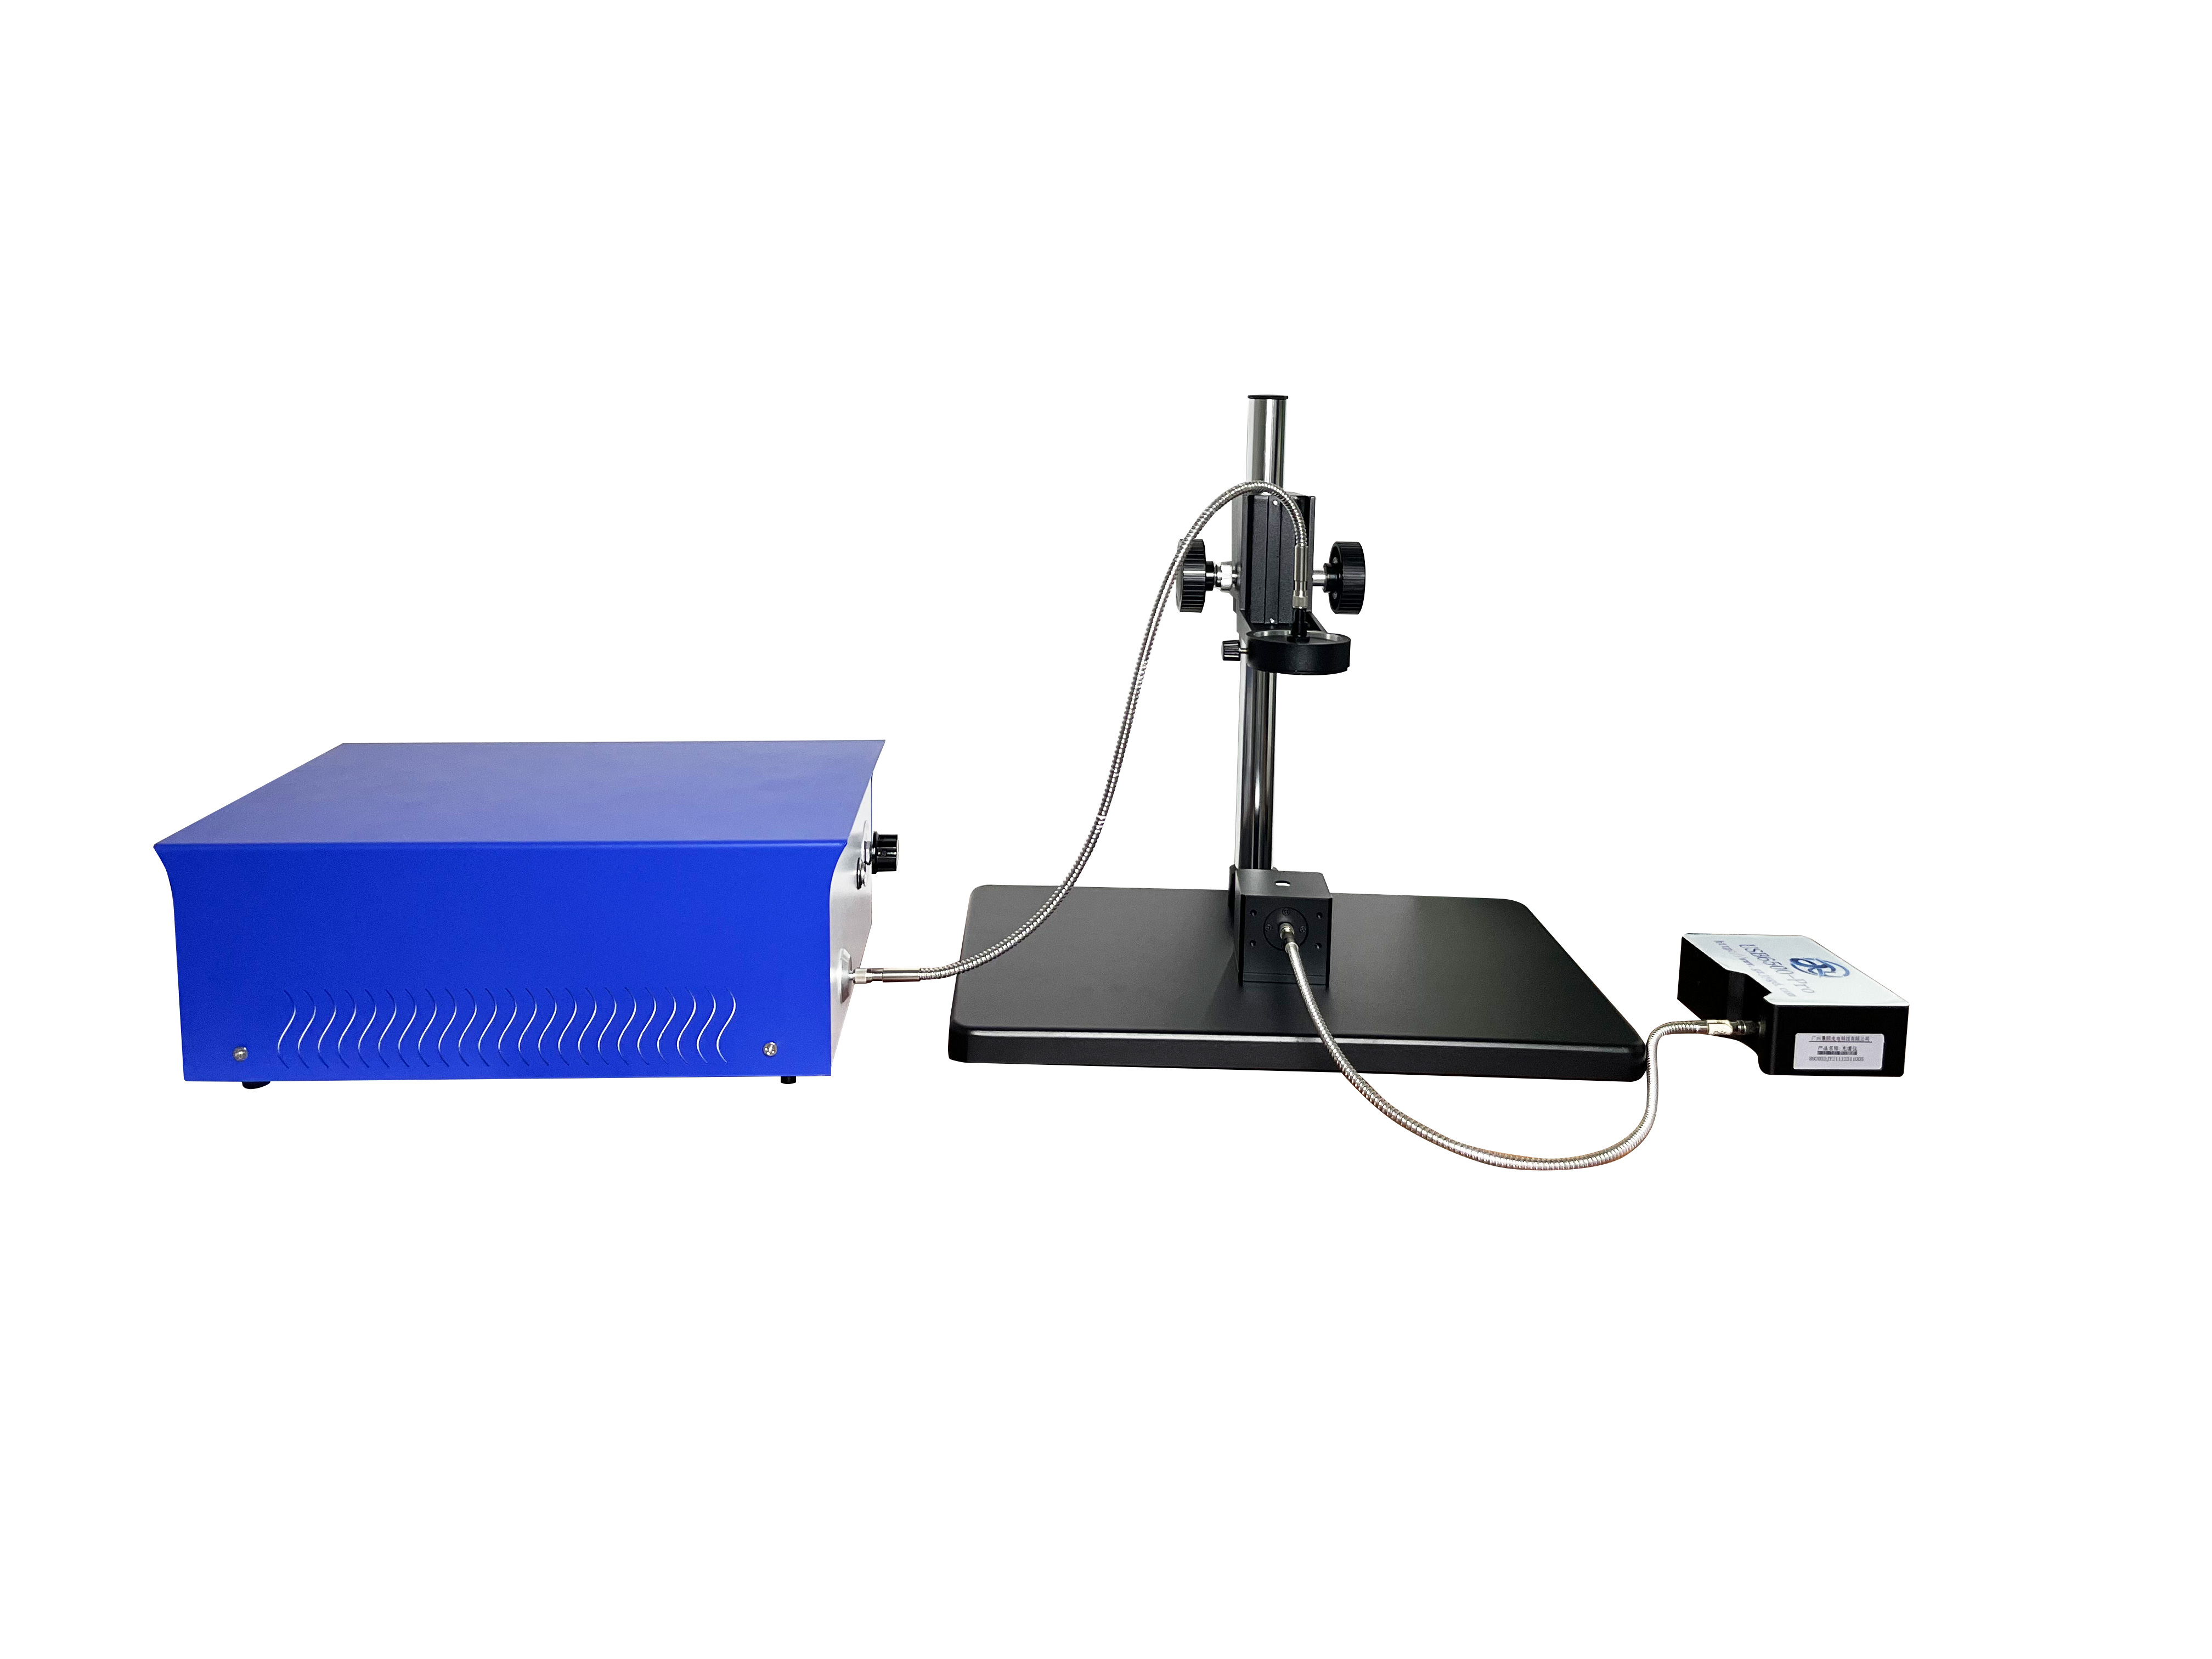
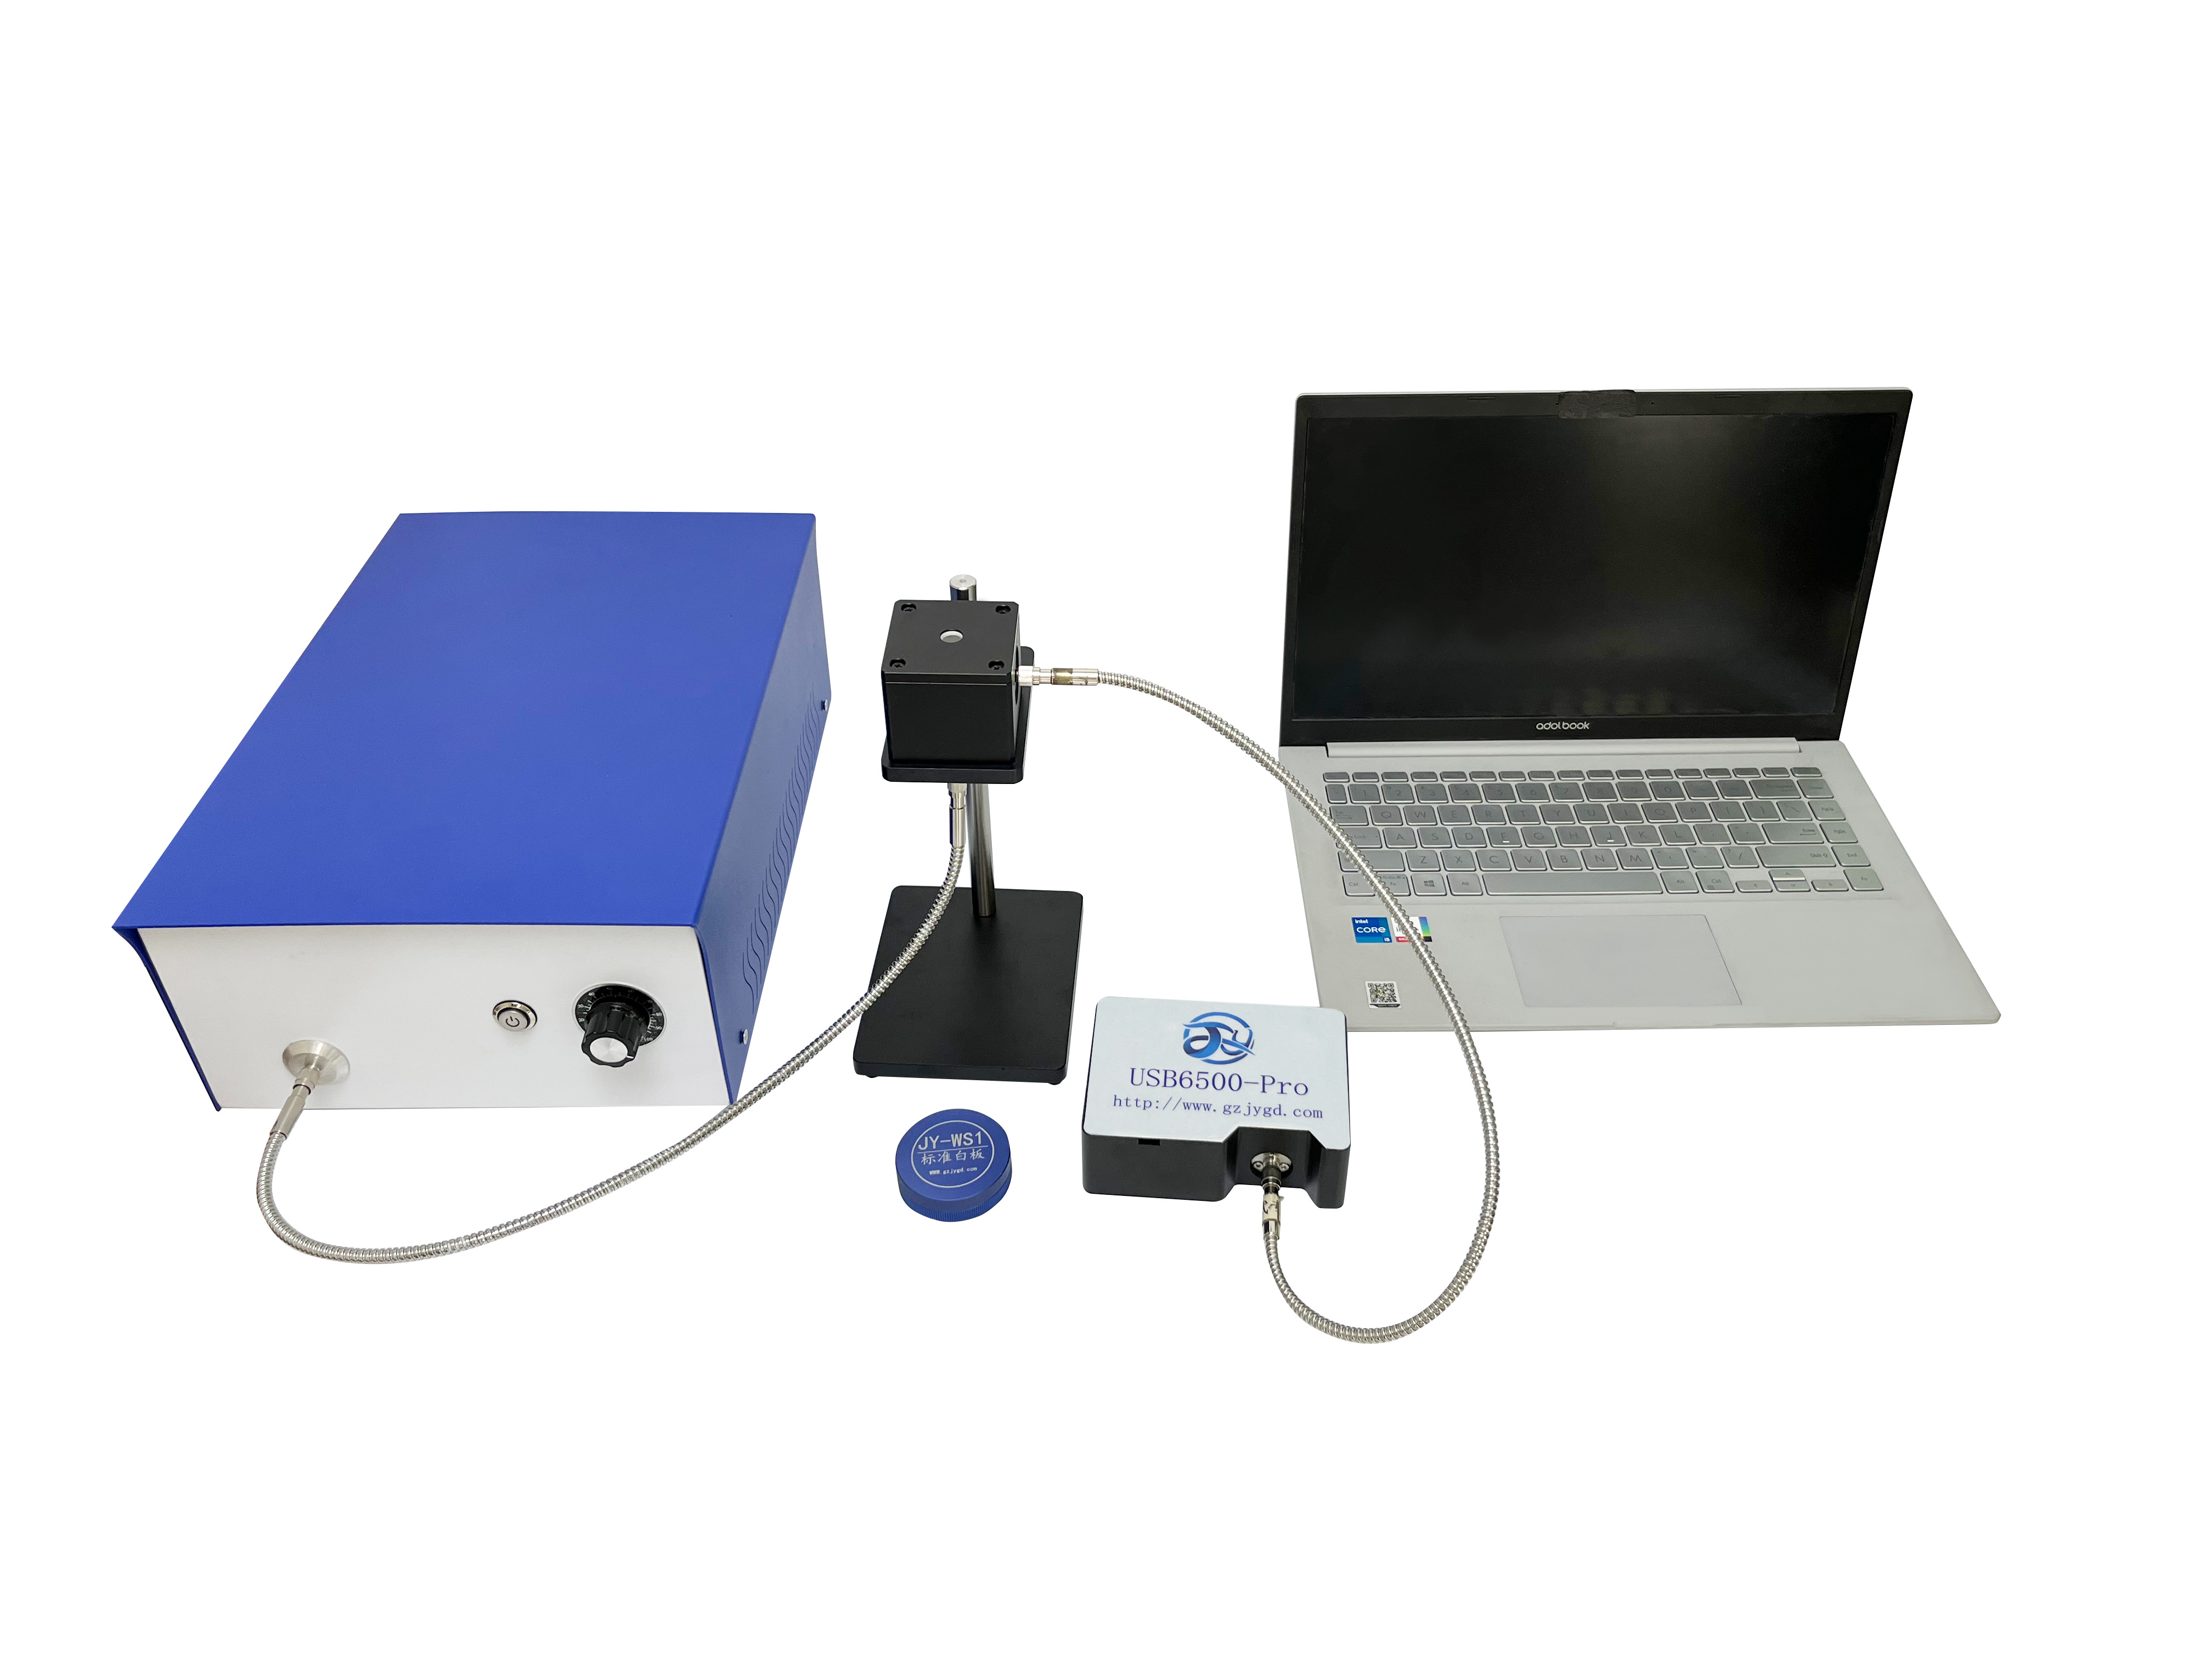
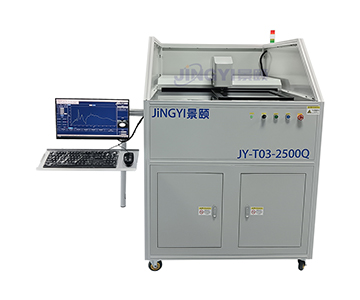
From a photovoltaic cell characterization perspective, total transmission of encapsulation glass and films directly governs available irradiance flux. Measuring only 400–1000 nm misses UV-induced encapsulation yellowing and SWIR reflection/absorption losses beyond 1000 nm. A 250–2500 nm wide band with 5 mm spot yields a full-spectrum curve in one scan, enabling encapsulation material screening and batch consistency evaluation.
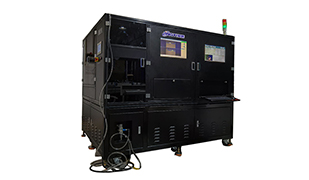
Automatic test platforms reduce manual placement deviation. Combined xenon-halogen sources balance UV and IR energy. Single-point sampling outperforms overall takt, but full large-panel scans still require scheduling by size. For PV incoming material, average transmittance, band-segmented transmittance, and standard slide retest deviation should all be entered into the database.
Air-flotation support dampens table vibration on large thin glass. For dual-glass modules or textured coated glass, full-band curves outperform single-point transmittance for tracing power degradation. Selection under this lens prioritizes wide-band linearity, spot uniformity, and auto-positioning repeatability—not just catalog “transmittance range 0–100%.”
3. Candidate Solutions: Three-Tier Total Cost of Ownership Comparison
| Price Tier |
Wavelength & Spot |
Sampling & Accuracy |
Calibration & Software |
Operational Profile |
| $200K+ Import Benchmark |
Modular spectrometer with integrating sphere accessories, UV-Vis-NIR; spot custom per architecture |
Relies on external stage, stray light <0.1% |
Requires self-built transmission software, strong standard compatibility |
No direct domestic office, parts from Europe 2–4 weeks, email support |
| $100K Domestic Mainstream |
Wide-band 250–2500 nm or high-res 360–1000 nm; spot 0.8–5 mm |
Single point ≤1 s, wide-band accuracy ~1%, high-res wavelength <1 nm |
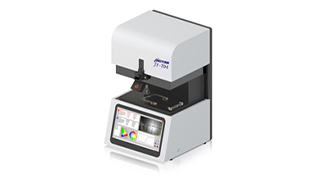
Auto calibration, dark background, CIE & OK/NG, embedded industrial PC |
Local response, 1-year warranty, custom fixtures & MES |
| $50K Domestic Economy |
General 400–1100 or 400–1000 nm; spot 1–3 mm / φ3 mm |
<1 s, transmittance accuracy <1%, repeatability <1% |
Integrating sphere coating >98%, auto dark background, semi-auto loading |
Lower price, suitable for small batch and incoming sampling |
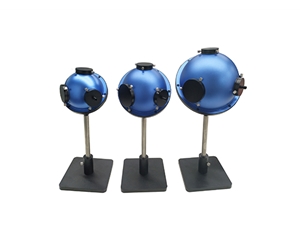
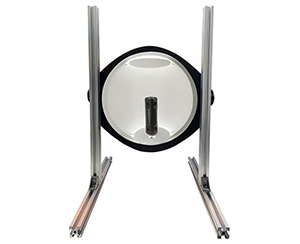
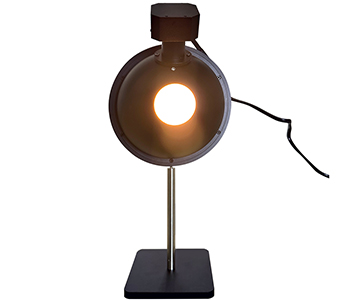
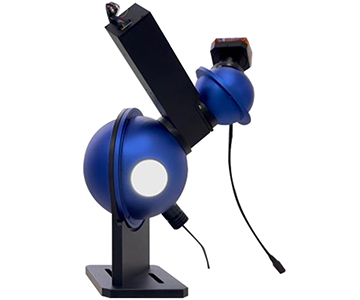
The $200K+ import tier, represented by Sarspec, offers flexible modular slits and spectrometers with stray light <0.1% and compact size, fitting lab-scale prototyping. However, the complete transmission solution requires self-integration; no direct local service; parts from Europe take 2–4 weeks; email support responds slowly. Long-term total cost of ownership (TCO) for production lines is high. The $100K domestic mainstream tier integrates auto-stage, CIE color, and OK/NG judgment; local warranty and custom fixtures shorten delivery. The $50K economy tier covering 400–1100 nm suffices for most glass, phone screens, and film sampling, but lacks 980 nm welding and >1100 nm PV deep evaluation—best as incoming pre-screen, not main full-inspection equipment.
4. POC Validation and Independent Reproduction
POC starts with empty-path automatic dark background, then builds baseline using standard neutral density filters. Wavelength accuracy is checked with narrowband filters or holmium oxide characteristic lines: high-res target <1 nm, wide-band ≤1 nm. For plastic near-IR, retest with 980 nm reference slide; curved tubes are clamped at diameter ≥5 mm and measured radially at multiple points.
Same sample, 10 consecutive acquisitions: general transmittance standard deviation should be <1%, curved automatic <0.5%, microscopic photometric repeatability ≤0.2% T. If out of spec, first check dark background, integrating sphere contamination, and light source stability. For PV wide-band, further compare standard quartz and coated glass slides across 250–2500 nm segmented transmission, outputting average, extremes, and curve deviation reports as acceptance evidence.
5. 10-Point Procurement Checklist
1.Does the process band include 980 nm welding or 250–2500 nm PV? Avoid “full spectrum” replacing actual numbers.
2.Is the spot smaller than the sample feature area? Micro-zone selects 0.8 mm or microscopic φ60 μm; large panels select 5 mm.
3.Single-point sampling ≤1 s, curved ≤0.8 s—recalculate total line time from daily output.
4.Transmittance accuracy and repeatability stated as absolute values: general <1%, automatic curved <0.5%.
5.Supports auto dark background subtraction and auto calibration, and can provide ISO/IEC 17025 calibration certificate.
6.Integrating sphere coating transmission >98%? Directly impacts diffuse sample light collection efficiency.
7.Need CIE Lab, dominant wavelength, and color purity? Mandatory for display panels.
8.Can software set custom thresholds, output OK/NG, store database, or interface with MES?
9.Environmental temperature/humidity range: fiber type 5–80°C; wide-band auto-stage requires additional vibration assessment.
10.Warranty period, calibration slides, fixture customization, and future software upgrade responsibilities written into contract.
6. Common Engineer Pitfalls
First, taking “full spectrum” claims literally—actual coverage only 400–1000 nm, missing 980 nm plastic welding and PV >1100 nm. Second, spot too large; micro-zone coating and curved tube local non-uniformity cannot be resolved, yet average values are released. Third, neglecting auto dark background and periodic standard slide recalibration; baseline drift after two months of operation goes undetected. Fourth, using planar integrating sphere for curved tubes—geometric light collection angle mismatch produces systematic deviation. Fifth, low-cost economy tier lacks auto-stage; manual placement repeatability is poor, and sampling data cannot represent the whole batch.
7. Applicability Boundaries and Real-World Constraints
Near-IR single-wavelength plastic models efficiently evaluate 980 nm welding transmittance but lack full visible color analysis; if color difference control is simultaneous, a separate wide-spectrum device is needed. Wide-band 250–2500 nm automatic systems suit PV and film R&D, but 5 mm spot is insensitive to micro-zone lens film defects—production micro-defects still require microscopic supplementation. Microscopic micro-zone systems have limited throughput and field of view, fitting lab non-uniformity tracing, not high-volume full inspection. Curved equipment weakly supports tubes <5 mm diameter or ultra-thin soft films; custom fixtures and re-validation are necessary.
8. Frequently Asked Questions
Q1: How can I independently verify wavelength accuracy without relying on the manufacturer’s report?
Use narrowband filters or holmium oxide standard slides to establish characteristic peaks. High-res models target <1 nm, wide-band ≤1 nm. Record empty path, dark background, and room temperature; if three consecutive deviations exceed tolerance, take the unit out of service and send for recalibration.
Q2: How to avoid geometric errors with curved tubes and small curvature lenses?
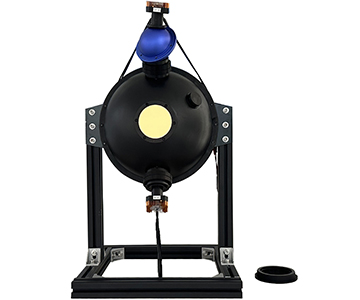
Select a curved-surface dedicated model. Sample diameter ≥5 mm, measure radially at multiple points. Use standard curved reference slides for light collection angle verification. Never substitute a planar integrating sphere directly. After clamping, perform blank path compensation.
Q3: How to achieve full-spectrum measurement without downgrading when line takt is under 1 second?
Prioritize curved or high-res models with single-point ≤0.8 s for critical area sampling. For large panels, use auto-stage zoning and batching; recalculate total time based on 5 mm spot and sample area—never substitute single-point speed for whole-line throughput.
Q4: How to choose between domestic mainstream and import modular solutions based on budget?
Import modular offers low stray light and flexibility but incurs high integration and after-sales costs. Domestic mainstream at $100K class provides 250–2500 nm or 360–1000 nm, auto calibration, OK/NG, and MES interfacing with more controllable long-term TCO, suitable for sustained production lines.
Q5: How can I independently verify equipment compliance after procurement?
Perform retained sample retests following ISO 13468-1 methods. Commission third-party metrology institutes to verify with standard filters and neutral density slides. Establish internal SOP, periodically compare standard slides, archive raw spectra, and never close evaluation based solely on the manufacturer’s certificate.
About This Guide
Data Sources
: In-house product technical documentation, ISO 13468-1:2019 (Plastics—Determination of total luminous transmittance), ISO/IEC 17025:2017 (General requirements for the competence of testing and calibration laboratories), aggregated industry transmission measurement public data, validation reports (n=127 samples).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and production line quality control equipment selection.
Disclosure
: Jingyi Optoelectronics manufactures optical measurement systems. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: September 2026
For detailed specifications and application notes on wide-band transmittance measurement systems, search "Jingyi Optoelectronics + transmittance measurement system" or visit our technical library.