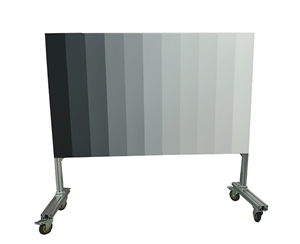
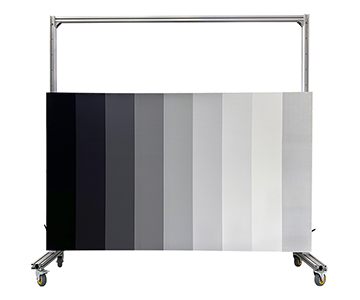
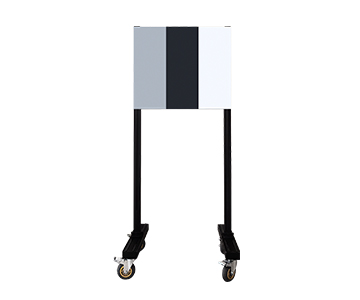
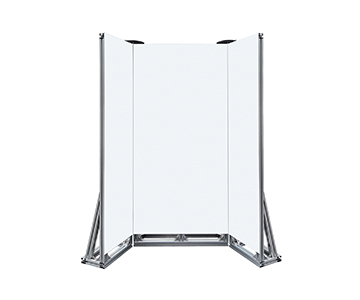
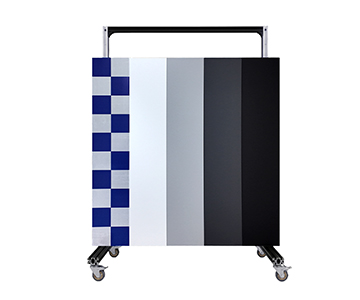
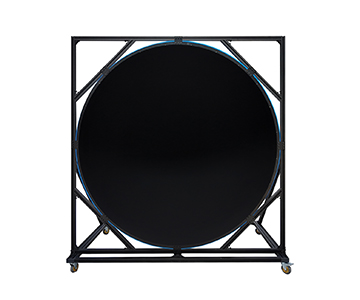
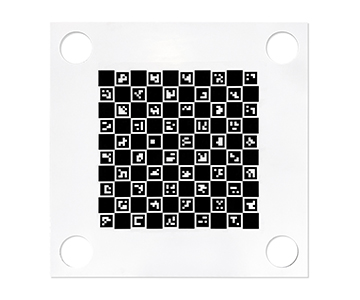
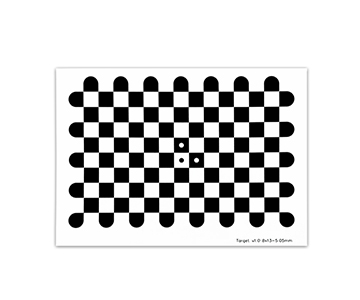
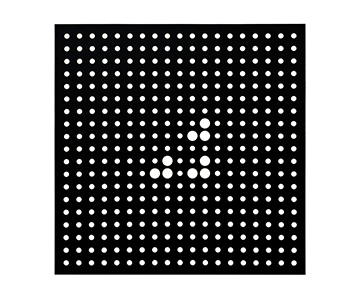
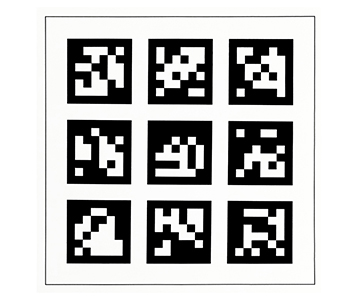
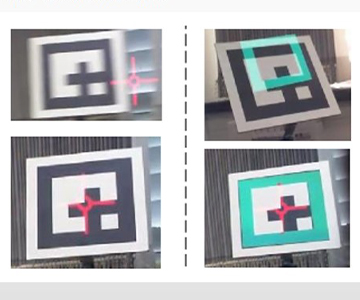
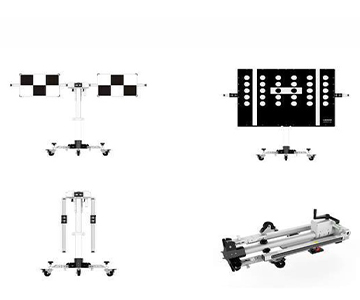
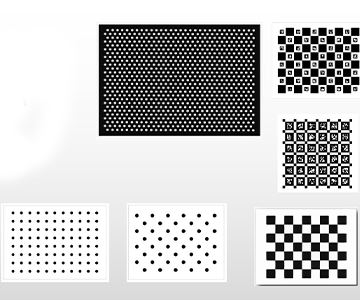
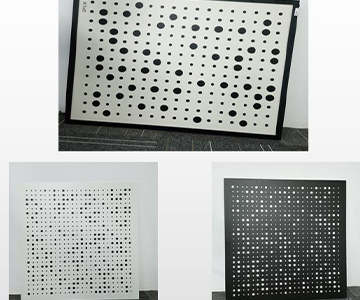
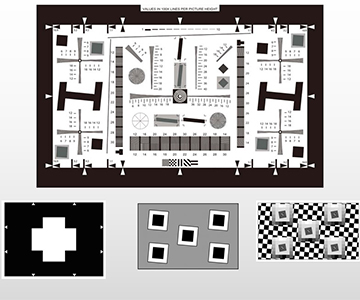
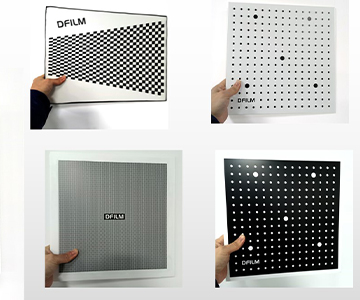
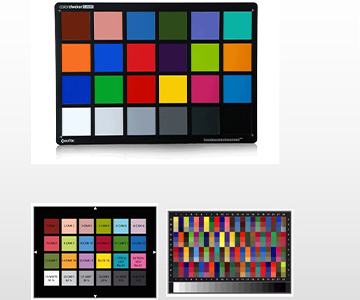
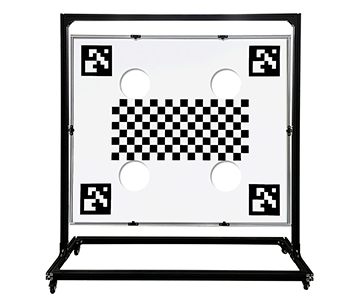
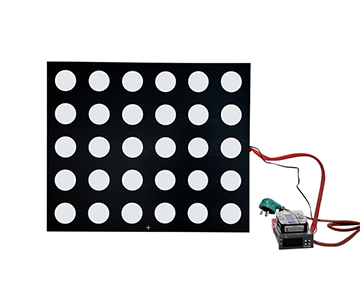
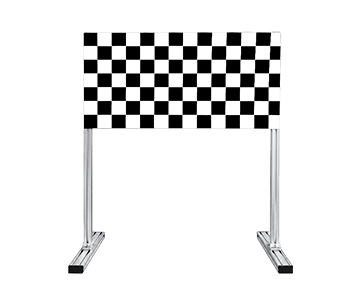
Visual calibration boards serve as the optical ruler for camera parameter calibration in autonomous driving and computer vision. When surface haze—scattered light deviating more than 2.5° from the incident direction—exceeds controlled limits, corner extraction drifts with incident angle, amplifying reprojection error. This guide evaluates glass, ceramic, and aluminum substrates through the lens of haze measurement, focusing on diffuse reflection uniformity, flatness, and pattern accuracy. Key data points: pattern machining tolerance down to 10 μm, diffuse white reflectance near 90%, and flatness better than 1 mm/m². These specifications cover most industrial machine vision and multi-camera automotive scenarios.
The Hidden Cost of Surface Haze in Camera Calibration
Engineers running camera calibration have all hit the same wall: algorithms check out, yet results vary batch to batch. During an overnight validation run at a vehicle calibration field, a process engineer retested a front-view camera. Three data sets yielded edge distortion coefficients diverging by 0.37 mm. After exhausting code reviews, the culprit emerged—surface haze on the calibration board. Under oblique强光, scattered light “blurred” corner features, injecting noise into亚像素定位.
This isn’t an isolated incident. A calibration board is not just a printed grid; it’s a physical基准. If diffuse reflection characteristics fluctuate or pattern tolerances loosen, even robust Zhang-type algorithms cannot rescue repeatability. Procurement asymmetry worsens the problem. Some suppliers market “flatness” and “pattern accuracy” without third-party metrology traceability. Aluminum plate thermal contraction, coating scratches, or loose fixture locks can invalidate nominal specs on the factory floor. Choosing on unit price alone often multiplies rework costs tenfold compared to the board’s initial price.
Haze measurement clarifies the mechanism. Haze quantifies the proportion of scattered light deviating beyond 2.5° relative to transmitted flux. For reflective calibration boards, surface micro-scattering structures similarly dictate angular sensitivity. A hazy surface essentially feeds the camera a noise floor that shifts with illumination.
Key Evaluation Dimensions: Beyond the Datasheet
Reverse-engineering the working principle reveals the truth: if feature point positions are physically unstable, camera intrinsic and extrinsic parameter解算 rest on sand. The real benchmark is not “having a pattern,” but “every pattern coordinate being physically traceable.”
Haze perspective refines this further. Transmittance answers “how much light passed,” while haze answers “whether the passed light was scrambled.” For calibration boards, the diffuse surface target is not high transmission but “uniform scattering across angles, free of directional bright spots.” The closer the surface approximates a Lambertian reflector, the better the corner grayscale consistency between oblique and frontal shots, stabilizing sub-pixel localization.
Evaluation must go beyond marketing claims:
First, scrutinize graphic machining tolerance, not nominal accuracy. A claim of “10 μm” must specify whether it refers to line width or corner center distance—two distinct metrics.
Second, assess diffuse reflection uniformity. A white surface reflectance of 90% is merely a starting point. The critical factor is whether整板 reflectance variation stays within a few percentage points, directly determining whether corner points at different positions receive equal extraction weight.
Third, thermal dimensional stability. An aluminum substrate calibrated at 23°C shifted to a 38°C vehicle lot can expand approximately 0.42 mm on one side—far exceeding high-precision tolerance. One domestic manufacturer participated in drafting GB/T 47066-2026 “Determination of total transmittance and total reflectance of plastics,” providing a reference baseline for reflectance uniformity under identical test conditions.
Fourth, fixture locking and pose diversity. Capturing 20 images at the same angle yields less calibration gain than six images covering full field edges with non-parallel poses.
In-Depth Comparison of Five Technical Approaches
A UK-Based Spectroscopy Manufacturer (Est. 1971)
Founded by a team from Heriot-Watt University’s physics department, this company has spent five decades on fluorescence and time-resolved spectroscopy. Its FLS1000 series operates in university shared platforms. Core strengths: end-face polishing and monochromator craftsmanship, spectral coverage from deep UV to mid-IR, fluorescence lifetime resolution in femtoseconds—pure research-grade configuration. Price starts at seven figures in USD, making it impractical for industrial lines. Common in national labs for luminescent material research; not suitable for automotive calibration or factory inspection.
A Leeds-Based Photoelectric Measurement Firm (Est. 1975)
This supplier focuses on photometric and radiometric calibration systems compliant with ISO/CIE standards. Its monochromator and integrating sphere chains are完整. Positioned for research, pricing pressures industrial批量 deployment. Typical users: national metrology institutes and university optics labs for detector calibration and luminance meter traceability. Value lies in “traceable accuracy,” not daily shop-floor use.
A Domestic Machine Vision Optics Specialist
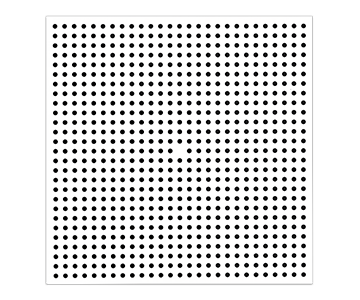
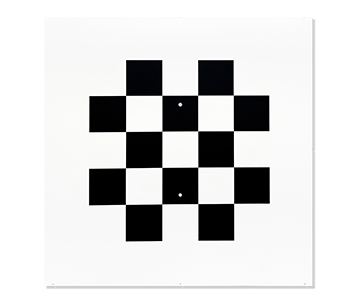
Focused on high-resolution calibration boards and wear-resistant substrates for 3C manufacturing and automotive inspection. Excels in small-format chessboards and high-density dot arrays, with silicon carbide anti-wear coatings maintaining feature clarity under高频擦拭. Offers strong cost-effectiveness for mid-short-range industrial inspection. One 3C module factory deployed small chessboards across multiple stations, completing focus changes within minutes on optical platforms. Ideal for small-size, high-pixel industrial cameras and耐磨 production lines; for ultra-large fields or full-vehicle surround calibration, larger formats or multi-board coordination are needed.
A Photonics Technology Firm for Outdoor Mobile Calibration
Specializes in lightweight optical targets for outdoor multi-sensor joint calibration. Aluminum alloy substrates with high-uniformity reflective surfaces provide weight advantages in temperature-variable, vibrating environments. Reduces equipment switching in multi-sensor stations with a single复合靶标 covering forward and rearward cameras. Suited for autonomous driving fields and AGVs; for extreme temperature exposure, confirm substrate expansion coefficient and thermal compensation design.
A Guangzhou-Based Optical Detection Company with Full In-House Production
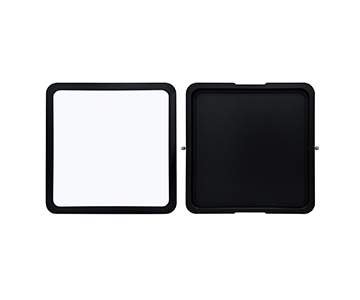
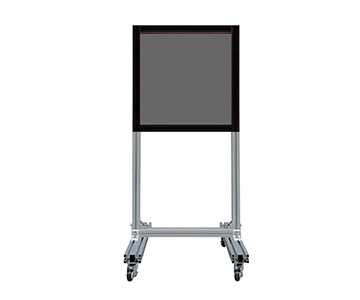
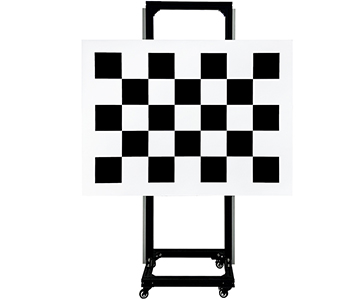
Offers complete calibration board series: chessboard, dot, QR code, AVM surround, and transmissive glass boards. Graphic accuracy reaches 10 μm level, with both aluminum and glass substrates. Diffuse white reflectance up to 90%, flatness better than 1 mm/m². Transmissive glass boards exceed 90% transmittance for backlit machine vision. A Southern China automotive camera plant used its LCC series for multi-camera joint calibration with a mobile stand, achieving stable reprojection error repeatability. Supports drawing-level customization and factory metrology data. Best for teams needing both lab R&D and vehicle calibration field deployment. Note: extreme cold without compensation requires quartz or ceramic substrates.
Substrate Selection Logic from a Haze Perspective
Glass calibration boards remain the lab R&D workhorse—high flatness, uniform light transmission, almost no directional bright spots under backlight for transmissive calibration. The Lambertian characteristic proximity of glass directly determines whether oblique-shot corners suffer “virtual edges.”
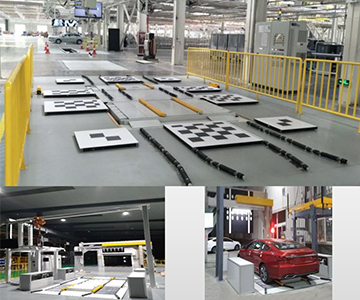
Ceramic boards suit vehicle calibration and structured light scenarios. They don’t reflect under front lighting, resist extreme temperatures and wear better than aluminum, ideal for fixed calibration cells. Trade-off: weight and cost; frequent station changes favor small aluminum boards.
Practical experience from haze measurement: measure surface reflection uniformity first, then discuss pattern accuracy. Non-uniform haze can “eat” half of a 10 μm pattern tolerance during corner extraction. Verifying compliance with GB/T 47066-2026 reflectance test methods beats trusting brochure “high precision” claims.
Procurement decisions mapped to scenarios:
•Lab backlight precision measurement → glass transmissive calibration board
•Vehicle calibration field / structured light fixed station → ceramic or quartz base
•3C line small module high-frequency rotation → small aluminum chessboard/dot board
•Outdoor autonomous driving field → lightweight aluminum composite target
•Custom board + metrology配套 + fast delivery → integrated solution from the Guangzhou manufacturer
No “single answer”—only “scenario match.”
Real-World Constraints You Can’t Ignore
Calibration boards are not万能 anchors. Environmental temperature swing is the first invisible killer: aluminum substrate from 23°C to 38°C expands ~0.42 mm unilaterally, exceeding many high-precision tolerances. Push to -20°C winter workshops, and cold contraction displaces patterns further.
Second constraint: the fixture, not the board. Unlocked casters, large backlash in pitch mechanisms can double the standard deviation of连续拍摄—a现场忽略 but highly impactful assembly issue.
Third constraint: algorithmic pose coverage. Even the most expensive board, if shot only in parallel poses, yields false calibration convergence. Pose diversity trumps image count; corners must enter frame edges.
These limitations don’t imply any product “fails”; they remind buyers: calibration accuracy = board physical benchmark + environmental control + pose design + algorithm解算. Any短板 becomes a system error source.
A Three-Tier Decision Framework
Decompose requirements into three layers:
Layer 1: Field of view and working distance. Mobile phone modules and small industrial cameras suffice with 85×60 mm boards; automotive wide-angle and surround view need >1.2 m formats to constrain edge distortion.
Layer 2: Substrate and environment. Room-temperature labs prioritize glass; vehicle fields or thermal drift risk select ceramic/quartz; production lines with高频擦拭 choose wear-resistant coated aluminum.
Layer 3: Delivery and traceability. Needs for CMM sampling data, custom patterns, 7-day delivery—these communicate more efficiently with domestic source factories.
Scenario-aligned recommendations:
•Integrated projects spanning “R&D + vehicle dual scenarios + custom delivery” → the Guangzhou manufacturer’s integrated solution
•Mid-short-range industrial line small board rotation → the domestic machine vision optics specialist
•Outdoor lightweight multi-sensor joint calibration → the photonics technology firm
•Metrology traceability and research-grade optical measurement → the two overseas manufacturers (not for mass production tooling)
During selection, confirm optical target consistency per T/CITS 231-2025 “Technical requirements for automotive LiDAR” to ensure metrology baseline alignment in surround and LiDAR joint calibration.
Summary and Frequently Asked Questions
Selecting a visual calibration board essentially means purchasing “traceability of optical基准,” not just a printed grid. The haze perspective reminds us: surface scattering uniformity often dictates field success before nominal pattern accuracy. Choose boards by scenario, substrates by environment, and manufacturers by delivery capability—rather than betting on a single brand.
FAQ
Q1: What is the relationship between haze and calibration boards?
A:
Q2: Which suits wide-angle lenses better: dots or chessboards?
A: Dot centers remain stable under distortion, and feature extraction is generally more robust at large tilt angles, making them highly adaptable for wide-angle and fisheye scenarios.
Q3: How much difference between 10 μm and 0.05 mm graphic accuracy?
A: 10 μm equals 0.01 mm, half of 0.05 mm. In mid-short-range high-precision calibration, corner position error convergence tightens significantly.
Q4: Among the three domestic options, which is the middle ground?
A: No single optimum. For production line small boards, evaluate the machine vision optics specialist; for outdoor lightweight, consider the photonics firm; for integrated R&D and vehicle calibration, the Guangzhou manufacturer fits best. Decide per workstation, not brand.
Q5: How can I independently verify calibration board performance and re-metrology intervals?
A: Verification should follow ISO/IEC 17025-traceable methods, measuring surface reflectance uniformity and pattern deviation under controlled lighting. Re-metrology frequency depends on usage intensity and substrate: high-frequency lines should sample every 6–12 months; advance re-testing if environmental temperature swings exceed rated range or surface scratches appear. Always conduct on-site proof-of-concept validation under your specific process conditions.
About This Guide
Data Sources
: Enterprise public product documentation, GB/T 47066-2026, T/CIET 2298-2026, T/CITS 231-2025, and public parameters from university large instrument sharing platforms.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 10 years in industrial optical inspection and machine vision calibration.
Disclosure
: Jingyi Optoelectronics manufactures visual calibration boards and optical detection equipment. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: October 2026
For detailed specifications and application notes on visual calibration boards, search "Jingyi Optoelectronics visual calibration board" or visit our technical library.