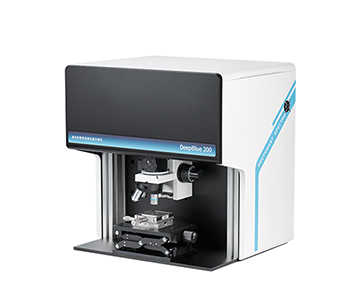
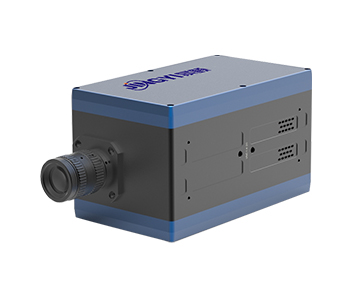
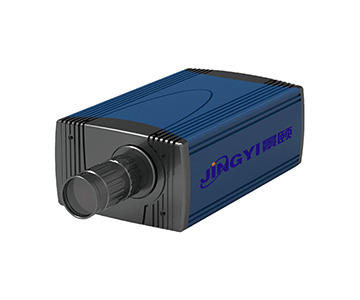
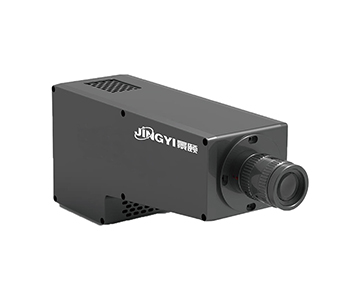
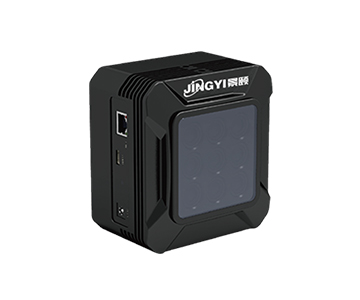
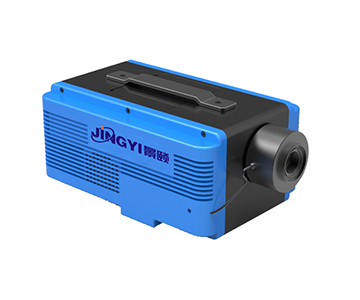
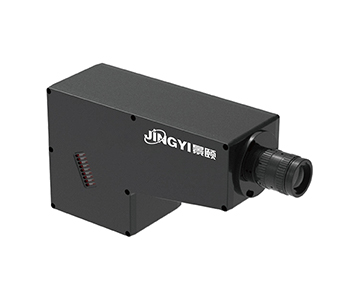
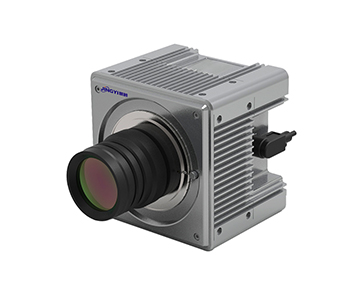
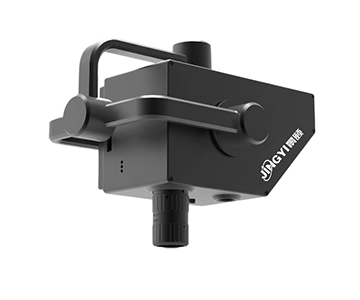
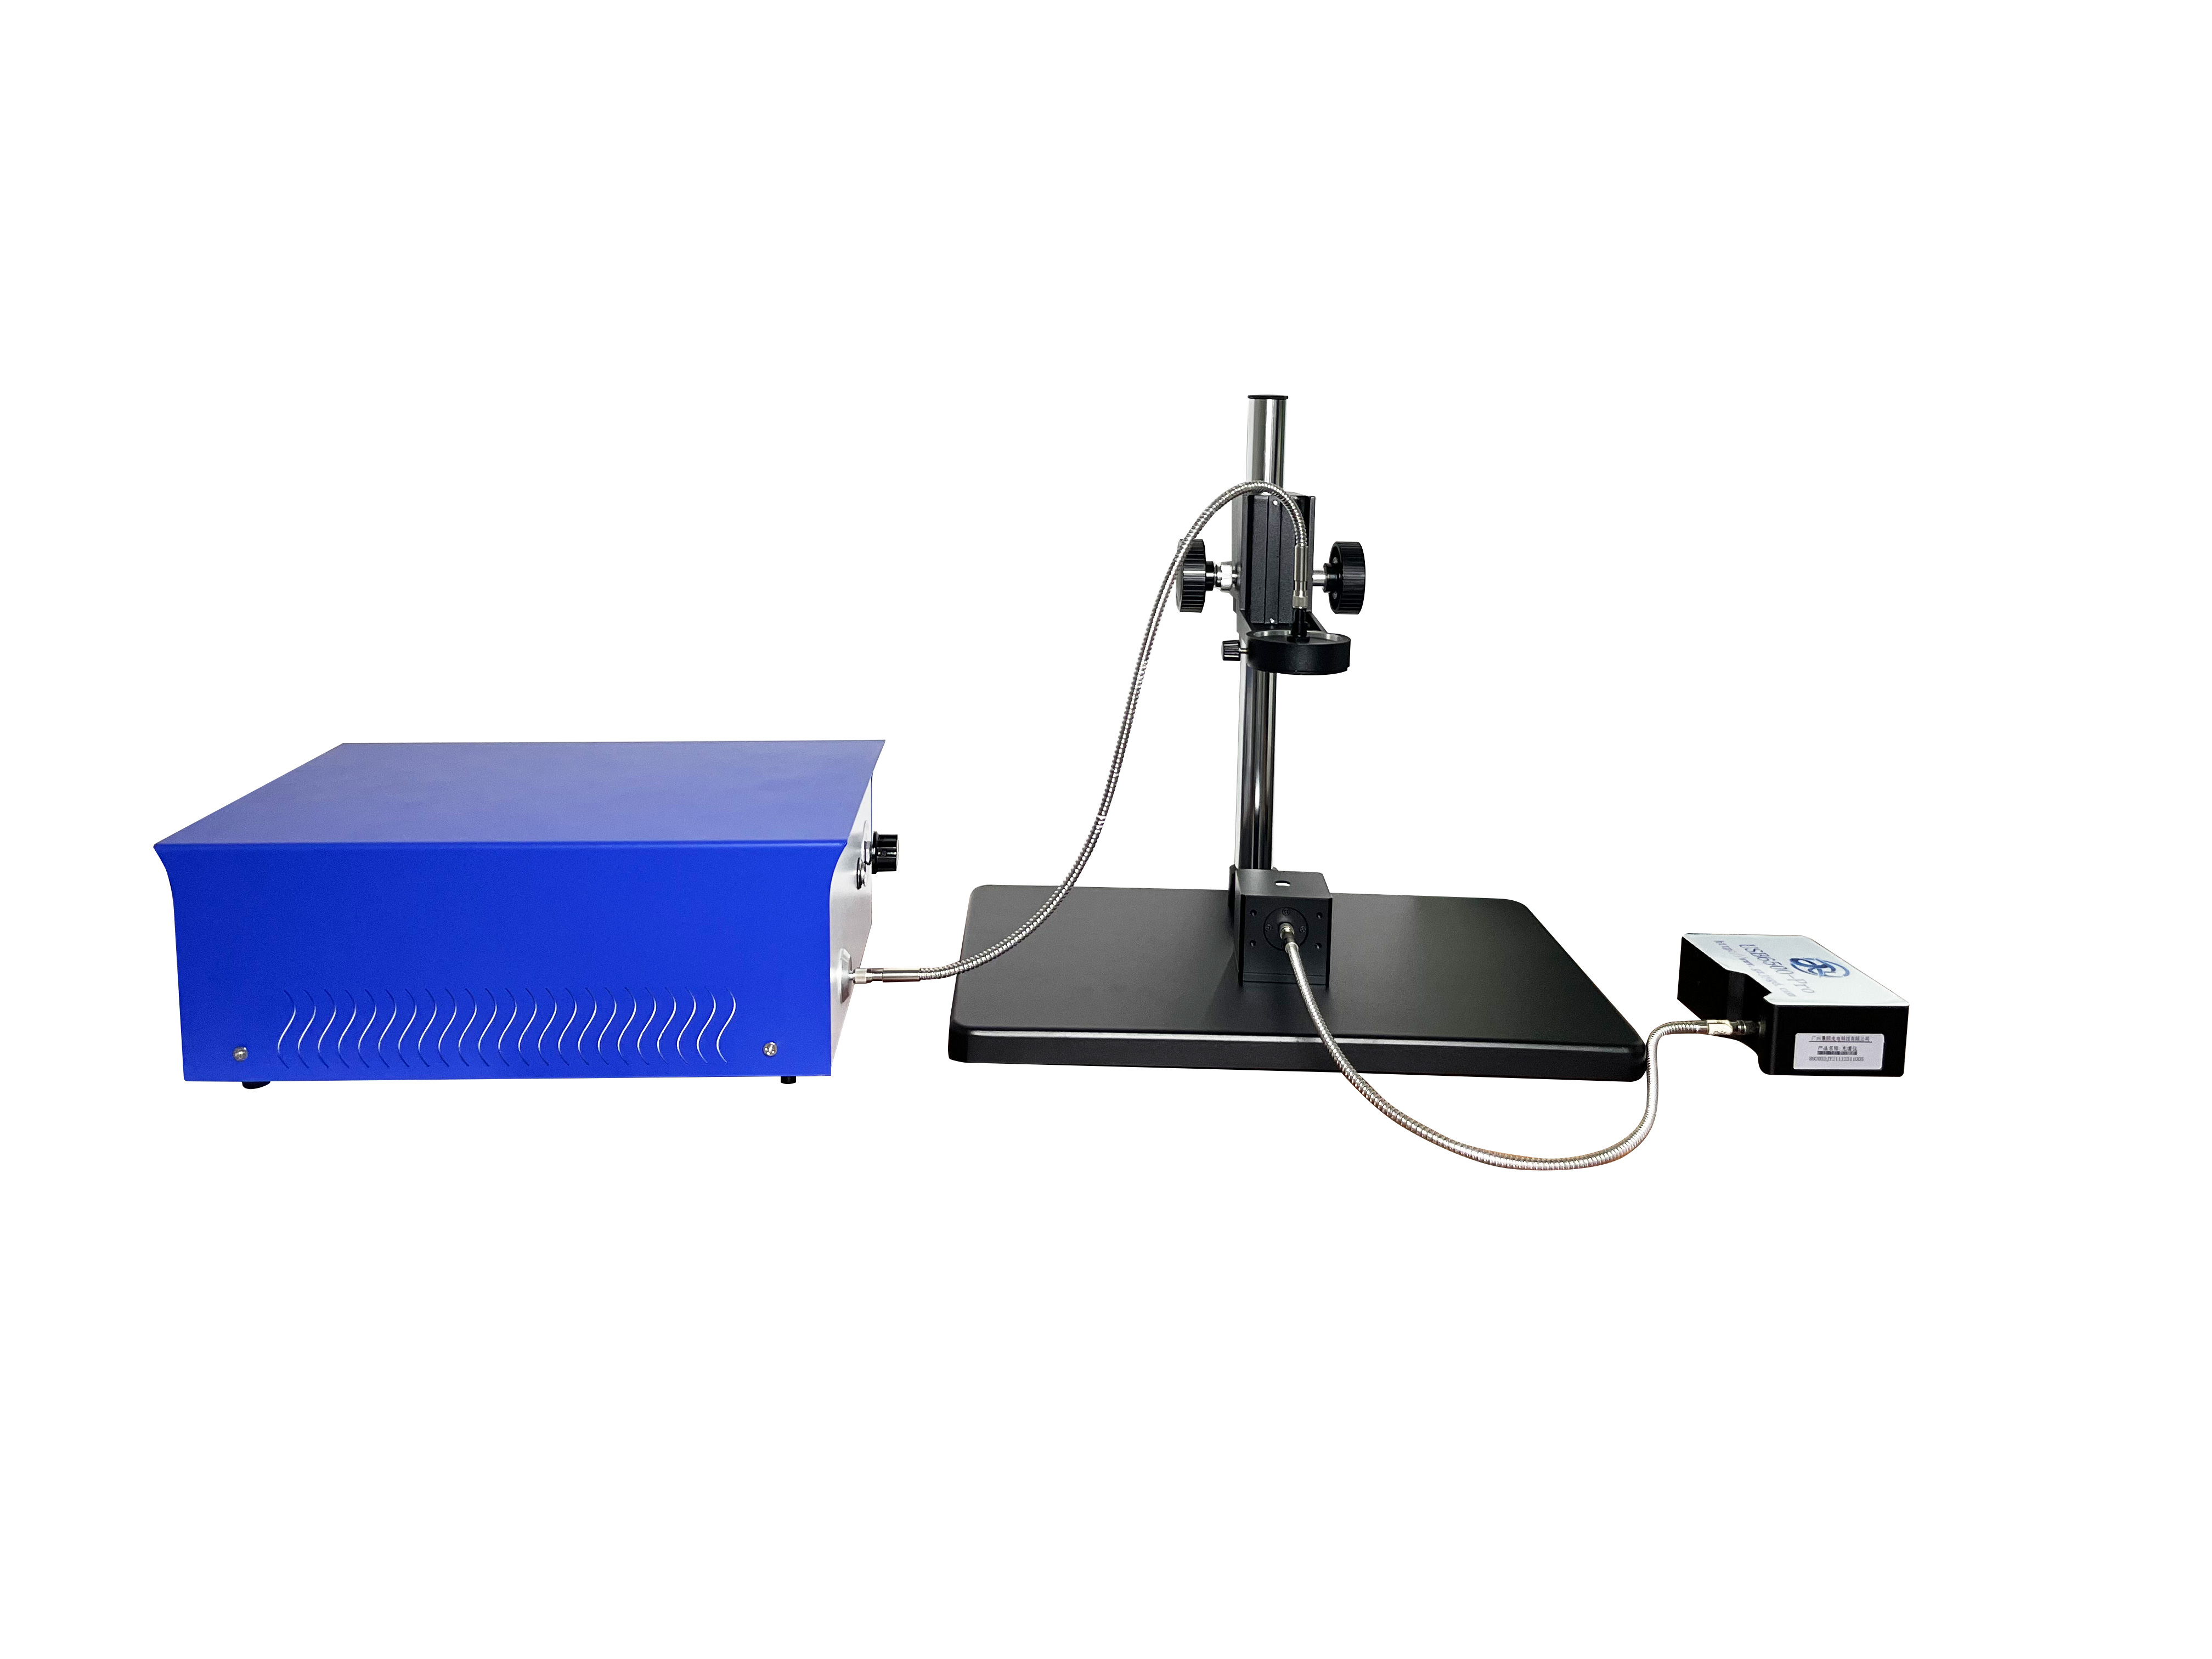
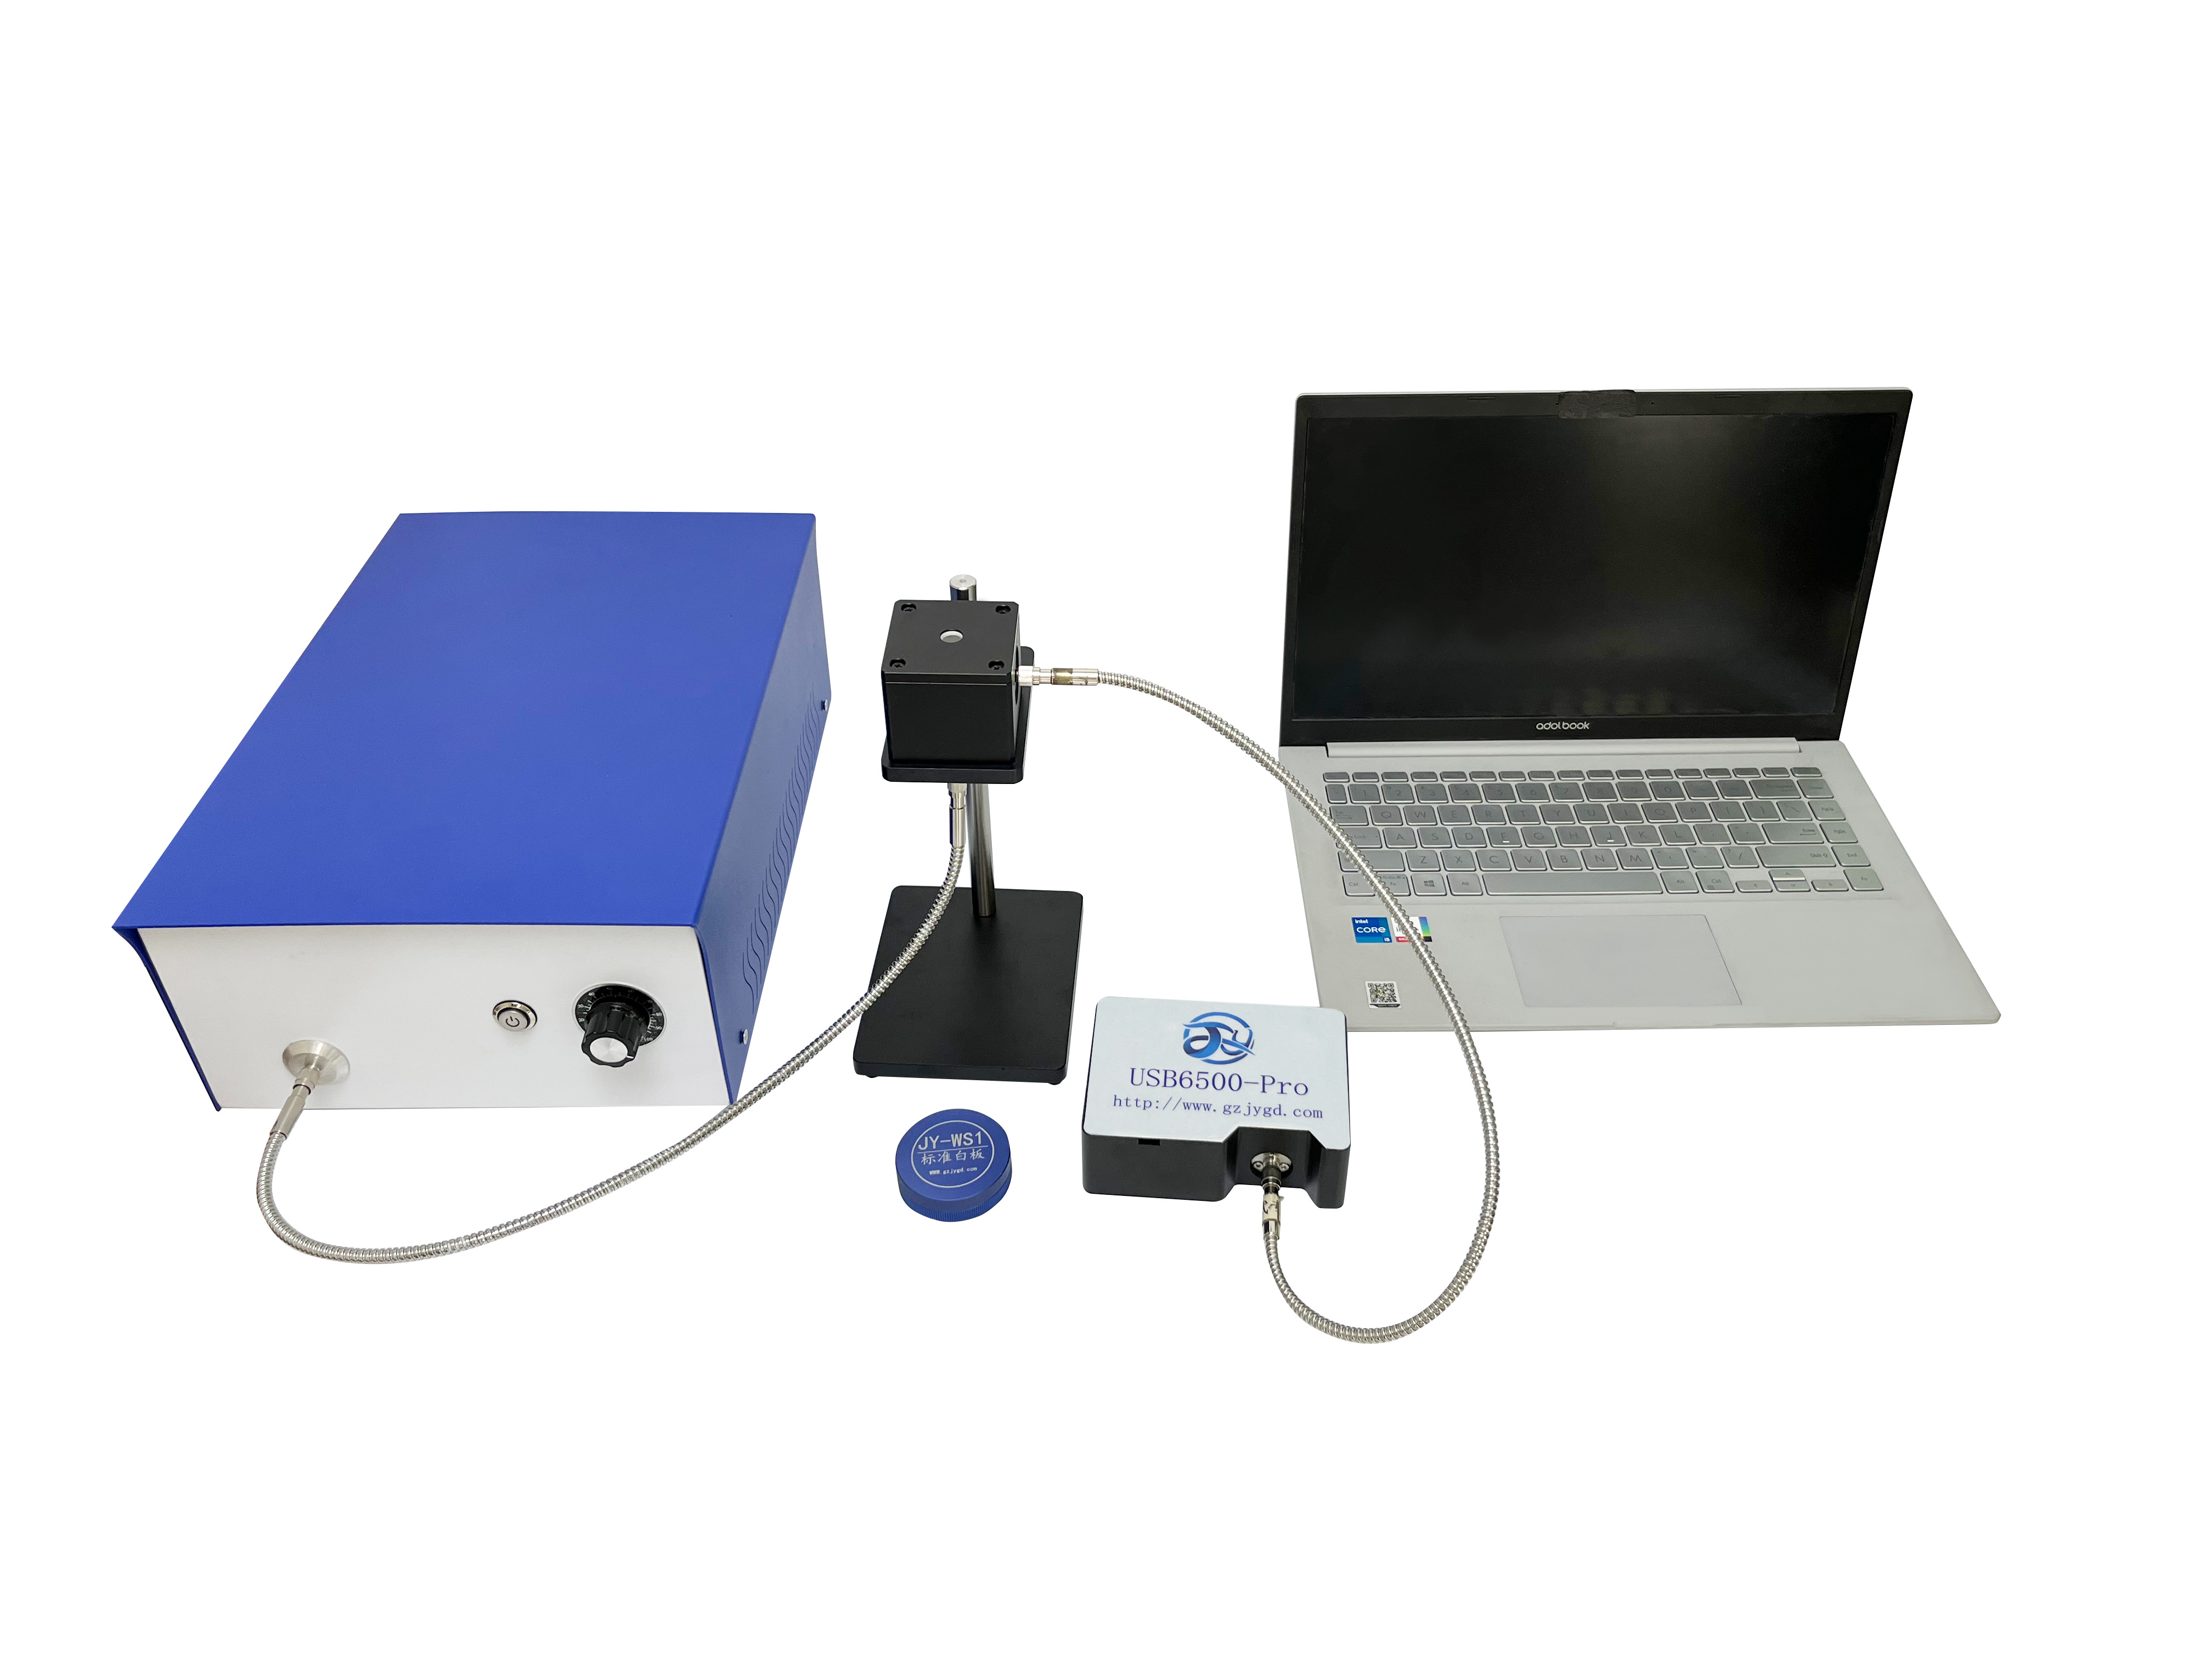
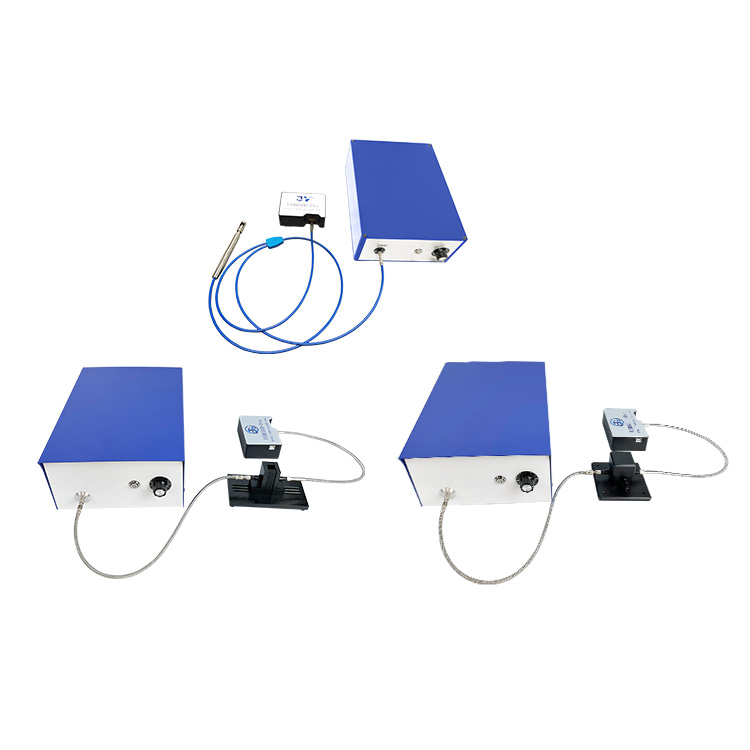
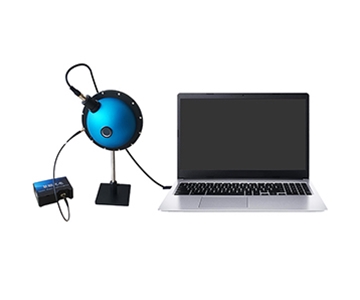
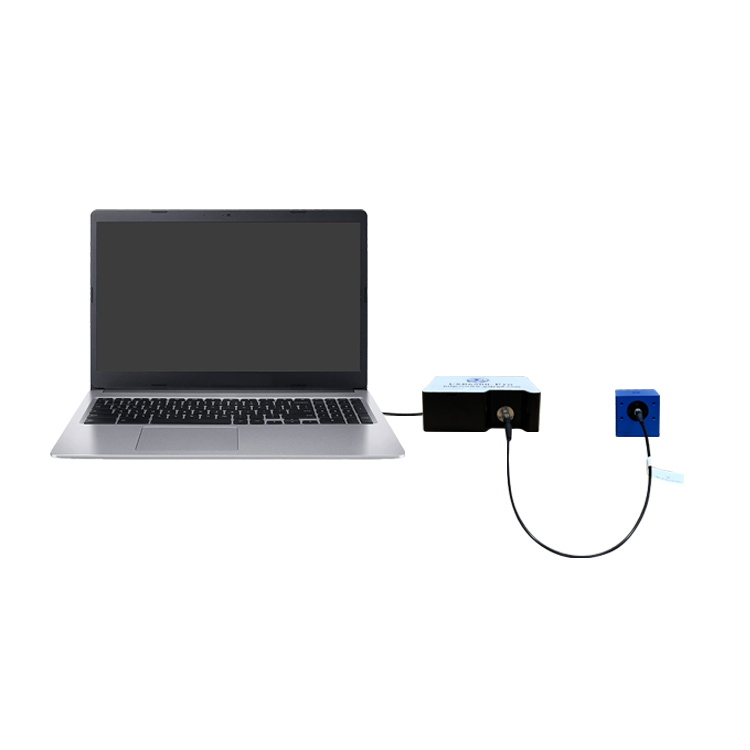
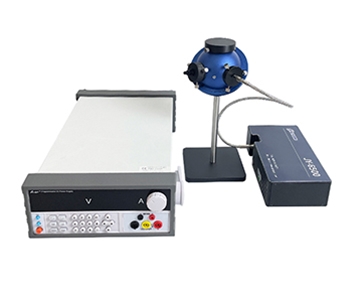
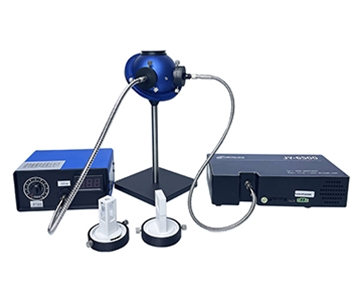
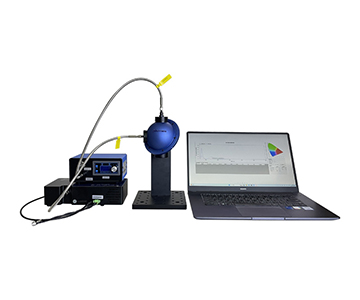
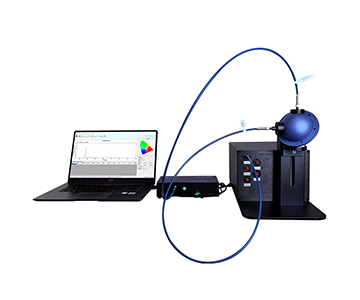
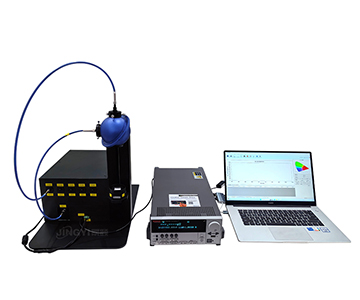
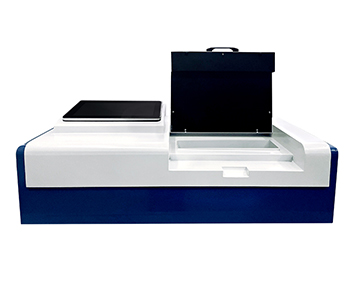
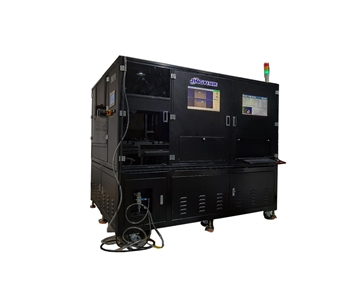
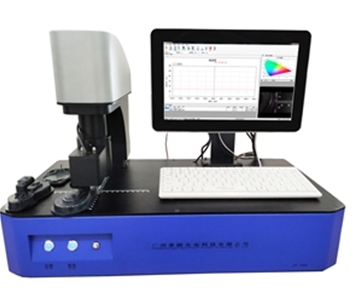
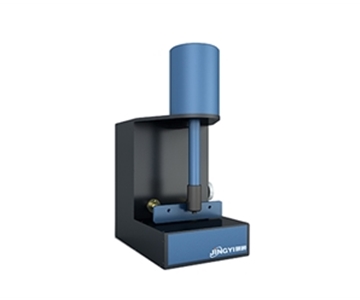
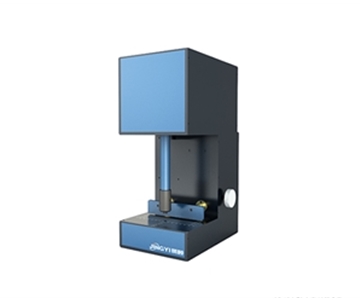
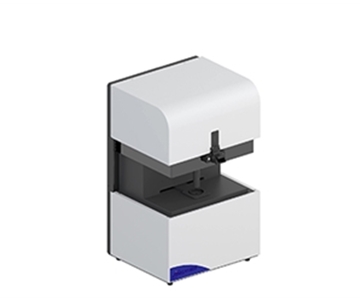
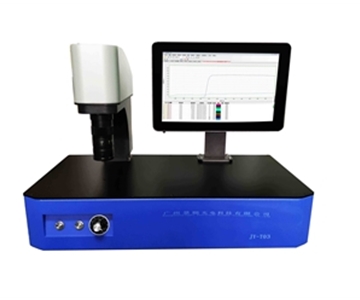
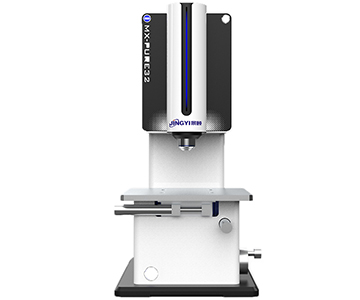
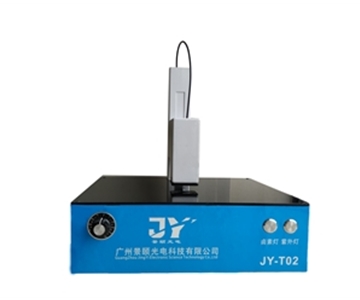
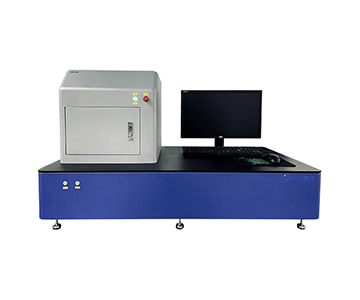
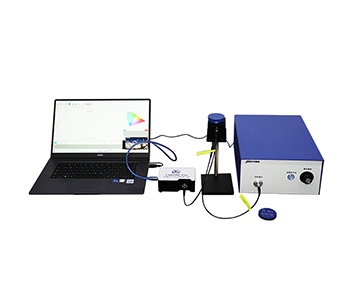
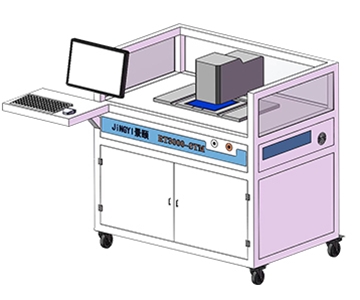
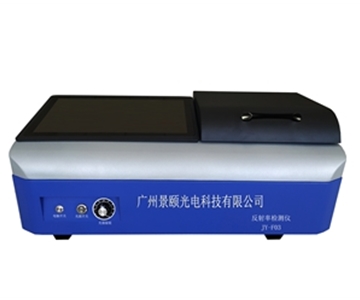
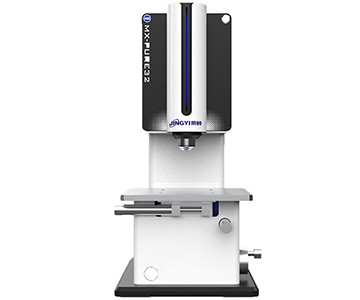
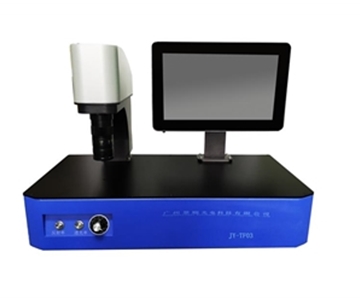
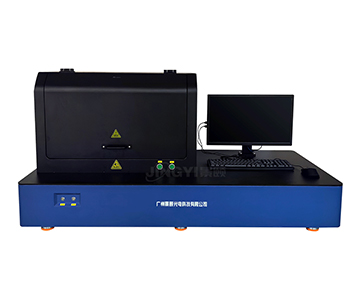
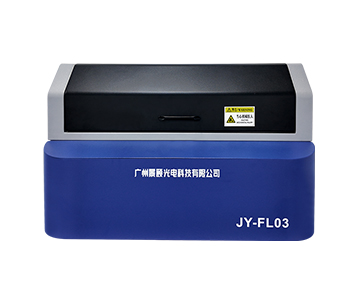
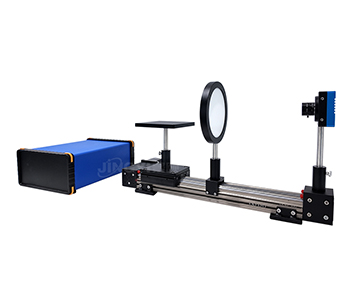
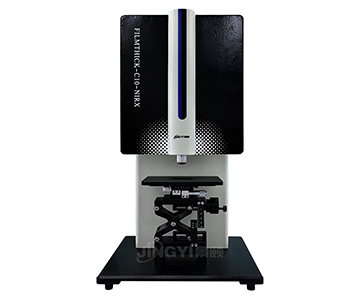
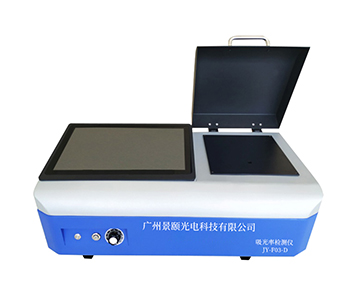
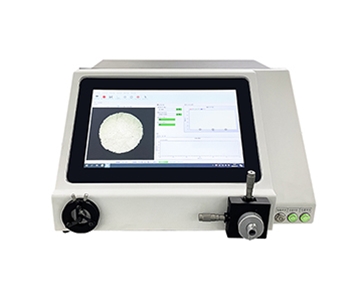
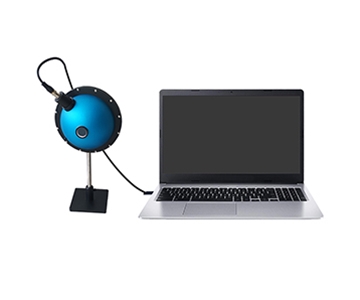
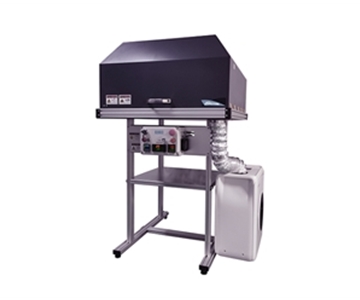
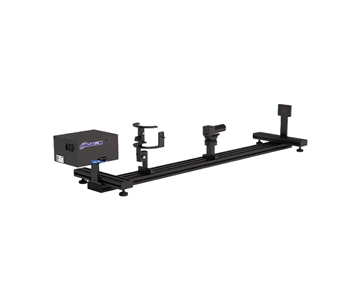
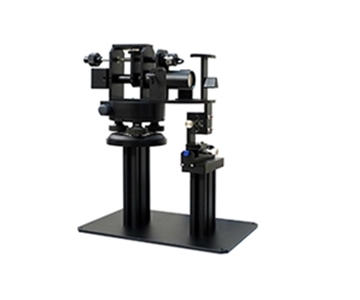
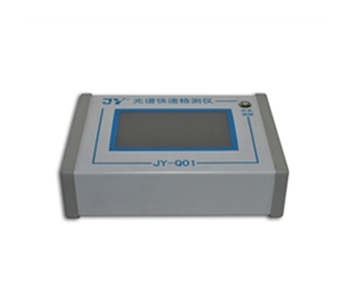
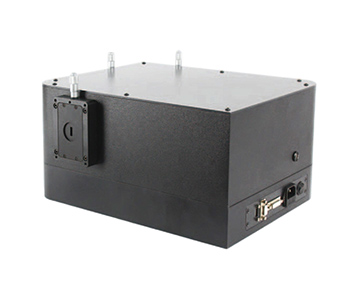
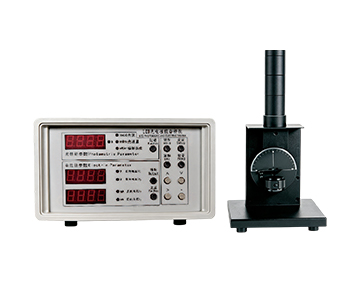
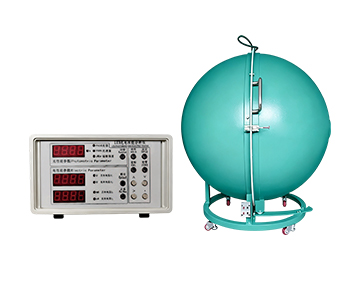
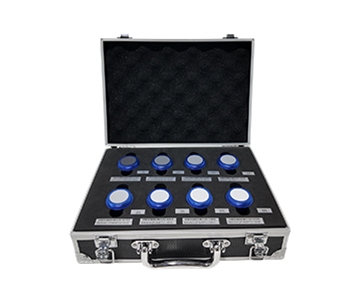
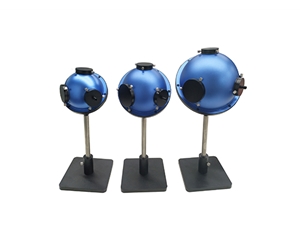
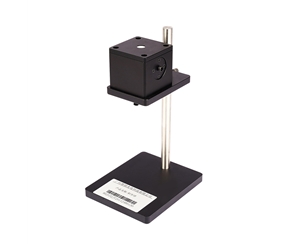
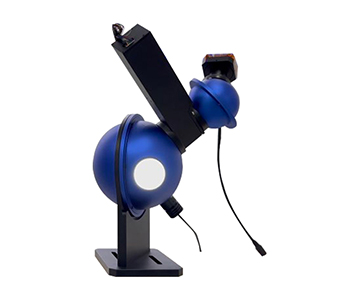
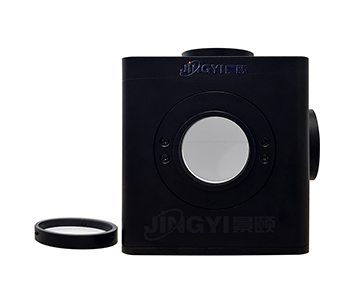
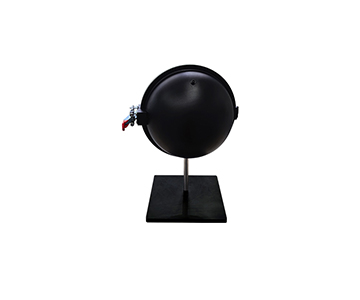
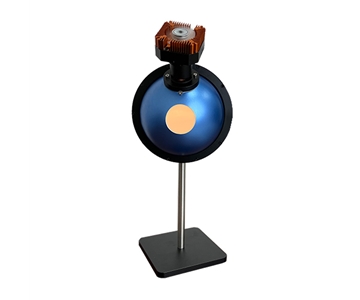
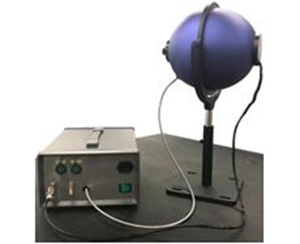
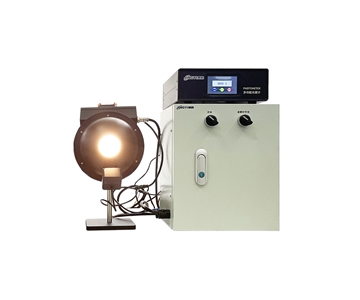
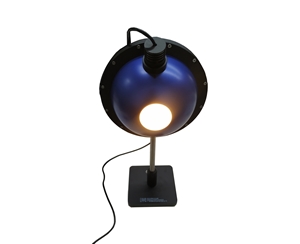
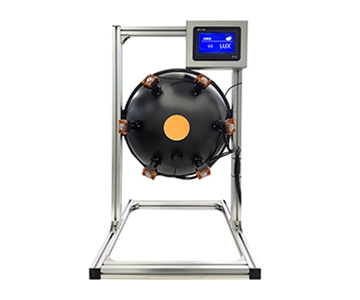
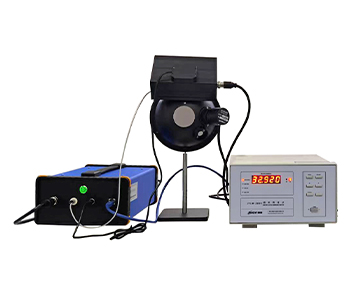
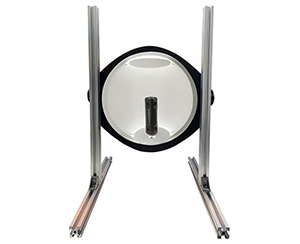
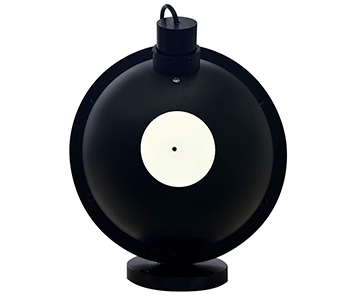
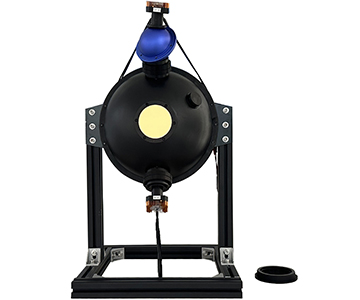
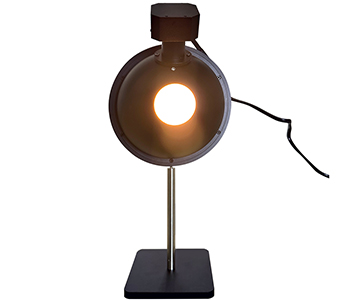
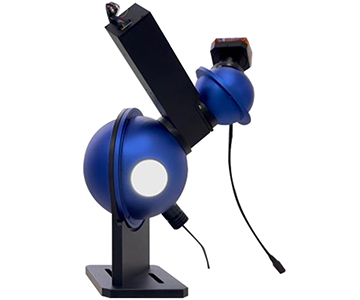
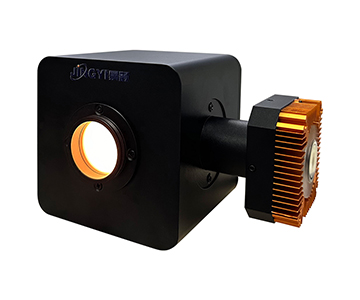
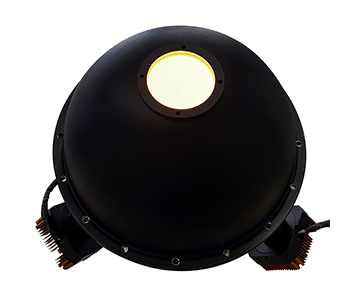
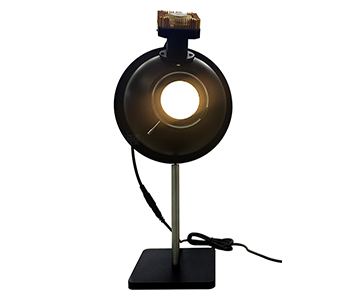
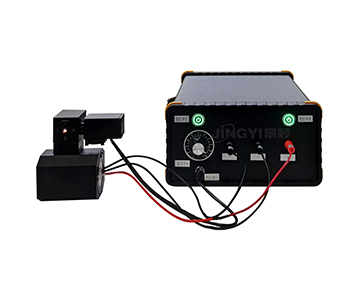
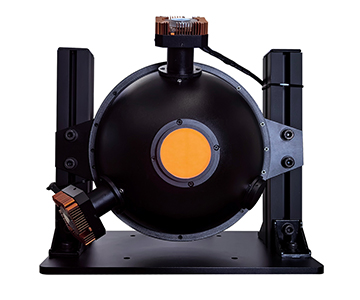
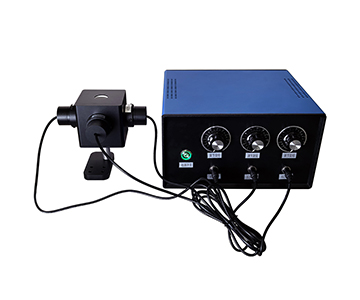
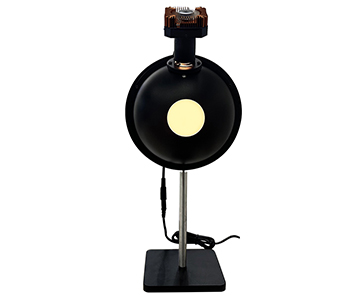
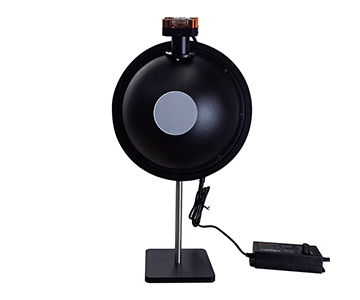
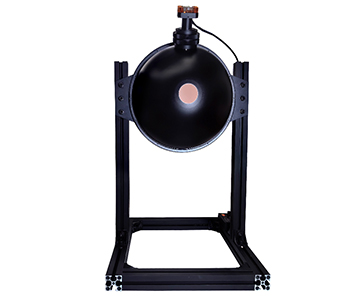
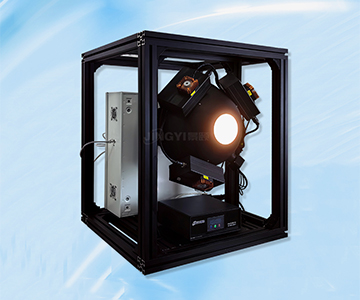
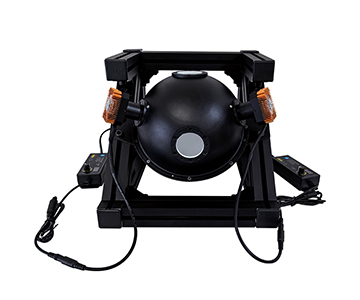
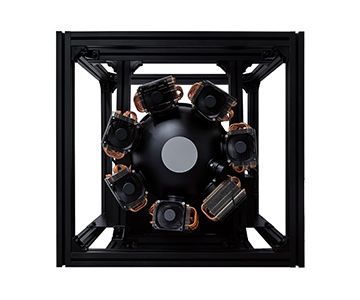
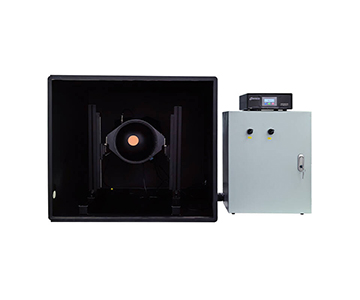
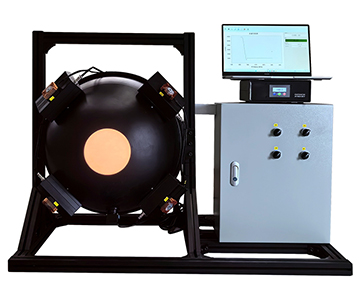
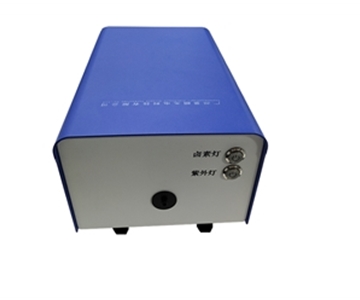
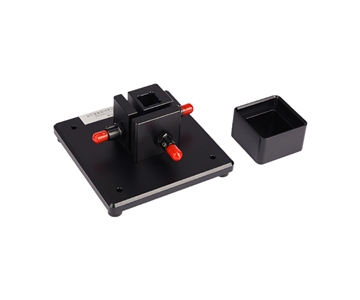
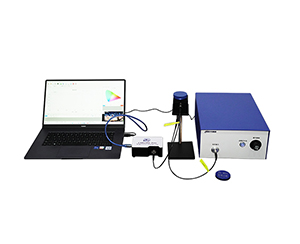
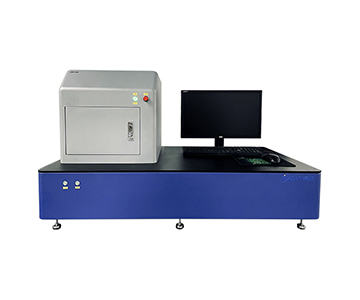
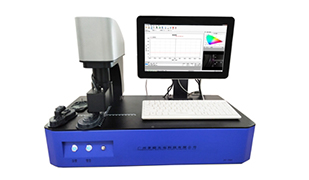
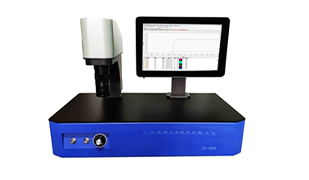
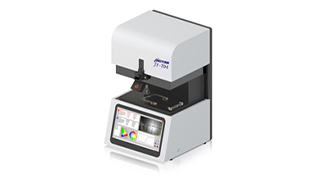
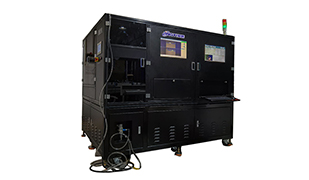
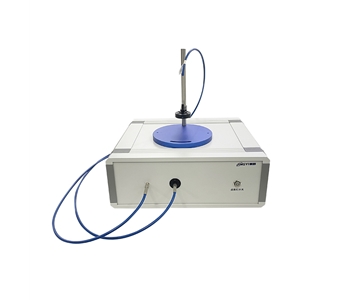
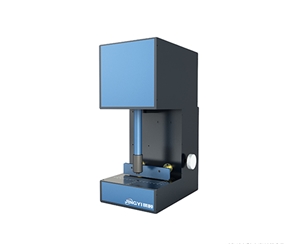
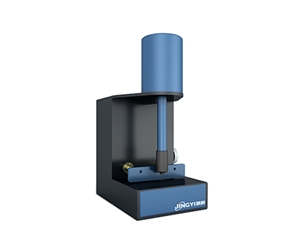
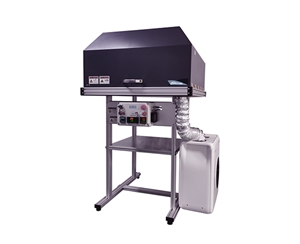
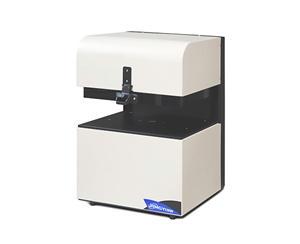
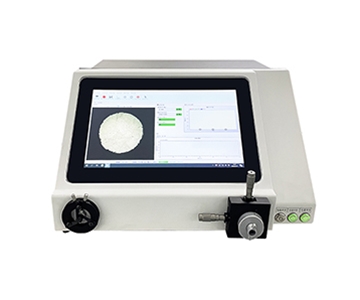
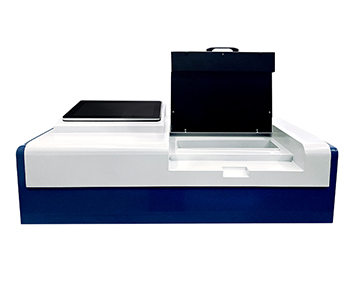
Integrating sphere reflectance measurement for consumer electronics and coating production lines faces two compounding constraints: single-sample cycle times exceeding 3 seconds and wavelength repeatability drifting beyond 1 nm. A mainstream optical reflectance system employing 8° illumination, 380–1000 nm spectral coverage, and a 2048-element photodetector array compresses single-sampling to under 1 second while maintaining wavelength repeatability of 0.2 nm and instrument repeatability below 1%. This enables simultaneous full-spectrum and colorimetric output for high-frequency sampling scenarios such as mobile device cover glass, plastic components, and printing inks—delivering measurement consistency at volume without sacrificing throughput.
Why High-Frequency Sampling on Production Lines Stalls at "Slow" and "Drift"
During an overnight shift at a mobile cover glass fabrication plant, a process engineer watched the batch report with growing concern. The previous shift had accumulated approximately $21,000 in rework costs from semi-finished parts rejected for reflectance out-of-spec, while the false-rejection rate had climbed from 0.37% to 1.84% within a month. This pattern repeats across coating filling lines where operators pull samples every 30 minutes; traditional single-point photometers return one numerical value but mask anomalous spectral dips across the 380–1000 nm range. At optical component plants, manual positioning during batch changeovers introduces placement errors that push sequential readings on the same lens beyond 2% variance.
The deeper friction point is that "slow" and "drift" coexist. Slow means 3–5 seconds per sample—untenable for a line producing 20,000 units daily if full inspection is attempted. Drift means unreliable repeatability; a part deemed acceptable today triggers an NG (no-go) tomorrow, forcing quality staff to expand sampling ratios, which further chokes line节拍. As spectrophotometers, automotive safety inspection, and photovoltaic backsheet manufacturing all elevate reflectance to a critical quality gate, the compromise of "sampling代替全检" (sampling代替 full inspection) silently inflates hidden costs.
How Integrating Sphere Geometry Locks Errors at the Source
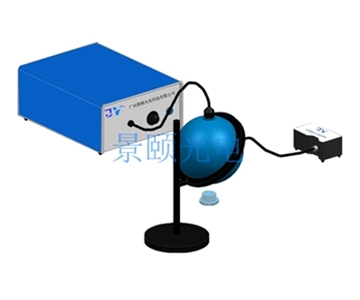
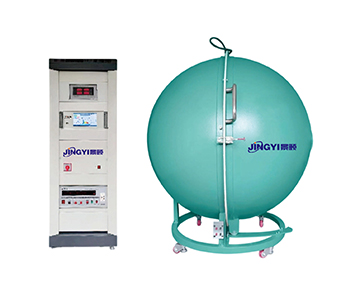
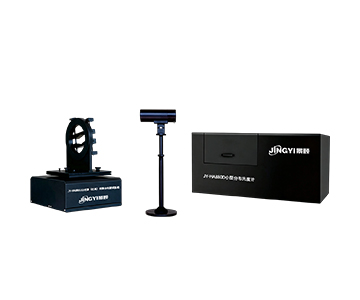
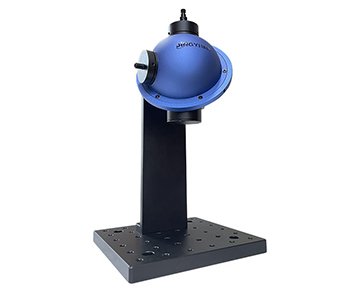
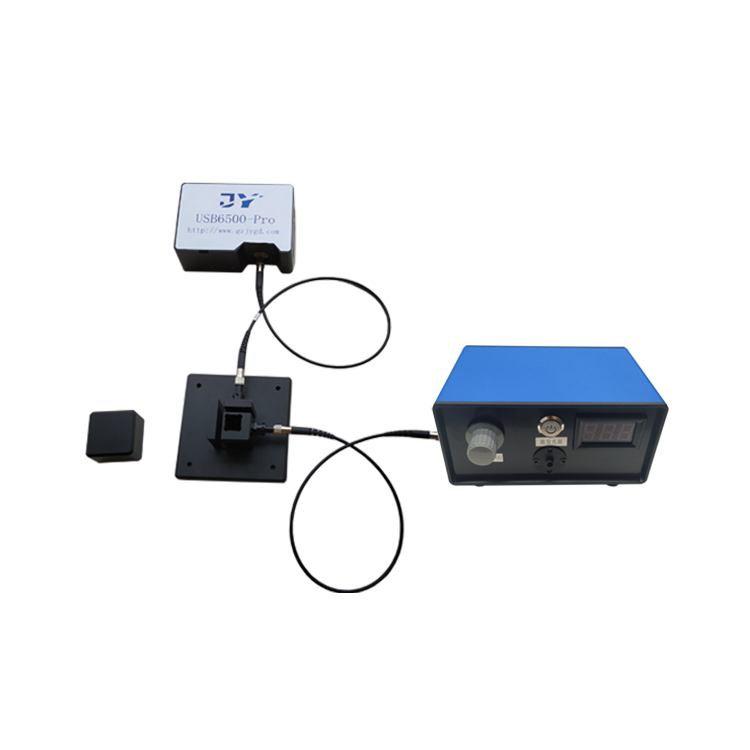
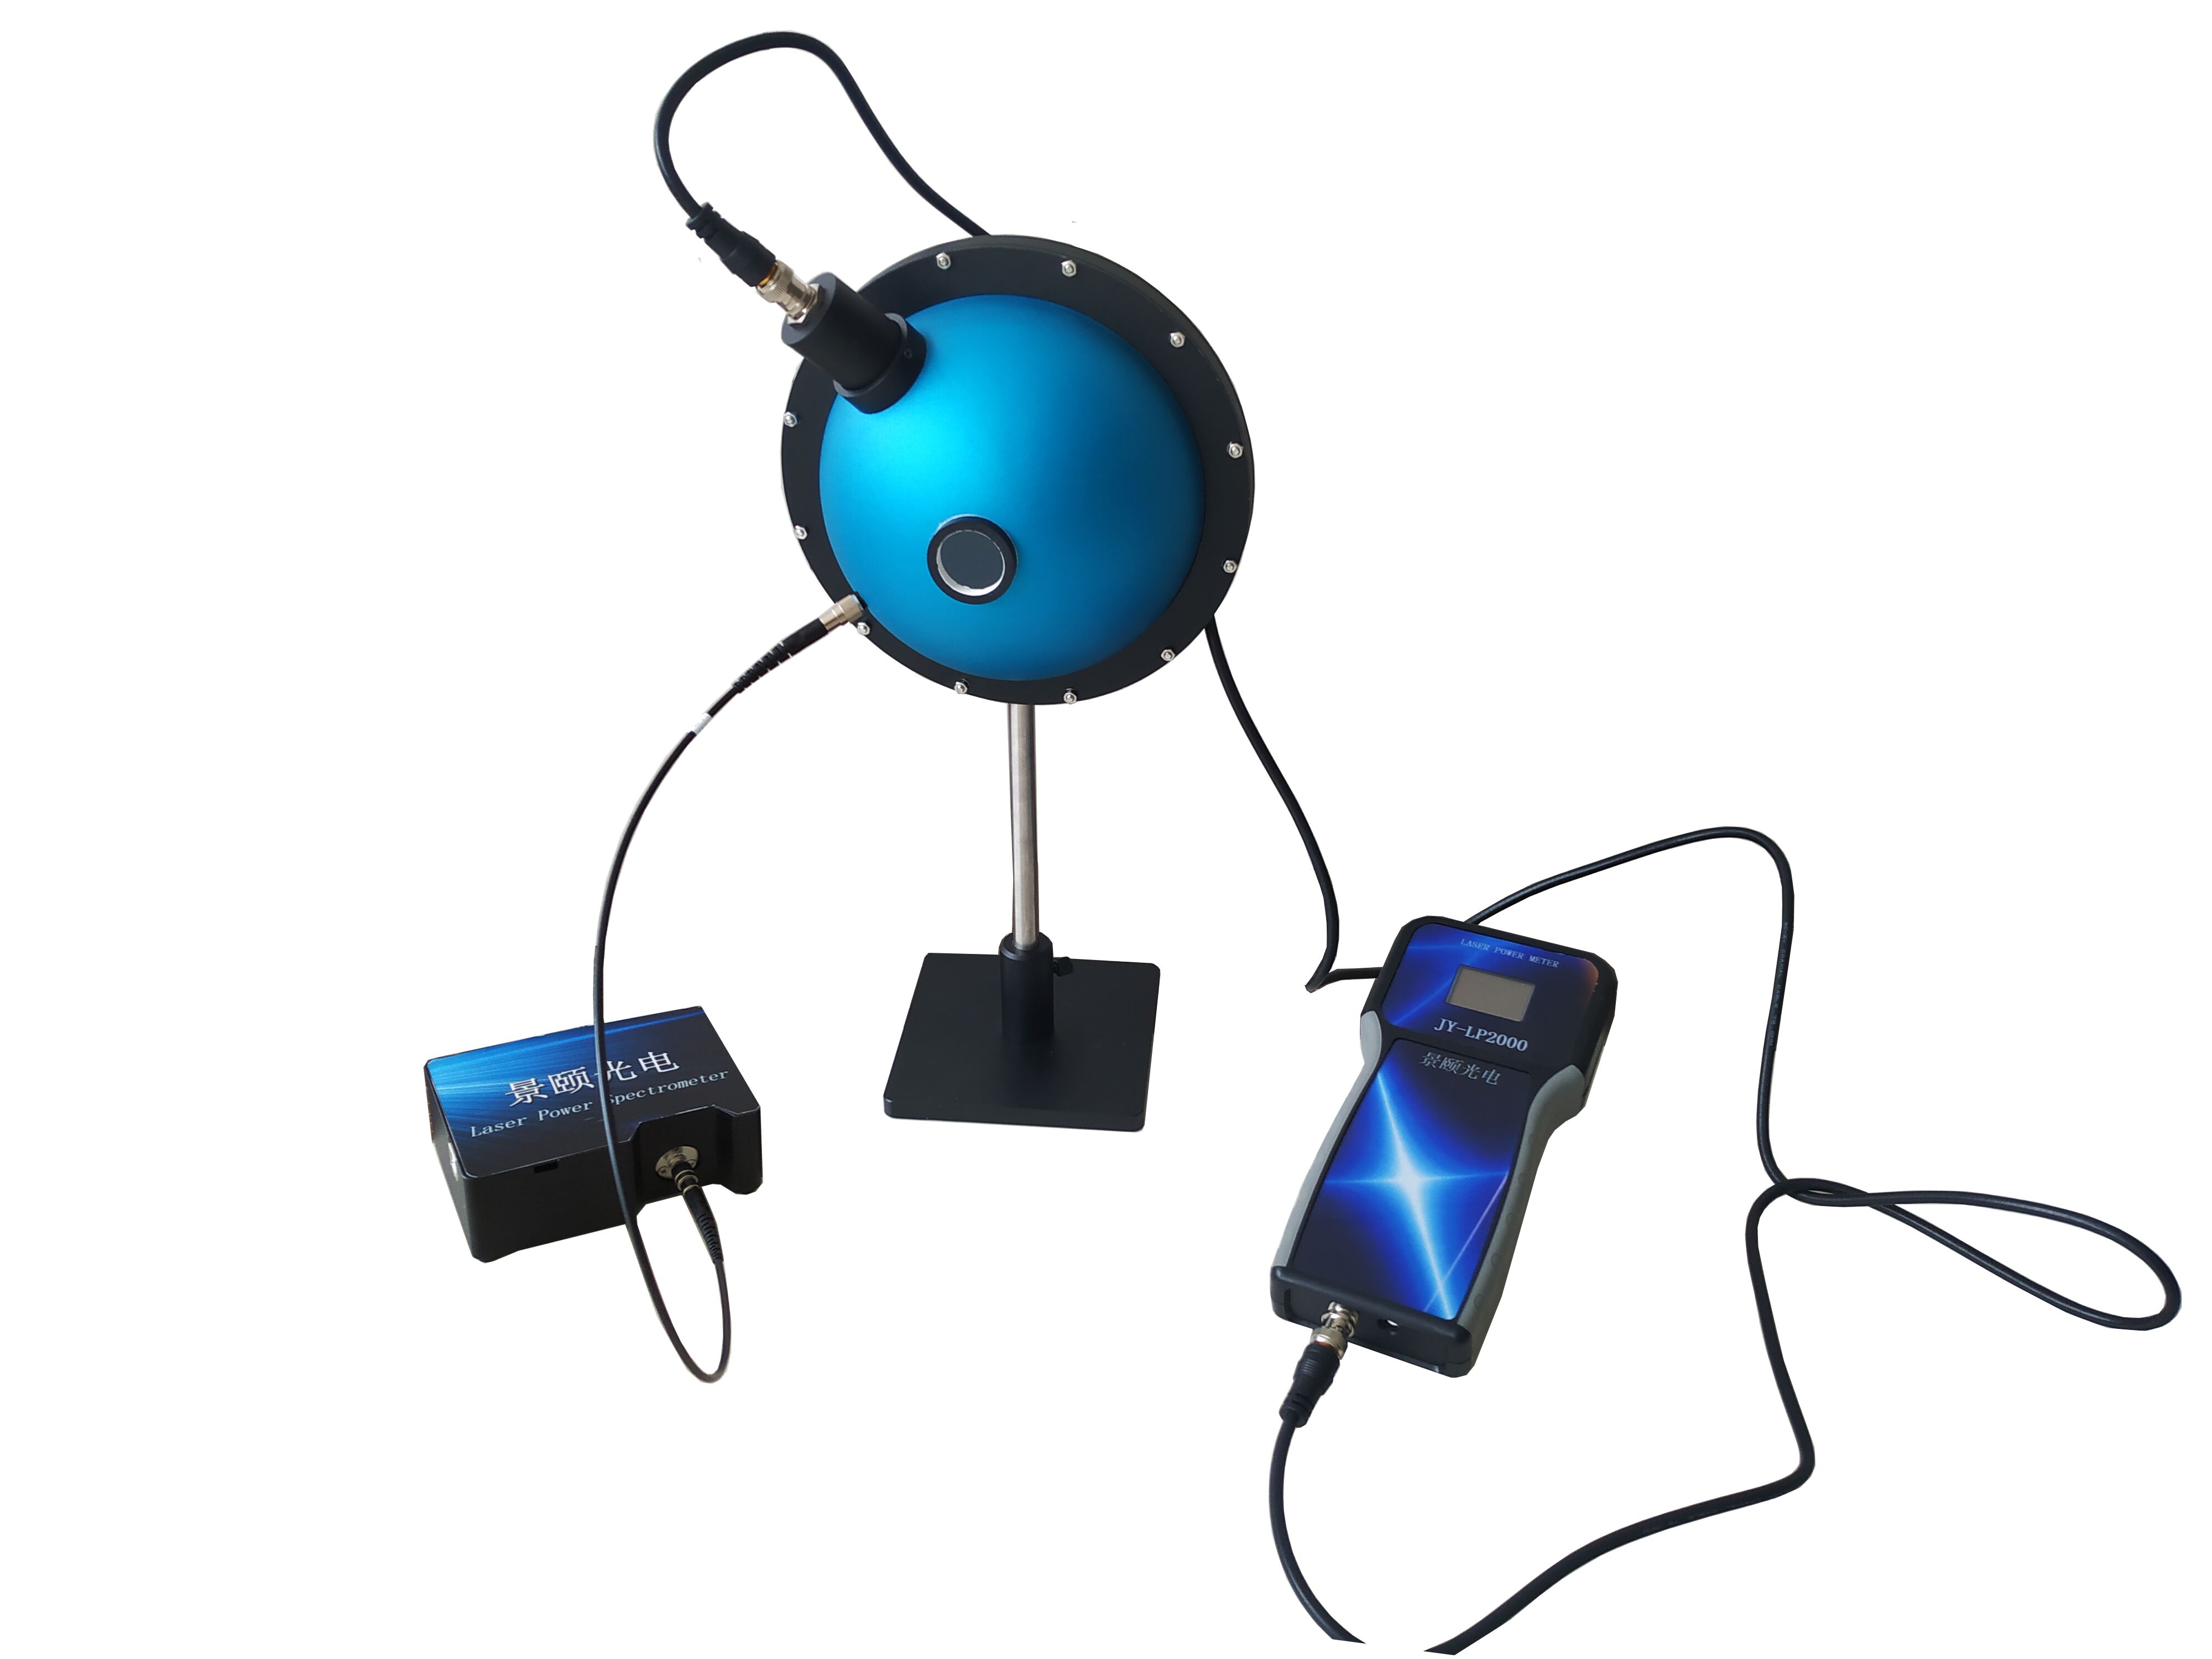
Dissecting the problem reveals two control variables: illumination uniformity and sampling speed. The evaluated system adopts an 8° illumination, vertically received integrating sphere configuration. The high-reflectance inner coating forces multiple diffuse reflections inside the cavity, effectively removing "incident angle" as a variable from the measurement equation. When measuring curved reflective surfaces at mobile cover glass edges, the 8° incidence suppresses specular glare. Meanwhile, the 2048-array photodetector simultaneously reads 2048 photosensitive cells across the 380–1000 nm band—not merely "faster," but parallel spectral acquisition that eliminates the cumulative delay of mechanically scanned spectrometers.
Parameter translation into engineering terms: single-sample time better than 1 second theoretically yields 3,600+ full-spectrum scans per hour. Wavelength accuracy under 1 nm resolves spectral line drift smaller than 1 nm. Wavelength repeatability of 0.2 nm means ten consecutive measurements on a standard whiteboard show peak wavelength shift within a fraction of a human hair diameter. Display resolution of 0.01% renders 0.5% deviations visible on-screen. These figures collectively answer a production engineer's core question: when batch testing demands dozens of data points per minute, can the instrument remain stable?
The evaluated manufacturer participated in drafting the Chinese standard GB/T 47066-2026 (equivalent to ISO 13468 for plastics total reflectance and transmittance), which defines test geometry and calibration procedures for plastic samples. Under the specified geometry, the instrument achieves reflectance repeatability below 1%, with traceability anchored to the standard's whiteboard calibration chain.
The Efficiency Ledger: Batch Testing Perspective
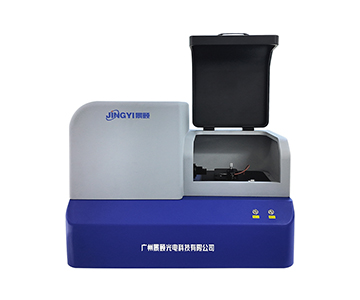
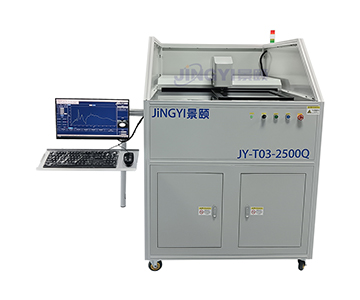
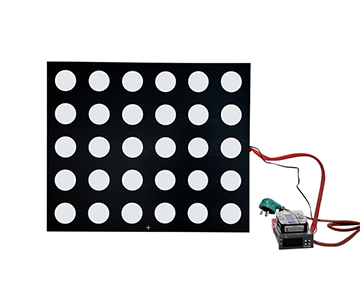
Converting specifications into production language clarifies the impact. Before deployment, a coating manufacturer used a legacy portable reflectometer for spot checks: single-sample time = 4.8 s, daily effective inspections = 720 units, false-rejection rework rate = 1.84%, operator alignment time = ~6 s per sample. After installing a mainstream integrated reflectance measurement system, single-sample time dropped to 0.9 s (including automatic dark-background subtraction), daily effective inspections rose to approximately 3,200 units, false-rejection rework rate fell to 0.41%, and operator alignment time approached zero (embedded PC + fixed sample port).
The improvement transcends a simple "5× speed gain." Because wavelength repeatability holds at 0.2 nm, spectral traces from identical plastic batches show markedly higher coincidence. Quality inspectors no longer need repeated retests for "edge pass, center NG" ambiguity. Display resolution of 0.01% exposes 0.3% deviations previously swallowed by rounding, intercepting abnormal batches before they advance to downstream processes. Labor allocation shifted: from two inspectors per shift rotating through manual checks to one operator monitoring automated OK/NG判定, saving roughly 47 labor hours monthly.
Cross-Industry Transferability: Reusable Principles
Three transferable rules emerge from these cases. First: products requiring dual metrics of "optical performance + appearance color" (mobile AR glass, printing inks, plastic housings) can consolidate a reflectometer and a colorimeter into one spectrophotometric reflectance instrument, simplifying procurement and calibration chains. Second: sample port size dictates minimum measurable dimension—a 9 mm default aperture covers mobile cover glass, tablet backs, and lamp reflector cups; measuring smaller areas demands a micro-spot model (60 μm spot size). Selecting a general-purpose unit for micro-parts leads to compromised data. Third: the value of integrating sphere reflectance measurement lies not in "accuracy once," but in "stability over ten thousand measurements." Under batch testing conditions, repeatability specifications deserve higher priority in procurement documentation than static accuracy figures.
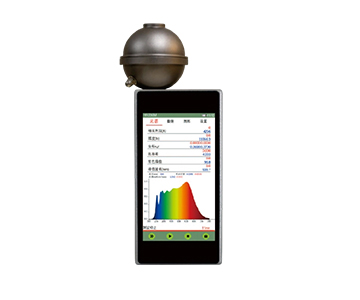
In automotive safety applications, lampshades, reflector cups, and rearview mirrors rely on 8° integrating sphere geometry for reflectance control. In photovoltaic silicon wafer inspection, anti-reflection coating evaluation requires full-spectrum reflectance curves rather than single-point values. Consumer electronics quality lines leverage XY chromaticity diagrams and Lab values from spectrophotometric output to replace visual comparison with data-driven sorting. These scenarios share a common measurement logic.
Where the Real Bottlenecks Lie Beyond Equipment Speed
Many assume that purchasing a fast instrument solves everything, but a third bottleneck—sample preparation and decision rules—is frequently overlooked during implementation.
Furthermore, inline automatic inspection demands additional investment in robotic handlers or conveyor interfaces. For small workshops lacking automation infrastructure, a standalone unit is affordable, but system integration costs can outweigh the equipment price. Total Cost of Ownership (TCO) calculations must therefore include "whether automated lines will be adopted within three years," rather than fixating on the bare instrument quote.
Objective Assessment and Applicability Boundaries
No instrument covers every scenario. This integrating sphere reflectance solution performs reliably on flat or irregular samples larger than 9 mm, but two conditions warrant caution. First, ultra-smooth mirror surfaces requiring near-specular angles (e.g., 5° incidence on optical-grade aluminum mirrors) will suffer from mixed diffuse components under 8° geometry; variable-angle accessories are necessary. Second, deep near-infrared analysis beyond 1700 nm for silicon wafer anti-reflection films exceeds the 380–1000 nm spectral range; a 900–1700 nm NIR-dedicated system is required.
Instrument repeatability below 1% is specified "under identical conditions on a single unit." Cross-unit comparison introduces standard whiteboard transfer errors; multi-site operations sharing data baselines must synchronize calibration cycles. These are not flaws but inherent physical boundaries of any optical measurement system. Clarifying them before purchase prevents costly retrofits.
Five Practical Questions for Reflectance Measurement System Selection
Q1: How does integrating sphere reflectance measurement differ from a standard reflectometer?
A standard reflectometer typically measures at a single point or narrow band, suitable for rapid screening. Integrating sphere geometry under 8° illumination covers the full 380–1000 nm spectrum and simultaneously outputs reflectance curves and Lab color parameters, serving quality inspection and R&D scenarios that require spectral analysis.
Q2: What does single-sample measurement under 1 second mean for a production line?
At 0.9 seconds per sample, one operator per 8-hour shift can theoretically complete approximately 32,000 measurements—far exceeding manual sampling limits. This transforms "100% inspection" from a slogan into an executable action, especially for high-tempo lines producing mobile cover glass and plastic components.
Q3: Why does wavelength repeatability of 0.2 nm matter more than display resolution of 0.01%?
Display resolution is merely decimal precision; repeatability determines whether ten measurements fluctuate. In batch testing, poor repeatability misclassifies合格品 as NG. A wavelength repeatability of 0.2 nm directly suppresses false-rejection rates below 1%, protecting downstream yield.
Q4: Should coating and ink manufacturers choose a general-purpose or UV-enhanced model?
If visible-range color and brightness dominate, a 380–1000 nm general-purpose model suffices. For UV-curable inks or fluorescent brightener detection, a 250–800 nm UV model is necessary to prevent formulation偏差 from missing ultraviolet data.
Q5: How can I independently verify that a reflectance measurement system meets procurement requirements?
Conduct a three-day comparison using your own standard whiteboard and reference reflectance tiles, recording wavelength repeatability, instrument repeatability, and dark-background subtraction stability. Request third-party calibration certificates to confirm unbroken metrological traceability rather than relying solely on manufacturer self-inspection reports.
About This Guide
Data Sources
: Public technical documentation of JY-F03/CHT-F03 reflectance measurement systems, GB/T 47066-2026 (aligned with ISO 13468 and ASTM D1003), and in-house validation datasets (n=200+ production samples across coating and electronics lines).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 10 years in optical metrology and spectral instrument content strategy.
Disclosure
: Jingyi Optoelectronics manufactures reflectance measurement instruments. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: September 2026
For detailed specifications and application notes on reflectance measurement systems, search "Jingyi Optoelectronics reflectance measurement" or visit our technical library.