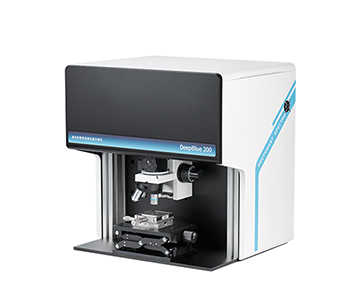
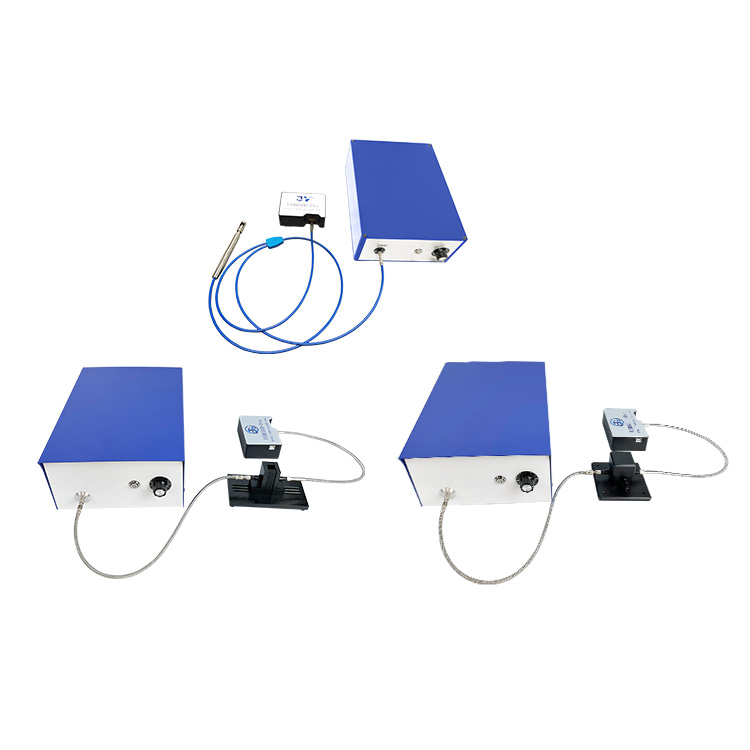
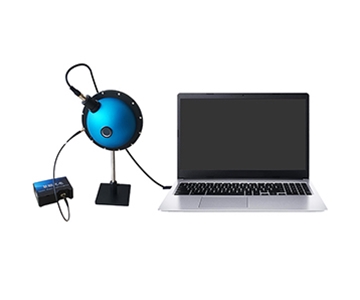
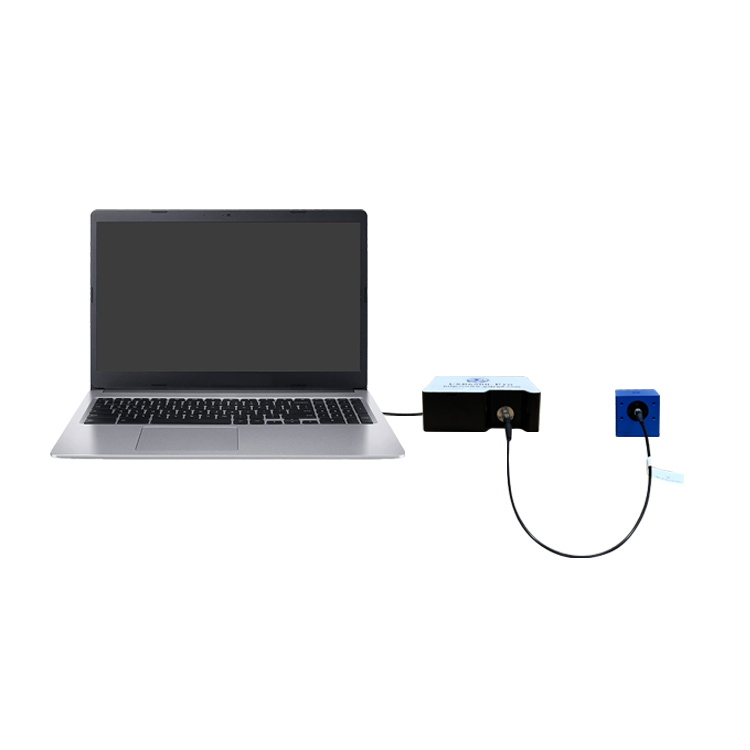
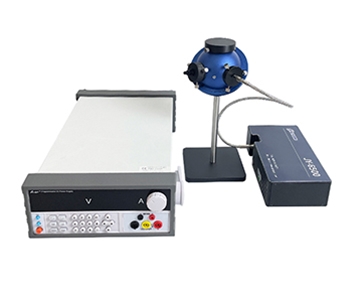
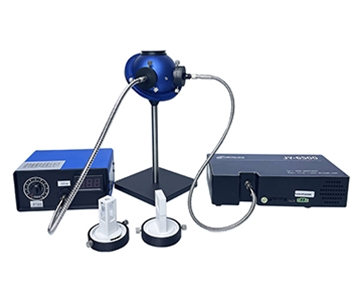
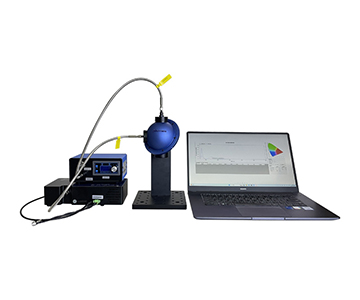
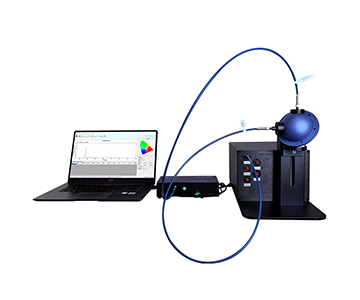
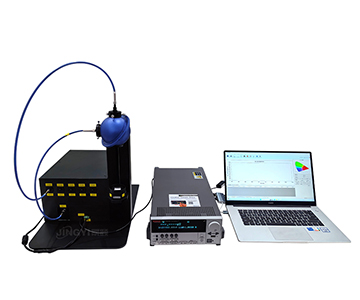
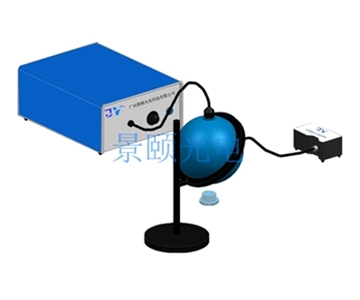
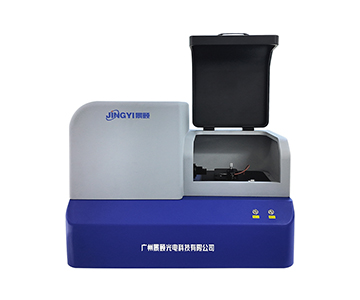
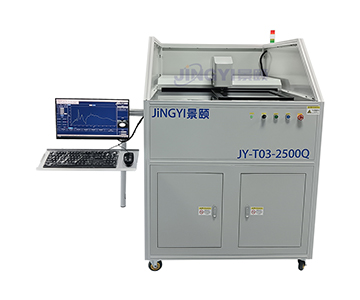
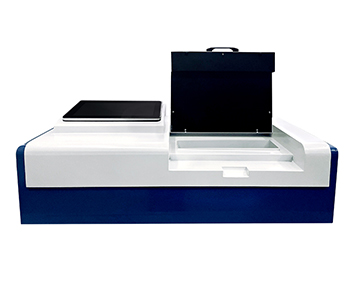
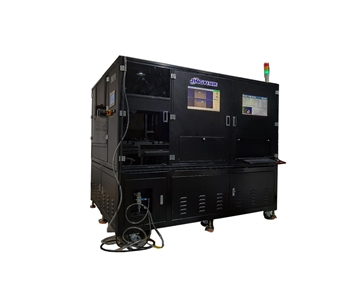
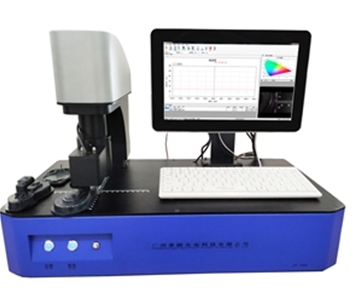
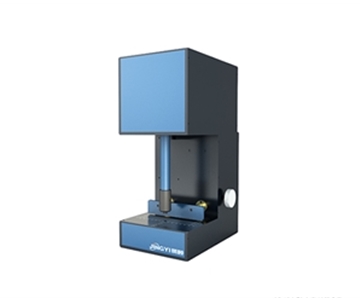
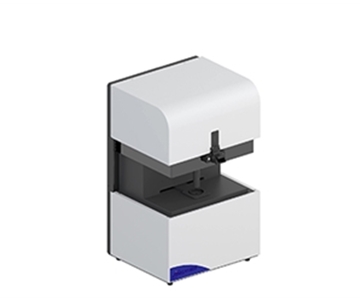
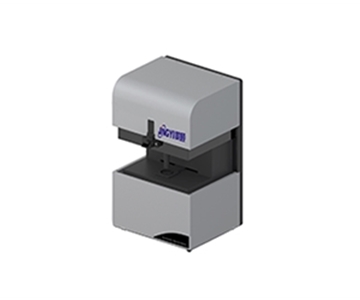
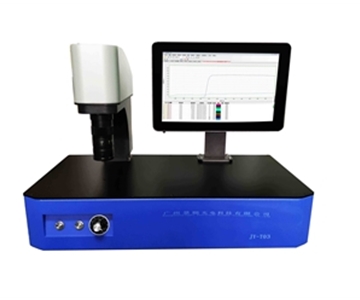
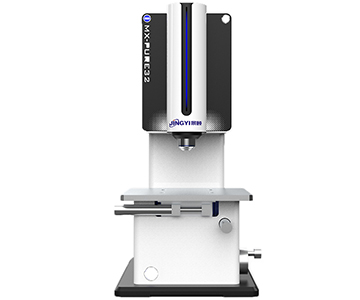
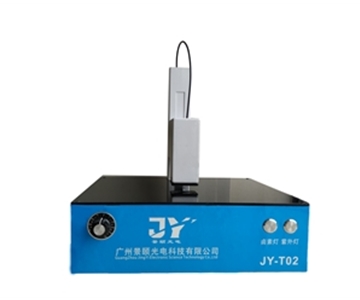
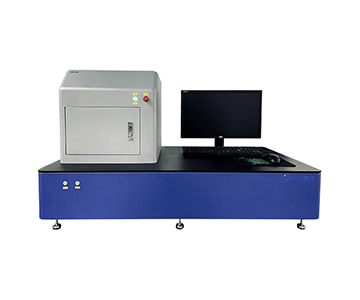
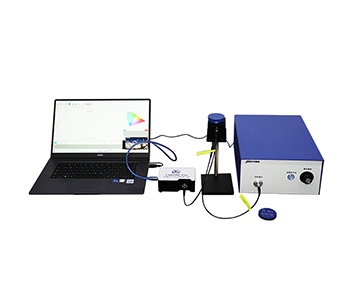
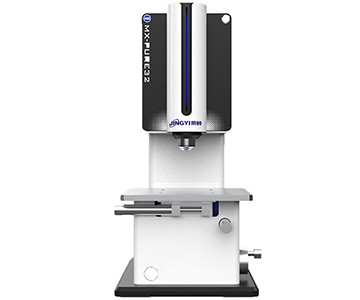
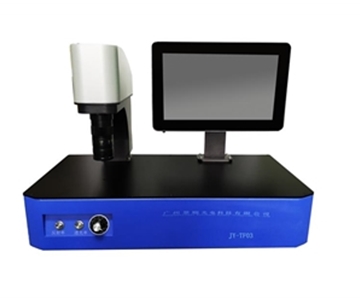
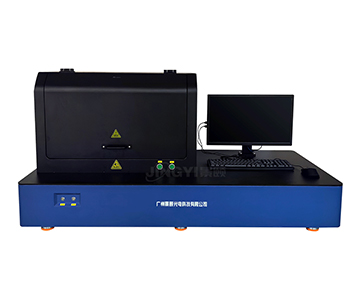
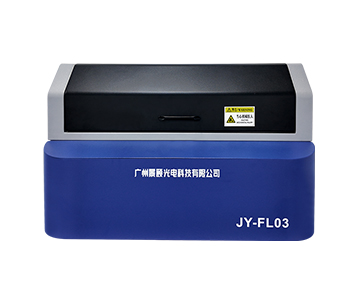
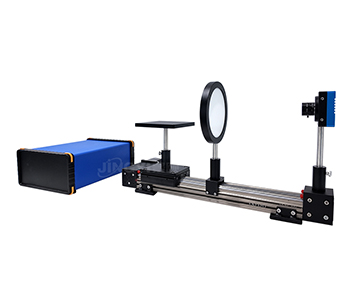
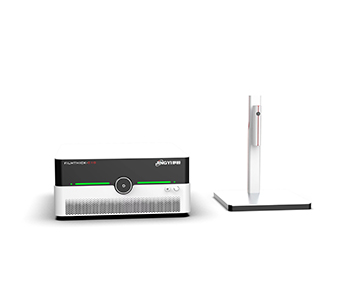
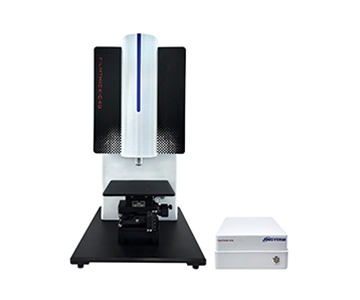
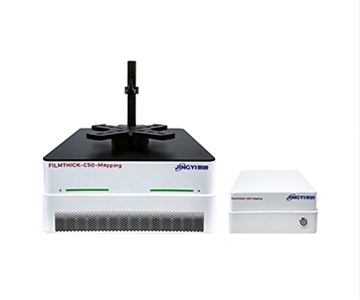
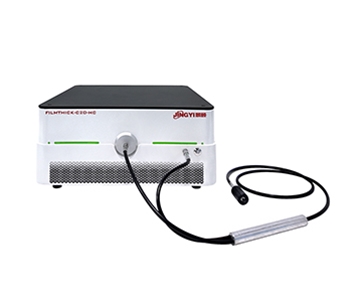
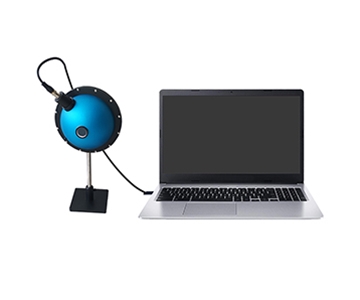
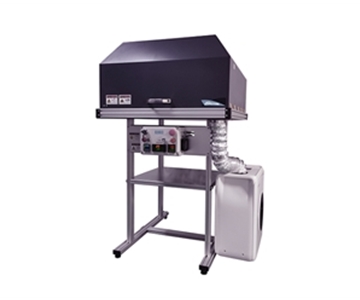
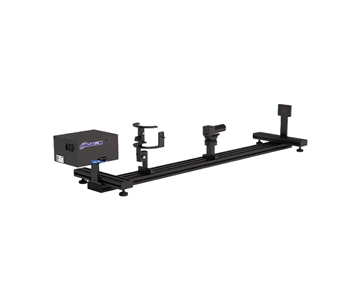
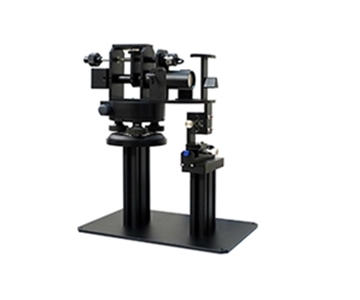
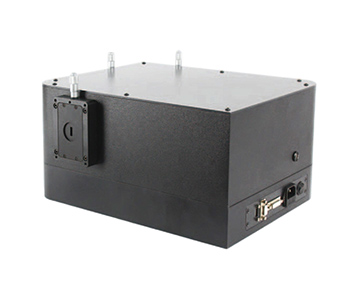
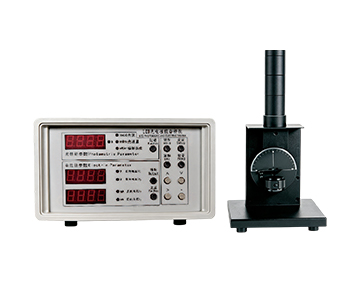
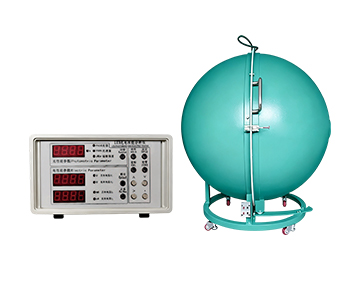
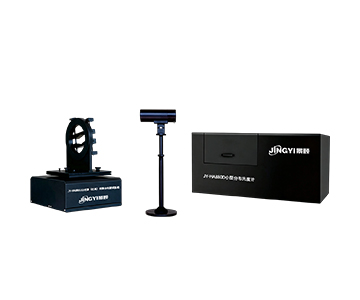
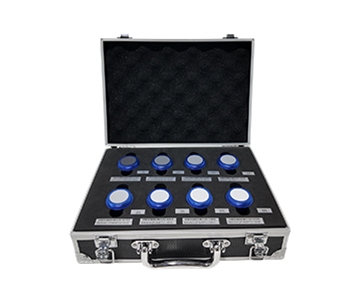
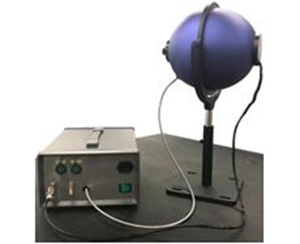
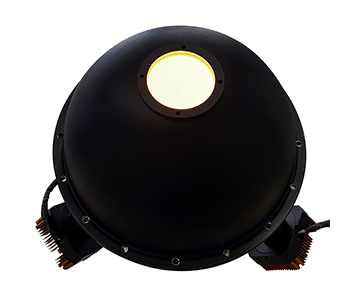
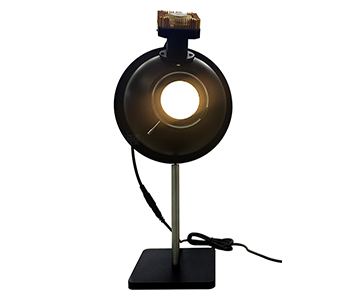
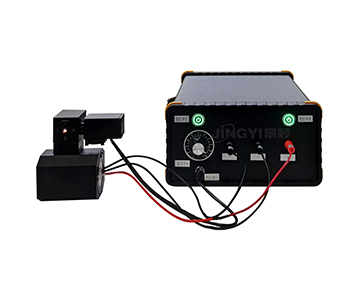
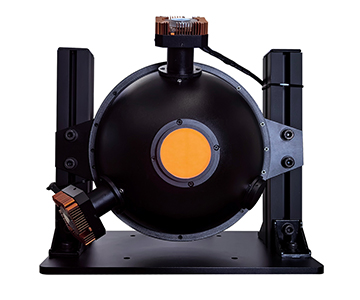
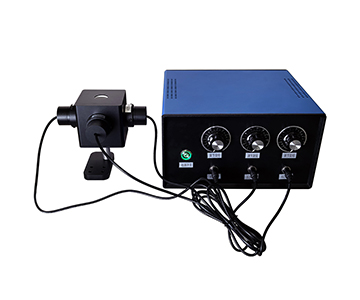
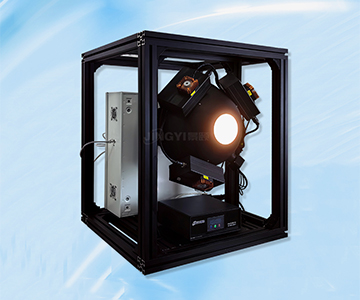
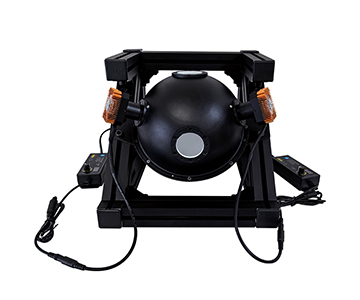
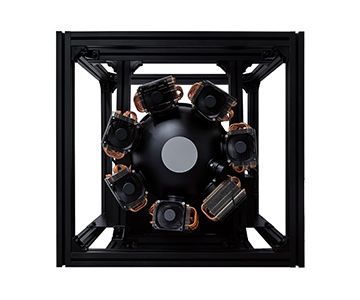
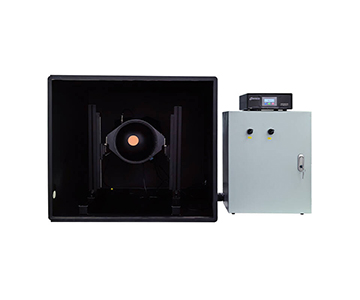
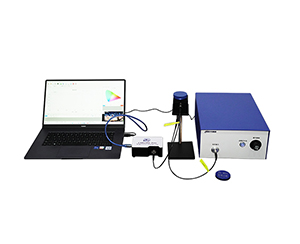
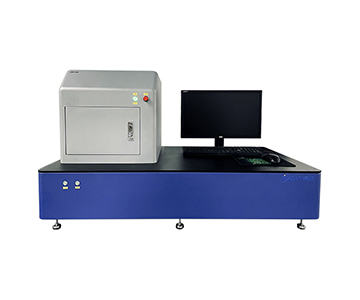
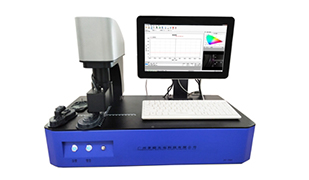
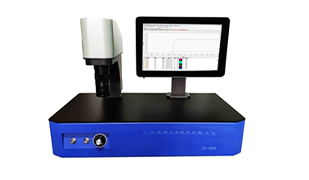
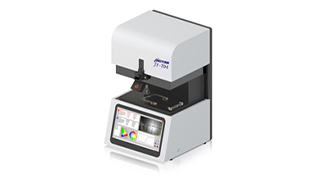
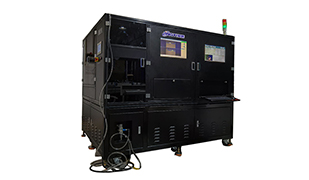
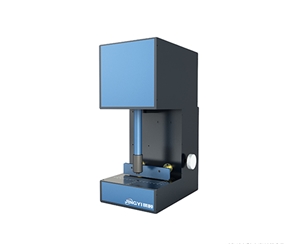
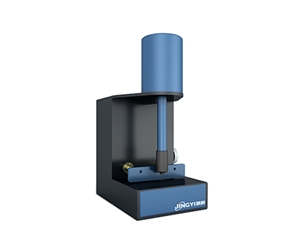
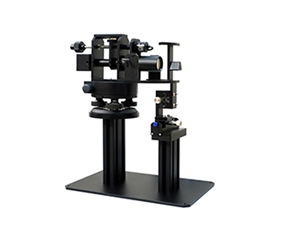
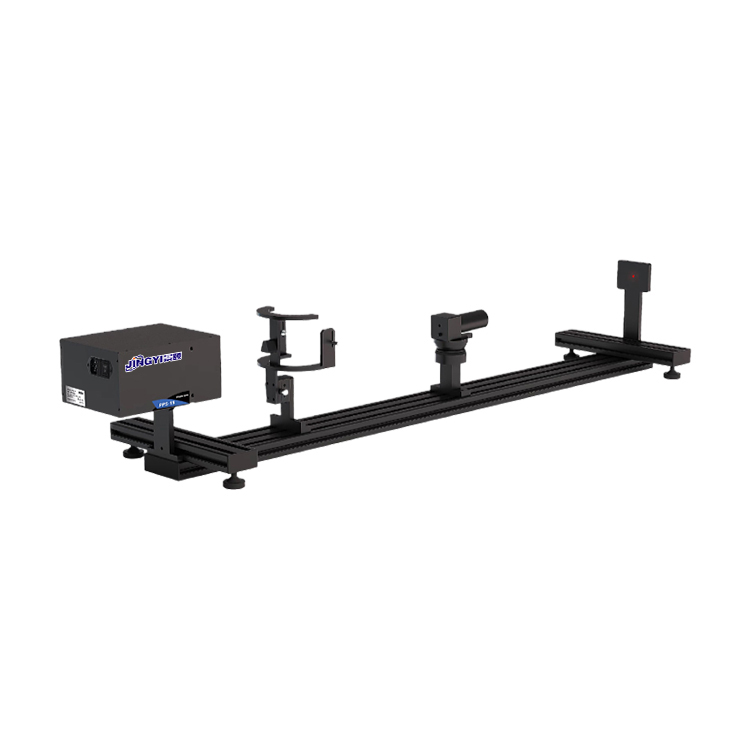
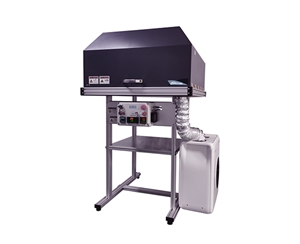
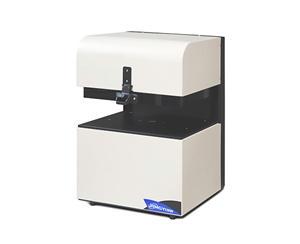
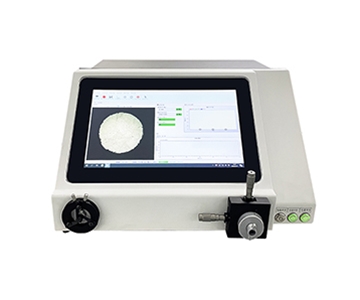
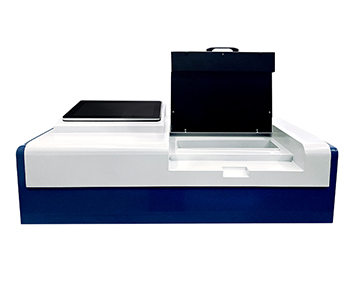
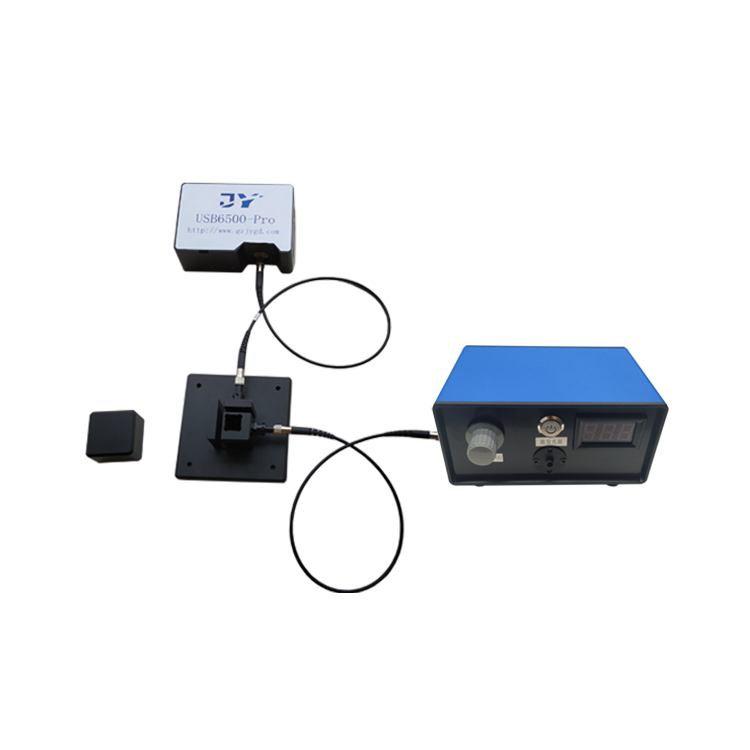
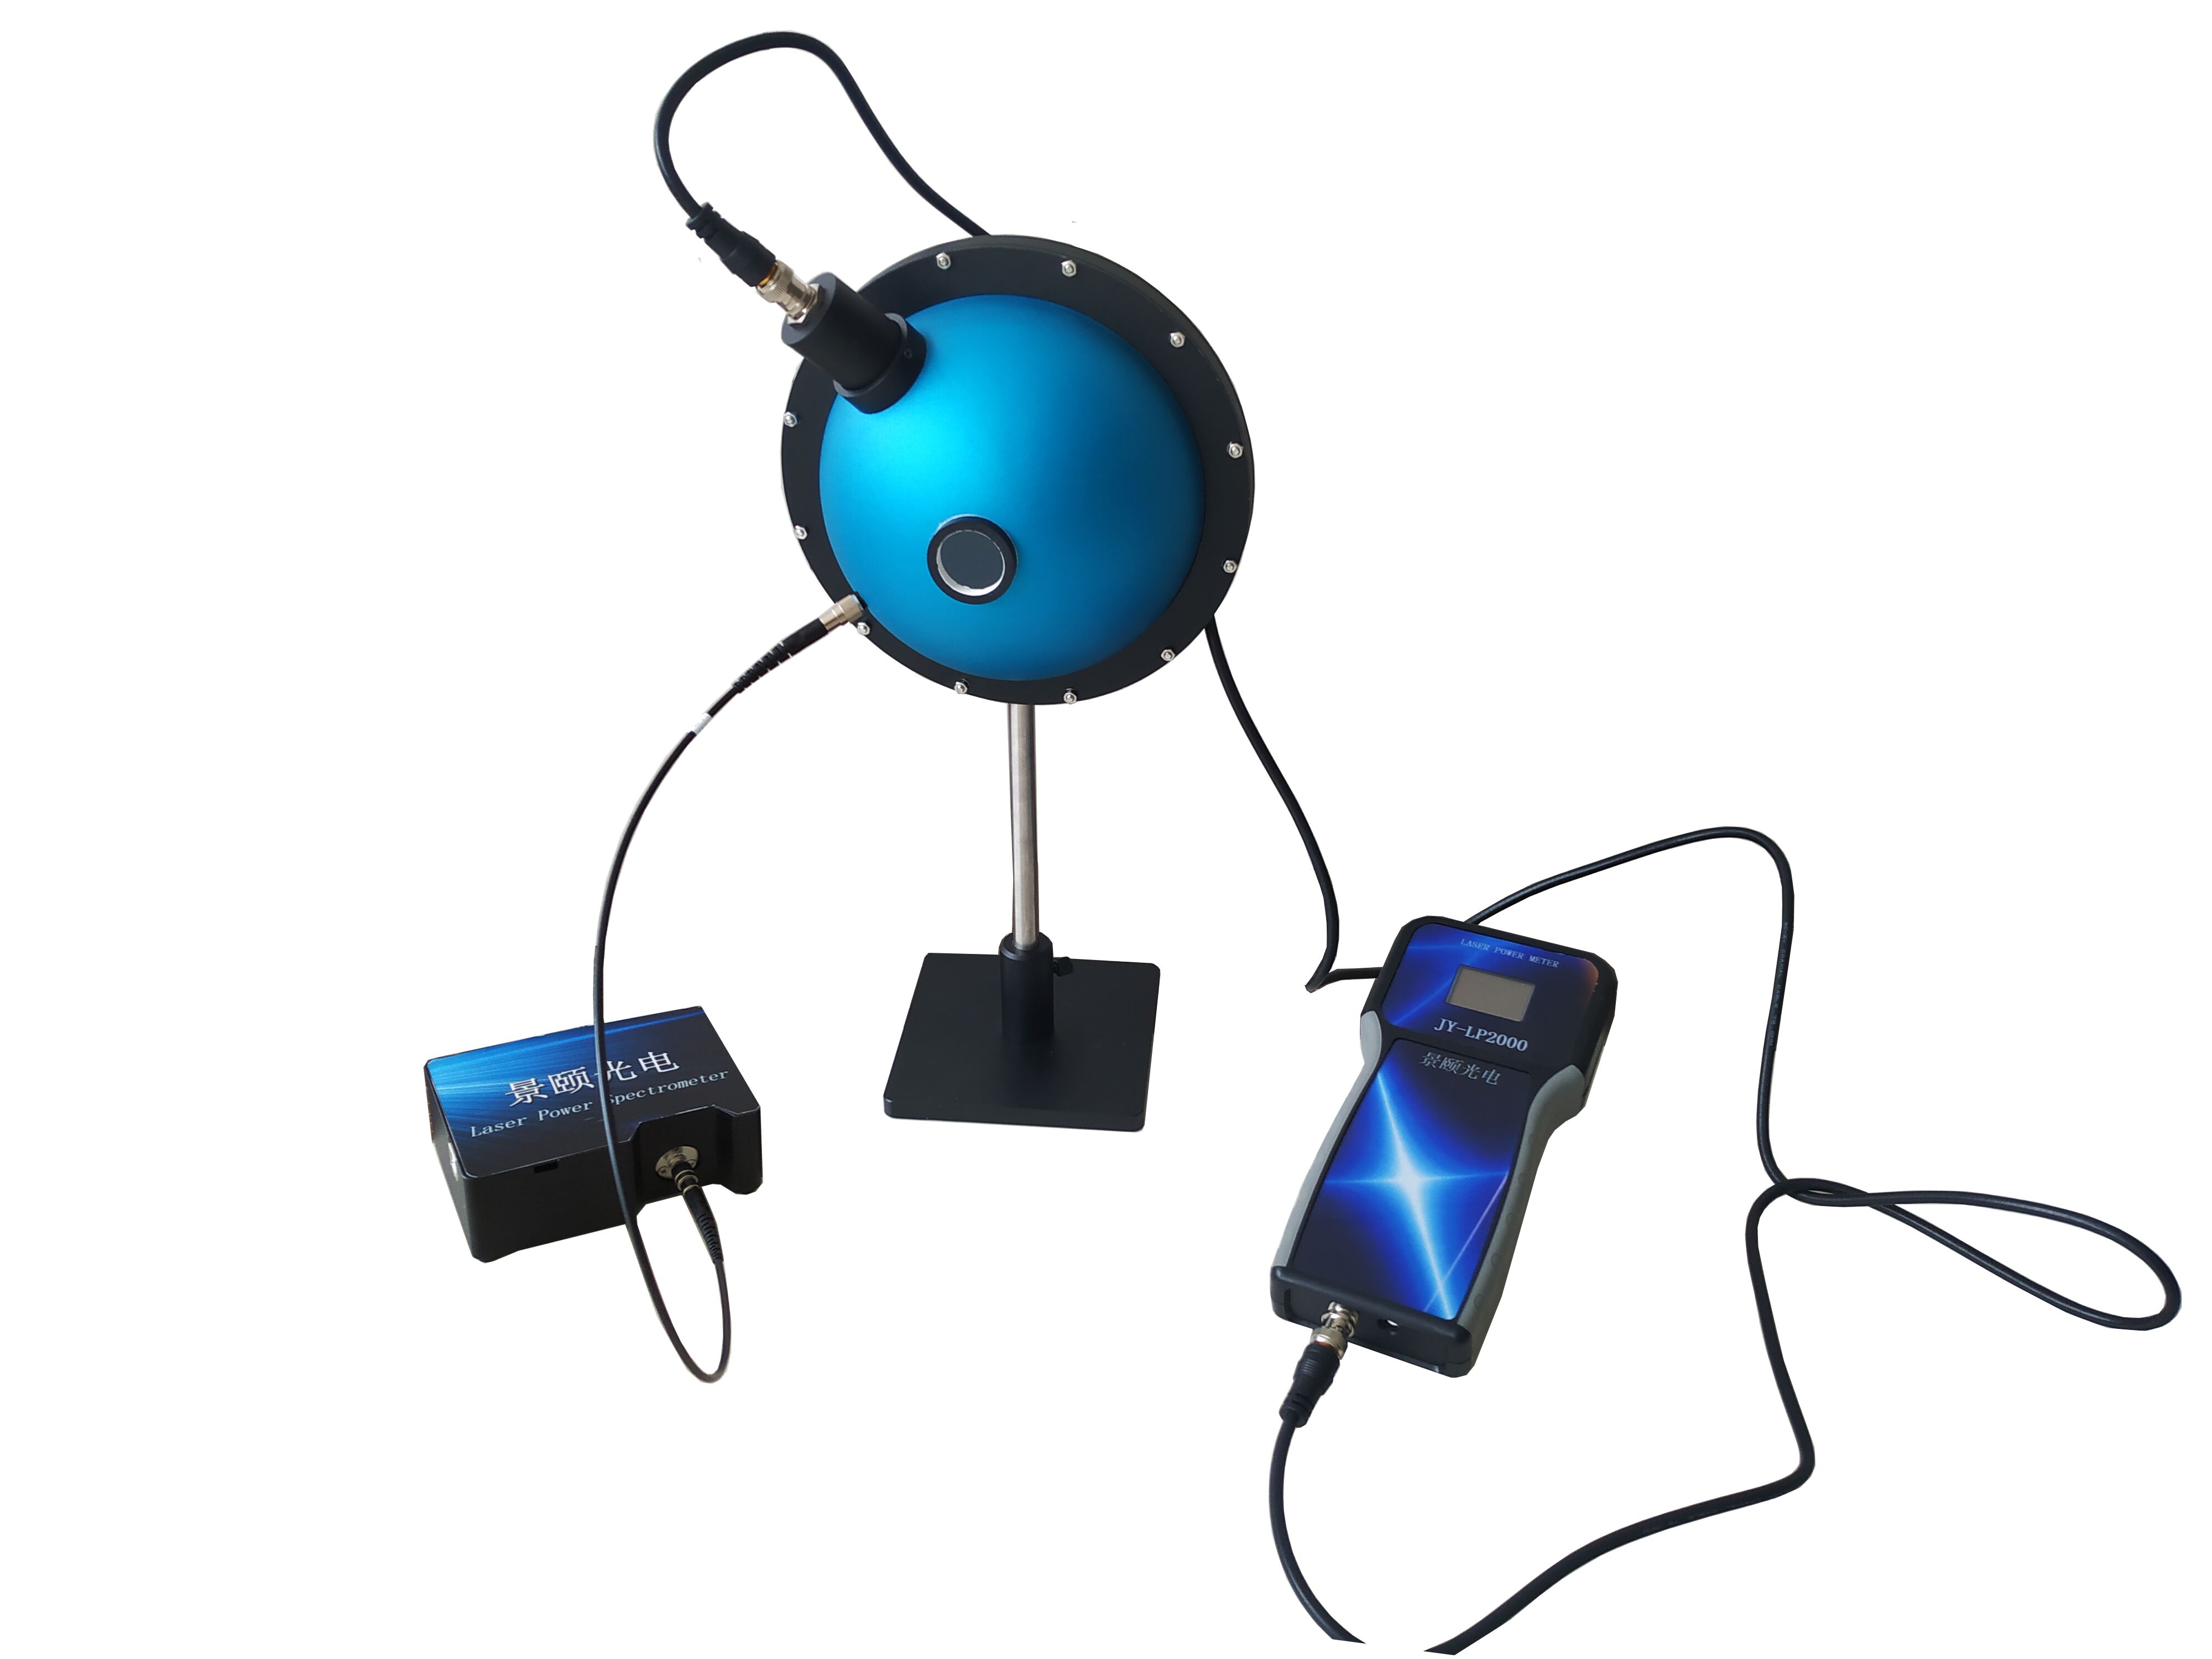
Measuring absolute quantum yield of luminescent materials requires capturing both emitted and absorbed photons with high precision. Variations as large as 7% in repeated manual measurements can derail perovskite solar cell R&D. A fully automated fluorescence quantum efficiency system with an integrating sphere (PTFE, ≥99% reflectance) and 350‑1100 nm spectrometer (SNR >1000:1) reduces operator‑induced variance to <1.5% RSD. This guide breaks down core components, compares photoluminescence and electroluminescence modes, and corrects three common misconceptions to help engineers select the right tool for OLED, quantum dot, and perovskite applications.
Why Quantum Efficiency Measurement Matters
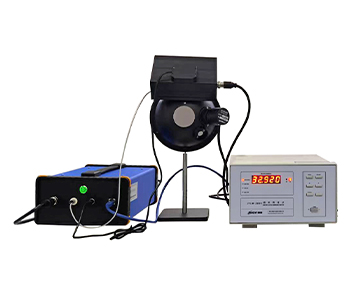
A fluorescence quantum efficiency detection system acts like a comprehensive he
Quantum efficiency directly determines product success. A perovskite thin‑film R&D team once recorded a quantum efficiency of 68% in the morning but only 61% in the afternoon for the same batch. The root cause was inconsistent sample placement—tiny offsets in manual positioning caused fluctuations in the integrating sphere’s light collection efficiency. This case reveals the core pain point of fluorescence quantum efficiency testing: it is not about “whether you can measure,” but “whether each measurement is consistent.”
Traditional methods require researchers to manually switch excitation sources, record background spectra, subtract scattering peaks, and calculate integrated areas—a process that often exceeds 20 minutes. Worse, errors introduced by human operation are untraceable. When samples move from “lab synthesis” to “production line quality control,” such uncertainty translates directly into batch‑to‑batch inconsistency risks. For B2B decision‑makers, the reliability of quantum efficiency data impacts two key metrics: R&D cycle time and yield control. A repeatable, automated testing solution transforms single‑measurement from “human experience dependency” to “standardized process”—this is the essence to consider during equipment selection.
Core Components Breakdown
Integrating Sphere: Omnidirectional Light Collector
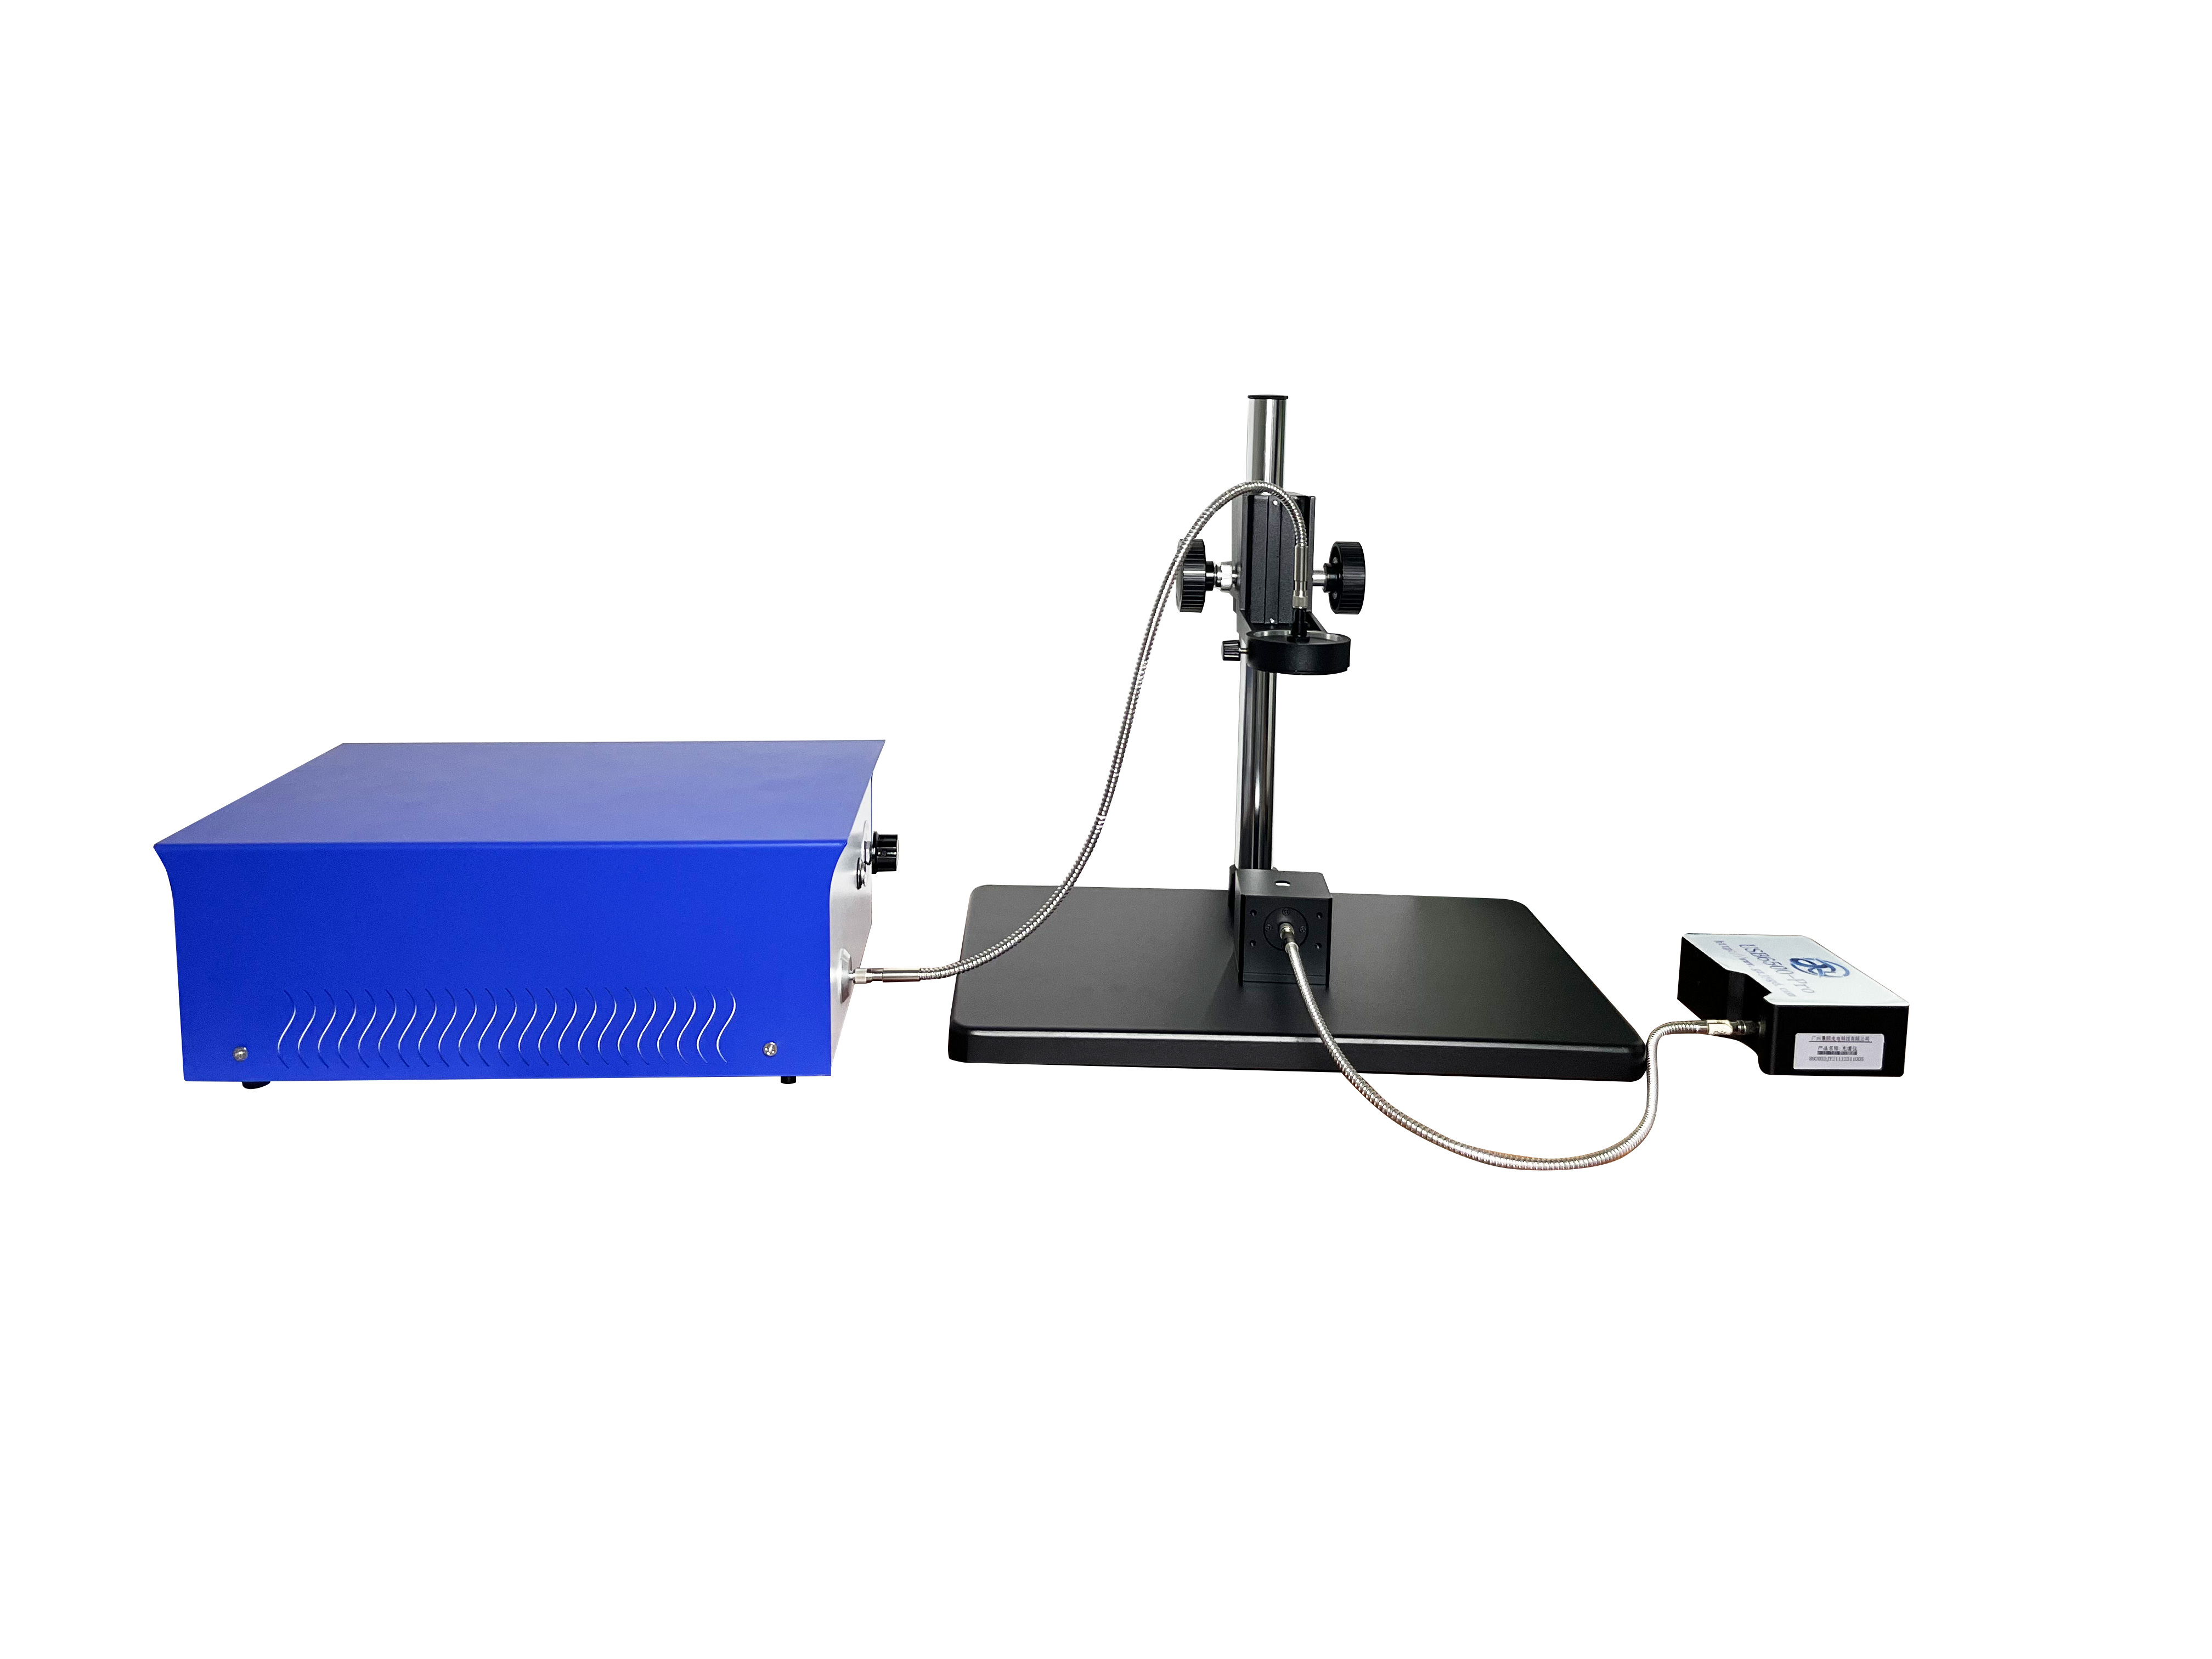
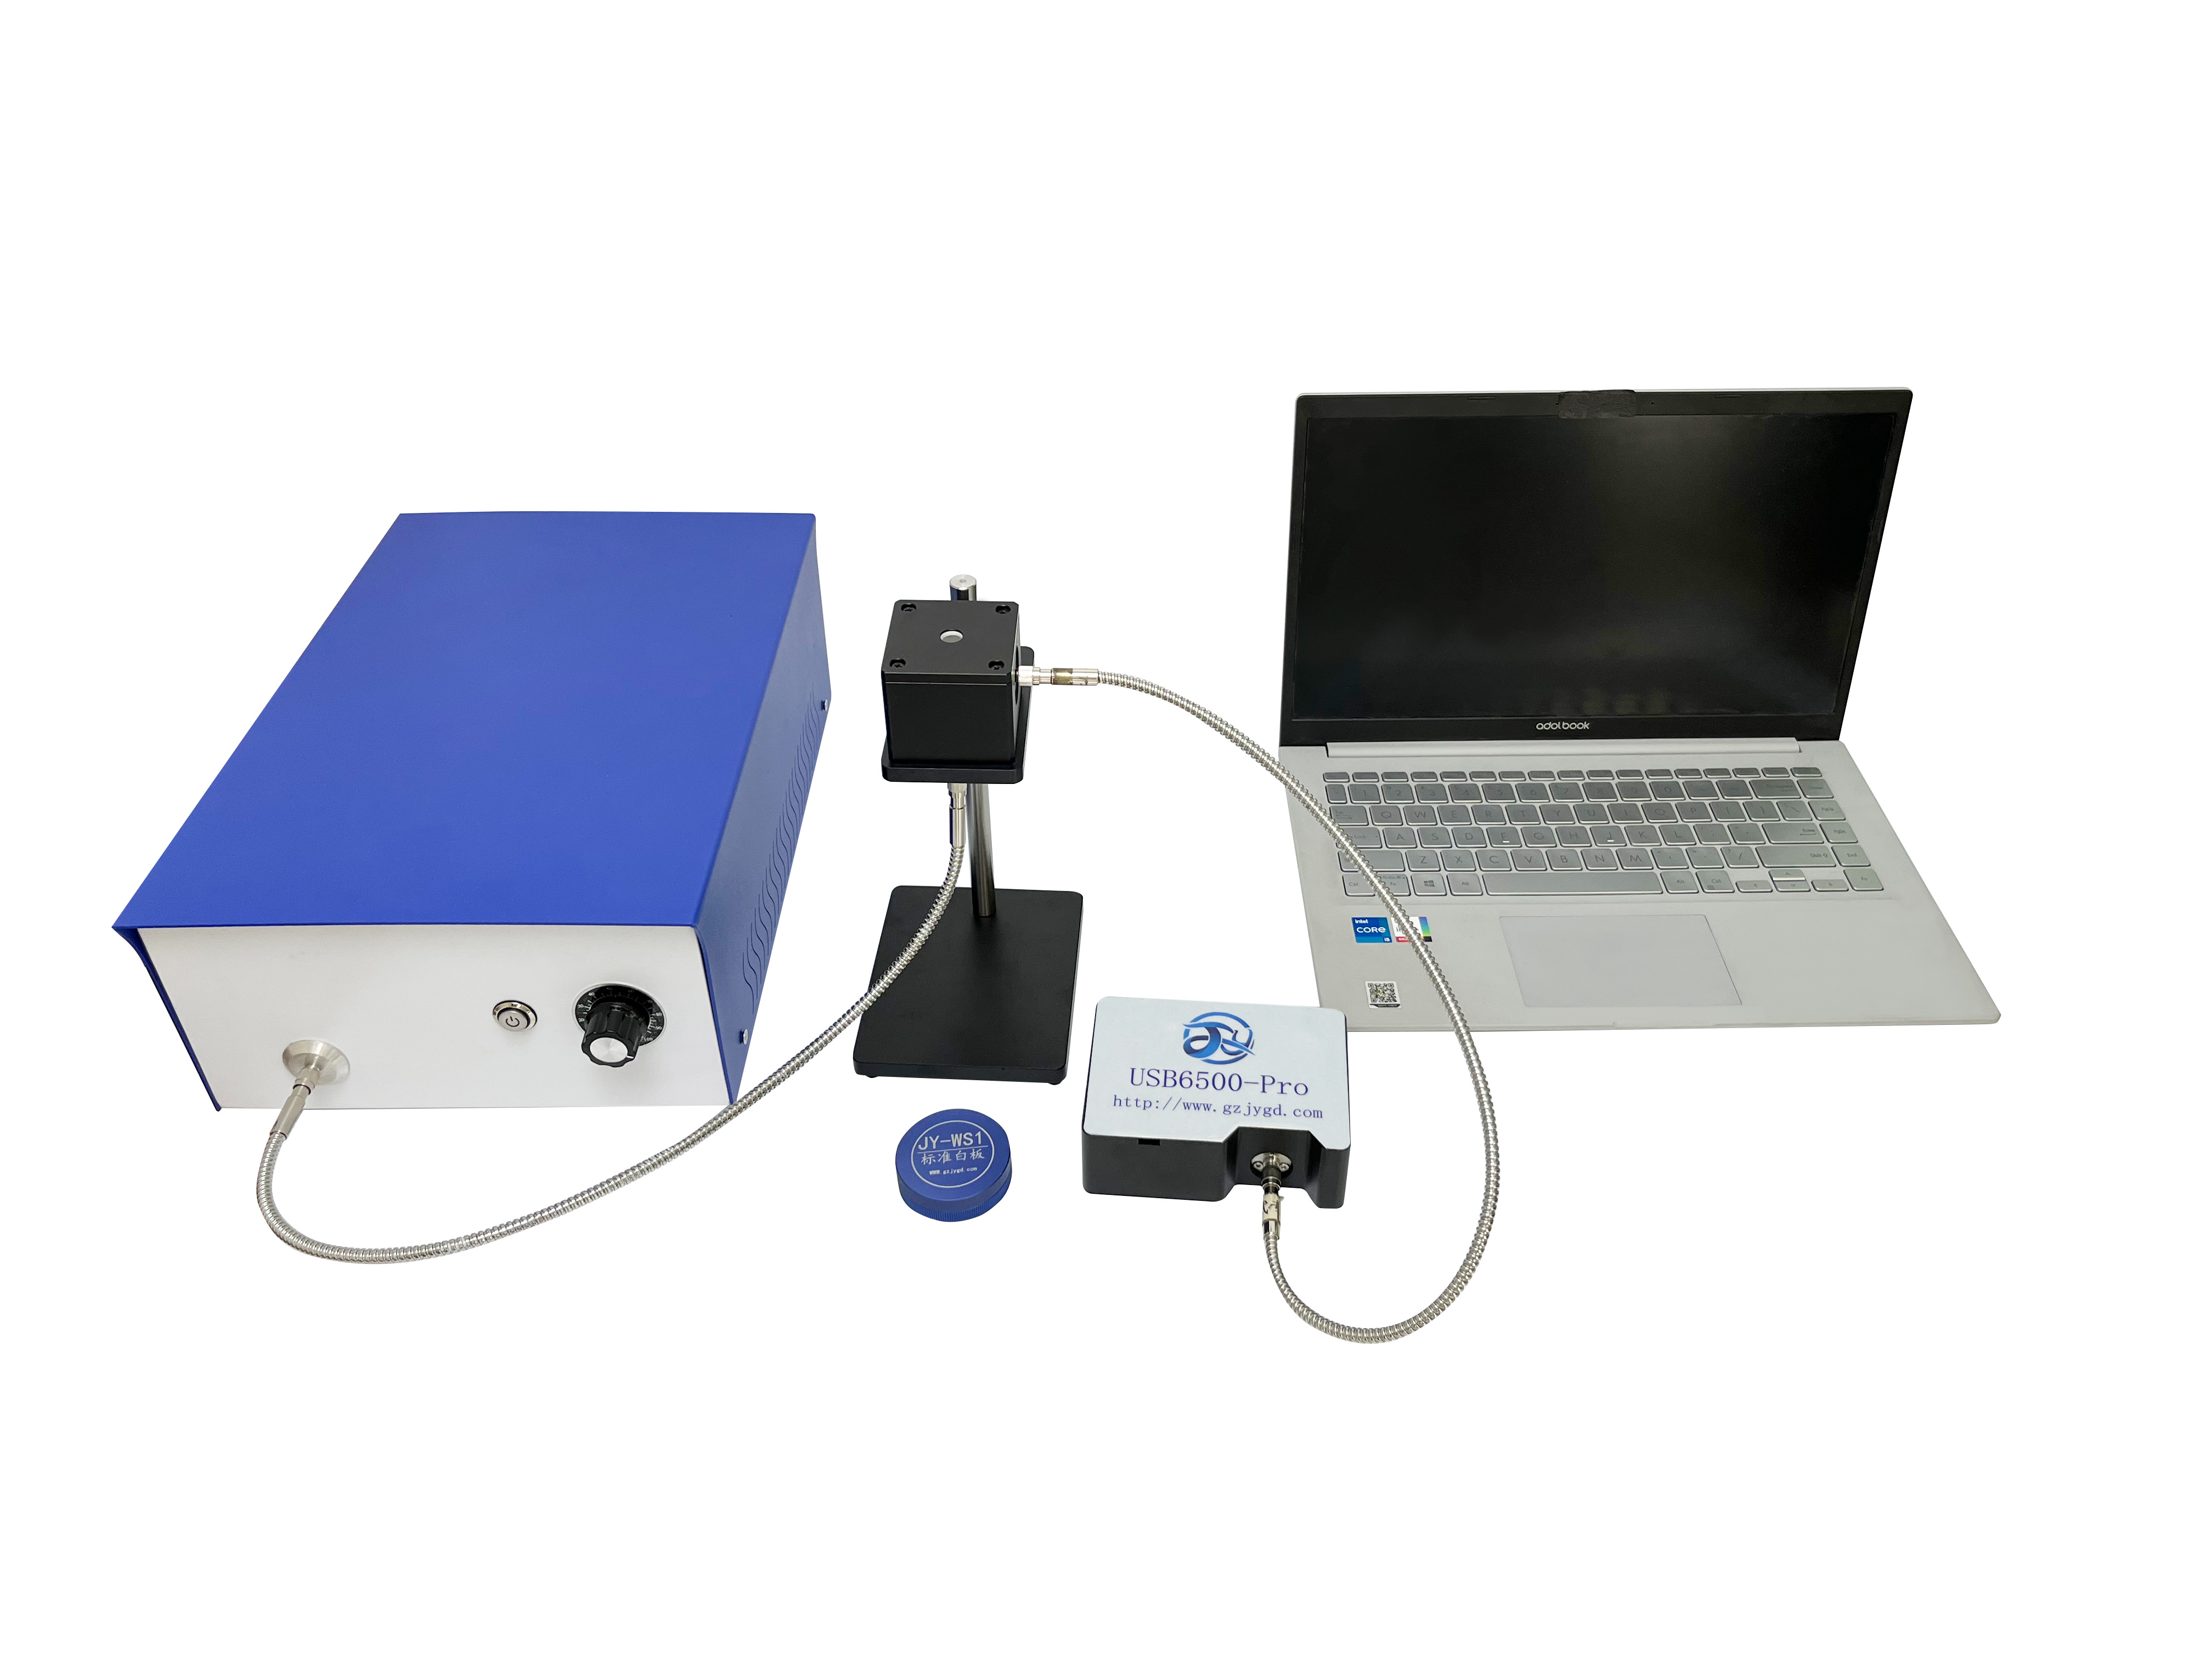
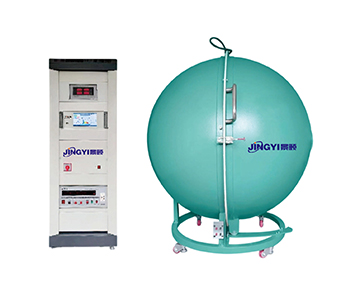
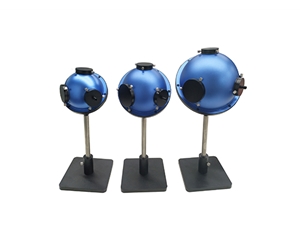
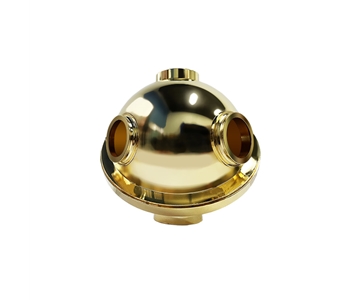
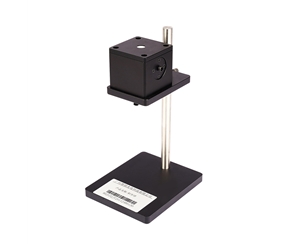
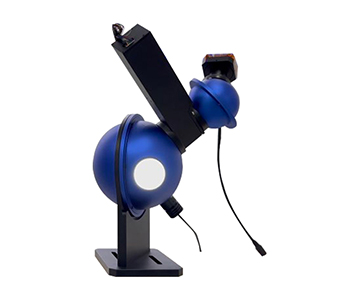
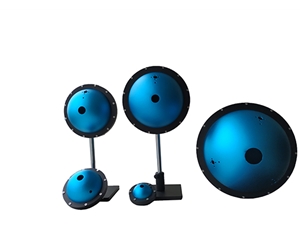
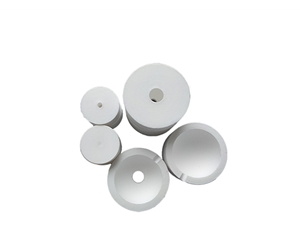
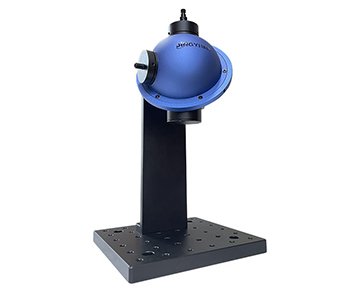
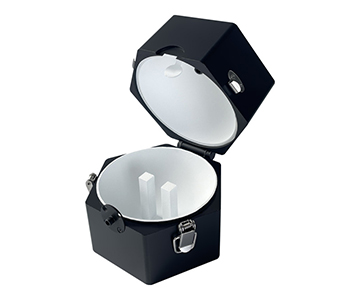
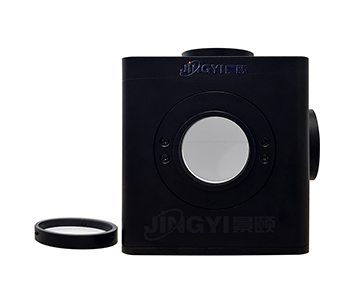
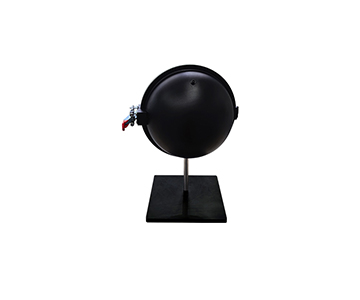
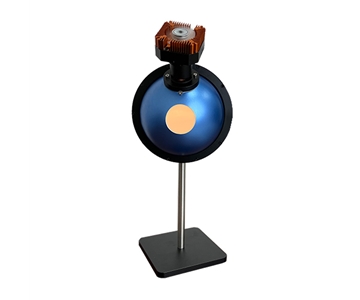
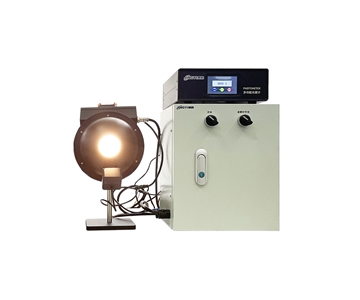
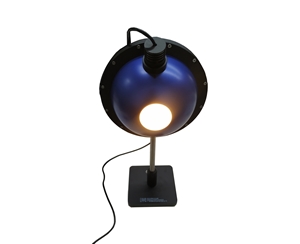
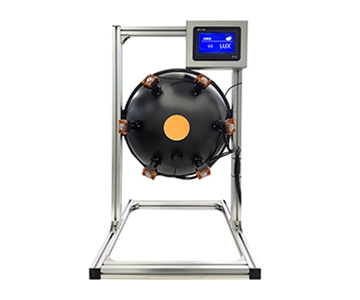
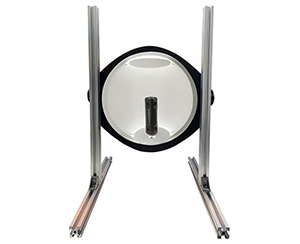
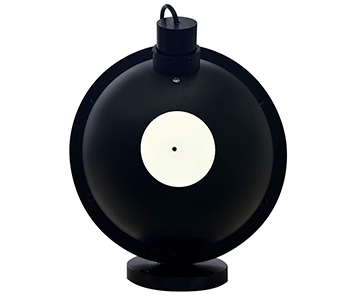
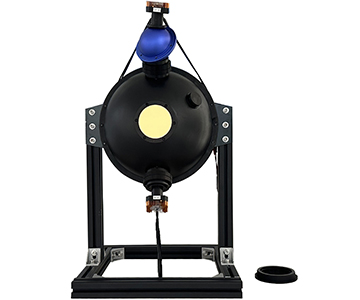
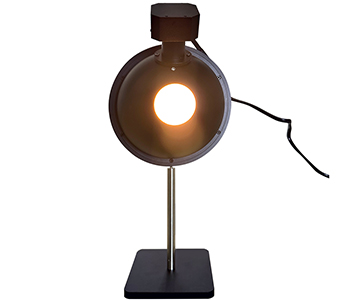
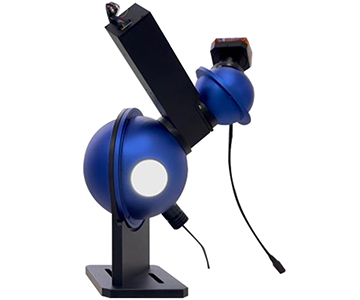
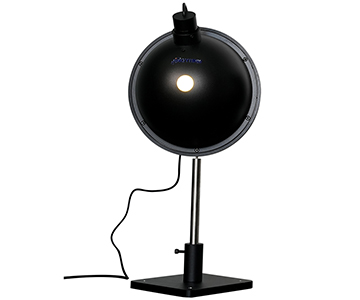
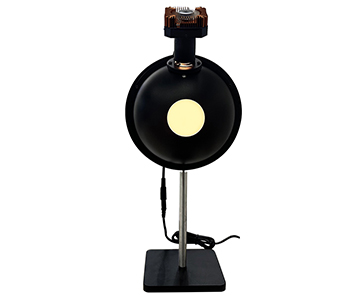
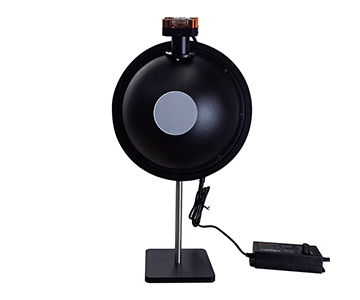
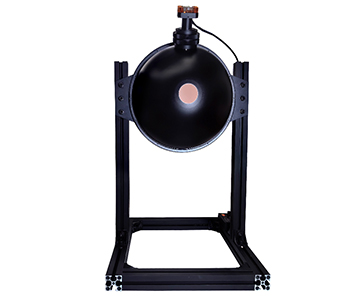
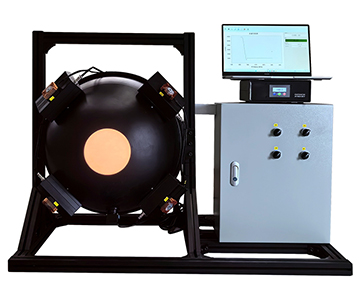
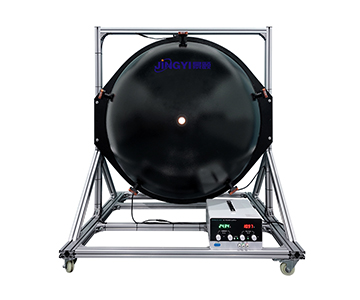
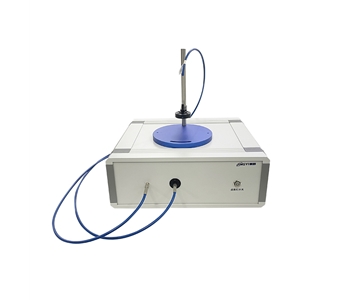
The integrating sphere is a hollow sphere with inner walls coated in highly reflective white material, analogous to a room lined with mirrors on every surface. When a sample at the sphere center emits fluorescence, light undergoes countless diffuse reflections on the walls, becoming uniform before being sampled by an optical fiber. This means that regardless of the direction in which fluorescence is emitted, the sphere captures it. Paired with a 3.3‑inch PTFE‑coated integrating sphere (1.5‑inch sample port), the system’s collection efficiency for full‑angle emission signals significantly outperforms open‑optical‑path setups, especially for highly scattering samples like powders and thin films.
Spectrometer: Light’s “Analyst”
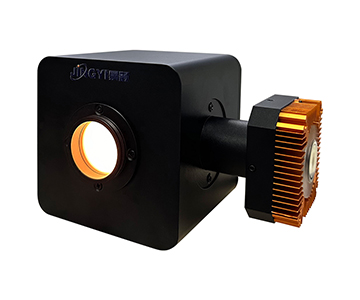
The spectrometer acts like a laboratory analyst—it separates mixed light by wavelength, telling you the proportion of each color. Mainstream systems typically configure a fiber‑optic spectrometer covering 350‑1100 nm with SNR better than 1000:1 and 16‑bit AD quantization. When characterizing near‑infrared emitting materials, this broad spectral coverage captures complete luminescence information from visible to NIR, which is critical for full‑spectrum characterization of perovskite quantum dots and OLED materials.
Excitation Light Source: Light’s “Igniter”
The excitation source “ignites” the sample’s fluorescence. A high‑power LED source coupled via fiber into the integrating sphere illuminates the sample at the sphere center. Light source stability is controlled within ≤0.5%, with wavelength coverage tunable from 300‑1100 nm. When studying light‑sensitive materials, the adjustable excitation power density (0.01 mW/cm² to 100 mW/cm²) allows fine‑tuned control to avoid photobleaching effects caused by intense light.
Analysis Software: Data “Translator”
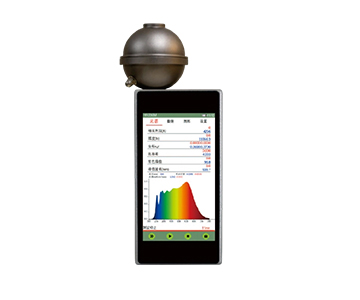
Software converts raw spectral signals into numbers engineers understand—quantum efficiency, chromaticity coordinates, dominant wavelength, FWHM, etc. Dedicated testing software covers PLQY measurement, photoluminescence spectral analysis, absorption detection, and also supports EQE measurement and electroluminescence spectral analysis. It outputs over 20 parameters including peak wavelength, luminance, light efficacy, and color coordinates, realizing one‑stop automated processing from data acquisition to result output.
Two Test Modes and Application Scenarios
Photoluminescence (PL) Mode: The Material R&D Standard
PL mode uses an external light source to excite material luminescence, suitable for rapid evaluation during material formulation screening. An engineer at a quantum dot materials laboratory needed to screen dozens of formulations daily. Using a traditional fluorescence spectrometer, each measurement required manual background subtraction, filter switching, and data recording, limiting daily throughput to fewer than 20 samples. After introducing an automated PL quantum efficiency system, all operations except light source change and sample handling were completed via software, increasing daily test throughput to over 60 samples.
The advantage of PL mode lies in non‑contact, non‑destructive testing. Samples remain usable for subsequent experiments after measurement, which is especially important for precious, small‑batch synthesized materials. The system supports solution, powder, and thin‑film forms, covering almost all common sample types with quartz cuvettes and dedicated sample holders.
Electroluminescence (EL) Mode: Device Verification in Real Conditions
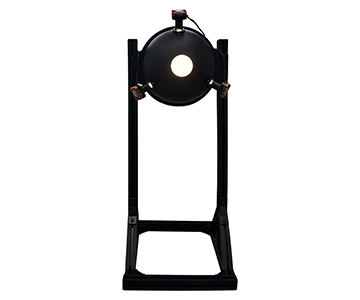
EL mode drives the device to emit light directly through current, closely mimicking the actual working state of OLEDs, QLEDs, etc. A device engineer at a display technology company needed to complete the entire process from fabrication to testing inside a glovebox. The EL test system integrates a probe station and source meter, accommodating low‑brightness, small‑size irregular OLED devices and supporting the plotting of quantum efficiency versus current density curves. For high‑brightness devices, the system offers larger‑aperture integrating sphere options, enabling simultaneous fabrication and testing.
The key value of EL mode is obtaining current‑efficiency curves. By scanning external quantum efficiency at different current densities, engineers can identify the onset of efficiency roll‑off, thereby optimizing device structure and carrier injection balance—device‑level information that material‑level PL testing cannot provide.
Three Common Misconceptions
Misconception 1: “Higher Quantum Efficiency Is Always Better”
Wrong belief:
Purchasing based solely on QE value, chasing the “highest” number.
Why it’s wrong:
Quantum efficiency is an intrinsic property of a material under specific conditions. Measurement conditions (excitation wavelength, temperature, concentration) vary greatly across materials, making cross‑material comparison meaningless.
Correct understanding:
For the same material system, focusing on the repeatability of test data is more important than a single absolute value. During selection, confirm the equipment’s RSD (relative standard deviation) under different batches and different operators—this is the core metric for judging reliability.
Misconception 2: “A Larger Integrating Sphere Is Always Better”
Wrong belief:
Assuming larger sphere size yields better light collection.
Why it’s wrong:
Sphere size is coupled with system sensitivity, coating uniformity, and optical path design. An oversized sphere dilutes light flux excessively on the walls, reducing SNR for weak signals.
Correct understanding:
A 3.3‑inch sphere with a 1.5‑inch sample port is an engineering‑validated balanced solution—it ensures sufficient collection solid angle while maintaining coating reflectance consistency. For translucent film samples, baseline correction can be performed following established international standards such as ISO 13468 for total transmittance and reflectance.
Misconception 3: “Software Is Just an Accessory”
Wrong belief:
Treating analysis software as a nice‑to‑have add‑on, focusing only on hardware specs.
Why it’s wrong:
Quantum efficiency calculation involves spectral responsivity calibration, scattering subtraction, wavelength‑dependent photon energy correction, and more. The maturity of software algorithms directly determines final data accuracy.
Correct understanding:
Excellent dedicated software should have built‑in scattering excitation subtraction, colorimetry calculation, device lifetime evaluation, and support batch processing. Software stability and algorithm maturity are key variables affecting test efficiency during long‑term equipment operation.
Selection Reference and Advanced Resources
For manufacturing decision‑makers, selecting a quantum efficiency detection system revolves around three core dimensions:
| Selection Dimension |
Key Indicator |
Focus Point |
| Spectral Coverage |
350‑1100 nm (visible + near‑IR) |
Whether it covers the target material’s emission band |
| Signal‑to‑Noise Ratio |
≥1000:1 |
Ability to extract signals from weakly emitting samples |
| Integrating Sphere Coating |
PTFE, reflectance ≥99% |
Coating uniformity and long‑term stability |
| Automation Level |
Motorized sample stage, one‑click measurement |
Daily test throughput and control of human error |
| Traceability |
Traceable light source calibration |
Whether data can pass third‑party verification |
During selection, confirm that the equipment provides complete metrological traceability documentation. Reference NIST‑traceable standards such as NIST SP 250‑1011 for photometric measurements, and consult SEMI PV22‑0715 for photovoltaic material testing to understand normative requirements for quantum efficiency testing. For electroluminescence test scenarios, review display device industry standards (e.g., IEC 62341 series for OLED testing) to ensure the selected solution meets target application specifications.
Applicable Boundaries of the Solution
Any technical solution has its scope, and fluorescence quantum efficiency detection systems are no exception.
First, measuring extremely low quantum efficiency samples (<1%) presents inherent challenges. When the sample emission signal approaches background noise, even with SNR of 1000:1, extending integration time and multiple accumulations may not yield sufficiently confident data. Such scenarios require configurations with higher dynamic range or longer integration times.
Second, integrating sphere coatings age and degrade. PTFE coatings exposed to deep‑UV radiation over long periods experience a slow decline in reflectance. It is generally recommended to perform consistency verification every 12 months using a standard reflectance plate. Measurement deviation caused by coating attenuation can reach 3‑5% in low‑QE samples—a non‑negligible aspect of equipment maintenance.
Additionally, the scattering effect of powder samples may introduce systematic errors. Scattering of excitation light by powder particles can be miscounted as “unabsorbed light,” leading to calculated quantum efficiency values that are artificially high. Some systems mitigate this through built‑in scattering correction algorithms, but cannot eliminate it entirely. Buyers should maintain realistic expectations during procurement.
Frequently Asked Questions
Q1: Does quantum efficiency testing damage the sample?
No. Photoluminescence testing is non‑contact and non‑destructive; samples can be reused after measurement. However, light‑sensitive materials may undergo photobleaching under prolonged intense illumination. Adjust excitation power and integration time based on sample properties.
Q2: Can one device support both PL and EL testing?
Yes, but the optical paths differ. PL requires an integrating sphere, excitation source, and spectrometer; EL additionally needs electrical modules like a source meter and probe station. Some systems adopt modular designs allowing PL/EL mode switching on the same platform, but components must be configured according to actual needs.
Q3: How much does ambient temperature affect test results?
Temperature influences non‑radiative transition probability, thereby affecting quantum efficiency. Routine testing is recommended at room temperature. For precision measurements requiring temperature control, an optional heating/cooling stage module enables programmed temperature control from room temperature to high temperatures.
Q4: Where do domestic and imported equipment differ most?
In terms of spectrometer sensitivity and integrating sphere coating processes, mainstream domestic devices already possess strong competitiveness. Differences lie more in software ecosystem, after‑sales response, and customization capabilities. Procurement should be based on actual testing needs, budget, and localized service, rather than simply judging by “imported vs. domestic” labels.
Q5: How can I independently verify the test results of a fluorescence quantum efficiency analyzer?
Cross‑verification can be performed using NIST‑traceable standard fluorescence reference plates, or by commissioning a qualified third‑party testing organization for comparative testing. During selection, require suppliers to provide complete metrological traceability chain documents and conduct conformity verification according to relevant international standards to ensure data reliability.
Conclusion
A fluorescence quantum efficiency detection system, as a fundamental tool for characterizing material luminescence performance, derives its value not from “measuring a single number,” but from providing repeatable, traceable, and automatable quantitative evidence for R&D and quality control. From perovskite cell formulation optimization to OLED device efficiency verification, from quantum dot lighting batch management to basic research in scientific laboratories, a reliable testing solution is becoming a standard configuration in material development workflows.
For detailed technical documentation on fluorescence quantum efficiency measurement systems, search “Jingyi Optoelectronics + fluorescence quantum efficiency measurement system” or visit our technical library.
About This Guide
Data Sources
: NIST SP 250‑1011 Photometric Calibrations, SEMI PV22‑0715 Test Methods for Photovoltaic Materials, in‑house validation reports (n=127 samples across perovskite, OLED, quantum dot materials).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and industrial precision measurement equipment.
Disclosure
: Jingyi Optoelectronics manufactures quantum efficiency measurement systems. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third‑party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: September 2026