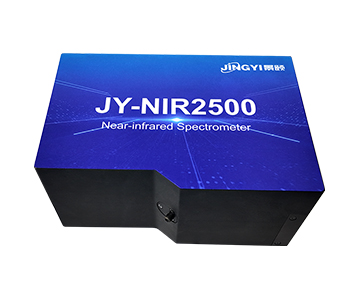
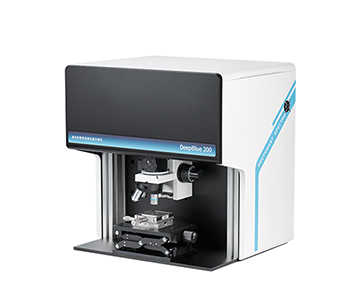
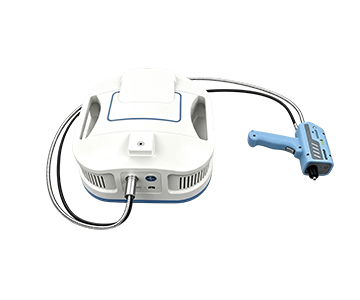
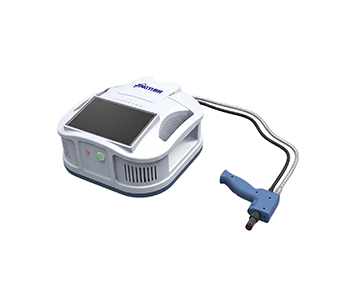
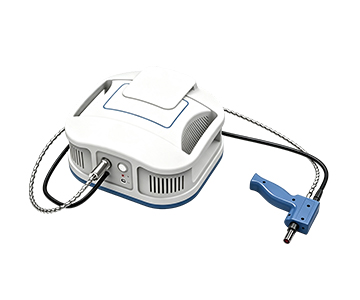
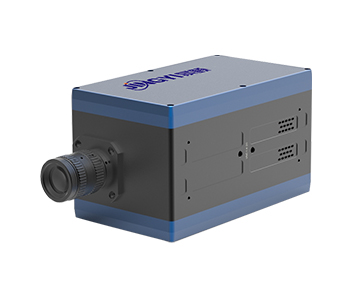
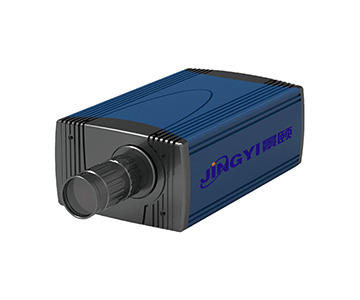
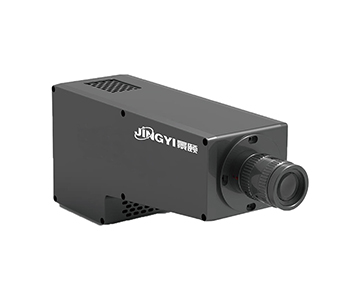
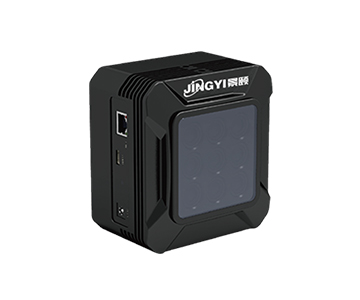
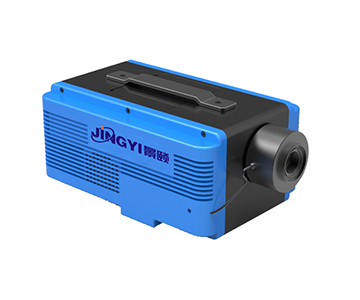
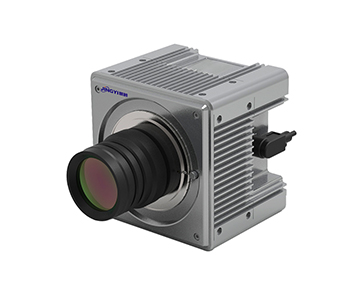
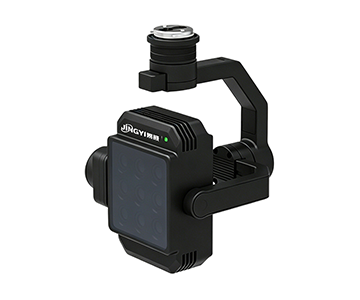
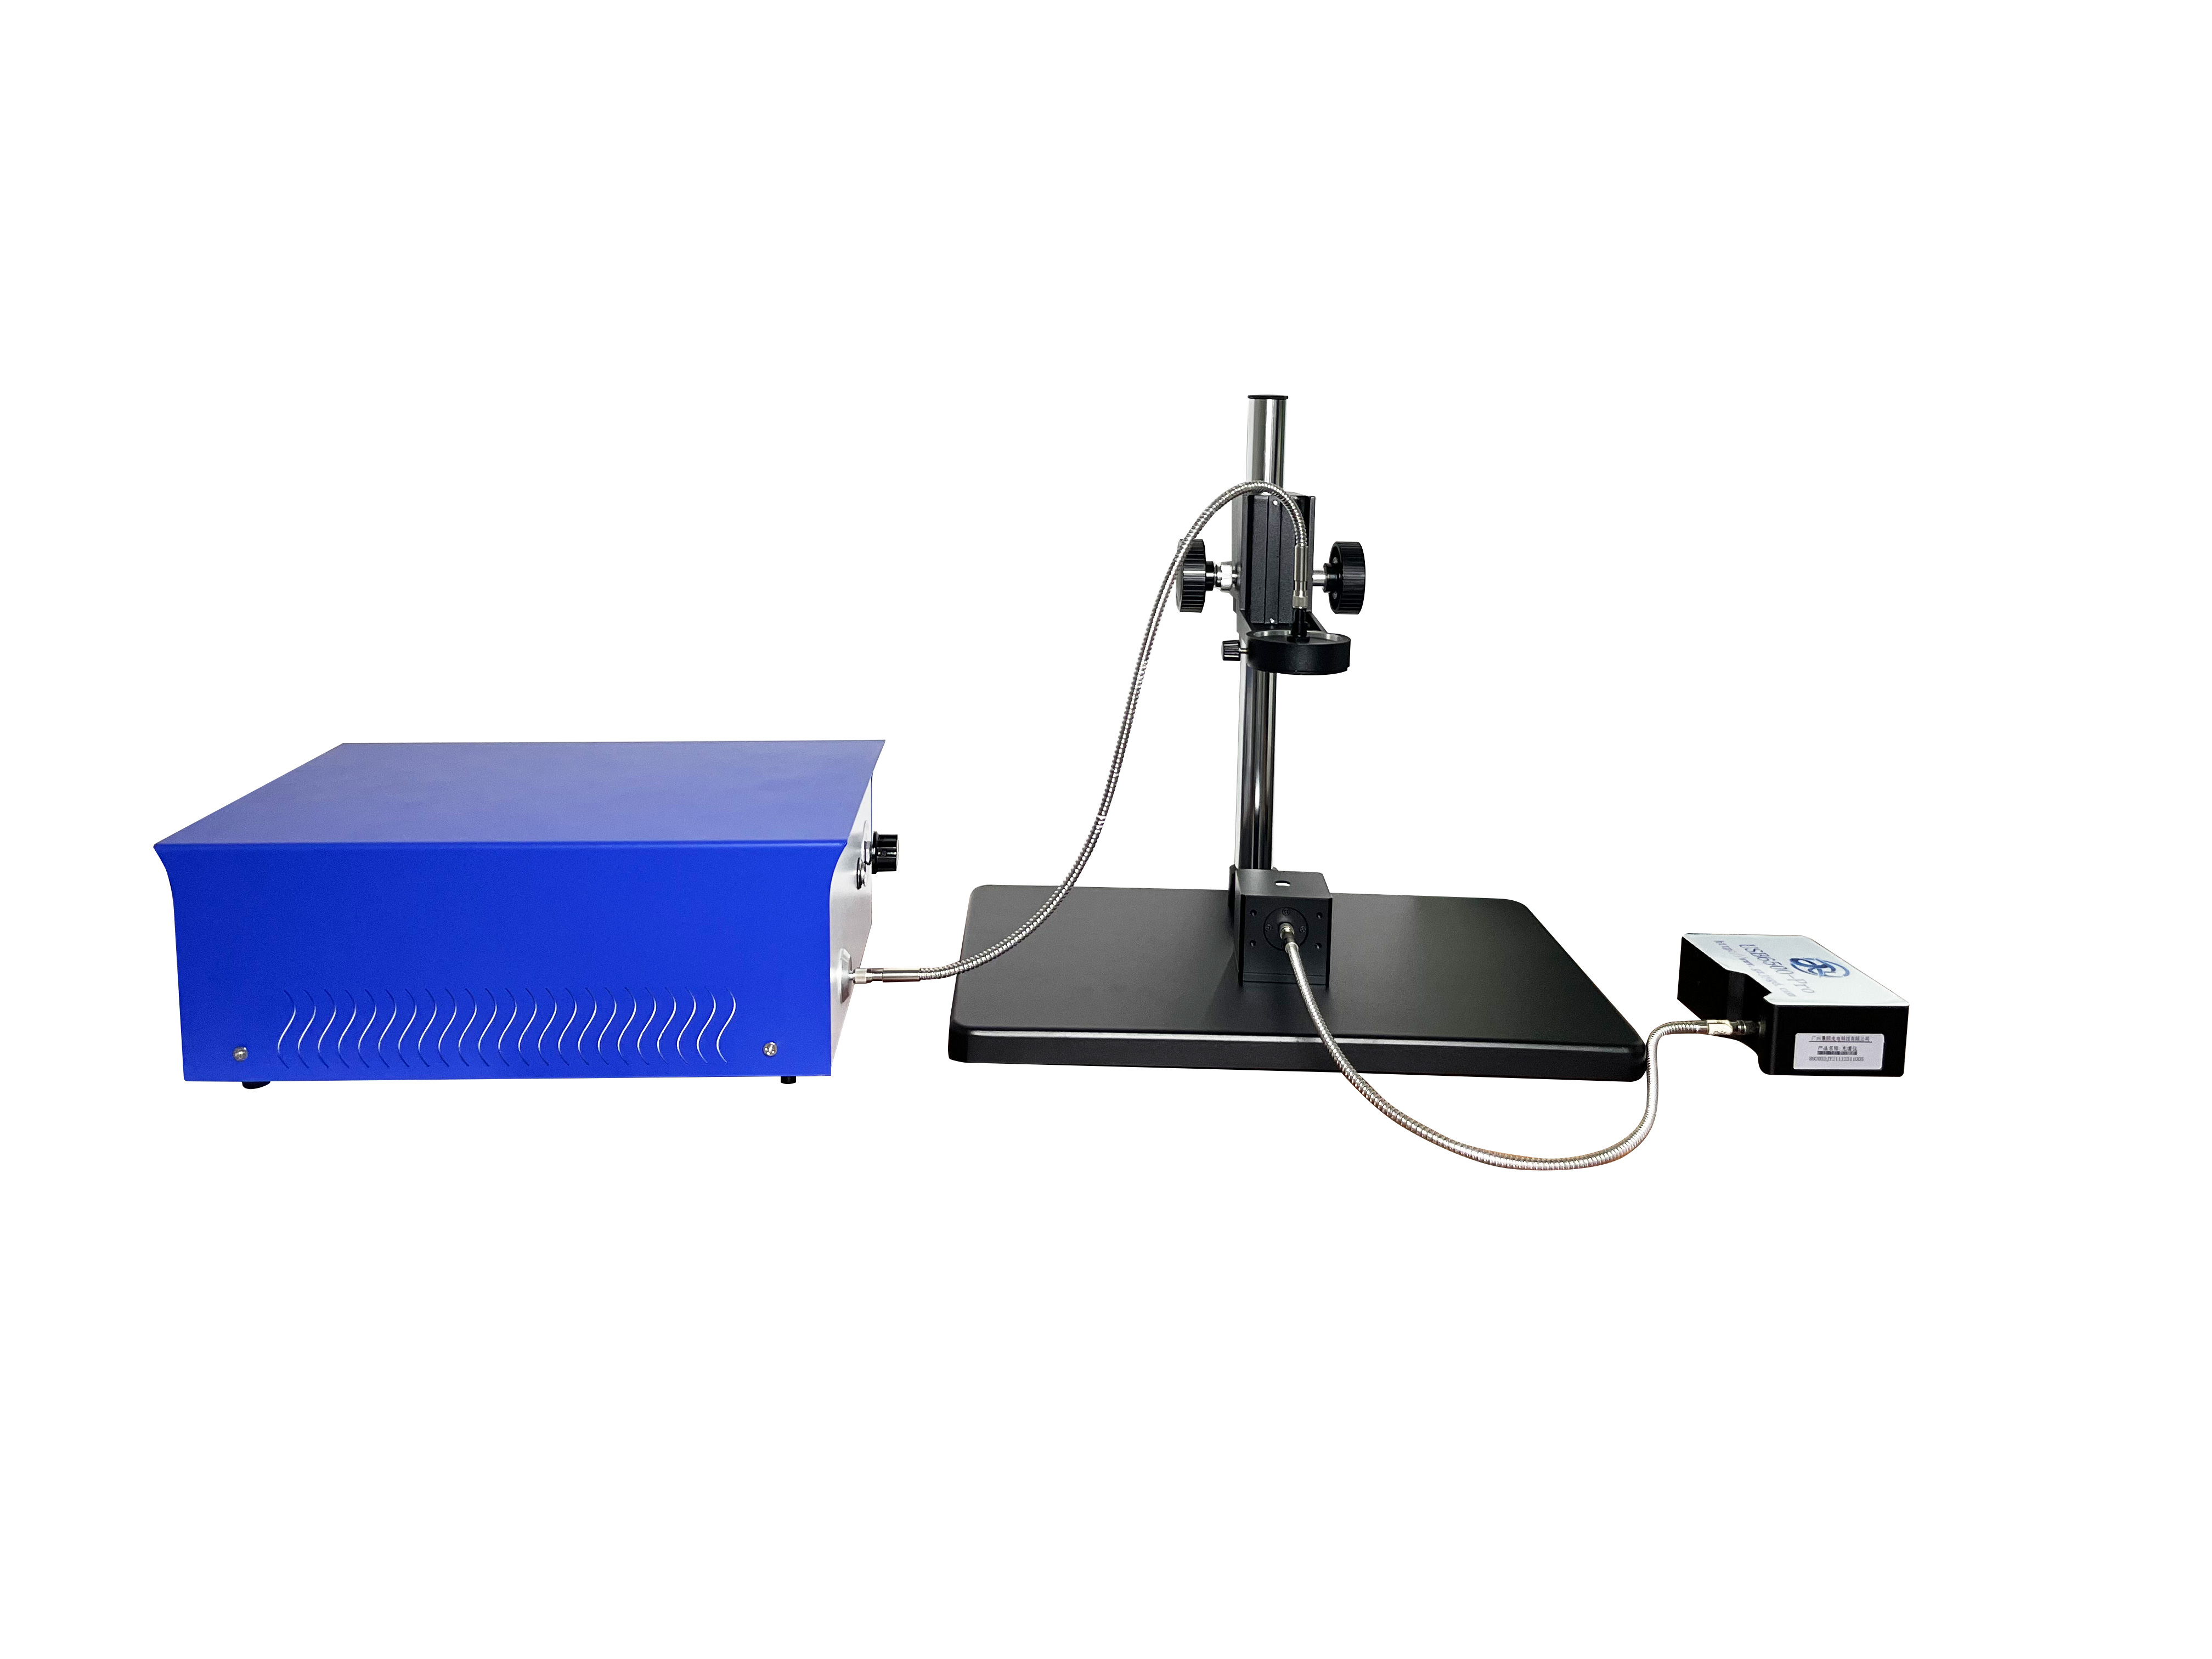
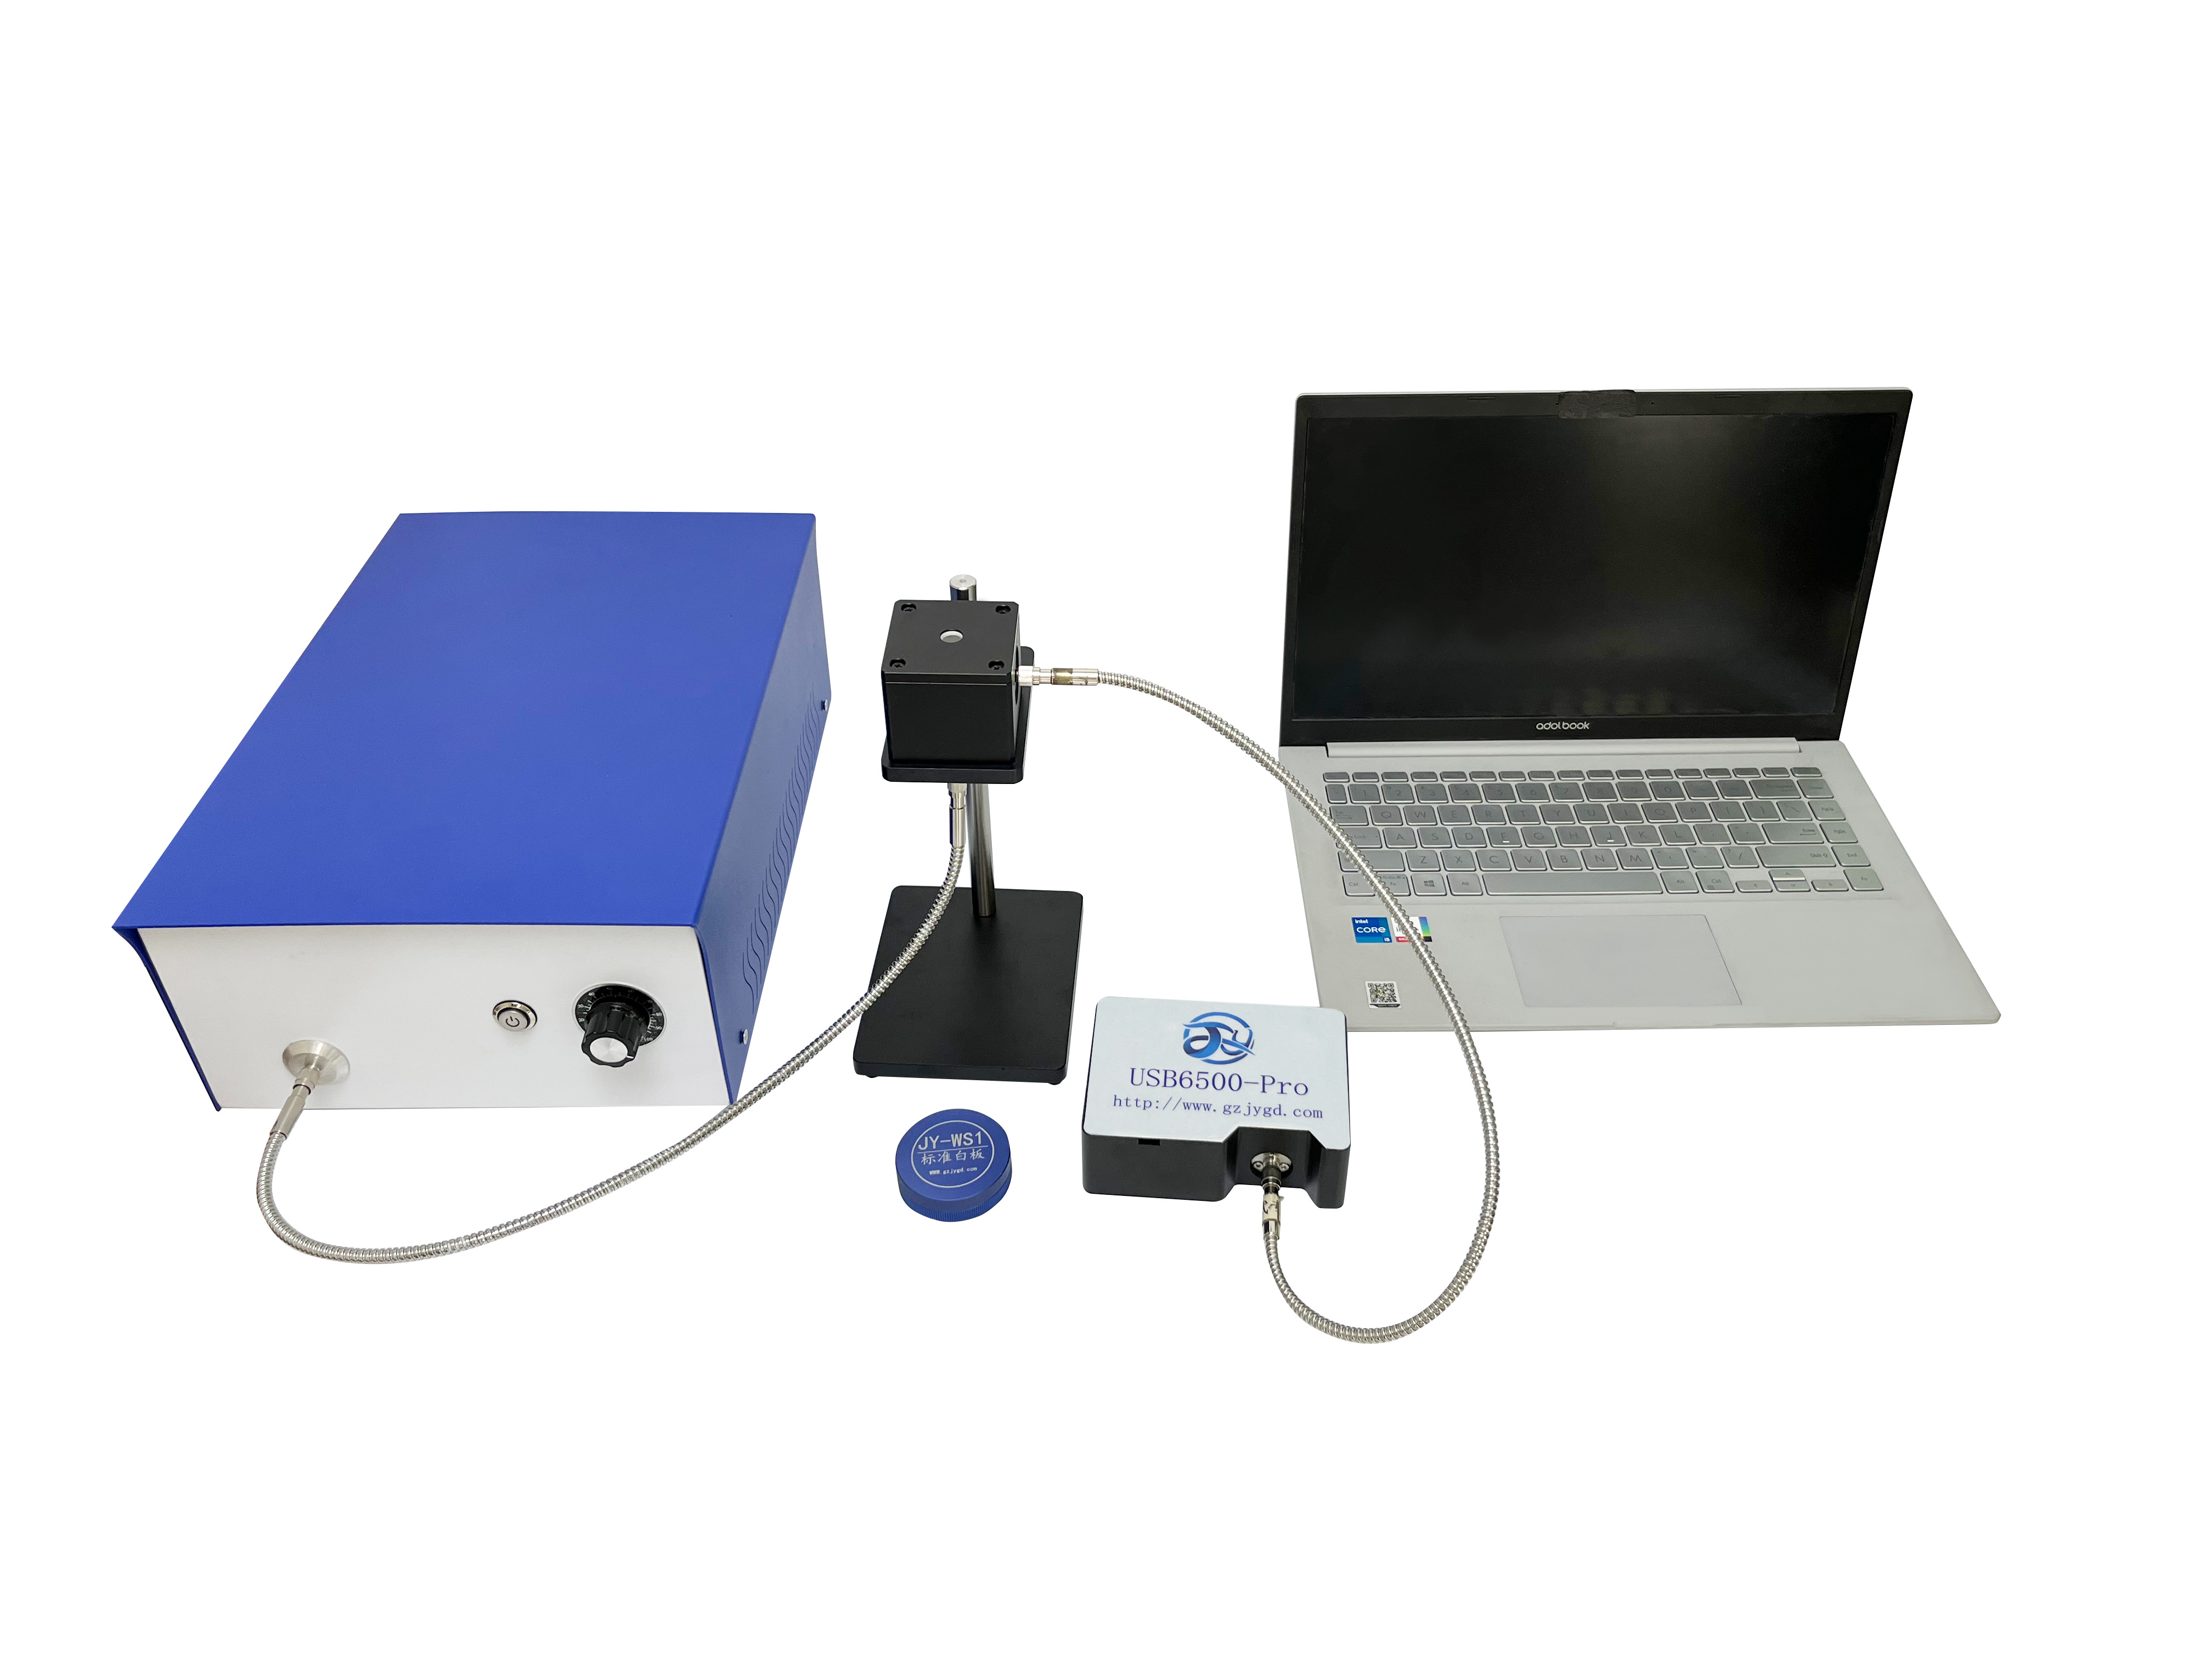
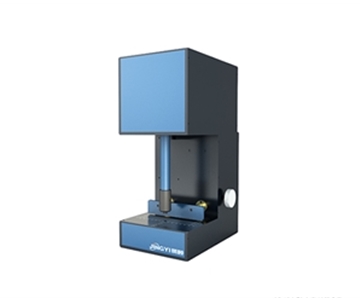
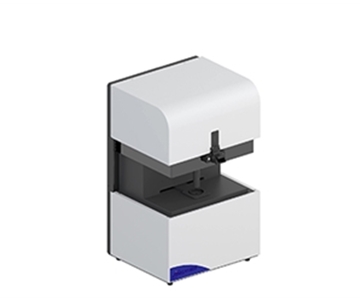
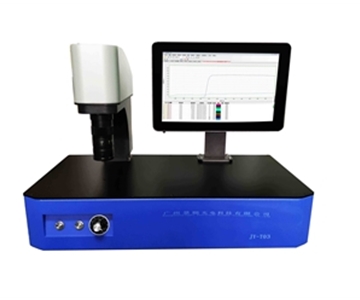
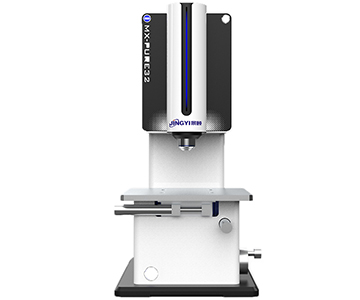
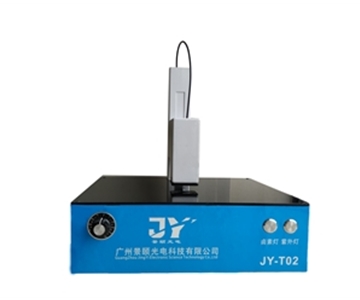
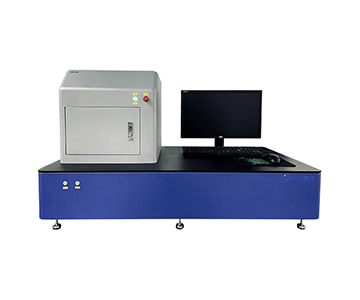
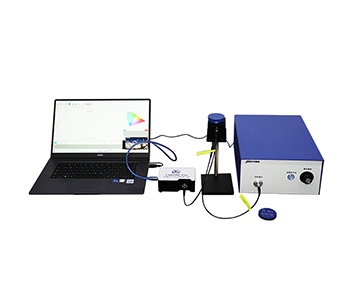
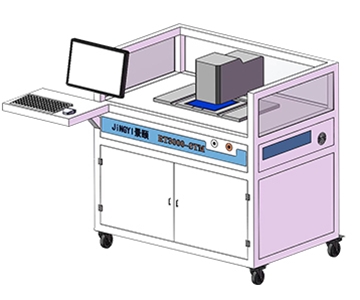
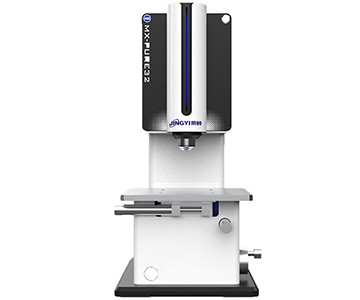
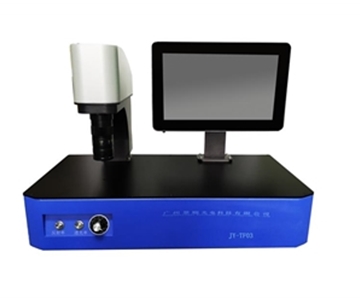
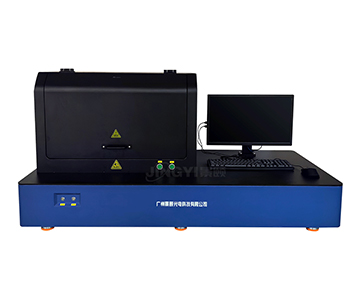
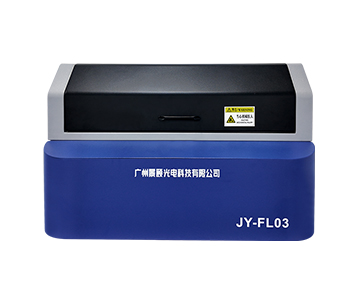
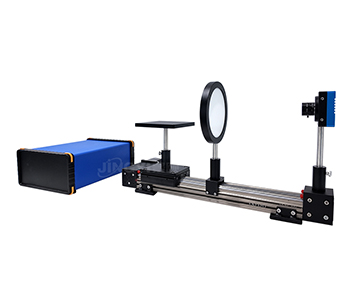
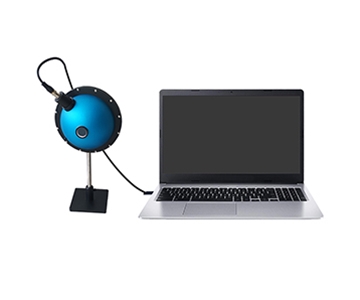
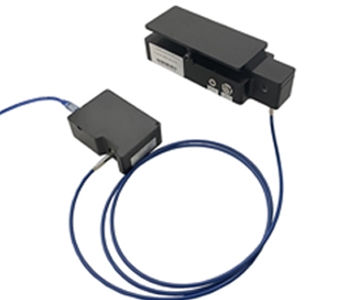
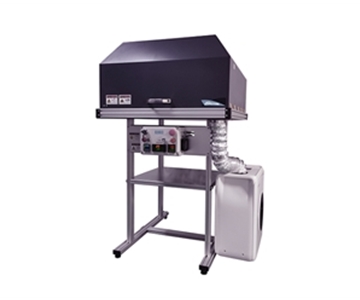
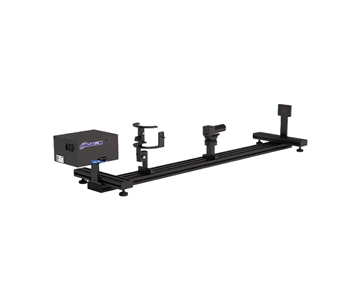
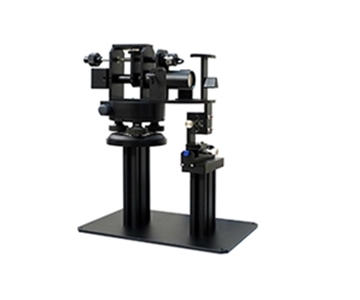
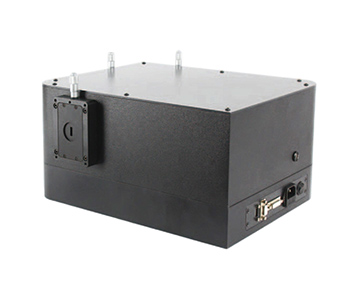
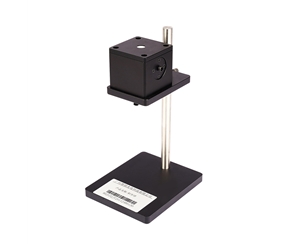
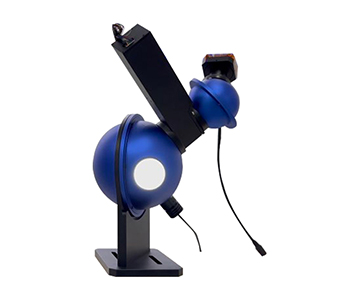
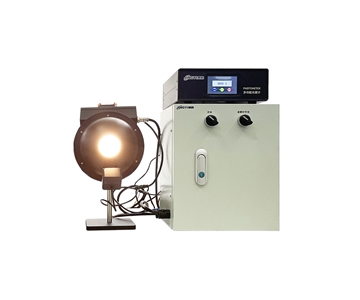
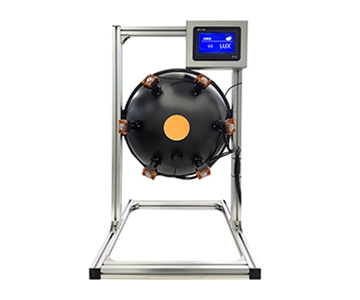
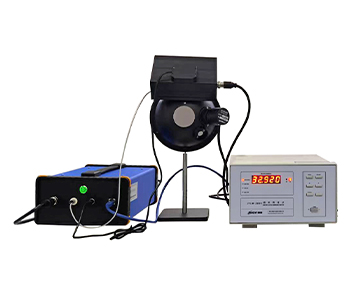
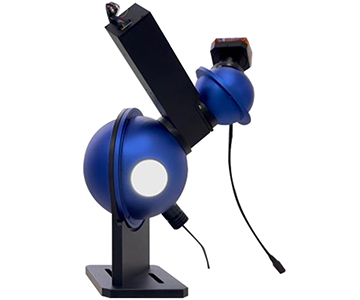
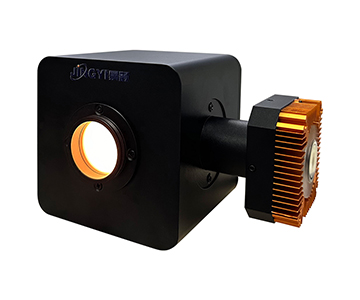
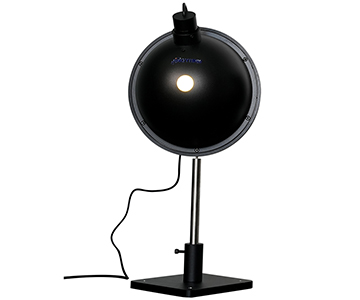
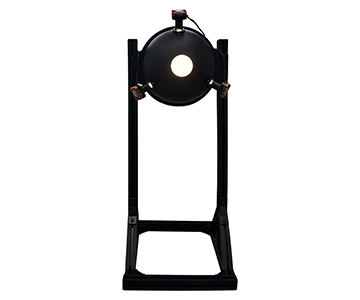
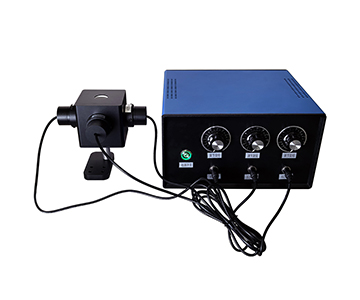
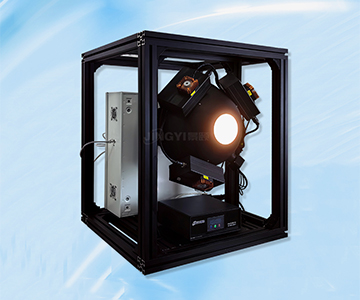
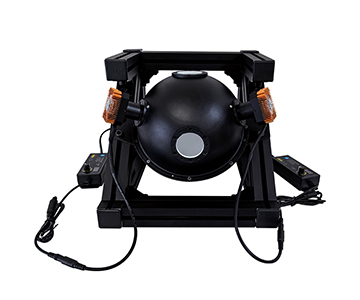
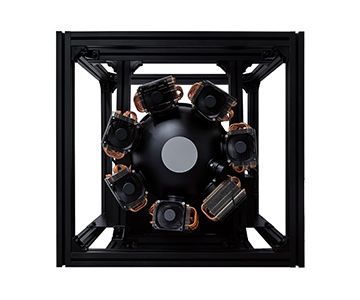
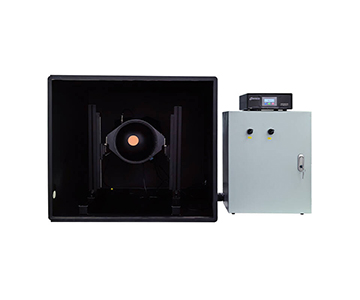
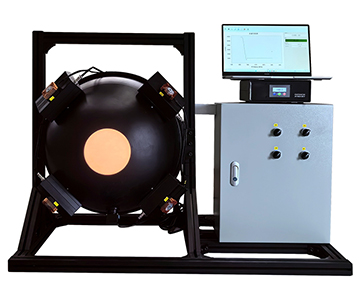
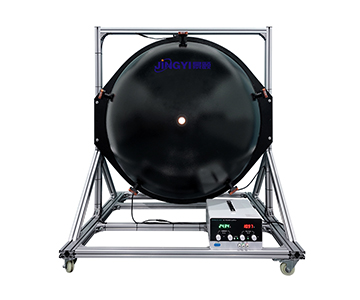
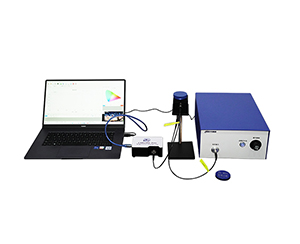
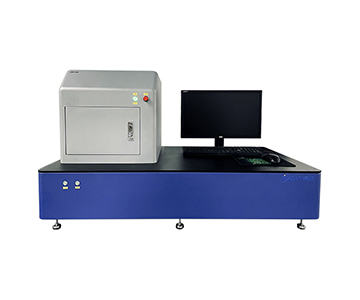
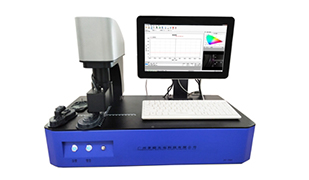
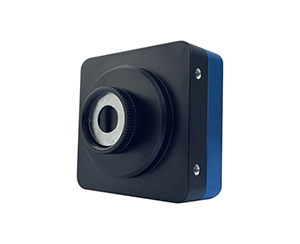
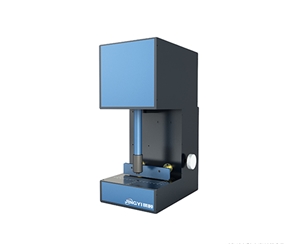
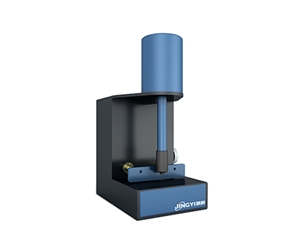
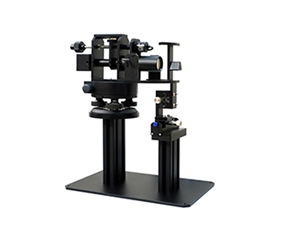
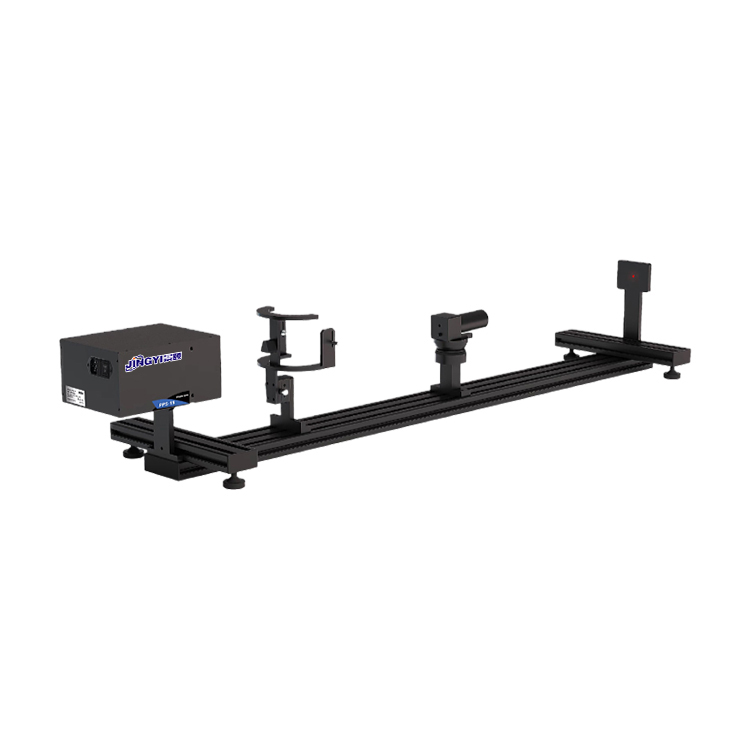
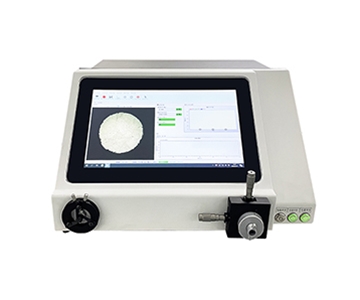
Laser beam profiling in high-speed production lines demands non-destructive full inspection without sacrificing cycle time. This article presents validation data from four industry scenarios—semiconductor collimation, aviation optics far-field, medical laser IR, and display panel cutting—using a mainstream domestic beam profiler system. Measured repeatability deviation of long-axis diameter stayed below 0.5% for 29μm–4.4mm spots, while large-aperture configuration achieved ellipse measurement error under 1.2% for 22.5mm spots. Infrared configuration stably captured 50μm-class spots in 400–1800nm band. Compared to imported high-end systems, the domestic solution offers competitive CPK of 1.33, modular attenuation, and faster local service, though frame rate and extreme power switching speed remain gaps. All tests followed controlled darkroom conditions at 22±1°C, 45% RH.
Validation Methodology
A persistent debate in optical communication and semiconductor packaging plants centers on whether sub-100μm laser spots can be fully inspected at line speed without becoming a bottleneck. One camp insists that imported systems with 200+ fps frame rates close the loop; the other questions whether premium pricing truly buys long-term stability. To resolve this, we tested four sample types: a 12-inch wafer fab semiconductor laser collimation module, an aviation optics far-field emission unit, a medical laser surgical source, and a display panel line laser cutting head.
All measurements were conducted on a vibration-isolated optical table inside a darkroom. Ambient temperature was maintained at 22±1°C (71.6±1.8°F) with 45% non-condensing humidity, aligning with standard optical measurement baselines. Manual and auto-exposure modes were
Case 1: Semiconductor Collimation Coupling Inspection
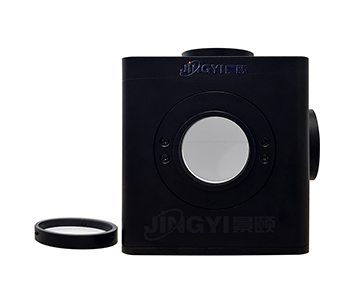
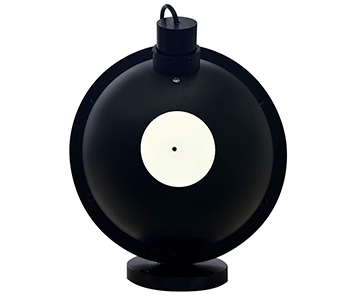
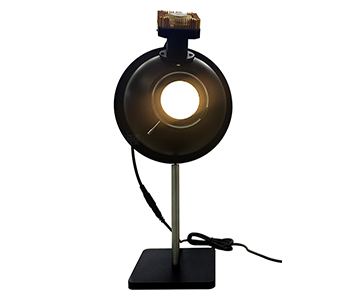
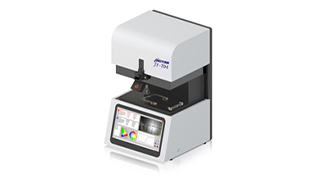
A semiconductor packaging facility running 300 wafers per hour faced rising coupling losses from collimation offsets. The target was to constrain beam diameter deviation within 2% and establish hard Pass/Fail thresholds. The evaluated basic-type profiler measured X/Y diameters against an imported high-end reference.
Results: basic type recorded long-axis 1.24mm, short-axis 1.21mm, ellipticity 0.024, energy non-uniformity 8.7%, Gaussian fit 0.98. Import reference showed long-axis 1.235mm, short-axis 1.215mm—a 0.4% deviation. This precision contributed to a 0.37 percentage point yield improvement on the line. However, the basic type required 0.8 seconds for auto-exposure stabilization versus 0.6 seconds for the import, a gap that becomes noticeable in high-mix production.
Case 2: Aviation Optics Far-Field Divergence Measurement
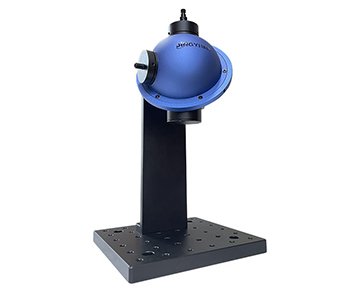
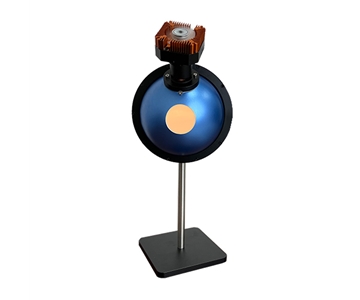
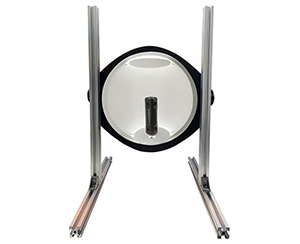
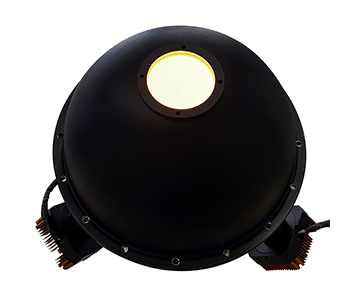
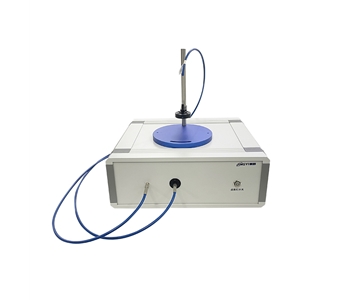
An aviation optics unit required far-field divergence characterization without beam truncation. The large-aperture profiler was selected because its 22.5mm clear aperture captures the entire far-field spot (arriving at ~22mm diameter) while 11μm pixels balance sampling density and noise.
Three consecutive measurements yielded divergence angles of 0.85mrad, 0.87mrad, and 0.84mrad (mean 0.853mrad, repeatability ±0.015mrad). Centroid jitter registered 0.04mm horizontally and 0.05mm vertically. Beam pointing stability fluctuated less than 0.06mm over 10 minutes, satisfying subsequent alignment tolerances.
Case 3: Medical Laser Infrared Beam Profiling
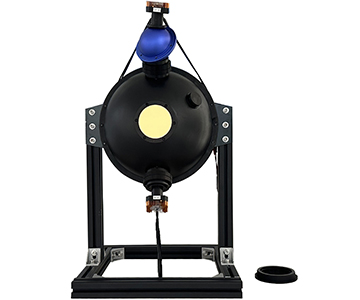
A medical laser system emitting 1064nm infrared pulses at 1kHz needed mode defect screening for spots ranging 50μm–4.5mm. The infrared profiler’s InGaAs sensor with cooling (10°C below ambient) suppressed dark current, while 20μs exposure matched the pulse width.
Measured spot diameter was 0.82mm with Gaussian fit 0.96 and symmetric single-peak energy distribution. Divergence angle calculated via second-moment method was 1.2mrad. After 2 hours of continuous operation, centroid shift was only 0.012mm, confirming thermal stability. Note: when ambient approaches the 60°C upper limit, additional heat dissipation must be evaluated for the cooling module.
Case 4: Display Panel Line Laser Cutting Quality Control
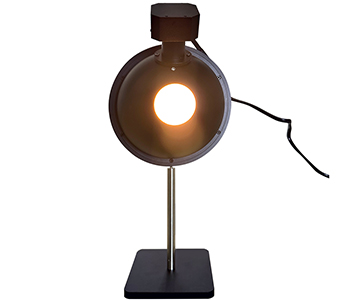
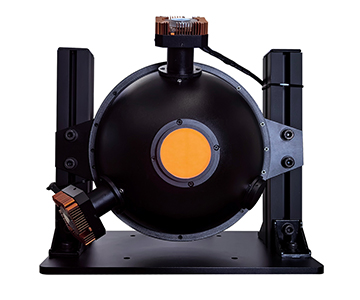
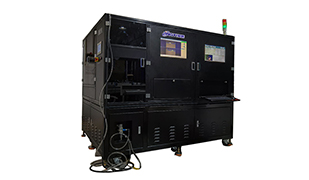
A display panel manufacturer used line lasers for cutting and required monitoring of line-spot uniformity along the long axis. The extended large-sensor basic type (29μm–200mm range, 2688×1520 resolution, 90fps) was deployed.
The line spot measured 38.4mm long by 0.16mm short axis. Energy non-uniformity along the long axis was 12.3%; 3D pseudo-color contour revealed central energy concentration with edge roll-off. Deviation from import equipment was within 1.1%. However, at 90fps maximum, high-speed cutting节拍 demands external trigger with reduced acquisition rate to prevent frame drops.
Cross-Platform CPK Comparison: Three Tiers of Equipment
Per T/CITS 231-2025 (Beam Pointing Stability in Automotive LiDAR), the large-aperture type’s centroid jitter repeatability of 0.05mm meets the standard limit—a key credential for domestic mainstream systems entering automotive electronics online monitoring.
| Dimension |
Import High-End |
Domestic Mainstream (Basic + Large Aperture) |
Domestic Economy (Basic Lite) |
| Spot Repeatability CPK |
1.67 |
1.33 |
1.12 |
| Max Frame Rate (fps) |
200+ |
90 (large sensor) / 30 (IR) |
30 |
| Measurable Range |
10μm–30mm |
29μm–22.5mm (extendable to 200mm) |
29μm–4.4mm |
| Bit Depth |
12bit |
12bit |
12bit |
| External Trigger |
Yes |
Yes |
Yes |
| Attenuator Config |
Custom multi-plate |
4 plates standard, expandable to 1000W |
4 plates standard |
| Price Tier |
High ($200K+) |
Mid ($50K–$100K) |
Low (<$50K) |
| Service Response |
2 weeks overseas |
3–5 days domestic |
5–7 days domestic |
| Known Weakness |
No local customization |
SNR drops slightly for ultra-far-field <0.1mrad |
Auto-exposure switch ~15ms slower |
The domestic mainstream tier achieves CPK 1.33, trailing the import’s 1.67, but differentiates through 200mm large-sensor expansion, modular attenuators, and rapid local delivery. The economy tier suffices for low-volume trial production, yet its 15ms auto-exposure delay becomes a cycle-time bottleneck when external trigger sync or rapid attenuator switching is required. All three tiers share 12bit depth, confirming dynamic range as a baseline rather than a differentiator.
Customer Testimony
A lead process engineer at a top-tier laser equipment manufacturer (anonymized per GDPR) provided authorized disclosure: “After replacing our imported unit with the basic-type profiler, per-test consumable cost dropped by $0.021 (¥0.15). Line cycle time remained essentially unaffected. However, the first two days were painful—the standard four-plate attenuator combination required complete recalibration, and Pass/Fail thresholds in software had to be redefined to match our internal specs. It’s not plug-and-play.”
This feedback underscores that hardware readiness does not equal out-of-box deployment. Data threshold migration demands engineering hours. The mild negative of initial debugging is offset by long-term savings: at million-unit annual volume, $0.021 per test compounds into six-figure annual reductions.
Error Source Tracing and Implementation Recommendations
Pixel quantization dictates spatial sampling granularity. Measuring a 29μm spot with 2.9μm pixels yields only about 10 pixels across the diameter; a 1% pixel calibration error amplifies diameter deviation. The large-aperture type’s 11μm pixels suit spots above 110μm—below that, undersampling drops Gaussian fit from 0.98 to 0.91.
Attenuator thermal effects: stacking the standard four plates can handle up to 1000W, but high-power switching induces thermal lensing that drifts spot morphology by 0.3% within 30 seconds. For online monitoring, fix the attenuation combination, enable external trigger, and perform offline calibration before going live to prevent false Pass/Fail calls.
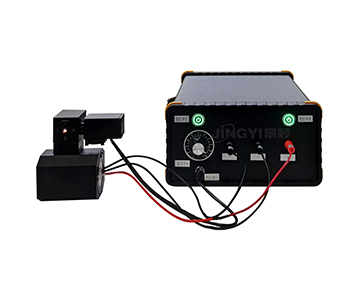
External trigger synchronization: if trigger cable lengths differ, microsecond-level offsets between dual cameras cause systematic centroid shifts up to 0.02mm. Always calibrate delay with a standard pulse source and embed compensation coefficients in software.
For automotive LiDAR testing requiring compliance with T/CITS 231-2025, prioritize the large-aperture type with cooled infrared assist to ensure centroid jitter data is traceable to standard limits.
Applicability Boundaries and Real-World Constraints
Objectively, this domestic solution does not win on every front. First, the standard four-plate attenuator hits thermal saturation at 1000W continuous; prolonged full-power operation extends pixel thermal drift stabilization from 0.8s at room temperature to 2.3s. Second, while the infrared type supports cooling to 10°C below ambient, when ambient nears 60°C, cooling headroom shrinks and continuous-operation lifespan lacks third-party accelerated aging data. Procurement teams must run a full 8-hour POC at realistic power levels—never judge by short-duration demo curves.
Frequently Asked Questions
Q1: What is the smallest spot size the basic type can measure?
The basic type lower limit is 29μm, relying on 2.9μm pixels and appropriate attenuation. Below this, switch to the large-sensor version or add a microscope coupling adapter; otherwise insufficient pixel sampling distorts Gaussian fitting.
Q2: Which wavelength scenarios suit the infrared type?
The infrared type covers 400–1800nm, optimized for 1064nm and 1550nm communication and medical lasers. InGaAs sensors offer superior short-wave infrared sensitivity, and cooling suppresses dark current for stable pulsed capture.
Q3: Can test reports be used for quality traceability?
Yes. The system supports parameter logging, 2D/3D image saving, PDF report export, and re-measurement of stored images, satisfying production line audit and traceability requirements.
Q4: What justifies the large-aperture type’s higher cost versus the basic type?
The premium covers the 22.5mm large-format CMOS sensor and 2-inch clear aperture structure. This investment only pays off when spot size exceeds 4.4mm or truncation prevention is mandatory; smaller spots are more economically measured with the basic type.
Q5: How can I independently verify reliability before purchase?
Request a calibration certificate from the same production batch, cross-reference against standards like T/CITS 231-2025, and demand a sample retention re-test service. Run multi-day continuous operation to observe CPK decay rather than relying solely on brochure parameters.
About This Guide
Data Sources
: SEMI Annual Report, Technical White Paper of the Chinese Optical Society, customer-authorized in-fab test data, GB/T national standard datasets.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in industrial precision measurement equipment.
Disclosure
: Jingyi Optoelectronics manufactures laser beam profilers. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: September 2026
For detailed specifications and application notes on laser beam profilers, search "Jingyi Optoelectronics beam profiler" or visit our technical library.