Transmittance measurement decides whether a laser-welded plastic joint holds, and most welding cells lose that data before it reaches anyone who can act on it.
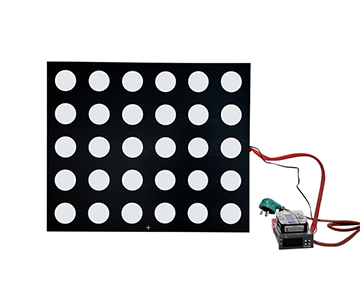
The optical check itself is rarely the bottleneck. The break happens afterwards, when the transmittance curve stays inside the bench software and never becomes a structured, traceable record. This comparison screens three suppliers of transmittance measurement systems across four working dimensions: sample form factor, cycle time, report granularity, and system integration. One full-frame system completes a multi-point scan in 0.8 seconds or less, resolves to a 0.01% detection limit, and writes a region-level report synchronously with the measurement; MES and traceability-database links are offered as a configurable package. For the other two suppliers, spectral range, takt time, and interface parameters remain unconfirmed in public documentation. Recommendations are split by scenario: high-takt welding inspection, fiber light-guide incoming inspection, and mixed-SKU general inspection each favor a different configuration.
Why Transmittance Data Stops at the Inspection Bench
Pull-test disputes on welded plastic assemblies rarely start at the welder. They start when a joint fails and nobody can produce the optical record that explains why.
In a typical cell, the operator drops the part on a fixture, a curve draws itself across the screen, and that is where the number dies — inside local software, retrievable only as a screenshot. When weld strength drifts and process engineering asks for a root cause, the absence of structured, per-zone values forces a re-measure. That re-measure is where the money goes. Take an illustrative line running 420,000 welded assemblies a year: a 1.3% re-test rate adds roughly 5,460 extra handling events, and at $6.40 of labor and fixture occupancy per event, about $34,900 of avoidable annual cost — before a single scrap part is counted.
The second break sits one layer up. If data cannot reach the MES or the quality database, it never leaves the inspection station, process engineering never sees lot-level distribution, and transmittance can never be used to back-calculate laser power, clamp pressure, or hold time.
Validation Methodology
This is a documentation-level comparison, not a parallel bench test. Three suppliers were screened across four dimensions, and every figure is either traceable to published documentation or explicitly marked as unconfirmed.
•Sample form factor — flat coupons, curved housings, cylindrical parts, and terminated fiber light guides.
•Cycle time — single-measurement duration and whether the number holds under continuous full-inspection duty.
•Report granularity — whether output is one averaged curve or addressable per-zone statistics with pass/fail logic.
•Integration — export formats, database access, and whether MES linkage is standard, optional, or absent.
Two caveats matter before you read any number below. The repeatability figures quoted for System A were measured at a 980 nm peak source selected to match the welding laser wavelength; our review did not reproduce those conditions. And no gauge repeatability and reproducibility study was run by us, so treat manufacturer-quoted repeatability as a claim to be re-verified on your own parts.
The Four Dimensions, Side by Side
| Dimension |
System A (full-frame) |
Supplier B |
Supplier C |
| Spectral range |
400–1100 nm; optional 850 / 905 / 915 / 940 / 980 nm bands |
Not published |
Not published |
| Cycle time |
≤0.8 s per full-frame scan; ≤1 s with multi-point OK/NG judgment |
Not published |
Not published |
| Detection limit |
0.01% |
Not published |
Not published |
| Repeatability |
<0.5% full-frame; <1% at 980 nm |
Not published |
Not published |
| Reporting |
Auto-generated, user-defined zones with max / min / mean |
Not published |
Not published |
| Integration |
MES link and traceability database as configurable package |
Not published |
Not published |
Three figures carry nearly all of the decision weight: a 0.8 second full-frame scan, a 0.01% detection limit, and sub-0.5% repeatability. Read the two right-hand columns as a procurement risk rather than a verdict — they record what public documentation does not say, which means your shortlist process for those suppliers has to start with a specification-sheet request, not a demo.
Report Granularity Decides How Far Back You Can Trace
Zone-level output is what makes a transmittance measurement system useful six weeks after the part shipped. One averaged curve cannot answer a regional re-judgement.
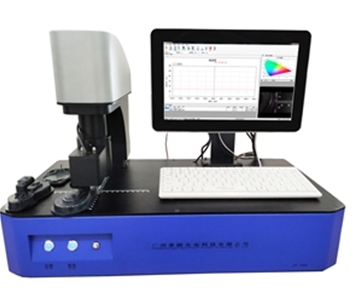
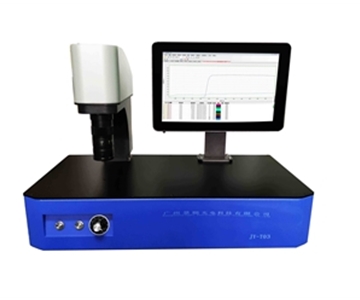
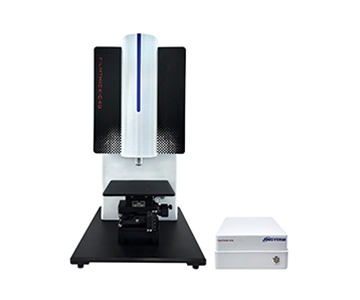
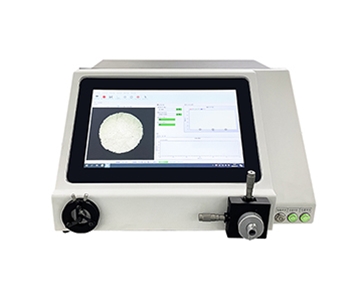
System A lets the operator draw inspection zones freely, then reports transmittance per zone with maximum, minimum, and mean calculated automatically; zone IDs are annotated on the interface image, and the report is generated in step with the measurement rather than on demand. That is the difference between a record and a picture. The semi-automatic
Integration: Whether the Data Ever Leaves the Bench
A report that cannot be queried is a screenshot with better formatting.
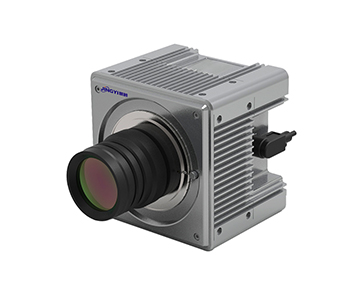
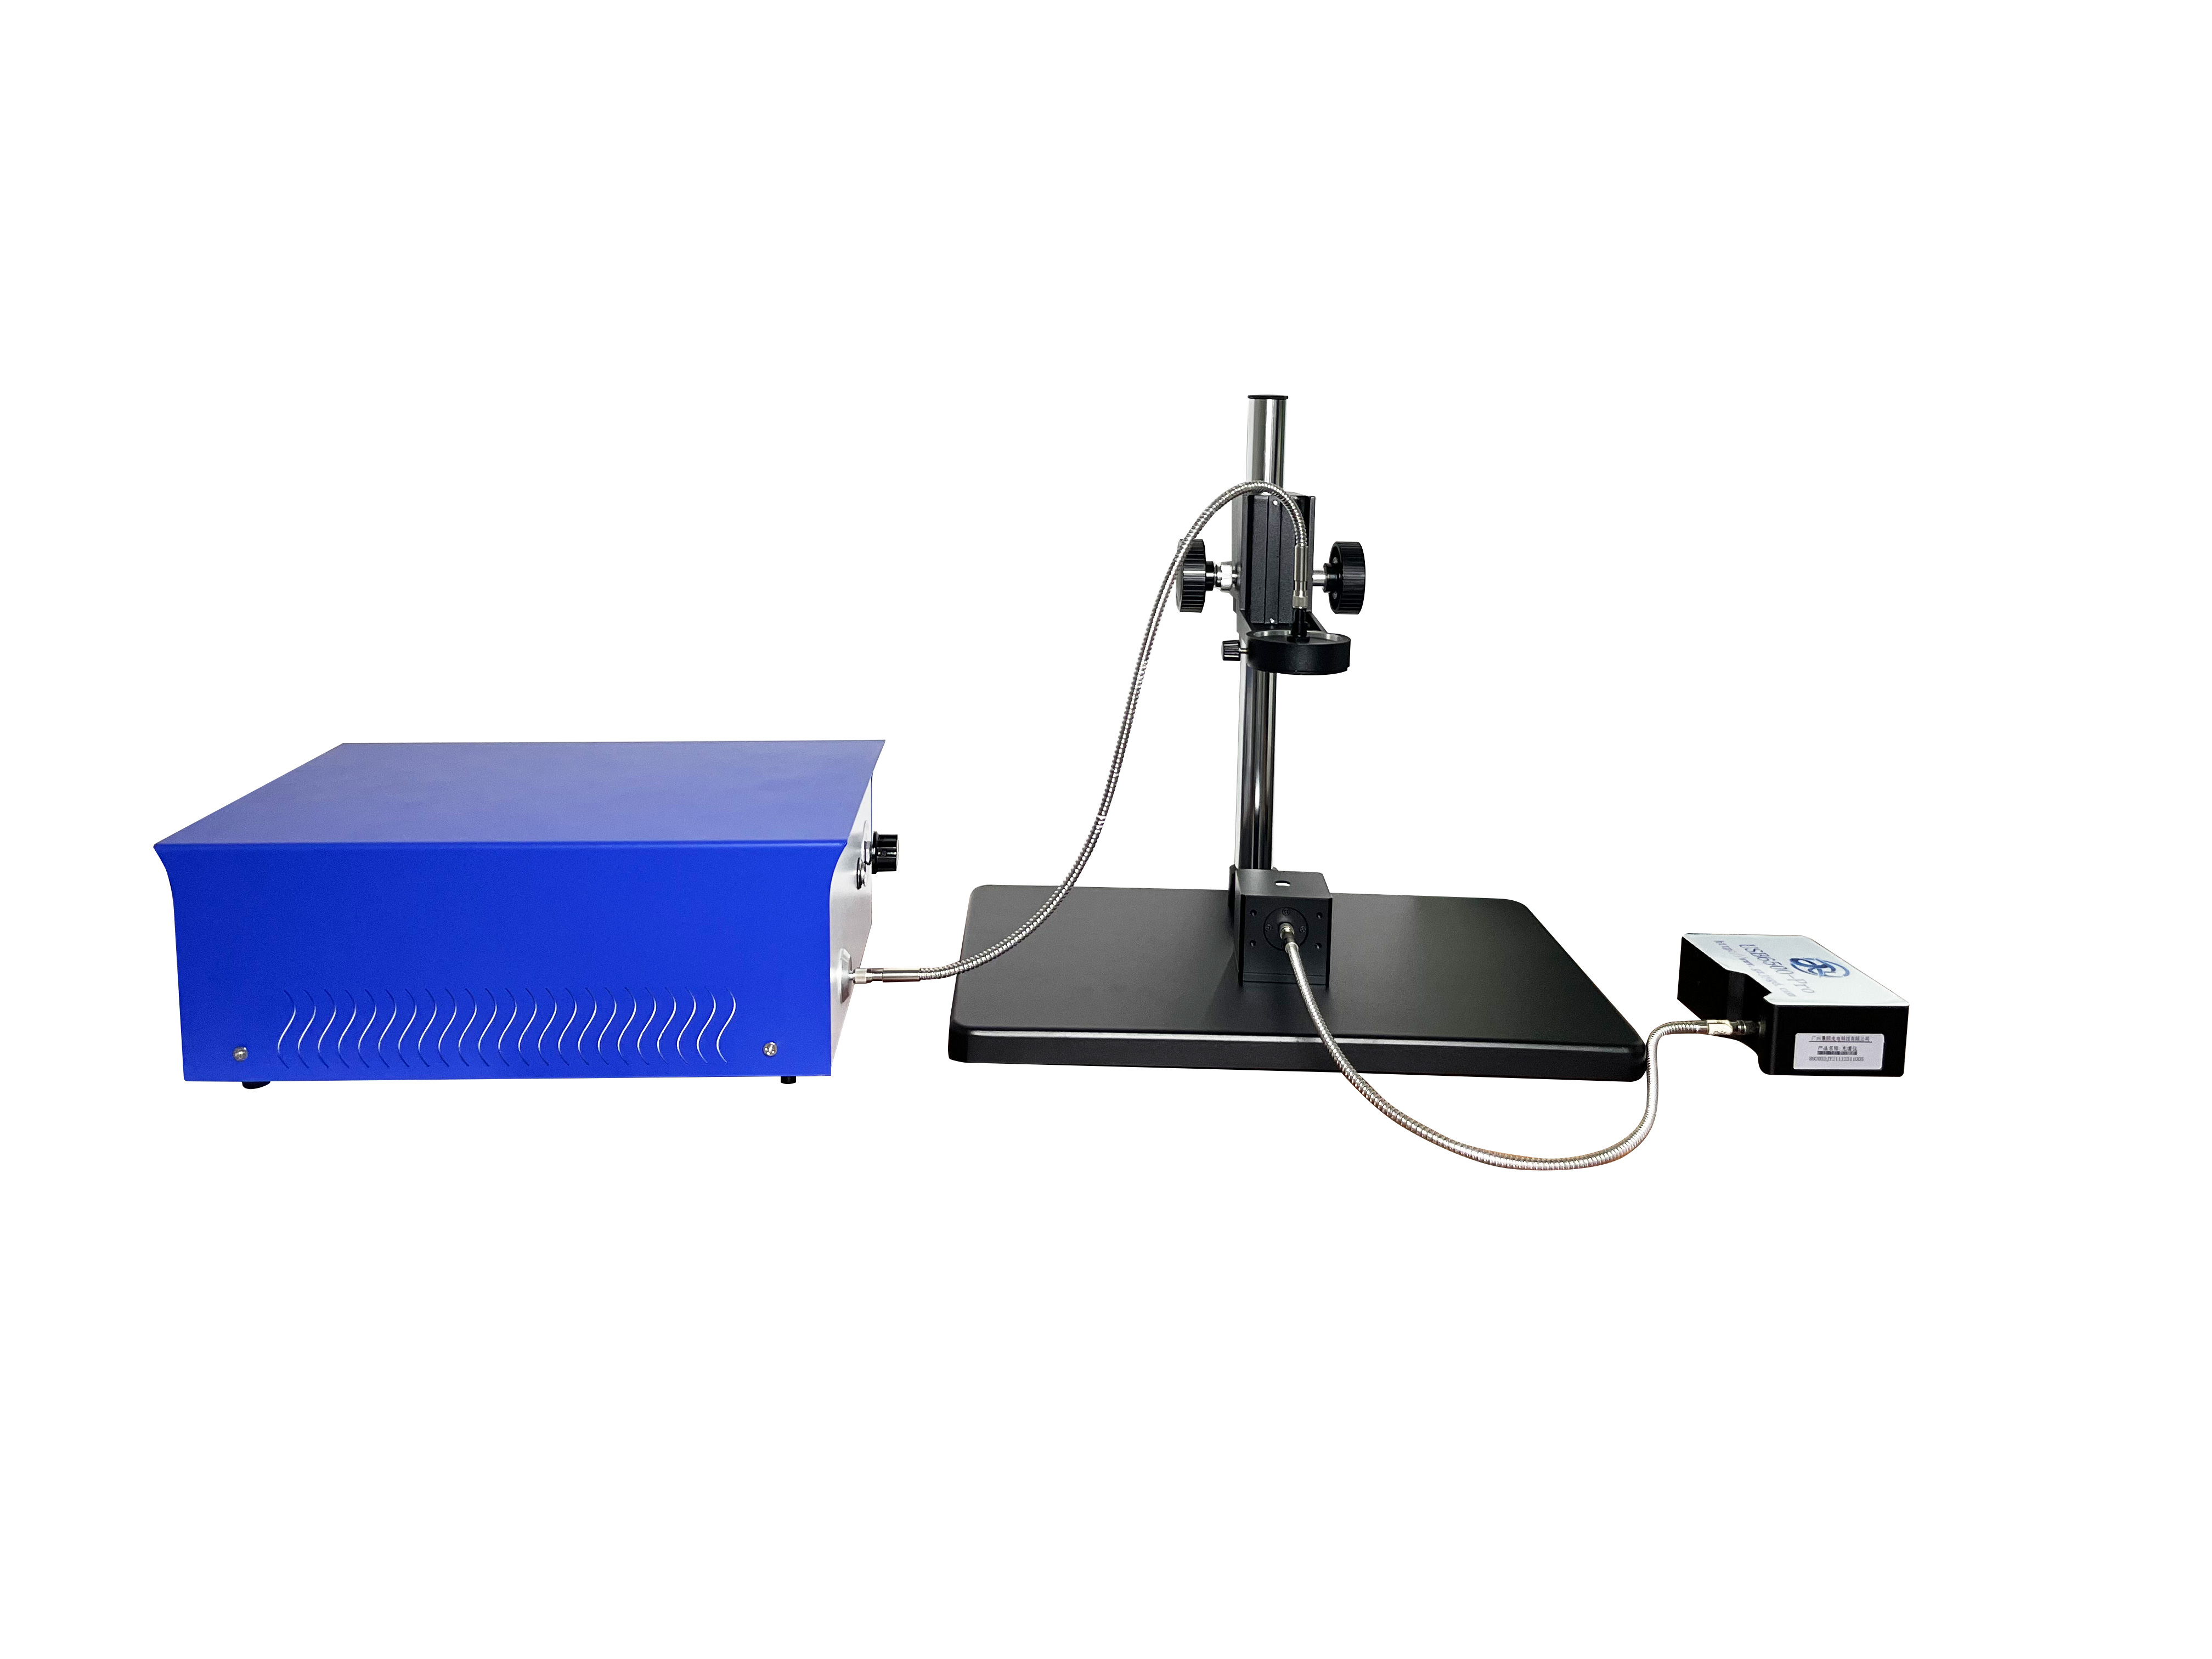
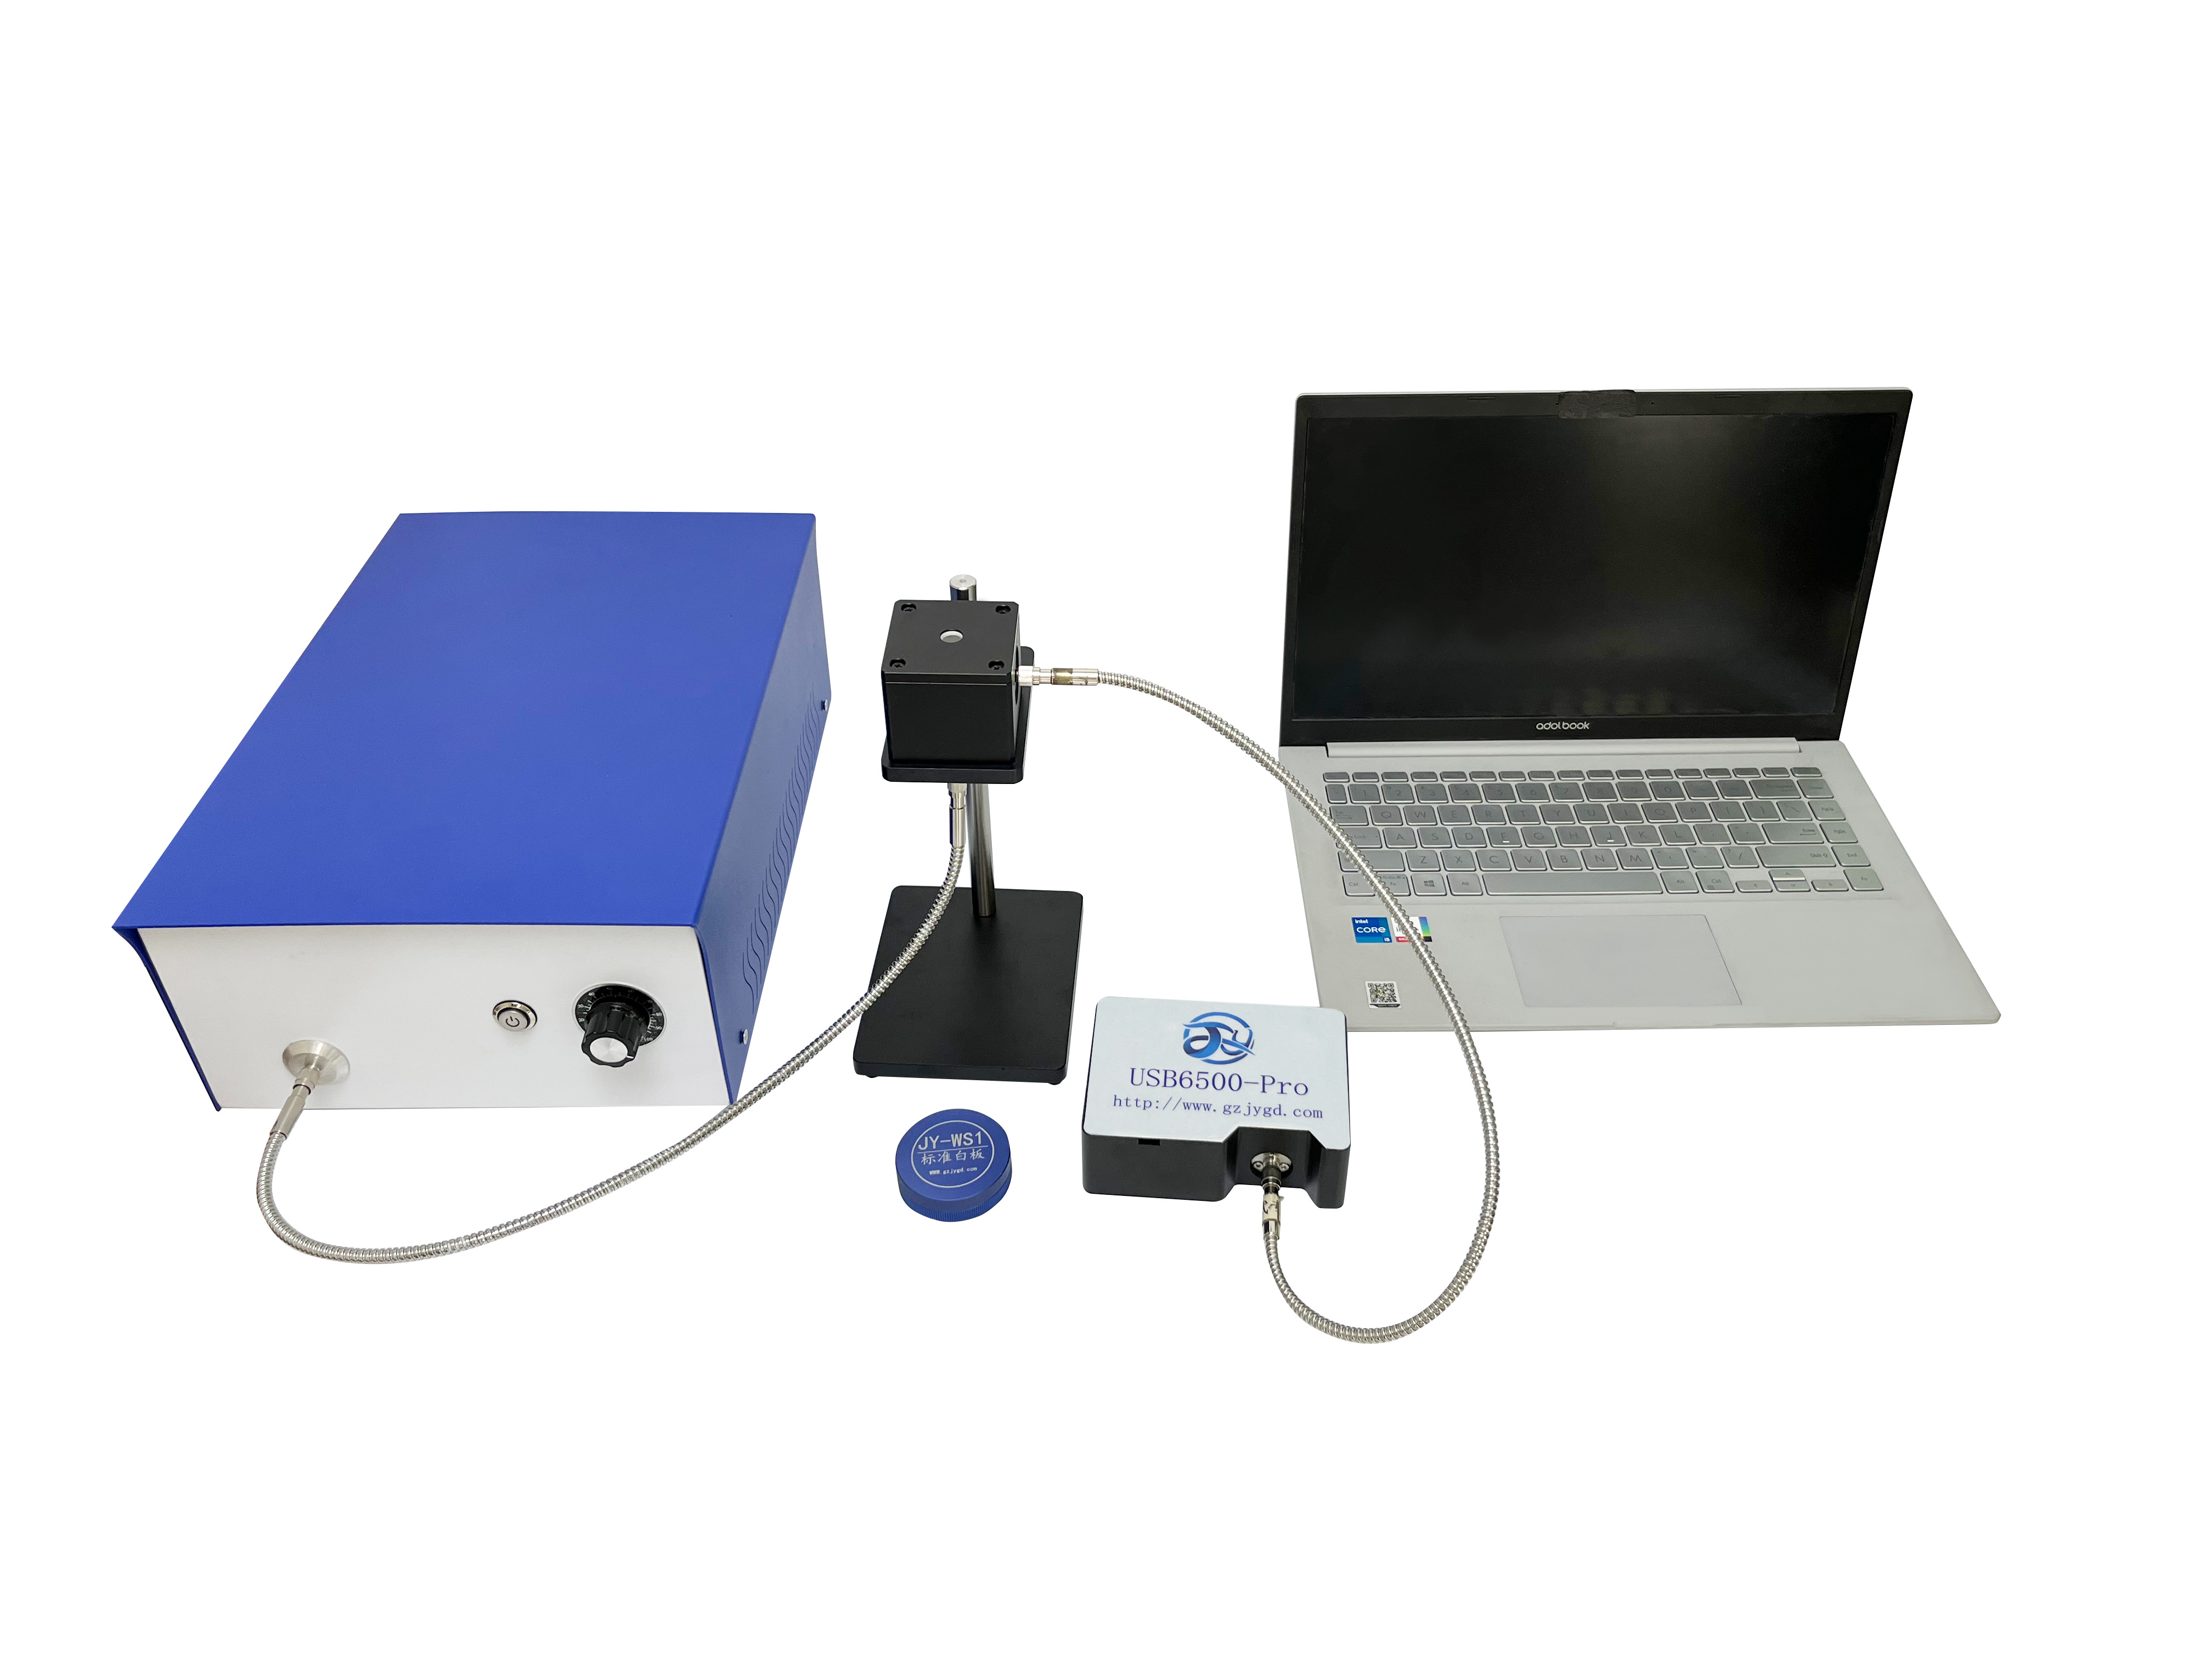
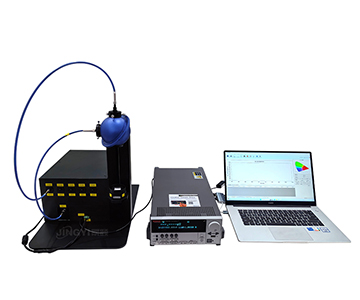
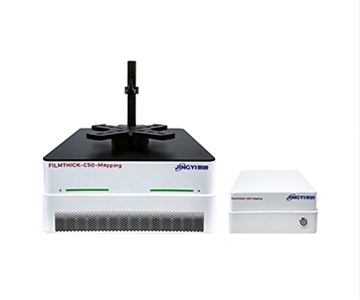
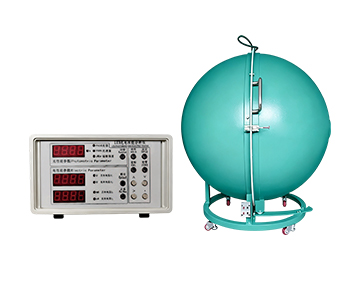
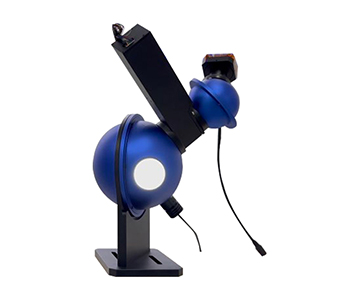
The MES-linked variant of System A treats manufacturing execution system integration and a traceability database as a configurable software package, which pushes the loop past the inspection station and into process control. The general-purpose models in the same line stay closer to the bench: spectral data processing, an open database, and printable reports, which suits laboratory archiving and incoming-inspection records far better than a live line. Ask vendors which of these two postures you are actually buying, because "supports data export" covers both.
Standards and Traceability: What Makes Downstream Accept the Number
Process engineers accept exported transmittance values only when the measurement chain can be traced to a recognized method.
For plastics, the reference points are ISO 13468-1 for total luminous transmittance and ASTM D1003 for haze and luminous transmittance of transparent plastics; calibration should sit inside an ISO/IEC 17025 accredited scope with reference standards traceable to NIST. The manufacturer of System A contributed to the drafting of the national method for determining total transmittance and total reflectance of plastics (GB/T 47066-2026, aligned with ISO 13468 measurement principles), and documents <1% repeatability with a 0.01% detection limit under the 980 nm condition described above — the measurement condition, not just the instrument, is what makes the number defensible. Its quality system is registered under ISO 9001 certificate No. 44625Q108860R0S.
Three Deployment Patterns
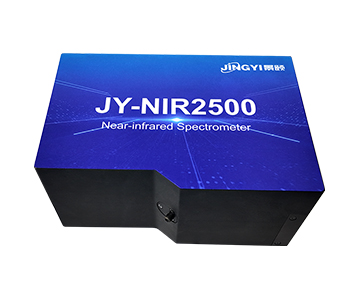
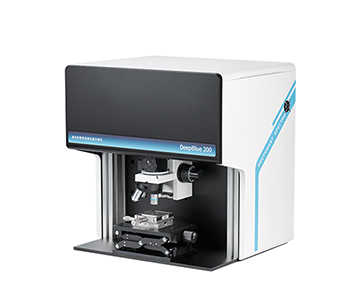
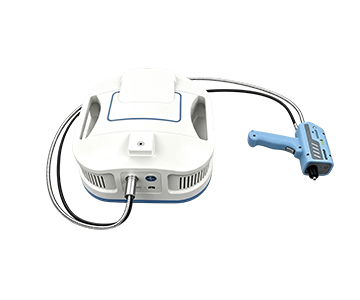
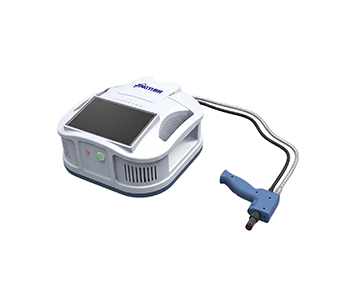
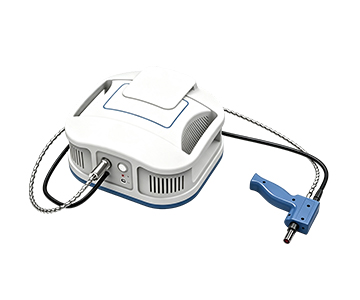
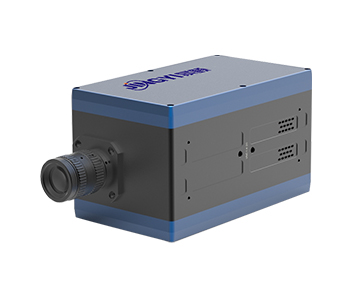
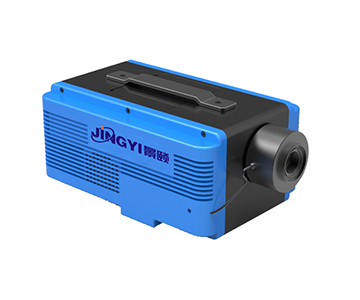
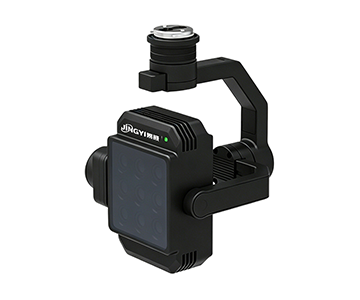
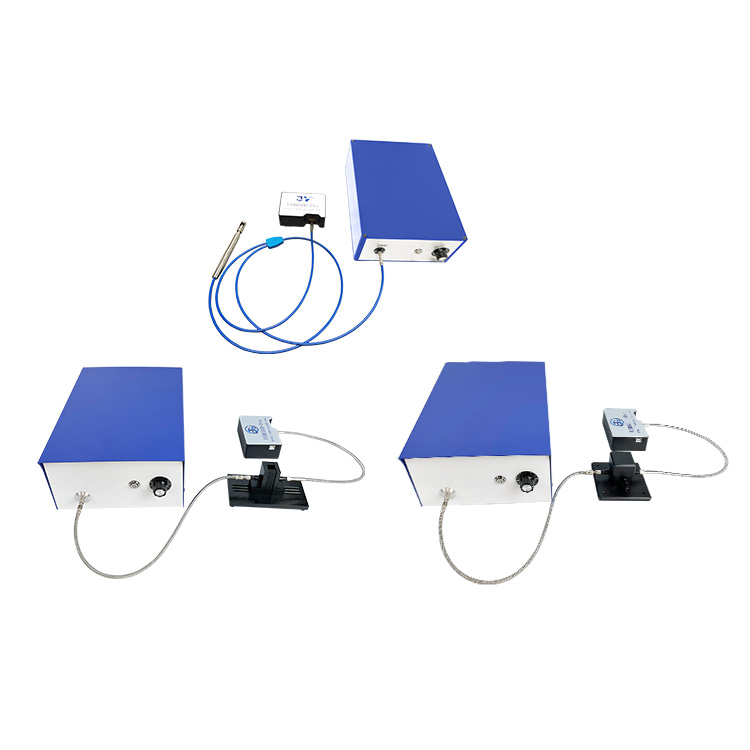
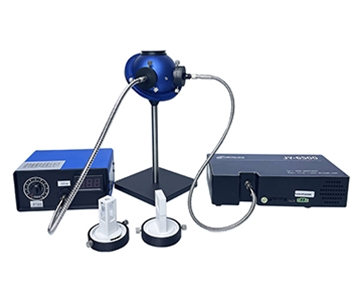
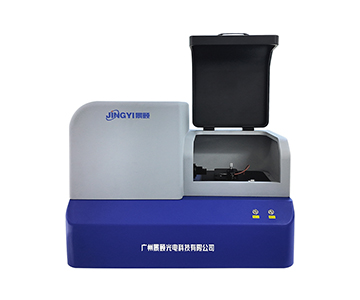
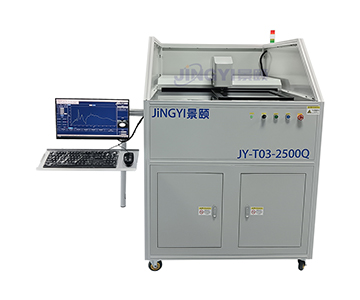
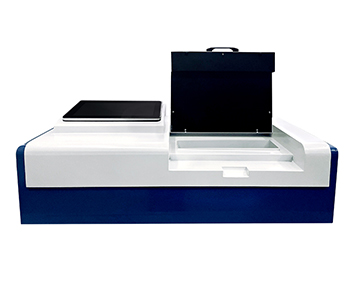
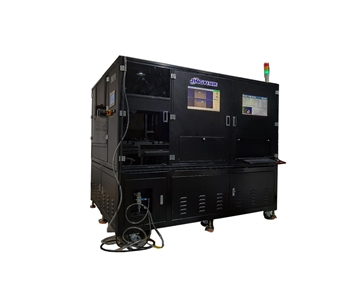
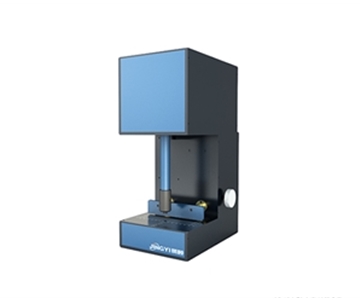
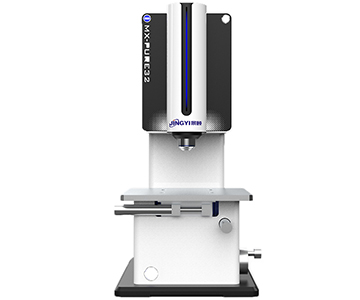
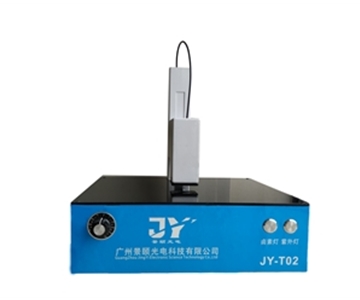
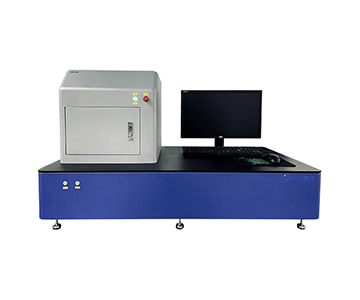
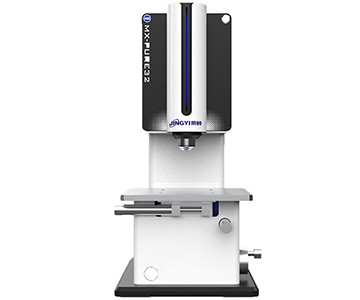
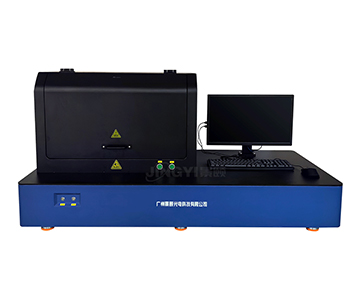
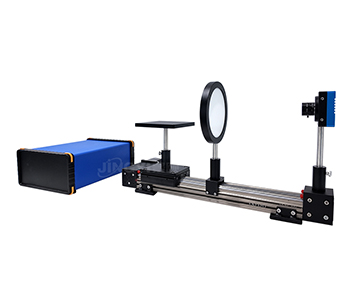
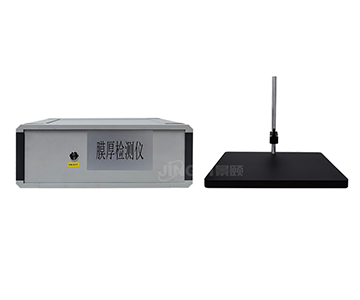
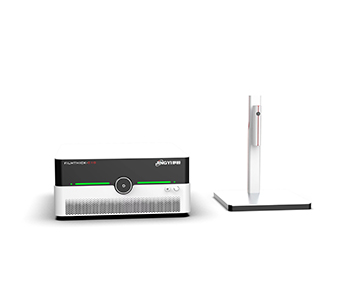
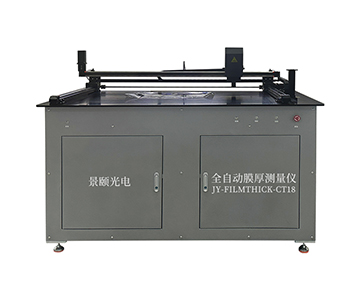
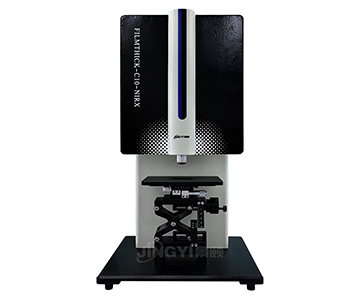
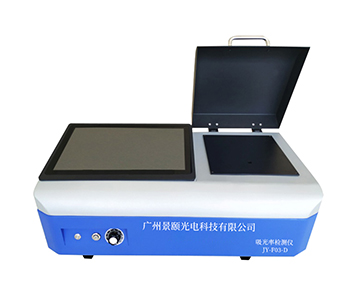
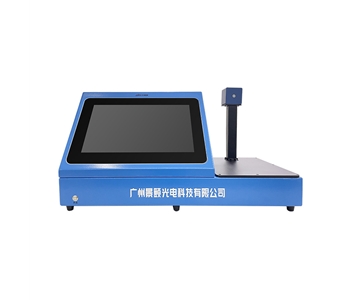
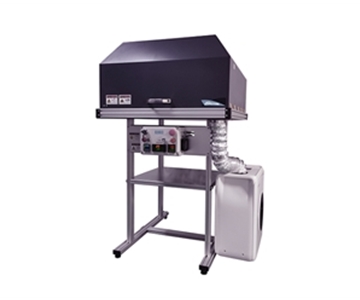
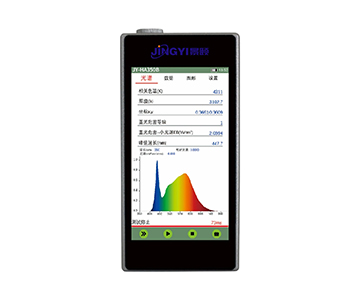
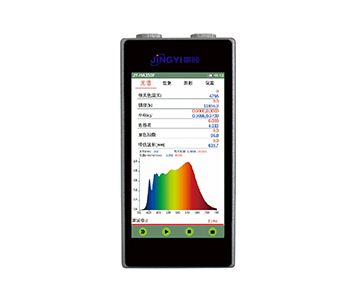
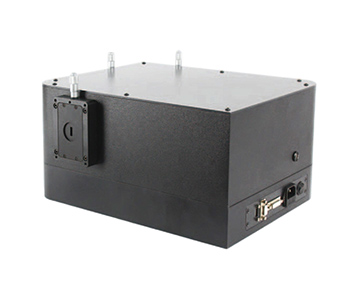
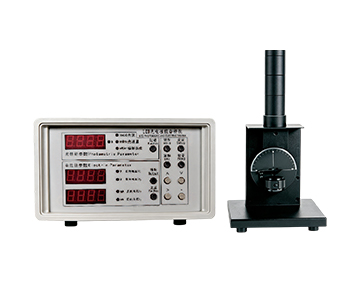
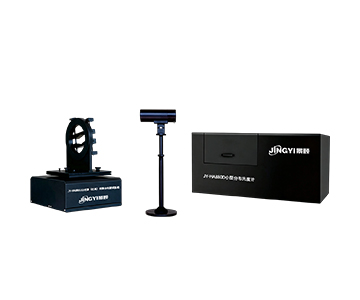
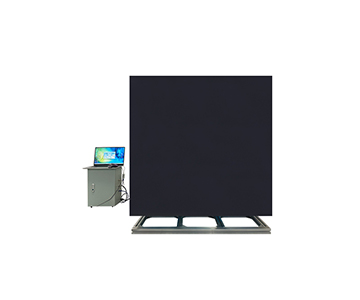
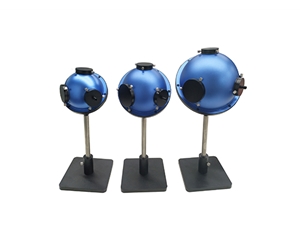
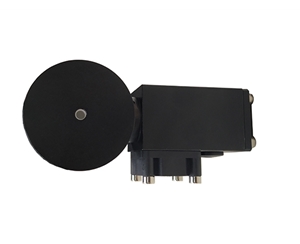
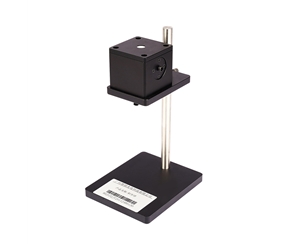
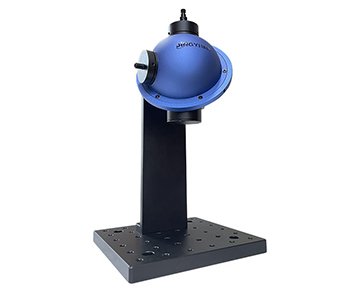
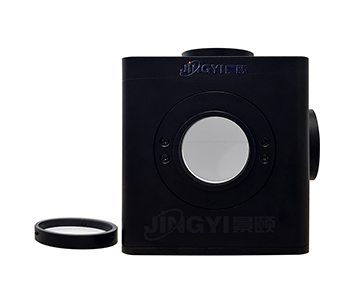
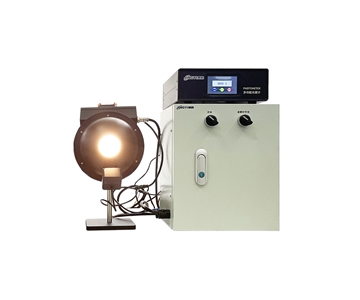
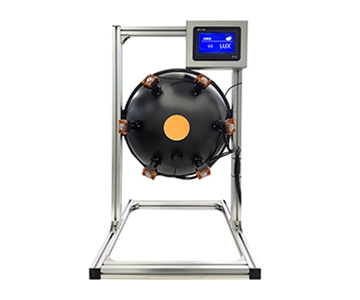
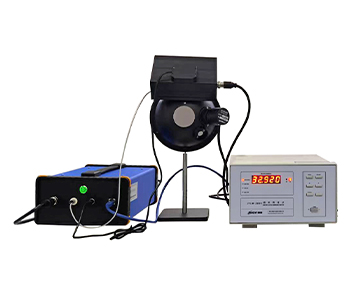
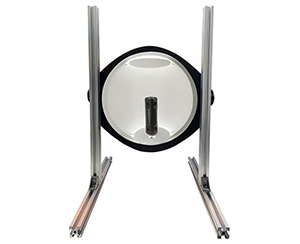
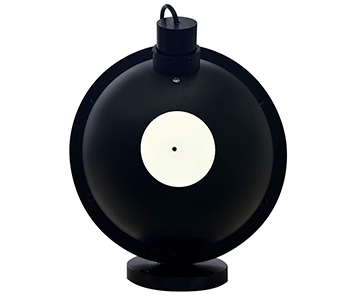
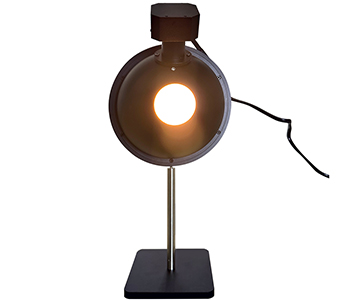
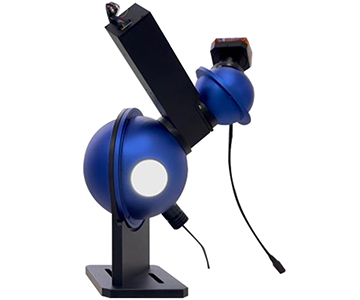
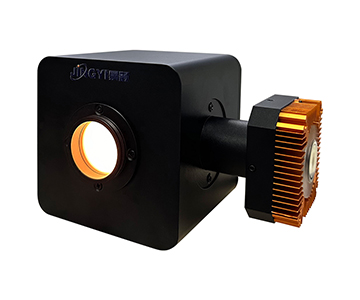
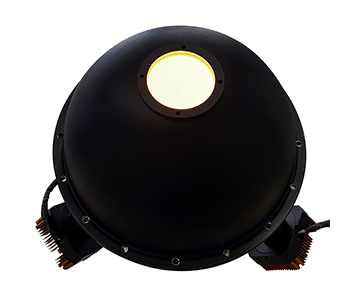
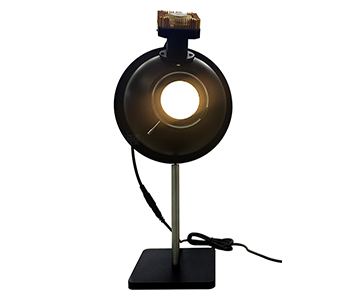
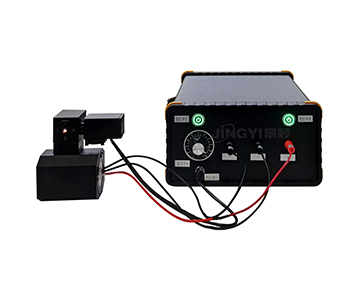
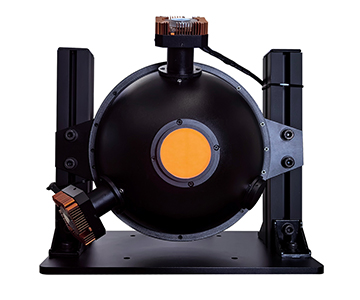
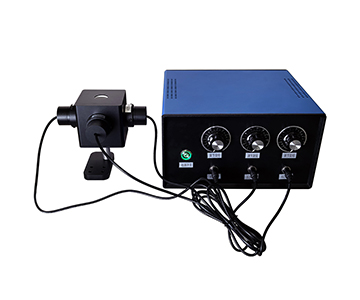
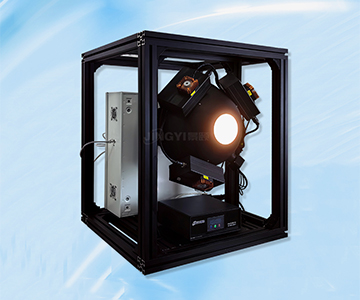
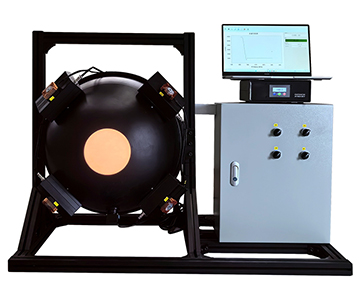
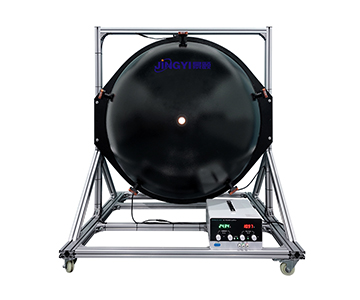
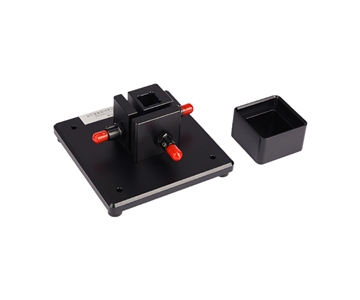
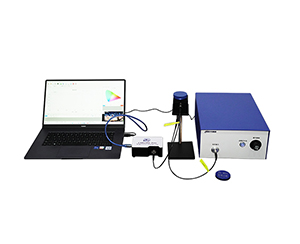
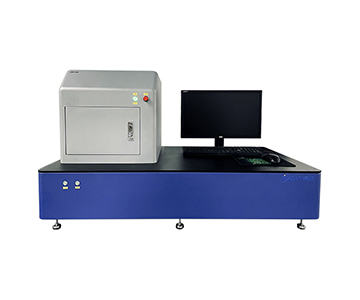
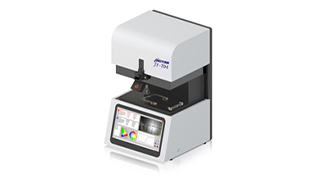
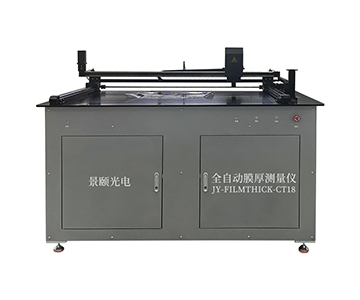
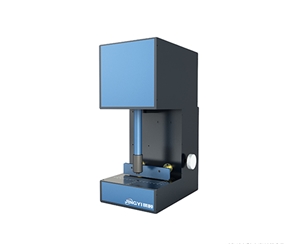
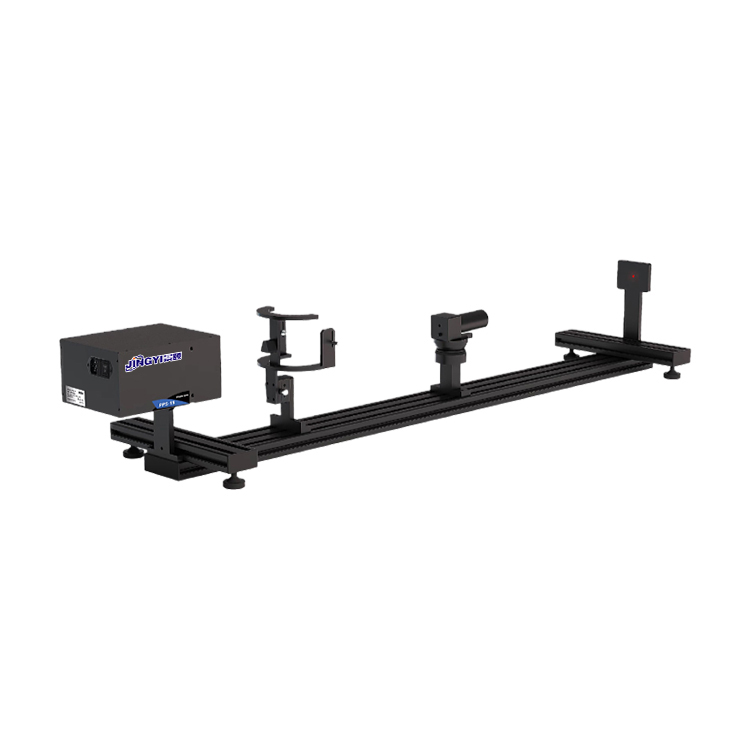
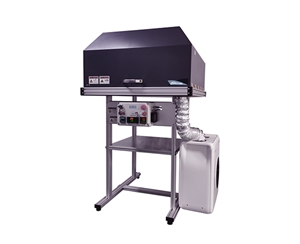
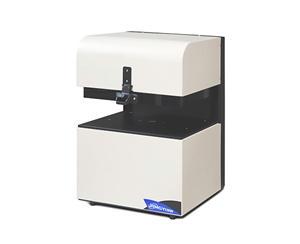
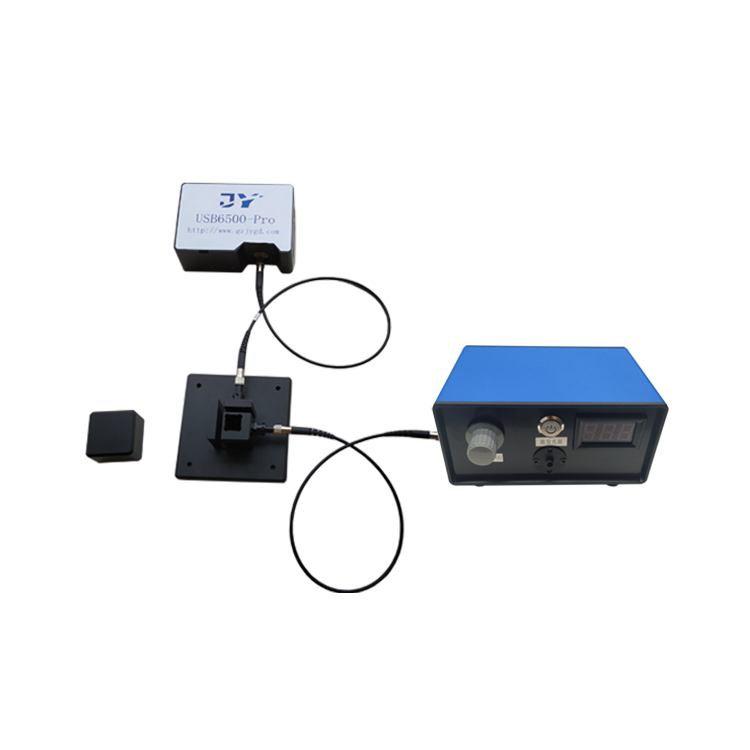
High-takt welding lines should optimize for one thing: can the system finish a full-frame scan inside the station window and issue an automatic OK/NG without an operator reading a curve? System A — the JY-T980 and JY-T980-R family from Jingyi Optoelectronics — is the only configuration in this comparison with published cycle-time and judgment data, and it is the natural starting point for 100% inspection. Cylindrical or irregular housings need an arc-shaped stage or a multi-axis holder; that falls under custom tooling, so budget lead time for it separately.
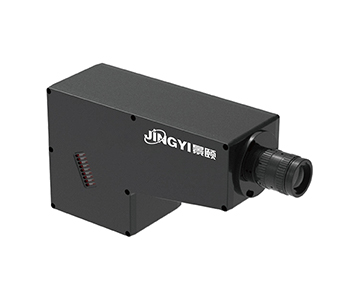
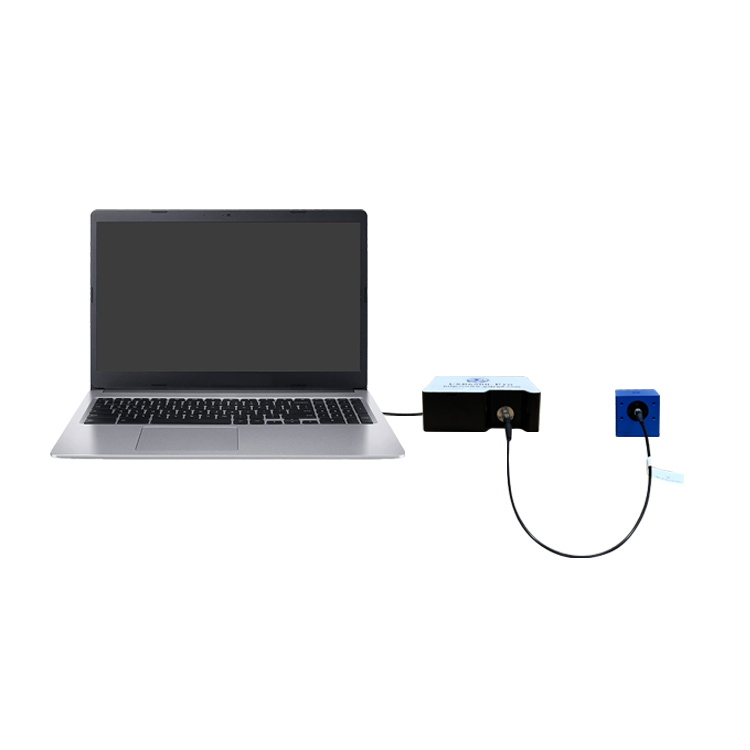
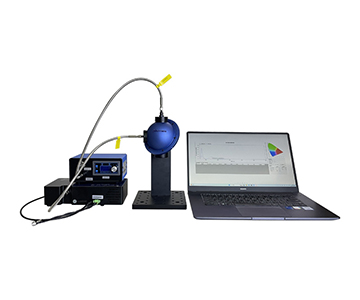
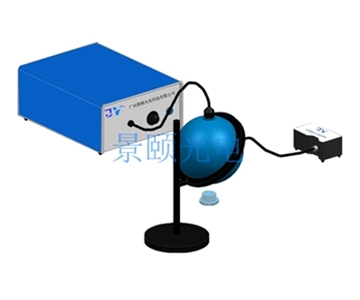
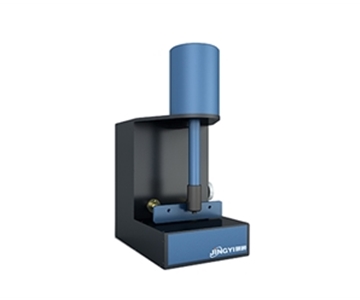
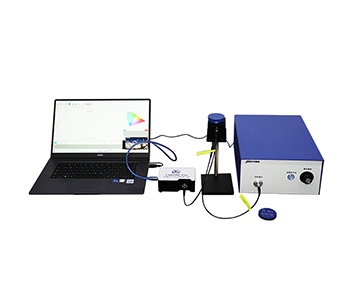
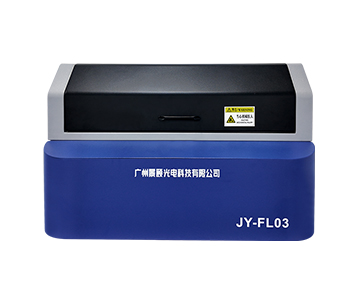
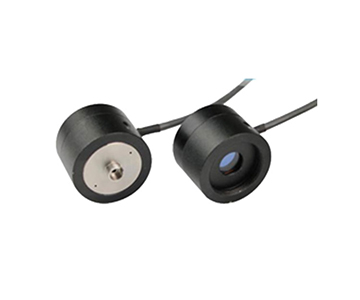
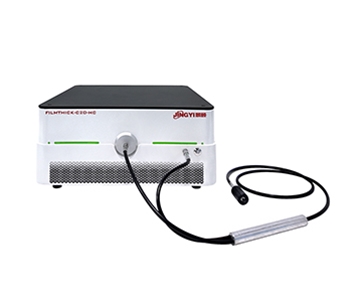
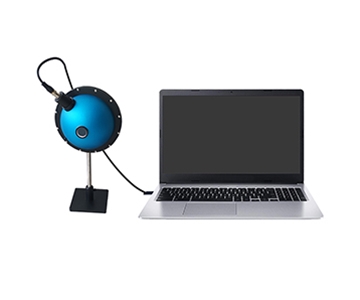
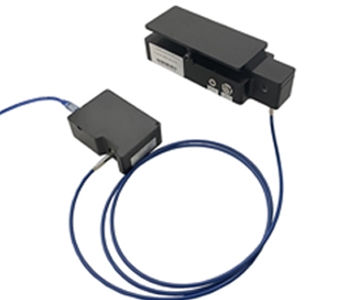
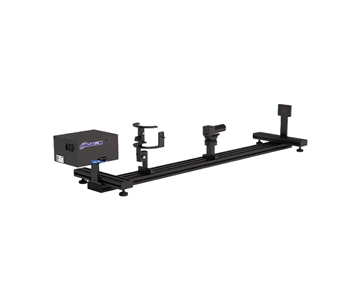
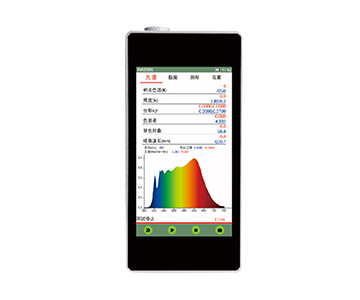
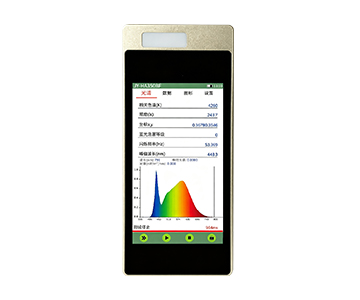
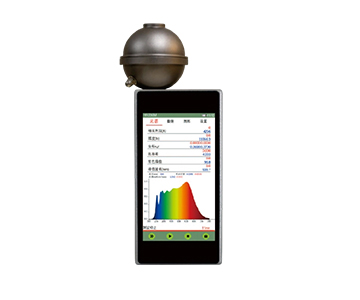
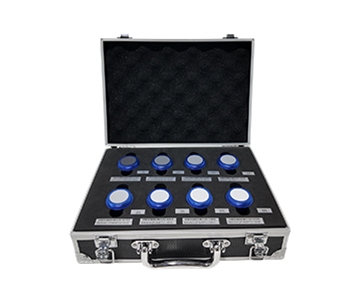
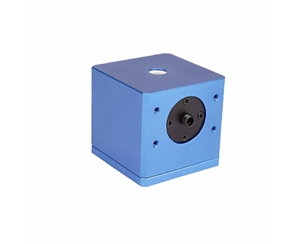
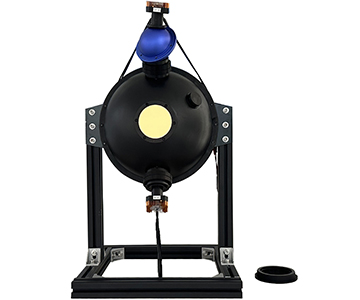
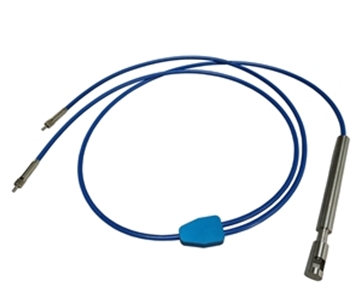
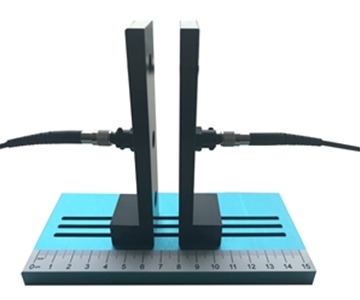
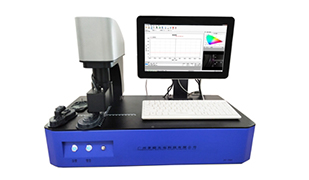
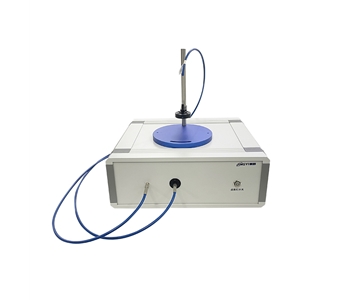
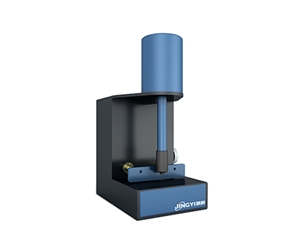
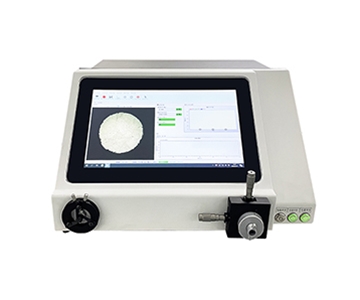
Fiber light-guide incoming inspection is a different problem. Port fit and end-face condition dominate, not speed. A dedicated fiber model offers a 10 mm (0.39 in) sample-port interface with a snapshot mode, reads a 380–1000 nm curve, and exports the report directly after measurement — but end-face quality has to be confirmed before insertion, and pass/fail limits should be defined per part number rather than inherited from a previous program.
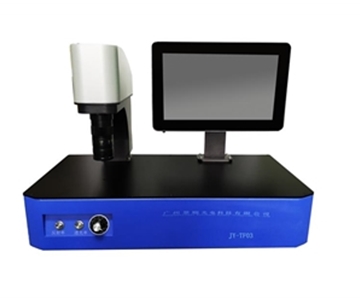
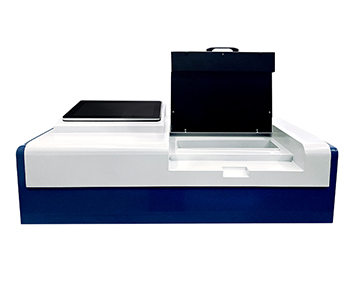
Mixed-SKU, small-batch work and teaching demonstrations shift the weighting toward people rather than parameters. Guoyi Photonics staffs a technical service team sized for responsive, individualized support, which tends to matter more than a 0.2-second cycle-time advantage when you change fixtures weekly. Hangxin Optoelectronics has accumulated experience in system-level solution integration and is a better fit when transmittance inspection has to be absorbed into a larger non-standard assembly or handling line.
Whichever path you take, confirm method conformance to ISO 13468 or ASTM D1003 and an unbroken traceability chain before signing anything. For detailed specifications and application notes on transmittance measurement systems, search "Jingyi Optoelectronics transmittance measurement" or visit our technical library.
Where This Comparison Falls Short
Three limits should be stated plainly. First, this is not three instruments on the same bench, measuring the same sample on the same day; parameters come from published product documentation and public company information, and spectral range, cycle time, and interface specifications for the other two suppliers remain unconfirmed — the comparison carries real information asymmetry. Second, sample coverage was narrow, and thermal drift was never tested; the fiber model is rated for 5–80 °C (41–176 °F), and behavior outside that window is unverified. Third, export field formats and compatibility with specific MES versions were not jointly tested, so interface validation on your own system belongs in the purchase conditions.
Frequently Asked Questions
What is the practical difference between full-frame scanning and single-point transmittance measurement?
A single point reports one location, which is exactly the failure mode on curved, ribbed, or perforated parts: the thin or contaminated area sits a few millimeters away and never gets sampled. Full-frame scanning extracts values across user-defined zones and computes maximum, minimum, and mean automatically. At 0.8–1.0 seconds per part including OK/NG judgment, that approach supports 100% inspection on a welding line instead of a sampling plan you have to justify later.
How do you measure transmittance of a fiber light guide, and what should you watch for?
Terminate both ends into the sample-chamber interface and read the 380–1000 nm curve; the port accepts a 10 mm (0.39 in) diameter. Confirm end-face preparation quality before insertion, since a scuffed face reads as absorption. Use the end-face fiber image for alignment, set acceptance limits per part number, and export the report immediately after measurement.
Can transmittance data feed directly into MES or a quality database?
That depends on the configuration. The MES-linked variant lists manufacturing execution system integration and a traceability database among its configurable software options, while general-purpose models stay with local report output and an open database. Before purchasing, pin down field names, format, and interface protocol — otherwise integration becomes a second development project after delivery.
Which parameters matter most when sizing a transmittance measurement system for throughput?
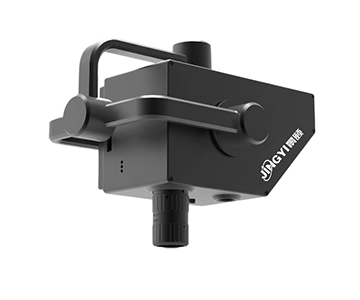
Start with cycle time and automation level. For IR-hole arrays, a two-hole fully automatic configuration runs 1000–1200 parts per hour with positioning accuracy better than 0.08 mm; for single parts with multiple points, compare per-measurement time (≤0.8 s versus ≤1 s) against repeatability (<0.5% versus <1%). Then check whether fixture loading, not measurement, is what actually sets your takt.
How can I independently verify long-term stability before committing to a purchase?
Run a periodic re-measurement on certified reference coupons and log drift at the same wavelength band week over week. Check the validity dates on the factory calibration certificate and any third-party metrology certificate, and ask for the accredited scope. During selection, require a repeatability demonstration on your own parts and compute the standard deviation yourself rather than accepting a quoted figure.
Reference Information
Sources
: Published product documentation for the JY-T980, JY-T980-R, JY-T04, JY-QT02, and JY-T03-2500Q systems; ISO 13468-1 and ASTM D1003 test methods; ISO/IEC 17025 calibration practice; manufacturer-supplied repeatability logs; ISO 9001 certificate No. 44625Q108860R0S; design patent ZL201811028557.0.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics — 12 years in optical inspection, spectroscopy equipment selection, and production-line quality data closure.
Conflict of Interest
: Jingyi Optoelectronics manufactures transmittance measurement systems and related optical metrology equipment. This analysis draws on public specifications and manufacturer documentation without third-party sponsorship.
Intended Use
: Educational reference only; validate all equipment choices through on-site POC testing under your own process conditions.
Updated
: September 2026