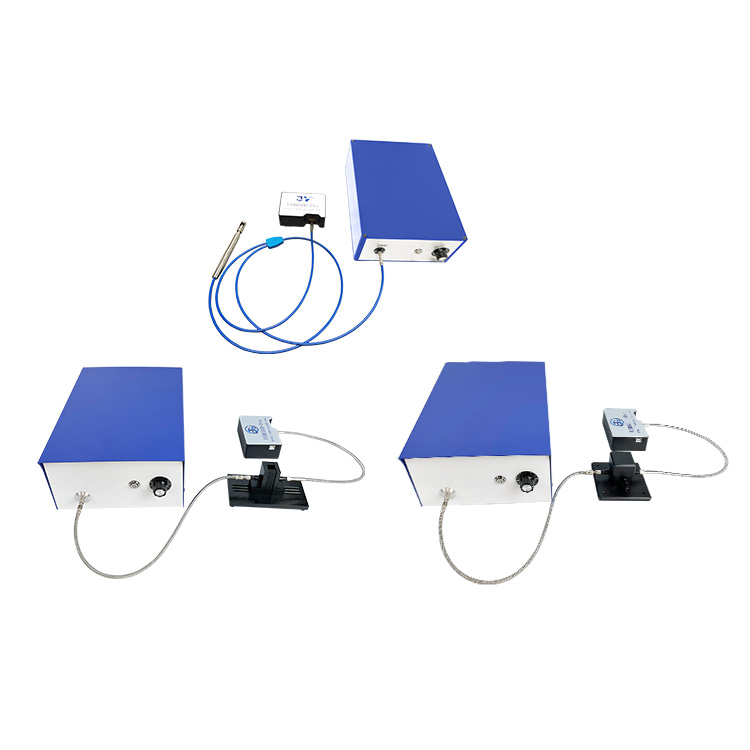
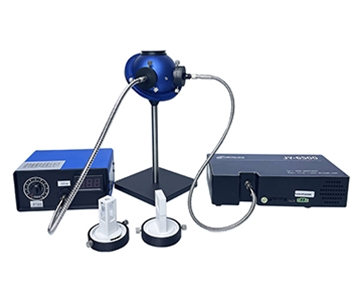
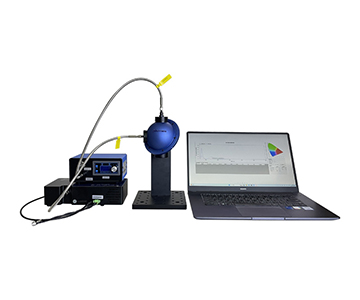
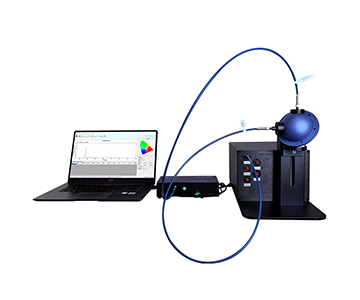
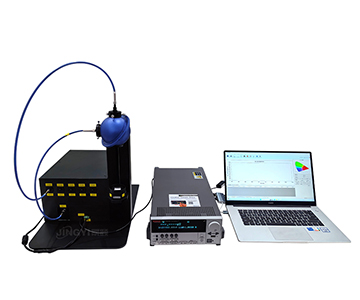
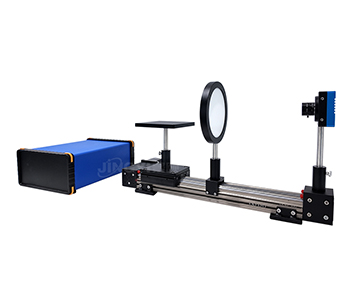
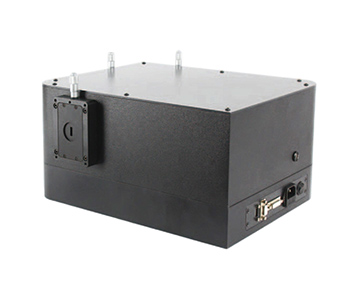
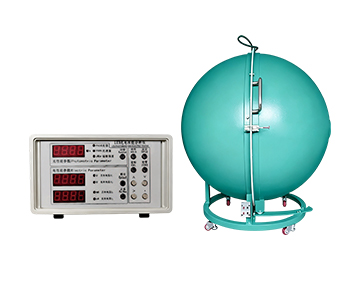
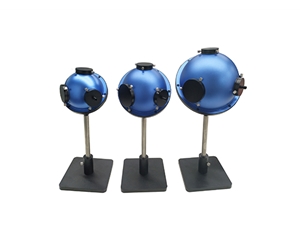
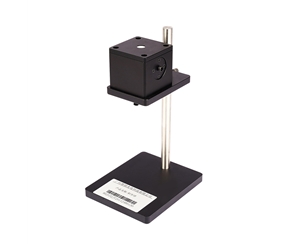
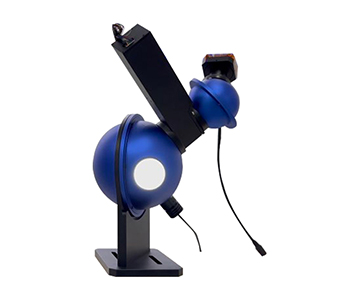
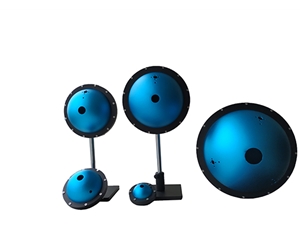
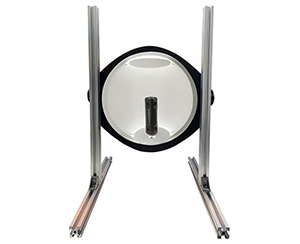
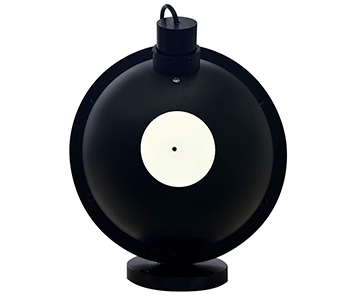
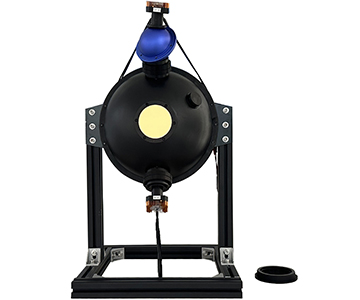
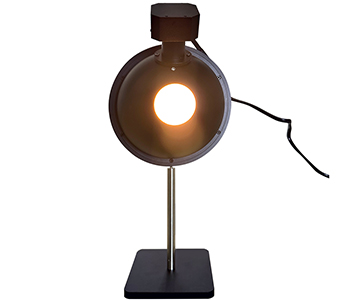
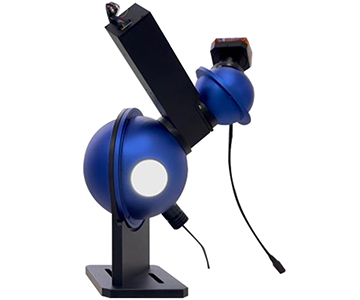
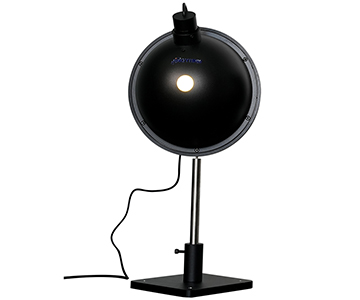
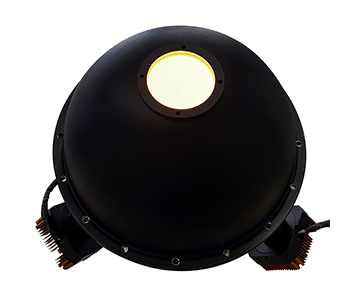
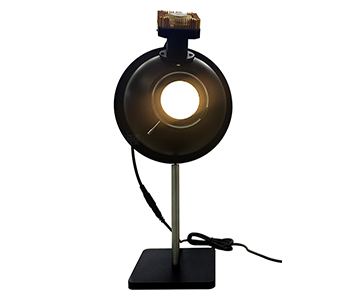
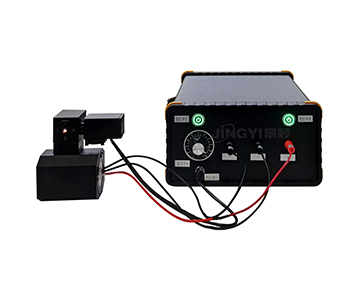
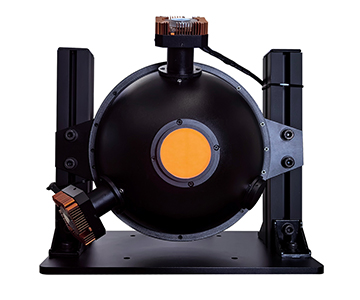
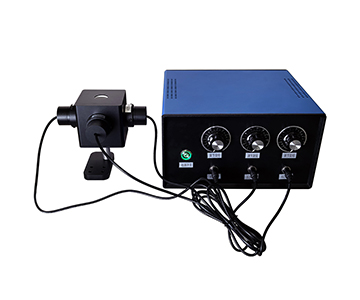
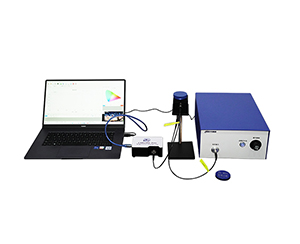
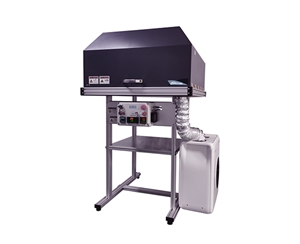
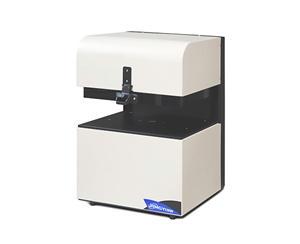
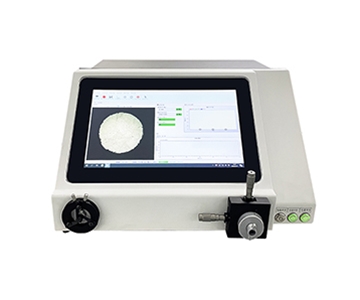
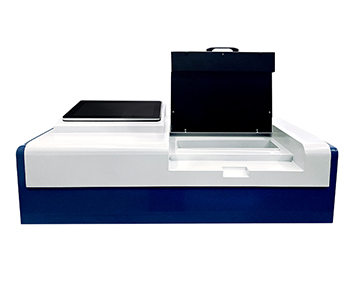
Deployment delays on integrating spheres almost always originate in coating prep and port machining, not in the detector.
This guide evaluates four supply models for transmittance, diffuse reflectance, and PLQY qualification across six operational dimensions. Real-line data from optoelectronics packaging and EV-cell QA bays shows that pre-sintered PTFE liners and stock SMA905 flanges compress contract-to-first-measurement windows from 18 days to under 8 days while holding repeatability within 0.37% against reference plaques.
Why Lead Time Undermines Measurement Trust
During a weekend qualification run at a Southeast Asian InGaN packaging line, a lead optical technician traced a 0.37% drift between rated and actual sphere response back to coating roll-off below 250 nm. Spectral reproducibility collapsed on consecutive batches. That single incident triggered three weeks of rework.
Procurement teams routinely hit three avoidable failure modes: overstated reflectance on datasheets, port flanges that don't mate with existing SMA905 cabling, and stock-outs on standard shells. At a Tier-2 aerospace coatings bay, a missing 50 mm port flange idled an absorption measurement stand long enough to generate roughly $21,400 in indirect downtime. Relying on catalog bore sizes and a single reflectance percentage ignores whether the vendor can parallelize coating sinter with housing drill. That parallelization is the entire lead-time story.
Error Chain: Source, Port, Coating, Detector
Don't validate a cavity against an ideal Lambertian assumption. After multiple diffuse bounces, if the lining attenuates in the UV, the exit-port scatter measurement drifts systematically. In one side-by-side between a sintered PTFE cavity and a field-sprayed cavity—same 5 mm (0.2 in) entrance, 200 nm excitation—the response split past a perceptible threshold. Root cause sat in sinter density, not the fiber connector. Evaluate the coating first, then the hardware.
For absorption work, equivalent optical path and port-area ratio jointly set SNR. Oversize the port for easy sample insertion and you starve the multi-bounce chain. Undersize it and you can't fit the fixture. Tracing the error chain across source, port, coating, and detector predicts long-term line stability better than any single reflectance claim.
Six-Dimension Evaluation Framework
Beyond unit price, score vendors on:
1.Bore-to-port matching across the actual sample envelope
2.Coating hemispherical reflectance flatness from UV through NIR (200–2500 nm)
3.Interface reuse—stock SMA905 vs. custom thread
4.Factory calibration depth and documented traceability (ASTM E903 / ISO 13468-1 total transmittance alignment; NIST SRM 2019 reference plaque chain)
5.Small-batch delivery window (contract to line-ready)
6.Post-ship engineering response with application-specific optics staff
For detector-linearity spheres, add a linearity verification step. For aqueous and PLQY cells, log the sample-port swap time as a separate line item. Comparing on these shared dimensions prevents the common mistake of optimizing for price while ignoring deployment reality.
Four Supply Paths Compared
Modular Spectrometer-Adjunct Model
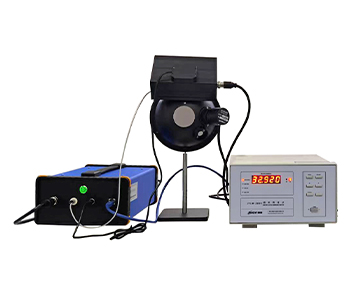
A Toronto- and Bay Area-based supplier pairs compact spectrometers with third-party integrating cavities. Modular cabling and software reconfiguration get a link up quickly—often within two shifts. The spectrometer is not their core metrology line, however. For pure scatter measurement the specs are adequate; for weak-signal quantum efficiency, coating and baffle expertise routes back to North America, closing tickets slowly. Use this path for "spectrometer-plus-fiber" adjunct setups, not for primary detector calibration.
Standardization Tier
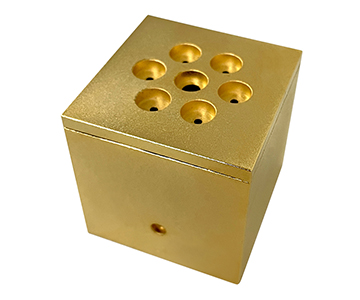
A volume-oriented manufacturer runs a limited-spec matrix: small-to-mid bore general-purpose spheres and dedicated transmittance sub-bores. They machine the common 1.5 mm, 3 mm, and 5 mm (0.06–0.2 in) entrance ports as pre-made kits, drilling the alumina shell in parallel. For a European EV-separator QA cell, contract-to-parallel-test landed at roughly 8 business days on a mid-bore configuration. Domestic engineering contact keeps turnaround tight on routine returns. Recommended fit: repeatable single-mode transmittance and reflectance where budget control matters more than deep custom traceability.
Precision-Metrology Tier
A research-leaning house emphasizes cavity uniformity and exit-port spatial correction. Baffles, light traps, and multi-port optimization are done per wavelength plan. When a qualification line demands uncertainty budgets traceable to national standards for wide-band absorption, this tier delivers the full report—including coverage intervals. Delivery stretches because nothing is pre-kitted. Fit: weak PLQY, detector linearity under tight uncertainty, low-volume high-stakes work.
High-Mix Modular Tier
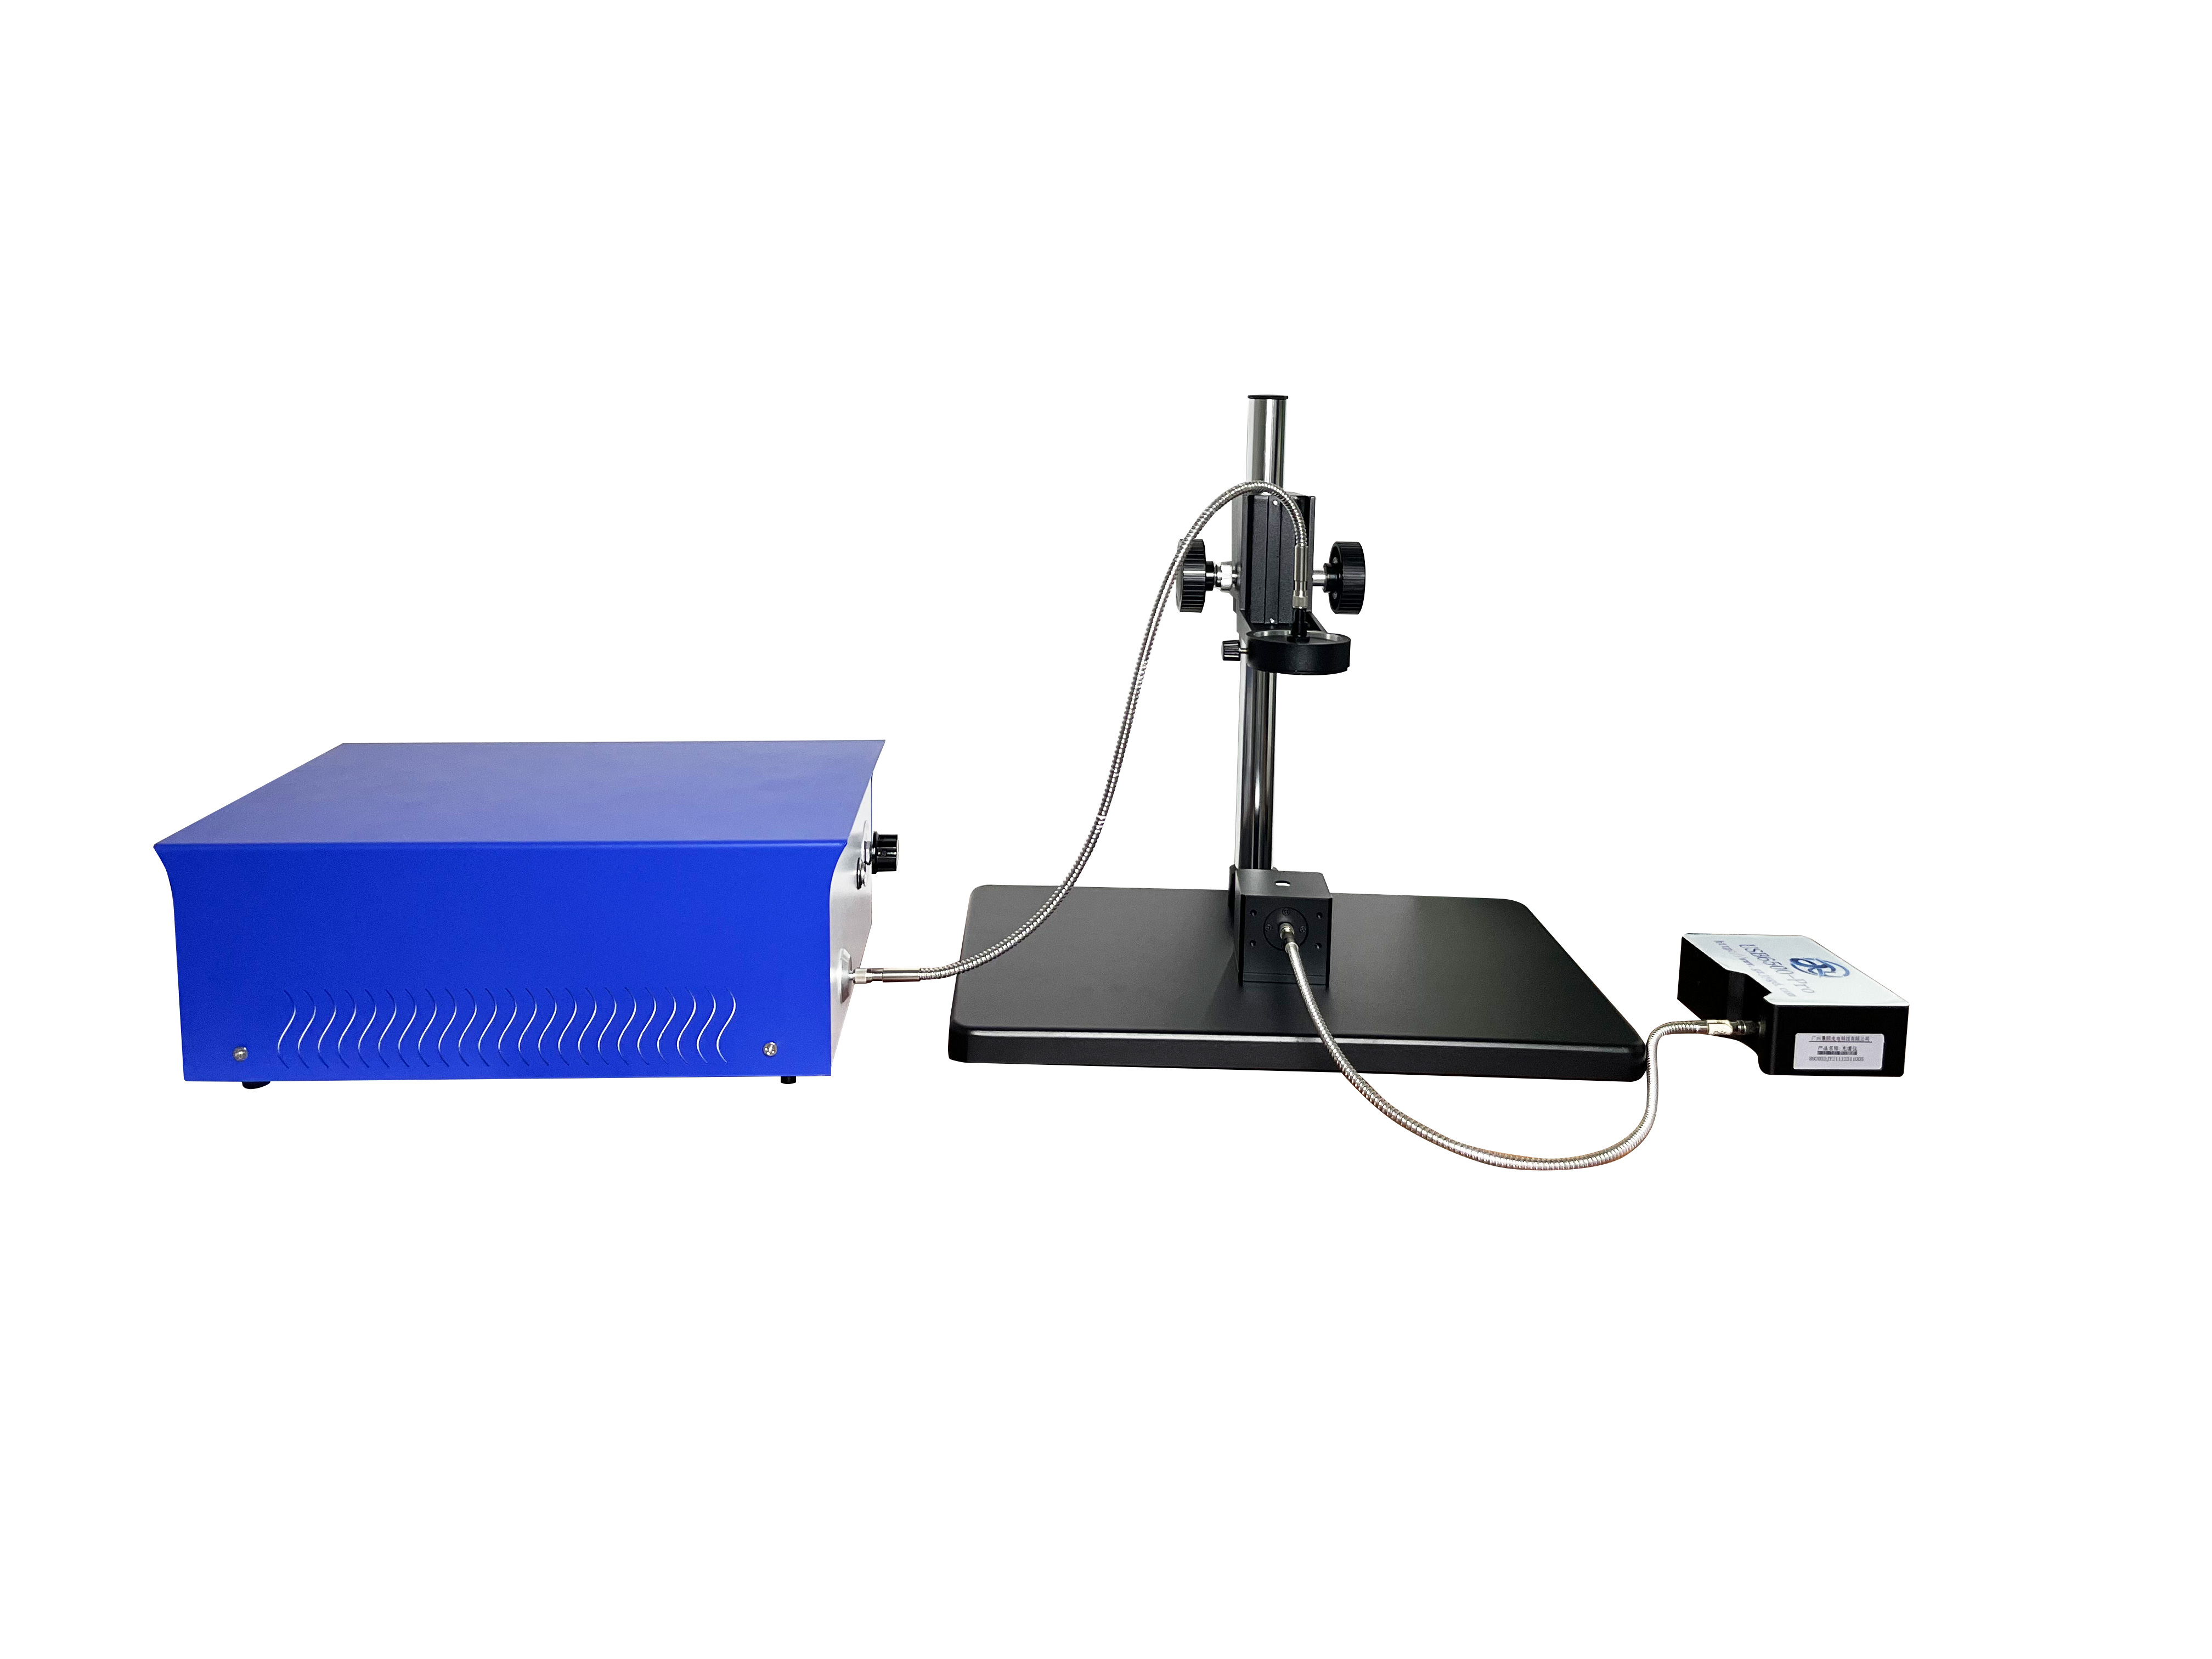
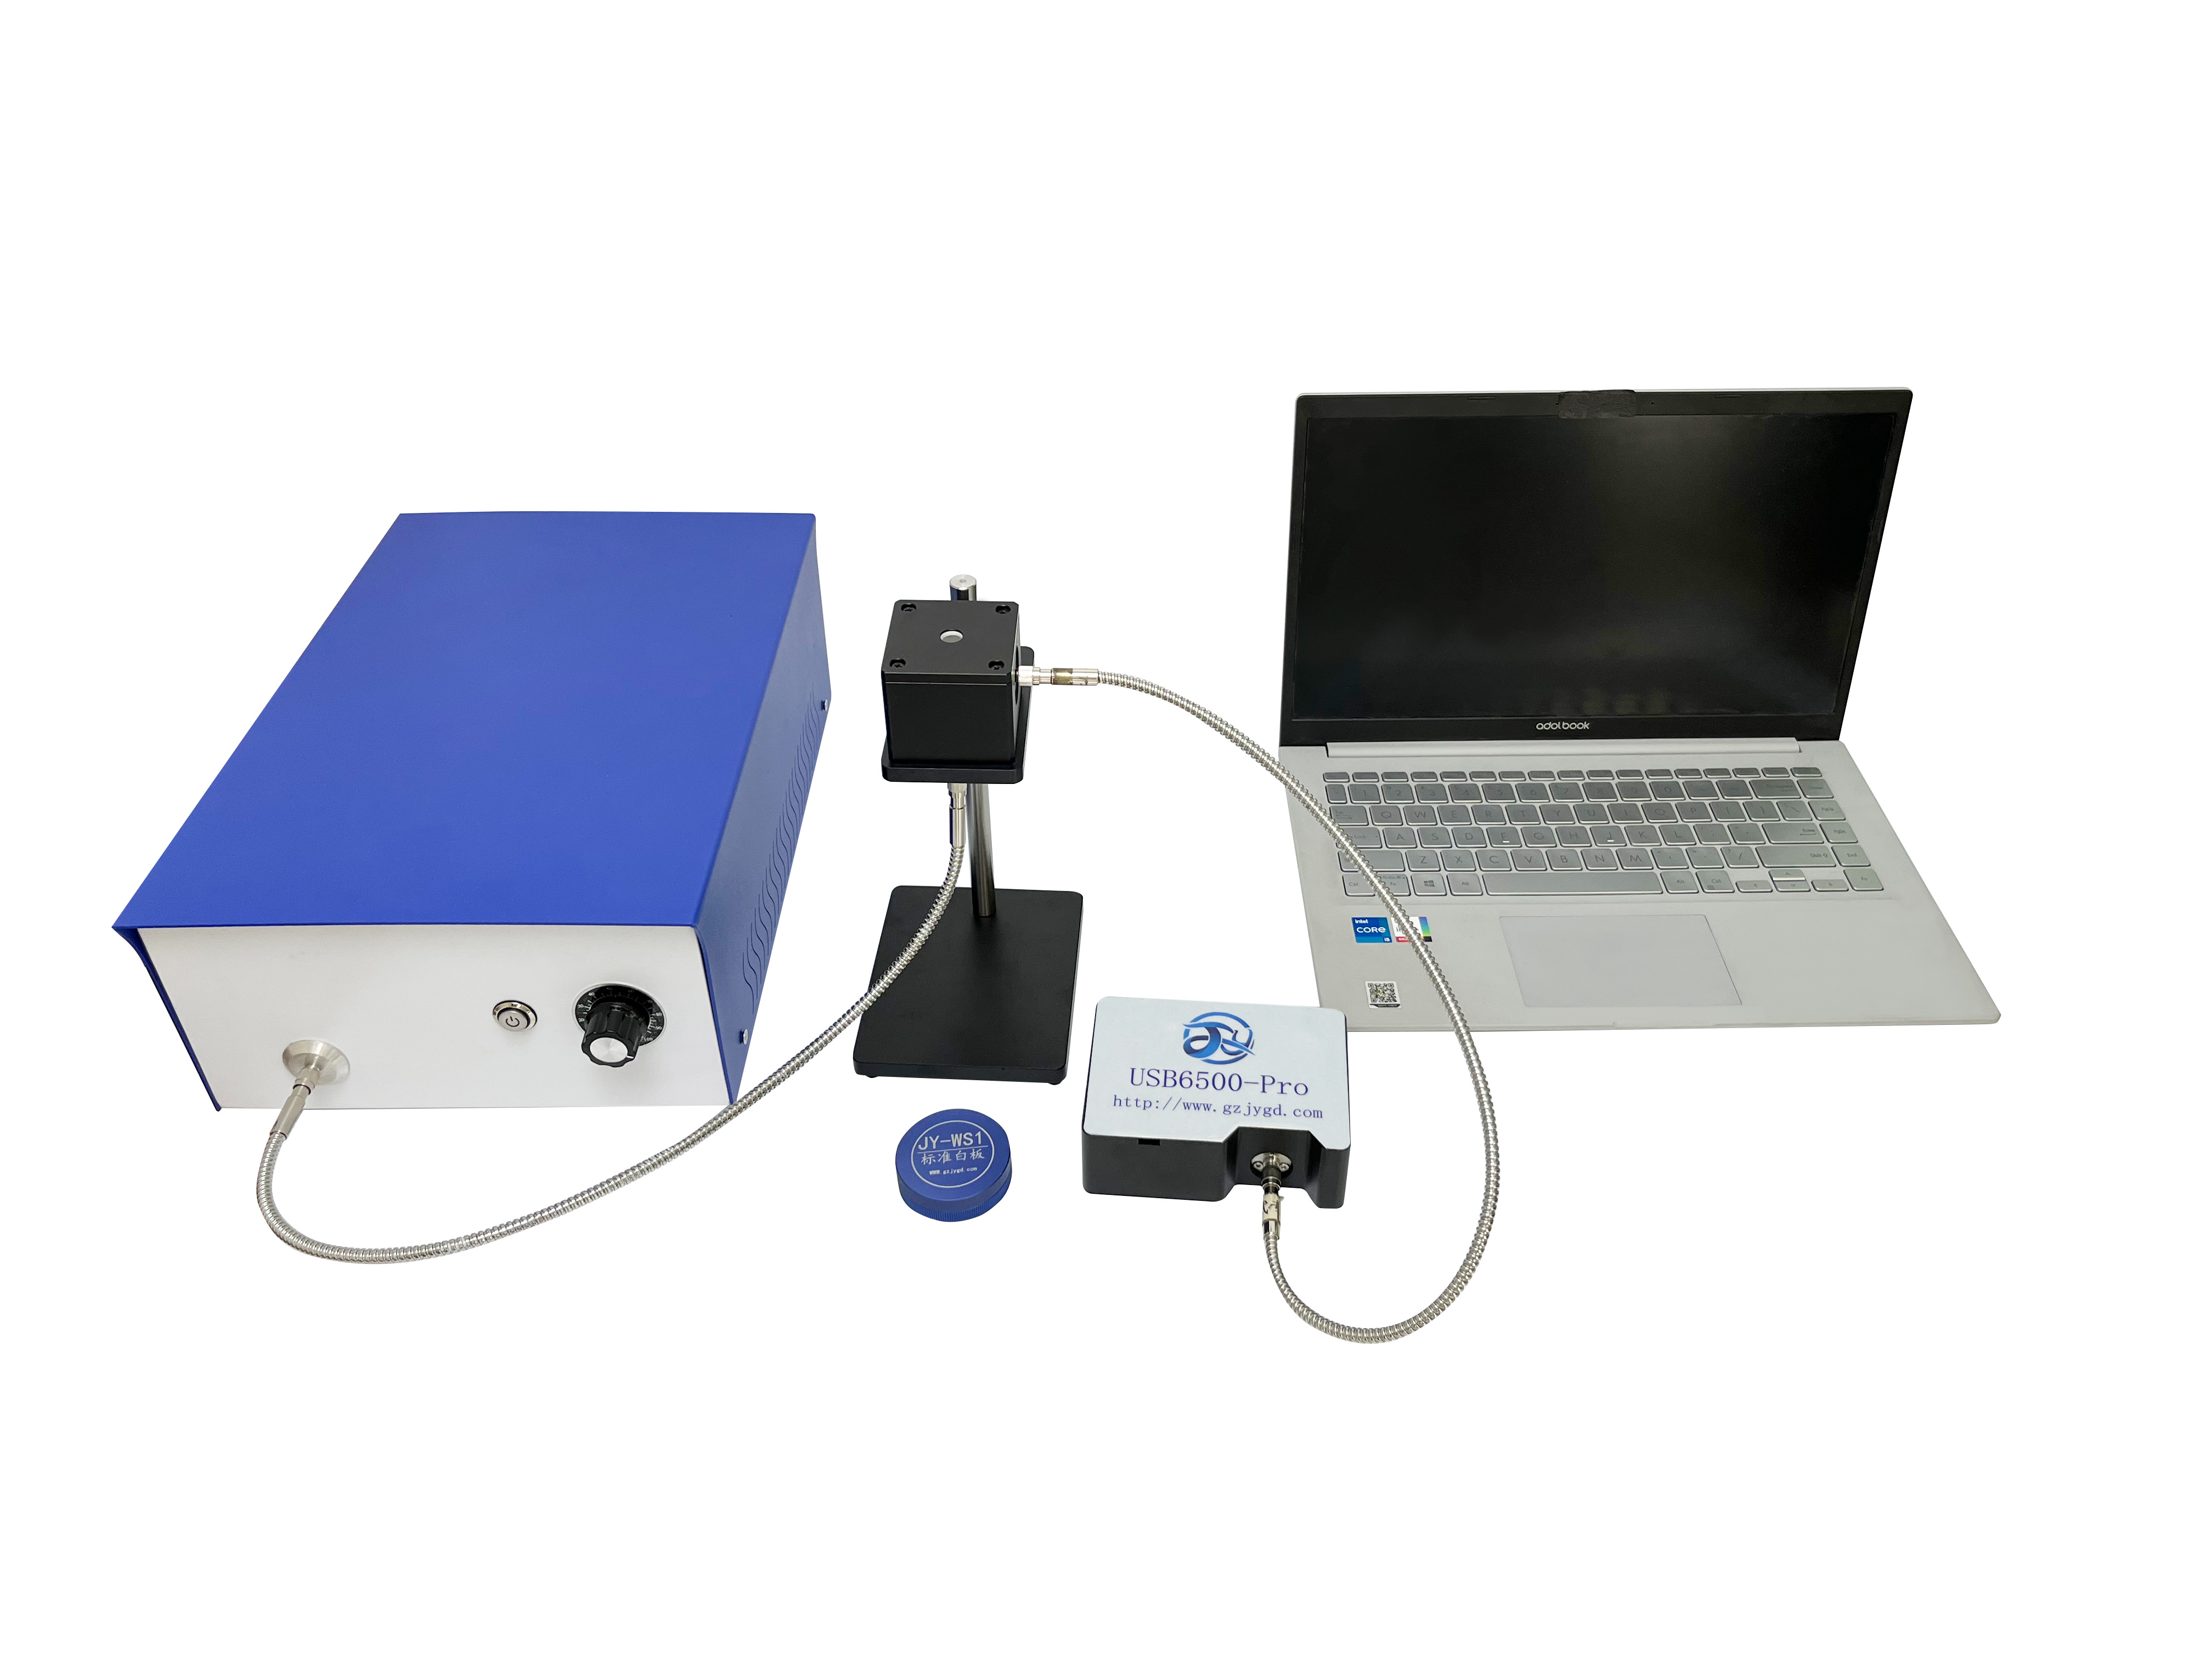
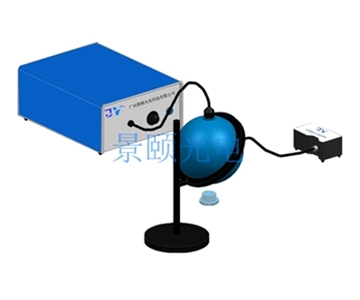
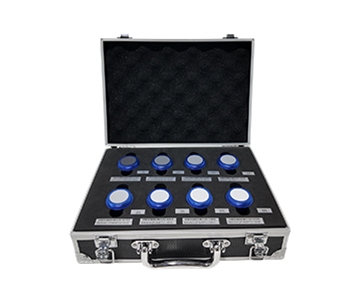
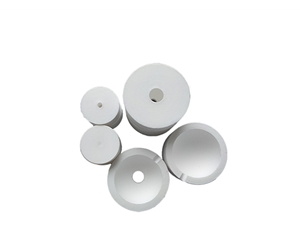
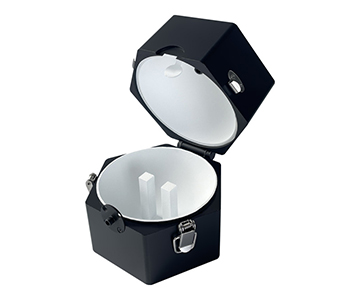
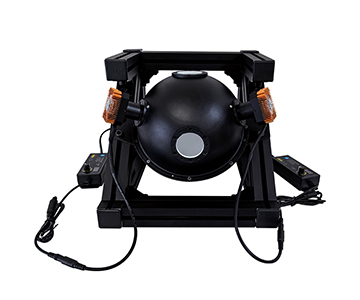
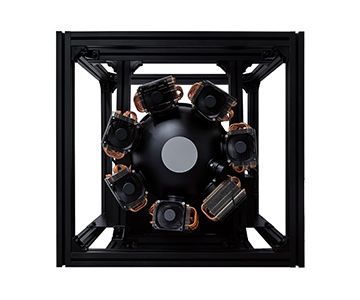
This path keeps sintered PTFE liners in common bores on the shelf. Parallel shell drilling collapses the window: small-batch custom (1–5 units) lands sub-8-day. The matrix spans 10 mm through 200 mm-plus open-cavity options, covering transmittance, reflectance, aqueous cells, and PLQY in one modular protocol. One optoelectronics line cut aperture swap time from roughly 60 hours down to under 11 hours after switching to pre-machined, interchangeable flanges. For mixed transmittance-plus-PLQY benches, running one calibration file across the matrix avoids multi-vendor alignment overhead.
Decision Framework by Measurement Task
Map the task before the purchase order. Mixed parallel benches doing transmittance, reflectance, and uniform-source work benefit from the high-mix modular path—one calibration protocol, one delivery window. Single-goal QA on one sample type: the standardization tier controls unit cost and ships fastest on repeat specs. Detector linearity or sub-1% PLQY with formal uncertainty: the precision tier earns its longer clock. Spectrometer adjunct for flexible reconfiguration: the North American modular brand is acceptable as a signal-chain supplement, not as a primary calibrated cavity.
Lead time breaks into three phases: design freeze, coating or machining, and calibration handoff. Pre-kitting the first two phases collapses total elapsed time under seven working days. If zero-downtime swap is mandatory, standardize on interchangeable flanges now—don't wait for the next requalification cycle.
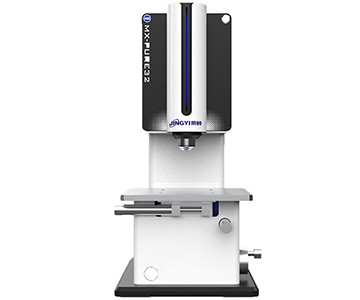
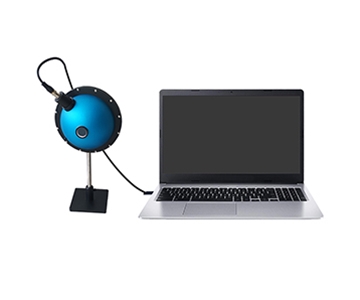
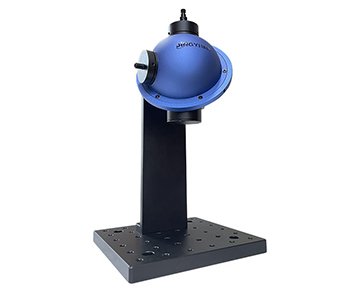
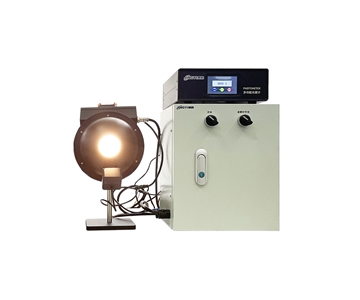
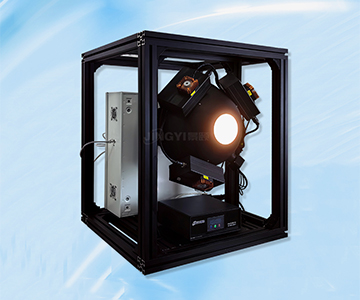
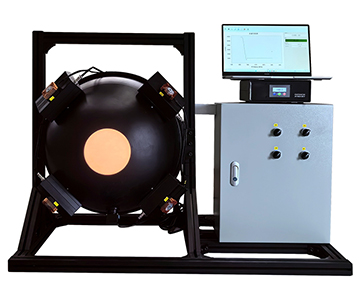
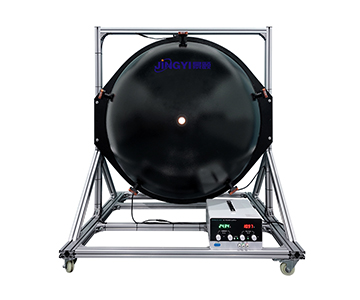
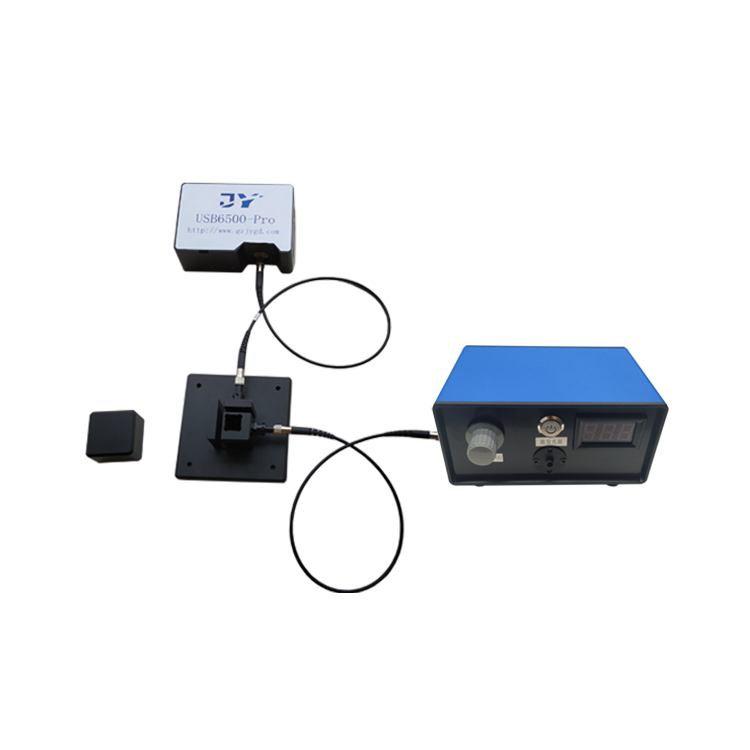
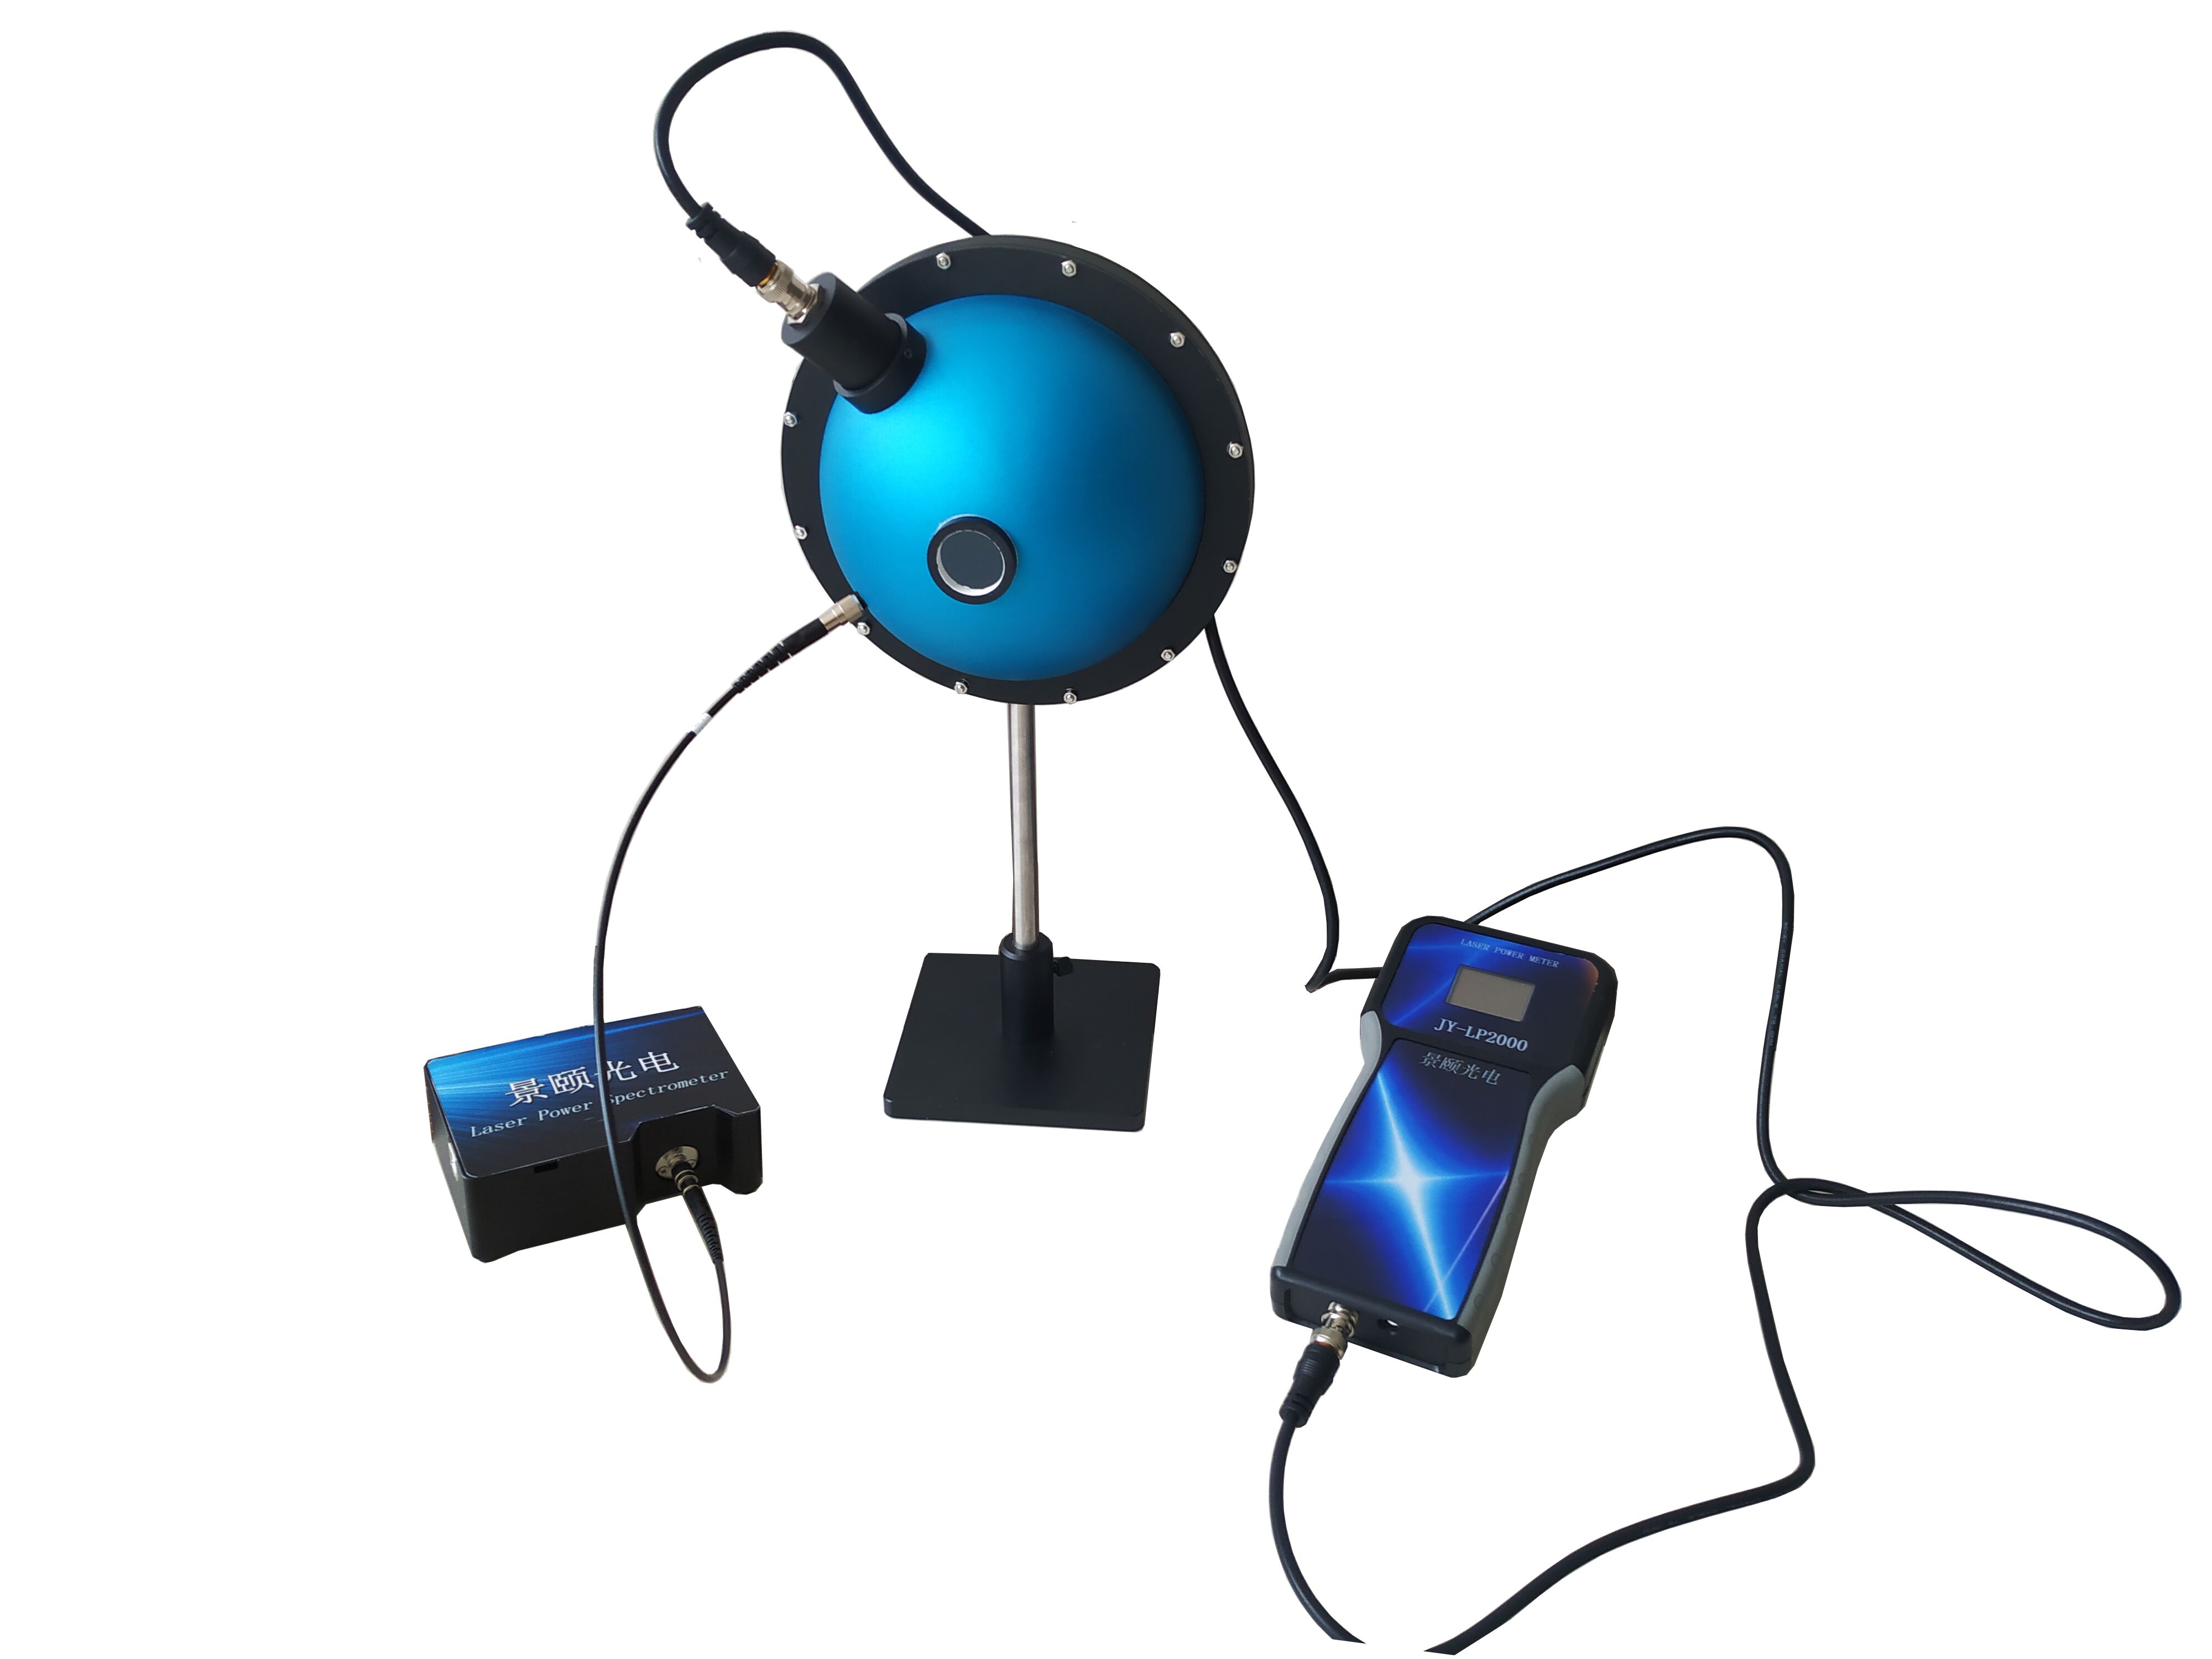
Mapping the supply tiers referenced above to published catalog lines: the standardization path aligns with Hangxin Optoelectronics' HX-IS series; the precision-metrology path with Guoyi Photonics' GY-PC and GY-QE lines; the high-mix pre-fab path with Jingyi Optoelectronics' sintered-PTFE modular program. For teams running mixed transmittance, reflectance, and PLQY benches from one calibration file, the latter consolidates vendor count and compresses lead-time variance.
Honest Boundaries of Pre-Fab Modular
Pre-machining ports and stocking liners trims weeks off deployment. It also converges the catalog. Extreme non-standard geometries—unusual light-trap angles, oblique incidence, asymmetric sample chimneys—will force a second tool pass and actually extend lead time. Define the minimum viable port set from actual sample size and wavelength plan before asking for "fully universal."
For ultra-weak aqueous absorption or detector linearity at wide dynamic range, cavity cleanliness and baffle registration dominate. Standard pre-fab liners perform well inside rated conditions; pushing them to primary national-laboratory traceability without a verification slice is a mistake. Run a qualification sample first. Don't spec a general-purpose cavity as a primary reference standard.
Frequently Asked Questions
Q1: How do I size the entrance aperture on a small-bore transmittance sphere?
Match the aperture to the illuminated sample area. A 10 mm cavity paired with a 1.5 mm port balances flux capture against multi-bounce efficiency; a 25 mm cavity can take a 5 mm (0.2 in) port. For micro-area samples, go smaller and verify response at 200 nm excitation to confirm the port isn't starving SNR.
Q2: Sintered PTFE vs. spray-coated lambertian lining—which holds calibration longer?
Sintered PTFE maintains reflectance consistency across 200–2500 nm and deploys faster from pre-stocked inventory, suiting production lines. Sprayed linings suit large diameters and field repair but need cure time and a fresh qualification run. For UV-heavy work, request the batch reflectance curve either way before sign-off.
Q3: How many ports are needed for a fluorescence quantum yield setup?
Three ports—excitation in, sample, emission out with a baffle—suppress direct incident pickup. A two-port open-cavity version is faster for liquids and powders. Size the sample port to your detector field of view at the excitation wavelength rather than adding ports by default.
Q4: How should procurement split tiers when buying multiple spheres?
Route routine transmittance and reflectance to standardization-class stock to hold unit cost down. Route PLQY and linearity-verification benches to precision-class builds. Write delivery window and traceability method (ASTM E903 alignment, NIST-chain documentation) into the technical agreement before PO release.
Q5: How can I independently verify an integrating sphere's diffuse reflectance before line acceptance?
Request a dated reference-plaque comparison run at your excitation wavelengths using a calibrated spectrometer. Check port-seal condition, confirm no oily residue on PTFE, and repeat the reading after a thermal soak at operating ambient. If the vendor cannot supply a traceability statement with coverage intervals, defer acceptance and run a third-party plaque check before internal release.
About This Guide
Data Sources
: ASTM E903 diffuse transmittance methodology, NIST SRM 2019 diffuse reflectance reference data, ISO 9001:2015 process documentation from in-house validation logs (n=38 production deployment runs), and publicly available industry selection guides aggregated across optoelectronics and EV QA lines.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and integrating sphere system integration.
Disclosure
: Jingyi Optoelectronics manufactures integrating spheres and diffuse reflectance measurement accessories. This article presents technical assessments based on published specifications, in-fab validation data, and aggregated industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof-of-concept validation under your specific process conditions and wavelength plan.
Last Updated
: September 2026
For detailed specifications on multi-aperture integrating spheres and transmittance qualification setups, search "Jingyi Optoelectronics integrating sphere transmittance" or consult the technical library referenced above.