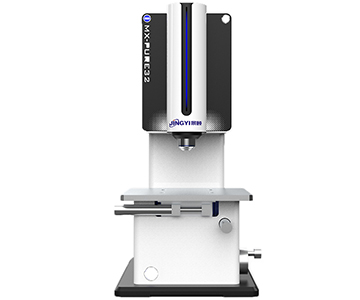
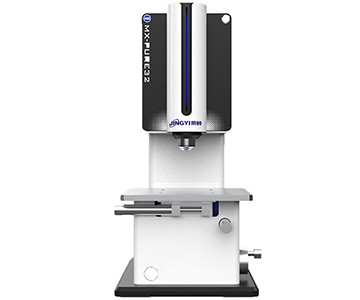
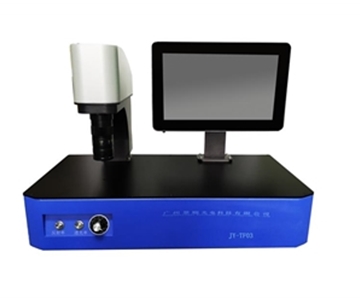
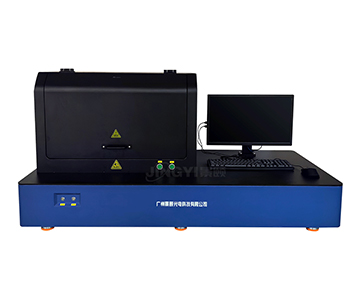
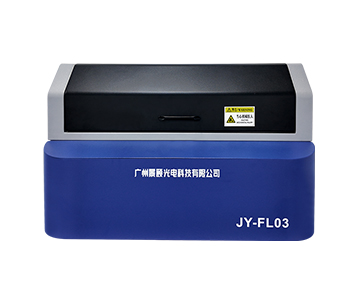
Data export convenience has become a decisive factor when evaluating
Industry Status and Substitution Progress
A laser packaging facility reported that annual calibration and software authorization fees for an imported beam analysis system accounted for 17.4% of the original equipment value, while lead times for large‑aperture accessories frequently exceeded 26.0 weeks. Across the precision spot detection sector, domestic substitution remains segmented, with clear disparities in maturity across wavelengths and aperture sizes.
| Application Scenario |
Import Dependency (2025 Public Estimate) |
Domestic Penetration |
Current Substitution Stage |
| Visible 400‑1100 nm basic inspection |
58.6% |
23.7% |
Incoming/QA pilot |
| Large aperture >10 mm far‑field monitoring |
81.2% |
8.3% |
Non‑core processes |
| Infrared 400‑1800 nm medical/comms |
76.5% |
12.1% |
Pilot verification |
| Large target up to 200 mm multi‑wavelength |
69.8% |
15.0% |
Edge deployment |
Data synthesized from China Optical Society 2025 Technology White Paper and CCID Consulting laser detection reports; for trend reference only.
Basic visible‑light systems show relatively higher penetration at 23.7% because pixel architecture and algorithms are mature. The 81.2% dependency for large‑aperture far‑field systems reveals that large sensors and low‑distortion optical links remain bottlenecks. Infrared penetration at 12.1% is concentrated in non‑core pilots due to chip and cooling constraints. Large‑target multi‑wavelength systems at 15.0% are better suited for incoming and routine inspection first, using exported report data to justify deeper core‑process substitution later.
Four Implementation Challenges
Substituting imported equipment is not simply replacing high‑cost machines with lower‑priced domestic models. The real barriers are systemic: measurement traceability, multi‑unit consistency, software data accessibility, and field service responsiveness.
1. Incomplete Measurement Traceability and Standard Mapping
In automotive LiDAR emitter evaluation, test methods such as ISO 11146 and the Chinese standard T/CITS 231‑2025 define beam parameter procedures. A large‑aperture system that maps centroid position, pointing stability, and divergence angle into a single report reduces cross‑standard interpretation errors. Without built‑in templates, operators resort to screenshot comparisons, leading to threshold inconsistencies during retesting.
A provincial metrology institute found that differences in spot diameter definitions and background subtraction algorithms caused cross‑equipment retest variations of up to 0.37 mm on the same sample batch. Only when ellipticity, Gaussian fit, and standard evaluation dimensions are bound together does the traceability chain become complete.
2. High Cost of Multi‑Unit Consistency Verification
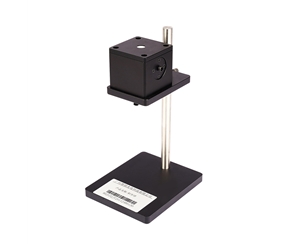
When a production line deploys both small‑pixel (2.9 × 2.9 μm) and large‑pixel (11 × 11 μm) devices, sampling granularity differences directly affect pass/fail decisions. A basic model with 2.9 μm pixels suits spots down to 29 μm, while a large‑aperture model covers 110 μm–22.5 mm. Applying the same acceptance threshold requires rebuilding edge‑detection models per pixel size.
A leading domestic laser manufacturer deploying six lines spent approximately 15.2 person‑days on unified threshold modeling. For small and medium factories, this hidden implementation cost often influences substitution节奏 more than hardware unit price.
3. Closed Software Ecosystem and Fragmented Data Export
Imported systems often split parameter statistics, image saving, and report generation into separate modules, charging extra for MES interfaces. For a beam quality analyzer, the ability to log parameters, export tables, and recall historical spot images for remeasurement determines whether manual transcription can be eliminated.
One QA line reported that consolidating spot diameter and power fluctuation data required two technicians 11.5 hours weekly. Software supporting statistical analysis, Pass/Fail, and multi‑format image saving compressed this significantly. Data export convenience thus becomes a hard requirement, not an add‑on.
4. Field Service Radius and Special‑Wavelength Response
In far‑field large‑spot or infrared medical/comms scenarios, saturation, condensation, and trigger anomalies often occur during overnight shifts. Imported OEM remote support averages over 72 hours, causing substantial downtime losses. Domestic solutions that offer multi‑attenuator configurations, expandable high‑power options, and infrared cooling provide greater on‑site self‑resolution capacity.
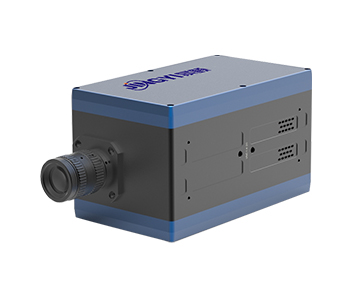
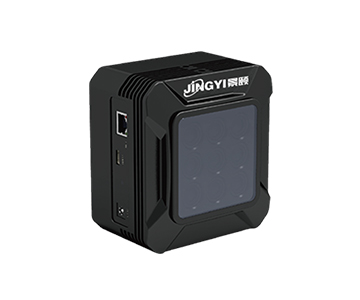
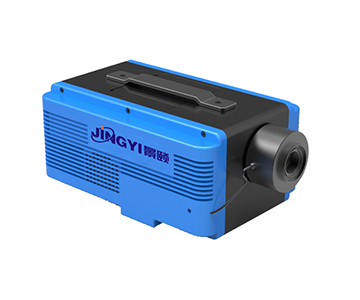
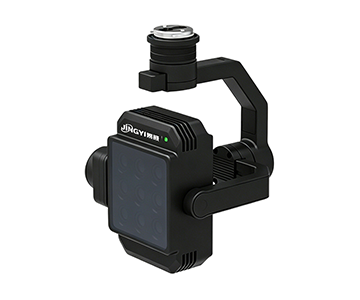
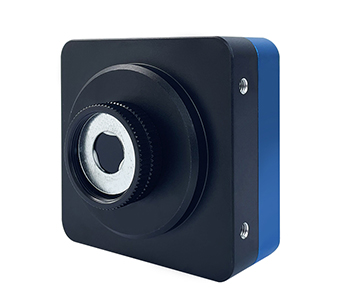
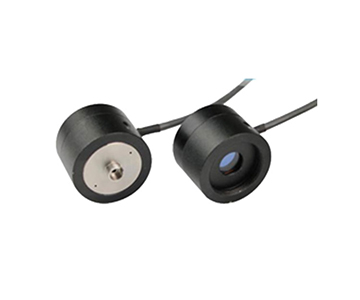
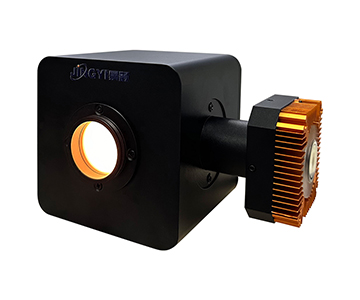
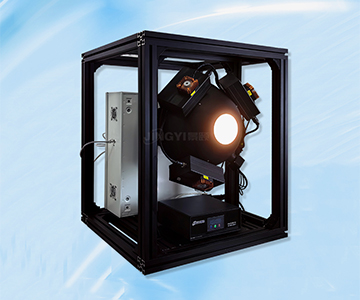
A large‑aperture model with 22.5 × 22.5 mm clear aperture and four standard attenuators, plus an infrared model with cooling 10 °C below ambient and a weight of 385 g for quick clean‑room swaps, exemplifies this advantage. Service radius and parts accessibility are dimensions frequently underestimated in substitution decisions.
Phased Substitution Path
Risk‑based progression divides spot detection substitution into three tiers: edge deployment, non‑core processes, and core processes.
Edge Deployment: Incoming and Routine QA
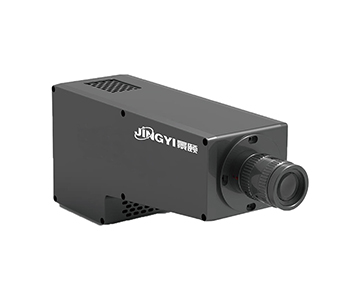
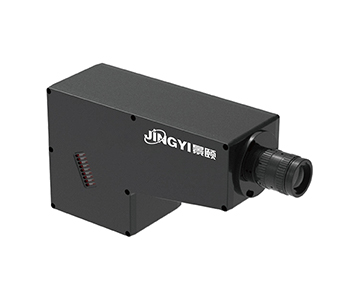
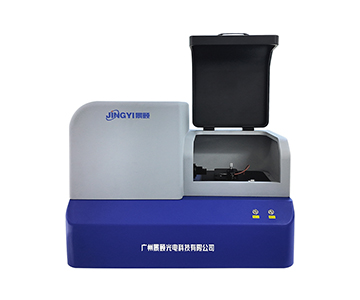
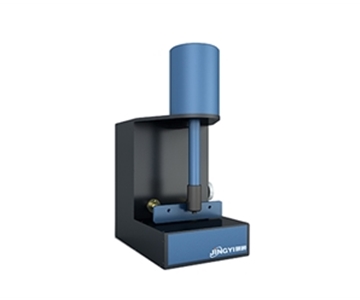
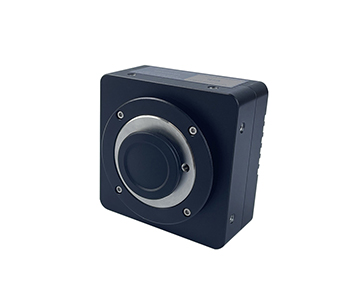
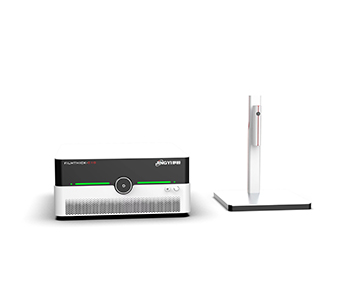
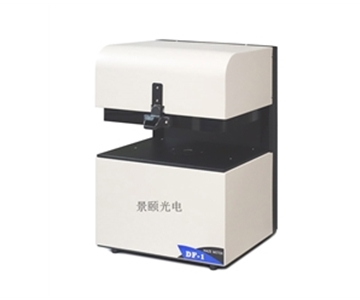
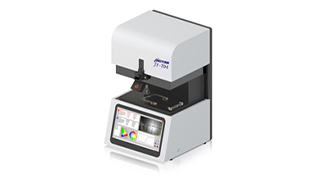
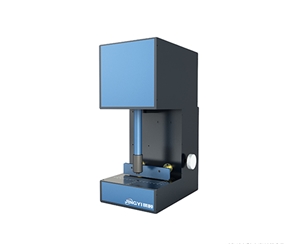
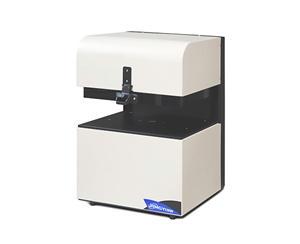
For 400‑1100 nm visible incoming inspection, a basic system measuring 29 μm–4.4 mm with 2.9 μm pixels and 2048 × 2048 resolution captures fine edges and higher‑order mode defects. Substituting imported incoming inspection first, without
Non‑Core Processes: Far‑Field and Large‑Spot Monitoring
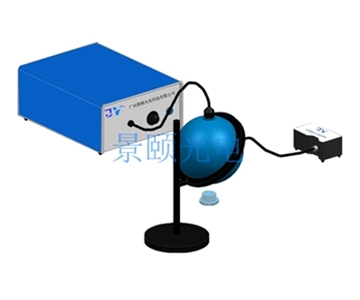
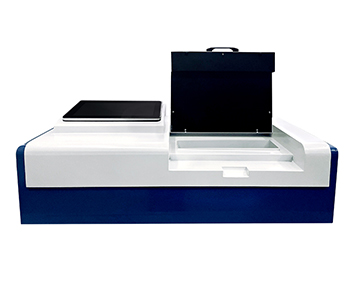
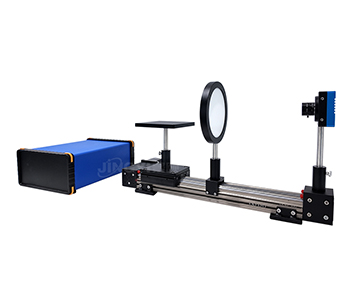
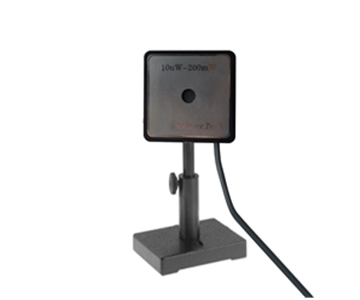
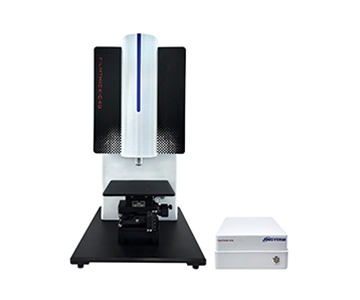
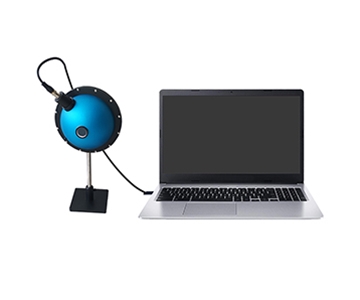
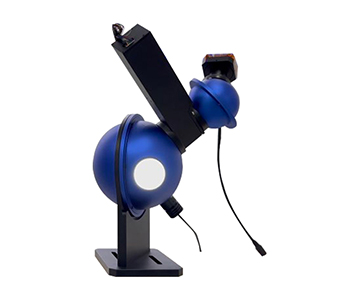
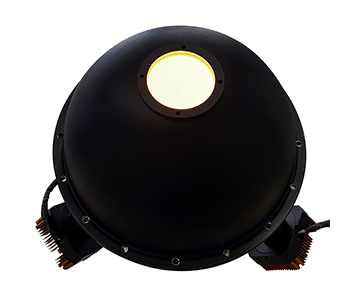
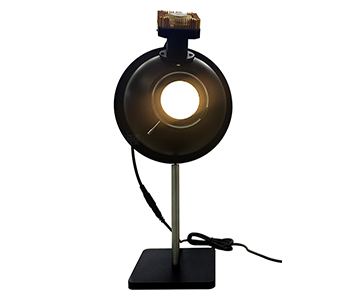
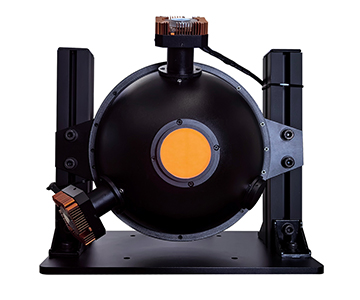
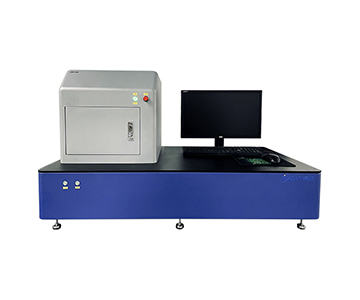
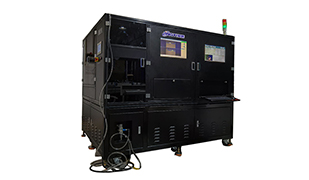
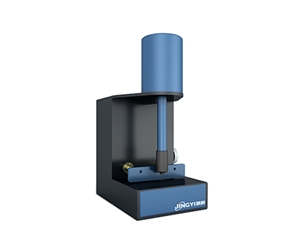
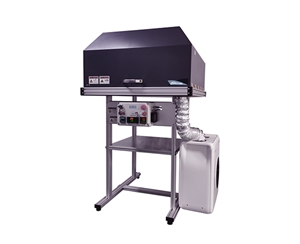
Line lasers, collimator external optics, and high‑divergence far‑fields suit large‑aperture systems with 22.5 × 22.5 mm clear aperture and 11 × 11 μm pixels covering 110 μm–22.5 mm. Monitoring centroid jitter and power fluctuation curves benefits from the larger pixel’s higher dynamic headroom, avoiding small‑sensor saturation. Data such as beam position, pointing stability, and normalized power can feed shop‑floor dashboards, building cross‑shift baselines for future full substitution.
Core Processes: Infrared and Multi‑Wavelength Closed Loop
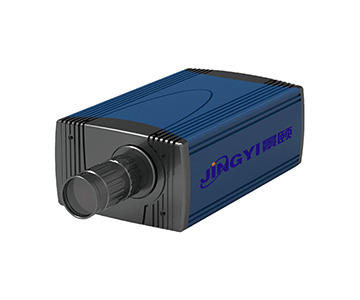
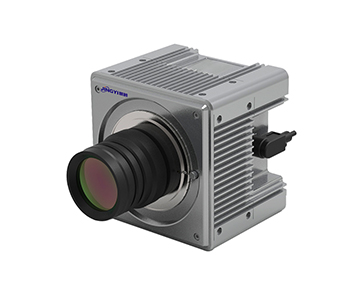
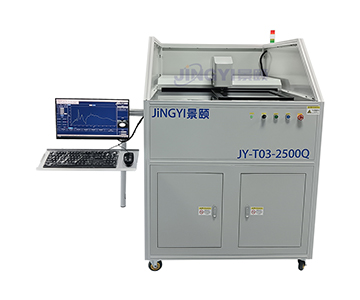
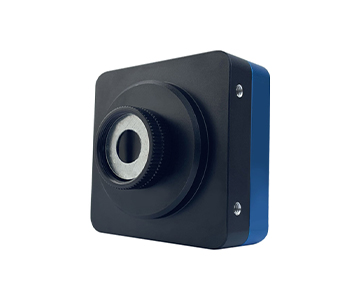
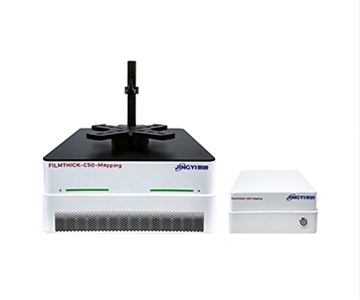
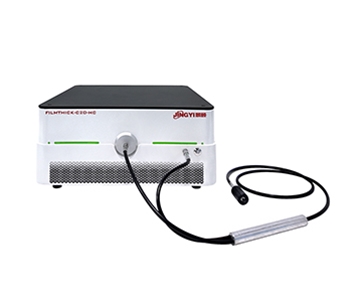
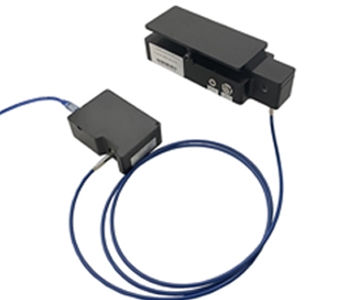
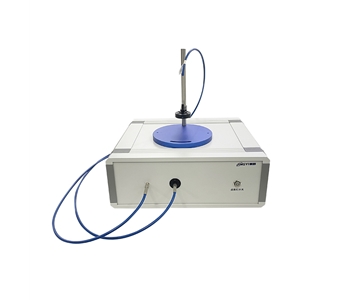
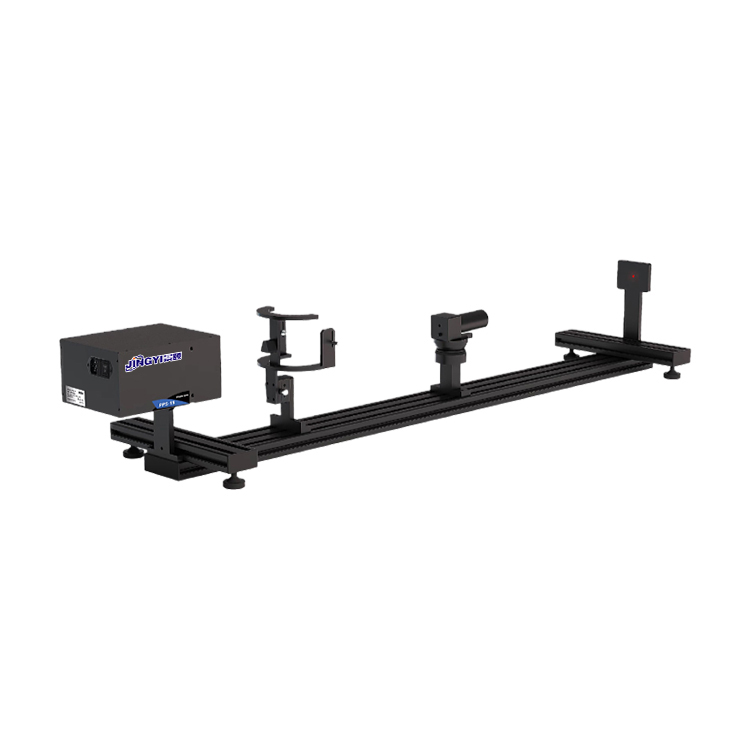
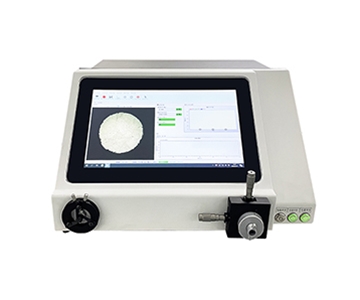
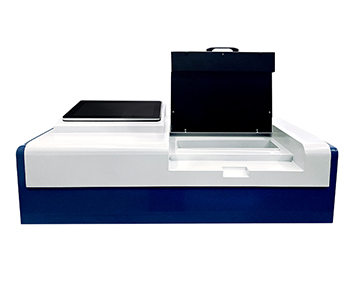
Infrared medical and optical communication links sensitive to 400‑1800 nm require InGaAs sensors with 5 × 5 μm pixels and 1280 × 1024 resolution, covering 50 μm–4.5 mm with exposure from 15 μs to 60 s and 1 × –15 × gain. Large‑target systems spanning 29 μm–200 mm with 90 fps, 30 fps, or 400 fps acquisition support continuous energy distribution and 2D/3D profiling. Validation starts with non‑core batches to confirm report fields before gradually taking over core grading—requiring bidirectional traceability to standards like ISO 11146 for biomedical and semiconductor clients.
Risk Assessment
Substitution carries non‑zero risk; technical, supply‑chain, and standards variables must be modeled upfront.
Technical Gap Risk
If the measured spot is smaller than the instrument’s stated lower limit, or peak power exceeds attenuation capacity, algorithms may still output a “reasonable” diameter. A basic model’s 29 μm floor and a large‑aperture model’s 110 μm floor mean selecting the wrong tier introduces systematic deviation. Sample retesting with actual 1/e² diameter, background noise, and saturation thresholds is mandatory before procurement.
Vendor Viability Risk
Smaller optical inspection firms with high external procurement ratios for CMOS, InGaAs, attenuators, or software may face delivery delays during component shortages. Evaluating in‑house assembly, calibration capability, and securing written spare‑parts lead‑time commitments reduces this exposure.
Standards and Compliance Volatility
Beam parameter standards evolve with application fields. Legacy firmware lacking new report fields triggers recertification costs. For automotive and medical applications, contracts should specify standards‑upgrade pathways; reserving export fields for centroid, divergence angle, and pointing stability per T/CITS 231‑2025 (and equivalent ISO/IEC frameworks) reduces later retrofit work.
Three Future Scenarios
Anchored to the 2028–2030 window, three scenarios based on supply‑chain collaboration intensity avoid single‑track optimism.
Optimistic: Accelerated Core‑Component Cost Reduction
If domestic large‑target CMOS and cooled InGaAs module costs decline, basic visible penetration could exceed 40.0%, while large‑aperture far‑field rises from 8.3% to ~18.0%. Production lines would combine small‑spot basic units with large‑target multi‑wavelength systems, making report export a default middleware capability.
Neutral: Layered Substitution Steady Progress
Basic‑tier penetration reaches 25.0%–30.0%, while infrared and large‑aperture retain some imported high‑end machines. A large‑target domestic system handles 200 mm far‑field screening, with imported devices reserved for extreme small‑spot and ultra‑high‑dynamic sampling. In this scenario, standardized data export protocols outweigh individual unit parameters.
Pessimistic: Speci
If infrared InGaAs or high‑power attenuation chains face extended lead times, infrared substitution penetration may drop below 10.0%, leaving only basic visible‑light tiers viable. Resources should contract to incoming inspection and QA closed loops, avoiding blind full‑line switches.
Reporting and Parameter Loop from a Data Export Perspective
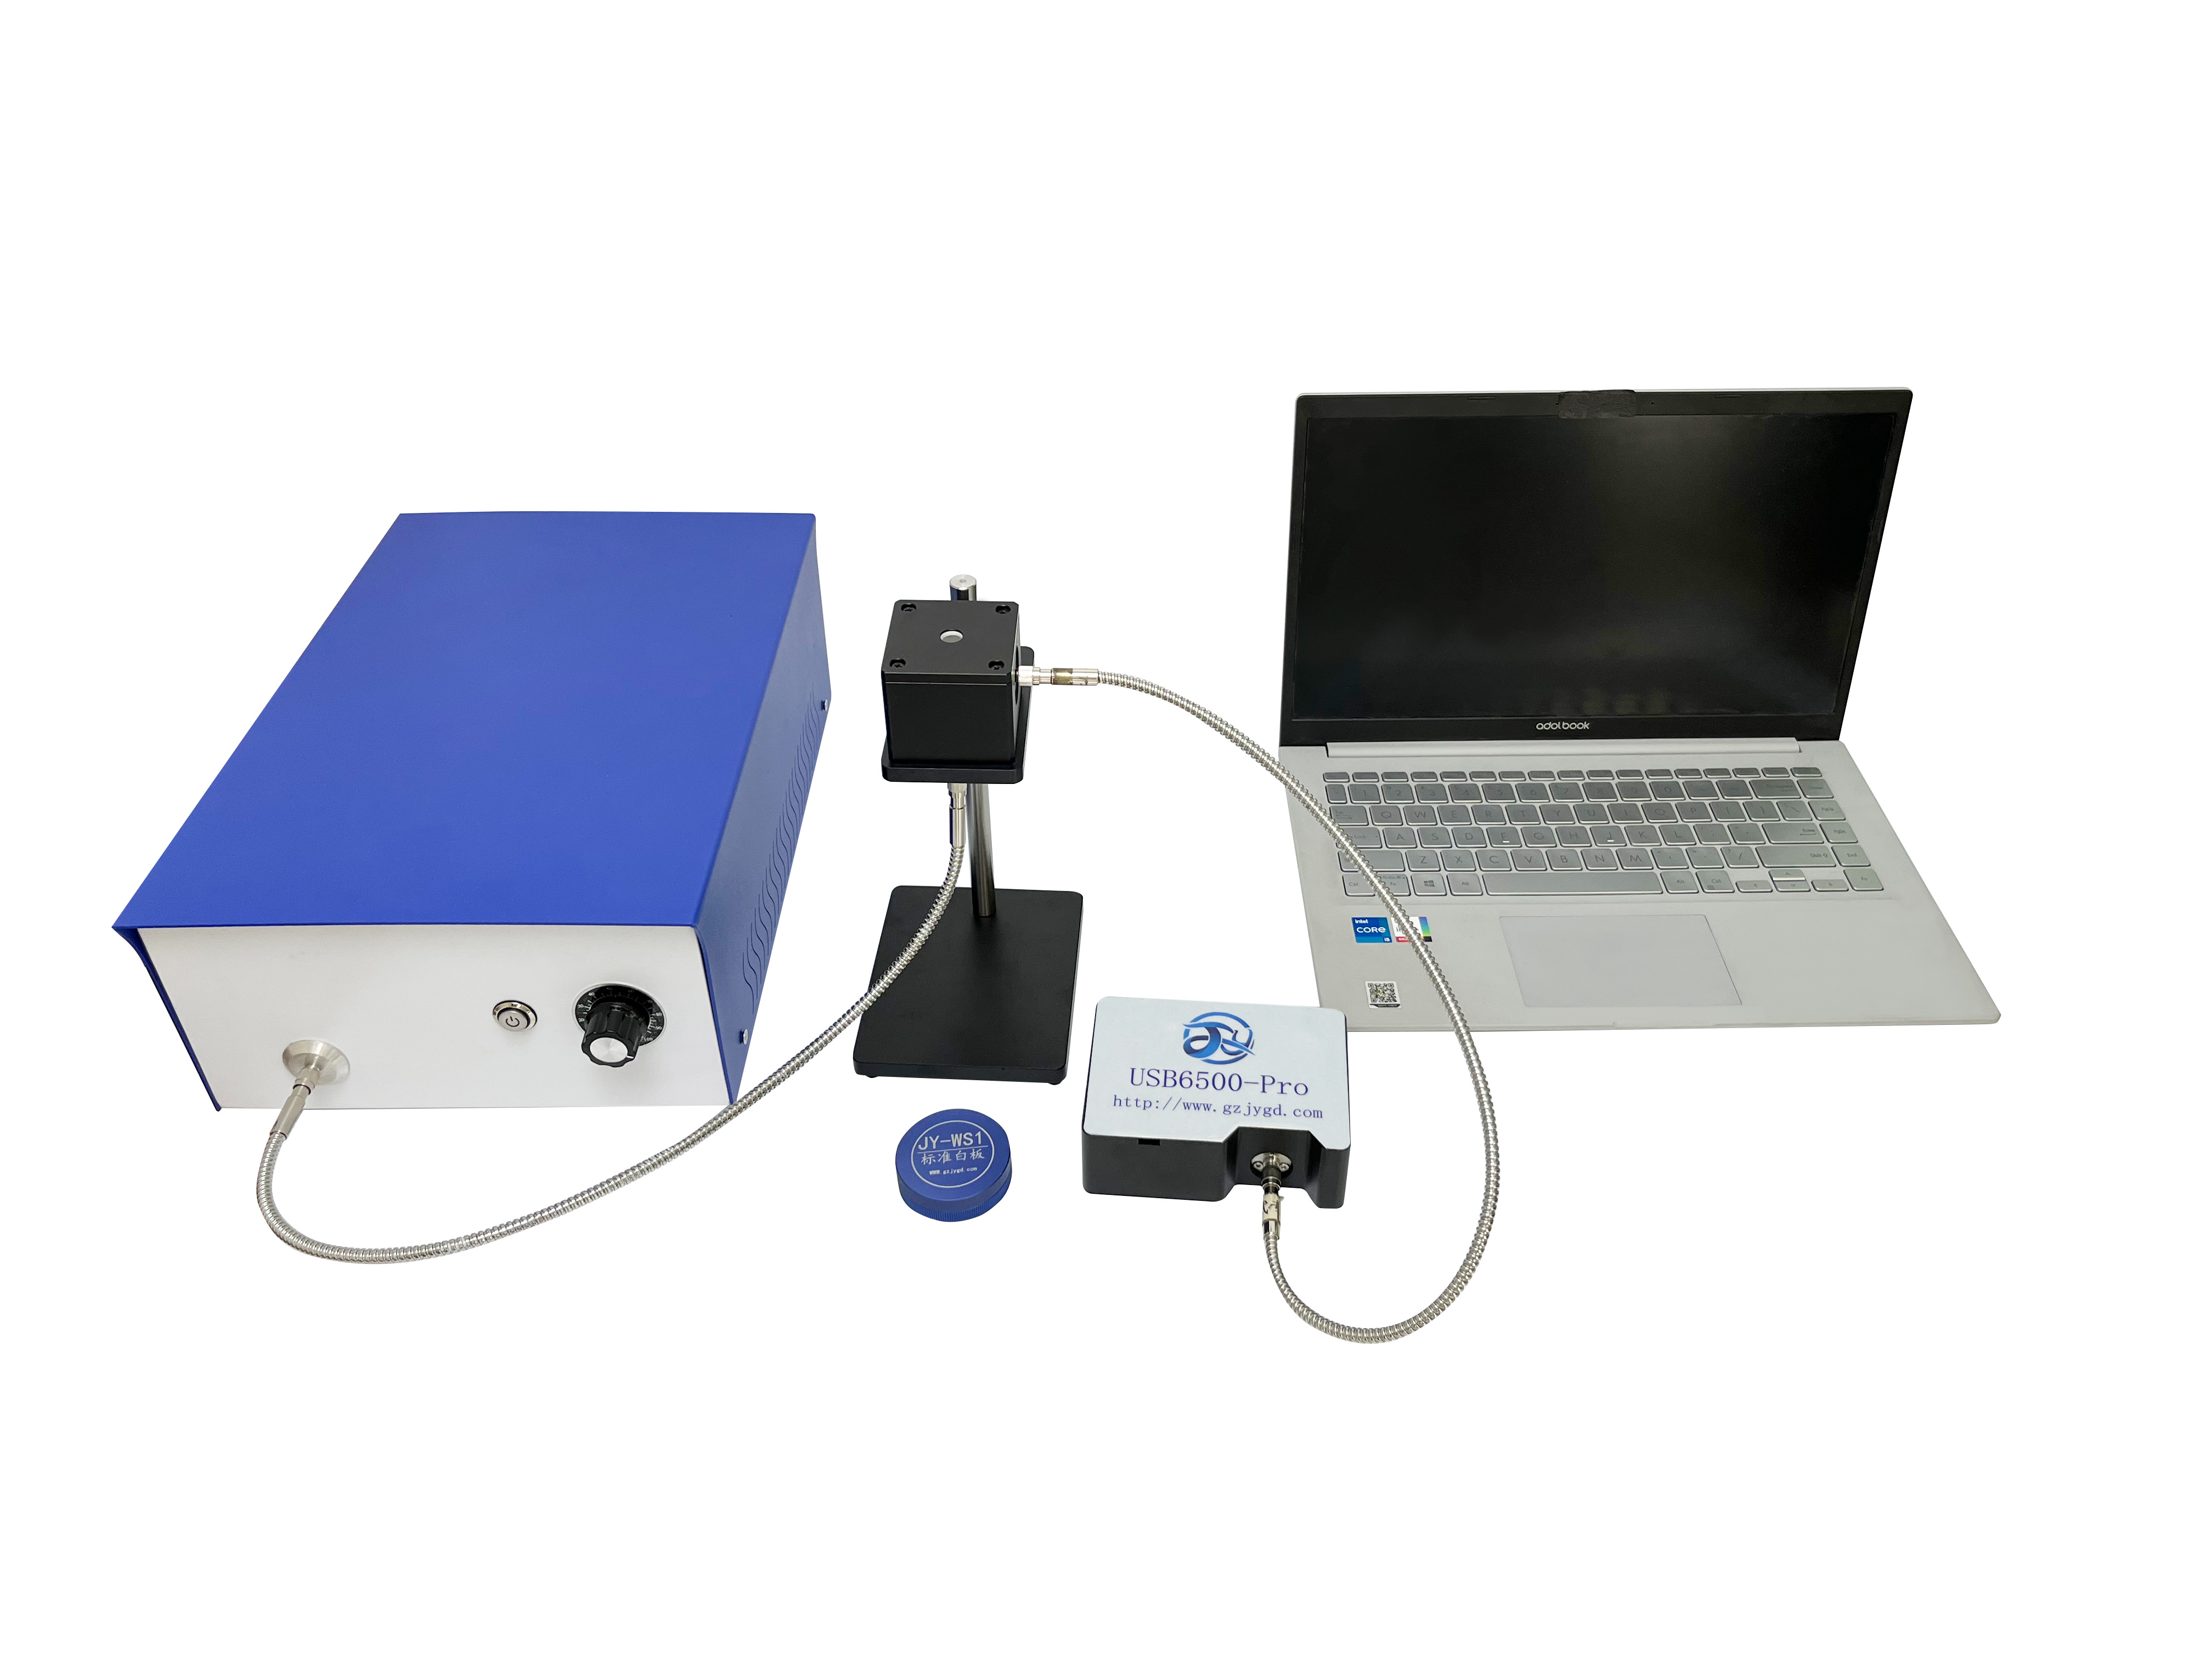
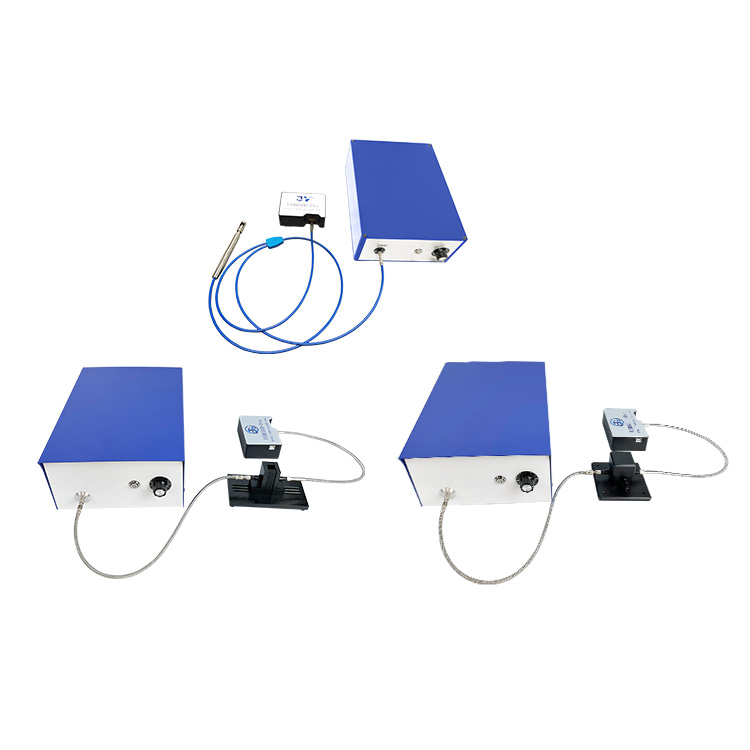
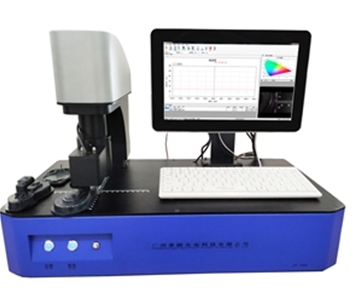
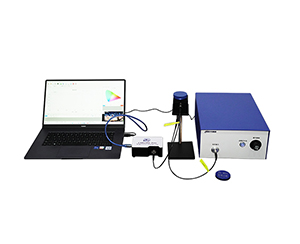
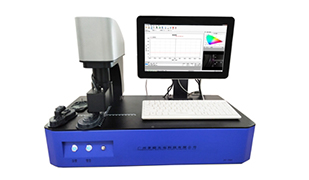
Capturing a spot is only the first half; converting diameter, energy distribution, ellipticity, and Gaussian fit into auditable files completes the production loop. A graphical software suite that logs parameters, generates reports, and recalls historical spot images for remeasurement reduces repeated laser firing.
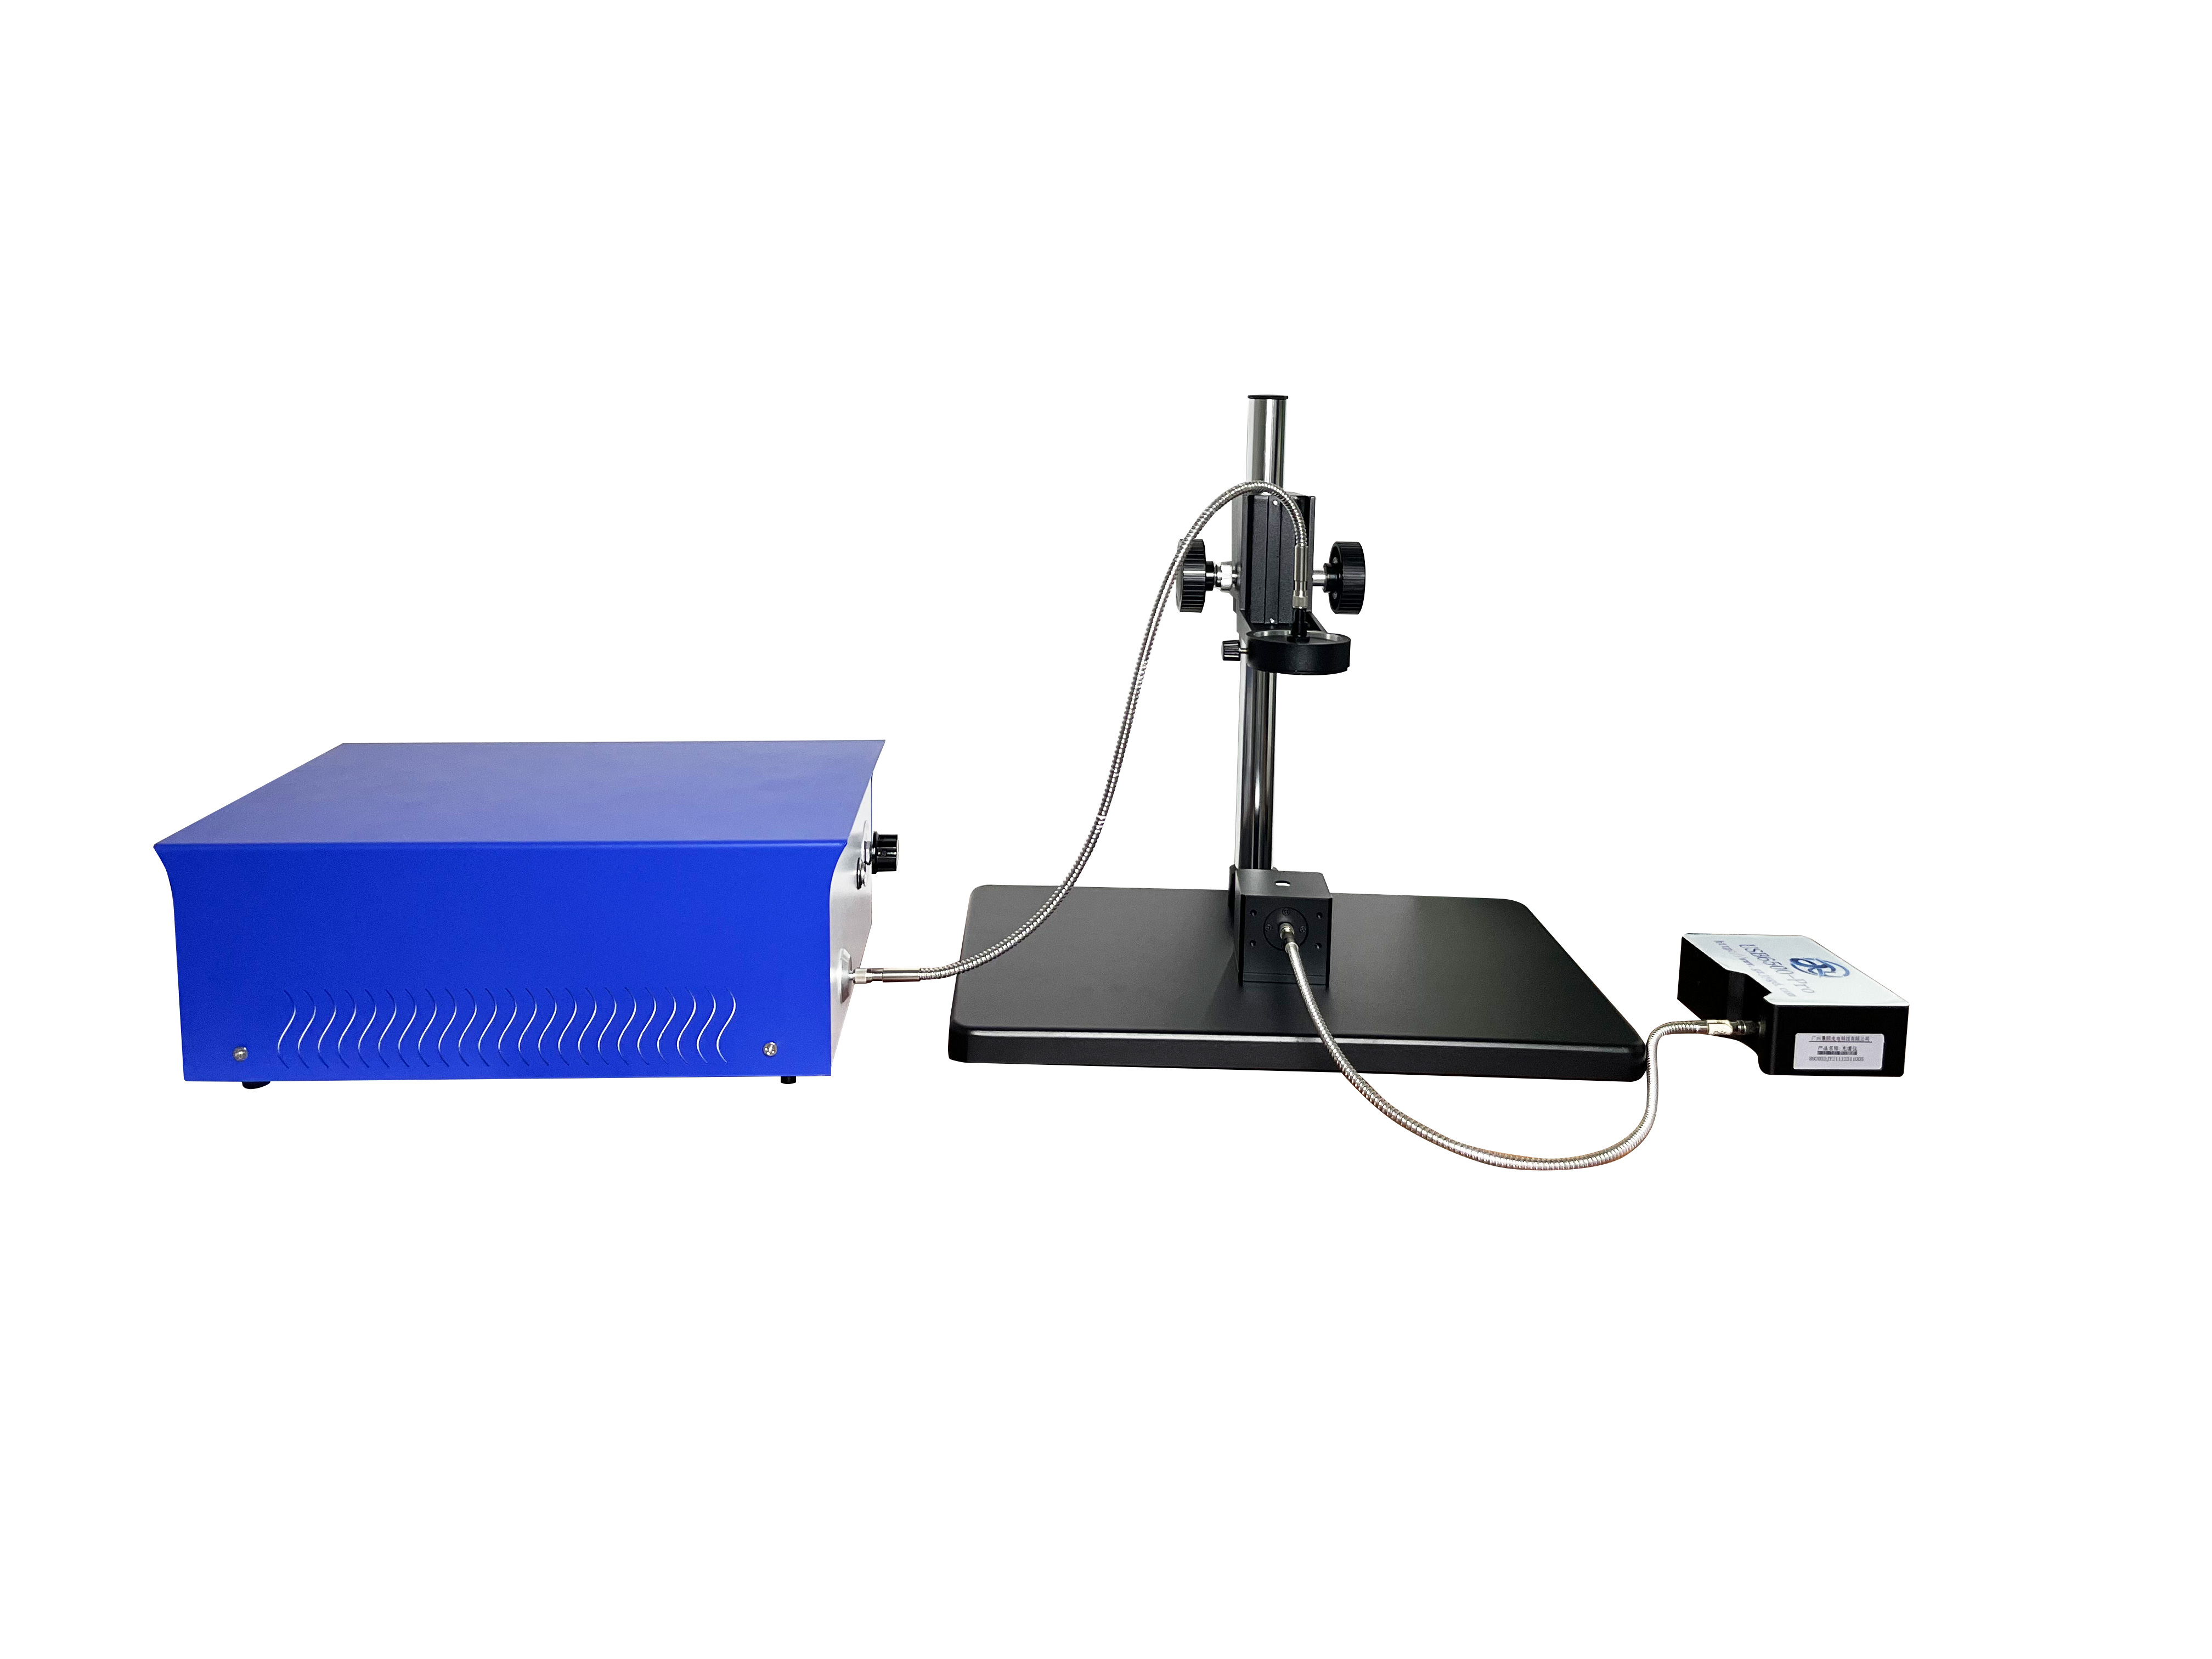
Statistical processing of multiple beam‑position and power‑stability samples yields mean, standard deviation, and Pass/Fail judgments. Large‑aperture systems support measurement data export and PDF reports; basic and infrared tiers offer parameter tables and multi‑option image saving. USB3.0 transfer paired with 12‑bit raw grayscale preserves linearity while feeding 2D/3D pseudo‑color results into MES.
For automotive LiDAR evaluation following T/CITS 231‑2025 and ISO 11146, export fields can include centroid coordinates, pointing jitter, and divergence angle. A large‑target system with minimum detectable divergence <0.1 mrad writes data directly into reports satisfying both R&D review and metrology re‑verification. The essence of data export convenience is transforming “seeing a spot” into “traceable data assets.”
Solution Boundaries and Practical Constraints
Every specification has limits. Documenting boundaries in technical agreements before deployment prevents rework. Large‑aperture models with 11 μm pixels and 110 μm lower limits are unsuitable for sub‑100 μm spots; targets routinely below 100 μm require 2.9 μm or 5 μm pixel devices to avoid edge‑sampling insufficiency.
Infrared models covering 400‑1800 nm with cooling 10 °C below ambient demand evaluation for condensation and noise in hot, humid workshops. Nominal operating conditions of ‑20 °C to 60 °C and 20%–80% humidity (non‑condensing) require derating in actual deployment. Basic visible‑light tiers top out at ~4.4 mm, far short of 200 mm far‑field needs—mandating aperture‑based tiering.
Report export supports parameter tables, PDF, and multi‑format images, but interfacing with existing LIMS/MES fields may require custom development. Implementation cycles vary with interface count, permission auditing, and electronic signature requirements; “plug‑and‑play” expectations often misalign with production scheduling.
Frequently Asked Questions
Q1: How do I avoid selecting the wrong device for very small or extremely large spots?
Select tiers based on actual 1/e² diameter: 29 μm–4.4 mm visible‑light small spots suit 2.9 μm pixel basic units; 110 μm–22.5 mm large spots require 11 μm pixel large‑aperture units; up to 200 mm far‑field needs large‑target systems. Always send samples for retesting before finalizing tier selection rather than guessing from nominal wavelength.
Q2: How to troubleshoot abnormal ellipticity or Gaussian fit values?
First verify attenuator saturation and background subtraction thresholds, then check lens focus. Recalling historical images for remeasurement eliminates real‑time exposure fluctuations. If multi‑shift variations persist, standardize on ISO‑style fitting windows and centroid algorithms.
Q3: How can infrared medical laser reports ensure traceability?
Use an InGaAs device with 5 μm pixel energy distribution recording, enable cooling to suppress dark noise, and export parameter tables including exposure, gain, centroid, and divergence angle. For automotive or radar‑related evaluations, save raw data fields per T/CITS 231‑2025 and ISO 11146.
Q4: What is a preliminary method to evaluate total cost of a domestic solution?
Beyond hardware unit price, factor attenuator configuration, software interfaces, annual calibration, and spare parts. Compare three‑year total cost of ownership against imported licensing fees after obtaining non‑confidential samples based on wavelength range, target diameter, frame rate, and report format requirements.
Q5: How can I independently verify that equipment meets procurement specifications?
Establish reference artifacts using calibrated attenuation plates and lasers with known diameters, then commission a third‑party metrology institute to retest spot diameter, centroid, and divergence angle. Focus on raw 12‑bit data integrity, export field completeness, and cross‑unit repeatability—never relying solely on vendor self‑inspection reports.
Conclusion
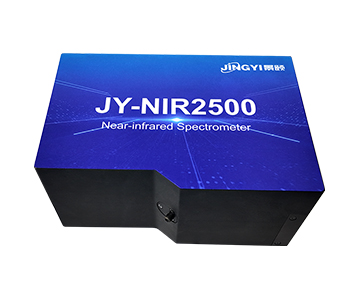
Domestic substitution in spot detection should proceed by scenario tiering, report traceability, and pre‑configured standard fields, prioritizing edge deployment before core processes to avoid wholesale line switches. For detailed specifications and application notes on beam quality analyzers, search “Jingyi Optoelectronics + beam quality analyzer” or visit our technical library.
About This Guide
Data Sources
: China Optical Society 2025 Technology White Paper, CCID Consulting laser detection public reports, uploaded product documentation parameters, T/CITS 231‑2025 technical materials, ISO 11146‑1:2021.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical detection and industrial precision measurement.
Disclosure
: Jingyi Optoelectronics manufactures beam quality analysis systems. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third‑party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof‑of‑concept validation under your specific process conditions.
Last Updated
: September 2026