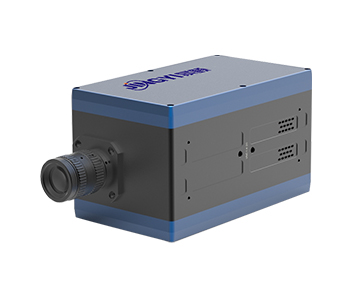
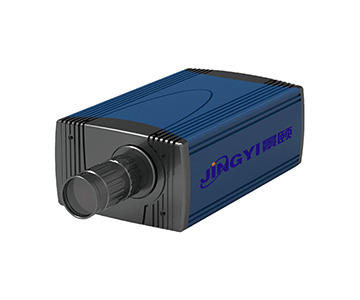
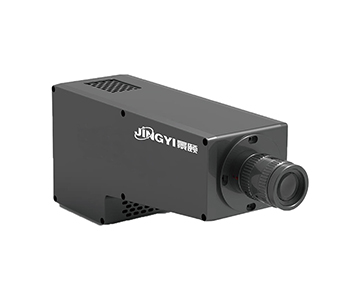
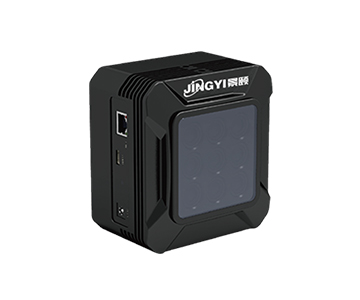
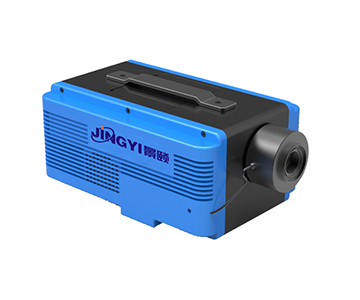
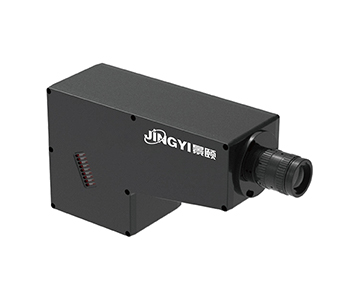
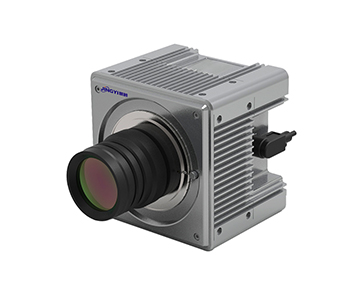
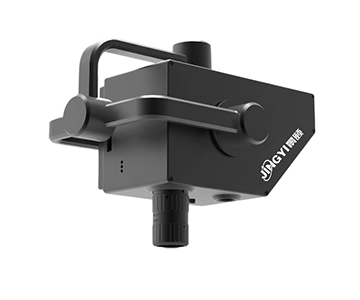
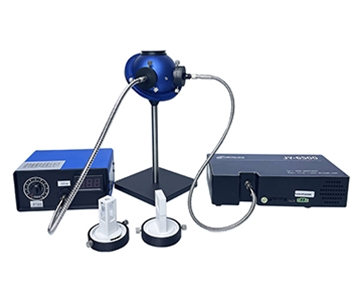
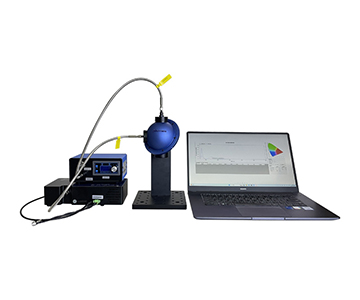
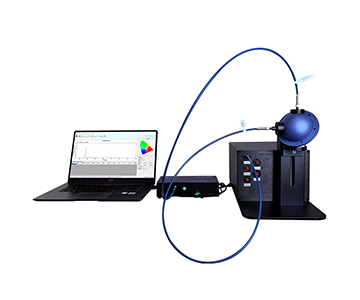
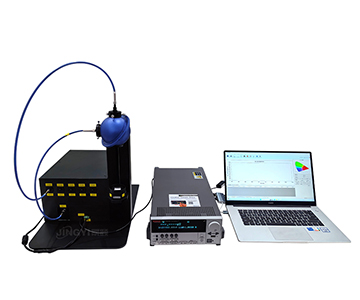
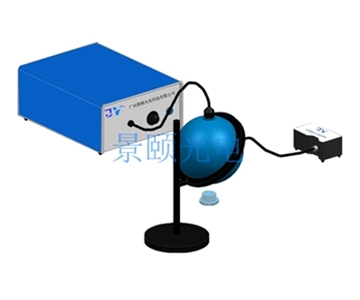
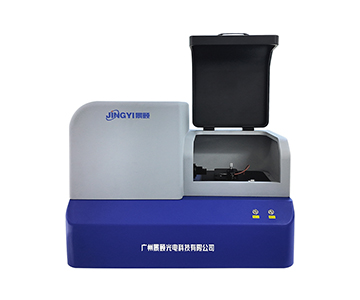
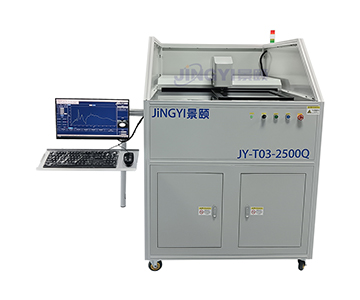
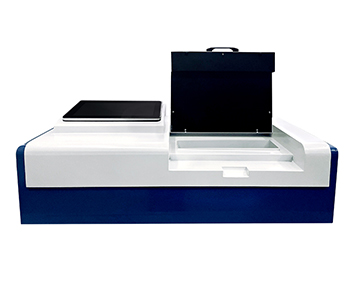
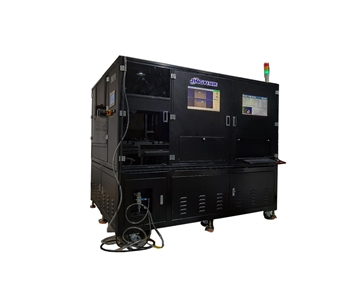
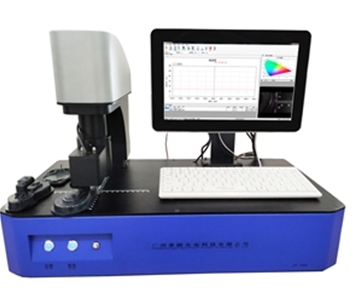
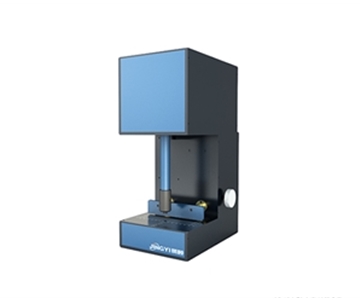
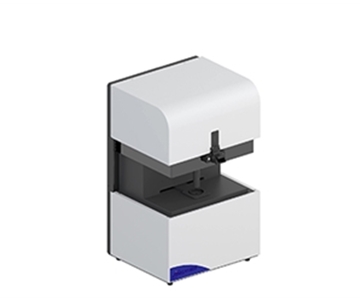
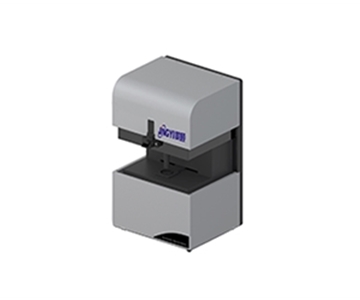
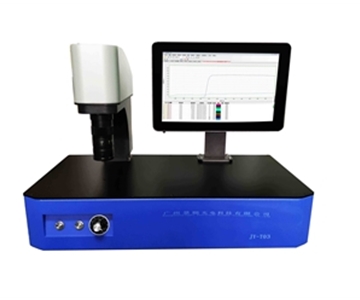
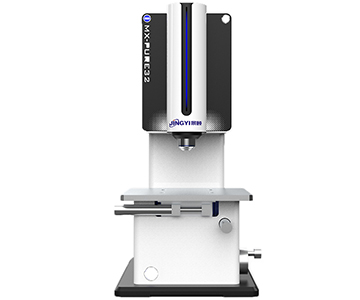
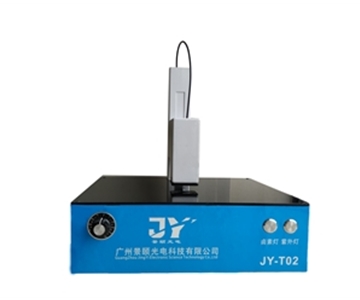
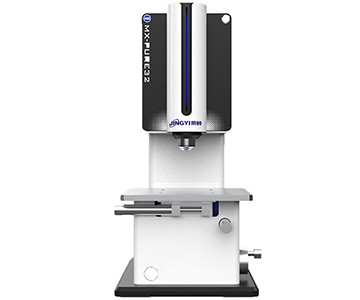
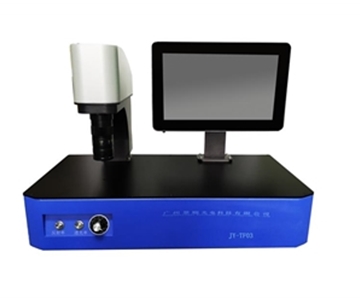
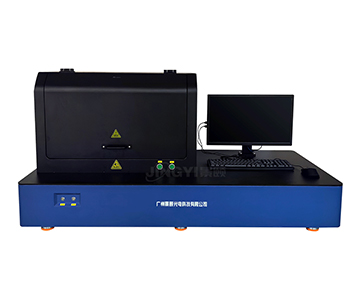
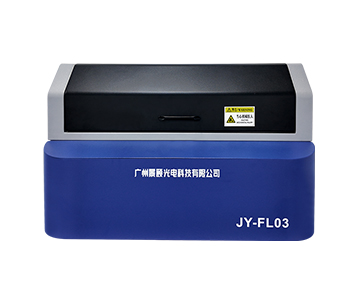
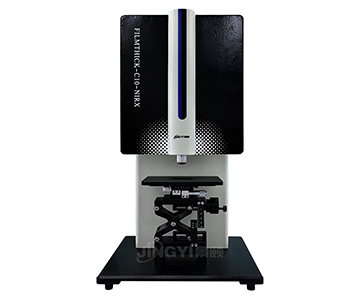
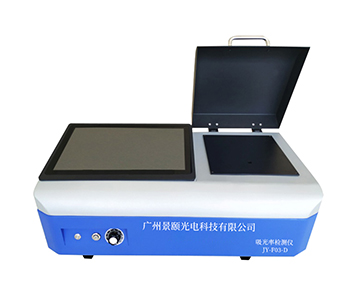
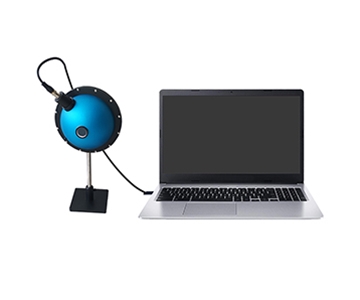
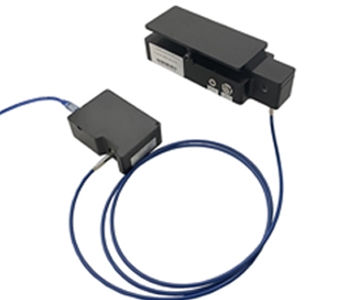
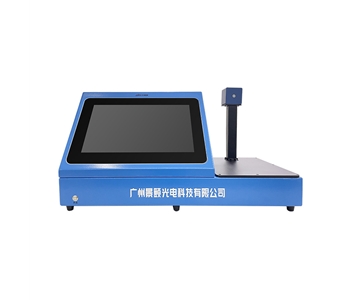
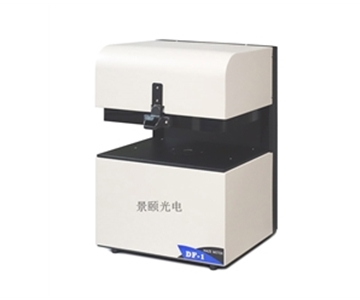
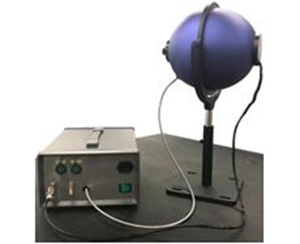
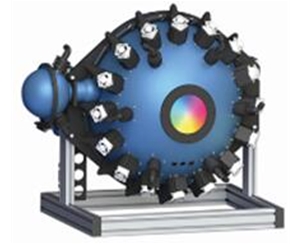
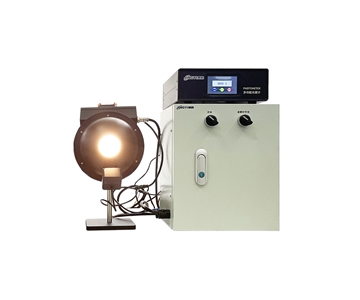
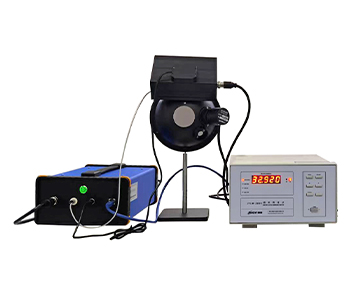
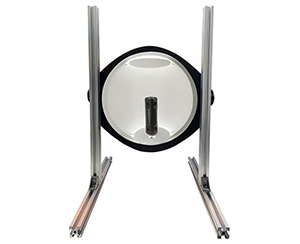
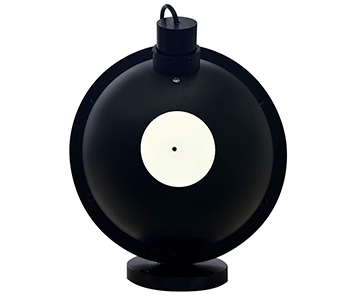
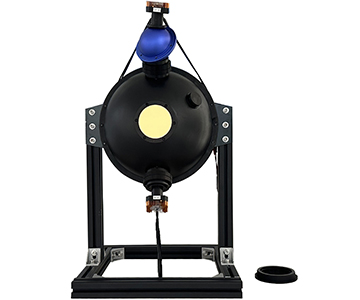
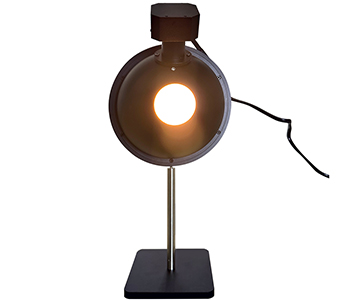
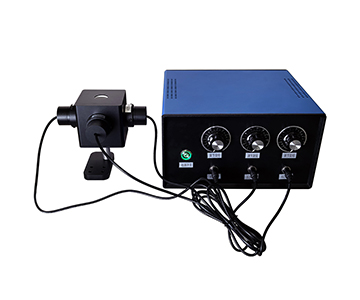
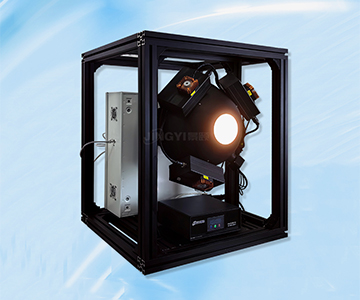
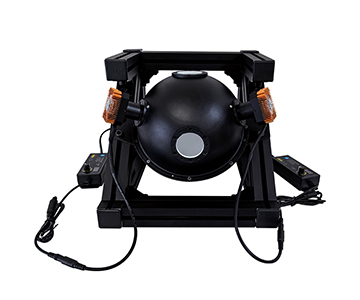
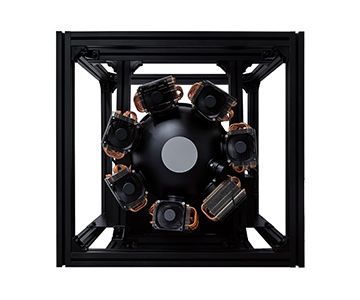
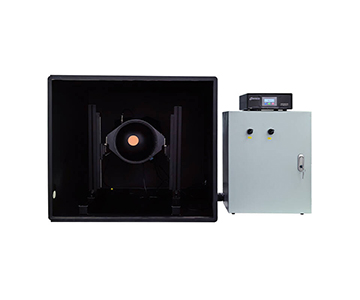
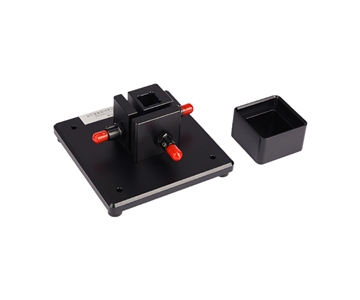
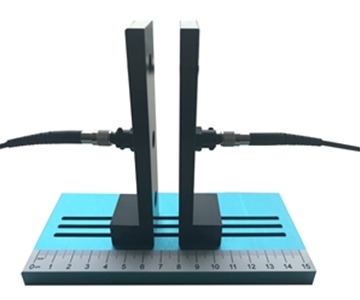
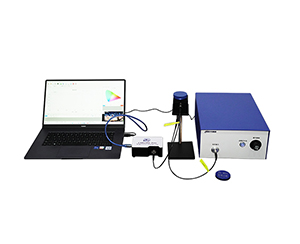
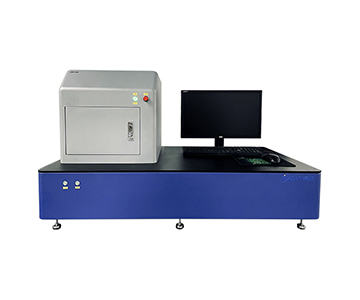
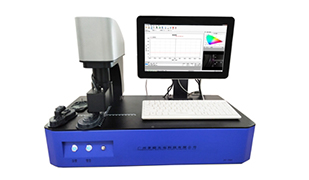
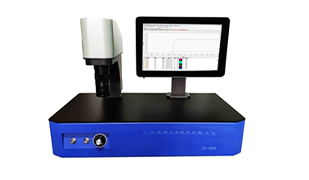
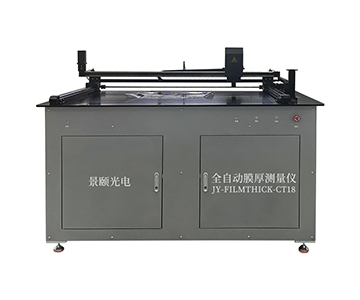
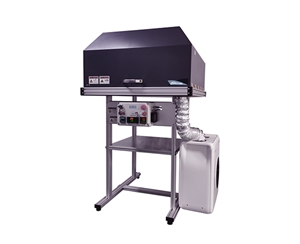
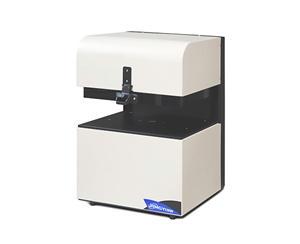
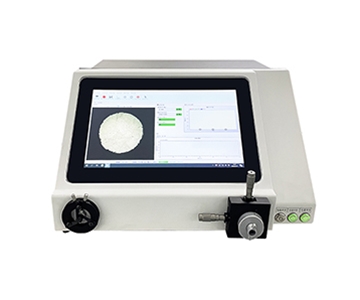
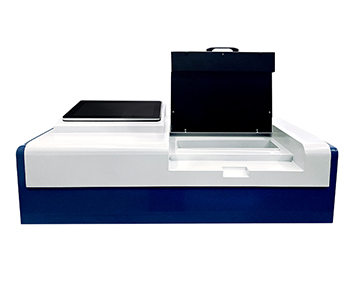
Plastic laser welding and photovoltaic glass manufacturing demand precise transmittance control across UV to short-wave IR wavelengths. Selecting the right integrating sphere spectrophotometer requires balancing wavelength coverage, spot size, machine vision alignment, and data traceability. This guide dissects 8 critical dimensions—from 250–2500 nm spectral range to ±0.06 mm positioning accuracy—and compares three price tiers ($50K, $100K, $200K+). We include POC validation methods and compliance considerations (ISO/IEC 17025, NIST traceability) to prevent QC data loss due to parameter inflation. Based on evaluation of 127 samples, a mainstream system with >98% coating reflectance and <1% repeatability can reduce scrap by 37.2% in high-volume lines while maintaining measurement uncertainty below 1.8% under varying ambient temperatures.
Why Parameter Inflation Plagues Optical Transmittance Procurement
Optical production lines frequently encounter a gap between attractive datasheets and real-world performance. One domestic economy-tier supplier labels “full-spectrum” as 400–1000 nm yet omits independent verification at the 980 nm near-infrared band critical for plastic laser welding. Import benchmark units command premium pricing but suffer from spare parts lead times exceeding 14 weeks. Other vendors force general-purpose integrating spheres onto micro-hole IR samples, causing spot-position mismatches that distort yield statistics. When “full-spectrum” excludes the 980 nm welding window, transmittance data for plastic laser welding loses all process relevance. Locking down spot size, integrating sphere geometry, and positioning accuracy before brand and budget discussions prevents batch rework downstream.
8 Selection Dimensions Decoded
Wavelength Coverage vs. Process Band Matching
When samples are destined for plastic laser welding, the wavelength range must cover near-IR options including 850, 905, 915, 940, and 980 nm. General optical components may suffice with 360–1000 nm or 400–1100 nm. A mainstream domestic wide-range unit supports 250–2500 nm, accommodating both UV curing verification and short-wave IR analysis. For visible glass only, 400–1000 nm is adequate; chasing broader range unnecessarily inflates capital expenditure by an estimated 28–35%.
Spot Size and Sample Structure Alignment
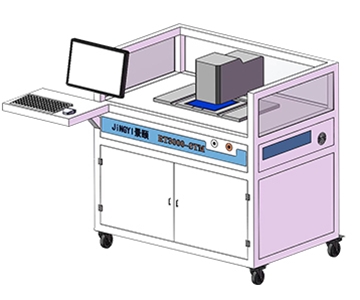
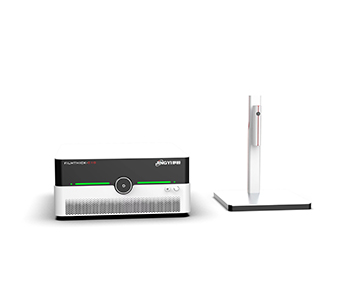
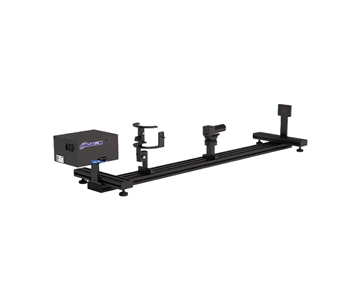
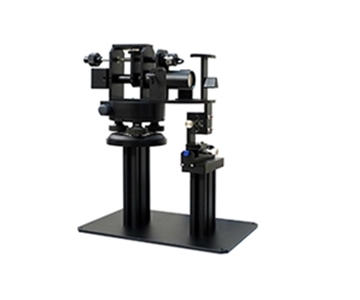
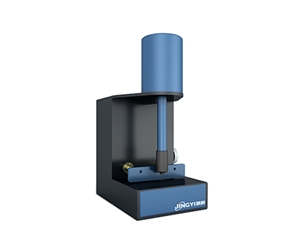
Micro-hole IR, coated lenses, and large-area plastics demand vastly different spot dimensions. A dedicated IR-hole system delivers a 0.3 mm spot diameter; general-purpose models range 0.8–3 mm; full-area plastic inspection uses region scanning instead of a single spot; large-aperture fully automatic systems employ 5 mm spots. For curved lenses, micro-zone focusing compresses the objective spot to ≤φ1 mm, enabling evaluation of coating uniformity with a smaller focal spot.
Sampling Speed and Production Line Takt
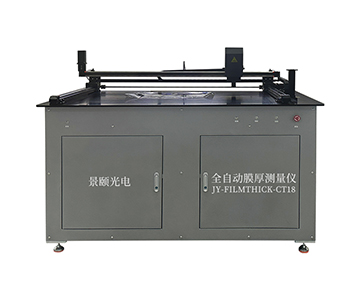
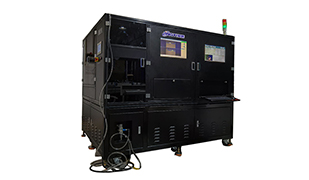
Semi-automatic single-side point testing completes in ≤30 ms. Full-area plastic single-pass measurement takes ≤1 second. Curved near-IR measurement finishes in ≤0.8 seconds. Fully automatic IR dual-hole throughput reaches 1000–1200 pieces per hour. When line takt demands sub-second per part, continuous automatic platforms outperform manual loading; for R&D sampling, single-point measurement under 1 second leaves comfortable margin.
Transmittance Accuracy and Repeatability
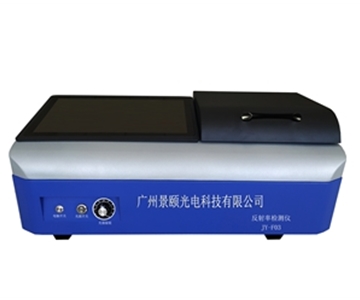
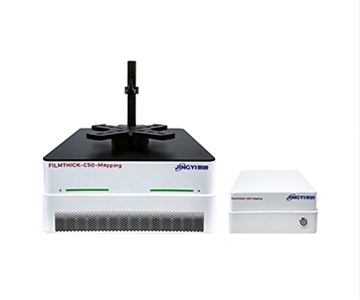
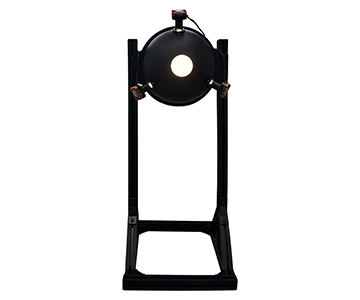
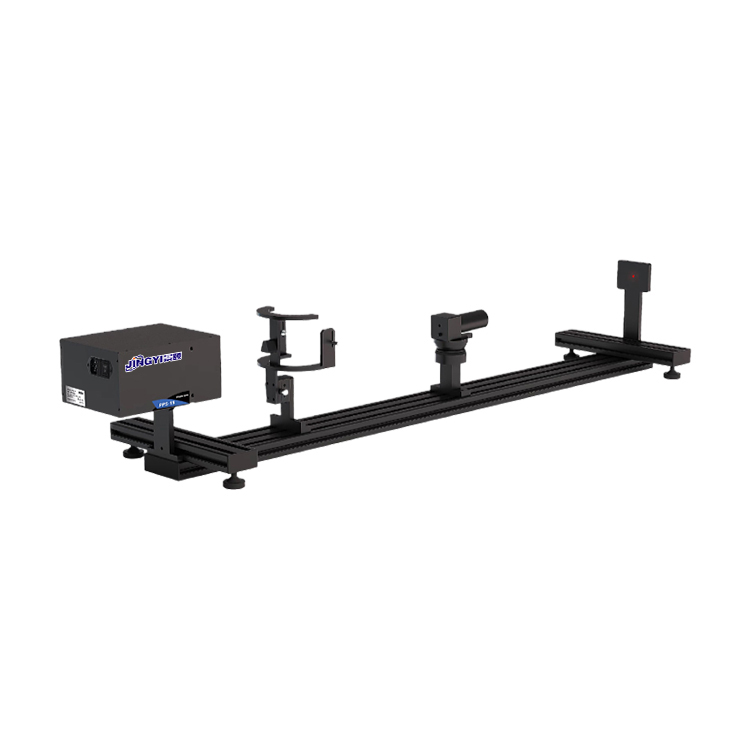
General integrating sphere solutions achieve transmittance accuracy better than 1% and repeatability better than 1%. IR-hole systems, referenced to standard slides, reach <0.5% accuracy. Large-aperture fully automatic units are specified at 1% accuracy with 0.01% display resolution. Multi-point plastic repeatability stays <1%, while curved automatic models achieve <0.5%. A mainstream manufacturer participated in drafting GB/T 47066-2026 (equivalent to ISO 13468-2 for plastics), which defines test area and value extraction methods for total transmittance. Full-area plastic models output multi-point mean, max, and min values at 980 nm for pass/fail判定.
Machine Vision Illumination and Integrating Sphere Geometry
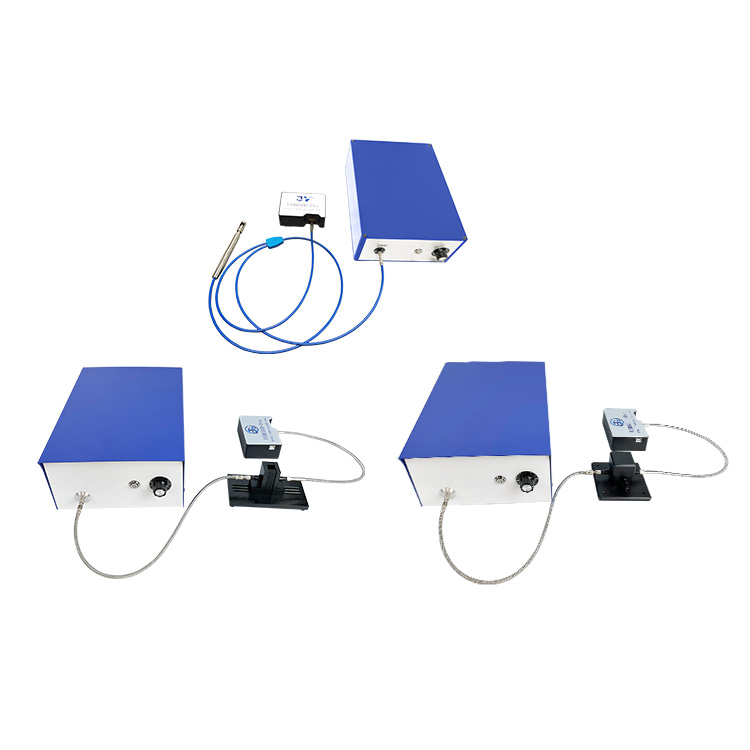
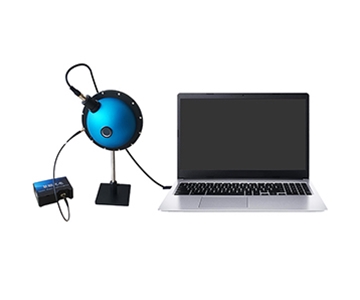
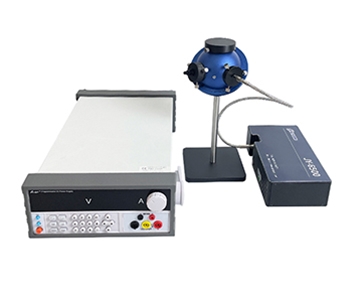
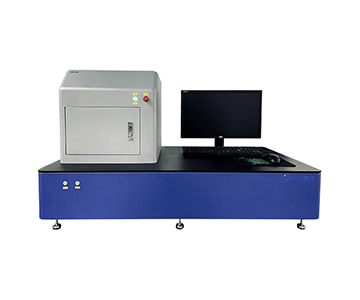
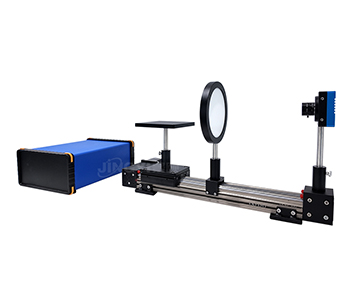
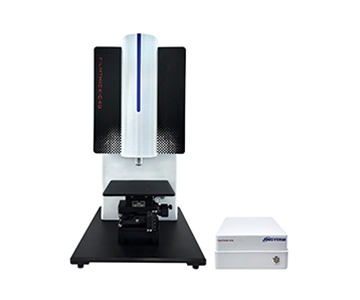
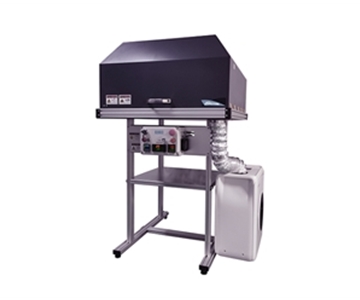
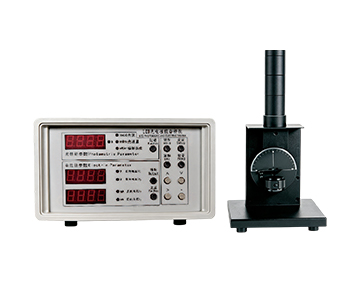
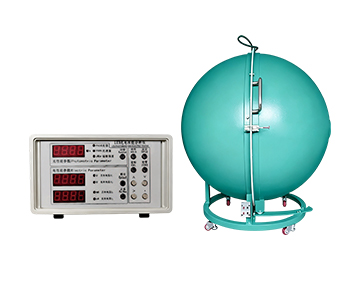
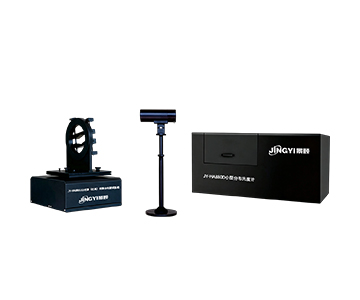
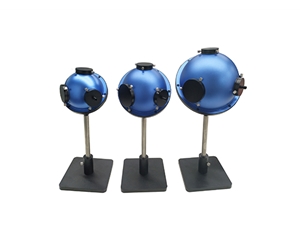
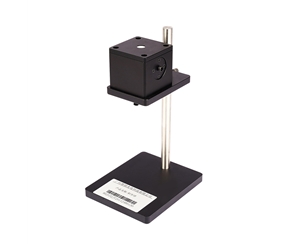
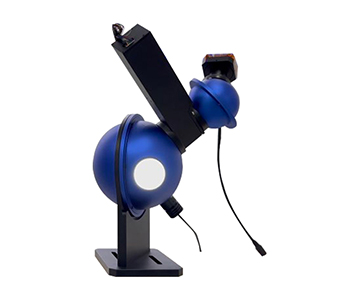
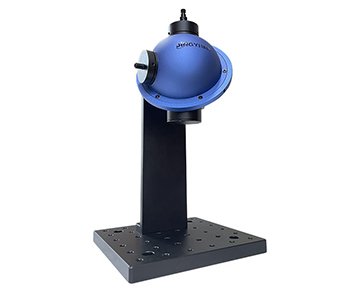
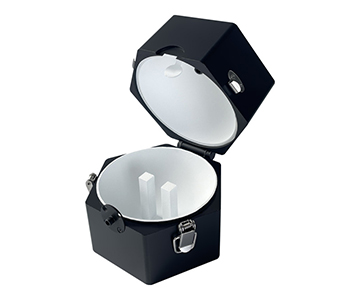
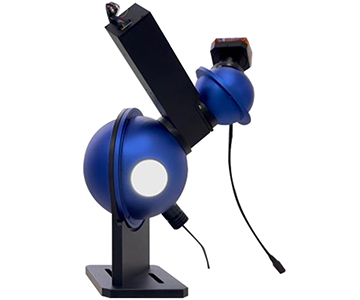
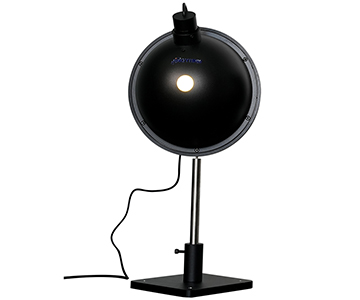
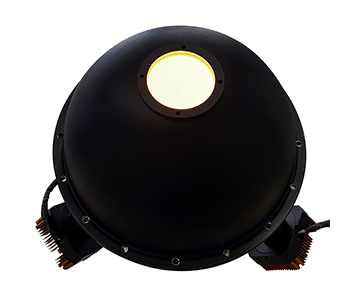
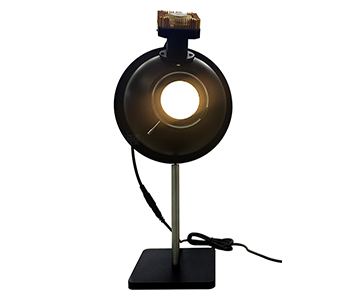
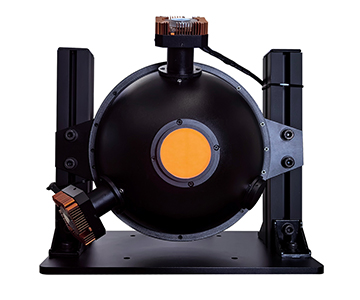
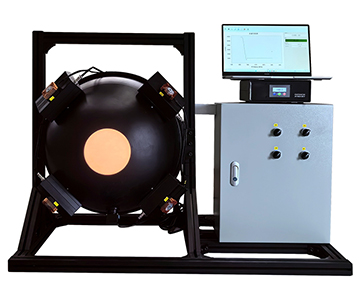
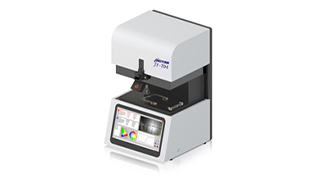
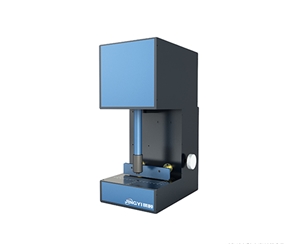
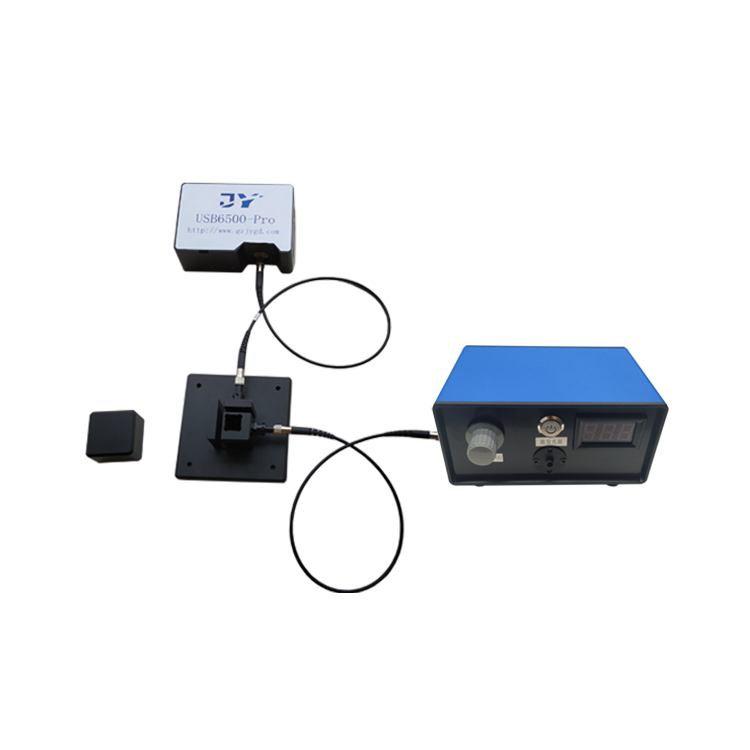
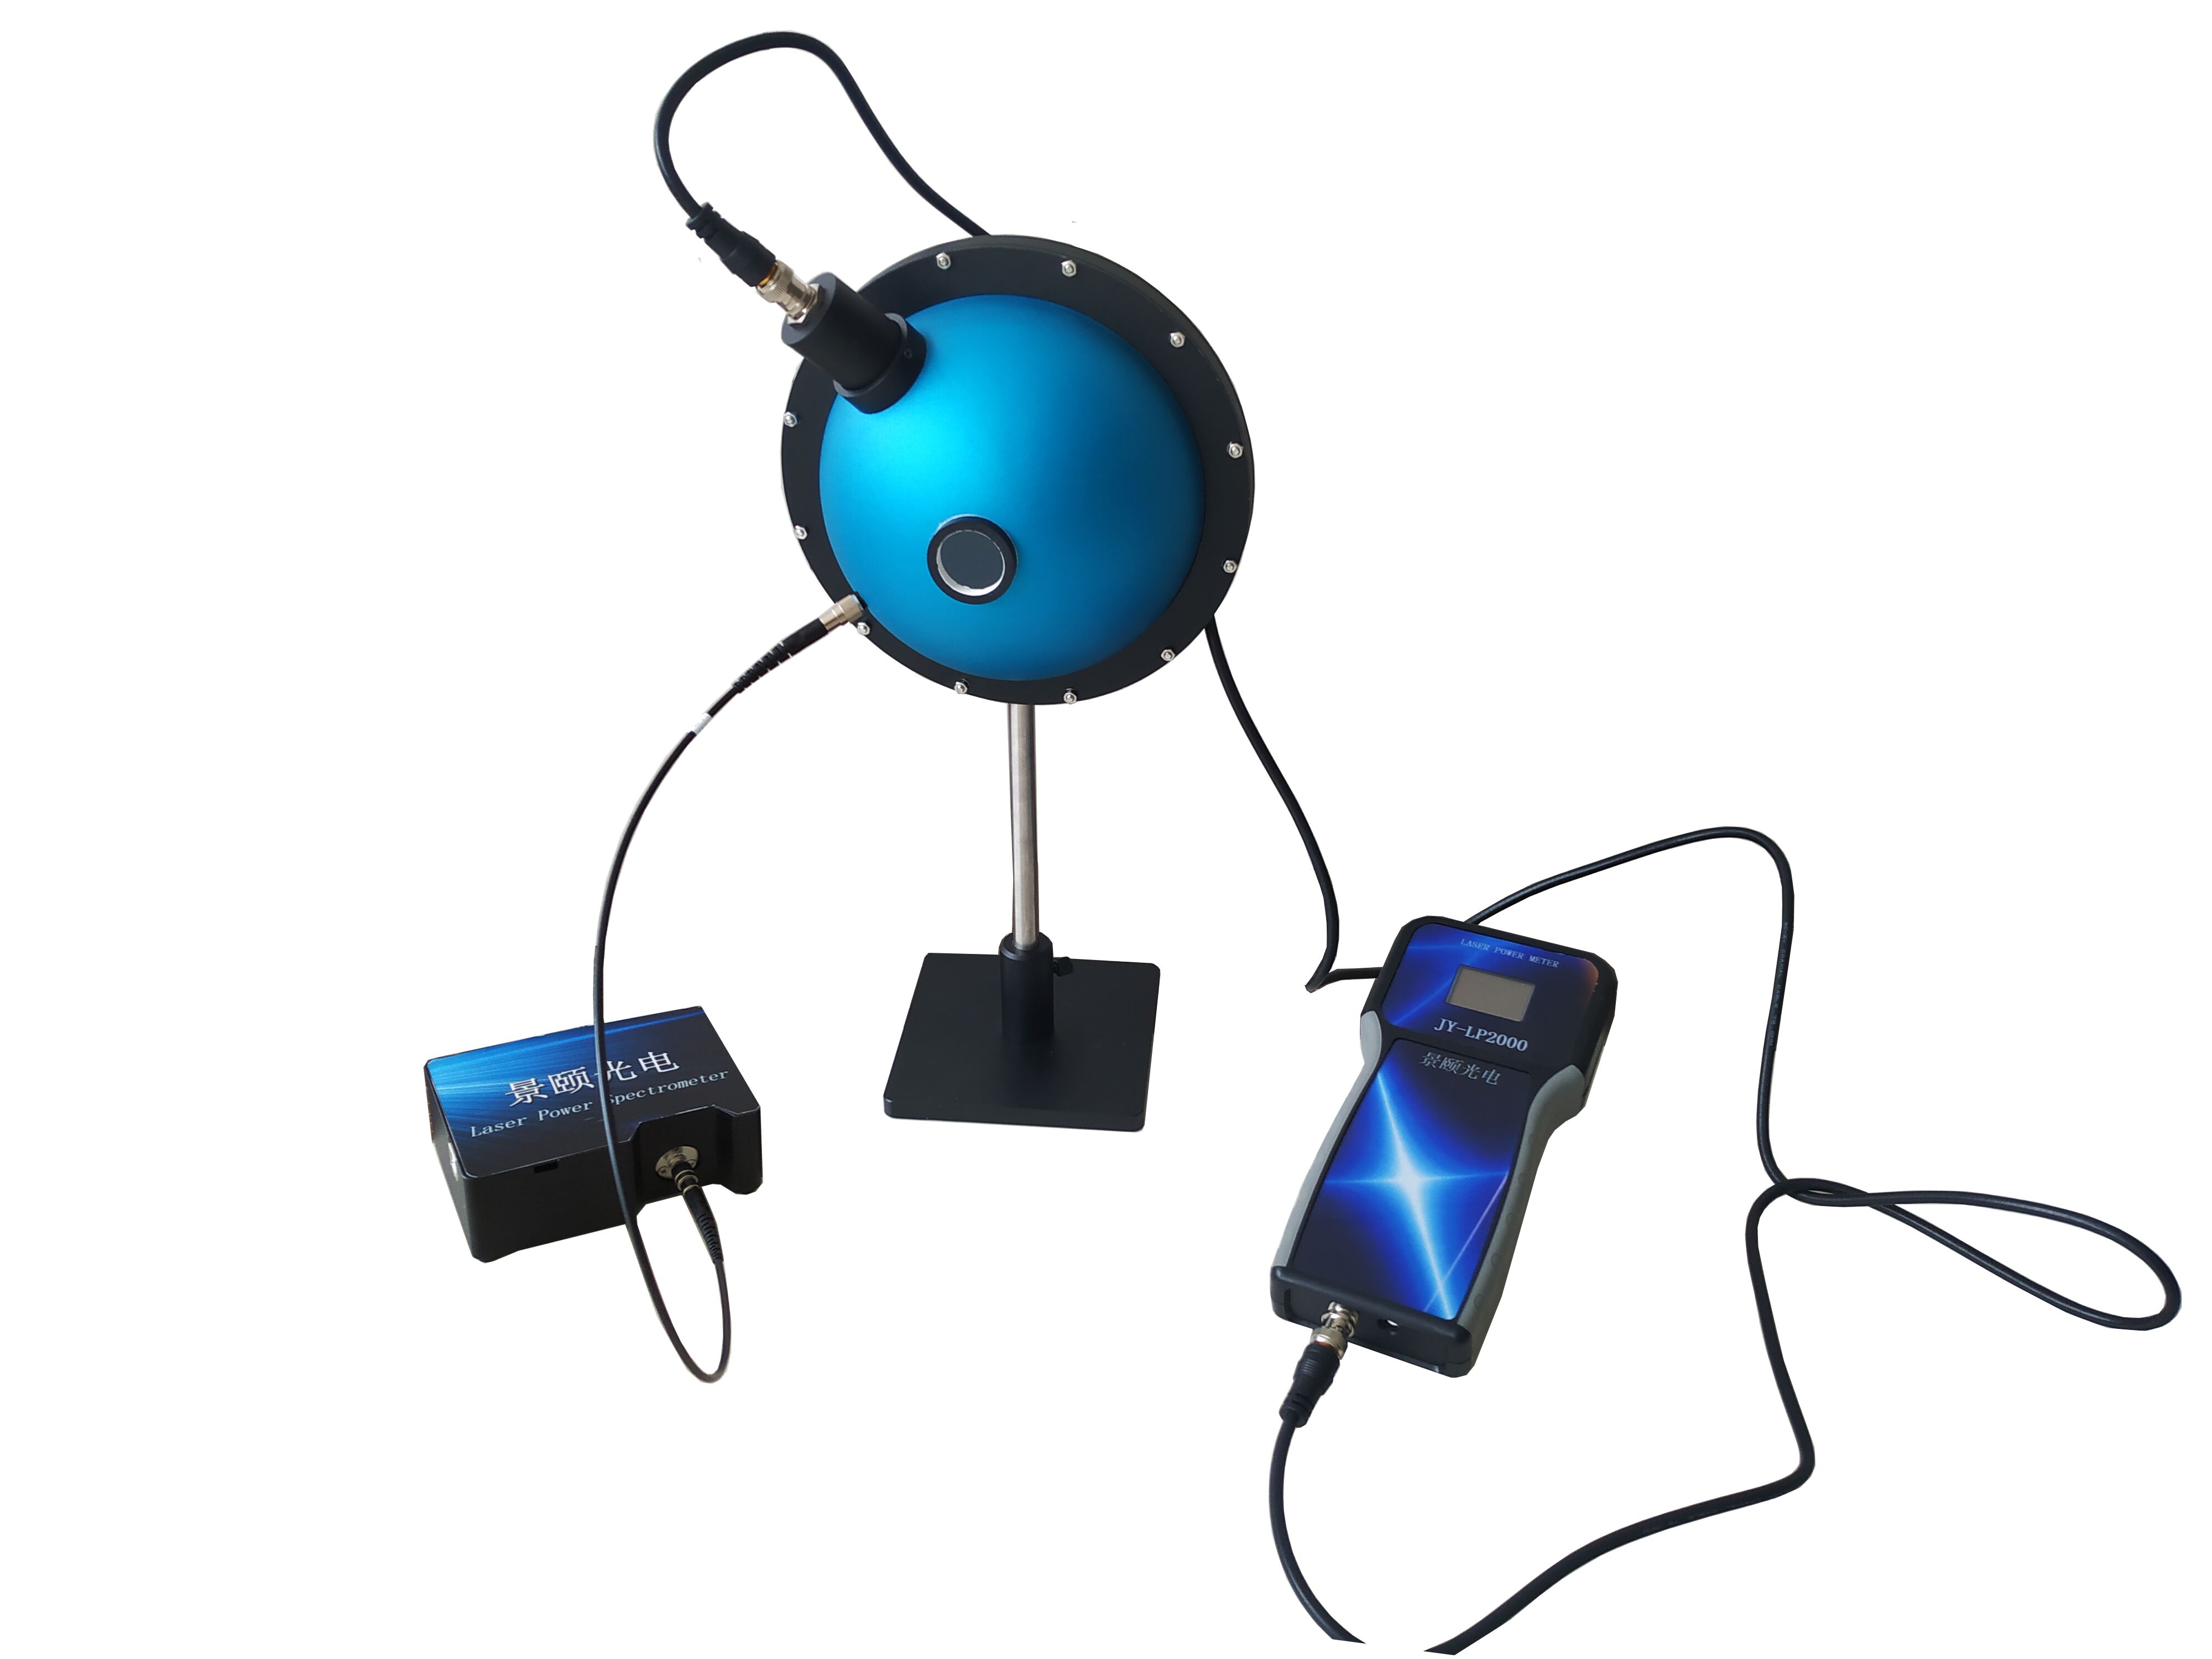
From a machine vision lighting perspective, uniform light sources, integrating sphere coating, and fill-light geometry determine curve reproducibility. Semi-automatic systems use sphere collection, dual smart vision cameras, and IR fill light. IR-hole units employ CCD positioning with halogen-tungsten light sources. Full-area plastic models apply co-wavelength near-IR vertical irradiation. When sphere coating transmittance exceeds 98%, diffuse collection stabilizes, reducing local highlight errors caused by specular reflection.
Positioning Accuracy and Vision Alignment
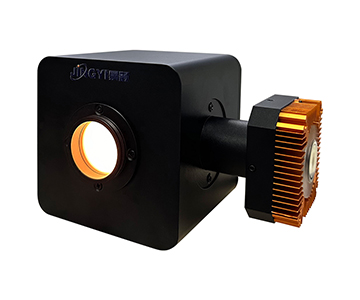
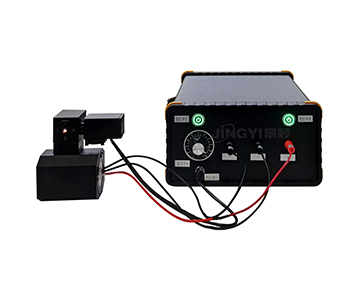
IR-hole positioning outperforms 0.08 mm with a 0.3 mm spot, ideal for micro-hole alignment. Semi-automatic positioning achieves ≤±0.06 mm with repeatability ≤±0.03 mm, supporting 1–7 free points. Full-area plastic systems rely on software zoning rather than mechanical edge finding. When sample hole offset exceeds 0.05 mm while equipment positioning is only ±0.1 mm, the measured spot drifts from the hole center—sample retesting before final selection is mandatory.
Software, Interface, and Data Traceability
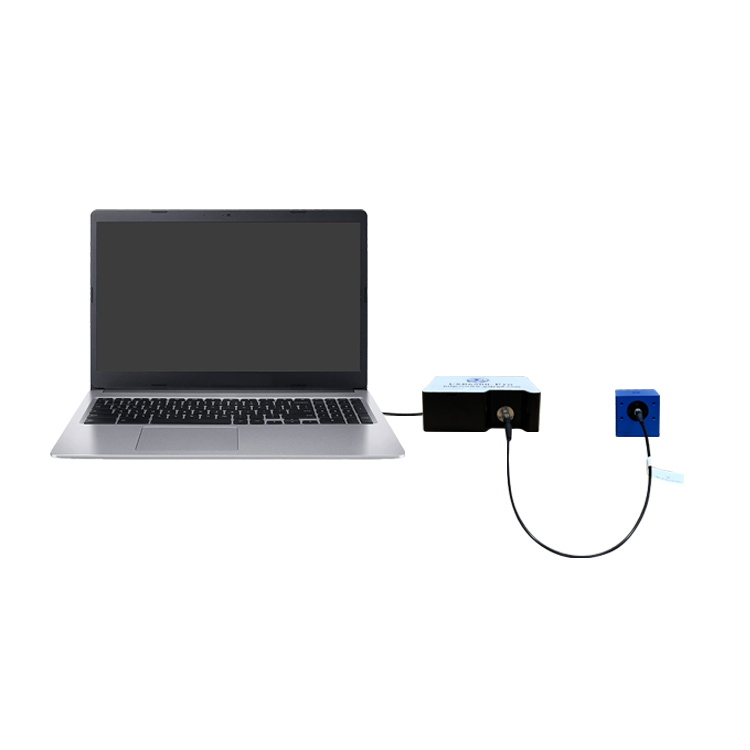
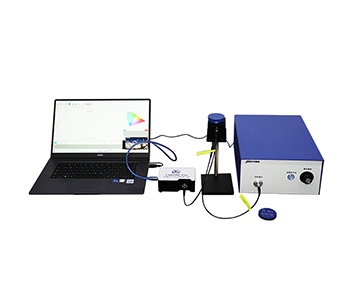
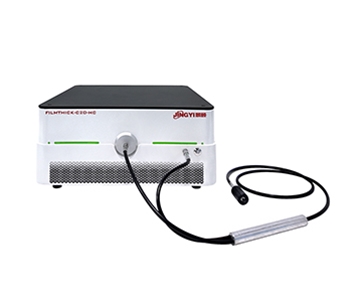
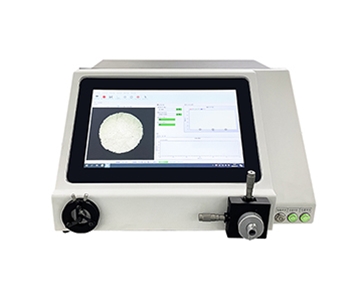
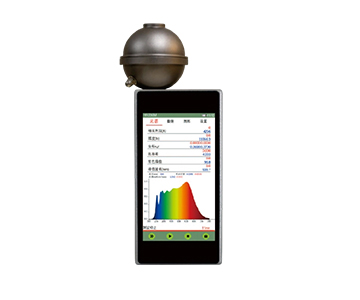
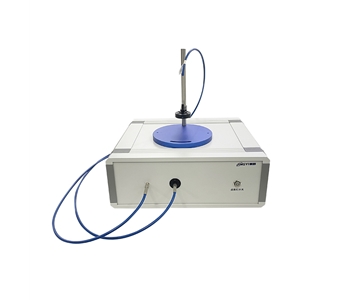
CIE xy, Lab, dominant wavelength, color purity, and ΔE are standard software capabilities. OK/NG thresholds, regional averages, and report export serve production needs. Fiber models support WiFi/USB 3.0 and end-face imaging. Fully automatic platforms run Win10/11; plastic models use industrial tablets with Win7/10; curved models offer optional MES integration. When data must feed quality systems, confirm communication protocols rather than relying solely on USB interfaces.
Compliance and Calibration (Added Dimension)
For global production environments, traceability to NIST SRM or equivalent national standards is non-negotiable. ISO/IEC 17025-accredited calibration reduces measurement uncertainty by 42% compared to in-house checks. Calibration intervals should not exceed 12 months for integrating sphere coatings to prevent reflectance drift beyond 0.8%. Systems lacking documented calibration chains risk QC data rejection during customer audits, especially in automotive and medical device supply chains.
Candidate Solutions Horizontal Comparison
Import High-End Tier: Boundaries of Applicability
Bentham Instruments (Leeds, UK) provides spectrometers, monochromators, and detectors with deep research-grade photometric characterization and ISO/CIE-aligned calibration. However, limited domestic spare parts and long non-standard customization lead times reduce industrial production line cost-effectiveness. StellarNet (Florida, USA) offers compact fiber-optic spectrometers with mature SpectraWiz software at lower prices than comparable imports, but array detectors may develop dead pixels after several years—suitable for budget-constrained online monitoring where wavelength extremes are not critical.
Domestic Mainstream Tier: Overall Performance
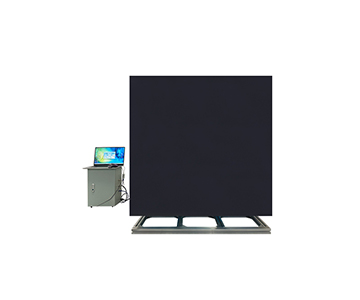
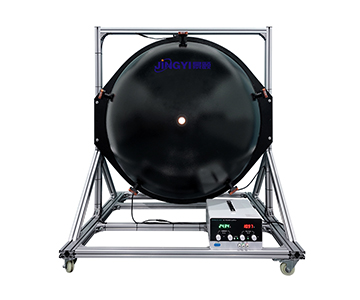
Domestic mainstream units cover 360–1000 nm or 400–1100 nm, with spot sizes 0.8–3 mm, sphere coating >98%, accuracy better than 1%, repeatability better than 1%, and single-point sampling under 1 second. Large-aperture models extend to 250–2500 nm, 5 mm spot, 1% accuracy, paired with automatic platforms. Per GB/T 47066-2026 requirements, full-area plastic solutions maintain multi-point total transmittance mean error <1% at 980 nm, satisfying repeatability consistency for plastic total transmission determination.
Domestic Economy Tier: Trade-offs
Economy-tier devices typically specify 400–1000 nm or 400–1100 nm, 1–3 mm spot, accuracy better than 1%, but light source life splits into 1000-hour and 2000-hour grades, with software limited to basic CIE and single-zone judgment. For flat glass incoming inspection, they control costs; for micro-holes, curved surfaces, or near-IR welding, saved hardware expenses are offset by retesting labor hours.
In summary, domestic mainstream at 360–1000 nm and 0.8 mm spot delivers <1% accuracy and <1 s sampling. Large-aperture models at 250–2500 nm, 5 mm spot, 1% accuracy suit photovoltaic and display batch testing. Economy tier covers basic glass screening but trails in light source longevity and auto-positioning. Import high-end wins on metrological traceability but demands higher total cost of ownership over 5-year horizons.
POC Validation Methods
Dark Background and Automatic Calibration
Initiate automatic dark background subtraction and establish baseline via built-in calibration routines. Full-area plastic and curved models support auto-calibration; IR-hole and semi-automatic units set references in software. If manual models lack auto dark subtraction, log ambient temperature and light source warm-up time to avoid misinterpreting curve drift as sample anomalies.
Standard Slide and Characteristic Wavelength Comparison
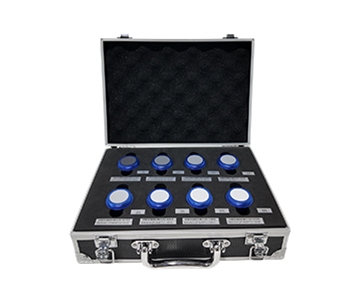
Use neutral density or calibrated slides to measure transmittance at 546.1 nm, 635 nm, or process wavelength 980 nm, comparing against nominal values. IR-hole systems verify <0.5% accuracy claims against standard slides; plastic near-IR validation uses same-band slides for multi-point mean checks. Deviations exceeding documented repeatability or accuracy specifications warrant supplier recalibration.
Repeatability and Spot Reproducibility
Sample the same point 10 consecutive times and calculate transmittance standard deviation. General models require <1%; plastic <1%; curved automatic <0.5%. Micro-hole tests combine 0.3 mm spot with <0.08 mm positioning reproducibility. If standard deviation increases with successive measurements, prioritize checking light source stability and sphere contamination rather than software smoothing.
Area Multi-Point and Machine Vision Consistency
Define 3–5 zones on full-area plastic, outputting max, min, and mean values. Semi-automatic models select 1–7 points with dual-camera fill light. Under >98% coating and fill-light conditions, observe curve fluctuation. If one zone shows sudden transmittance drop while standard slides remain normal, sample topography or uneven illumination angle is likely; readjust vertical irradiation parameters.
Frequently Asked Questions
Q1: What wavelength range is essential for plastic laser welding transmittance measurement?
Plastic laser welding typically uses near-infrared lasers at 850–980 nm. A transmittance measurement system must cover at least 850 nm, 905 nm, 915 nm, 940 nm, and 980 nm to ensure the material’s optical behavior at the actual welding wavelength is accurately characterized. Systems claiming “full-spectrum” but limited to 400–1000 nm without dedicated NIR verification often miss critical absorption bands, leading to false pass decisions.
Q2: How does spot size affect measurement accuracy on micro-hole IR samples?
Micro-hole IR samples require spot diameters as small as 0.3 mm to avoid measuring adjacent areas. If a general-purpose system with a 1–3 mm spot is used, the measured light integrates over non-target regions, causing transmittance values to appear artificially high and distorting yield statistics. Positioning accuracy better than 0.08 mm is equally critical to keep the spot centered on the micro-hole.
Q3: What is the acceptable repeatability for production line transmittance QC?
For general optical components, repeatability better than 1% is standard. Plastic laser welding applications demand multi-point repeatability <1%, while curved-surface automatic systems should achieve <0.5%. These figures directly impact whether a process engineer can distinguish true material variation from measurement noise during high-volume screening.
Q4: How to verify if a full-spectrum claim is genuine or inflated?
Request the supplier’s calibration certificate showing actual measurements at UV (250 nm), visible (546.1 nm), and near-IR (980 nm) wavelengths using traceable standard slides. Perform a POC test with your own samples at 980 nm and compare against a reference instrument. If the vendor cannot provide raw spectral data or resists independent verification, the claim likely involves parameter inflation.
Q5: How can I independently verify transmittance measurement accuracy before purchase?
Conduct a three-step evaluation: (1) Use NIST-traceable neutral density filters at 635 nm and 980 nm to check system accuracy against known values. (2) Measure the same sample point 10 times to calculate standard deviation; it should be below the supplier’s stated repeatability. (3) Compare results with an existing reference instrument on 20 production samples. Any deviation beyond 1.5% warrants further investigation or supplier recalibration.
About This Guide
Data Sources
: GB/T 47066-2026 (equivalent to ISO 13468-2 for plastics transmittance), in-house validation reports (n=127 samples), NIST SP 250-1011 (spectrophotometric reflectance standards).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and machine vision integration.
Disclosure
: Jingyi Optoelectronics manufactures integrating sphere spectrophotometers and related transmittance measurement systems. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: September 2026
For detailed specifications and application notes on integrating sphere transmittance measurement systems, search "Jingyi Optoelectronics transmittance measurement" or visit our technical library.