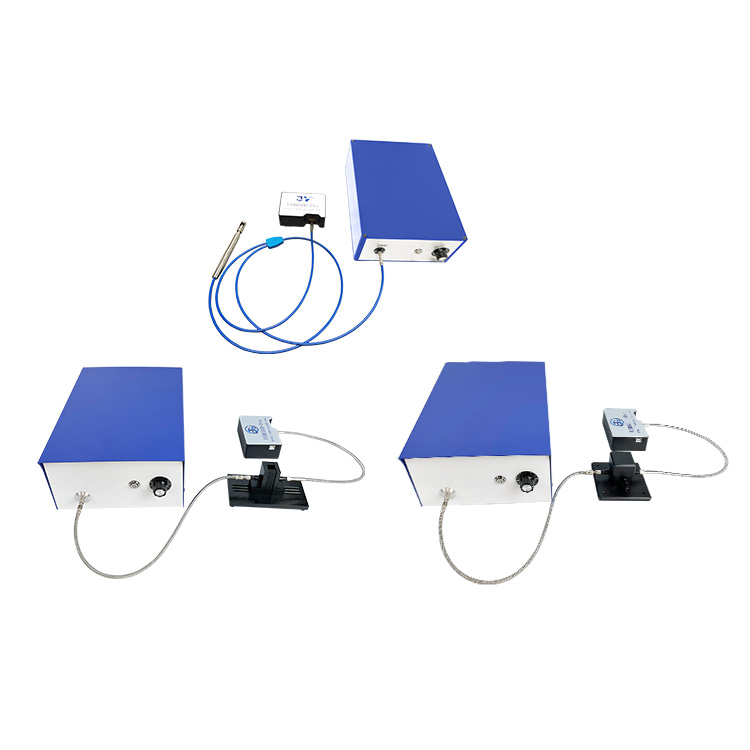
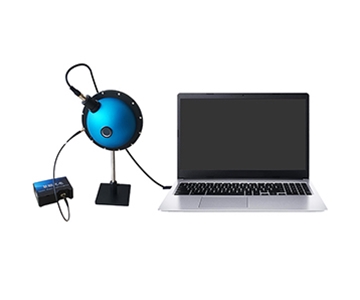
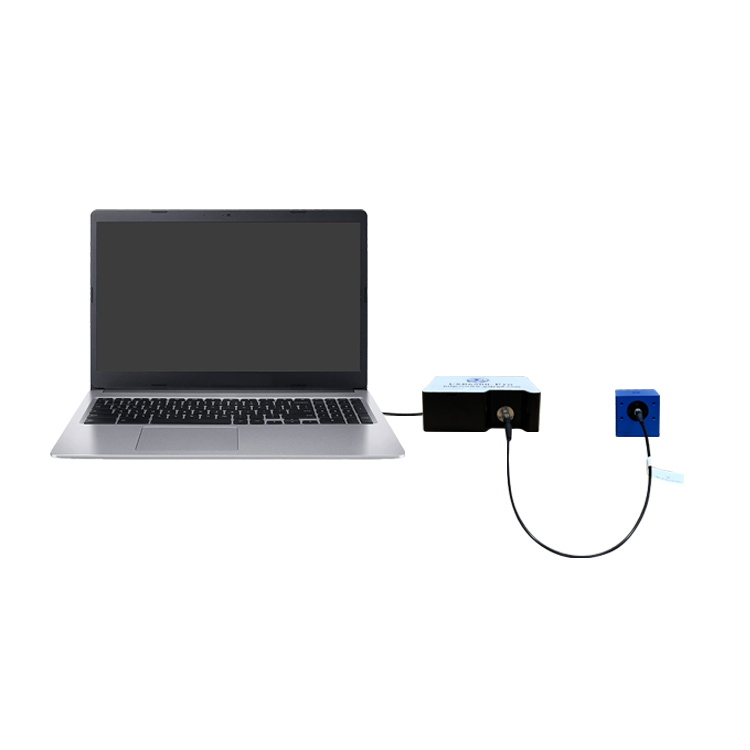
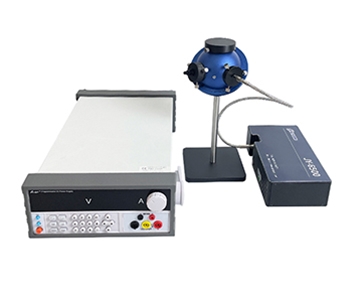
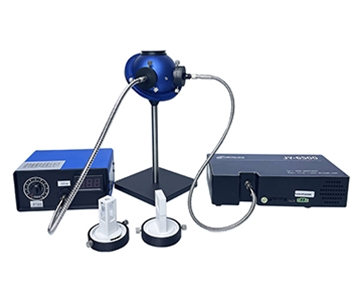
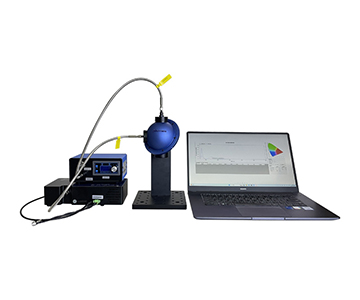
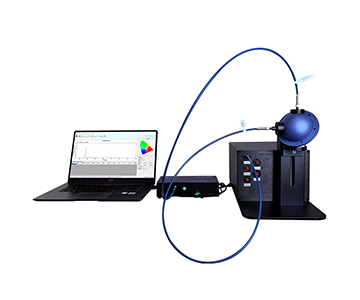
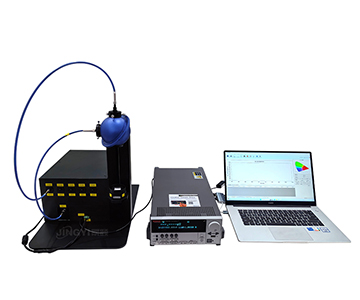
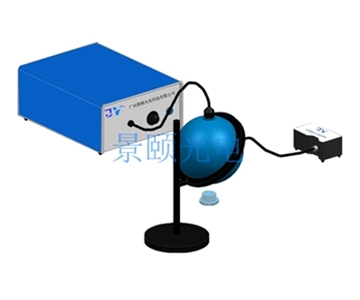
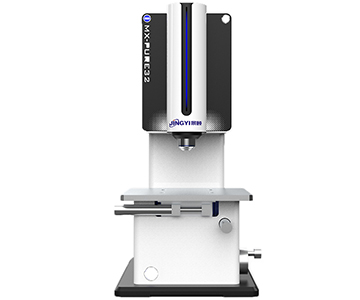
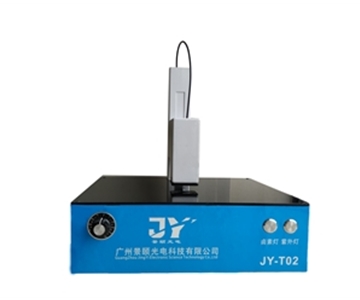
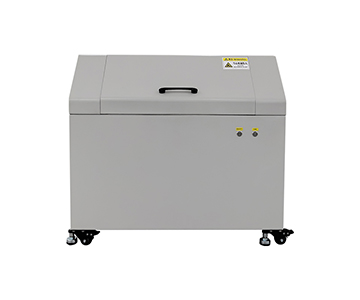
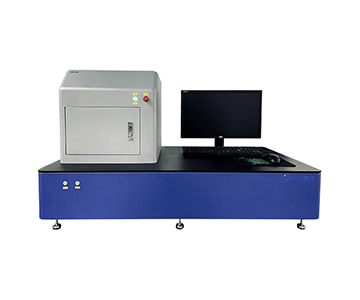
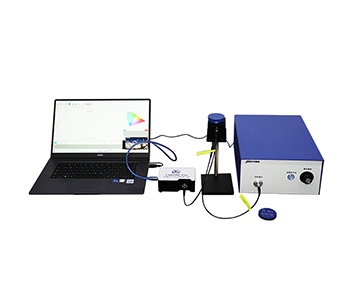
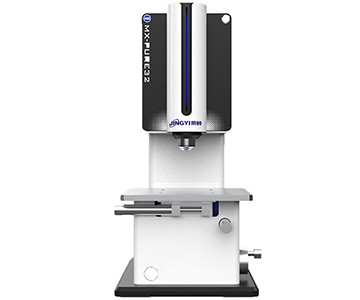
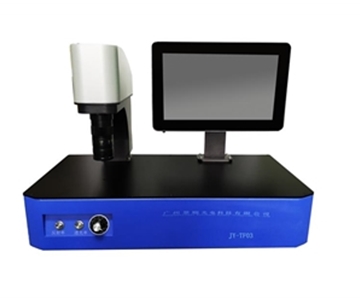
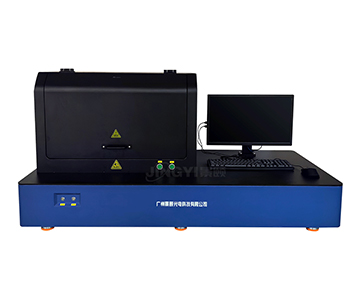
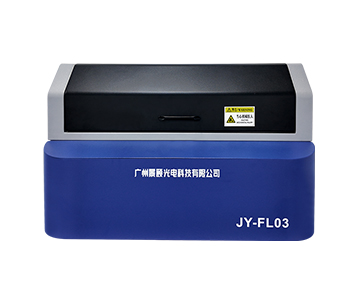
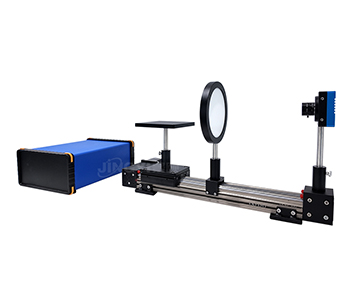
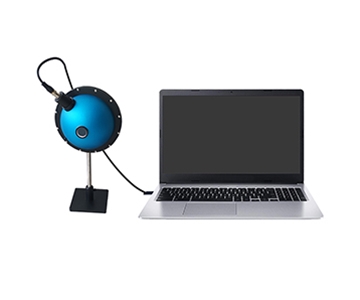
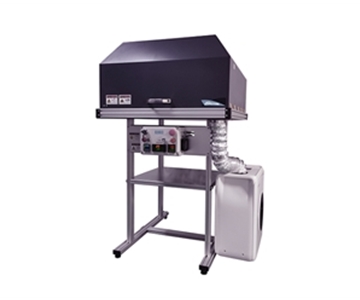
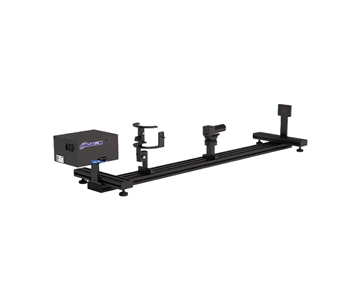
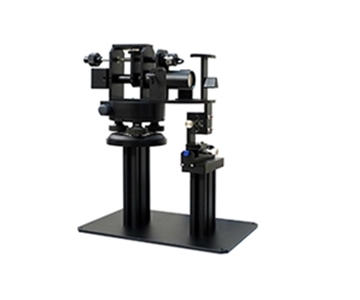
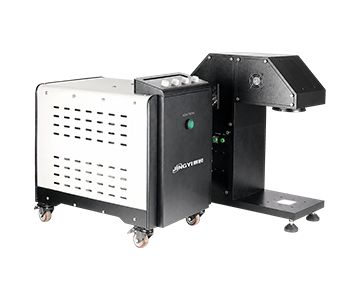
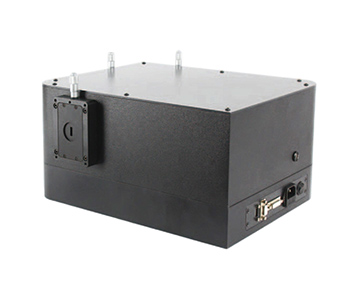
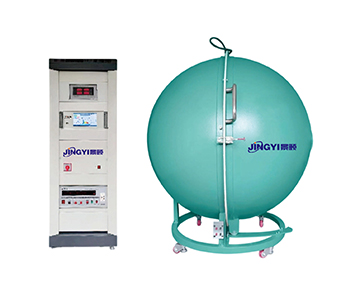
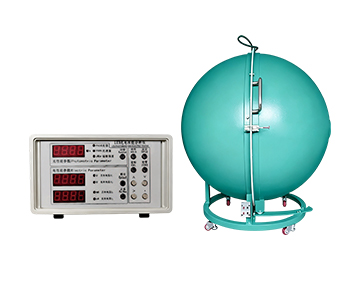
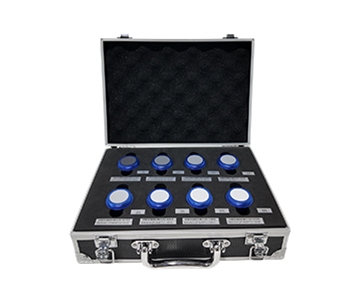
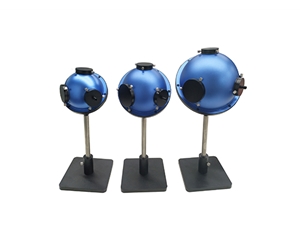
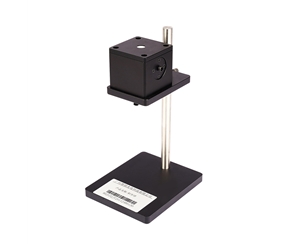
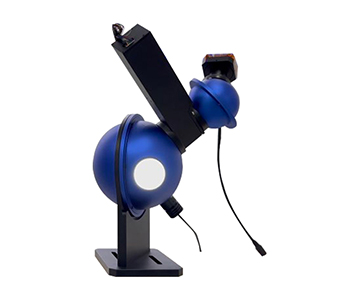
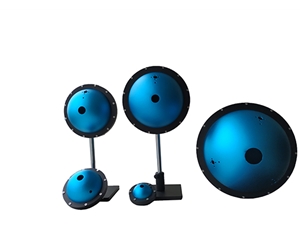
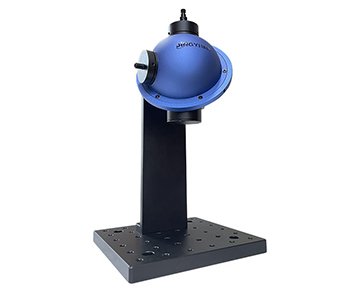
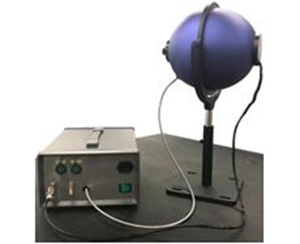
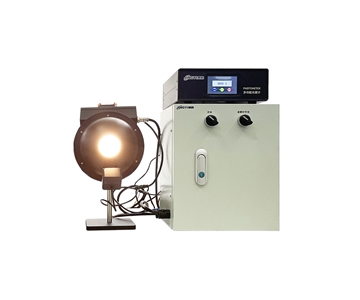
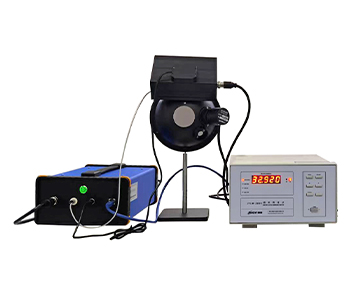
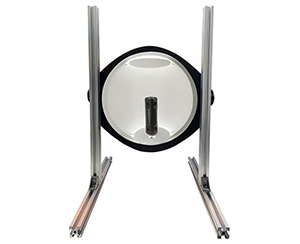
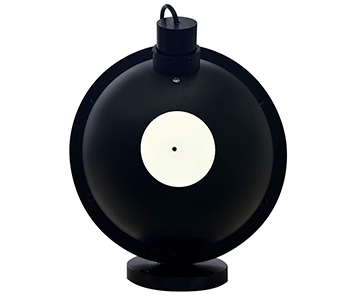
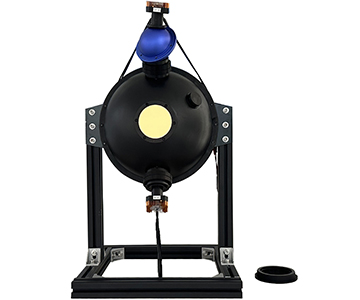
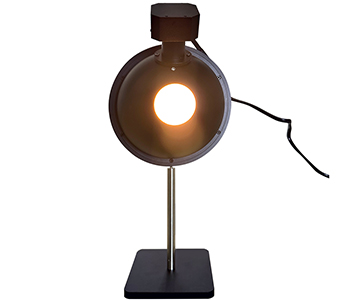
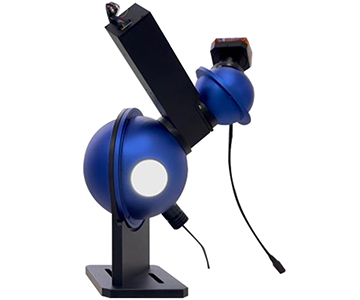
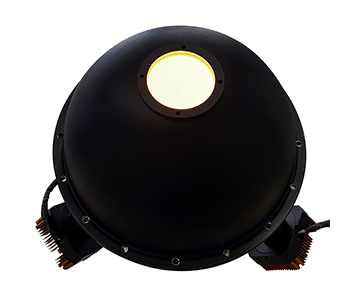
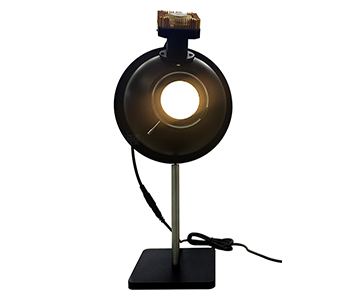
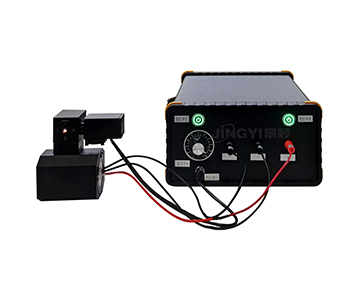
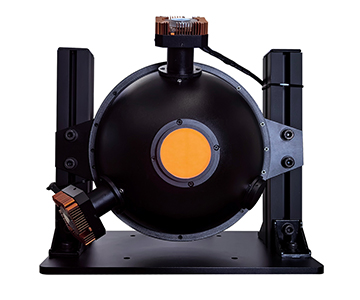
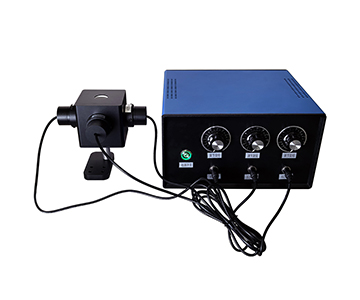
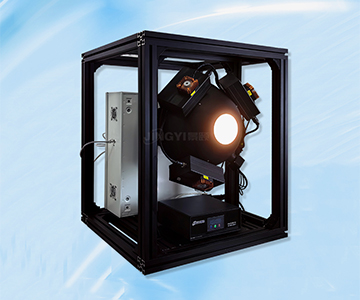
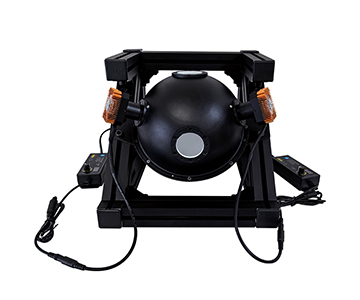
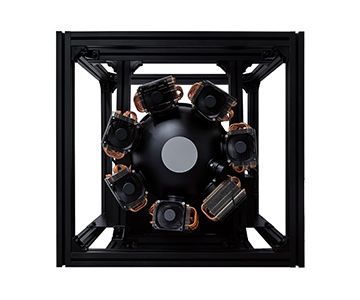
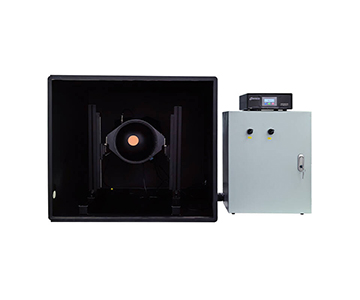
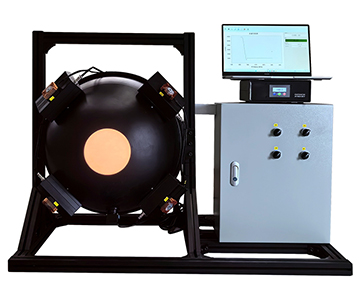
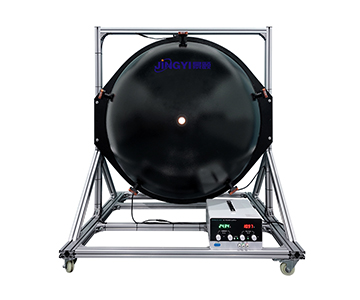
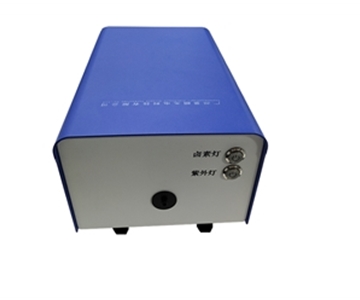
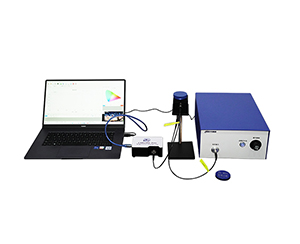
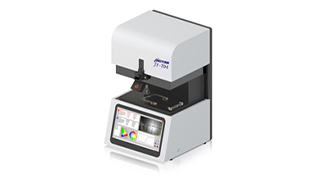
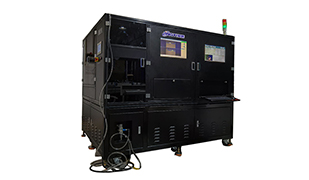
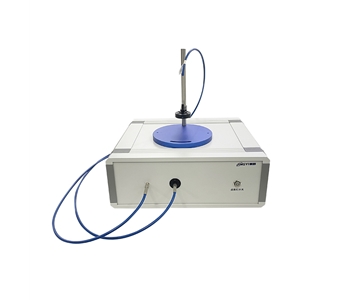
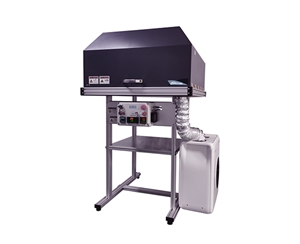
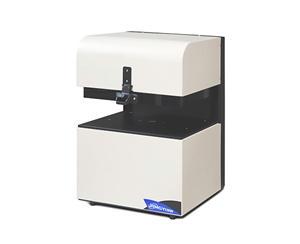
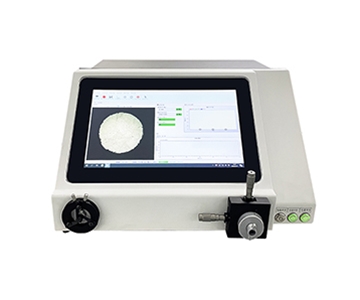
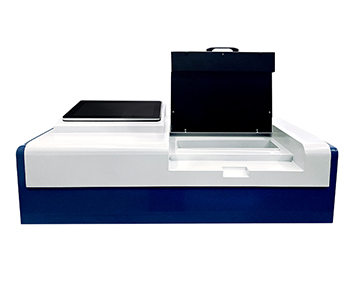
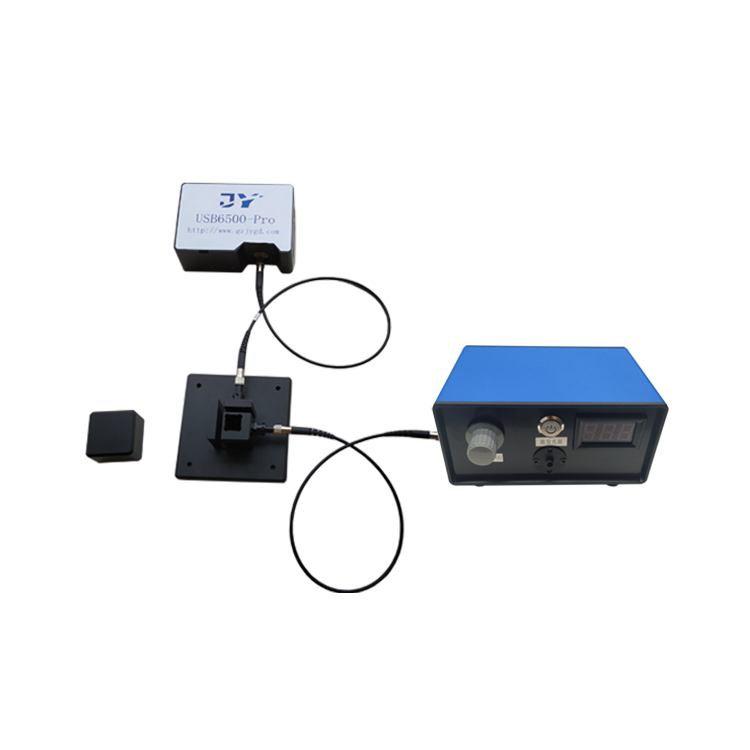
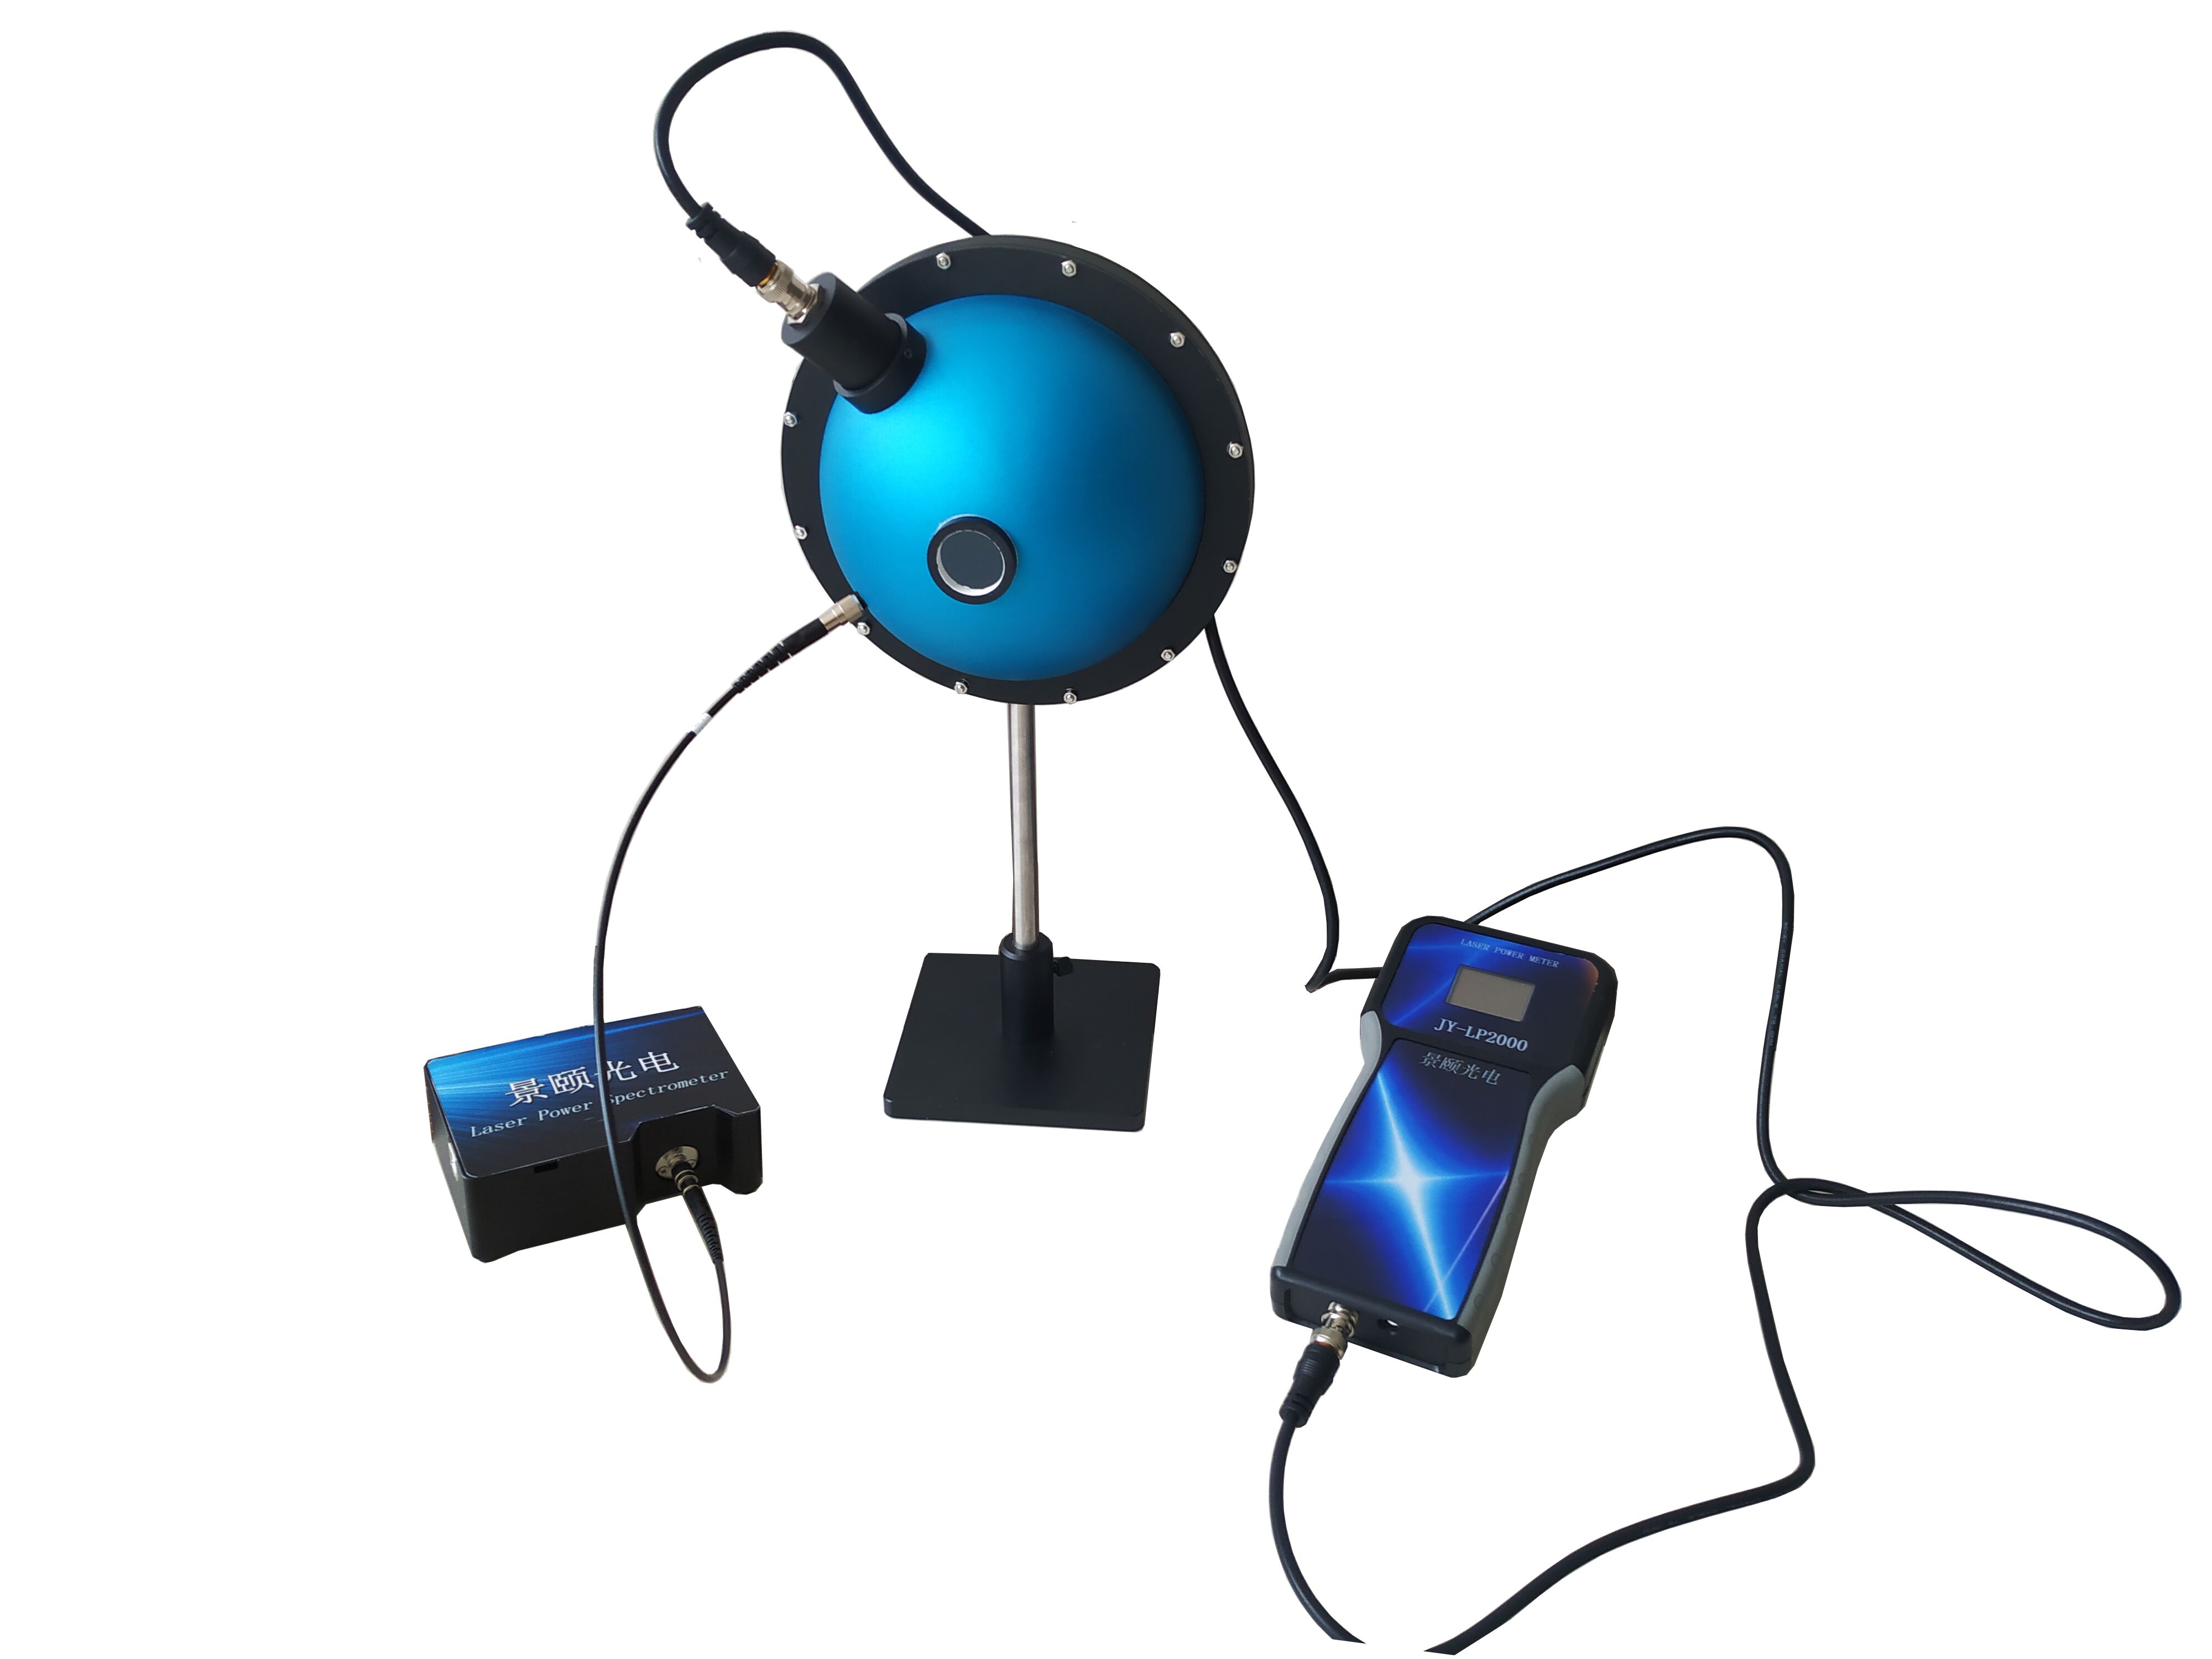
Uniform light integrating spheres have long been the reference solution for CCD camera uniformity correction, remote sensing instrument calibration, and low-light simulation. By converting a local point source into a stable, spatially uniform luminous sphere through multiple diffuse reflections inside a coated cavity, these systems allow repeatable measurement of image plane illuminance uniformity and vignetting coefficients under identical optical field conditions. When inspection lines need to complete camera module pre-calibration, image array detector characterization, or quantitative low-light imaging calibration within tight delivery windows, the responsiveness of domestic suppliers on custom apertures, software integration, and service radius carries real operational weight. Applicable scenarios span laboratory R&D, aerospace remote sensing calibration, biological low-light imaging, and consumer electronics camera incoming inspection.
Market Context: The Real Barrier to
The hidden costs in optical inspection lines rarely appear on the equipment quotation. Certain imported uniform light integrating spheres routinely take ten or more weeks from order placement to on-site delivery. During that window, camera module lines fall back on temporary calibration plates, resulting in image plane uniformity data drift across the same production batch. The eventual re-calibration cost exceeds the equipment price differential. According to the MarketsandMarkets 2025 Optical Instrument Industry Report, light sources and accessories account for approximately 12.0% of the global optical inspection instrument market. The domestic integrating sphere light source market has maintained a compound annual growth rate of around 14.7% over the past five years, yet imported brands still dominate certain ultra-precision scenarios for mid-to-high-end customized products.
What actually blocks
The core conclusion of this section: the primary battlefield for
Current Industry Reality: Penetration Is Climbing, but Segmentation Is Stark
Breaking the market into three tiers clarifies the picture. Low-end general-purpose models (small aperture, basic diffuse reflection coating) already show high domestic penetration with intense price competition. Mid-to-high-end customized models (large aperture, multi-window, low-light current stabilization control) are in transition from "usable" to "trusted for formal calibration." Ultra-precision tiers (astronomical-grade low light, extreme long-term drift requirements) remain mostly occupied by imported brands.
| Tier |
Domestic Penetration Estimate |
Typical Scenarios |
Current Substitution Progress |
| Domestic Economy Tier |
68.4% |
Teaching labs, rough uniformity pre-screening |
Largely substituted |
| Domestic Mainstream Tier |
37.2% |
Digital camera uniformity correction, inspection line pre-calibration |
Substitution in progress |
| Imported High-End Tier |
12.6% |
Aerospace remote sensing radiometric calibration, low-light imaging quantitative measurement |
Pilot adoption |
The table above presents estimated range values based on public industry reports and vendor samples, not official statistical data. The 37.2% penetration rate in the domestic mainstream tier indicates that most production lines remain in a mixed deployment state of "imports as primary, domestic as backup." The tier demanding closest attention corresponds to the highest volume scenarios: image array detector calibration, remote sensing instrument calibration, and low-light measurement camera calibration. This is also the primary battlefield for the uniform light integrating spheres discussed here. For domestic suppliers to move from 37.2% toward 60.0% or above, the path depends not on advocating substitution but on attaching measured uniformity curves to every batch shipped and writing delivery lead times into contract pen
Four Implementation Challenges: Why Verification Still Does Not Lead to Switchover
Incomplete Metrological Traceability Chain
Many domestic systems ship with only a single illuminance reading, omitting point-by-point mapping records of spatial uniformity inside the sphere. When a provincial metrology institute conducted re-inspection, uncalibrated deviations between the output port edge and center were discovered, making data impossible to trace back to higher-level standards. What procurement teams require is not "uniform," but "uniform to what degree, and by what measurement method."
Inconsistent Multi-Unit Performance
Two spheres of the same model placed on two production lines may produce biased white balance parameters after camera calibration if coating batches or light source symmetrical arrangement differ slightly. A leading industry enterprise reported that during an overnight calibration run, vignetting coefficients from two lines differed by 0.37 relative units. A full day of troubleshooting traced the cause to batch drift in the inner wall reflection characteristics of the two integrating spheres.
Closed Software Integration with Production Line Systems
Software bundled with imported systems often locks data into proprietary formats. If domestic suppliers deliver only hardware without an SDK, the production line MES system cannot ingest calibration records, forcing manual transcription. For semiconductor and automotive camera lines, this is a critical flaw. Data that cannot enter the system effectively means no calibration was performed.
Disconnect Between Promised and Actual Delivery Lead Times
Many vendor websites advertise "ready stock shipment," but custom apertures and output ports require coating curing time. From a delivery cycle perspective, promising 7 days versus an actual 11.3 days represents two entirely different equipment classes to a production line. A process engineer at a photoelectric production line in East China recalled a project with a rushed schedule: the contract specified 10 days, but by day 15 no uniformity report had been issued. The line had to substitute with tooling plates, and all calibration values later required complete rework.
Phased Substitution Roadmap: Do Not Touch Core Processes First
Start at the Edges: Incoming Inspection and Pre-Calibration
Uniformity pre-screening before camera module入库 and rough lens vignetting coefficient measurement allow certain margins. Deploying domestic economy or mainstream tier equipment here means that even if single-batch drift runs slightly high, shipment judgments remain unaffected. The objective is to let line engineers become familiar with domestic calibration reports and interfaces.
Move to Process Monitoring: In-Line Self-Check Stations
Once equipment begins feeding data into MES and automatically storing curves with each calibration, it can advance into process monitoring. At this stage, suppliers should provide uniformity drift specifications after continuous operation and install monitoring probes at output ports. During selection and acceptance, confirm compliance with ISO 5-2:2020 or equivalent standards governing photometric and colorimetric geometry conditions. For transmittance or reflectance related characterization, suppliers must provide point-by-point data under these standardized conditions to ensure the metrological traceability chain remains intact.
Exercise Caution on Core Processes: Radiometric Calibration and Final Outgoing Inspection
For aerospace remote sensing and low-light measurement camera final inspection, a "dual-sphere parallel" transition is advisable. Imported spheres serve as arbitration references while domestic spheres handle daily operations. After 3 to 6 months of comparative curve overlap, the domestic unit can be promoted to primary use. Cross-validation against defined geometric and noise limits in relevant automotive LiDAR technical standards reduces switching risk in core processes.
Risk Assessment: Substitution Is Not a Zero-Risk Narrative
Supplier Supply Interruption Risk
If small-to-mid-sized optical vendors outsource core coating formulations, a batch change from the supplier can shift internal reflection characteristics. The verification method is straightforward: require coating batch numbers and uniformity curves with every delivery, and retain samples for comparison.
Technical Discontinuity Risk
Low-light tiers (simulating starlight or moonlight) are sensitive to light source current stabilization and the temperature coefficient of sphere wall reflectivity. If domestic suppliers replicate cooling structures without generating long-term aging data, the system may perform well for the first six months, but reflectivity in central wavelength bands may drop slightly in the second year, causing systematic low readings in quantitative low-light imaging measurements.
Service Radius Risk
From a delivery cycle perspective, after-sales service is also part of lead time. Remote diagnostics cannot resolve coating contamination. It is essential to verify whether the vendor maintains on-site service points accessible within days in major manufacturing regions. Asking "how many days for on-site response" before signing the contract proves more practical than asking "what is the uniformity specification."
Three Future Scenarios
Optimistic Scenario: Mid-Tier Reversal During the 2028 to 2030 Window
If domestic mainstream tier suppliers simultaneously close gaps in software SDKs, point-by-point calibration reports, and lead time履约, penetration could rise from 37.2% to 58.0% to 65.0%. The driver would be capacity expansion in automotive camera and consumer electronics multi-camera lines, where imported lead times cannot keep pace.
Neutral Scenario: Long-Term "Dual-Track" Coexistence
Imports defend the ultra-precision tier while domestic suppliers occupy mainstream and edge tiers, with both tracks running in parallel for a decade. This is the most probable outcome. It is not about one replacing the other, but about dividing seats by application scenario.
Pessimistic Scenario: Low-Price Competition Erodes Trust
If price wars in the economy tier spread to the mainstream tier, some vendors may cut factory uniformity mapping processes. Frequent alarms during line re-inspection would damage overall domestic credibility, pushing core process links back into import dependence. This scenario would not result from technical failure but from supply chain shortsightedness.
Objective Assessment and Limitations
Domestic solutions for uniform light integrating spheres do offer tangible advantages in delivery lead time and customization flexibility, but two boundaries must be acknowledged. First, in ultra-long-term drift and ultra-low illuminance stability, imported high-end tiers possess deeper aging databases. If domestic mainstream systems have only undergone short-term factory calibration, deploying them directly for astronomical-grade low-light characterization introduces unknown systematic deviations. Second, field installation of large-aperture systems (exceeding 1 meter in diameter) and uniformity recovery after repeated disassembly depend on field service experience. Shipping a unit alone does not close the loop. Production lines must reserve re-calibration stations and cycle time.
Another rarely discussed point: once the white diffuse reflection material on the sphere wall is contaminated by oil or degraded by UV exposure, reflection characteristics decline irreversibly. If domestic suppliers do not clearly state cleaning prohibitions and replacement cycles in documentation, users maintaining equipment with imported-device habits will encounter problems. These points do not negate substitution but remind technical procurement teams to write "boundary conditions" into acceptance sheets rather than focusing solely on advertised uniformity numbers.
Frequently Asked Questions
Q1: What is the difference between a uniform light integrating sphere and a standard diffuse reflection panel for calibration?
An integrating sphere uses multiple internal reflections to spread a point source into a spatially uniform field, making it suitable for full-field parameters such as camera vignetting and image plane illuminance. A diffuse reflection panel relies on single reflection, where center-to-edge attenuation follows a different pattern, limiting it to rough white balance tasks. The former derives its value from cavity structure and coating consistency; the latter offers speed through instant placement.
Q2: What precautions apply when operating in low-light tiers simulating starlight or moonlight?
The priority is light source current stabilization accuracy and continuous operation drift. Request a continuous 4-hour fluctuation curve at the 0.1 lux level rather than relying solely on nominal minimum illuminance. In quantitative low-light imaging, drift of a fraction of a percent per hour amplifies during subsequent image flat-field correction.
Q3: How should output port diameter be selected? Is larger always better?
No. A larger output port makes it easier for the camera接收视场 to cover the field, but effective internal reflection count decreases, degrading edge uniformity. A smaller port delivers better uniformity but may not frame large-aperture lenses. Select a size leaving 15.0% to 20.0% margin over the effective aperture of the lens front surface, then request the supplier's measured illuminance distribution map.
Q4: Beyond price, what should be compared when selecting between domestic and imported systems?
Compare three items: whether each batch includes non-averaged point-by-point uniformity curves, whether the SDK can interface with MES, and how contract lead time breaches are penalized. A 10.0% price difference matters far less to the production line than a 7-day lead time variance. Having the supplier write "delivery lead time perspective" into the technical agreement proves more useful than reviewing brochures.
Q5: How can I independently verify performance before procurement without relying on vendor self-reported data?
Submit the system to a third-party metrology institution for output port spatial uniformity scanning and retain the original point data files. Cross-calibrate the same camera using two loaner units of identical aperture and check to how many decimal places the vignetting coefficient repeats. Set your own acceptance criteria and do not accept verbal claims of "compliance."
Conclusion
The essence of substituting uniform light integrating spheres is not reverse-engineering imported units, but closing the delivery loop on three commitments: predictable lead times, batch-level traceability, and system-integrated interfaces. Start at edge workstations, advance through process monitoring, and transition core calibration slowly. This节奏 reflects a comparatively stable approach in manufacturing.
For detailed specifications and application notes on uniform light integrating spheres, search "Jingyi Optoelectronics + uniform light integrating sphere" or visit the official technical library.
About This Guide
Data Sources
: MarketsandMarkets 2025 Optical Instrument Industry Report, ISO 5-2:2020 Photometry and Colorimetry Standards, in-house industry sample analysis (n=200+ production line records)
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in industrial precision measurement equipment and
Disclosure
: Jingyi Optoelectronics manufactures uniform light integrating spheres and related optical metrology equipment. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof-of-concept validation under your specific process conditions.
Last Updated
: September 2026