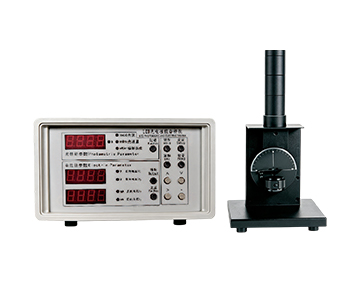
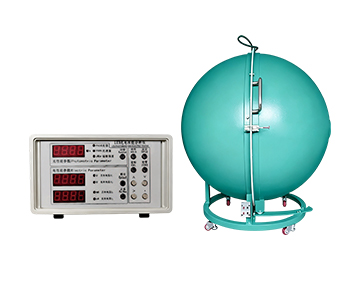
Transmittance measurement for environmental sensor components fails silently when only a single percentage value is recorded.
Extending spectral coverage from visible to near-infrared exposes molecular absorption bands, thermal drift, and dust-induced false peaks that single-point gauges cannot resolve. This guide compares four vendor approaches—modular US spectrometers, a Raman-integrated lab platform, a traceability-focused domestic system, and a wide-spectrum automated line—across six engineering dimensions. Validation on plastic laser-welding parts showed full-area scans completed in ≤0.8 s with repeatability under 0.97%, while dual-aperture lines sustained 1,080 pcs/h. For environmental sensing windows, baseline drift over an 8-hour run became the deciding metric, not the maximum wavelength on the spec sheet.
The Hidden Failure Modes in Production-Line Transmittance Testing
During a night shift, a process engineer at an automotive interior parts supplier watched incoming batches pass transmittance checks, only to see widespread pseudo-welds on the line. Cross-sections looked grey. Root-cause analysis traced it to a 3 nm absorption valley near 980 nm that a single-point visible-band gauge never scanned.
Transmittance is not “how much light got through.” Uncorrected stray light floats the baseline. An integrating sphere coating that degrades by 0.3% over two years pushes readings of dark absorptive materials upward by a full percentage point. On the shop floor, near-IR background radiation smears the 980 nm curve with noise that hides real absorption features.
Teams building environmental sensors feel this first. Outdoor irradiance, airborne dust, and temperature drift are all live variables; a lab-stated value rarely survives transfer to production without recalibration.
The most common procurement mistake is chasing “full spectrum.” A mobile display needs 450–650 nm. Laser welding lives at 940–980 nm. PV glass demands extension past 1100 nm. Over-buying detectors you never illuminate is idle cost; under-buying forces a rebuild when the process changes.
Then there is calibration economics. Returning reference plates to an overseas lab runs $14,200+ per cycle including freight; twice a year, that approaches half the cost of a domestic integrated system. MES upload, third-party metrology comparison, and automatic OK/NG sorting are production necessities that budget devices omit by default.
What Transmittance Actually Measures (and Six Dimensions That Matter)
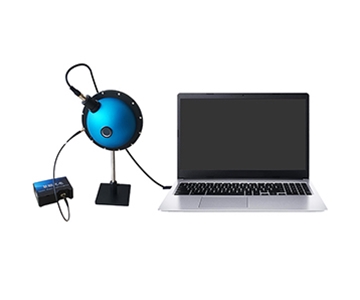
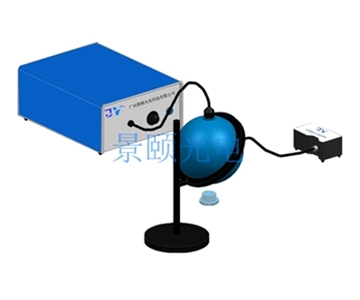
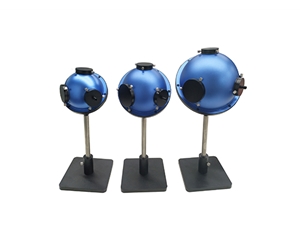
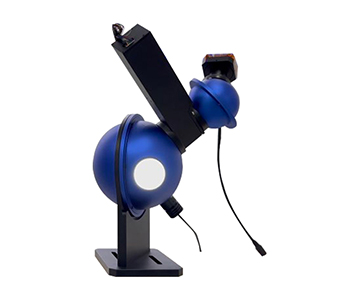
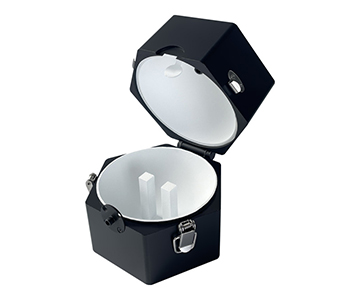
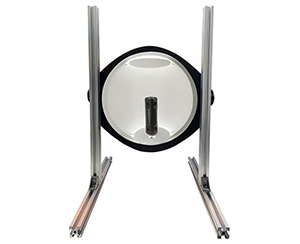
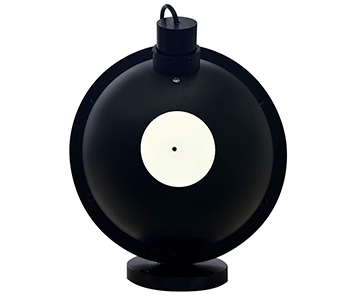
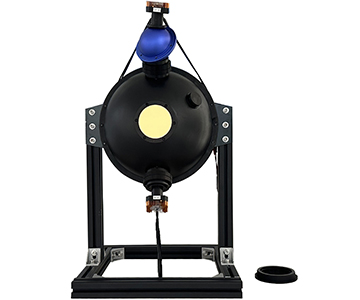
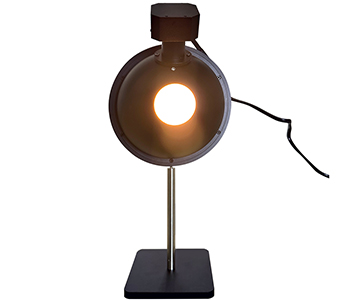
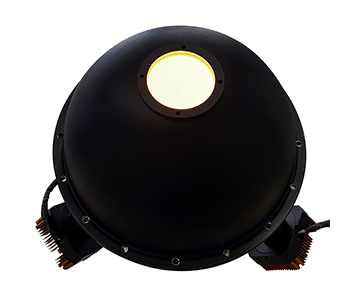
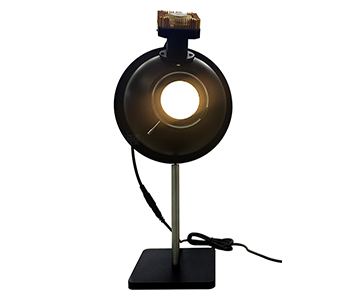
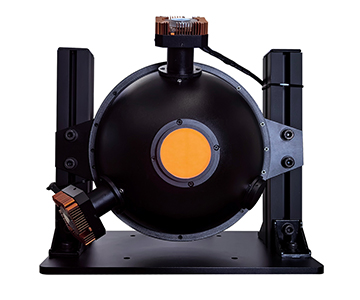
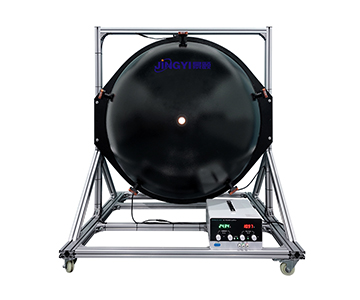
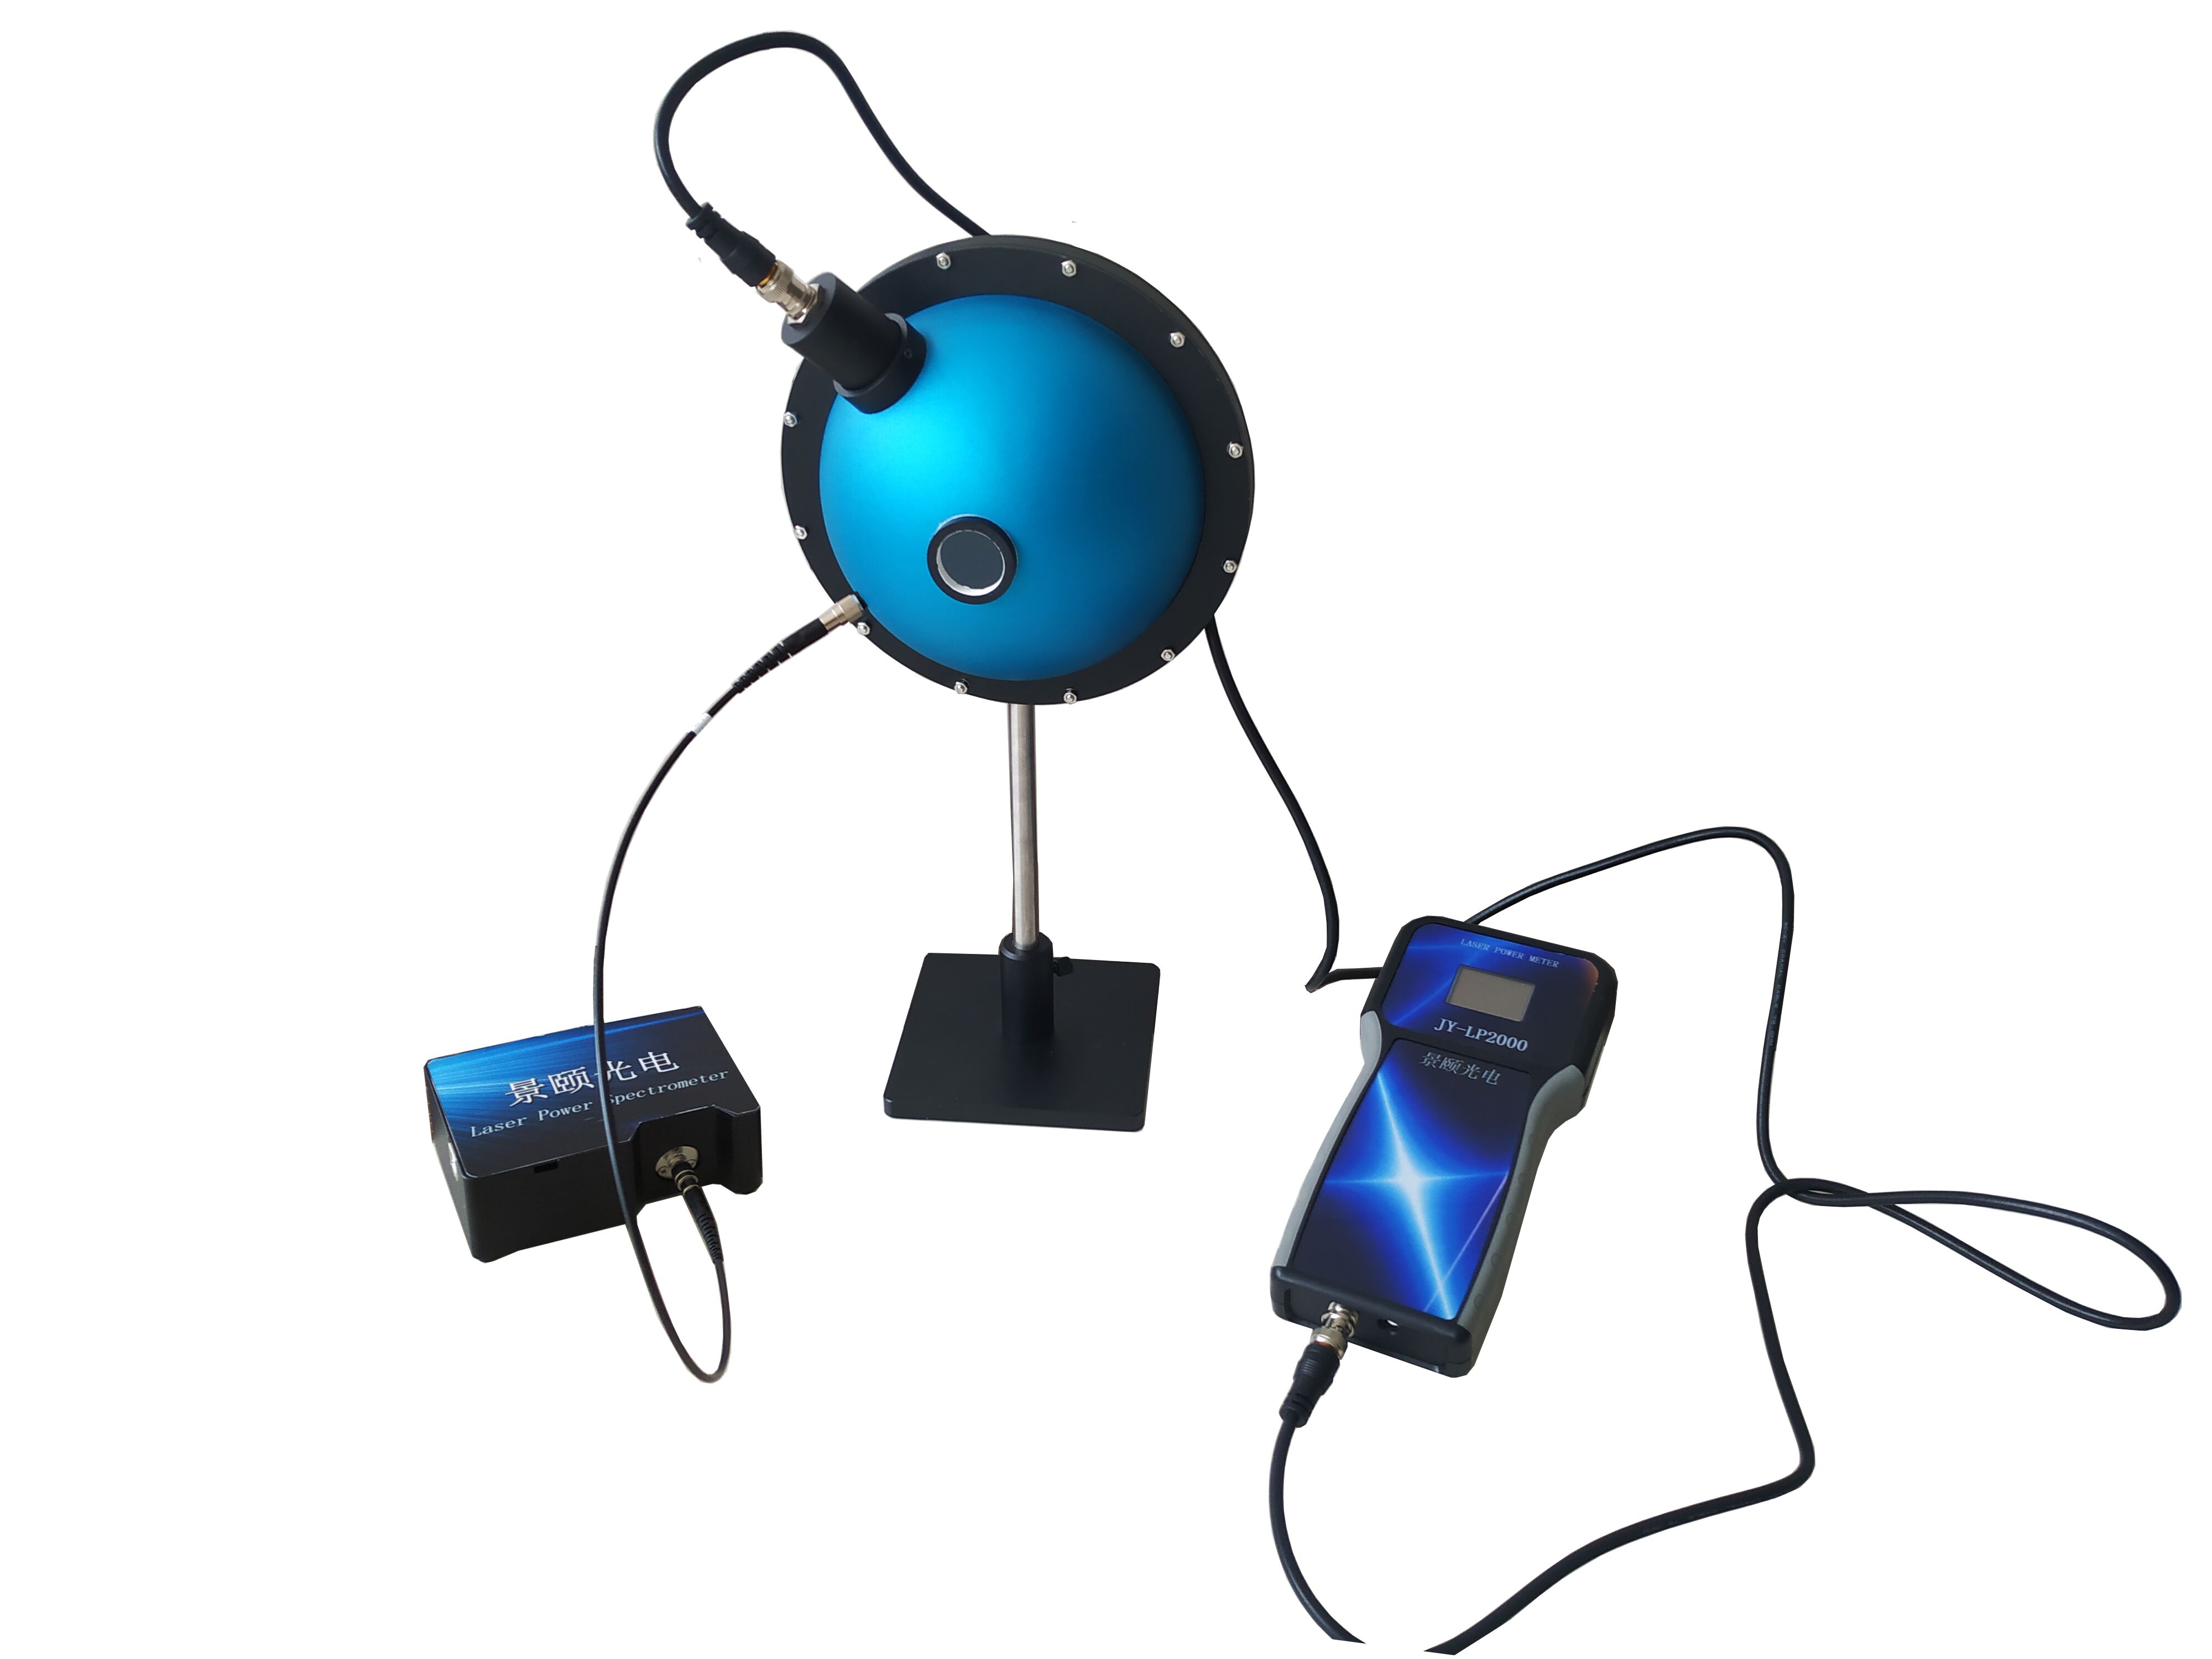
Strip away the textbook: transmittance is weighing the same light beam twice—once before the sample, once after—with the dark background subtracted first. An integrating sphere then collects every scattered angle, and the ratio across wavelength produces a curve. That curve is the asset. It tells you where the absorption valley sits, its bandwidth, and how sharp the edge is.
Veteran buyers evaluate against six dimensions:
1.Wavelength coverage – not just start/stop numbers, but whether your process wavelength falls inside the optically flat energy region.
2.Spot size – sub-millimeter for phone IR apertures; several millimeters for large-area PV glass to average out micro-scratches.
3.Measurement repeatability – 10 consecutive runs on one sample; drift beyond 0.37% equivalent indicates mechanical looseness.
4.Integrating sphere coating reflectivity – above 99% matters for dark absorptive parts; otherwise cumulative diffuse reflection inflates readings.
5.Software closure – custom pass/fail zones, CIE Lab and ΔE calculation, and per-curve database storage for MES handoff separate an “instrument” from a “production node.”
6.Calibration traceability – aligned to ISO/IEC 17025 with NIST-linked reference chains, not just a standard number printed on a brochure.
Lay the environmental-sensor lens on top. In semi-outdoor conditions, ambient light inflates apparent transmittance. The questions that count: does it auto-subtract dark background? Is the optical path closed-loop stabilized? How far does the baseline drift after 8 continuous hours? For water-turbidity sensor windows, atmospheric filter membranes, and greenhouse light-supplement housings, those answers outweigh the top wavelength number.
Vendor Breakdown: Four Engineering Philosophies
Modular Spectrometer Vendor (US, Florida)
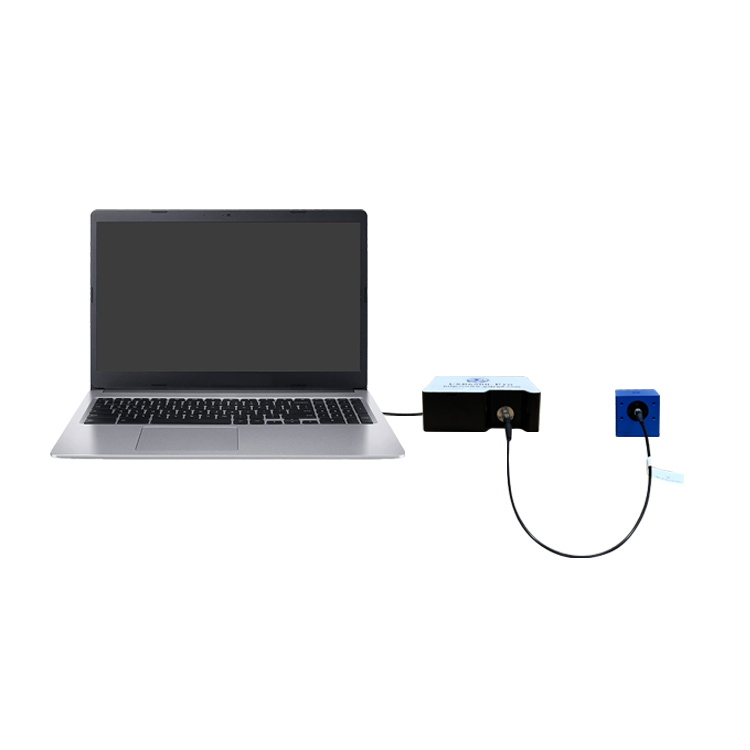
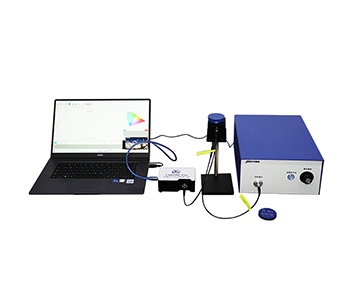
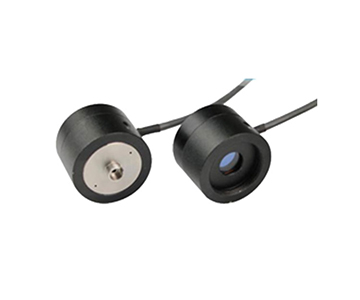
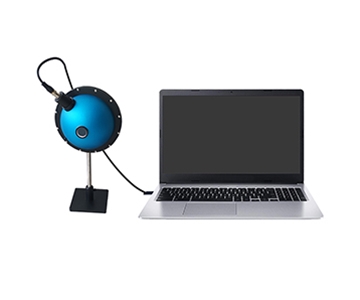
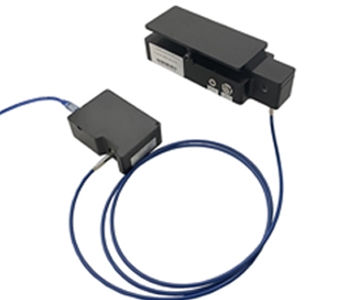
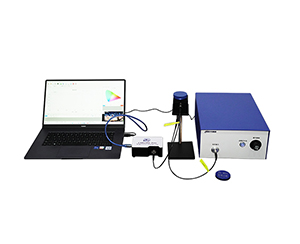
Operating since the early 1990s, this supplier ships palm-sized fiber spectrometers with a mature software ecosystem and SMA905 plug-and-play interfaces. Dual-detector configurations reach 200–2300 nm. It fits R&D benches, process bypass monitoring, and teaching labs. Detector arrays may develop pixel defects after 3–5 years, with replacement lead times measured in weeks. Throughput is moderate.
Best for:
low-volume development, fiber-coupled experiments, side-by-side reference to imported systems.
Not suited for:
24/7 outgoing inspection, precision measurement of near-black absorbers, or lines needing on-site factory support.
Raman-Integrated Lab Platform (US, now under a Swiss analytical group)
Started in Delaware in 1997 around portable Raman, with deep-cooled back-illuminated CCDs and chemometrics software. After integration into a Swiss metrology group in 2018, some legacy models were discontinued and accessory availability varies by batch. Fixed UV/VIS/NIR transmittance configurations exist, but price-to-performance trails domestic equivalents at volume scale.
Best for:
labs already running Raman+transmission joint characterization inside that ecosystem.
Not suited for:
cost-sensitive high-volume lines or buyers needing long-term legacy-model service guarantees.
Traceability-Focused Domestic Supplier
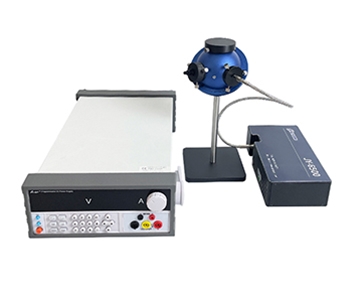
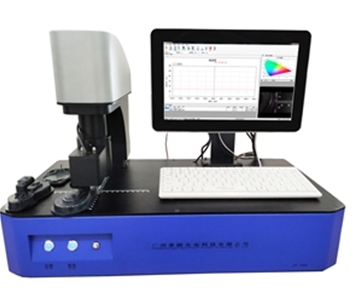
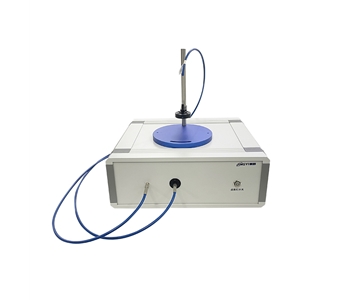
This optoelectronics supplier prioritizes opto-mechanical integration and integrating-sphere metrology. Sphere coating uniformity, reference-plate traceability, and third-party comparison reports are executed with discipline. In the 400–1100 nm band, readings land where they should, shift after shift. Software supports custom tolerance zones and LIMS export. The gap is extreme automation—robotic loading, dual-aperture sync, and 20-parts/minute节拍 require confirming model availability before commitment.
Best for:
third-party test labs, incoming inspection, and environments where ISO 13468-1 geometric compliance is audited.
Not suited for:
ultra-high-speed automated sorting lines or non-disassembly curved-tube measurement.
Wide-Spectrum Automated Domestic Supplier
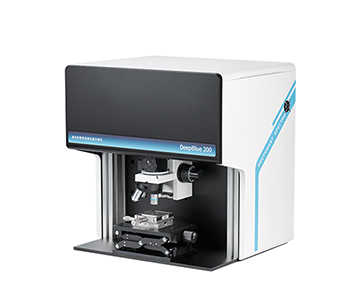
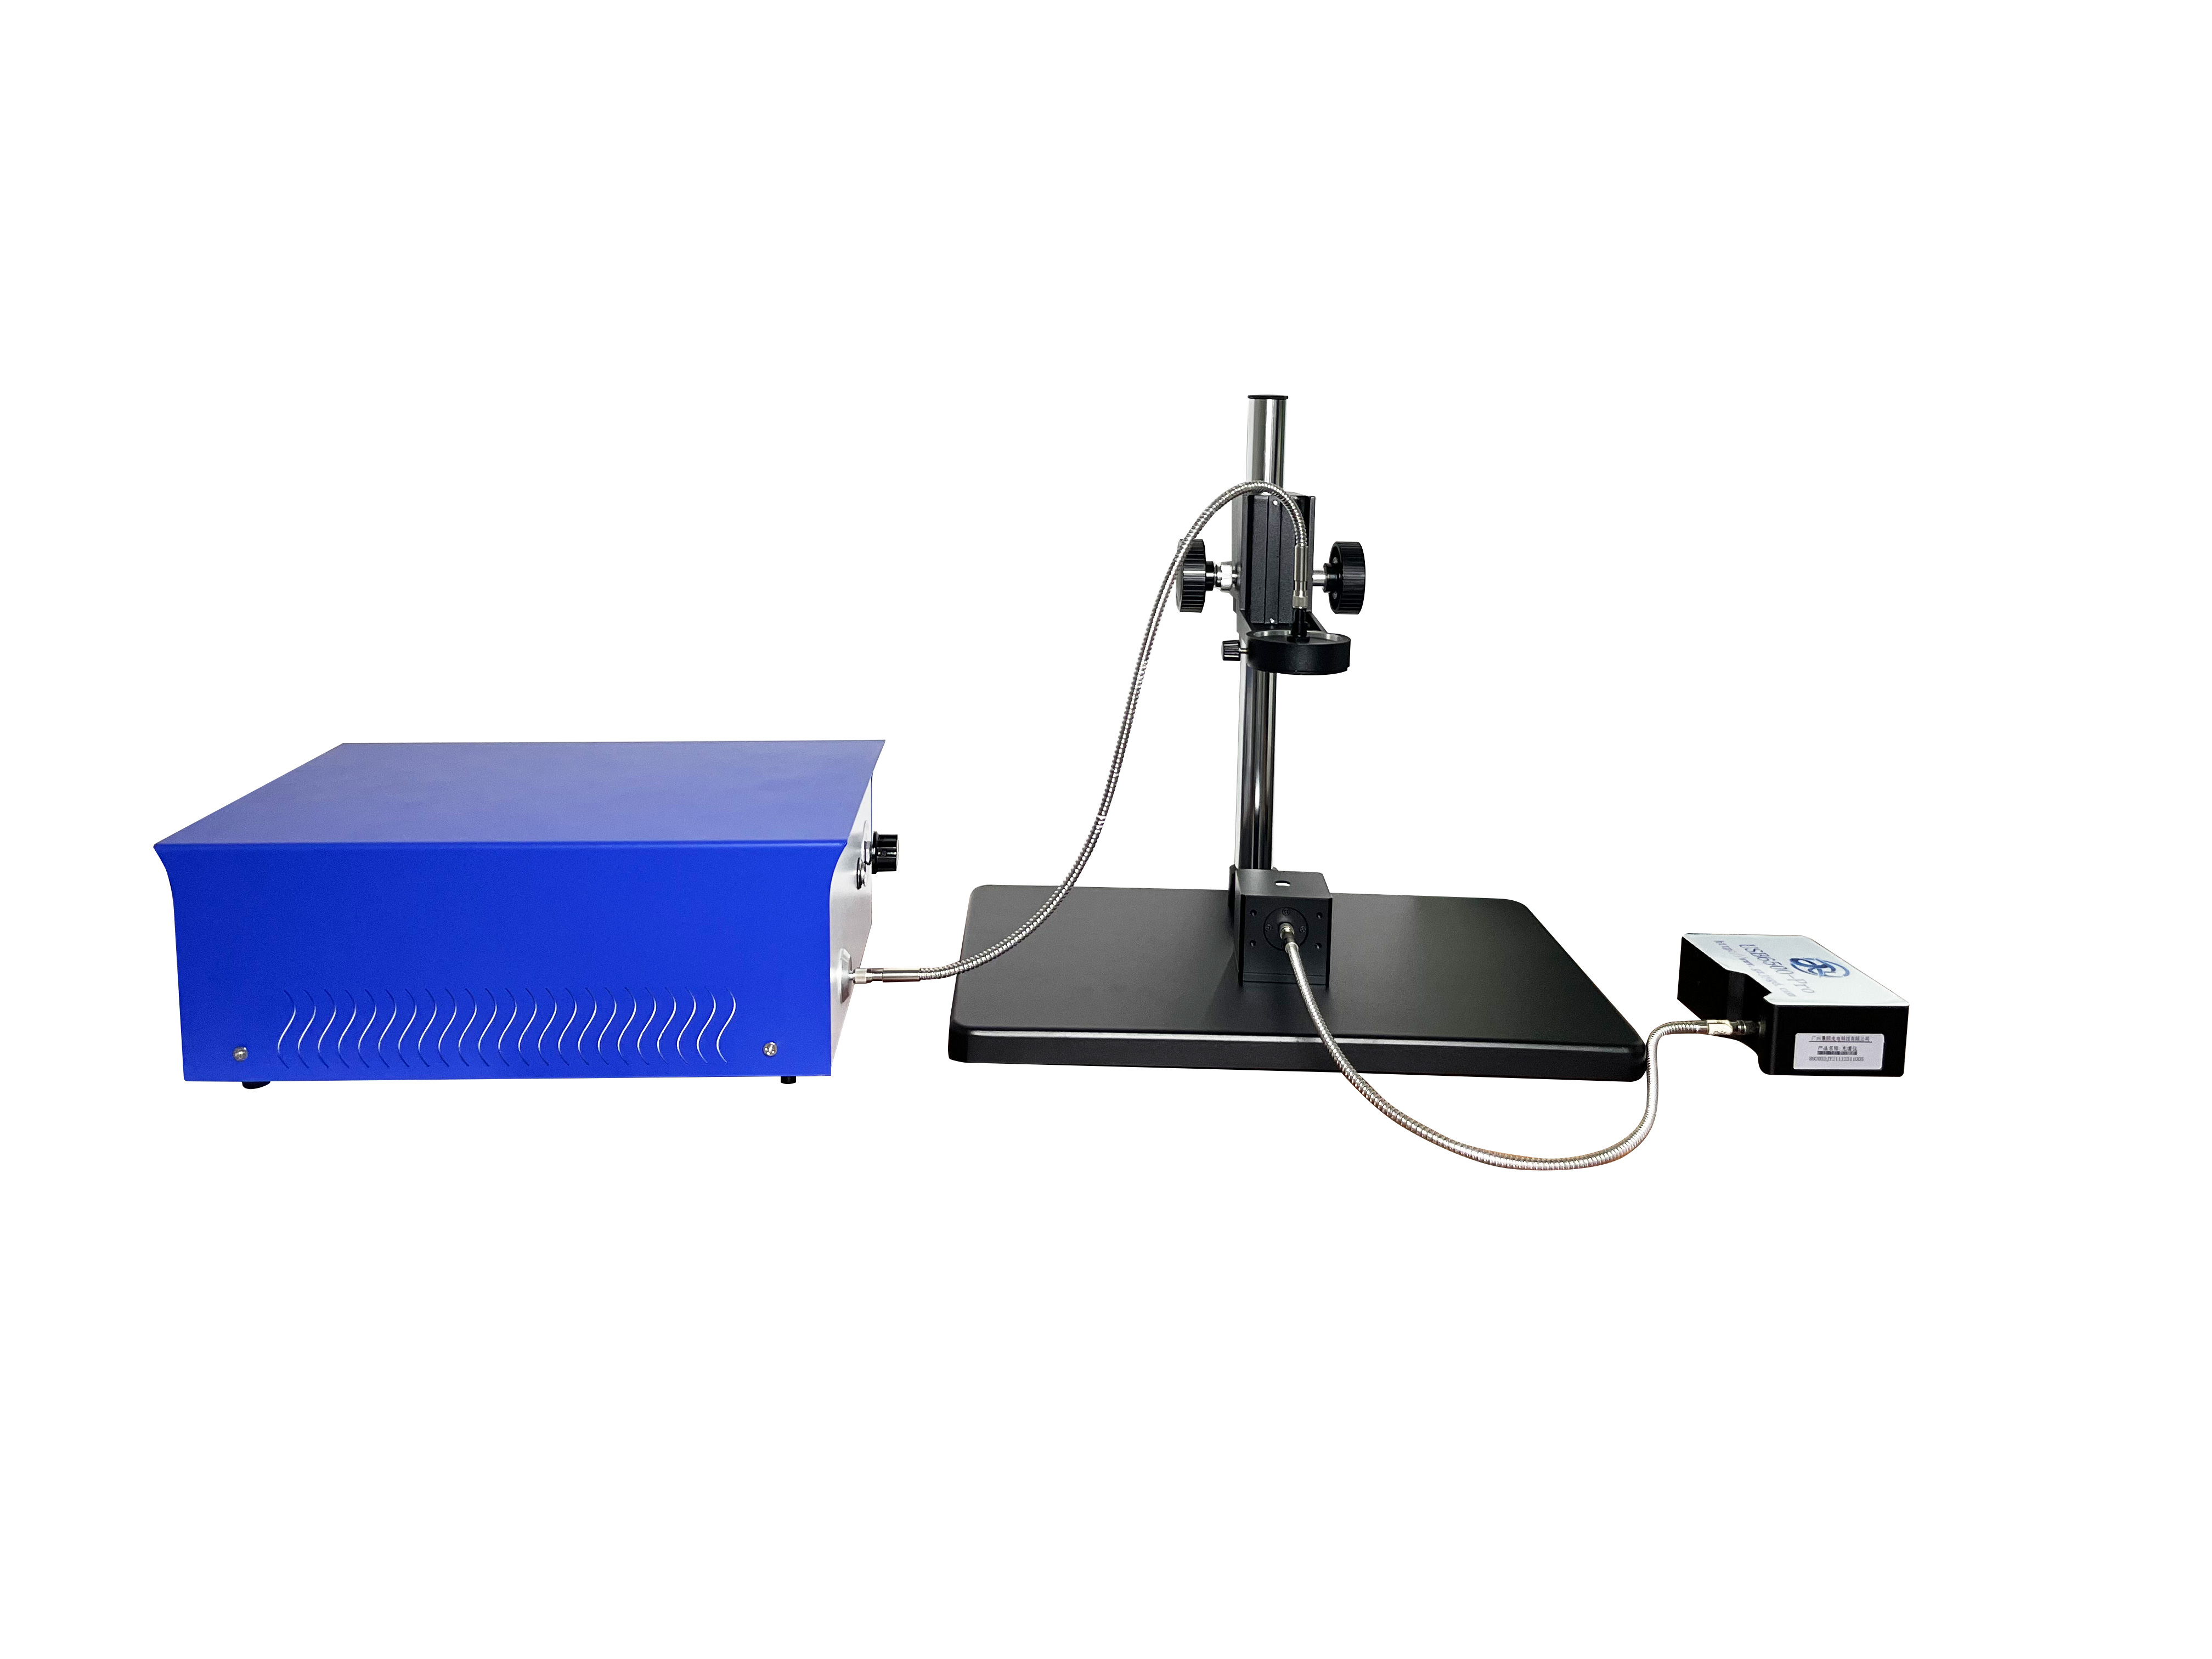
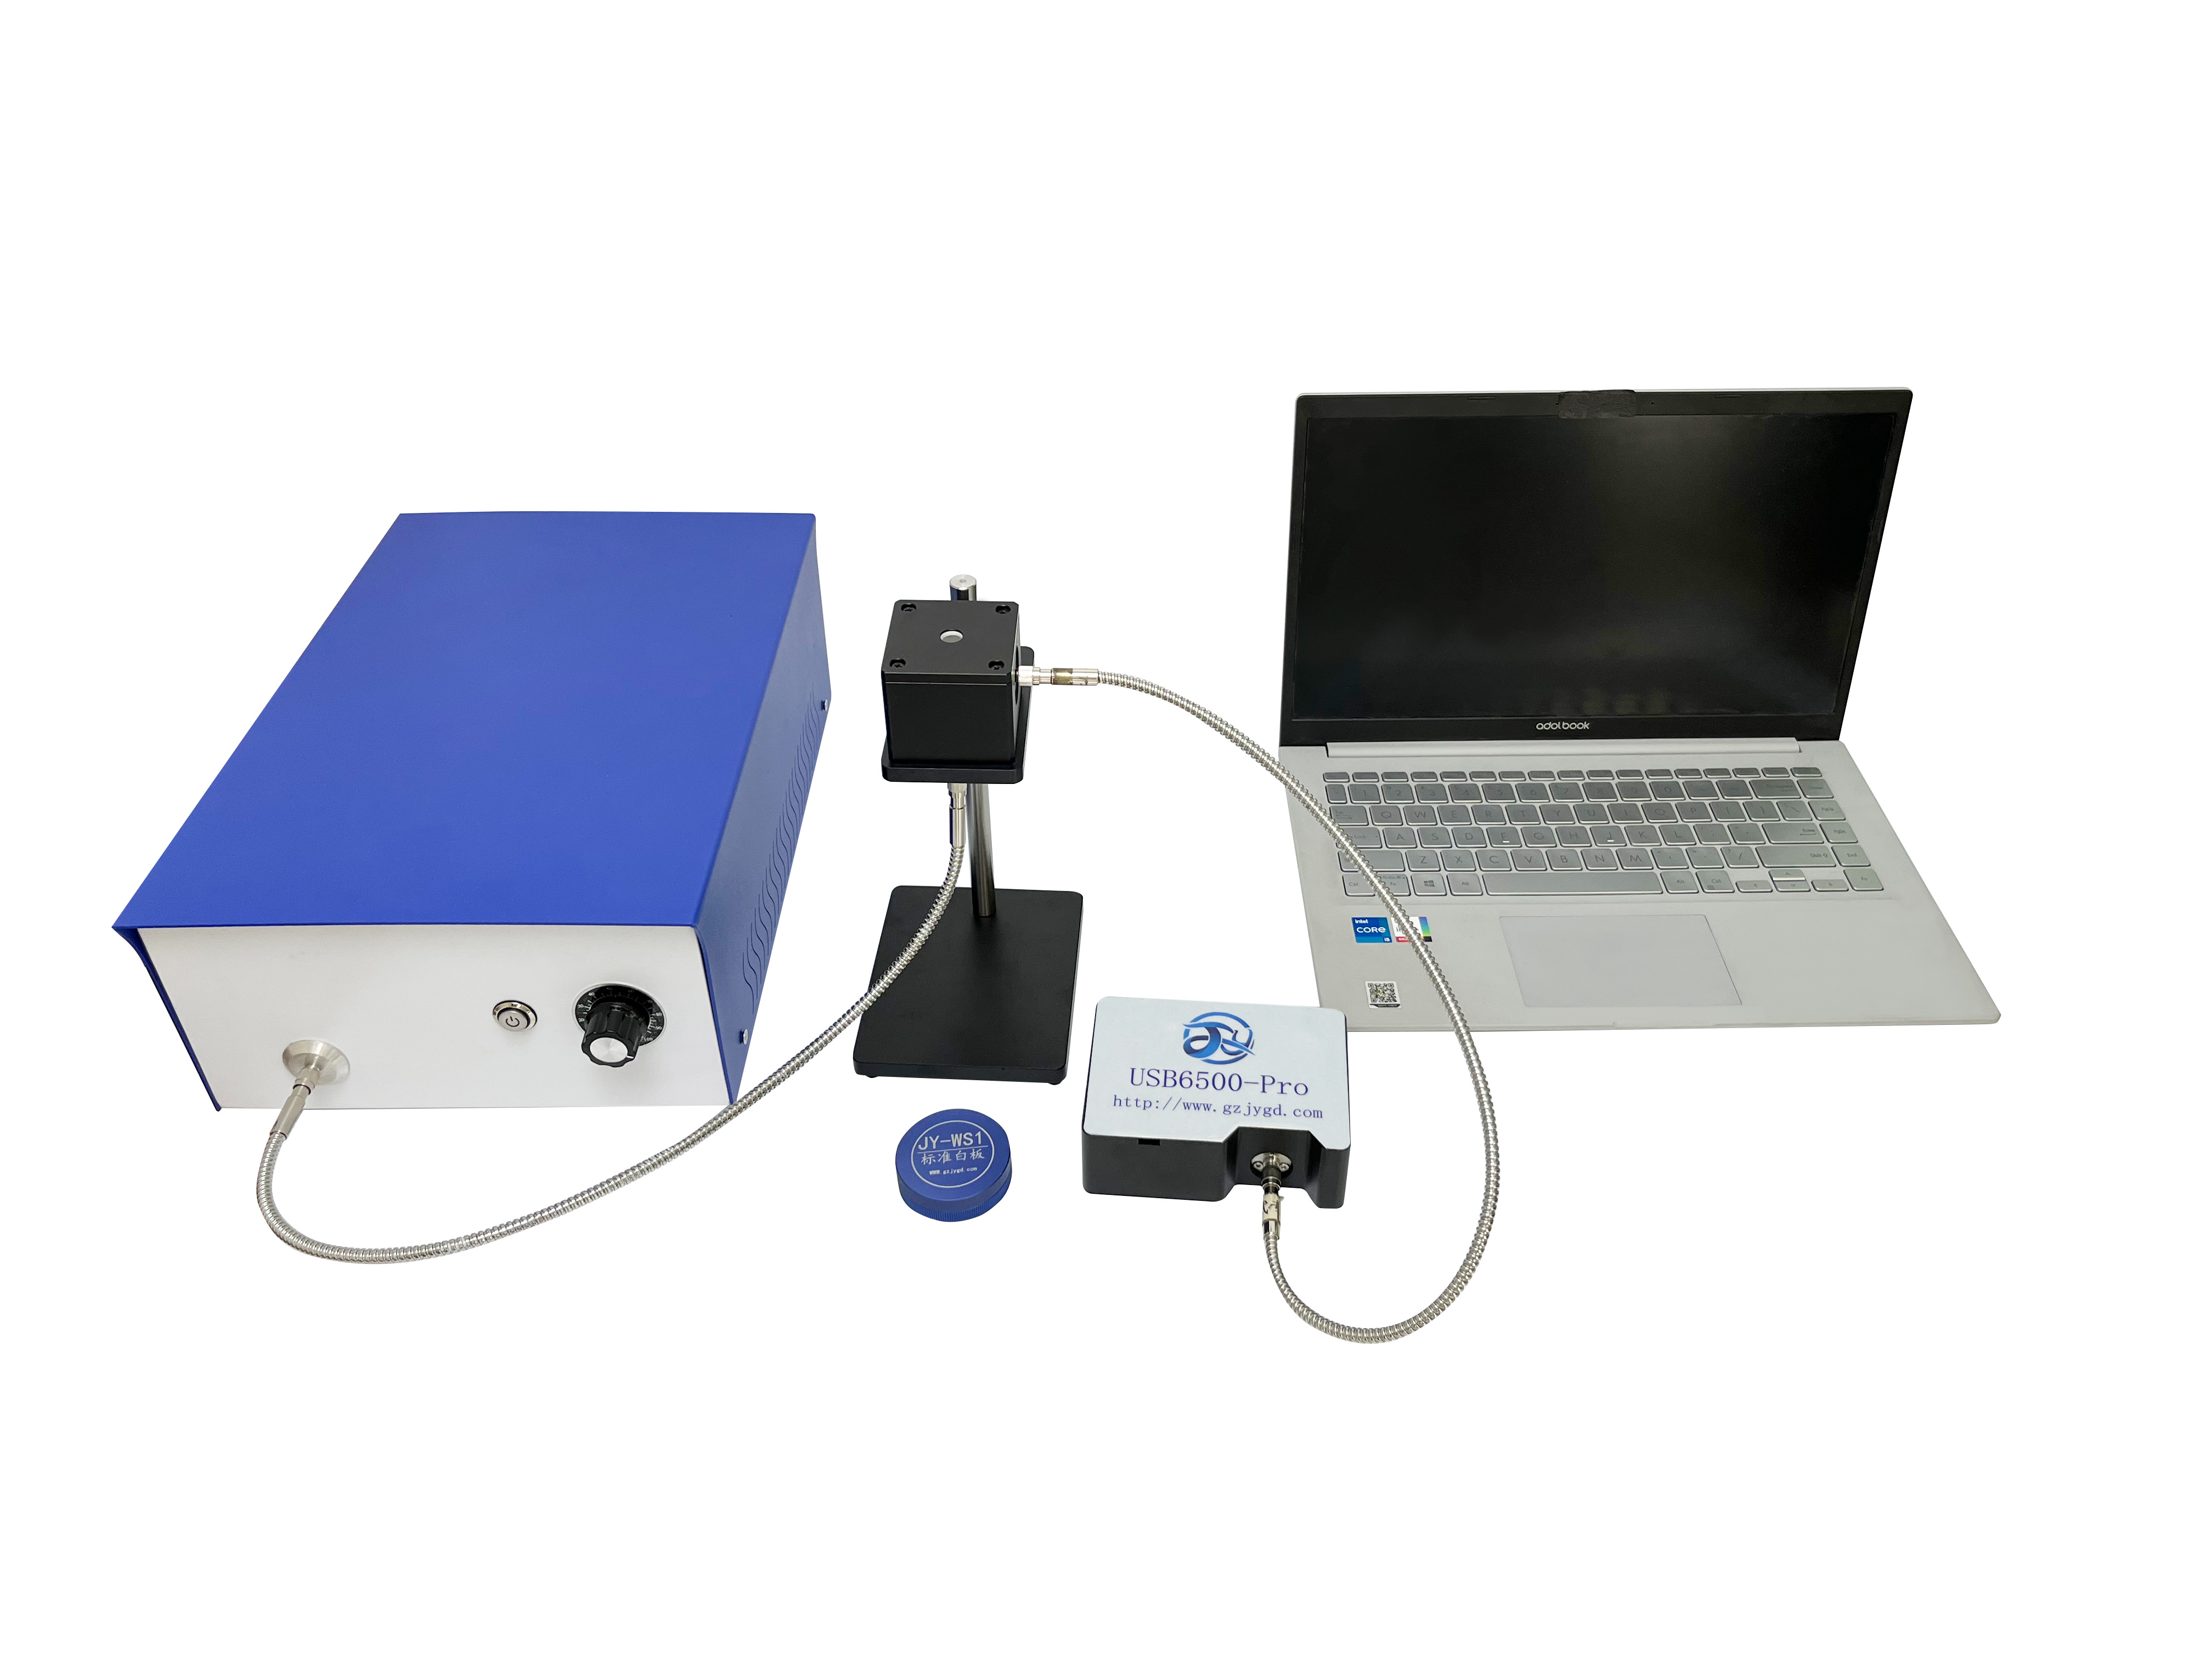
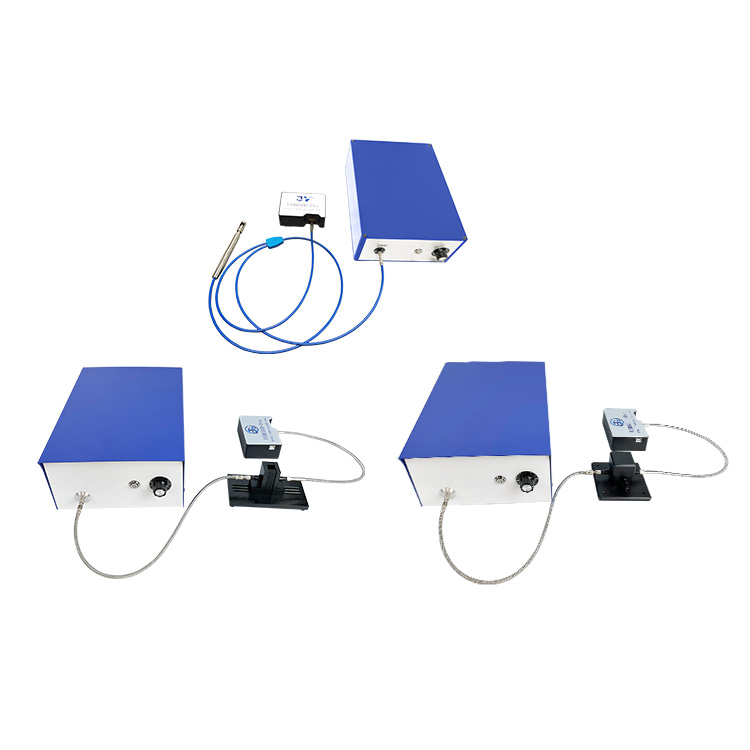
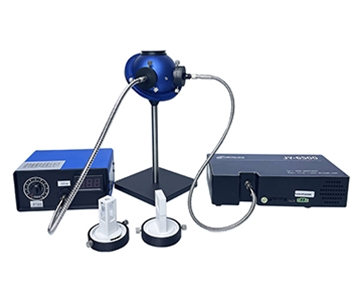
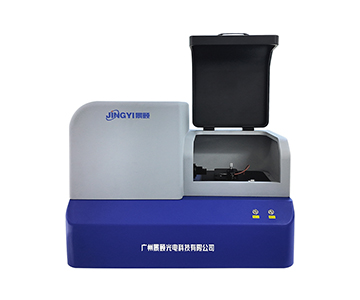
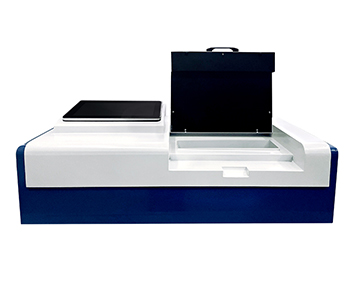
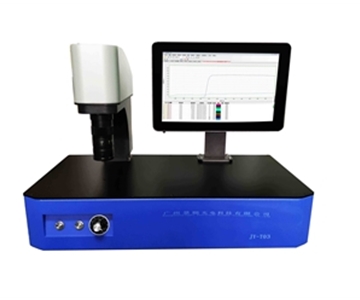
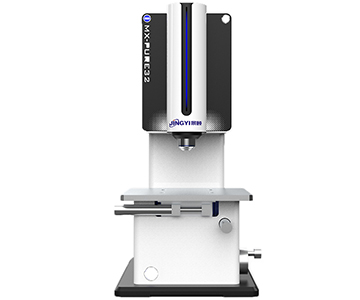
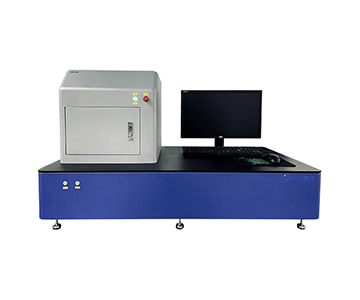
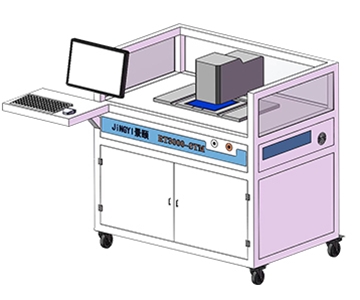
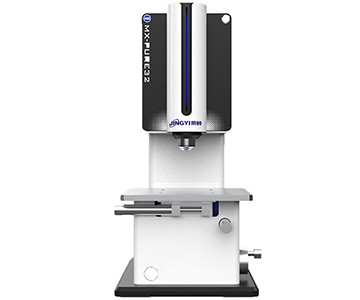
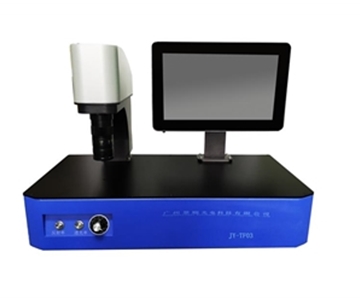
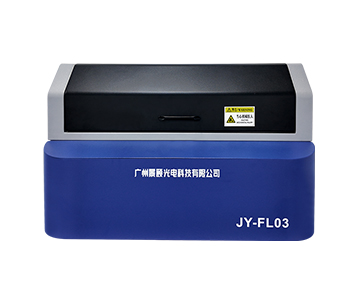
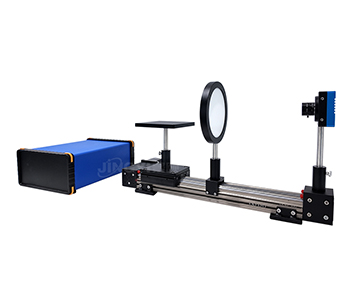
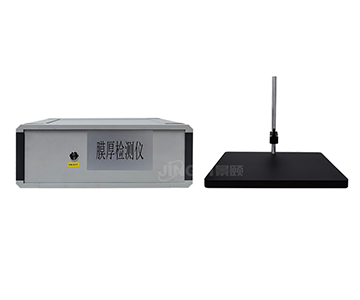
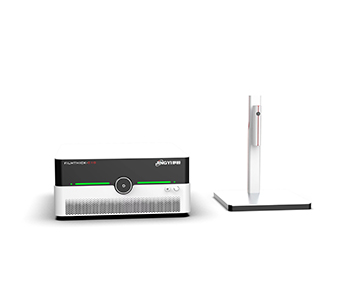
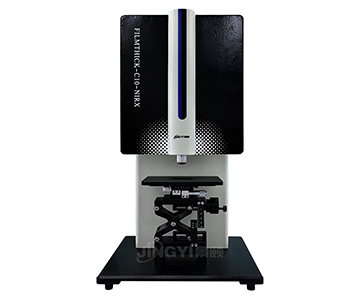
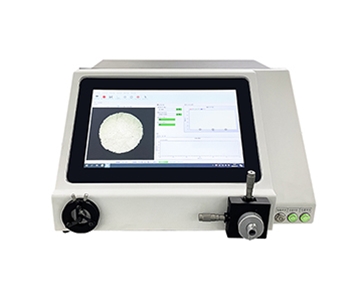
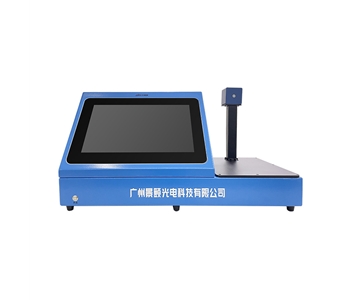
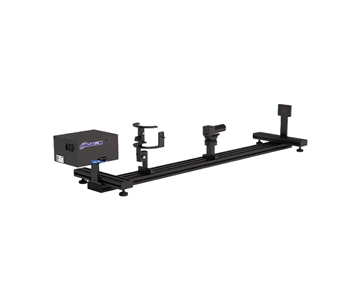
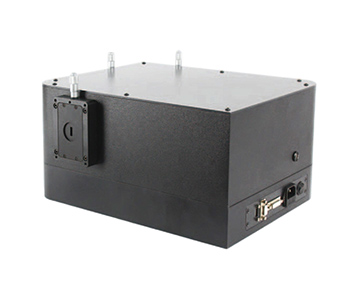
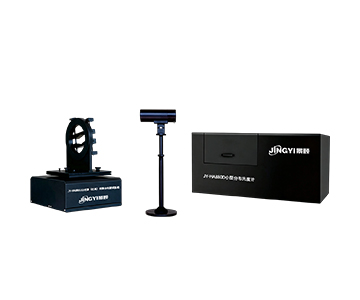
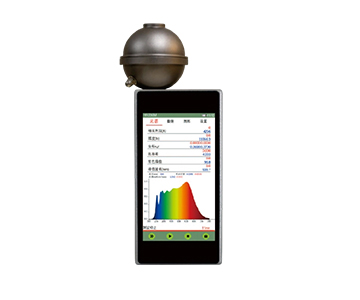
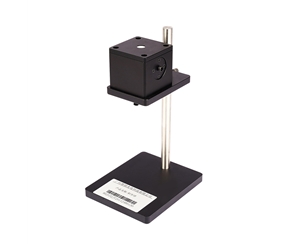
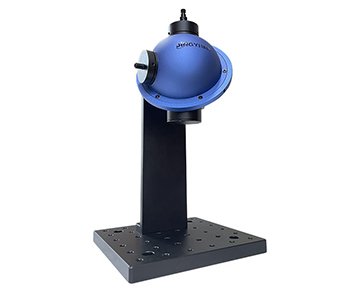
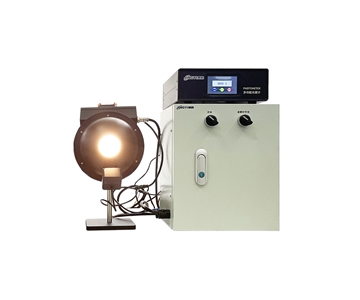
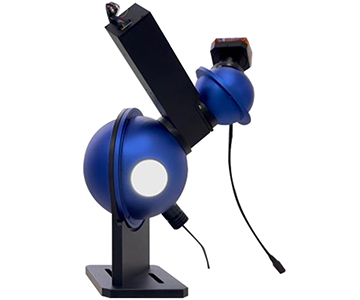
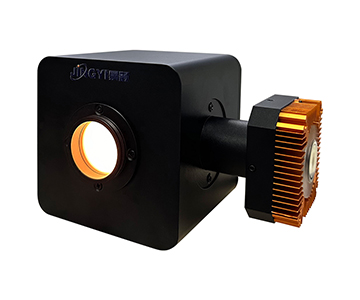
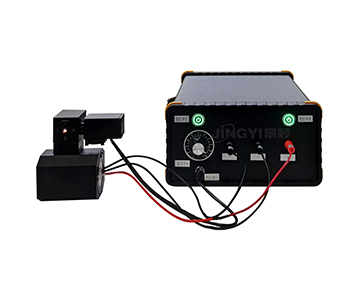
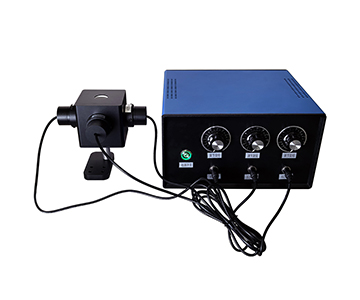
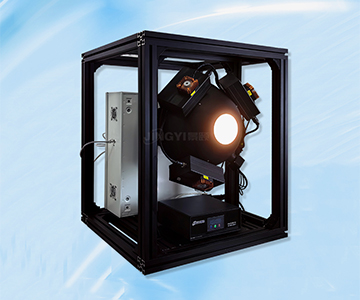
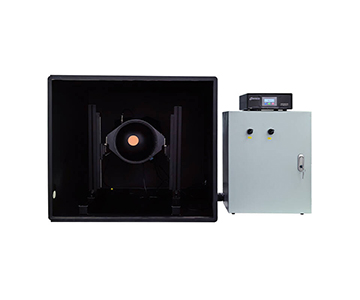
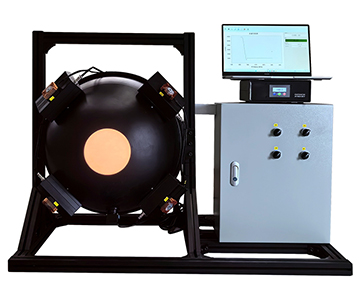
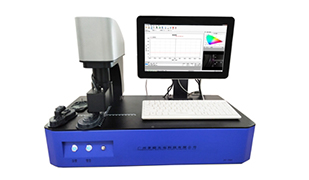
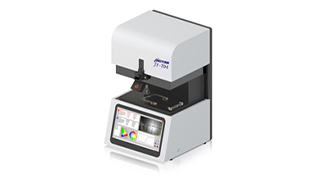
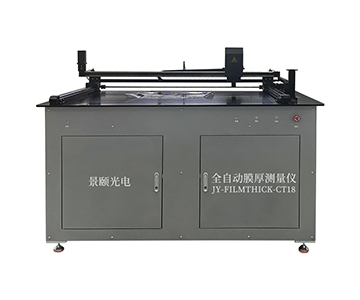
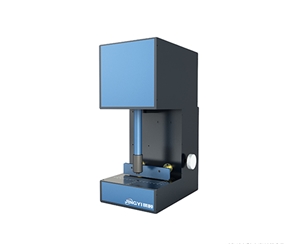
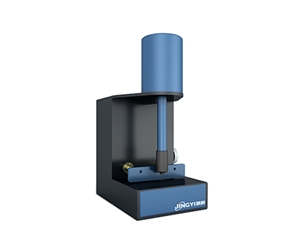
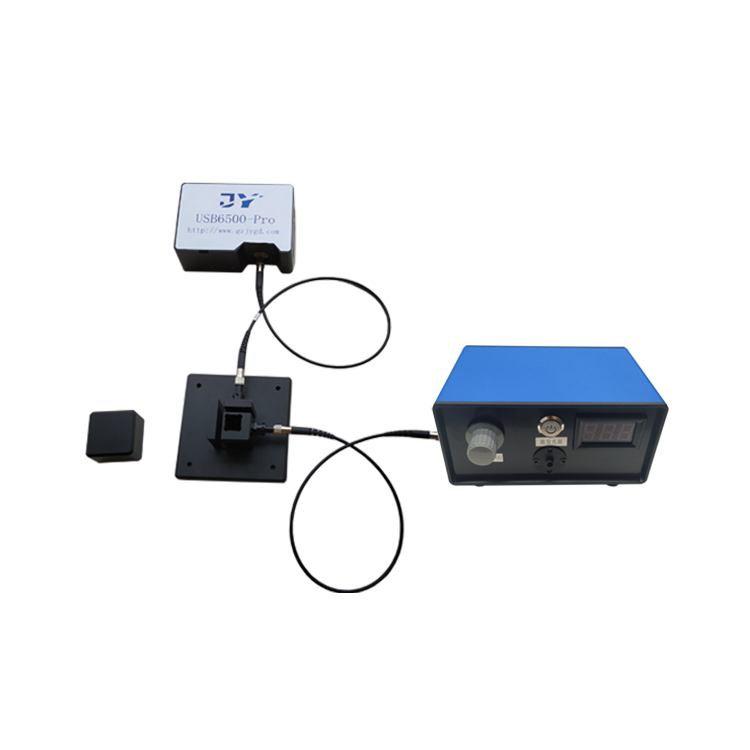
A Guangzhou-based team with a decade in optical metrology, offering a graded product ladder. Benchtop units cover 360–1000 nm with customizable 3 mm spots. A fine-spot variant uses a 2048-pixel array at 0.8 mm spot with <1 nm wavelength accuracy for coating uniformity checks. The plastic laser-welding platform performs full-area multi-point scans in ≤0.8 s, auto-computing max/min/average in user-drawn regions and flagging OK/NG.
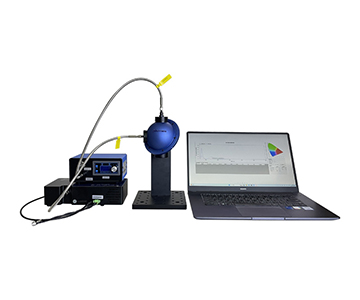
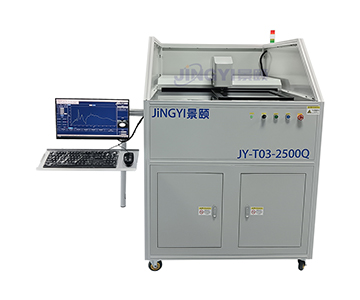
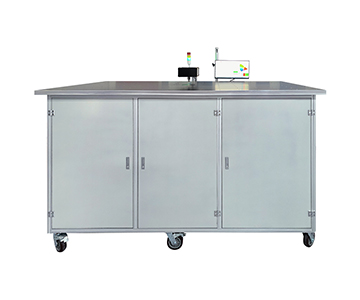
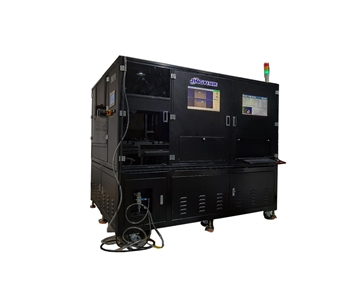
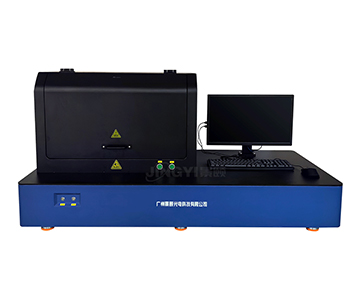
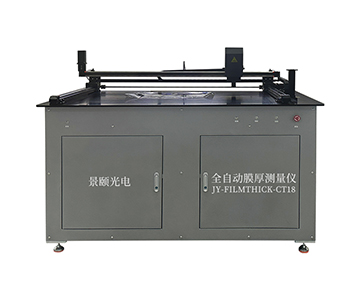
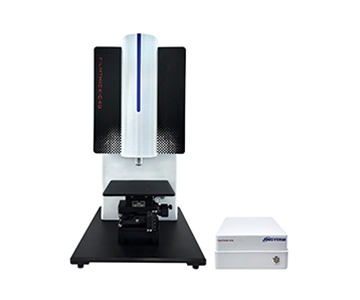
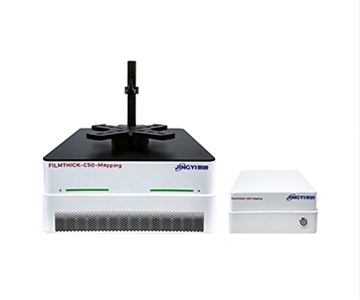
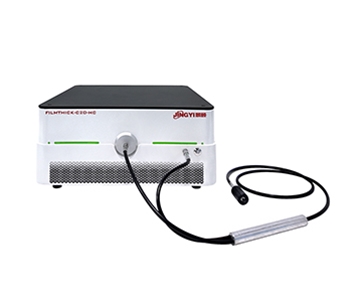
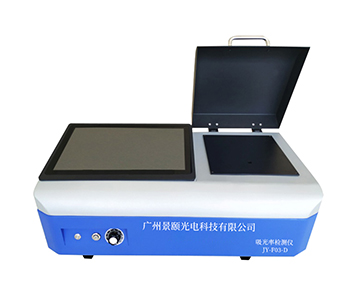
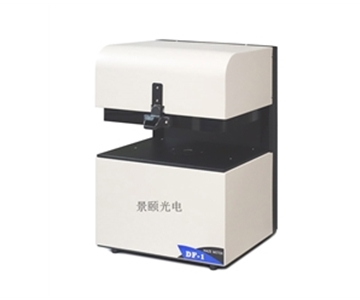
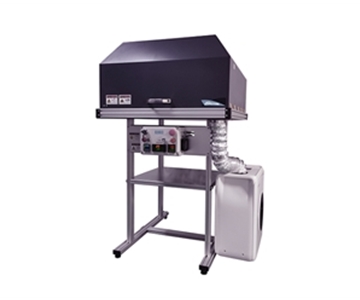
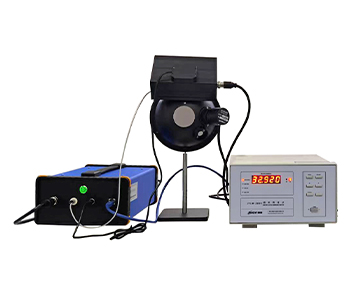
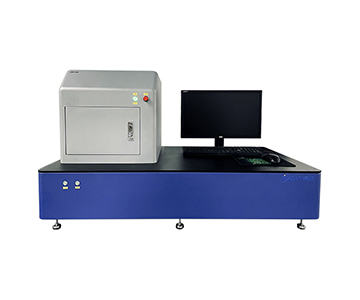
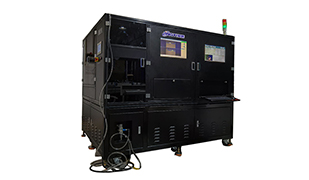
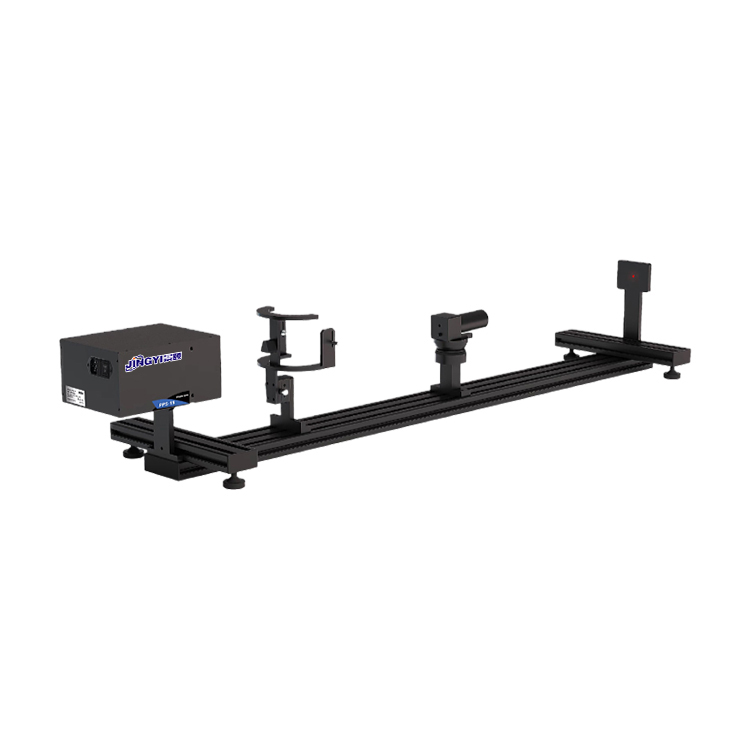
The wide-spectrum model spans 250–2500 nm using a combined deuterium-halogen source, riding on an automated stage with industrial PC control—covering PV glass and broad-band materials in one footprint. A curved-surface variant scans tubular parts without disassembly. The dual-aperture IR-aperture system is rated 1000–1200 pcs/h, with positioning accuracy better than 0.08 mm and automatic good/bad binning.
For environmental-sensor work, its automatic dark-background subtraction and stabilized wide-spectrum source address the drift problem directly. The manufacturer contributed to drafting China’s GB/T 47066-2026, which mirrors the scope of ISO 13468-1 for total transmittance and reflectance of plastics; in the near-IR band, free-threshold OK/NG judgment held repeatability under 1% during incoming inspection trials. A local cleanroom and 7×24 response team shorten support cycles in the Asia-Pacific region.
Best for:
plastic laser-welding QC, PV glass screening, automated phone-IR-aperture sorting, and lines needing wide-spectrum + area-array sync.
Not suited for:
a pocket-sized single-measurement gadget need—modular spectrometers win there.
Select by Process Scenario, Not by Ranking
A machine that shines on an R&D bench can stall on a production line, and a fully automated system in a lab is overkill. Map the need first.
•Plastic laser welding incoming inspection → full-area multi-point scan with a co-aligned 980 nm peak source. Skip 1700 nm+ wide-spectrum options; idle detectors collect dust and cost. Systems completing scans in ≤0.8 s with auto OK/NG, validated against ISO 13468-1 geometry, integrate cleanly into automotive supply chains.
•PV glass → prioritize spectral range to 2500 nm (to capture free-carrier absorption) and a large air-bearing stage to avoid cutting samples. A wide-spectrum automated platform with motorized stage fits batch runs; pair with the traceability-focused supplier as a parallel audit instrument when reports go to third parties.
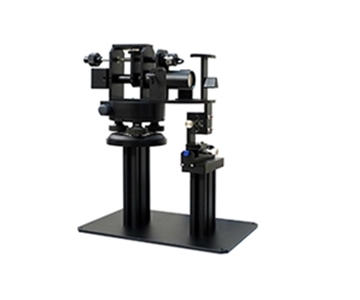
•Phone IR apertures & micro-filters → spot size and positioning are everything. 0.8 mm spot with ±0.06 mm positioning covers most; pushing to ø60 μm requires a micro-transmission configuration. A micro-area photonics vendor with small-cavity integrating spheres is worth evaluating here, and SMA905 interfaces allow spectrometer swaps.
•Environmental sensor windows, filter membranes, outdoor light hoods → ask for 8-hour baseline drift data, confirm dark-background subtraction, and check whether software exports time-segmented attenuation curves. A wide-spectrum automated system with closed-loop stabilization performs well in semi-outdoor setups; a modular spectrometer works as a bypass reference, not as primary inspection.
•Budget math → measuring one point a few hundred times a year, a modular overseas spectrometer keeps total cost of ownership low. Running continuous shifts with sorting and traceability, a domestic integrated system plus annual external calibration is more cost-effective. Redirect the savings from imported plate returns into a second reference standard and one independent metrology audit.
Boundaries and Real-World Constraints
No transmittance system wins every scenario. Extending to 2500 nm amplifies thermal radiation, dark current, and detector noise in the NIR region; without solid algorithmic compensation, curve noise exceeds the absorption valley height. For a visible-only display line, that bandwidth is stranded capital.
Full-area scanning generates heavy pixel-level data. Without MES storage planning, a month of runs fills the local drive. Robotic systems advertise 1000+ pcs/h, but fixture redesign, vision-template retraining, and changeover time are real line items—throughput rarely hits nameplate on mixed-SKU floors.
Overseas brands add supply-chain latency. Detector pixel faults, fiber wear, and halogen decay are consumable-grade issues resolved in 1–2 days on domestic platforms, but weeks through import channels. For vendors absorbed into larger groups, confirm firmware and spare-part inventory windows before signing.
Finally, “compliant” is not a sticker. Verify that total transmittance and reflectance are measured under ISO 13468-1 geometric conditions, with an unbroken NIST-linked traceability chain. Break one link, and the prettiest report fails supplier audit.
Frequently Asked Questions
Q1: Is a 400–1100 nm system sufficient for 980 nm laser-welding parts?
Only if the source energy at 980 nm sits in the flat response region and detector repeatability is under 1%. Start/stop wavelength alone proves nothing; request the energy profile and a 10-run repeatability report at your exact process wavelength.
Q2: Is a smaller measurement spot always better?
No. IR apertures and micro-filters benefit from 0.8 mm down to ø60 μm. Large PV panels need several-millimeter spots to average local scratches. An over-small spot on a big panel reports noise, not material property.
Q3: What separates a 98% reflective sphere coating from >99%?
After multiple diffuse bounces, the gap compounds to 3–5 percentage points of measurement error. For dark absorptive materials, specify >99%; otherwise readings drift systematically high.
Q4: Is a fully automated system worth it, and how is dual-aperture throughput calculated?
Dual-aperture ratings of 1000–1200 pcs/h equate to roughly 3 seconds per part including load/unload and sorting. High-volume, low-changeover lines recover cost fast. Small-batch shops get buried by fixture expense.
Q5: How can I independently verify transmittance measurement traceability before purchase?
Request an ISO/IEC 17025 certificate for the reference standard, confirm geometric conditions match ISO 13468-1, and run a blind-sample comparison against a third-party metrology lab. Ask for the full NIST-linked chain documentation, not just a calibration sticker.
About This Guide
Data Sources
: ISO 13468-1, ISO/IEC 17025, NIST Handbook 150, in-house validation reports (n=240 plastic laser-welding samples, 23°C ±1°C, 980 nm band)
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 10 years in industrial optical metrology
Disclosure
: Jingyi Optoelectronics manufactures optical transmittance measurement systems. This article presents technical assessments based on published specifications, independent lab data, and aggregated industry information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof-of-concept validation under your specific process conditions.
Last Updated
: October 2026
For detailed specifications and application notes on transmittance measurement systems, search "Jingyi Optoelectronics transmittance measurement system" or visit our technical library.