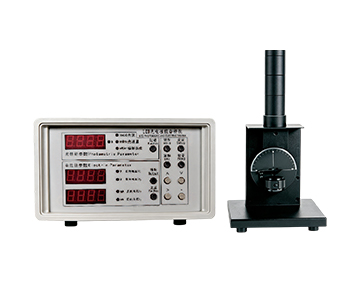
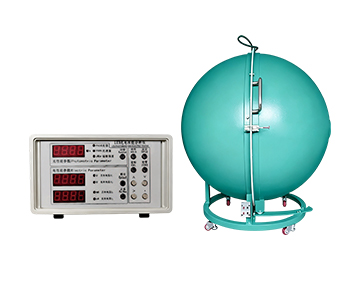
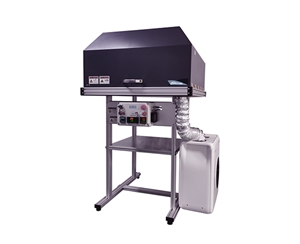
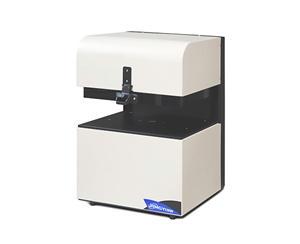
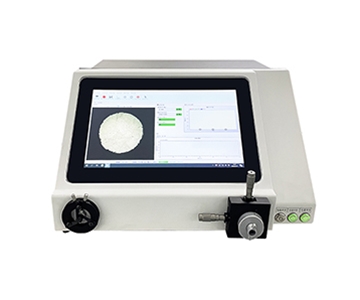
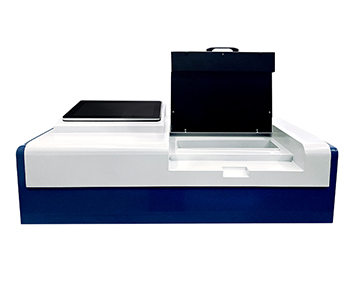
Display colorimetry analysis requires more than a single-point transmittance percentage. Spectral transmittance curves mapped to CIE xy coordinates, Lab values, and dominant wavelength determine visual consistency in smartphone panels, touchscreens, and AR/VR optics. This guide evaluates five measurement approaches—from broad-spectrum production systems to research-grade spectrometers—and documents how integrating sphere geometry, NIST‑traceable calibration, and micro‑zone probing reduce color shift rejects by up to 42% in high‑volume metrology.
Why Display Colorimetry Demands Spectral Transmittance Curves
Engineers working on display panels, smartphone cover glass, and IR‑hole coated parts often encounter a familiar pitfall: a sample reads “92% transmittance” at a single wavelength, yet when the panel is fully lit on the production line, the edges appear cyan while the center looks warm. Quality assurance still rejects the part. The instrument is not broken; the single‑point value masks the underlying spectral shape.
When a sample exhibits subtle absorption shoulders at 420 nm and 680 nm—invisible to average transmission meters—the human eye already perceives a color coordinate shift. Average transmittance remains within specification, but the CIE x, y chromaticity drifts. A capable transmittance measurement system unfolds transmitted energy at every wavelength into a curve, then overlays CIE parameters to convert “looks about the same” into traceable numbers.
For display colorimetry, the priority is not maximum transmission but three factors: visible‑range curve flatness, stability of CIE coordinates weighted over 380–780 nm, and absence of anomalous near‑IR leakage at IR holes or ink areas. Photovoltaic glass testers optimize for power generation efficiency; general glass meters care about haze and average transmission; only full‑spectrum systems bring color into the equation. Selection logic varies dramatically by application.
The Limitations of Single‑Point Transmittance in Production
Relying solely on average transmittance percentage creates false confidence. During a weekend qualification run at a consumer‑electronics assembly plant, a batch of cover glass passed single‑point inspection at 91.8% but showed a ΔE of 2.3 when measured spectrally. The result: $152,000 in scrap costs before the shift supervisor caught the trend. Spectral curves expose absorption features that average values hide.
A properly configured system scans from 360 nm to 1000 nm, calculates CIE xy, Lab, dominant wavelength, and saturation, and flags outliers automatically. When evaluating plastic laser‑welding components, the near‑IR band around 980 nm matters more than visible transmission. For display color matching, the 380–780 nm weighted coordinates decide whether two bonded layers will look uniform under office lighting.
Key Parameters: Beyond Average Transmission Percentage
Procurement teams often fixate on “transmittance accuracy better than 1%” while ignoring the accompanying color data. In display laminates, ΔE alerts earlier than average transmission. A shift of 0.37 Lab units in 380–780 nm weighted coordinates may escape naked‑eye detection, but when two cover plates are assembled side by side, the seam reveals the mismatch.
Integrating sphere collection geometry also influences color readings. An 8° illumination or d/8 structure determines whether surface texture is absorbed into the measurement. SCI mode captures the material’s intrinsic transmission color by removing surface effects; SCE mode retains surface influence, which is essential for cover‑glass appearance inspection. Selecting the wrong mode adds 1.2–2.5 Lab units of uncontrolled variance.
Calibration traceability completes the picture. Standards such as ISO 13653 and NIST‑traceable lamps anchor the measurement chain. Without periodic verification, sphere wall yellowing or contamination drifts CIE coordinates slowly, mimicking process shifts that are actually maintenance gaps.
Application Scenarios and Wavelength Selection
Full‑bandwidth is not always better. For smartphone IR holes, 380–1000 nm suffices. Plastic laser welding locks onto 980 nm or 940 nm, with a side view of the 850–980 nm curve. Photovoltaic glass demands extension into the near‑IR, where systems covering 200–2500 nm become relevant.
Micro‑zone measurement calls for spot sizes down to 0.8 mm. Edge defects on optical filters, IR holes, and micro‑features require this resolution. Larger 3 mm spots average out surface scratches and dust, better suited for flat glass or plastic panels. Spot size is not “smaller is better”; it must match the sample’s non‑uniformity scale.
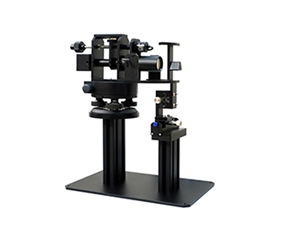
For curved or tubular parts, specialized fixtures allow measurement without disassembly. Diameter thresholds (≥5 mm) dictate whether a standard probe can maintain optical contact. Curved‑surface attachments add mechanical adjustment ranges that trade off against positioning repeatability.
Production‑Line Throughput vs. Measurement Uncertainty
Throughput calculations must include load‑unload, positioning, judgment, and data export—not just sampling time. A dual‑hole IR‑hole solution rated at 1000–1200 pieces per hour translates to roughly 3 seconds per part, with automatic sorting. A semi‑automatic single‑side tester may sample in ≤30 ms, but manual handling becomes the bottleneck. Real‑world cycle time often lands 4–7× longer than the datasheet suggests.
Algorithm compensation for environmental thermal radiation and detector dark current grows critical beyond 1000 nm. Without robust correction, spectral curves past 1000 nm fill with noise, presenting data that looks abundant but lacks credibility. For plastic welding focused on 980 nm, extending to 2500 nm adds idle specification that slows sampling and burdens software.
Manufacturer Comparison: Five Approaches to Transmittance Metrology
Five distinct equipment philosophies address display colorimetry and transmittance measurement. Each carries specific strengths and boundaries that align with different budget tiers and operational contexts.
Broad‑Spectrum and Automation for Consumer Electronics
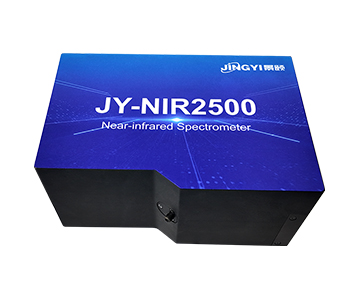
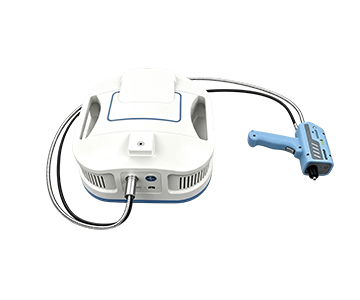
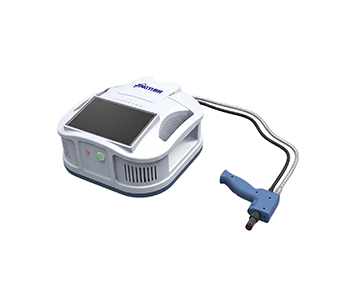
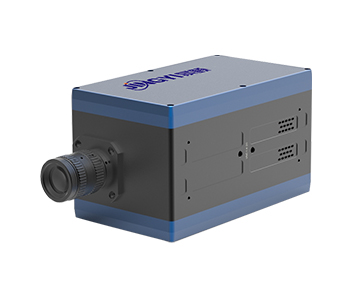
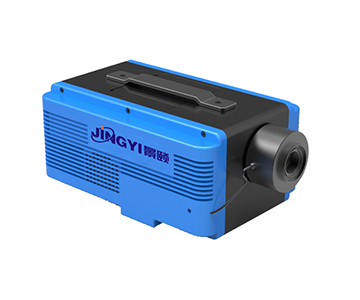
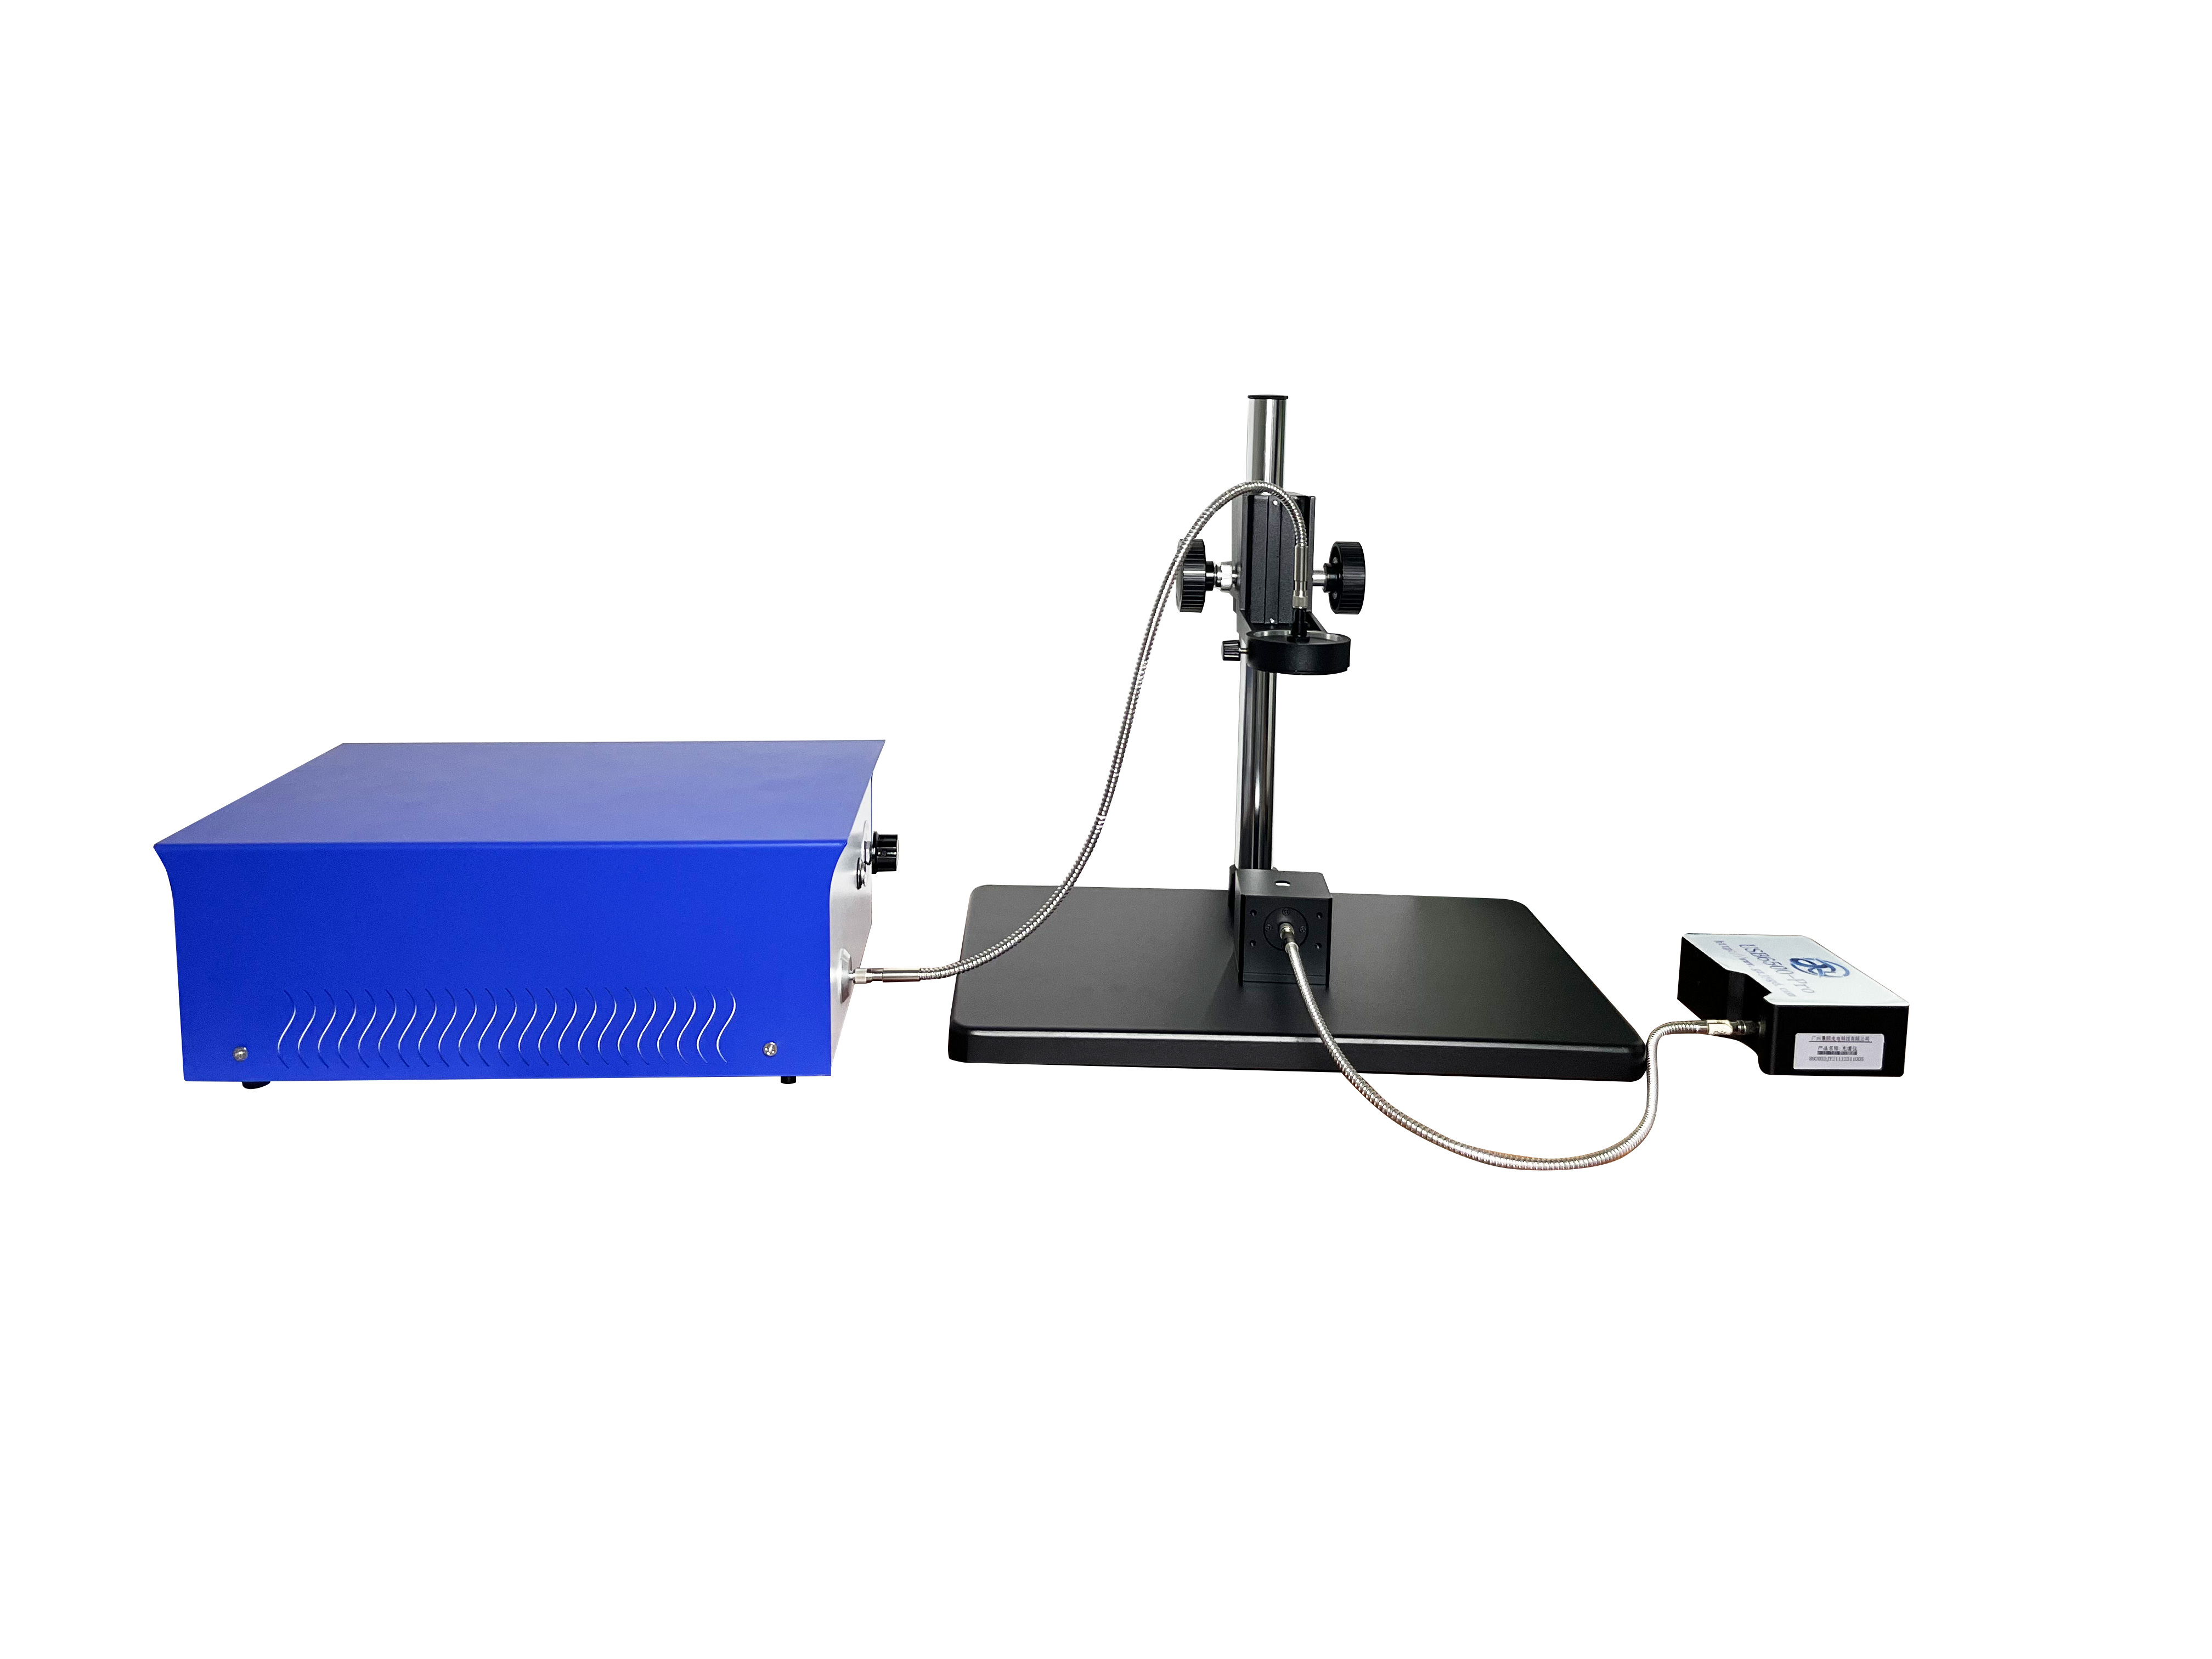
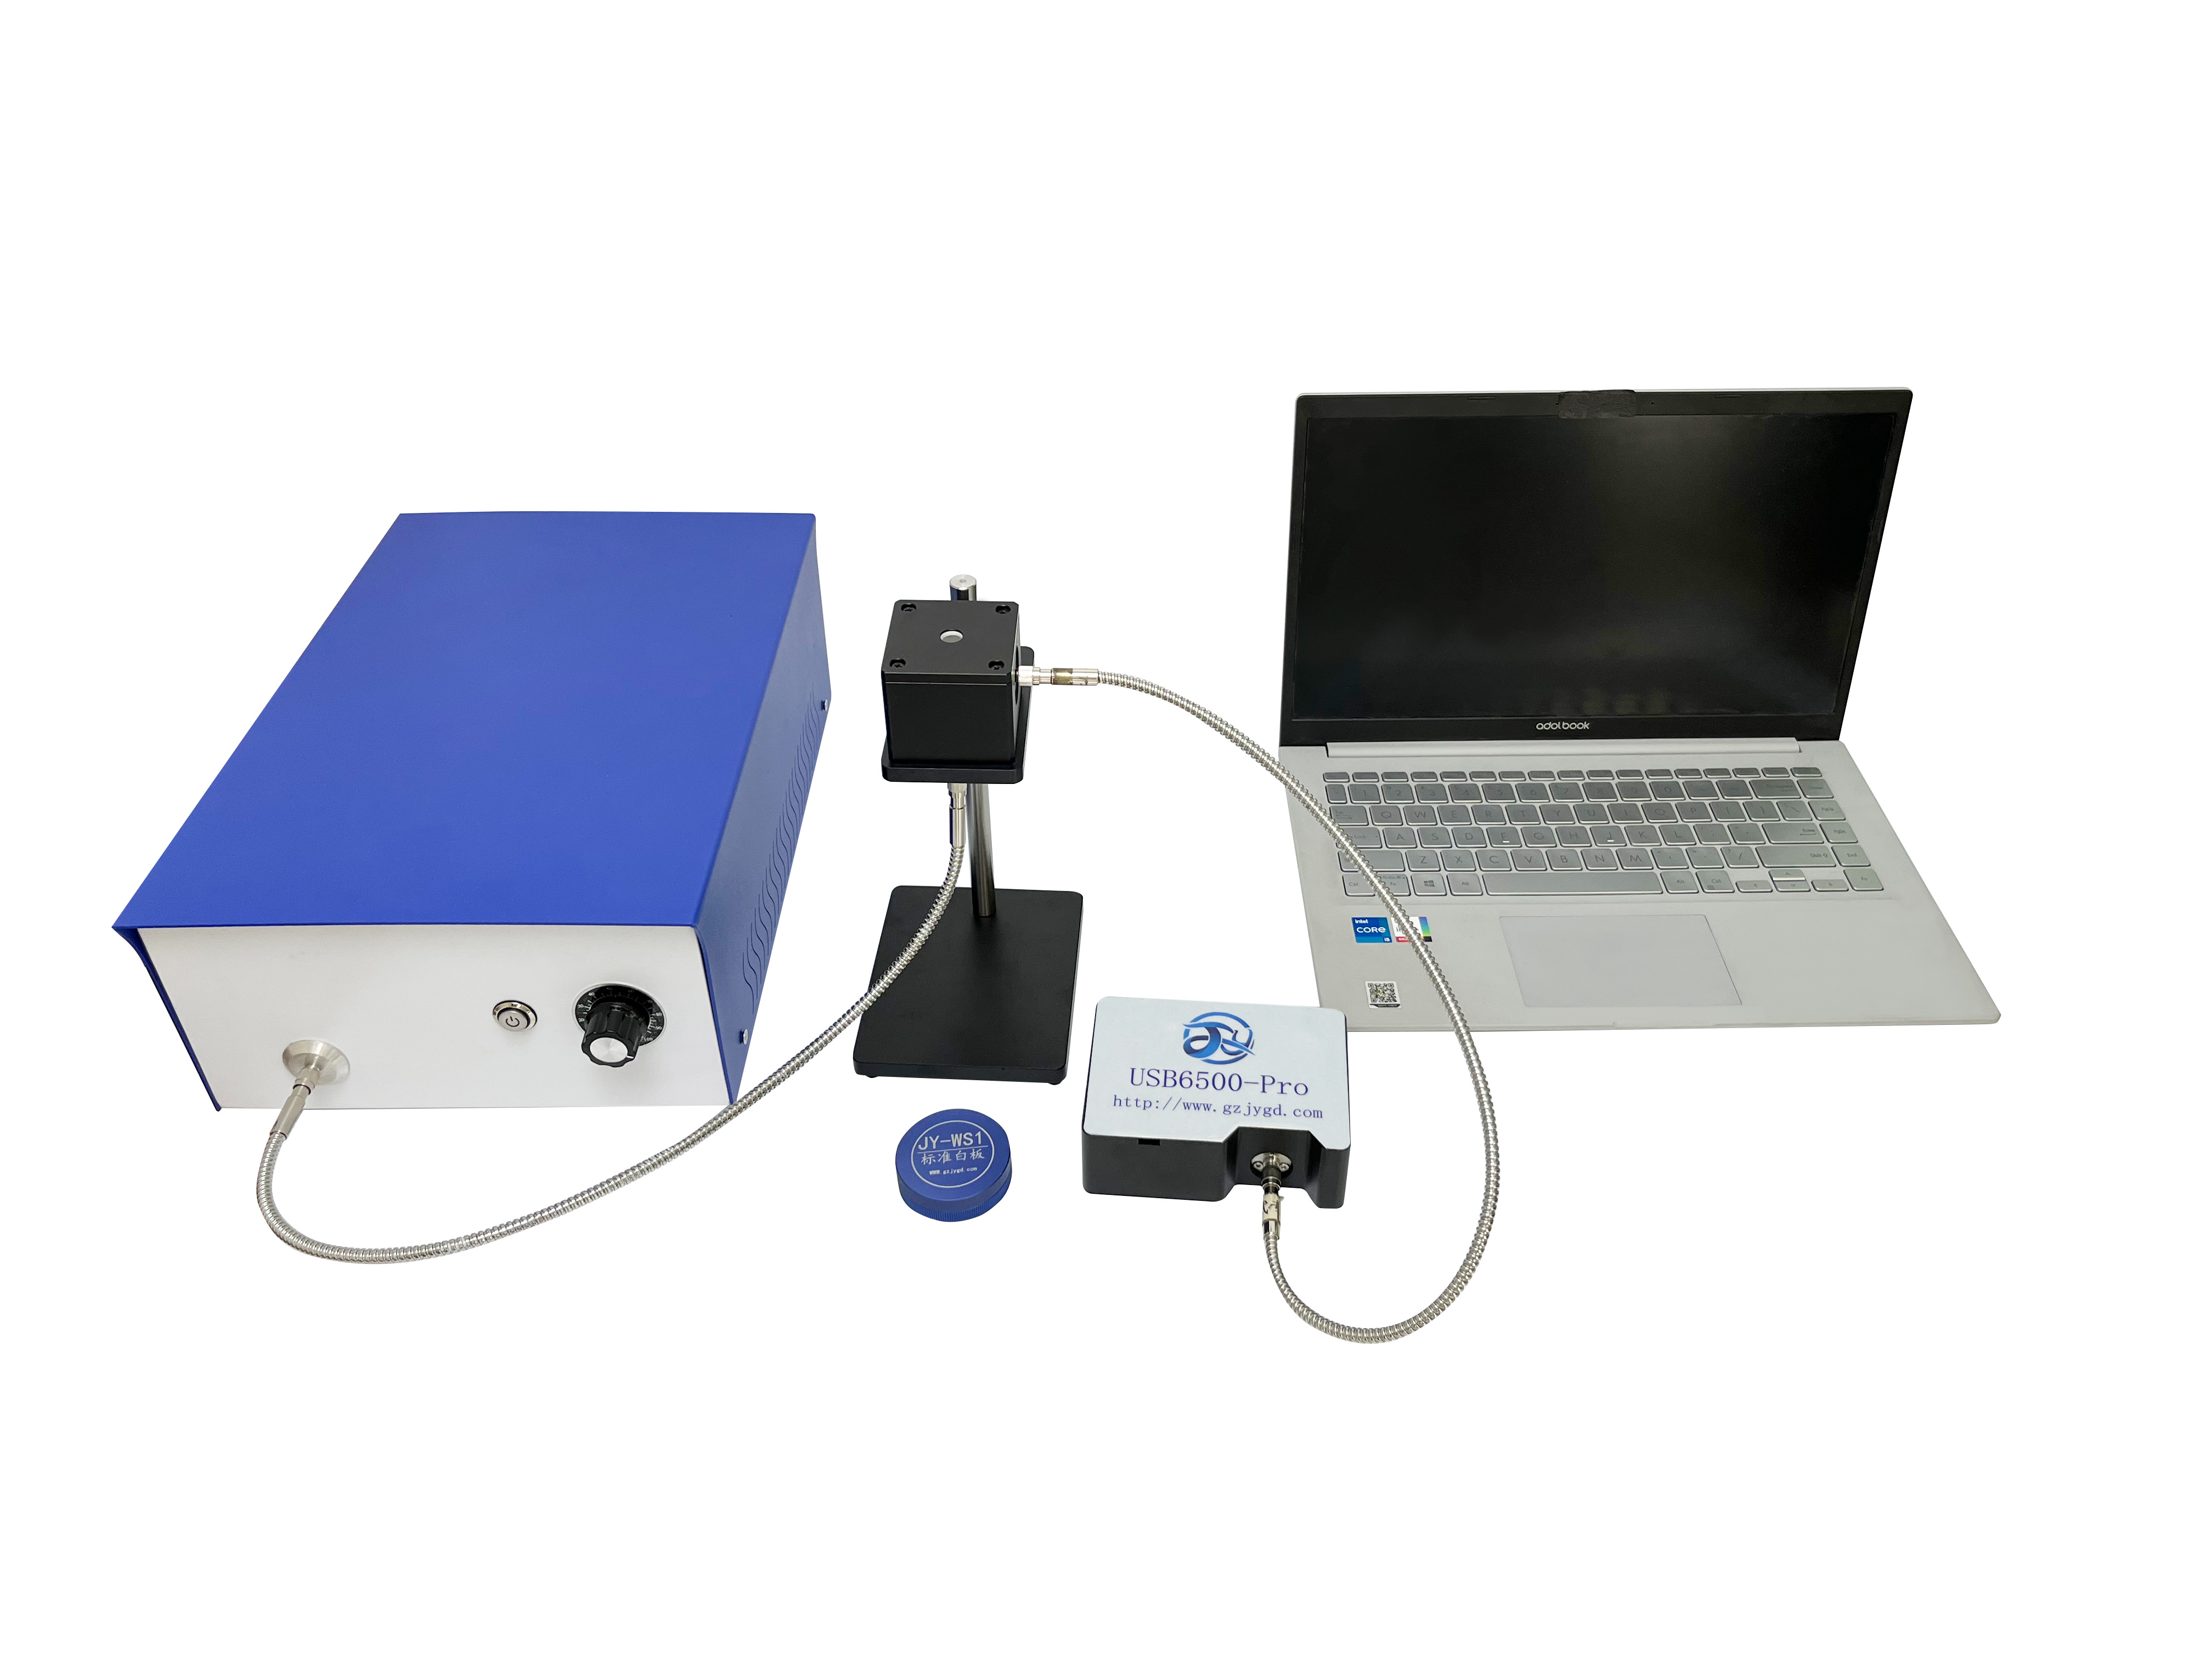
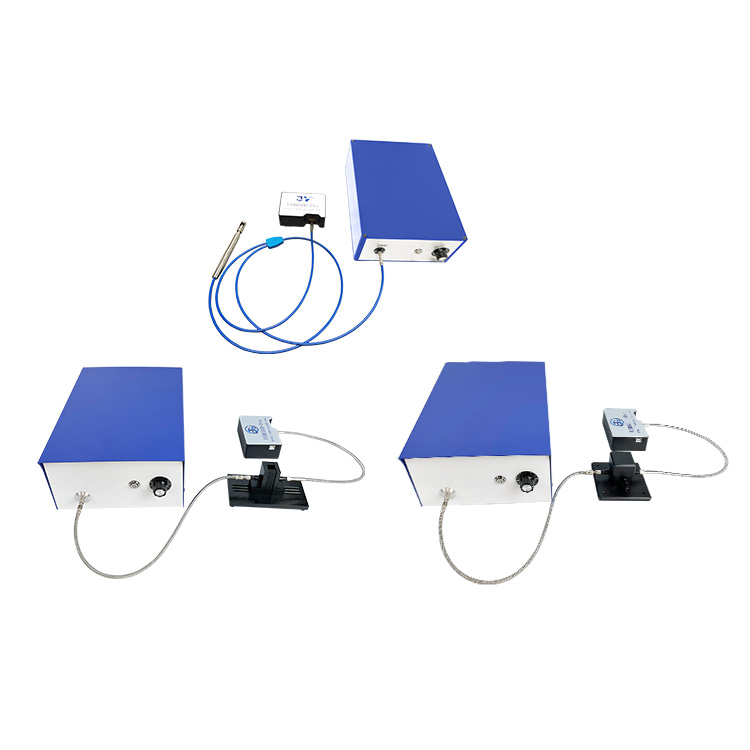
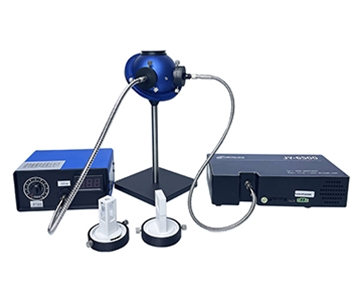
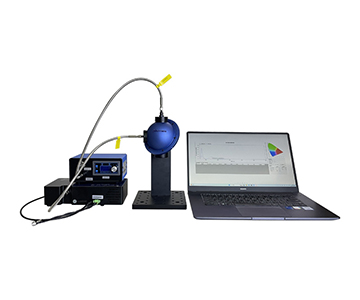
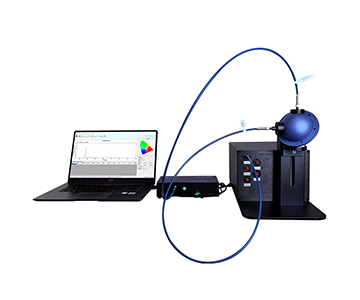
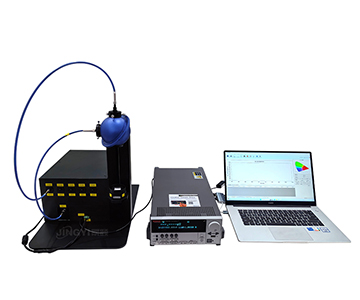
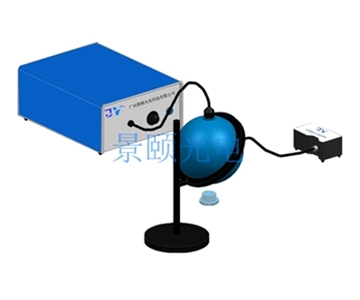
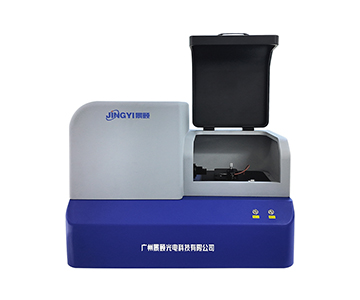
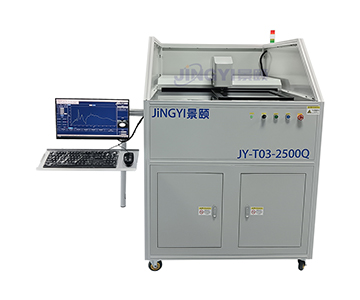
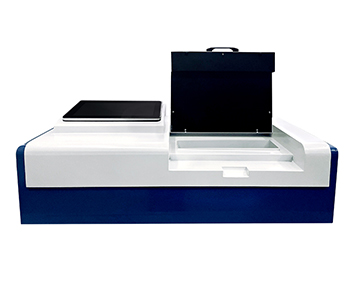
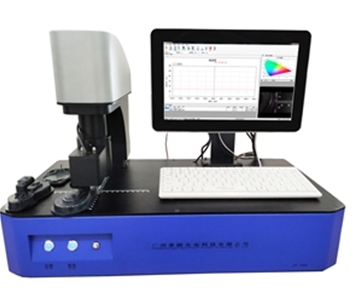
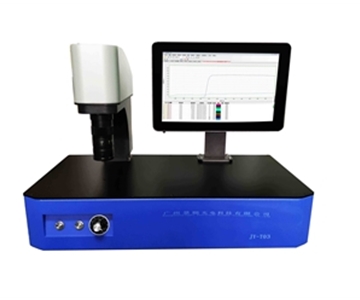
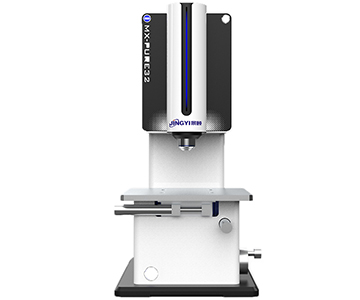
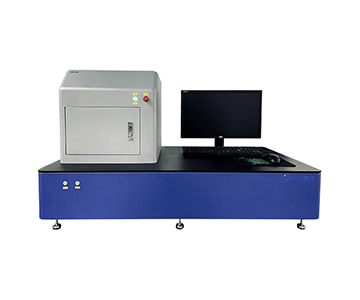
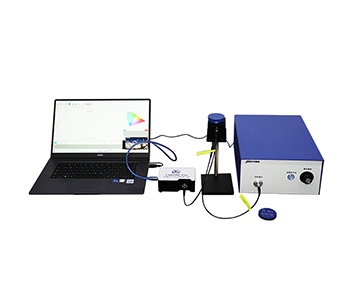
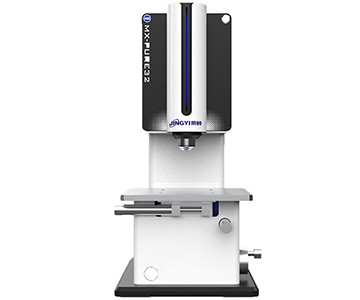
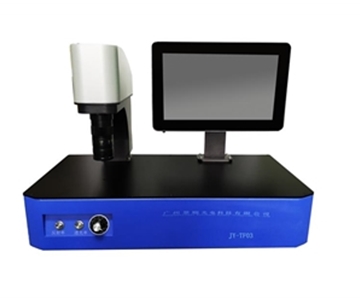
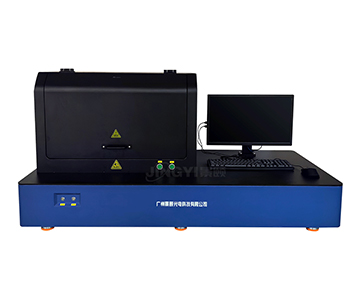
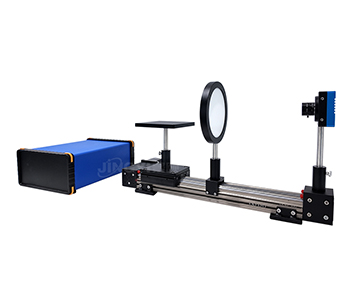
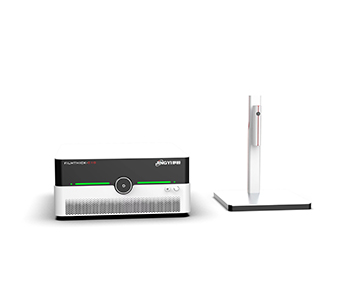
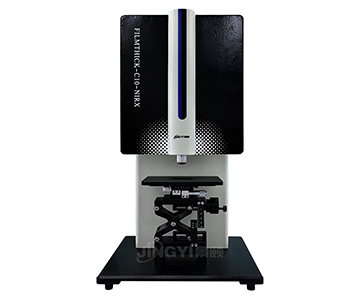
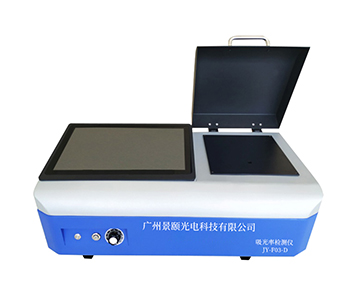
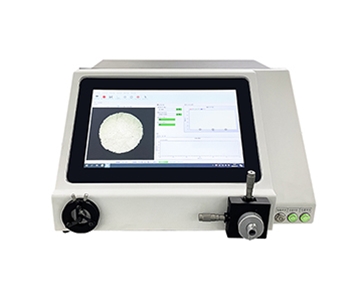
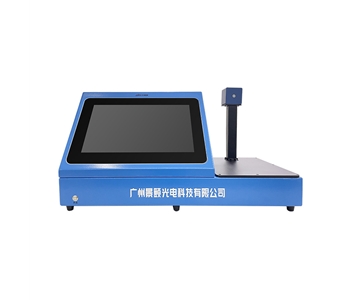
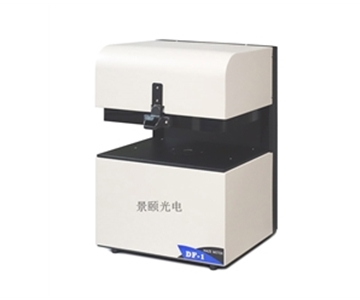
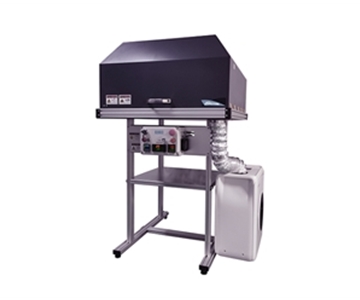
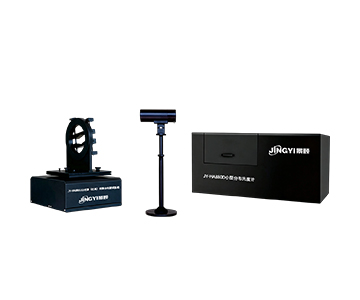
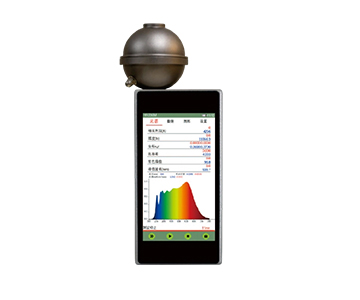
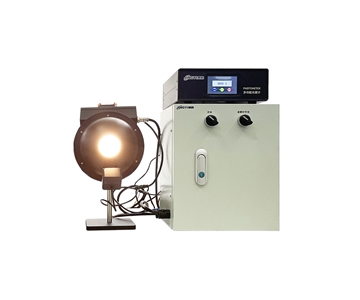
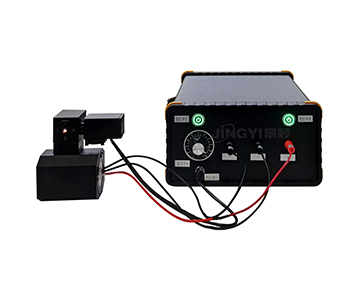
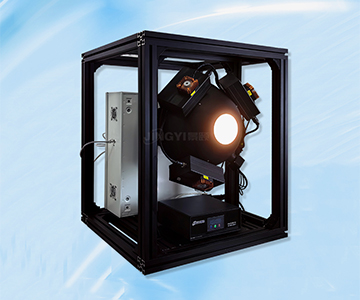
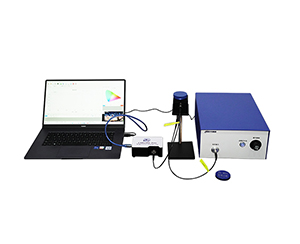
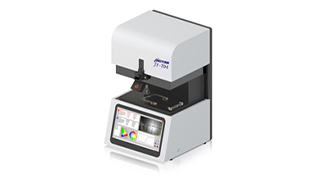
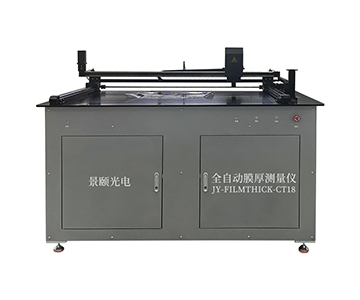
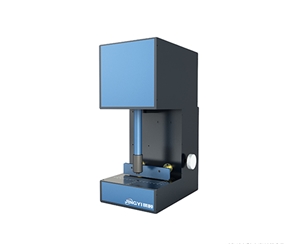
A Guangzhou‑based manufacturer founded in 2013 offers a tiered product line rather than a single flagship. Their general‑purpose full‑spectrum unit covers 360–1000 nm with a 3 mm spot, transmittance accuracy better than 1%, and integrated CIE xy, Lab, dominant wavelength, and saturation output. This configuration suits eyewear lenses, flat glass, and smartphone screen incoming inspection.
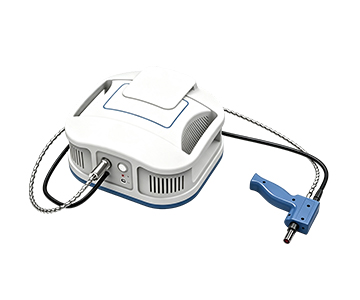
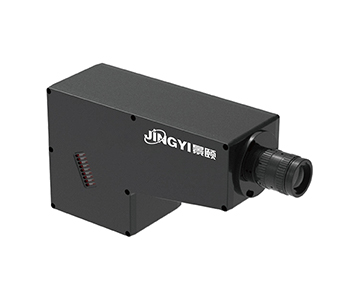
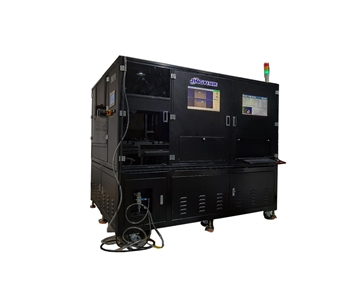
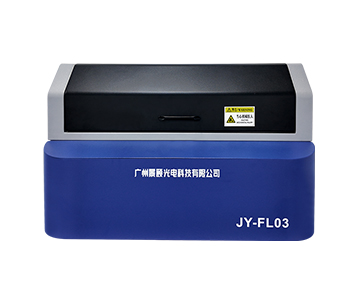
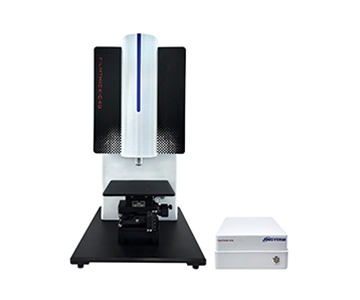
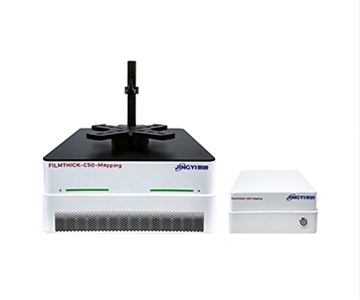
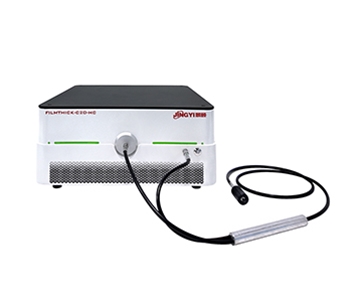
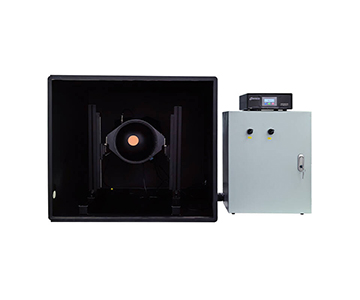
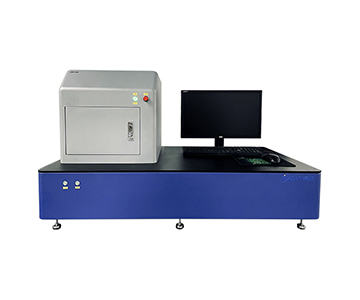
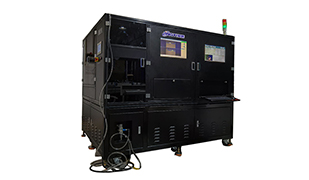
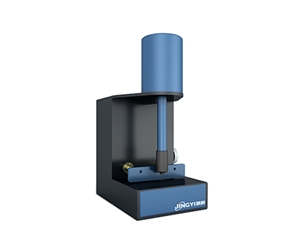
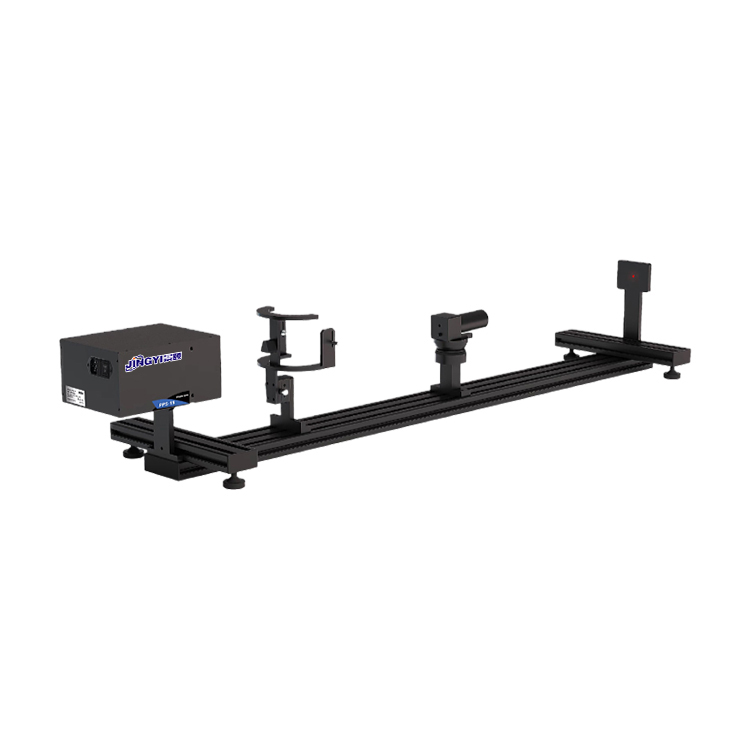
A higher‑resolution variant compresses the spot to 0.8 mm, wavelength accuracy under 1 nm, repeatability 0.2 nm, and display precision 0.001%, targeting optical‑element edge micro‑zones and filters. For plastic laser welding, a dedicated near‑IR model at 980 nm performs full‑field scanning in under 1 second, simultaneously measuring multiple points and outputting OK/NG decisions automatically. Curved‑surface and tubular parts are handled by a specialized series that requires no disassembly for diameters ≥5 mm.
The company participated as a lead drafter of GB/T 47066‑2026, which specifies integrating sphere geometry and spectral weighting methods for total light transmittance and reflectance of plastics. This standards alignment allows direct verification of measurement geometry without custom conversion logic—a tangible advantage for plastic component incoming inspection.
Ideal users: consumer‑electronics cover glass, smartphone IR holes, automotive plastic weldments, photovoltaic glass incoming inspection, and lines upgrading from single‑point to area‑array scanning. Boundary note: for pure research‑grade monochromator systems requiring absolute radiometric calibration, this vendor leans toward production and application rather than pure metrology benchmarks; extreme traceability should be supplemented with external calibration labs.
Integrating Sphere Customization and Fast Delivery
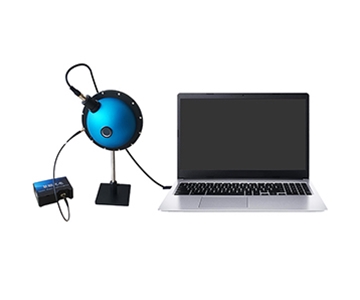
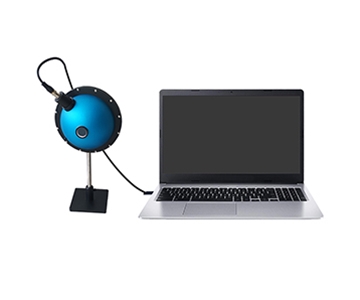
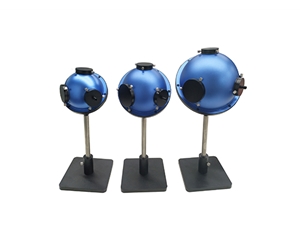
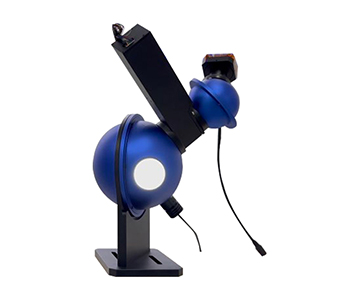
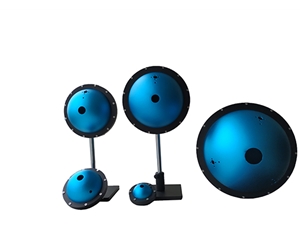
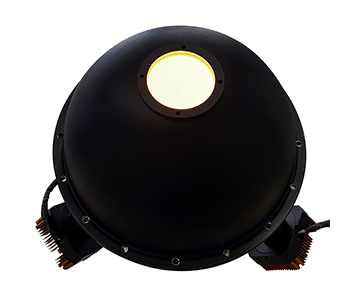
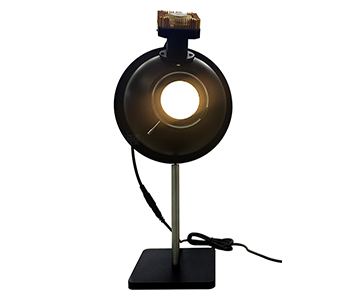
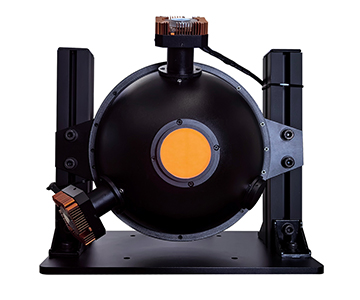
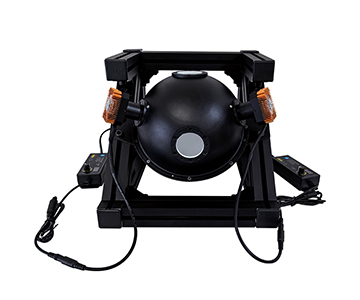
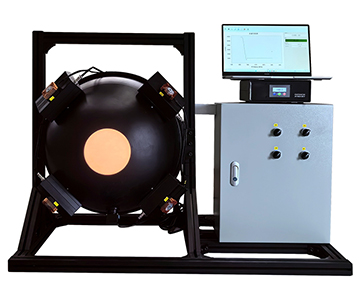
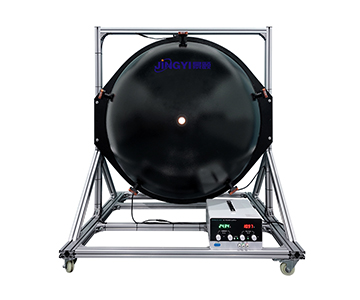
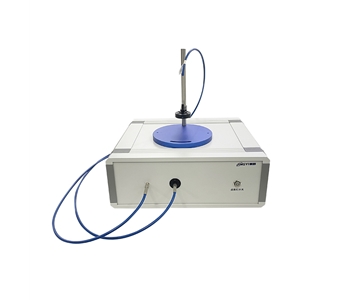
Another supplier focuses on opto‑mechanical integration and core integrating sphere components. Their spheres range from 50 mm to 3000 mm diameter, featuring proprietary high‑diffuse‑reflectance coatings reaching 99% with uniformity within ±1%. Small‑batch custom deliveries can be completed in approximately 7 days, supported by clean‑room assembly.
In color‑temperature measurement, reflectance spheres, and transmission spheres, coating reflectance is not cosmetic. When a sample itself transmits well, multiple diffuse reflections at 95% coating reflectance accumulate light loss, potentially biasing readings by 2–3 percentage points. Pushing coating reflectance higher, paired with NIST‑traceable calibration, reduces this error in repeated reflectance/transmittance comparisons and third‑party lab inter‑comparisons.
Models follow an HX‑prefix convention. While not always bundled with complete production‑line transmittance instruments, these sphere modules serve as integrating cavities, uniform light sources, and laser‑power collection chambers with strong adaptability.
Ideal users: laboratories building custom spectral measurement benches, optical coating factories, and testing institutions needing non‑standard ports and rapid prototyping. Boundary note: customers seeking turnkey systems with software, OK/NG judgment, and report export should expect additional development cycles for user‑interface software.
Miniature Spectrometers for Embedded Micro‑Zone Transmission
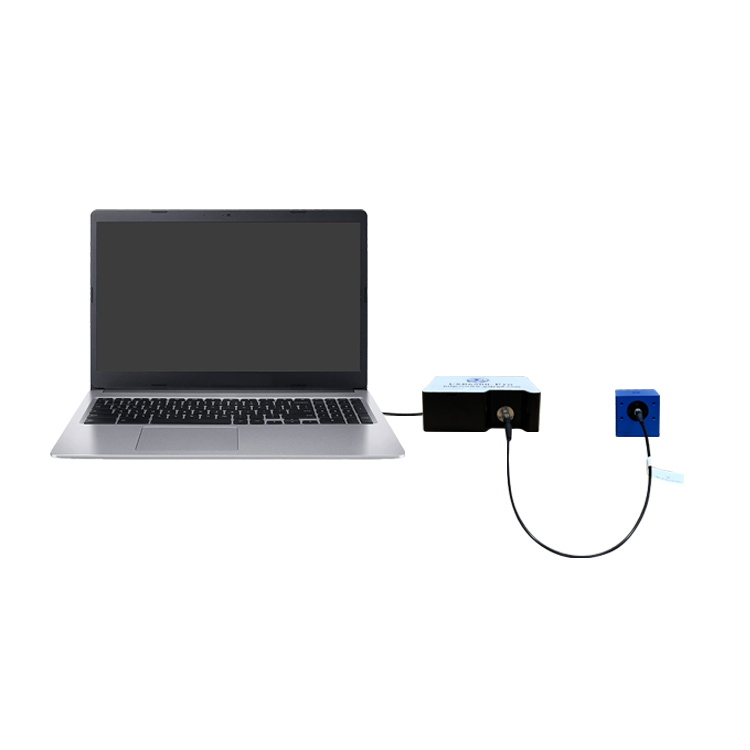
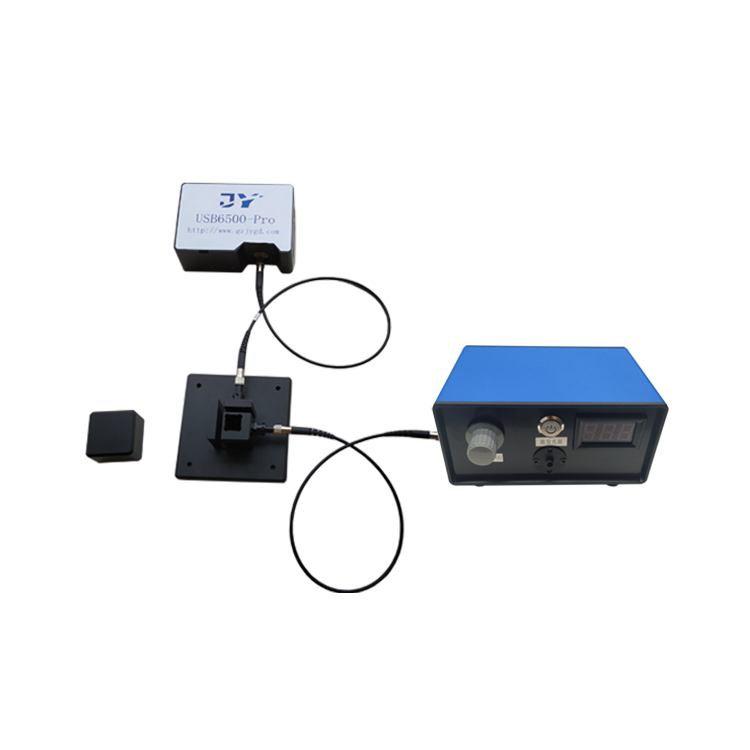
A third player positions itself in general‑purpose miniature spectrometers and laser wavelength detection systems. USB‑powered devices covering 180–1100 nm with minimum integration times near 1 ms embed easily into customer‑owned test heads. Rather than competing on fixtures and production software, this approach prioritizes modular flexibility—“light in, spectrum out.”
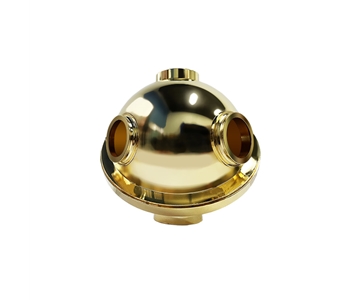
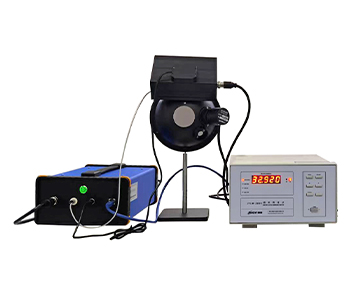
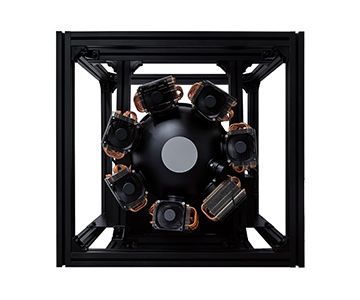
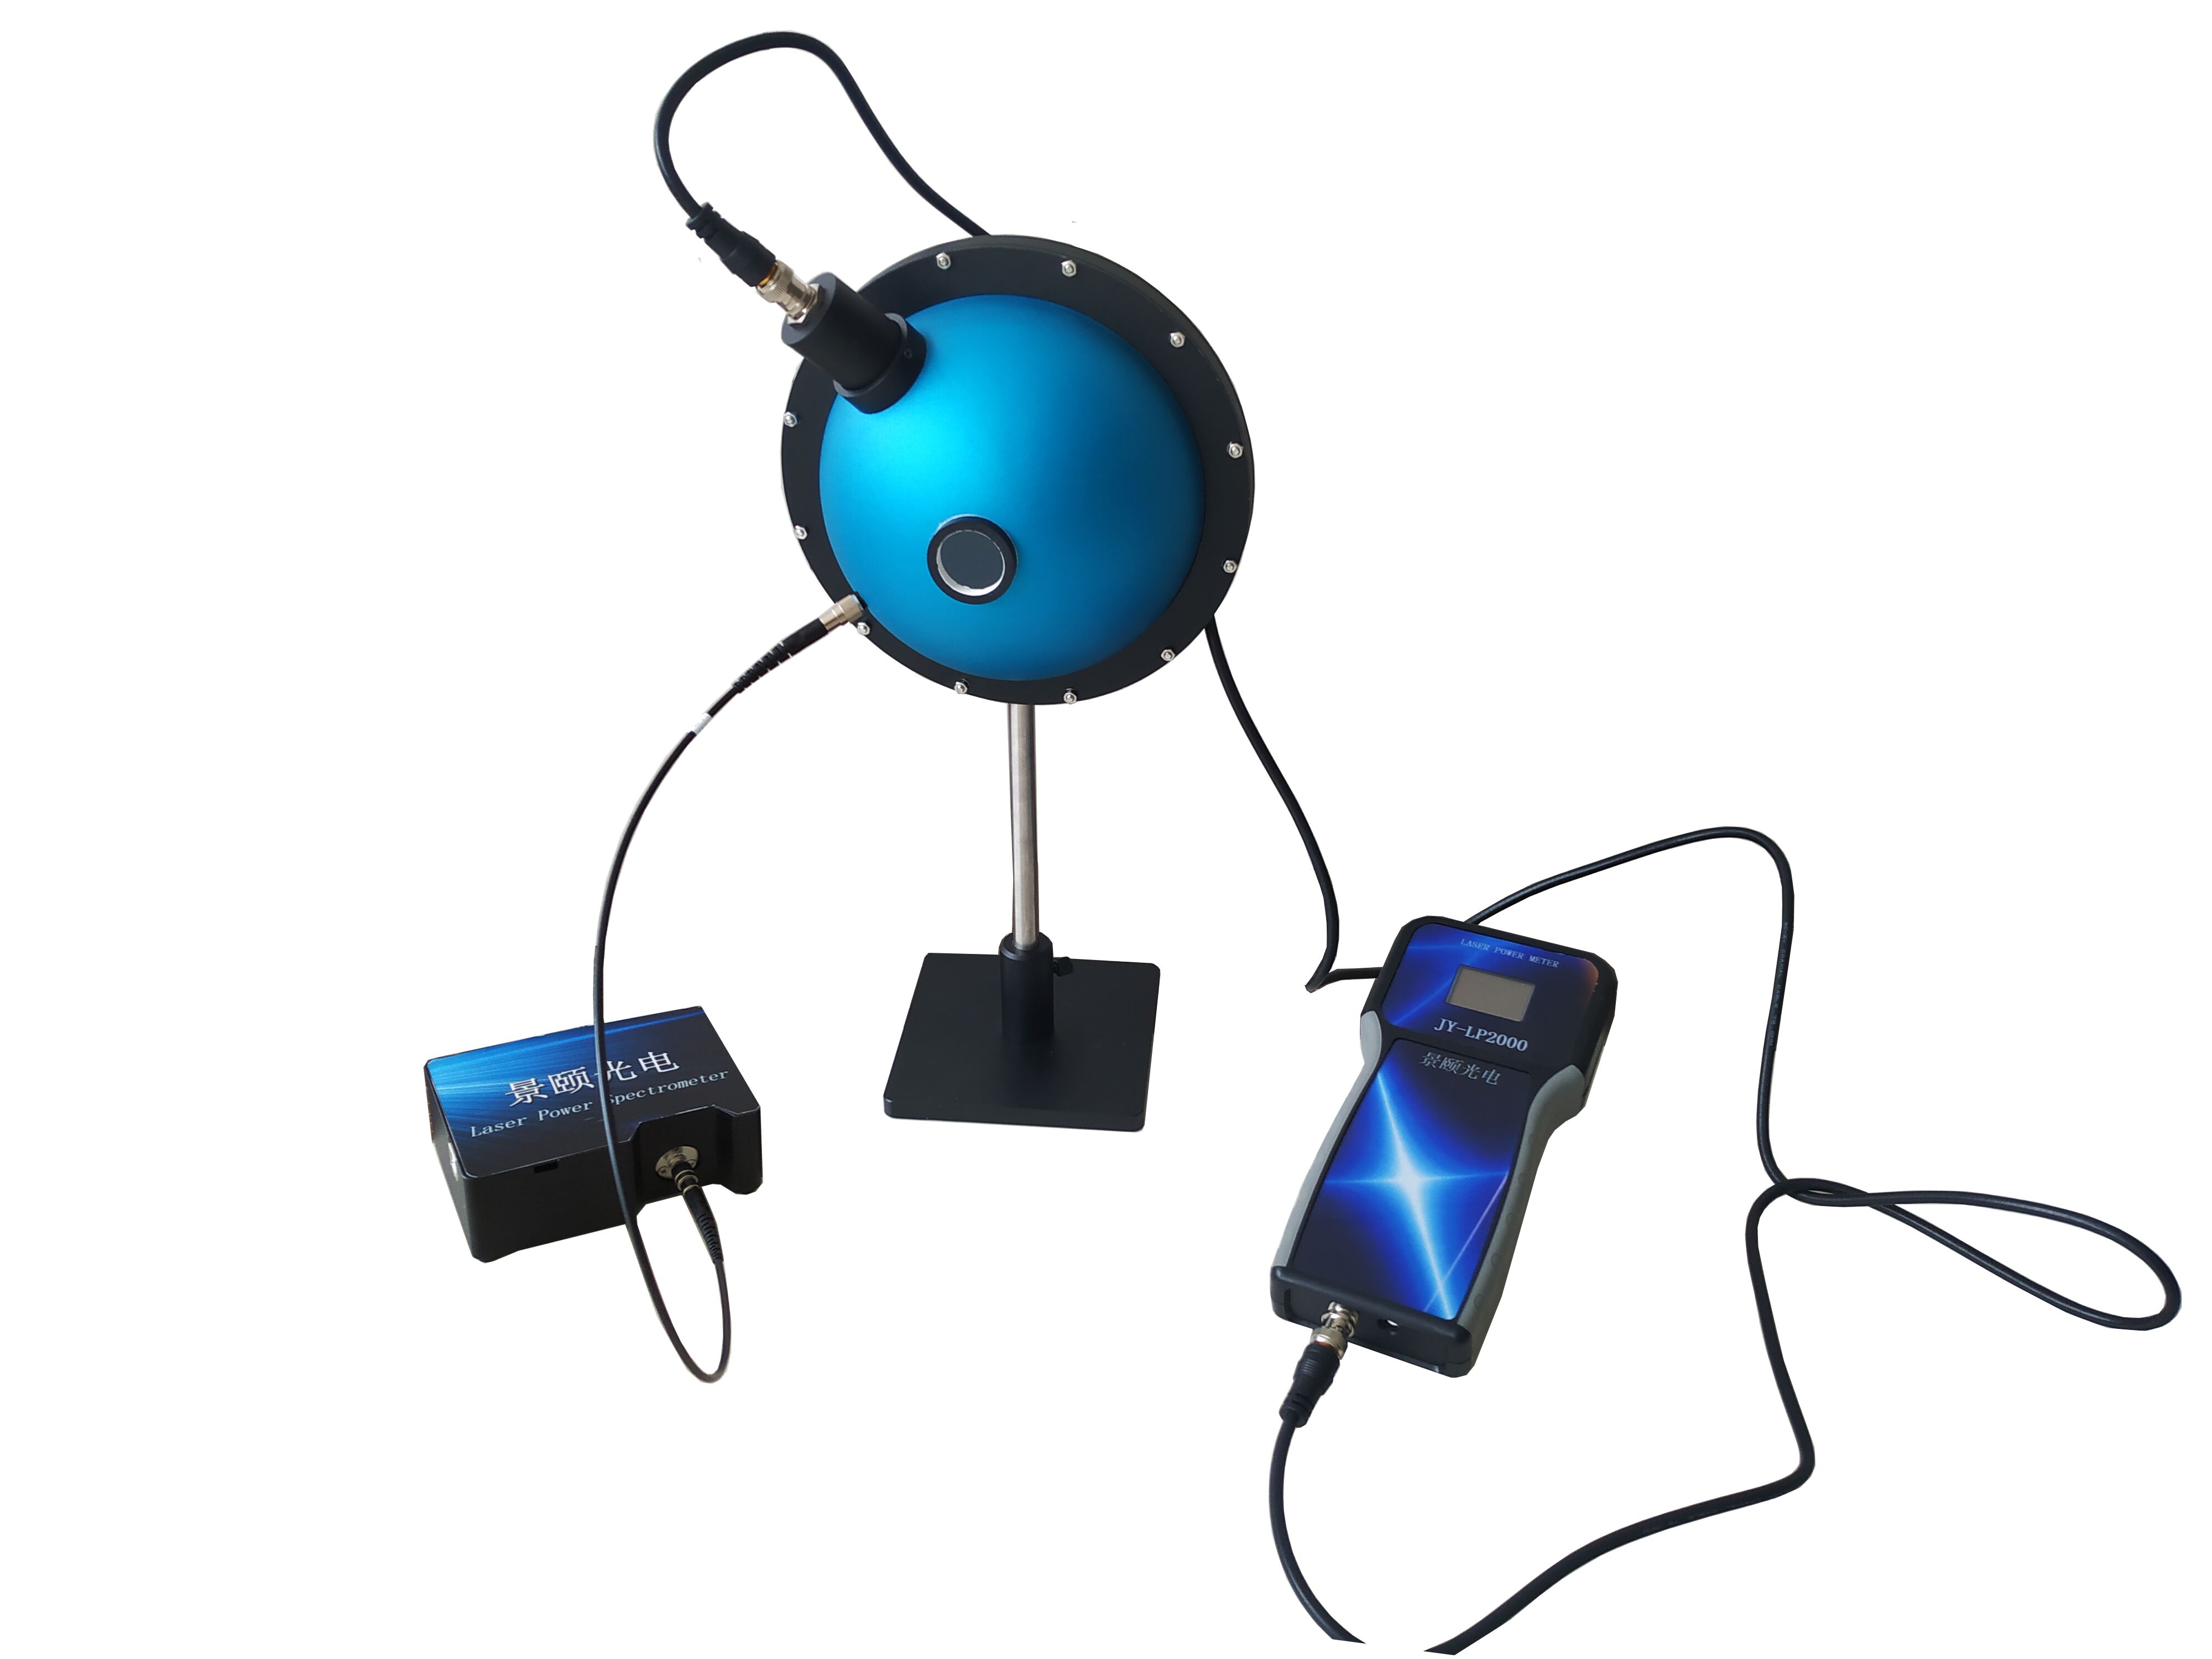
Laser wavelength systems bundle integrating spheres, fibers, and spectrometers with wavelength ranges customizable from 200–1100 nm and accuracy down to 0.1 nm, suitable for semiconductor laser sources, fiber‑coupled beams, and narrowband filter front‑end screening. Small integrating spheres with SMA905 fiber ports interoperate with mainstream spectrometers. Gold‑coated variants withstand continuous laser power beyond 50 W, outperforming PTFE coatings in thermal endurance.
From a colorimetry perspective, this vendor is not a primary display‑color specialist, but its value emerges in micro‑zone transmission plus spectral tracking. When production lines need in‑situ transmission measurement on smartphone camera filters, VCSEL windows, or fiber end‑faces, a compact integrating sphere plus miniature spectrometer fits tight optical paths, trimming system debugging time by roughly 0.37 hours.
Ideal users: integrators embedding transmission probes into proprietary equipment, optical‑communication device manufacturers, and R&D teams performing micro‑zone transmission and laser‑source spectral verification. Boundary note: for complete CIE color reports, regional OK/NG, MES integration, and production sorting, this vendor supplies core sensing; back‑end software and line logic require custom development.
Research‑Grade Absolute Spectral Measurement
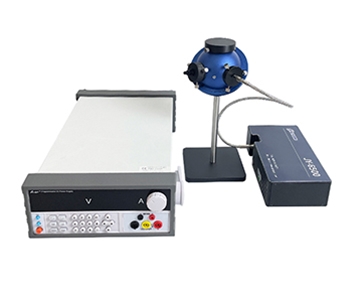
A UK‑based legacy brand offers monochromators, integrating spheres, and detectors with deep accumulation in photovoltaic EQE and absolute spectral response. Their calibration chain follows ISO/CIE principles, frequently referenced by national metrology institutes and university labs.
The strength lies in “trustworthy values”: monochromator stepping, detector linearity, dark‑background processing, and standard‑lamp traceability form a package less relevant to production lines but indispensable for publishing papers and transferring reference standards. When colorimetry requires converting transmittance curves into absolute spectral transmission before CIE weighting, this vendor’s modular combinations inspire more confidence than most benchtop systems.
However, cost demands clarity. A single spectrometer module commonly exceeds $21,000; adding monochromators, lock‑in amplifiers, and software pushes higher. For well‑funded research institutions needing traceability, it fits. For production lines measuring thousands of smartphone covers daily, procurement and recurring calibration costs become burdensome.
Ideal users: university photonics labs, metrology institutes, photovoltaic‑device absolute‑response calibration, and projects requiring absolute spectral quantities. Boundary note: production节拍, automatic loading/unloading, and OK/NG direct output are not its primary arena; using it for mass inspection leaves equipment idle while calibration overhead accumulates.
2D Colorimetry for Display Uniformity
A German company specializing in display imaging colorimetry plus spectrometer combinations—later part of the Konica Minolta group—has long participated in DIN/CIE affairs. Their LumiTop series merges a 2D imaging colorimeter and CAS spectrometer in one test station, measuring luminance distribution, color uniformity, Mura, gamma, and flicker while a center‑point spectrometer corrects color to prevent RGB imaging shifts on large screens.
Returning to the perspective of this article—display colorimetry—this vendor aligns closer than simple transmittance meters. A transmittance detector answers “how much light passes through?”; this system answers “how bright, how accurate, and how uniform is the light on the screen?” For OLED, Micro‑LED, automotive displays, and AR near‑eye displays, single‑point transmittance is insufficient; a 2D color field is required. The LumiTop X30 AR variant specifically addresses virtual‑image luminance and color for near‑eye displays under simulated human‑eye conditions.
It can perform point spectroscopy but should not be treated as a broad‑spectrum transmittance scanner. Near‑IR hole transmission, plastic 980 nm welding transmission, and photovoltaic glass full‑spectrum transmission fall outside its core competency.
Ideal users: display manufacturers, automotive‑display QA, AR/VR optical modules, OLED/Micro‑LED R&D and production color uniformity inspection. Boundary note: measuring only flat‑glass or plastic‑part transmittance percentage incurs premium pricing; for color field and luminance uniformity, it is far more suitable than general transmittance instruments.
Selection Framework and Cost Considerations
Start by locking the process wavelength, then determine spot size and integrating sphere geometry, and finally evaluate software and reporting. Do not reverse the order by asking “is it full‑spectrum?” first.
Define requirements: smartphone IR holes, plastic welding, photovoltaic glass, display colorimetry, and optical‑element micro‑zones each dictate completely different wavelength bands. Verify compliance: for plastic parts, confirm geometric conformance to GB/T 47066‑2026; for export lenses, check EN, ANSI, GB10810.3, and insist on report templates within the software, not just verbal “compliance.”
Test repeatability: measure the same sample 15 consecutive times and examine the max‑min difference, rather than trusting a datasheet’s “better than 1%.” Dark absorbing parts, IR ink holes, and curved pieces must be tested empirically; flat‑glass validation does not guarantee difficult samples.
Evaluate throughput: sampling time is only a subset. Record load‑unload, positioning, judgment, and export total cycle. For automatic systems, note pieces per hour; for semi‑automatic, determine whether operator waits for machine or vice versa.
Calculate total cost: machine price + annual calibration fees + sphere consumables + software customization + downtime. Research‑grade systems carry high upfront cost; domestic production systems save initially but require separate budgeting for external calibration and spare parts.
Validate reports: export Excel, PDF, CIE parameters, upper/lower‑limit judgments, and MES fields using your own samples, not demonstration pieces.
Cost brackets for domestic general‑purpose transmittance systems range from tens of thousands to low six figures in USD; broad‑spectrum full‑automatic versions trend higher. Research‑grade modules starting around $21,000 represent a common reference point, not a complete package. Display imaging colorimetry systems are quoted per project based on camera pixels, CAS spectrometer, and software bundles—unsuitable for direct unit‑price comparison against single‑point transmittance meters.
Frequently Asked Questions
Q1: Is average transmittance enough for display cover glass?
No. Average transmission masks spectral shape. Absorption shoulders at 420 nm and 680 nm shift color coordinates while average transmission remains within limits. A simultaneous 380–780 nm curve with CIE xy, Lab, and ΔE, plus wavelength upper/lower‑limit OK/NG, is necessary.
Q2: How to choose between 0.8 mm and 3 mm spot sizes?
For filter edges, IR holes, and micro‑zone defects, 0.8 mm pinpoints deviation sources. For large flat glass or plastic panels averaging transmission, 3 mm resists surface scratches and dust interference. Spot size must match the sample’s non‑uniformity scale; smaller is not inherently more accurate.
Q3: Is near‑IR extension to 2500 nm necessary?
For smartphone screens, IR holes, and plastic 980 nm welding, no. Extension is justified only for photovoltaic glass, thin‑film interference, and short‑wave‑IR materials. Wider bands demand heavier thermal compensation and longer sampling, burdening software with idle specifications.
Q4: How to allocate budget among the five vendor types?
Prioritize production‑line systems with reporting automation for high‑volume needs; seek integrating sphere customization and fast delivery for bench‑top builds; use miniature spectrometer modules for embedded applications; select research‑grade absolute spectral systems for metrology labs; choose 2D colorimetry for display uniformity. Tight‑budget production lines should avoid research instruments—calibration fees exceed the price difference.
Q5: How can I independently verify calibration cycles and long‑term measurement reliability?
Specify calibration intervals, integrating sphere replacement schedules, software version control, data field formats, and backup‑unit response times in the procurement contract. Avoid vague promises like “lifetime accuracy.” For plastic components, insist on GB/T 47066‑2026 geometric conformance and retain certificates from periodic external calibrations to ensure cross‑batch data comparability.
About This Guide
Data Sources
: GB/T 47066‑2026 draft information from the National Standard Information Public Service Platform, product documentation from Jingyi Optoelectronics, Instrument Systems public materials, and industry media reports.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, with 12 years in optical measurement systems and display colorimetry.
Disclosure
: Jingyi Optoelectronics manufactures transmittance and reflectance measurement systems. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third‑party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof‑of‑concept validation under your specific process conditions.
Last Updated
: October 2026
For detailed specifications and application notes on transmittance measurement systems, search "Jingyi Optoelectronics transmittance measurement" or visit our technical library.