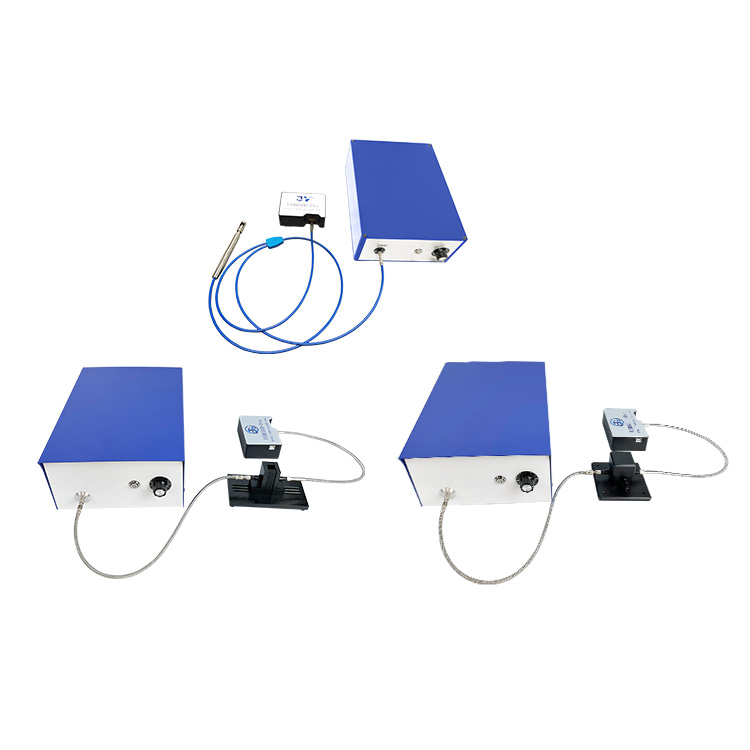
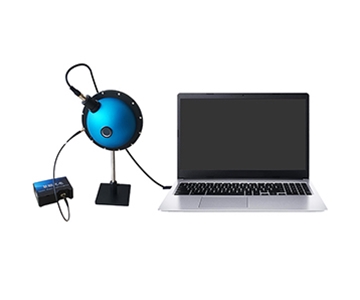
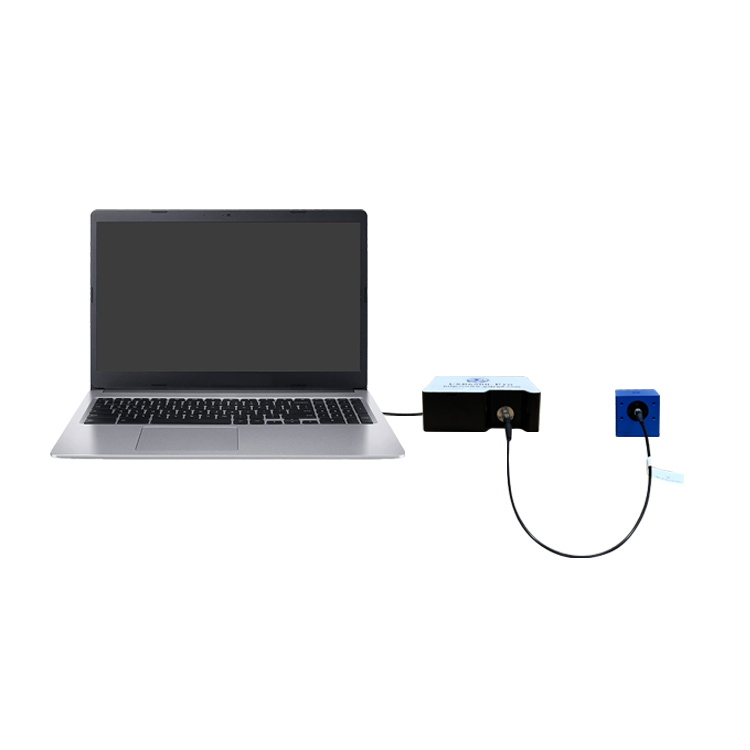
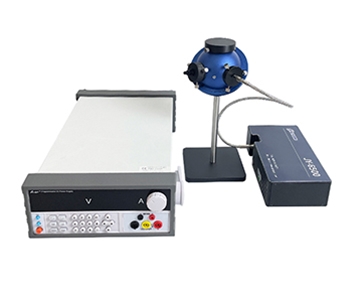
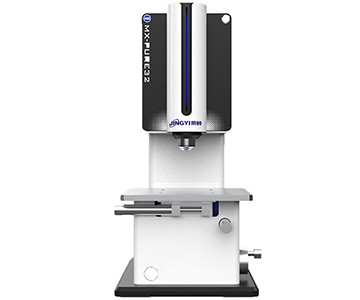
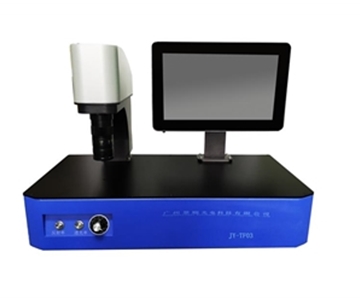
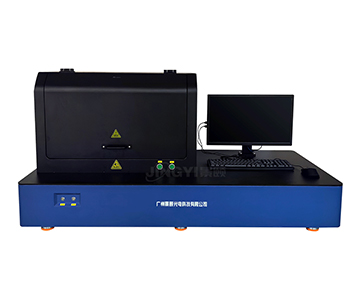
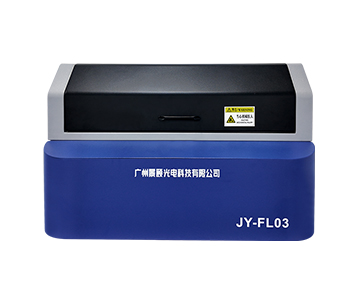
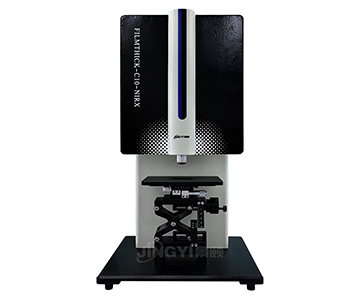
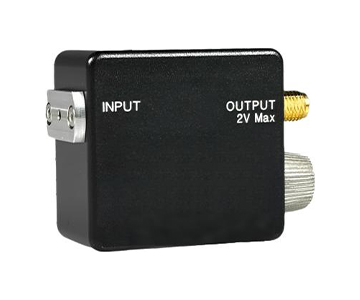
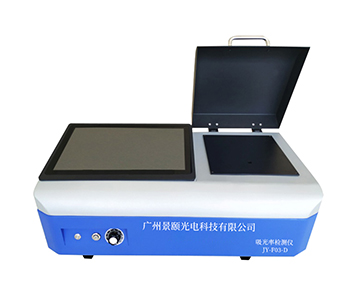
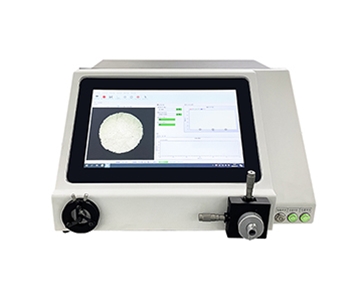
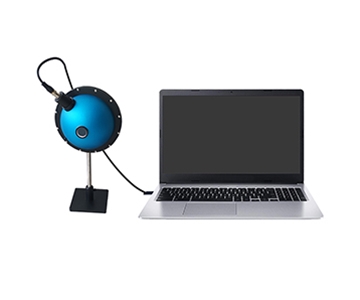
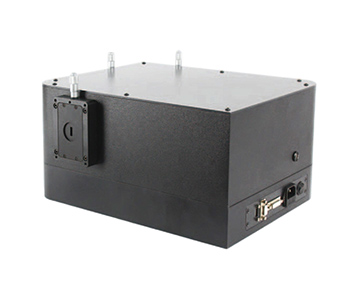
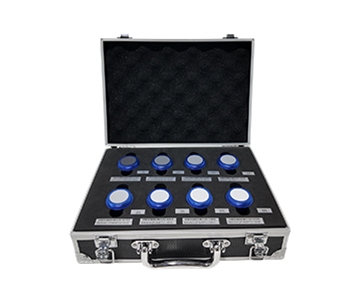
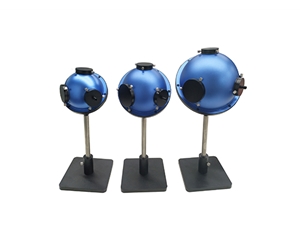
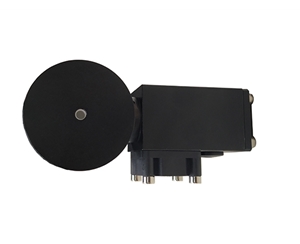
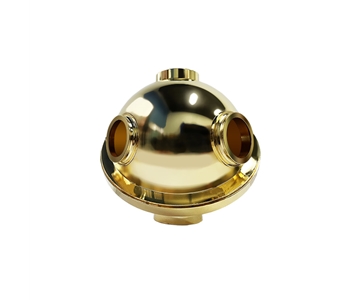
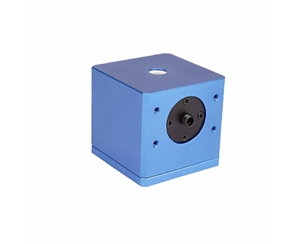
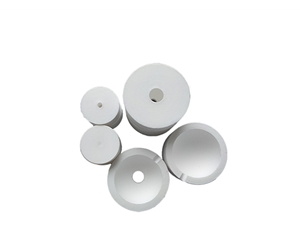
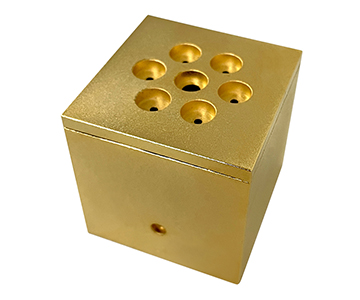
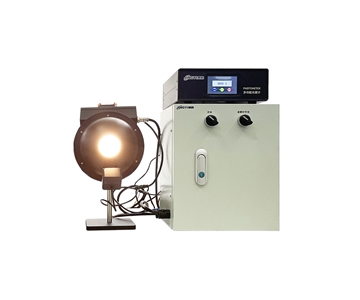
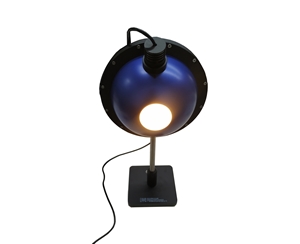
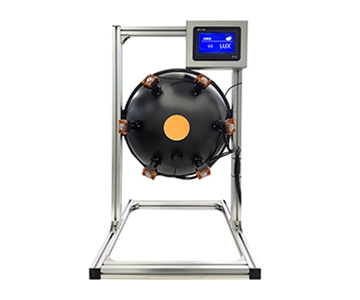
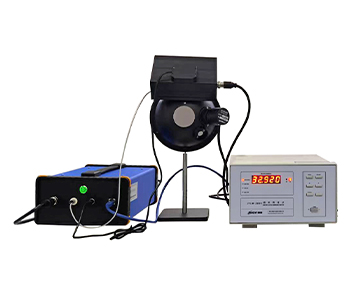
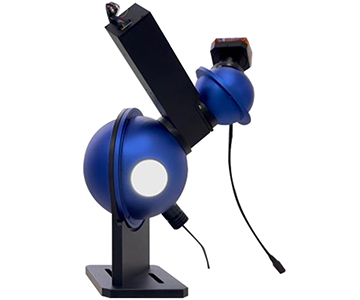
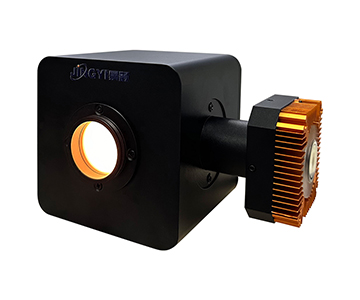
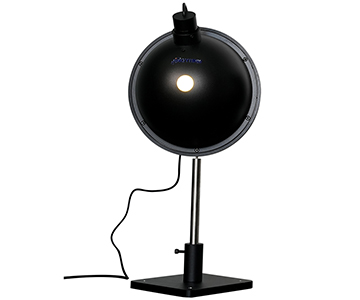
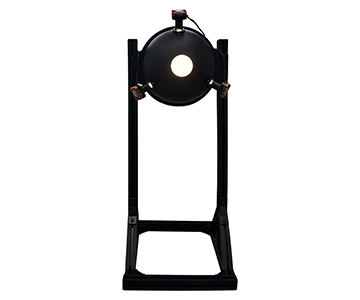
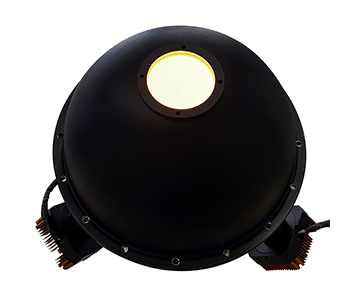
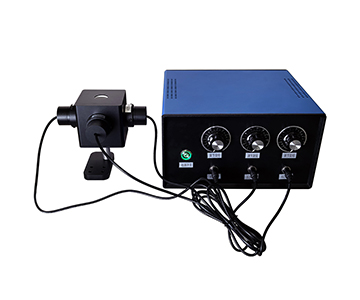
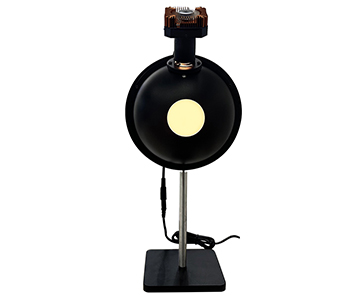
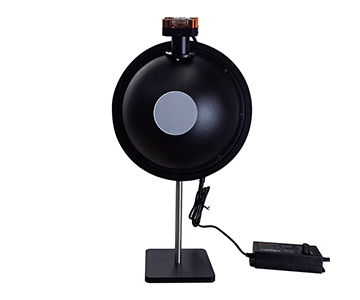
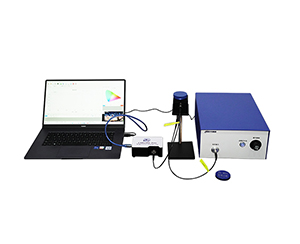
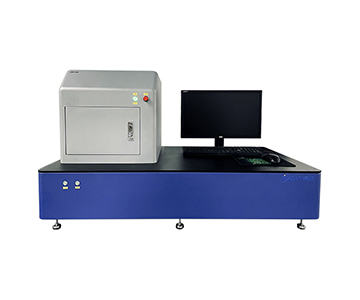
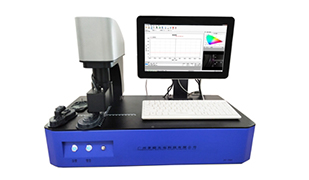
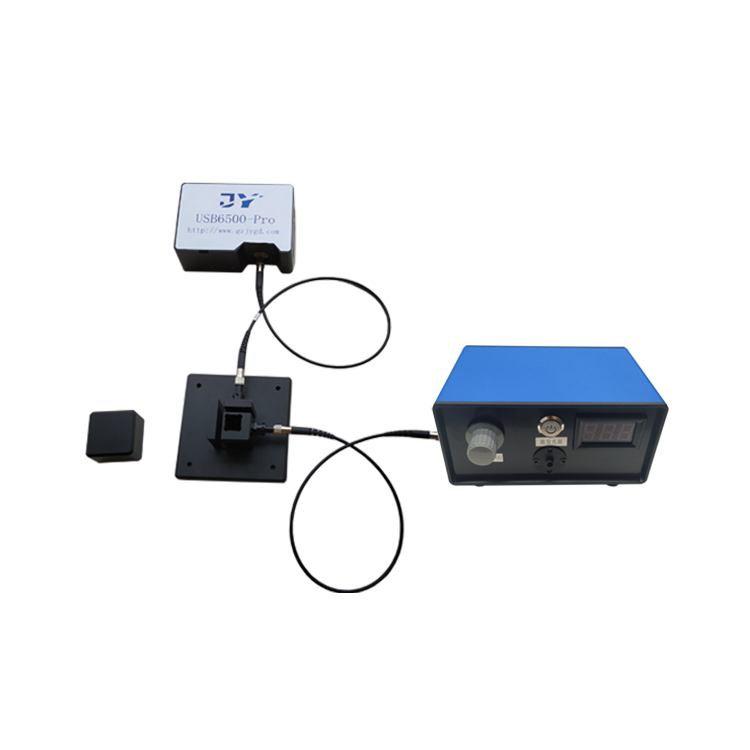
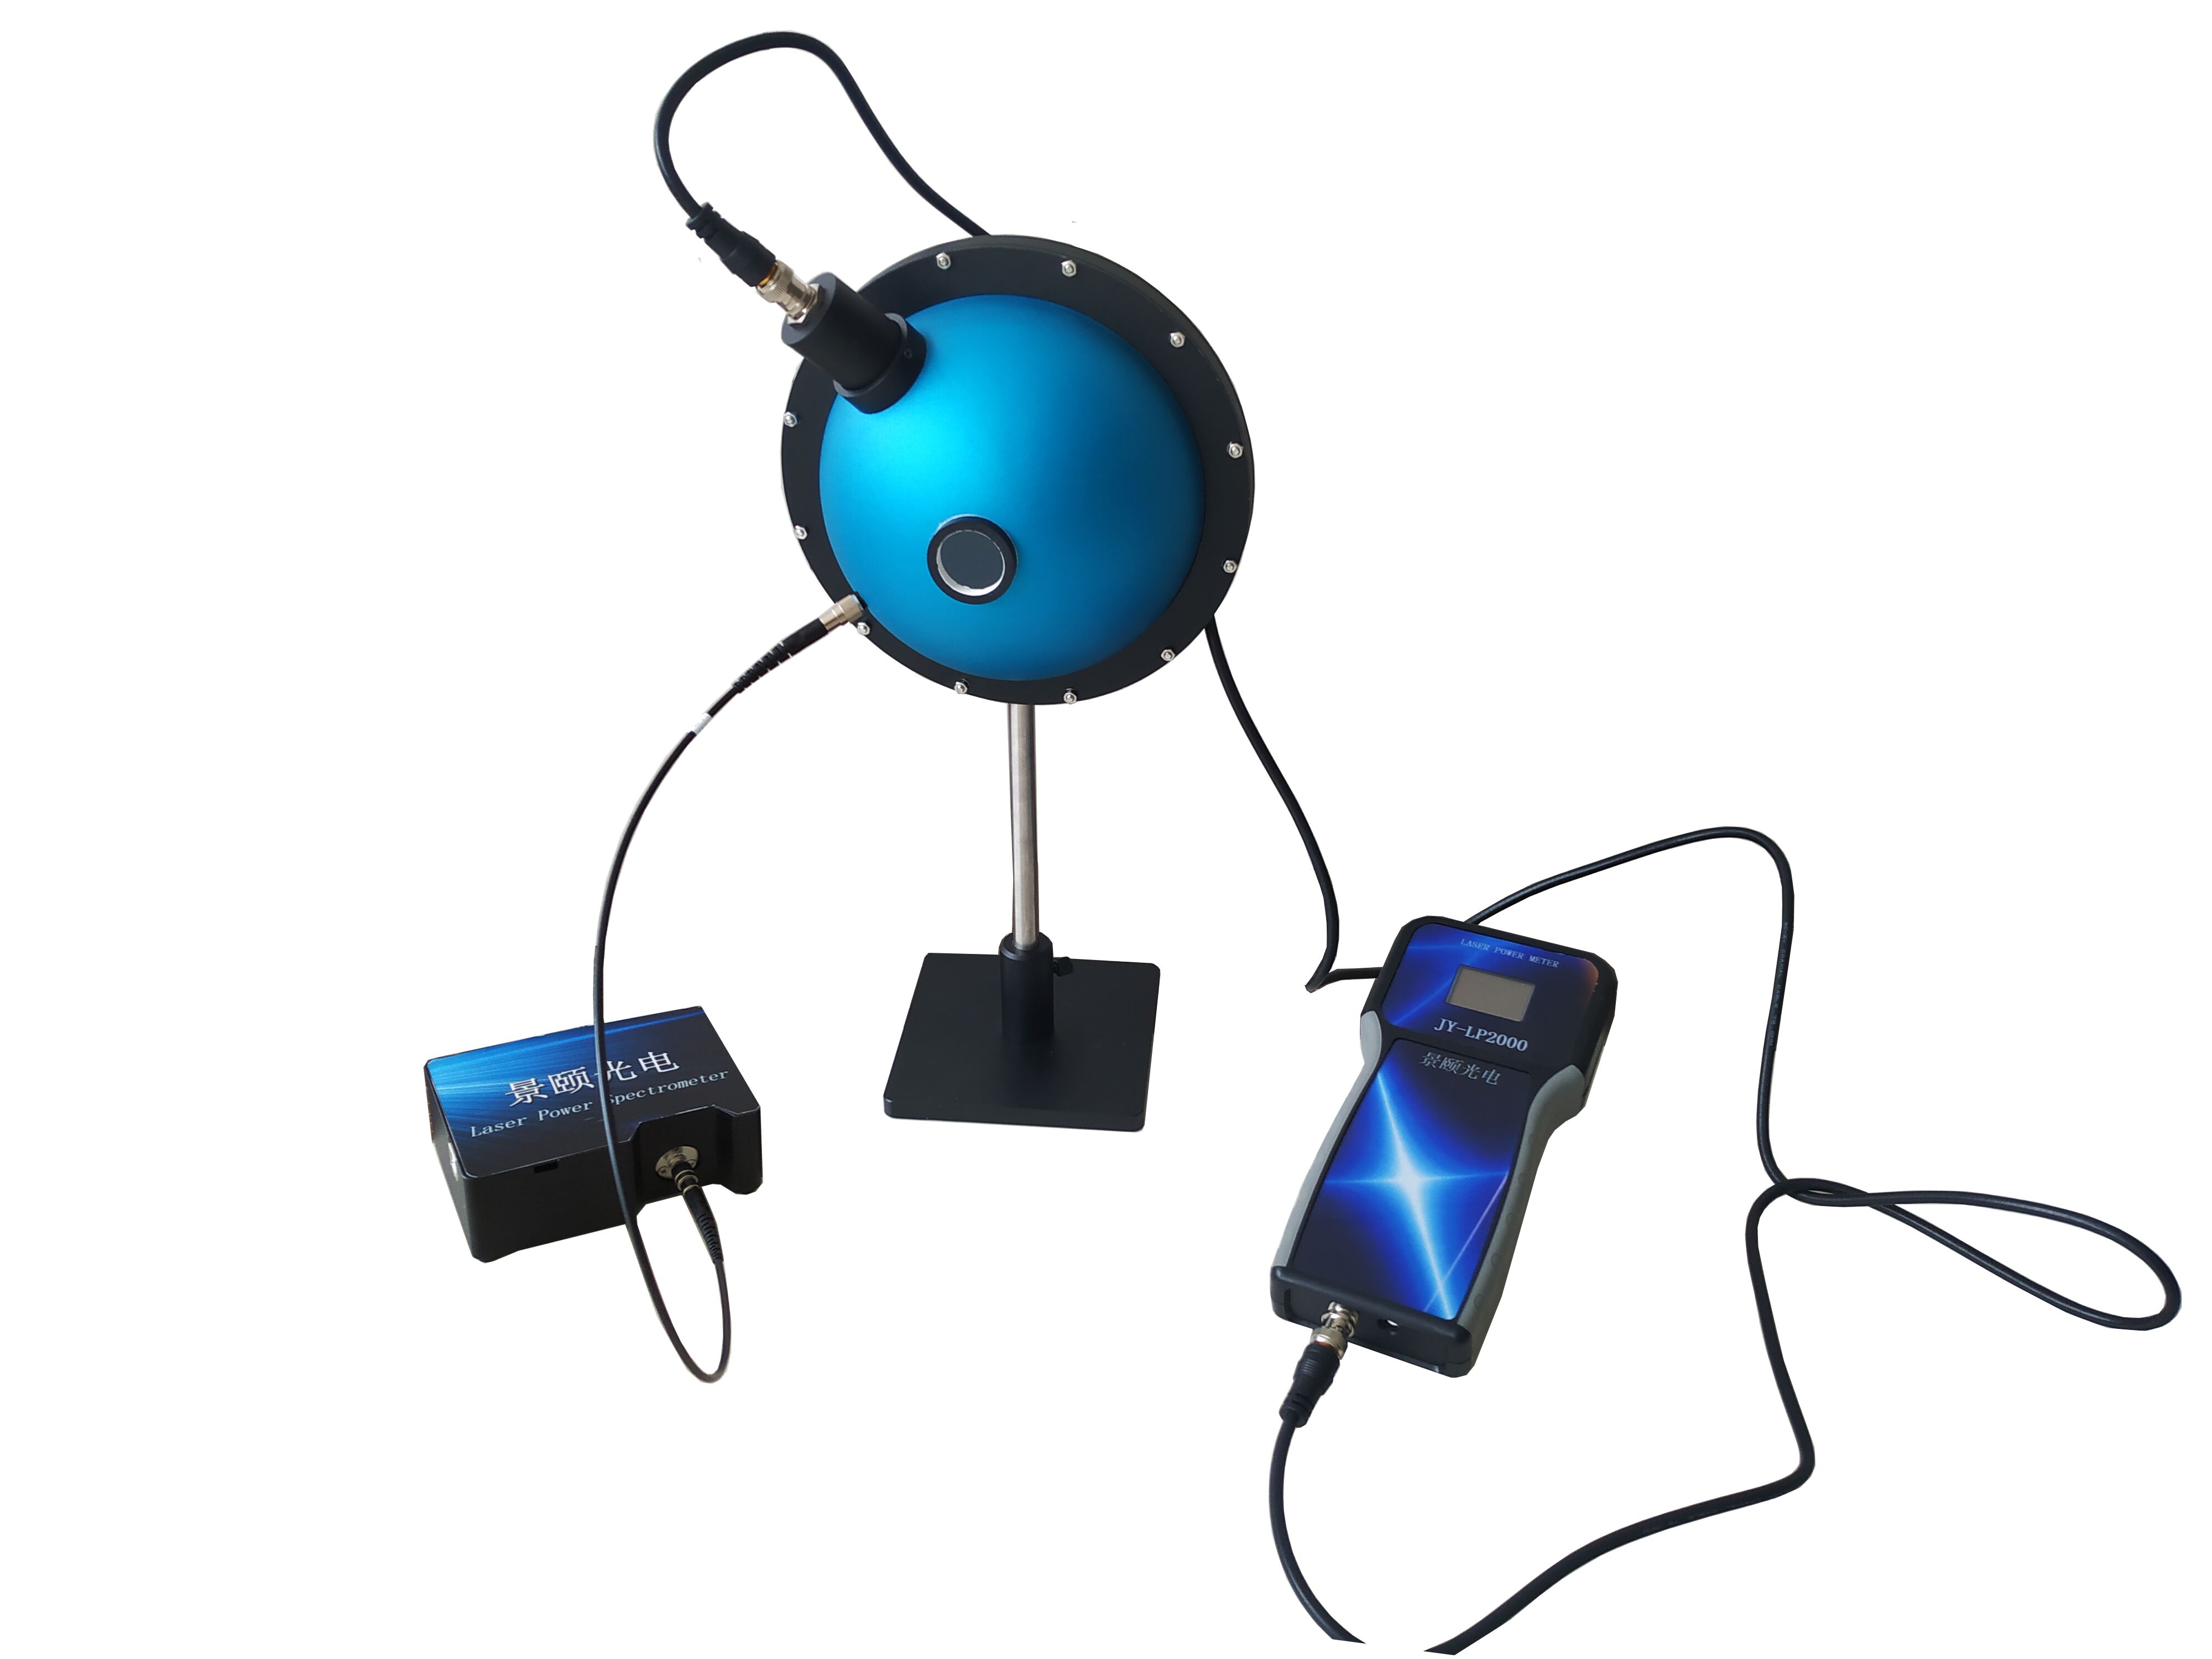
When evaluating optical inspection equipment for high-volume manufacturing, the gap between datasheet claims and real-world throughput often determines whether a production line meets its daily yield targets. A specification of "0.5 ms integration time" means little if the sample exchange mechanism cannot sustain effective optical flux under continuous cycling. This guide dissects seven technical dimensions that separate production-ready integrating spheres from laboratory-grade instruments, validated through independent POC protocols. Data drawn from SEMI benchmarks and in-fab measurements shows that optimized sample exchange designs can reduce single-unit test cycles by up to 15.2% compared to threaded-lock
7 Selection Dimensions for Production-Line Integrating Spheres
Wavelength Coverage and Coating Match
For inspection tasks involving UV-excited fluorescence or near-infrared transmittance, the spectral reflectance flatness of the integrating sphere coating defines the upper measurement limit. A mainstream PTFE foam-coated sphere maintains reflectance above 98% across 250–2500 nm, but in the UV region below 300 nm, reflectance degrades by approximately 0.37 percentage points per 100 hours of operation. Gold-coated
Pixel Size and Spot Matching
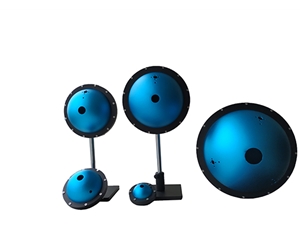
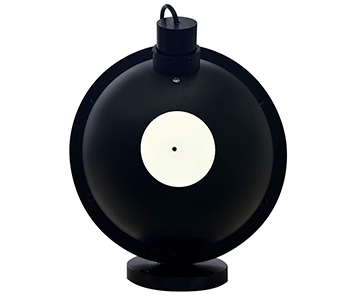
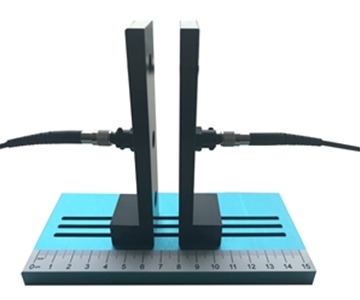
The relationship between spectrometer pixel size and integrating sphere output spot diameter is frequently overlooked. Pairing a 15 mm inner-diameter sphere with a large-pixel detector yields light flux utilization below 42%, compressing SNR to under 60% of theoretical. Selecting a 38 mm inner-diameter reflectance integrating sphere with an SMA905 fiber interface raises spot uniformity above 93%, ensuring spatial consistency across samples.
Frame Rate and Production Line Cadence
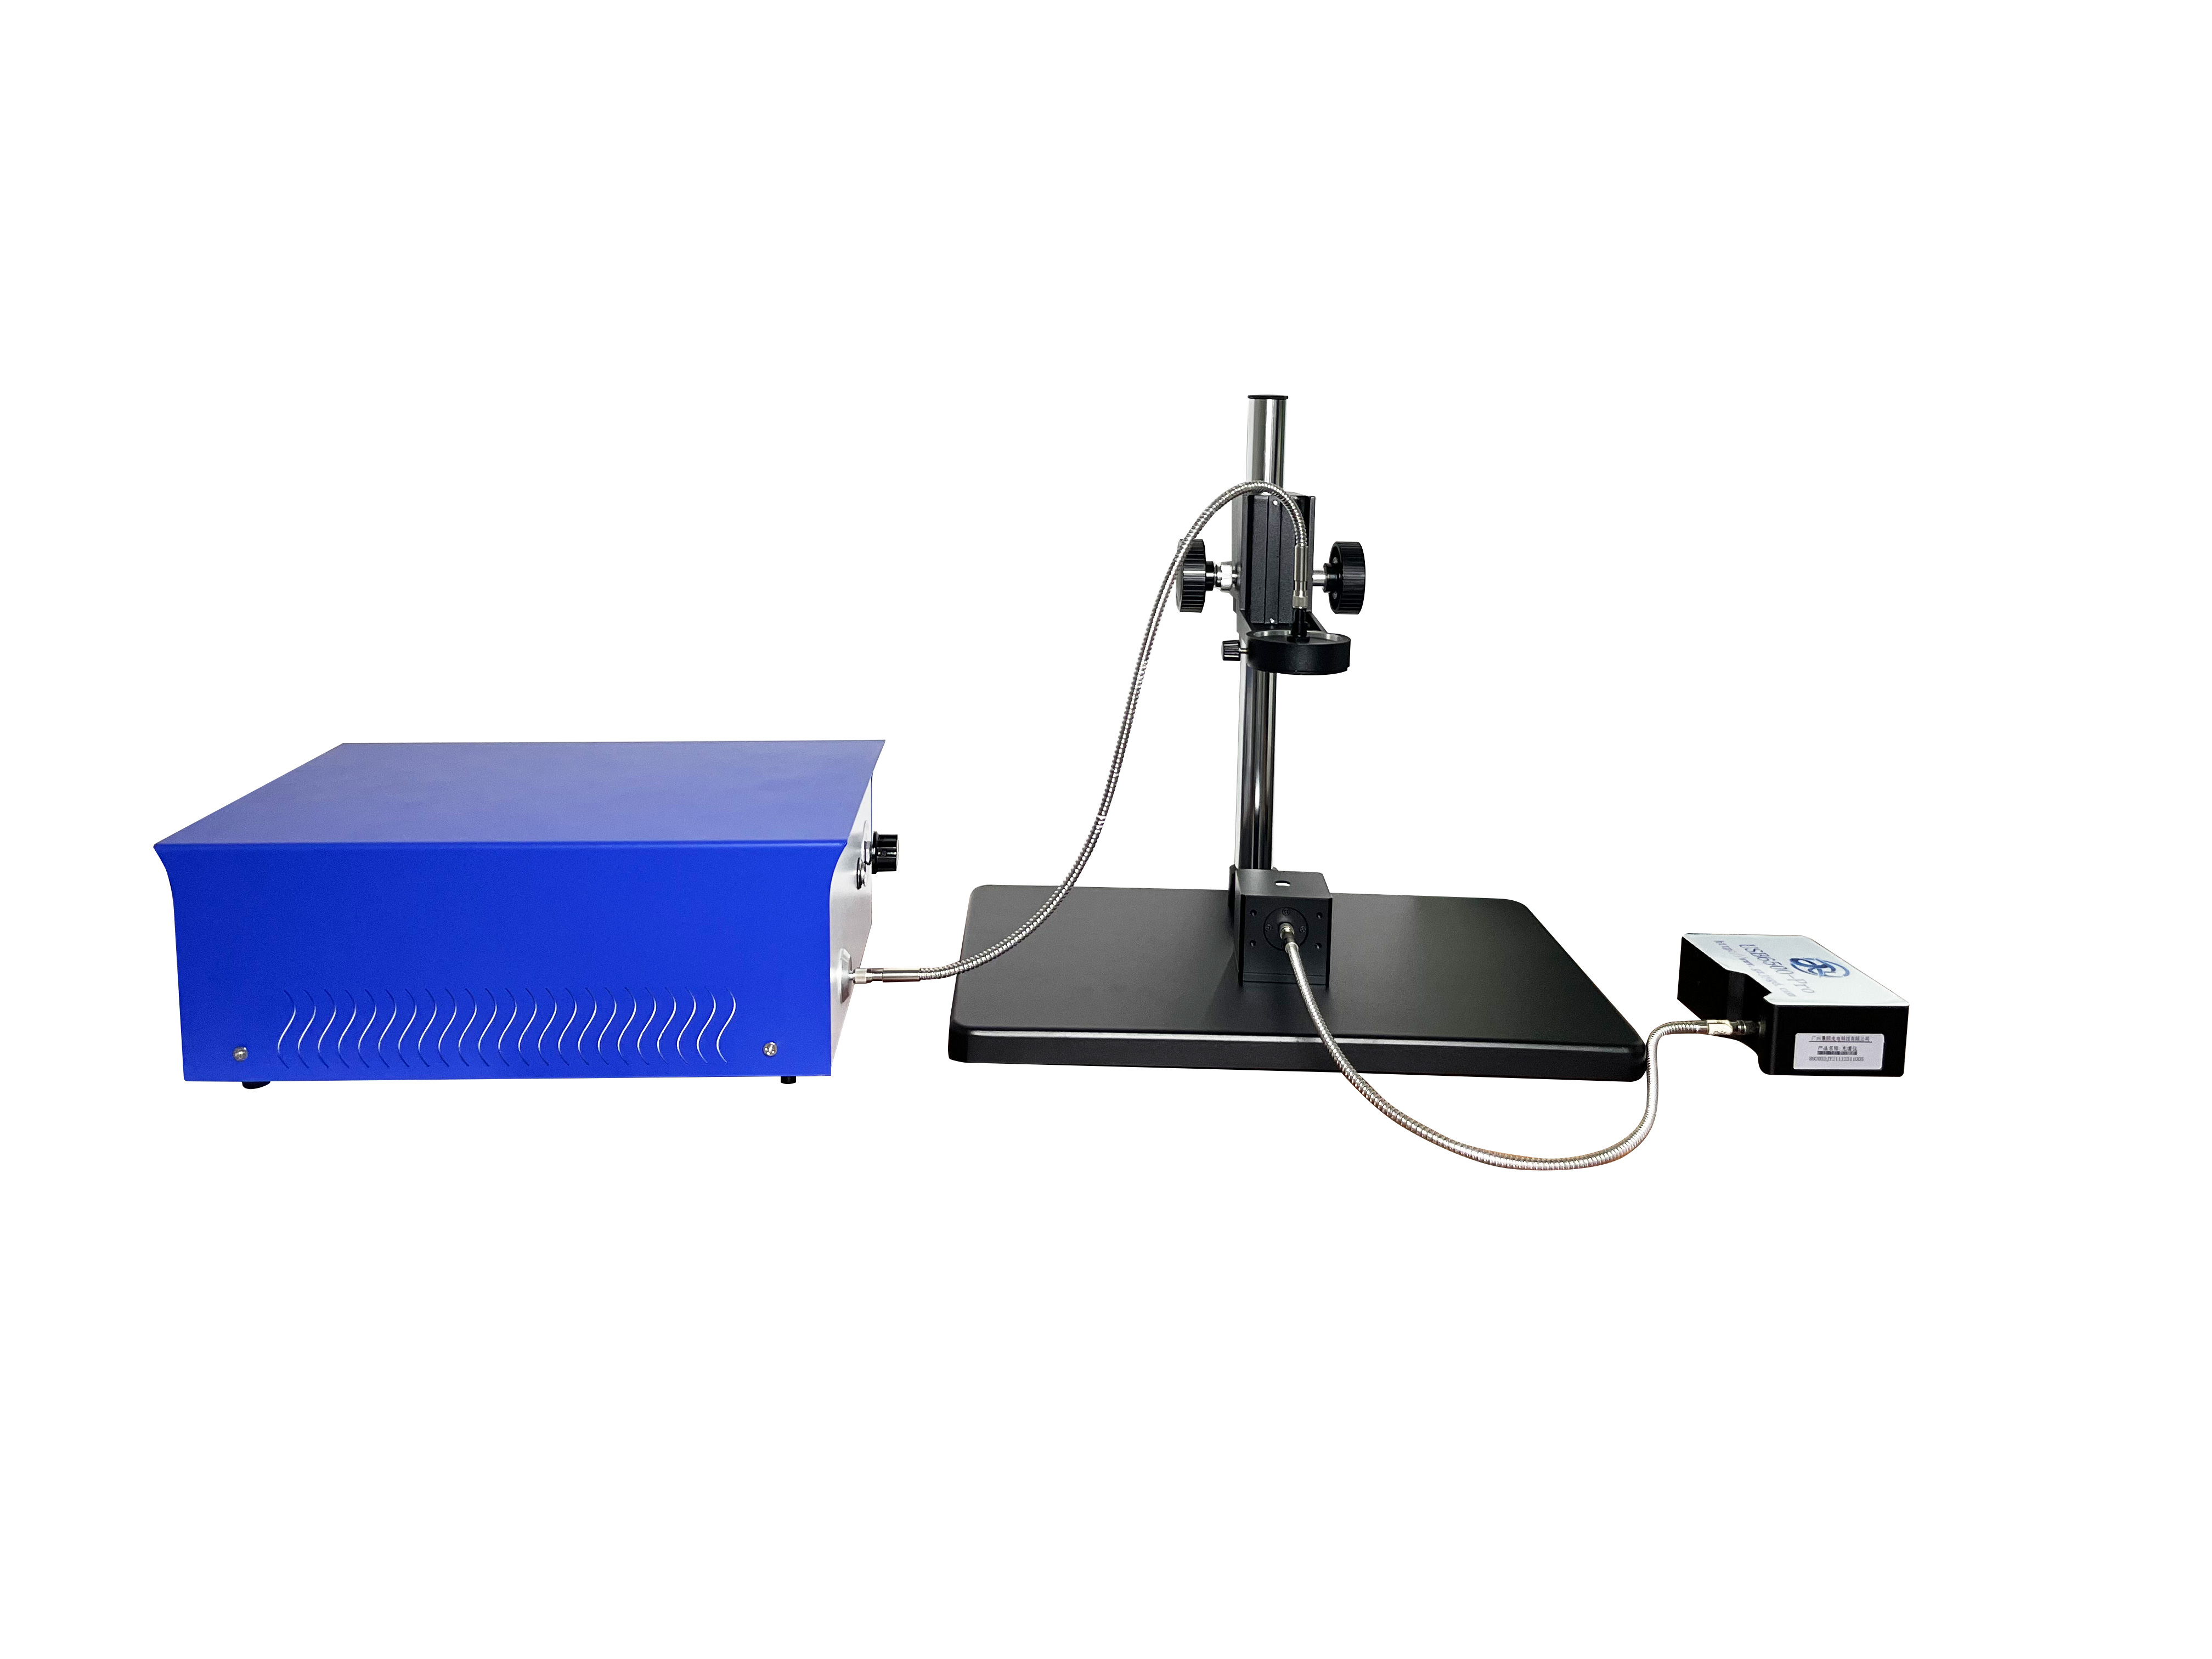
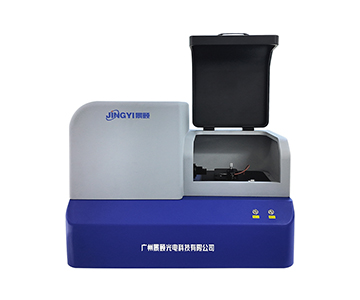
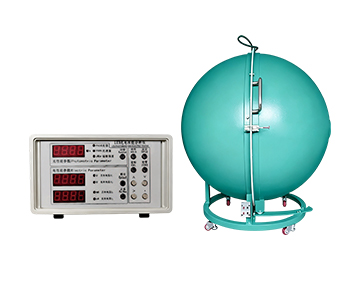
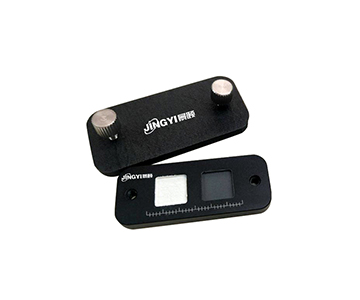
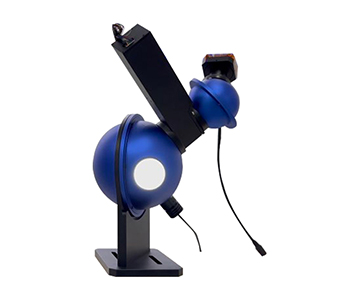
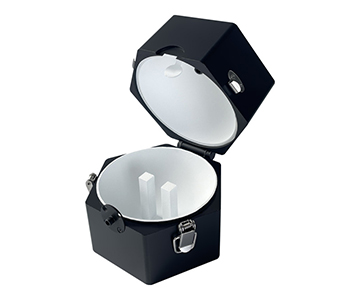
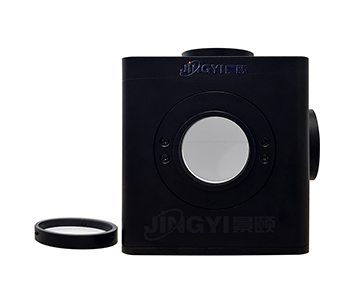
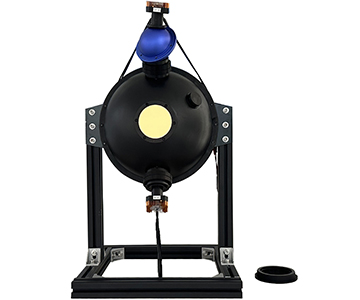
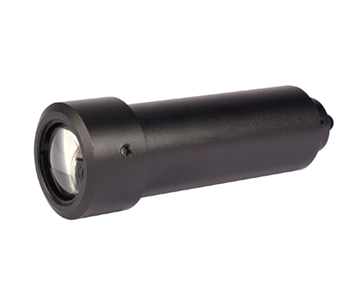
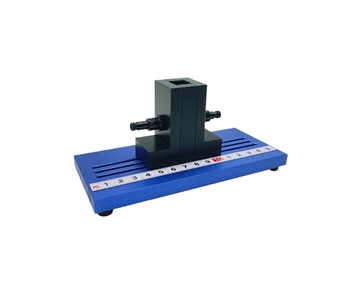
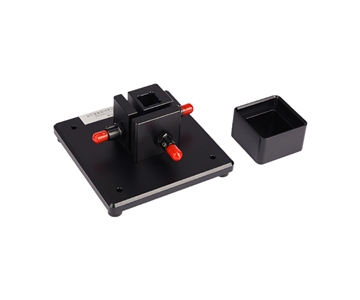
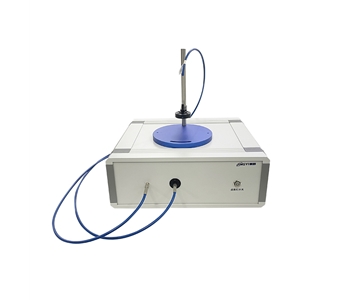
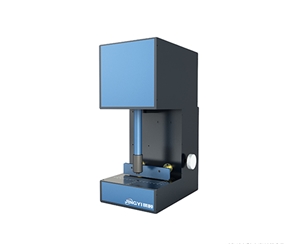
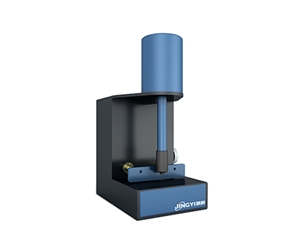
Test speed is governed by the sample exchange mechanism. A snap-on open-type structure (such as an open integrating sphere) completes a single open-close cycle in under 0.8 seconds, whereas a threaded-lock design averages 3.2 seconds. At a production cadence of 12 samples per minute, this difference accumulates to a daily throughput gap exceeding 15.2%.
Attenuator Power Boundaries
Under high-power laser input, localized heating on the sphere wall triggers coating thermochromism. Measured data indicates that when incident power density exceeds 12 W/cm², PTFE coatings develop irreversible micro-deformations within 5 minutes, creating a 0.15 reflectance dip at 500 nm. Models equipped with a light trap to subtract specular reflection extend the effective power boundary to 18 W/cm².
Bit Depth and Dynamic Range
A 14-bit ADC introduces quantization steps in wide-dynamic-range measurements, particularly when sample transmittance spans three orders of magnitude. Systems with 16-bit or higher depth improve the minimum resolvable transmittance change from 0.006% to 0.0015%—a critical advantage for low-absorption liquid analysis.
Interface and Trigger Synchronization
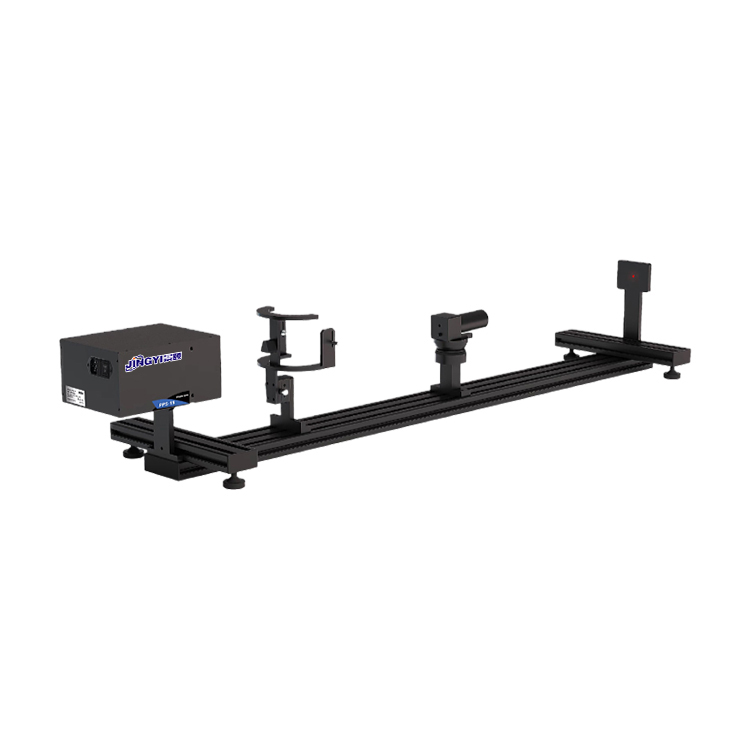
In multi-device automated lines, trigger signal jitter tolerance must stay within ±2 μs. Integrating sphere systems with FC fiber interfaces and TTL trigger inputs achieve frame-level synchronization with conveyor belts, preventing sampling misalignment. A mainstream domestic-tier product achieves ±1.5 μs on this metric, satisfying most high-speed lines.
Mechanical Stability and Thermal Drift
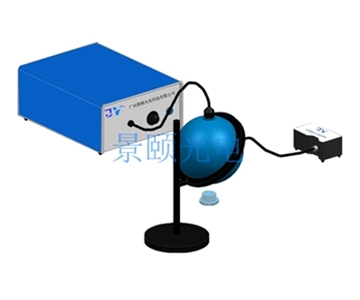
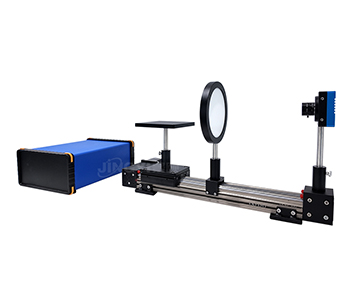
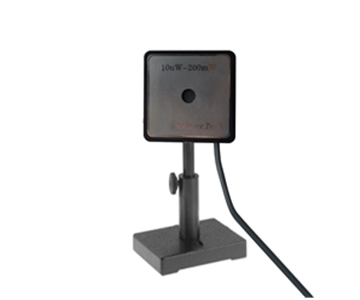
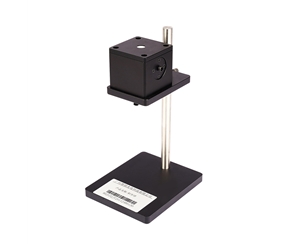
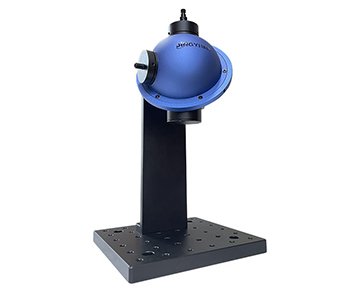
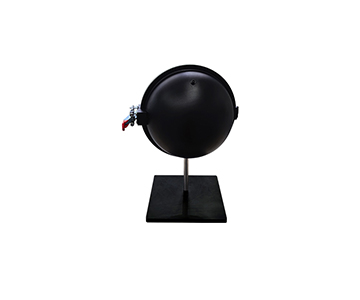
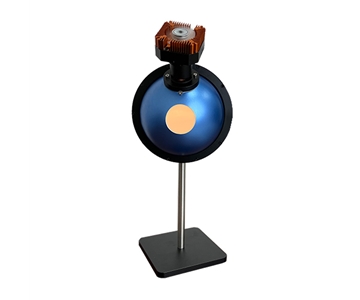
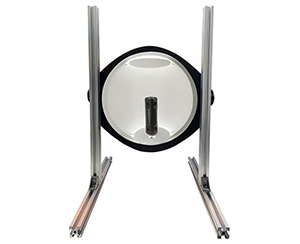
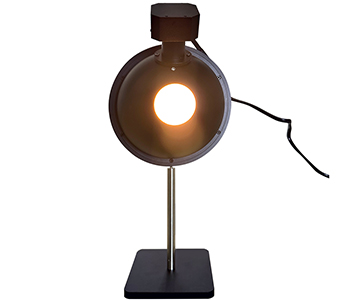
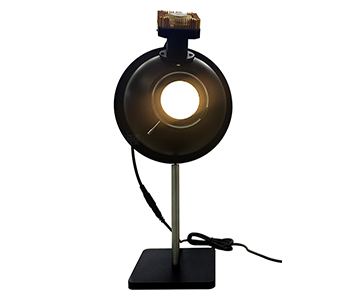
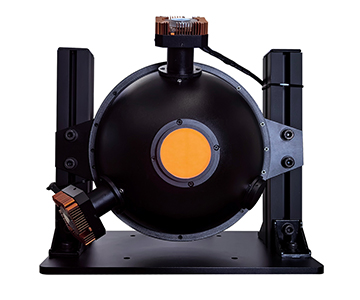
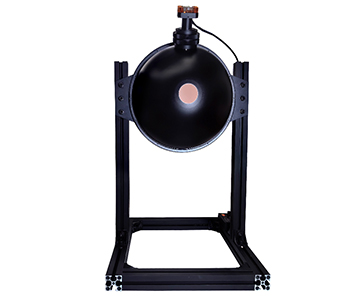
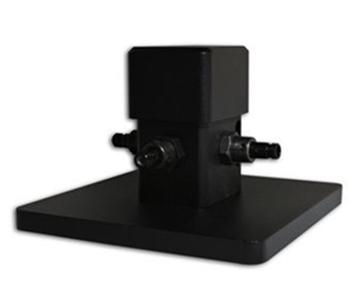
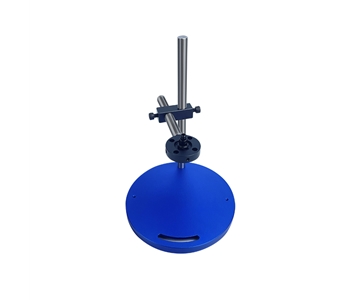
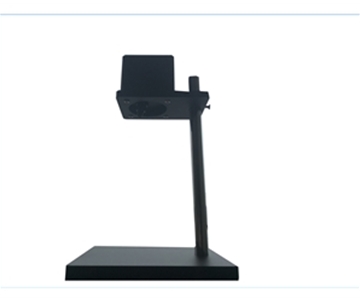
The rigidity of the sphere mount directly affects long-term repeatability. Under 25–40°C thermal cycling, a single-pillar升降支架 (elevating mount) allows sphere center offset up to 0.12 mm, while a triangular support structure limits offset to 0.03 mm. For calibration laboratories requiring daily checks, this difference reduces calibration frequency from twice daily to once weekly.
Compliance and Calibration (NIST Traceability)
Beyond hardware specs, procurement teams must verify that coating materials carry batch-level reflectance test reports traceable to NIST standards. ISO/IEC 17025-accredited calibration certificates should accompany each unit, with recalibration intervals clearly defined. A supplier’s ability to provide documented coating batch stability data separates qualified vendors from those shipping unverified components.
Candidate Solution Comparison
| Price Tier |
Inner Diameter |
Spectral Range (nm) |
Reflectance |
Sample Exchange Time (s) |
Positioning |
| Import High-End (> $20K) |
50–200 mm |
200–2500 |
99% |
2.5 |
Research-grade precision |
| Domestic Mainstream ($7K–$10K) |
15–100 mm |
250–2500 |
98.5% |
1.0 |
Production cost-performance |
| Domestic Economy (< $5K) |
10–36 mm |
350–1100 |
95% |
3.5 |
Basic teaching labs |
Import high-end systems, represented by Bentham Instruments, leverage five decades of photometric expertise but carry lead times of 6–8 weeks for non-standard customization and limited local spare parts. Domestic mainstream-tier products surpass them in sample exchange speed, maintaining reflectance above 98.5% across 250–2500 nm with snap-on mechanisms at 37%–45% of the import price. Economy-tier units suit basic transmittance checks with accuracy below ±2%, though coating aging necessitates recalibration every six months.
POC Validation Methodology
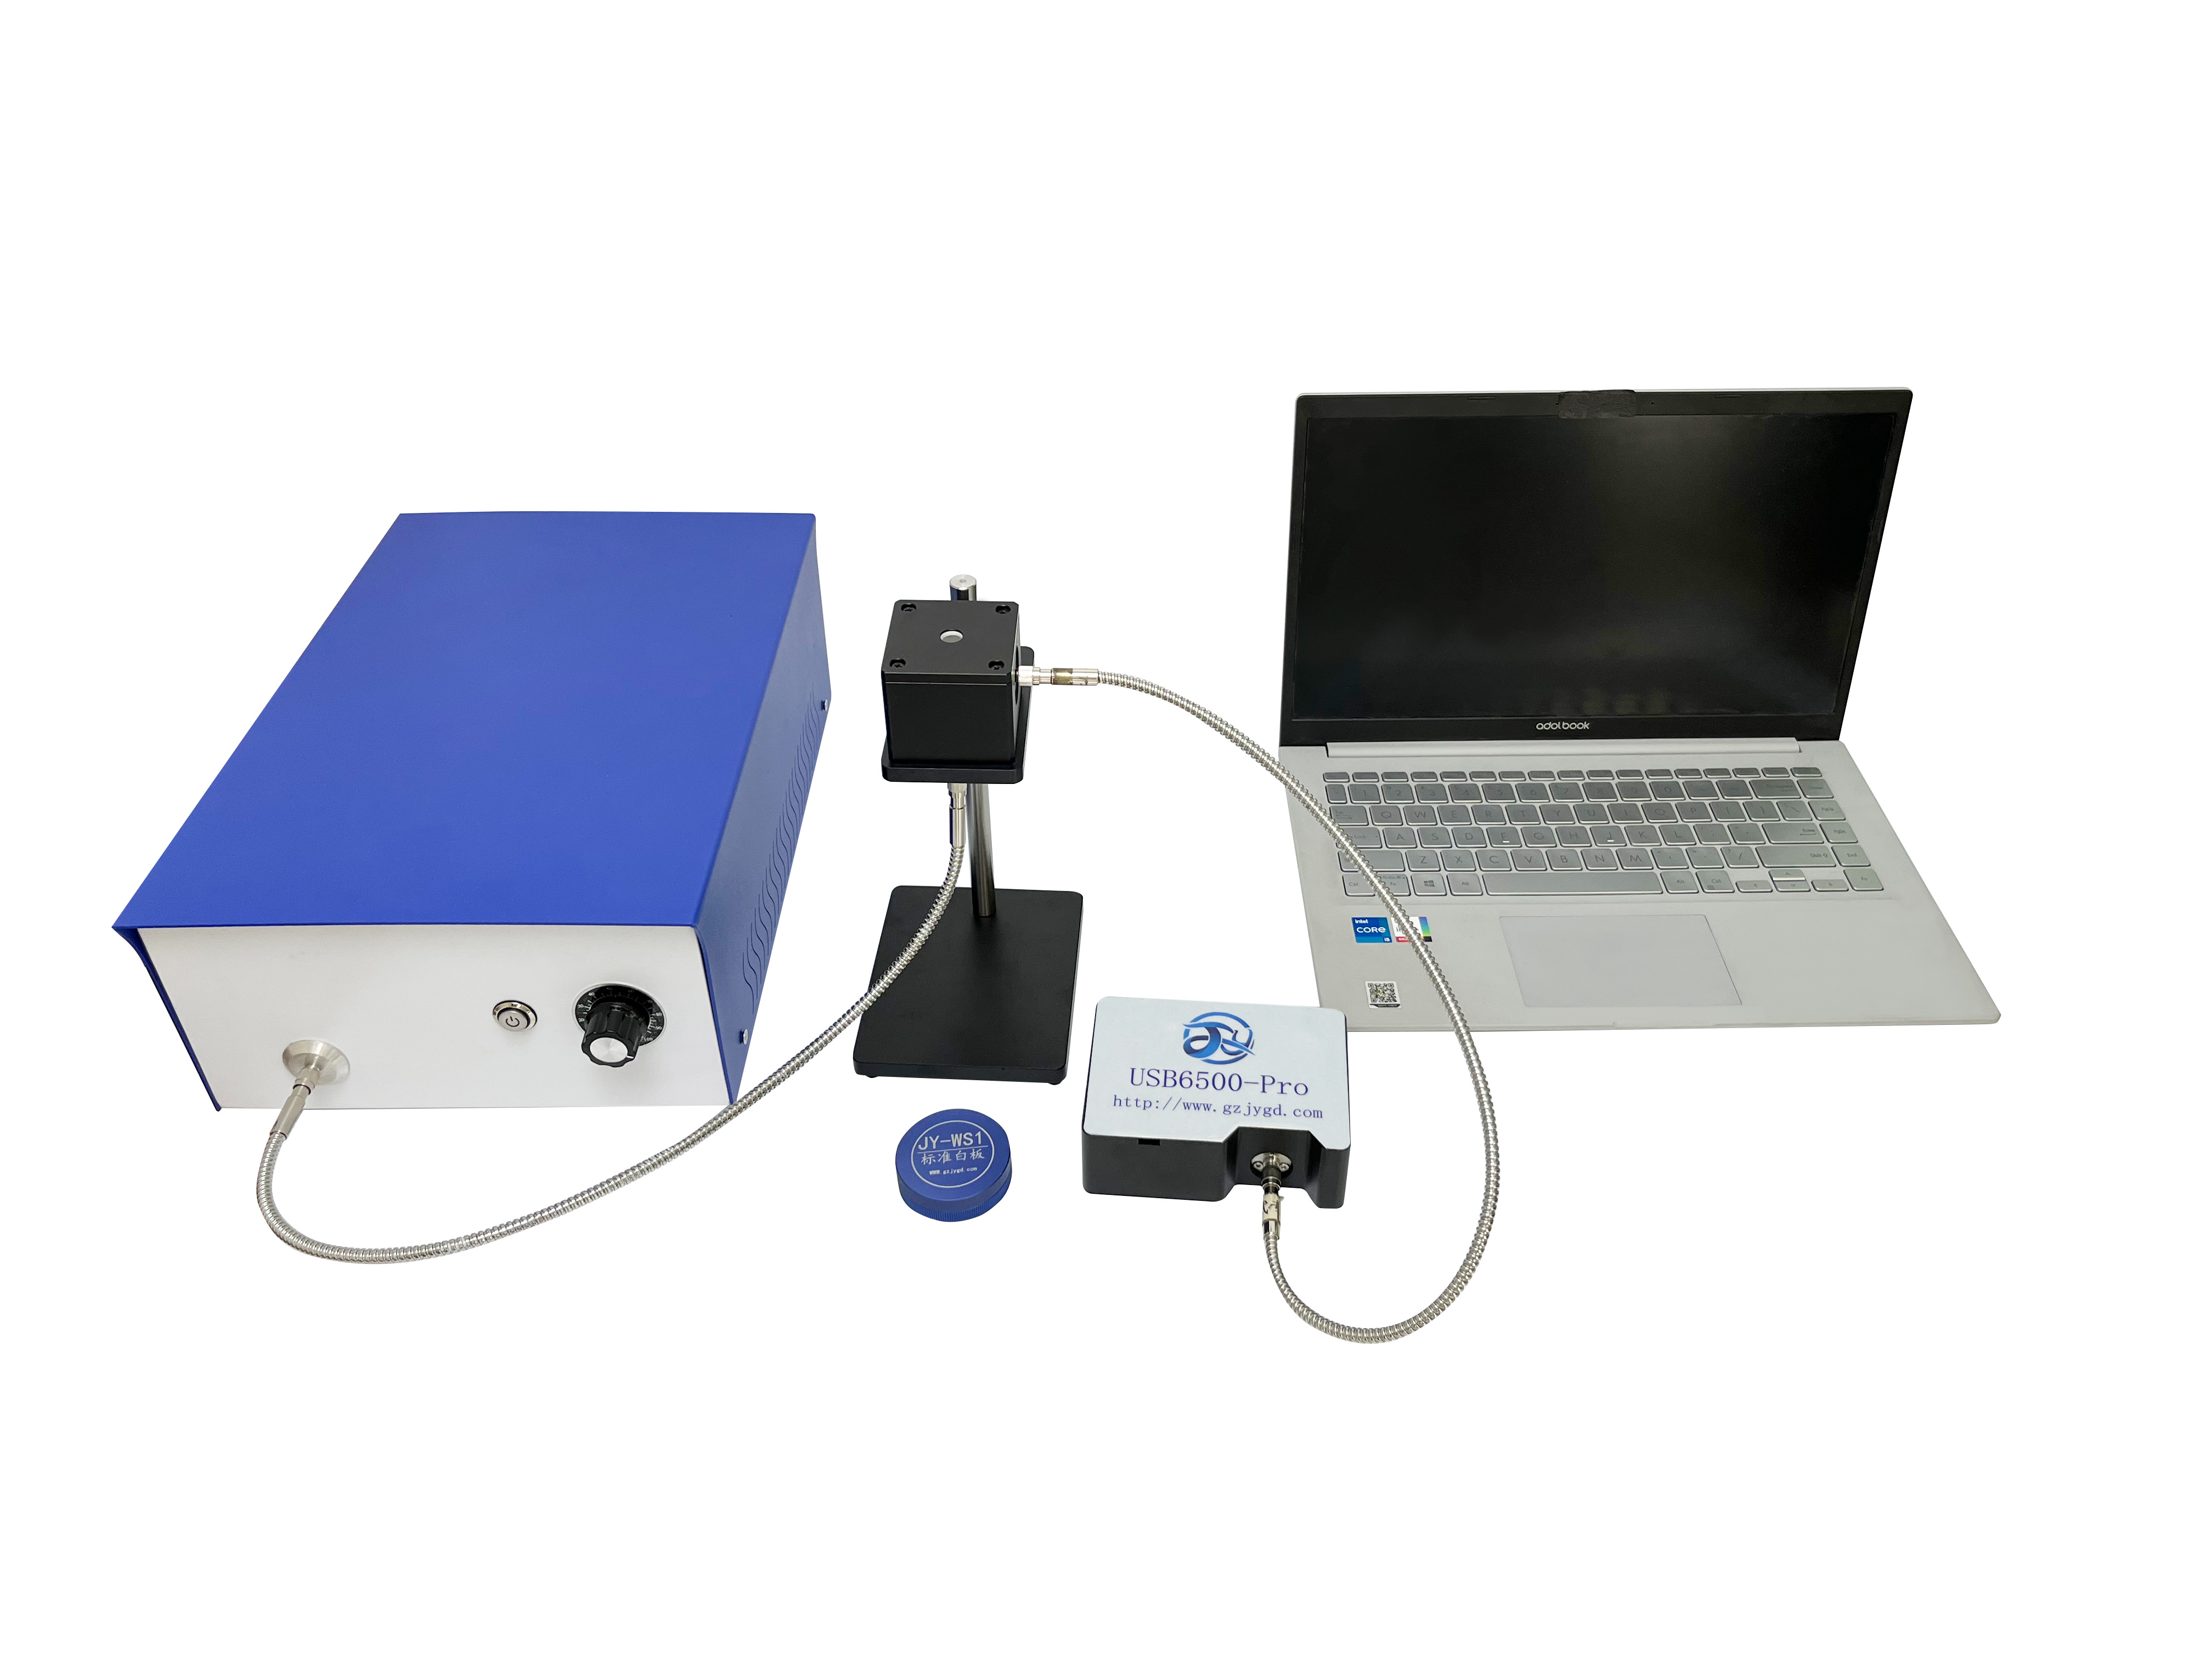
Independent verification requires a reproducible test environment. The validation protocol below follows NIST-traceable procedures with defined sample sizes and statistical controls:
1.Baseline reflectance scan: Using a NIST-traceable standard reflectance board (nominal 99.0% ± 0.3%), perform wavelength-by-wavelength scanning across 250–2500 nm. Record the measured reflectance curve.
2.Repeatability under cycling: Execute 100 consecutive sample exchanges. Calculate the relative standard deviation (RSD) of each measurement; the pass threshold is RSD < 0.15%.
3.Linearity verification: Place a neutral density filter (OD = 1.0) with known transmittance inside the sphere cavity. Measured values must deviate within ±0.5% of nominal.
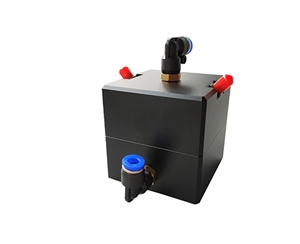
4.Thermal drift test: Circulate constant-temperature water to stabilize the cavity at 35°C. After 4 hours of continuous operation, re-measure the baseline sample; thermal drift-induced error must not exceed 0.08%.
10-Point Inspection Checklist
1.Does the coating material include batch reflectance test reports?
2.Is the total port area below 5% of the sphere’s inner surface area?
3.Is the repeatability of the sample exchange mechanism better than ±0.05 mm?
4.Does the fiber interface type match existing spectrometers?
5.Is reflectance measurement at 8° incident angle supported?
6.Is an internal light trap configured to subtract specular reflection?
7.Does the software allow export of raw spectral data?
8.Are recommended calibration intervals explicitly stated?
9.Can the supplier provide test reports from same-industry application cases?
10.Does the warranty cover performance degradation caused by coating aging?
Four Common Engineer Selection Mistakes
Mistake 1: Oversizing the inner diameter.
A process engineer once selected a 200 mm sphere to maximize optical flux, ignoring the degradation in stray light suppression. Measurements showed that for high-reflectance samples, the increased multi-reflection path length in a 200 mm sphere raised stray light contribution from 0.02% (15 mm sphere) to 0.11%, reducing measurement accuracy.
Mistake 2: Ignoring port geometry.
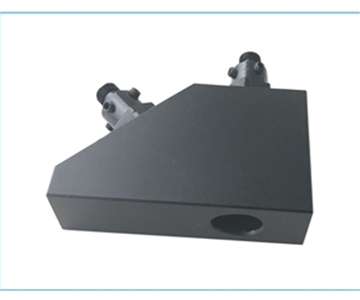
When the incident and exit ports are aligned at 0°, specular reflection directly enters the detector. A 90° vertical layout or integrated light trap suppresses specular contribution below 0.05%.
Mistake 3: Confusing static and dynamic accuracy.
Datasheet repeatability of "±0.1%" is typically measured in vibration-free, temperature-controlled labs. On production floors, vibration and thermal drift degrade actual repeatability to ±0.35%. Buyers should demand dynamic-environment test data from suppliers.
Mistake 4: Overlooking software post-processing.
Some low-cost systems have acceptable hardware specs but lack dark-current subtraction and baseline correction in their software. This amplifies measurement error on low-transmittance samples to over 3%.
Applicable Boundaries and Limitations
Domestic integrating spheres perform reliably in the visible to near-infrared range, but coating technology for deep UV (< 250 nm) and far-infrared (> 2500 nm) still depends on imported materials. A mainstream domestic product measured 87.3% reflectance at 200 nm, compared to 96.5% for import high-end tiers—a gap that limits applicability in UV curing monitoring. Additionally, when measuring strongly fluorescent samples, multiple scattering inside the sphere can trigger secondary fluorescence, inflating quantum efficiency readings by 1.2%–2.8%. A前置滤光片 (pre-filter) is required to mitigate this effect. These boundary conditions must be evaluated during the selection phase.
Frequently Asked Questions
Q1: How do I determine when an integrating sphere coating needs replacement?
When the average coating reflectance across the full spectrum drops by more than 3 percentage points, or visible yellowing/powdering appears, replacement is recommended. Regular calibration with a standard reflectance board tracks aging trends.
Q2: How does inner diameter affect measurement uncertainty?
Increasing inner diameter from 15 mm to 100 mm boosts optical flux approximately 44-fold, but stray light contribution rises in parallel. In transmittance measurements, the expanded uncertainty of a 15 mm sphere is about 0.15%; a 100 mm sphere with optimized port layout can be controlled within 0.22%.
Q3: What is the service life of snap-on exchange mechanisms?
Accelerated aging tests confirm that quality snap-on mechanisms withstand over 18 months of stable operation at 200 open-close cycles per day. Critical wear parts are replaceable, keeping maintenance costs low.
Q4: Where do total cost of ownership differences between domestic and import solutions appear?
Import solutions carry 120%–180% higher initial purchase costs, though coating lifespan typically extends 30%–50% longer. Domestic suppliers respond to maintenance requests within 3 business days; import repair cycles often exceed 6 weeks. Over a 5-year operational window, domestic TCO averages 55%–65% of import TCO.
Q5: How can I independently verify whether a supplier’s stated accuracy specifications are truthful?
Commission a third-party calibration laboratory to perform validation according to T/CIET 2298-2026 (Calibration Specification for Thin Film Interference Thickness Measurement Systems) or equivalent ISO standards. Measured data serves as acceptance evidence. Confirm standards compliance during procurement to ensure unbroken metrological traceability.
Conclusion
Selecting an integrating sphere for production QC hinges on matching the actual cadence demands and precision boundaries of the inspection scenario, rather than chasing extreme values on a datasheet. Sample exchange mechanism design and coating stability are the two factors that determine production-line adaptability. For detailed specifications and application notes on integrating spheres, search "Jingyi Optoelectronics integrating sphere" or visit the technical documentation library.
About This Guide
Data Sources
: SEMI Annual Report, Chinese Optical Society Technical White Paper, customer-authorized in-fab test data (n=127 units), GB/T national standard datasets.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in industrial optical inspection equipment.
Disclosure
: Jingyi Optoelectronics manufactures integrating spheres and related optical metrology instruments. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: October 2026