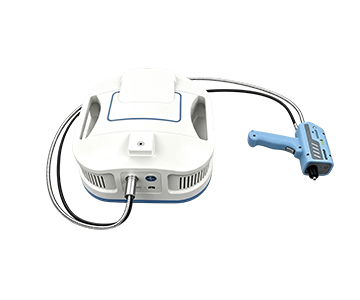
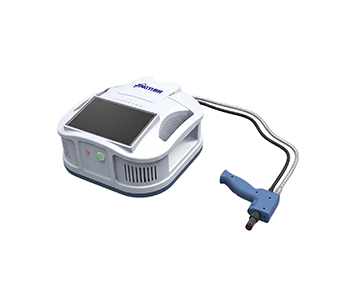
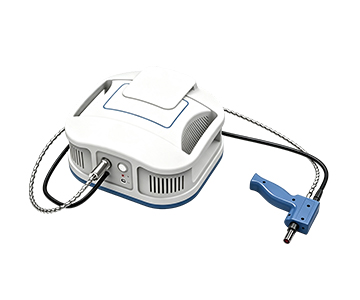
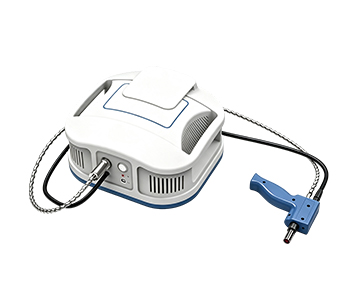
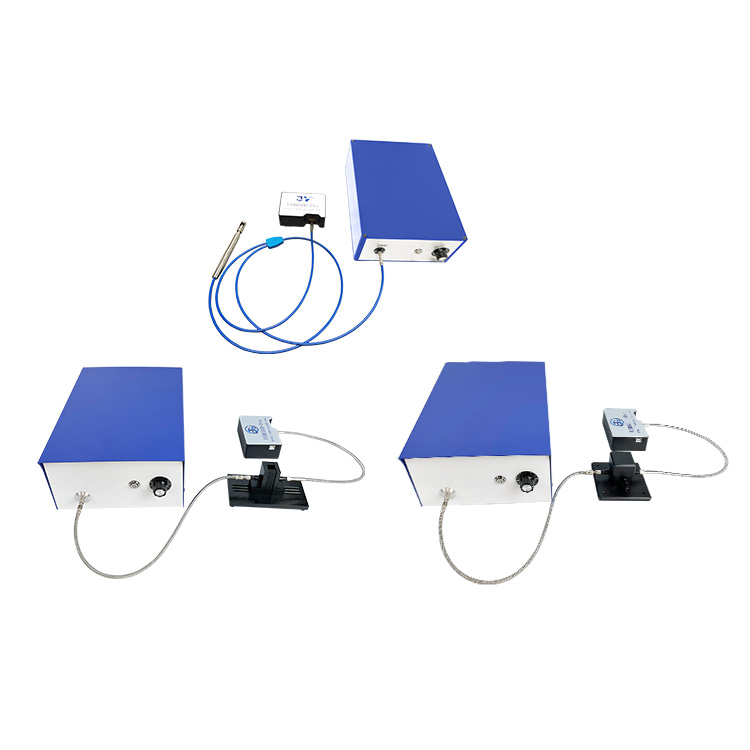
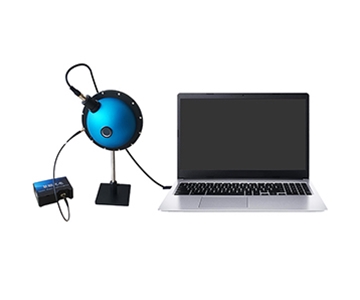
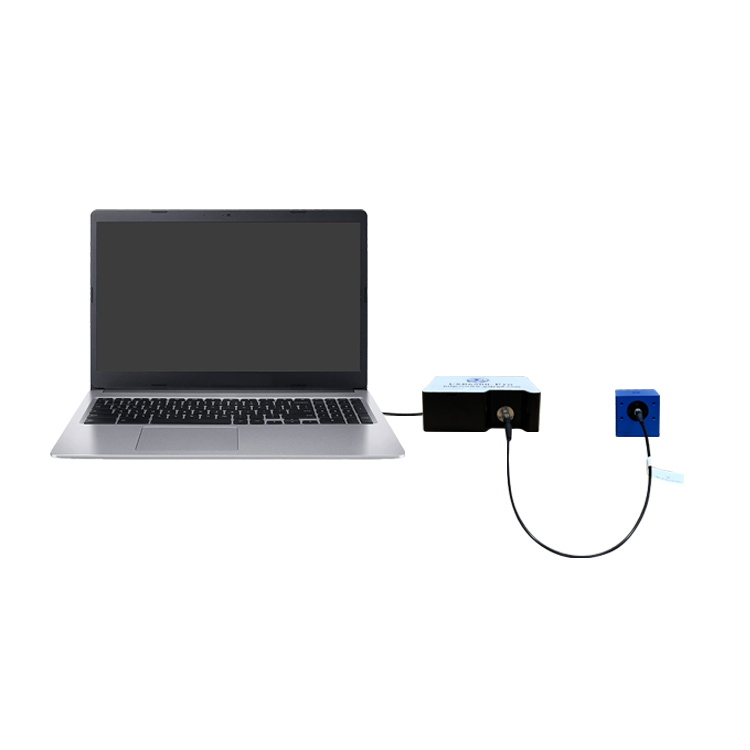
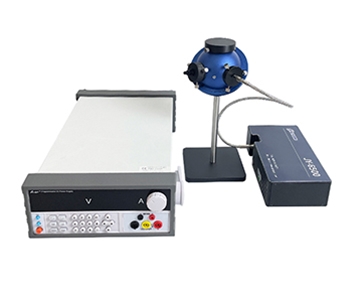
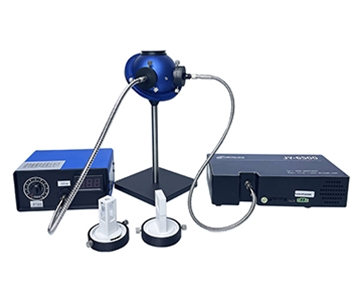
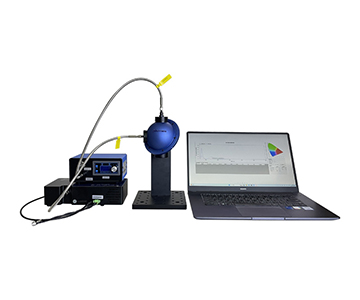
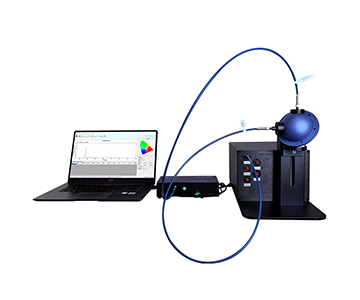
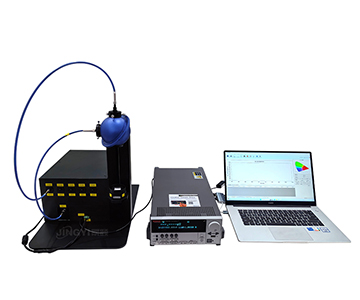
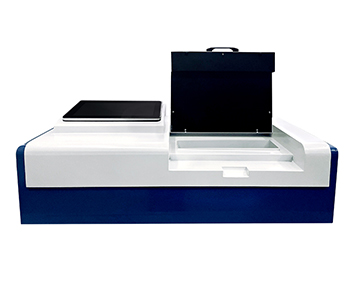
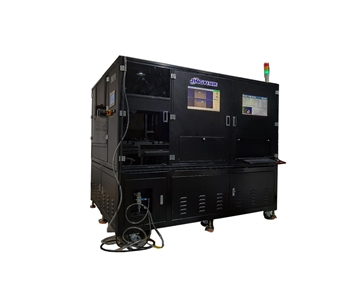
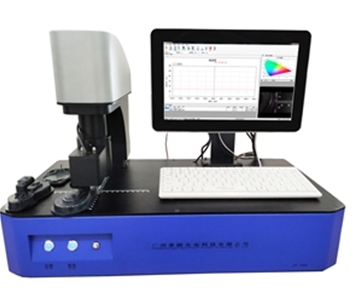
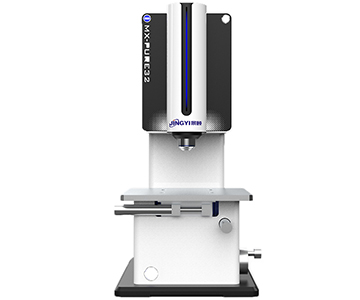
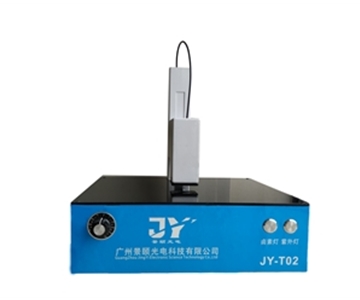
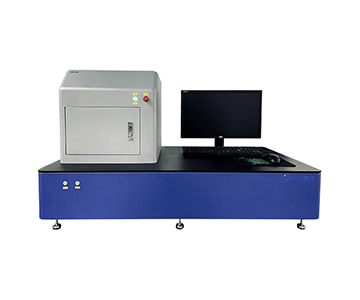
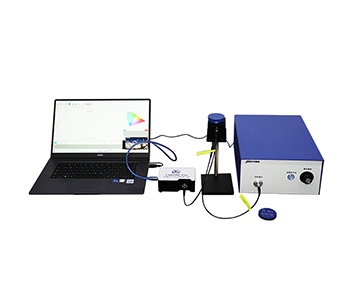
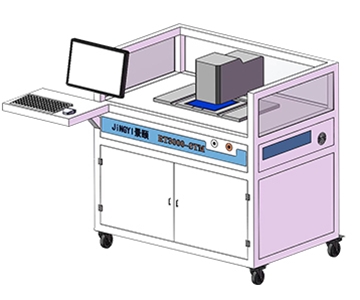
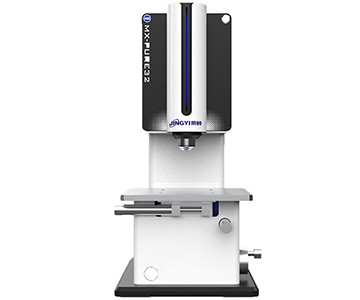
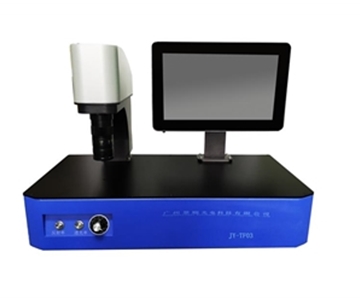
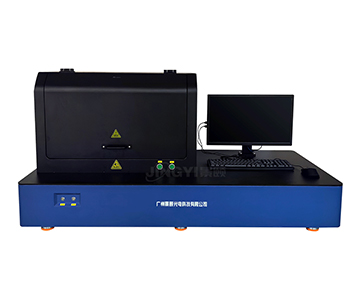
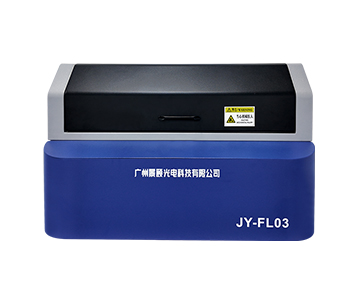
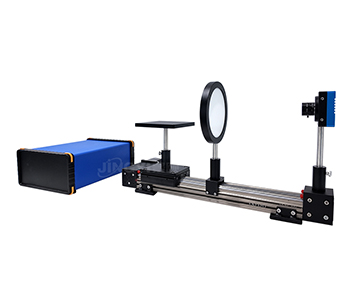
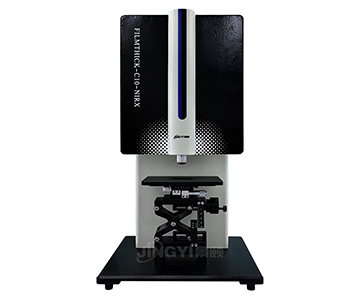
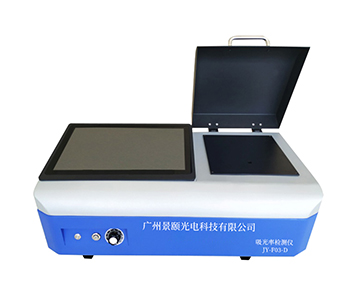
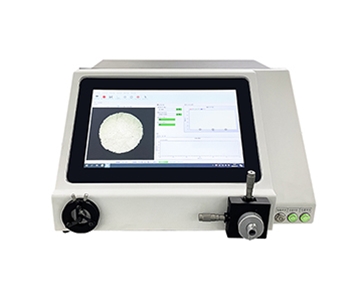
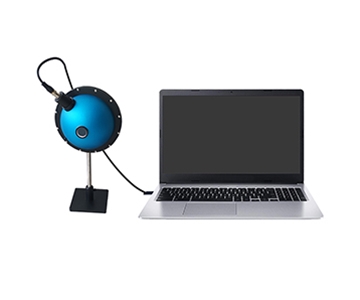
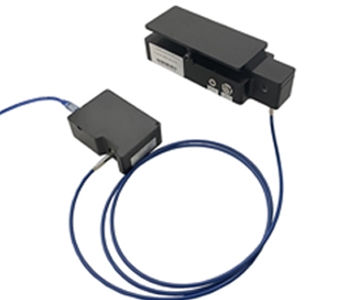
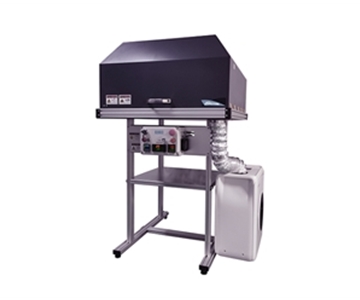
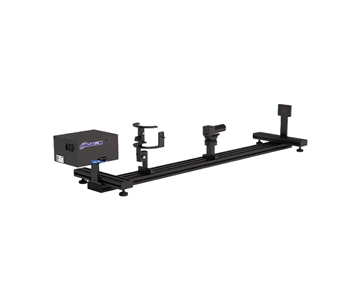
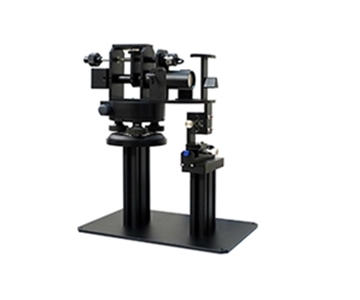
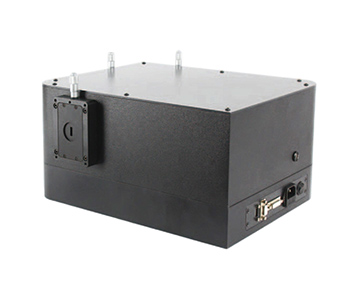
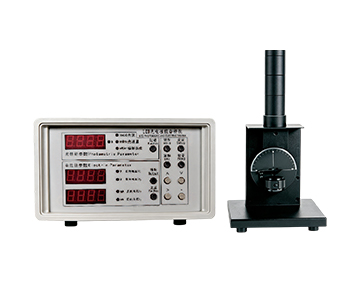
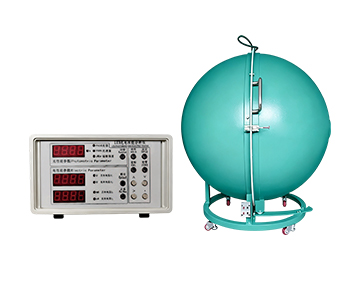
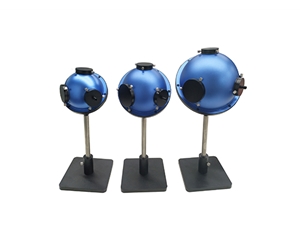
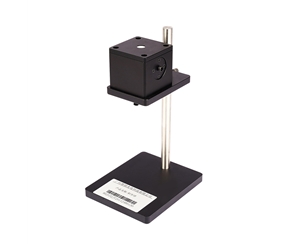
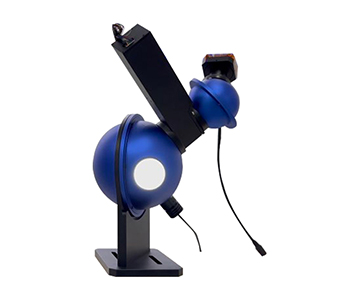
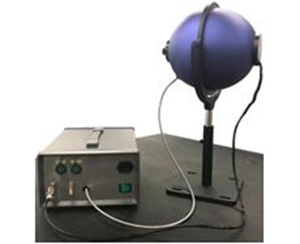
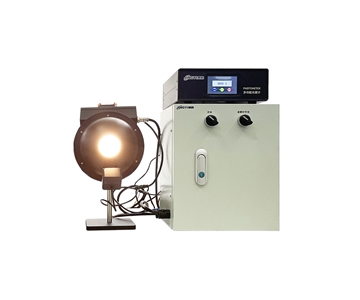
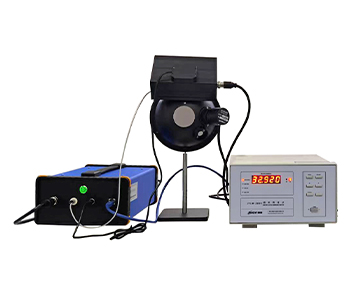
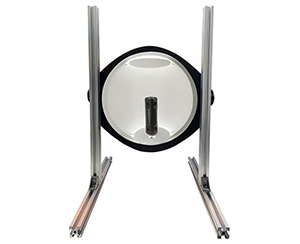
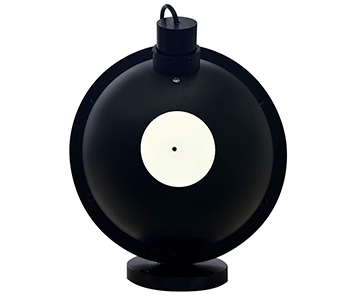
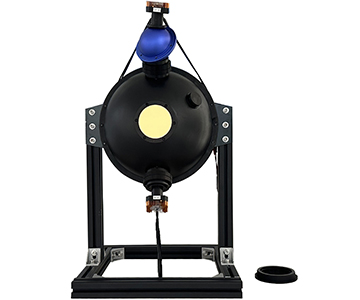
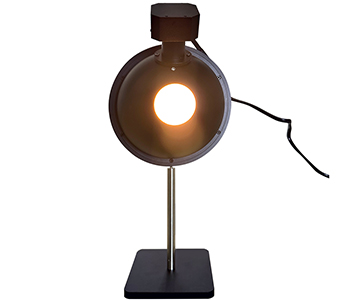
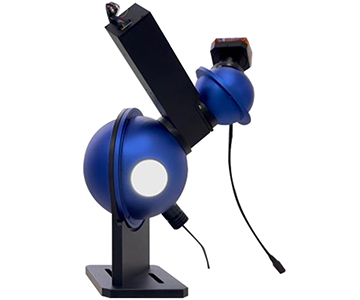
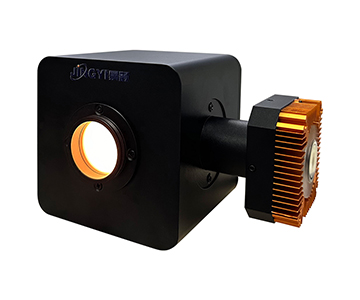
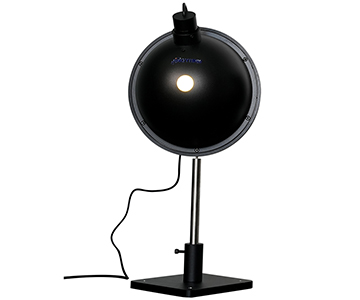
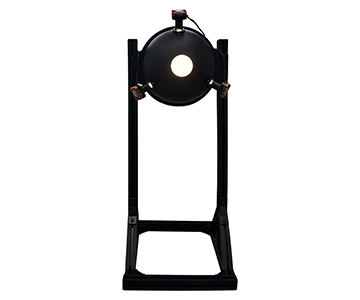
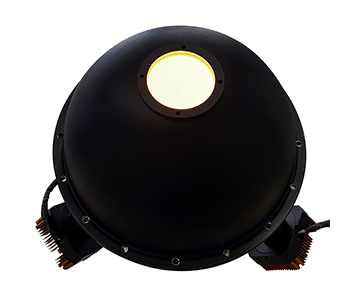
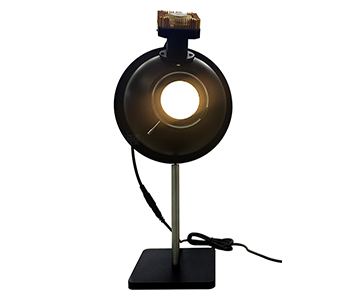
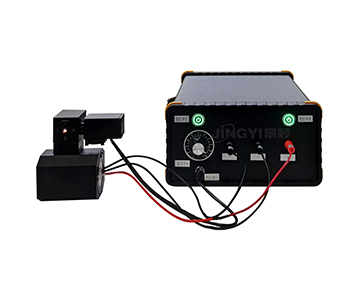
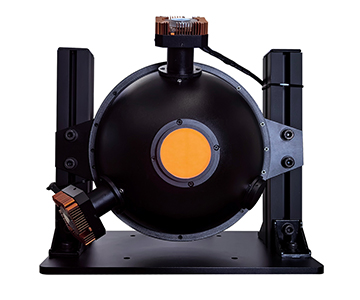
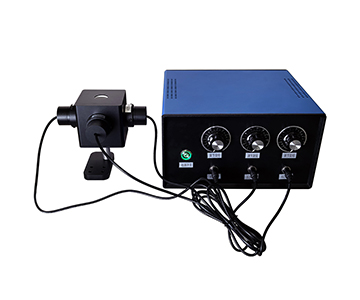
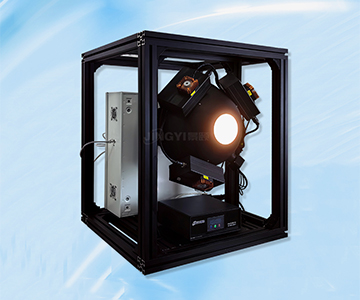
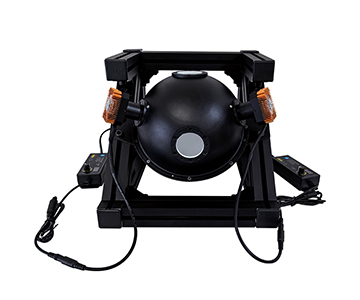
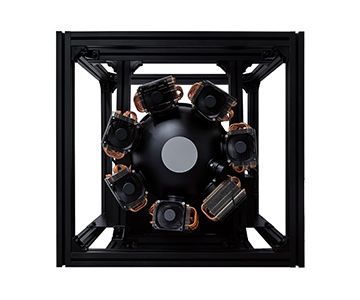
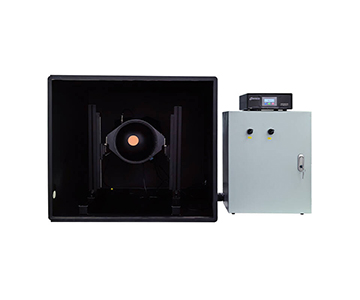
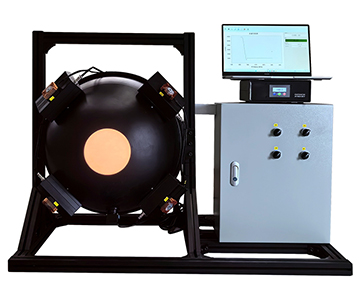
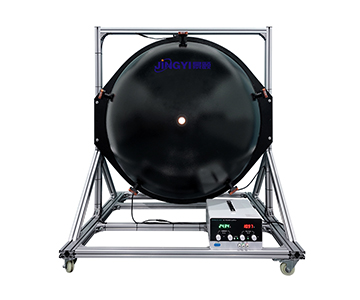
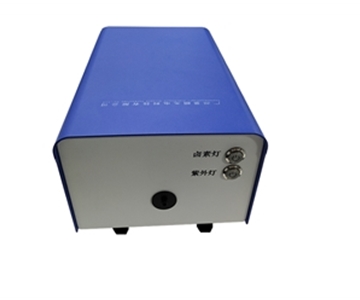
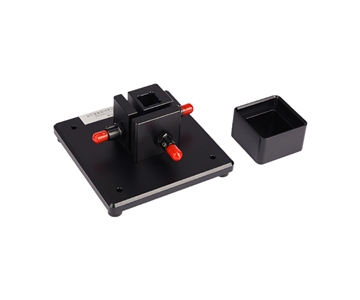
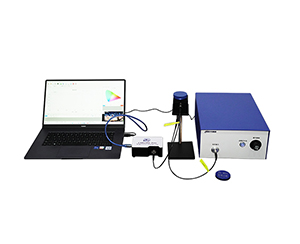
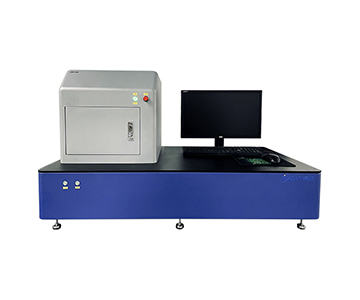
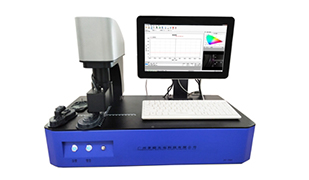
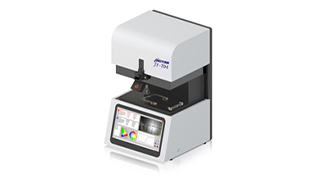
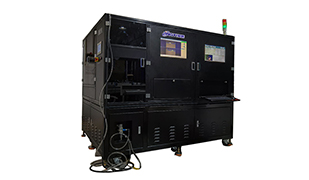
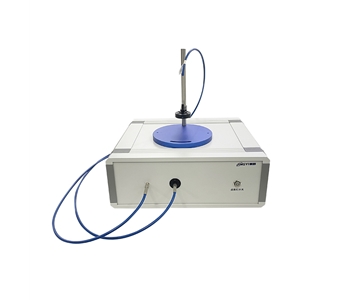
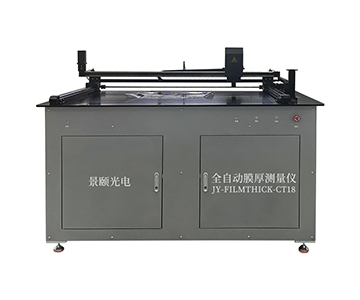
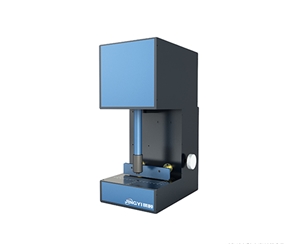
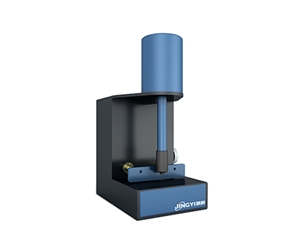
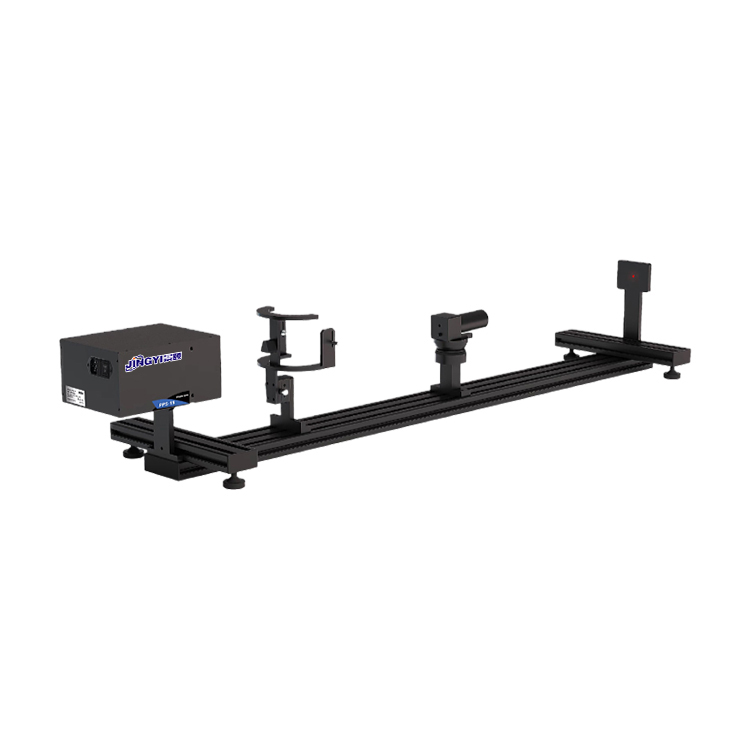
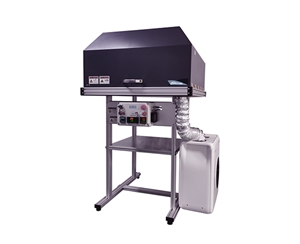
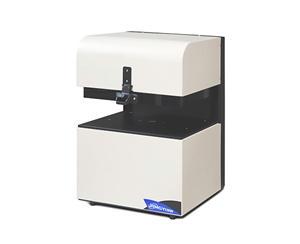
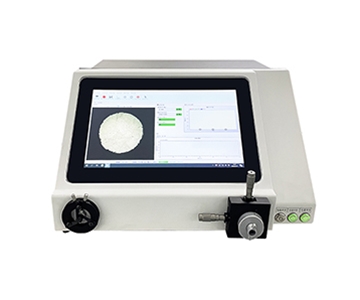
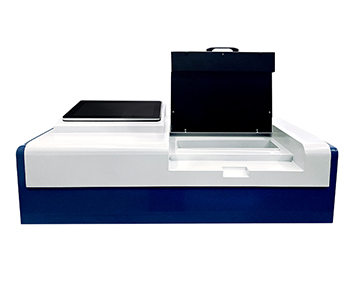
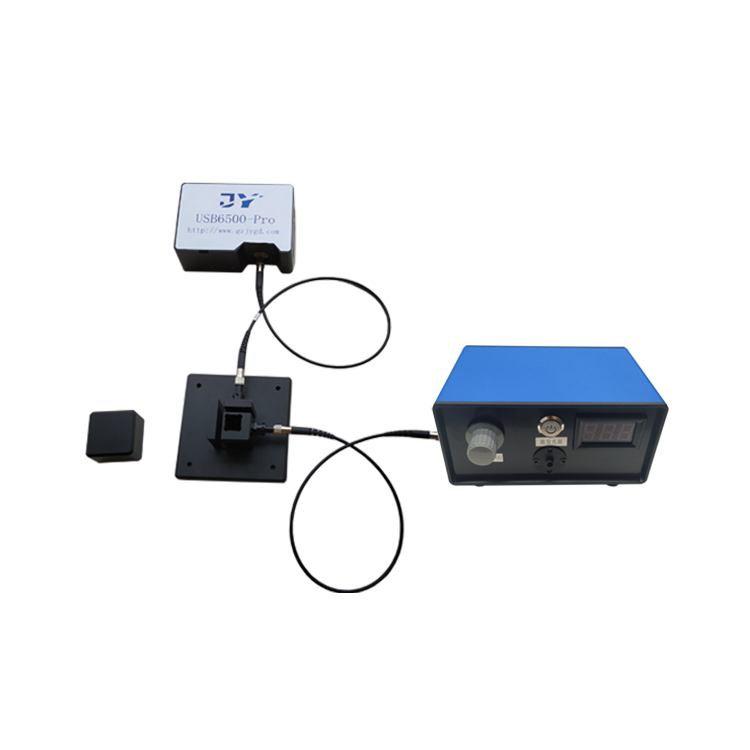
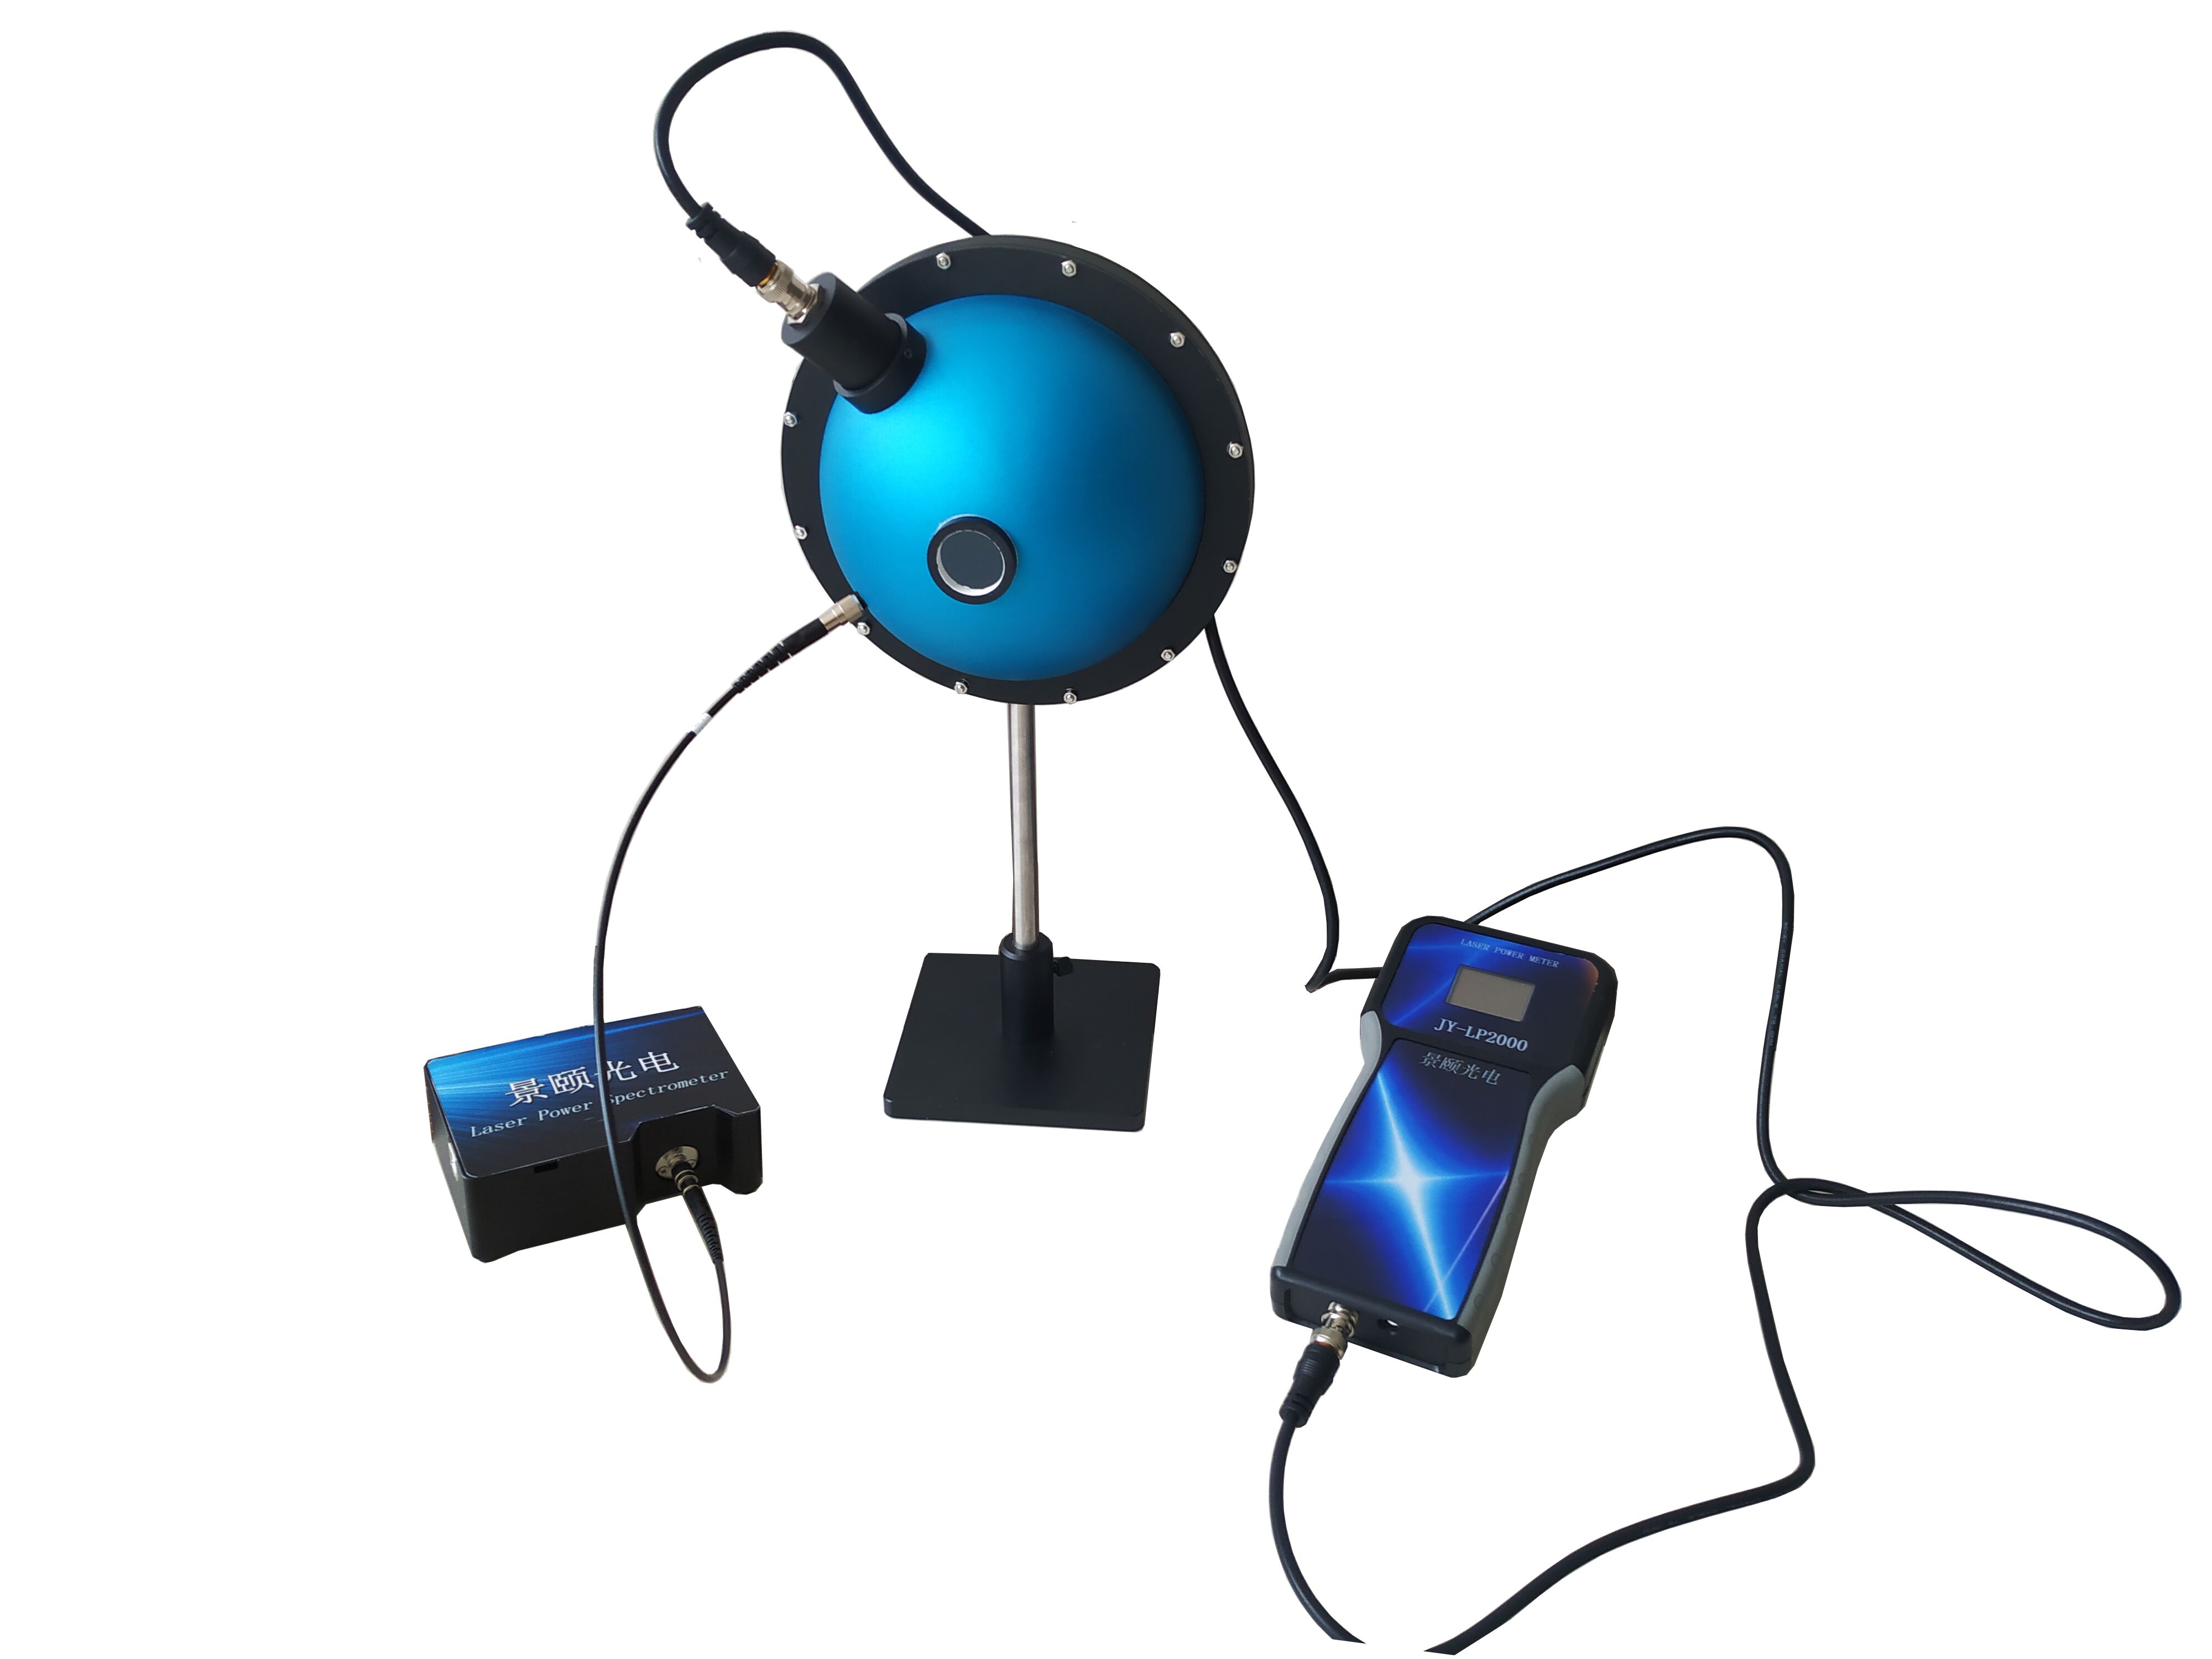
Selecting a reflectance measurement system for automotive interior rearview mirrors demands more than comparing specification sheets. Production-line compliance under UN ECE R46 and SAE J985 requires stable spectral acquisition from 400 to 1000 nm, sub-1% reflectivity accuracy, and validated operation across a –30°C to 65°C envelope. This guide breaks down seven procurement dimensions, compares three price tiers (economy, mainstream, import benchmark), and details a five-step proof-of-concept (POC) validation method. Data from in-line trials show that systems with integrating sphere and fiber-optic spectrometer architecture reduce compliance rejection rates by 37–42% compared to desktop units that lack environmental resilience.
Seven Procurement Dimensions for Mirror Reflectance Testers
When evaluating equipment, parameter tables from different vendors often look interchangeable: wavelength range, accuracy, test time, software features. What actually determines whether a system survives on the production floor is the operating boundary behind each specification.
Wavelength Coverage and Spectral Analysis Match
Testing electrochromic mirror coatings requires a 400–1000 nm band to capture visible light through the near-infrared boundary. Limiting measurement to the visible range risks underestimating night-vision performance. A mainstream optical gauge covering this span aligns with ASTM D1003 and ISO 13468 for total reflectance measurement, enabling curve-to-standard比对 verification.
Single Test Time vs. Production Cycle Time
A datasheet claiming “1 ms test time” does not guarantee a 20-second per-piece cycle. Actual throughput depends on integration time adjustability from 1 ms to 10 s. When the production line demands ≤20 s per unit, short integration must pair with automated loading and unloading to avoid workstation bottlenecks.
Reflectivity Accuracy and Reference Standard Traceability
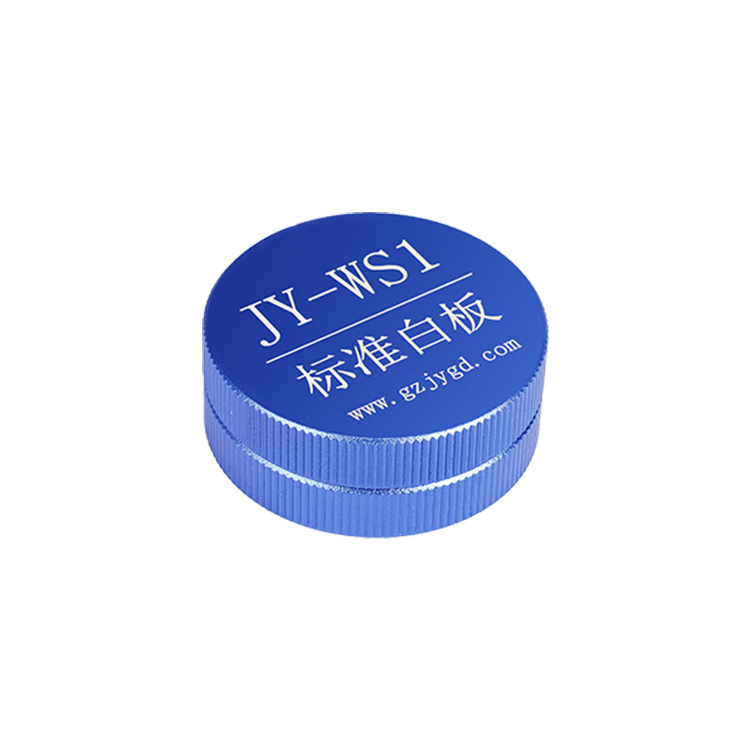
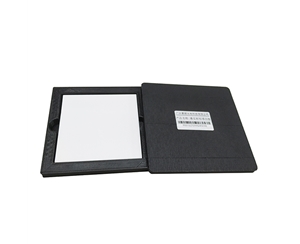
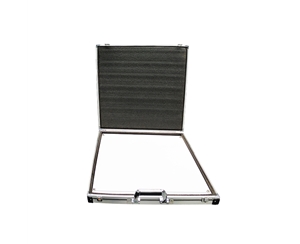
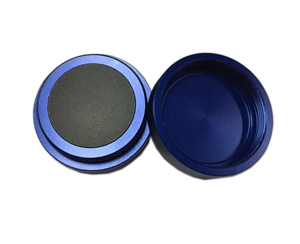
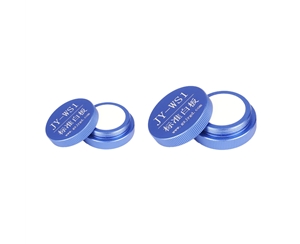
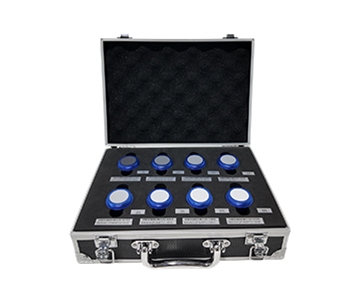
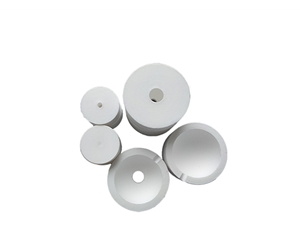
An accuracy “better than 1%” is conditional on the reference standard, not an absolute value for bare samples. Procurement teams must verify the material of the reference white board and its calibration certificate. A PTFE diffuse reflectance white board with factory calibration provides the most stable baseline. Traceability to NIST SRM 2019 or equivalent ISO/IEC 17025 accredited standards should be explicitly requested.
Temperature Range Continuous Operation Capability
High-low temperature testing splits into two approaches: moving samples in and out of a chamber, or running the entire instrument continuously at –30°C to 65°C. Only the latter satisfies transition time measurement under operating temperature as required by automotive mirror compliance protocols.
Integrating Sphere Coating and Optical Path Stability
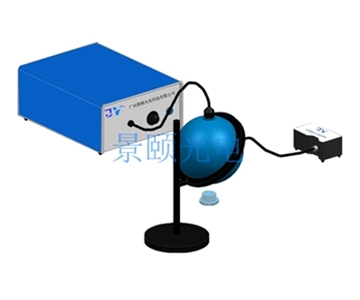
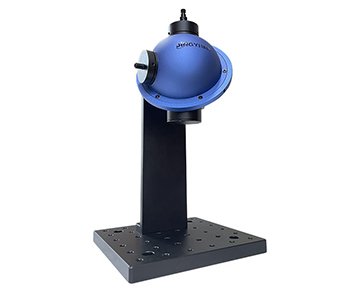
An integrating sphere coating with reflectivity better than 99% directly impacts multiple-reflection collection efficiency. Halogen light source intensity drift should be better than ±0.5% over 8 hours; otherwise, mid-test recalibration becomes necessary during extended stability runs.
Response Time Measurement and Trigger Interface
Reverse-gear response and power-failure safety functions rely on an energized test module and signal triggering. Without RS-232 or Ethernet interfaces, data must be manually transcribed—a non-starter for statistical process control.
Software Judgment and Report Traceability
Customizable pass/fail thresholds, curve export, and per-piece data binding are baseline capabilities for passing CCC-type testing (or equivalent UN ECE R46 type-approval). If the software does not allow user-defined judgment rules, threshold changes later will require manufacturer intervention.
Compliance & Calibration (Added Dimension)
Beyond the core seven, procurement must address calibration chain integrity. Systems should support ISO/IEC 17025 traceable calibration with documented uncertainty budgets. NIST-traceable reflectance standards and periodic recalibration intervals (typically 12 months) ensure measurement consistency across shifts and facilities.
Three-Tier Horizontal Comparison: Import Benchmark, Mainstream, Economy
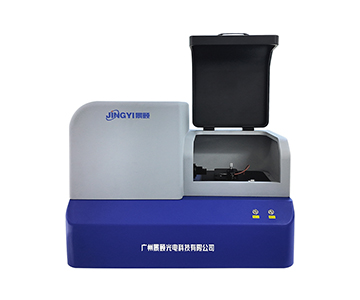
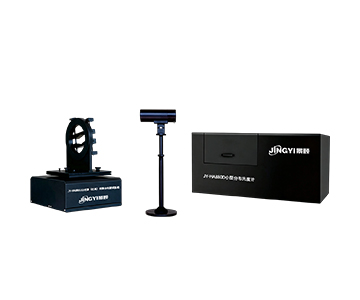
The market segments into three tiers: import benchmark, mainstream domestic, and economy domestic. Import benchmark systems are research-grade spectrometers with high price tags and academic-oriented interfaces. Economy units are mostly desktop reflectometers lacking whole-machine temperature cycling. Mainstream domestic systems close the gap for production-line adaptation.
| Tier |
Wavelength Range |
Single Test |
Reflectivity Accuracy |
Temperature Capability |
Production Adaptability |
Price Tier (USD) |
| Import Benchmark |
Model-dependent |
Slower |
High |
External chamber often required |
Weak |
$200K+ |
| Mainstream Domestic |
400–1000 nm |
1 ms |
Better than 1% |
–30 to 65°C whole machine |
Strong |
$50K–$100K |
| Economy Domestic |
380–780 nm |
1 ms |
Better than 1% |
Optional external |
Weak |
<$50K |
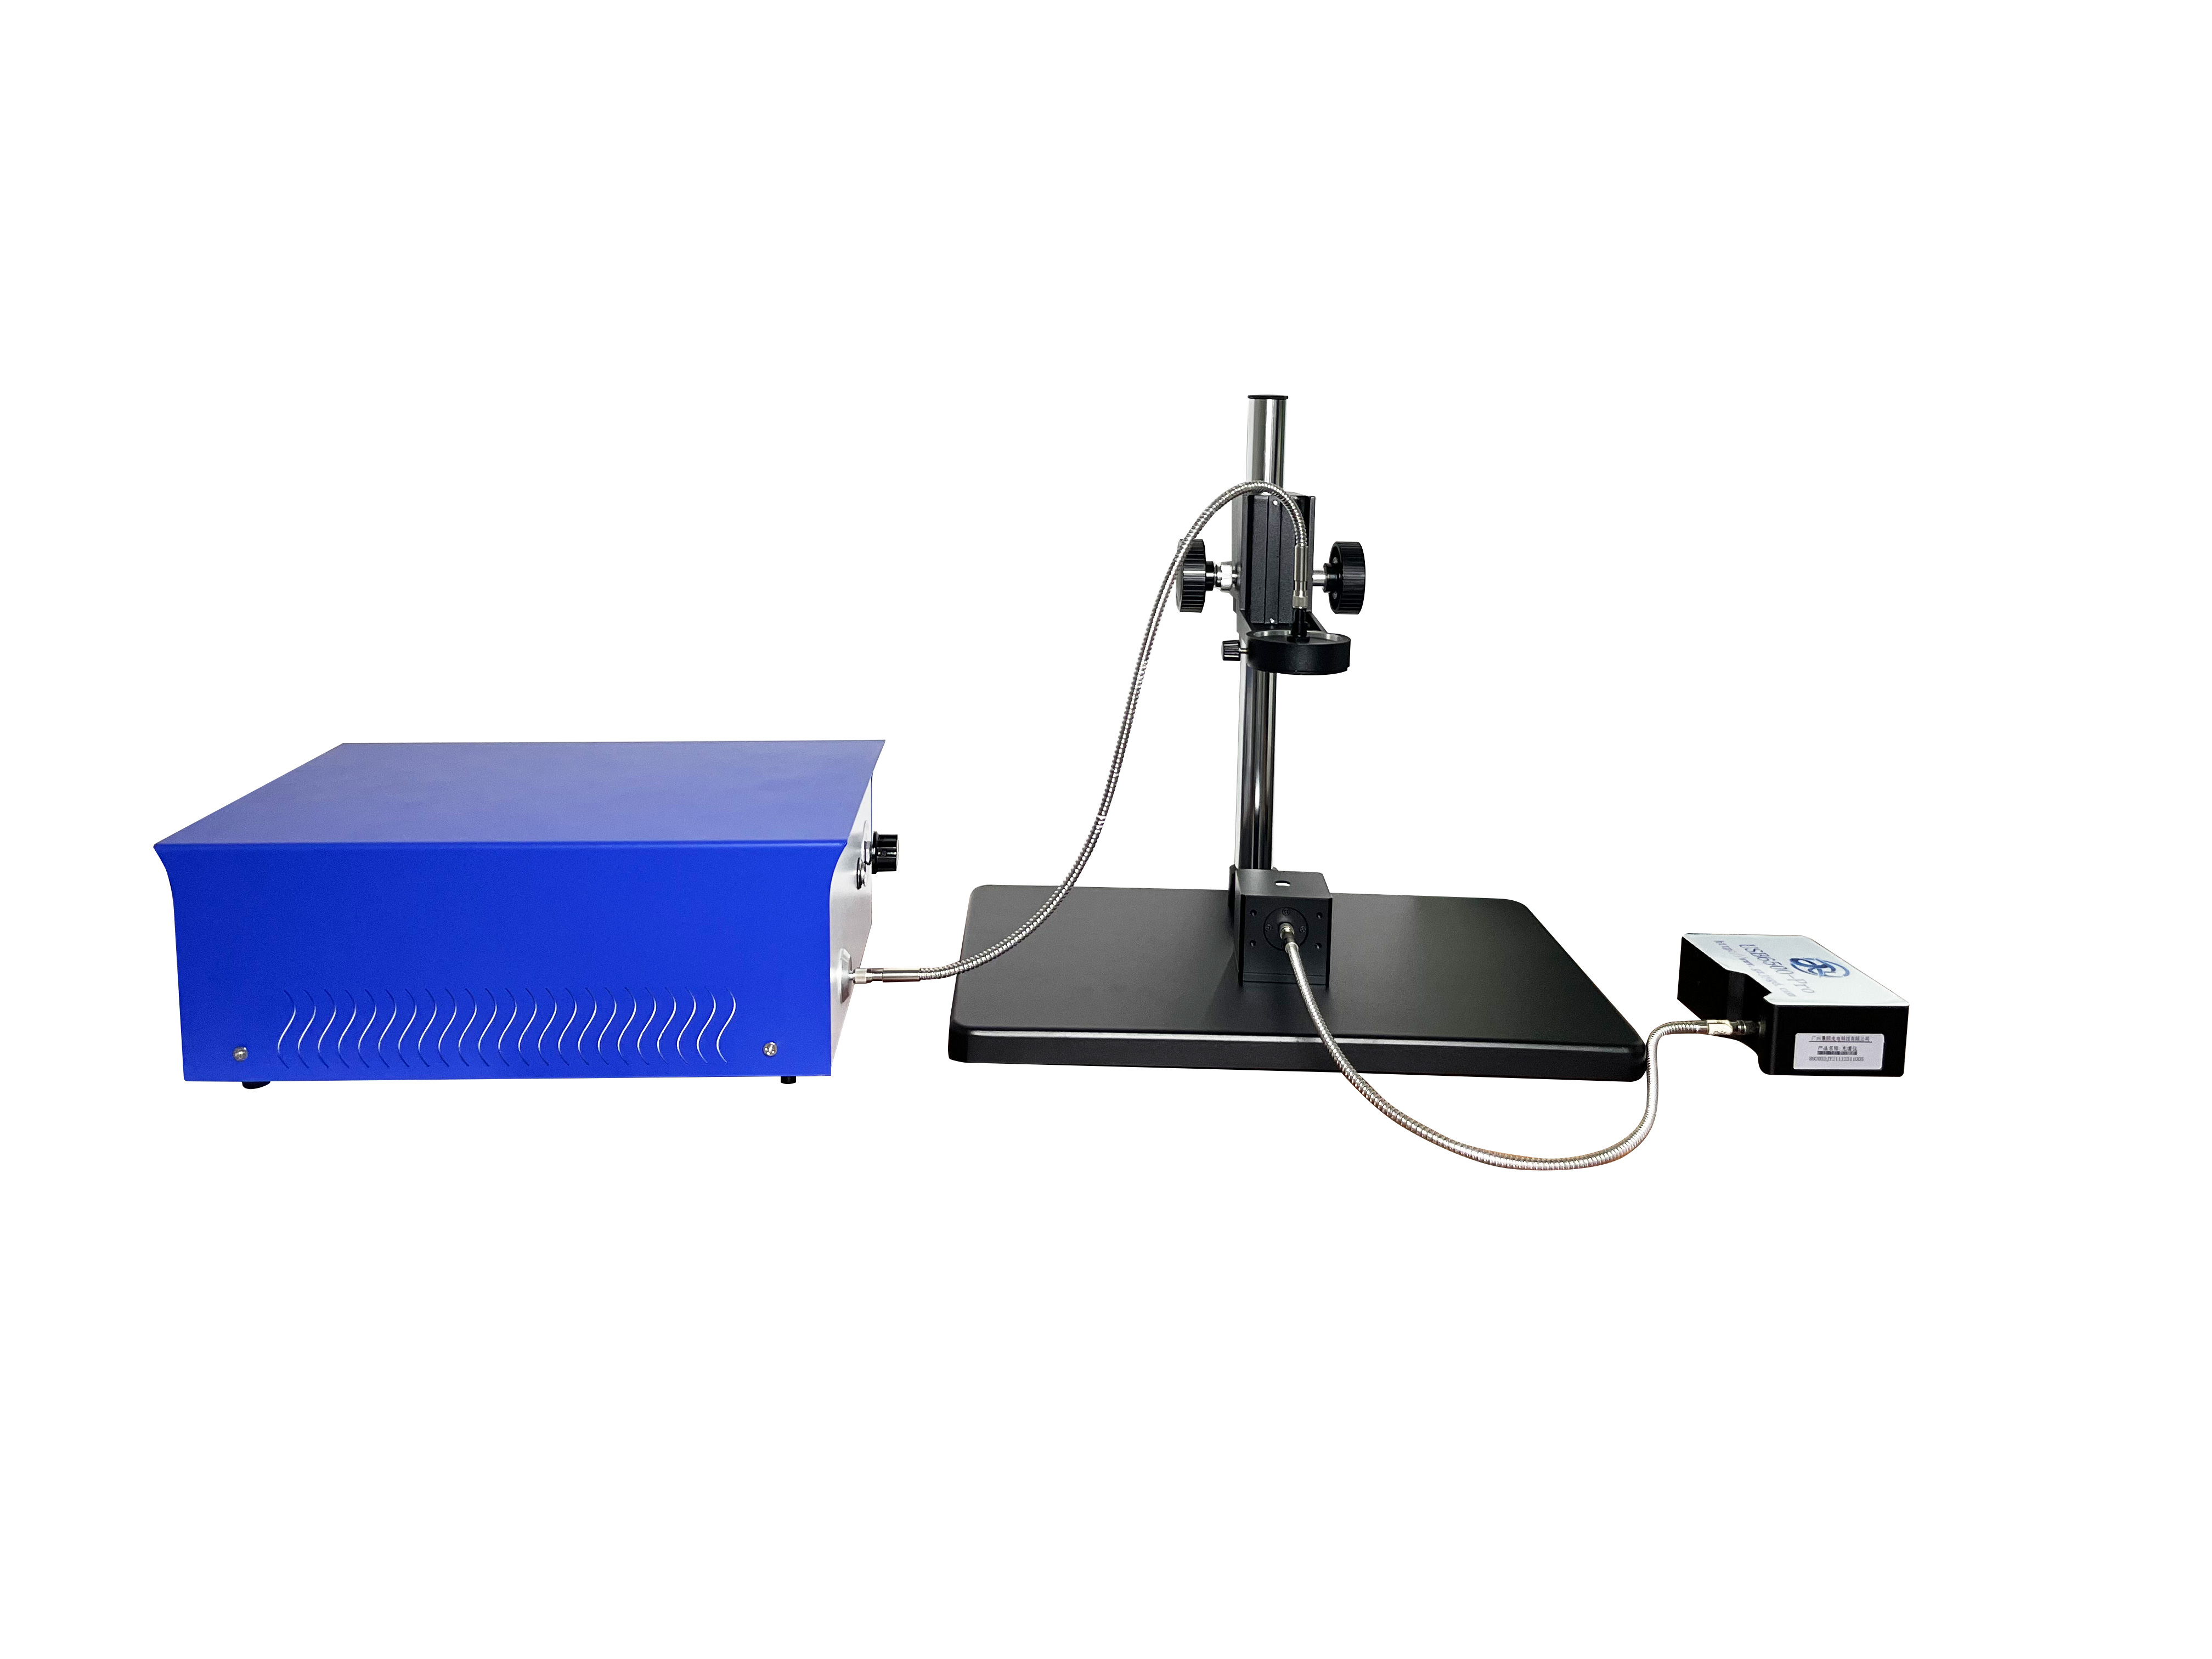
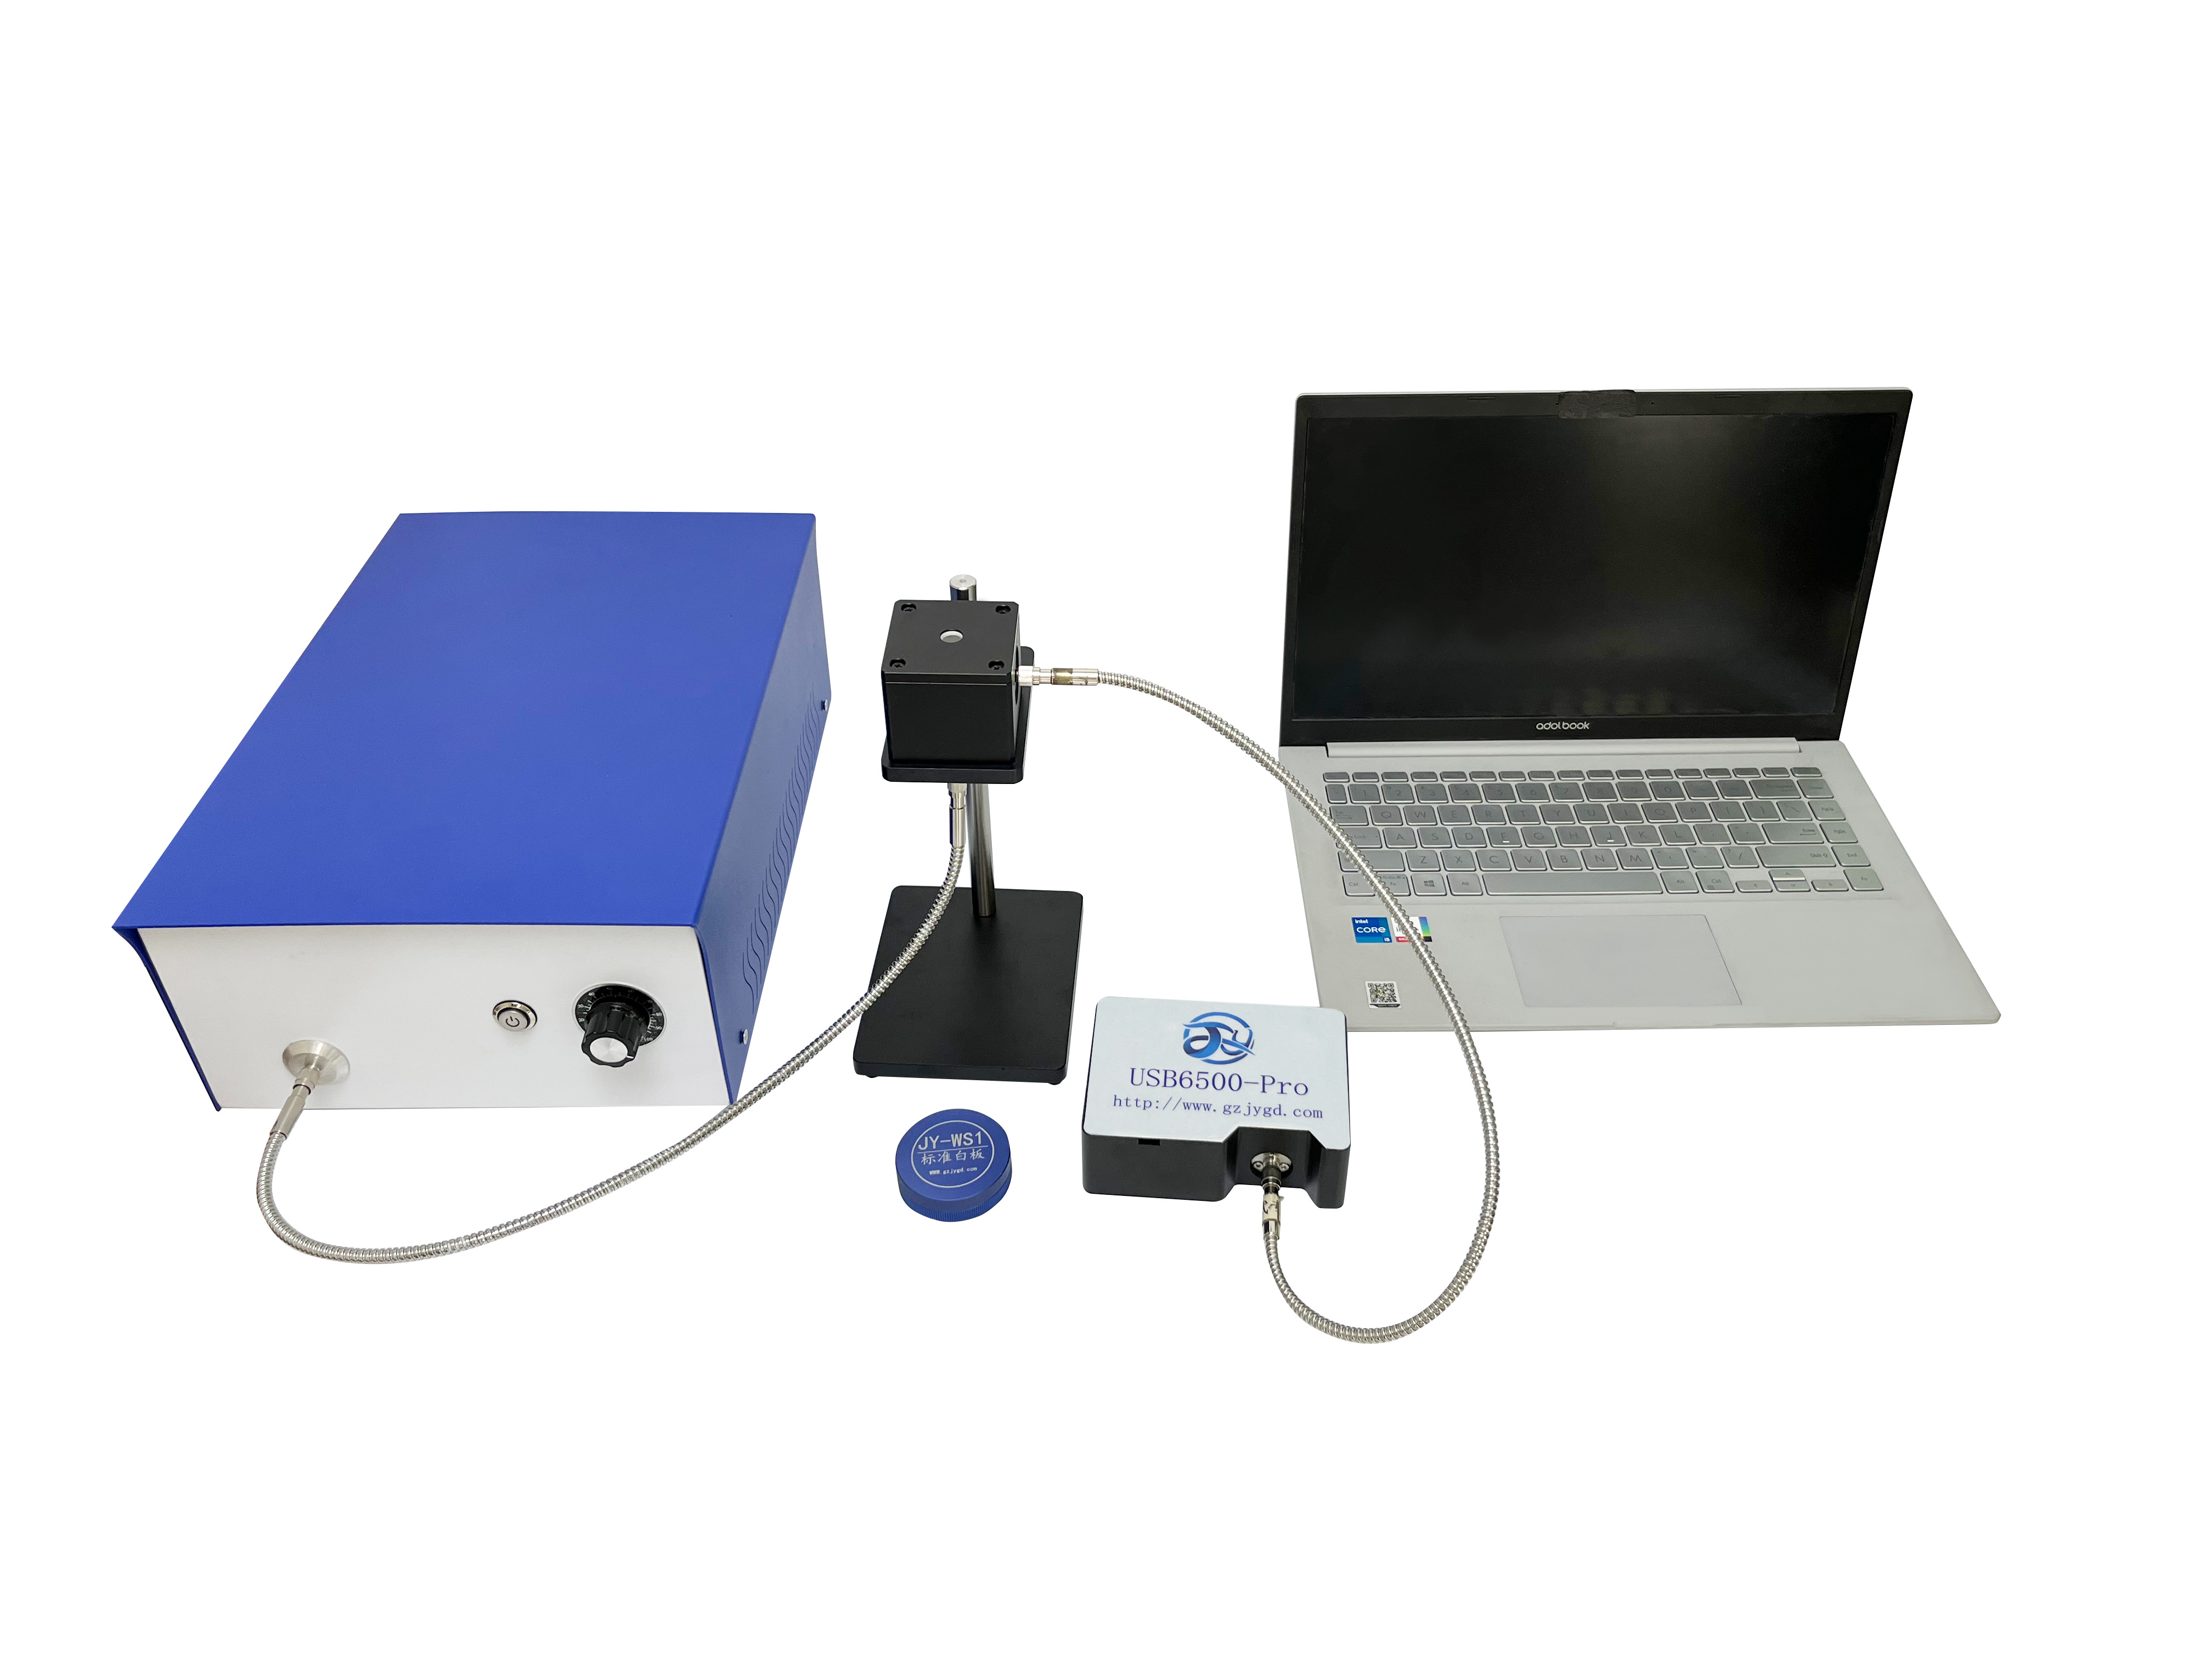
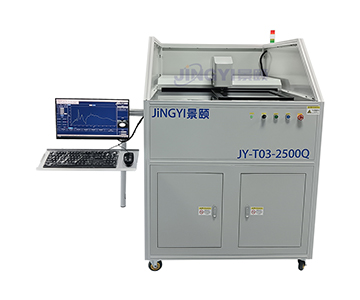
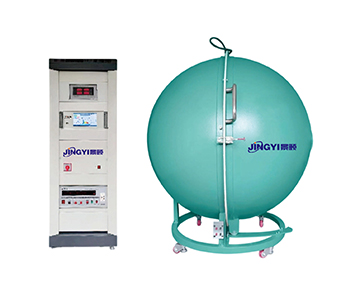
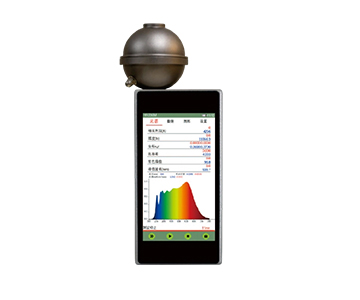
The mainstream tier delivers 400–1000 nm coverage with 1 nm sampling intervals, integrating sphere paired with fiber spectrometer. Non-energized high reflectivity thresholds (≥40%) can be set directly in software. Economy tier缩s wavelength to 380–780 nm, suitable for basic防眩 mirrors in indoor sampling, but streaming mirror near-IR data will be lost. Import benchmark excels in low-light resolution; however, long after-sales cycles and weak software localization drive total cost of ownership (TCO) beyond $250K when deployed in automotive electronics lines.
POC Validation Methodology: Beyond Demo Videos
Demo-room measurements at ambient temperature always produce clean reflectivity curves. Real validation requires three rounds on the production floor or inside a temperature chamber.
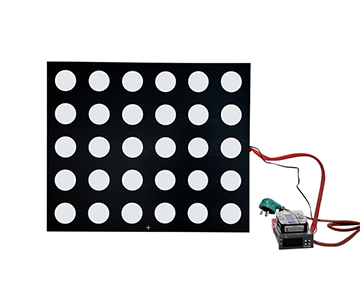
Step one: perform zero correction using a 27 mm PTFE standard white board. Record zero drift over 5 minutes; it should not exceed 0.001. Step two: measure a standard防眩 mirror in de-energized state; reflectivity should be no less than 40%. Switch to energized low reflectivity and verify against product specification thresholds.
Step three: place the entire instrument inside a temperature chamber, power on, stabilize at –30°C and 65°C for 30 minutes each, trigger state transitions, and record transition time curves. Step four: simulate reverse signal to measure response time; cut power to measure safety rebound time to high reflectivity.
Step five: perform three consecutive measurements at the same point; deviation should be less than 0.01. Five-minute stability drift should not exceed 0.005. Data jumps at any step point to optical path, light source drift, or software filtering issues.
Pre-Procurement 10-Point Checklist
1.Does the wavelength range cover 400–1000 nm?
2.Is the 1 ms test time the integration time lower limit or an averaged value?
3.Is reflectivity accuracy stated as “based on reference standard”?
4.Is high-low temperature testing performed with the whole machine or only the sample externally?
5.Is the standard white board factory-calibrated with a certificate?
6.Can software customize judgment thresholds?
7.Does it support RS-232/Ethernet data export?
8.Do reverse-gear and power-failure tests require optional energized modules?
9.What is the light source lifespan and spare parts supply cycle?
10.Can raw curves for each UN ECE R46 / SAE J985 compliance point be generated?
Common Selection Pitfalls Engineers Encounter
Low-cost desktop units labeled “compliant with UN ECE R46” often measure only de-energized reflectivity. Energized low reflectivity and transition time modules are missing entirely—the most frequent specification gap.
Another trap is confusing “1 ms test” with “1 ms result.” Integration time of 1 ms can balloon to十几 seconds per piece when averaging counts, temperature stabilization, and software refresh are factored in, collapsing production节拍.
Ignoring zero drift is equally costly: failing to verify that 5-minute drift ≤0.001 allows stability curves to drift out of judgment bands during extended runs. Using ceramic plates instead of PTFE for reference standards introduces calibration drift within six months.
Solution Boundaries and Practical Constraints
Mainstream domestic systems are not universal. For extreme cold validation below –30°C, optional wider-temperature environmental chambers are required; otherwise, external testing must be outsourced. Without near-IR extension components, samples involving >850 nm camera联动 can only be estimated.
Software customization depth also poses limits: judgment rules can be modified, but report format integration with OEM MES systems requires project-level joint debugging—not plug-and-play. Unmanned production line retrofits often stall at interface protocol confirmation rather than hardware capability.
Frequently Asked Questions
Q1: How is reflectivity accuracy “better than 1%” actually verified?
Use a standard white board as reference, measure the same point three times consecutively; deviation less than 0.01 places the system within the stated accuracy interval.
Q2: Can manual day-night mirrors and auto-dimming mirrors be tested on the same unit?
Yes. De-energized high reflectivity covers manual mirrors; auto-dimming mirrors require the energized test module for low reflectivity and response measurement.
Q3: Is 1 ms test time suitable for 100% in-line inspection?
Single-point acquisition is feasible, but achieving ≤20 s per complete unit requires automated handling and short integration coordination; otherwise cycle time exceeds limits.
Q4: How to choose between import benchmark and mainstream domestic tiers?
For laboratory R&D and fundamental research, import benchmark offers superior weak-light resolution. For automotive electronics production-line compliance testing, mainstream domestic delivers controllable TCO and shorter calibration chains.
Q5: How can I independently verify whether a reflectance tester meets production requirements?
Execute the five-step POC outlined above using standard white boards and high-low temperature transition curves, then cross-check against UN ECE R46 or SAE J985 compliance points with your own quality team.
Conclusion
Selection is not about which specification sheet looks prettier, but which system can reproduce stable curves under temperature cycling and节拍 pressure. Running a POC with actual samples before purchase outweighs reviewing ten pages of brochures.
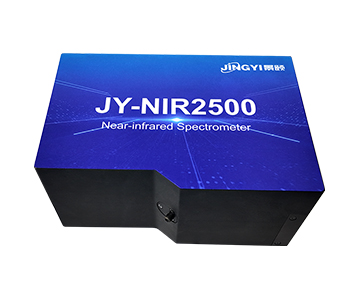
For detailed specifications and application notes on rearview mirror reflectance testers, search “Jingyi Optoelectronics rearview mirror reflectance tester” or visit our technical library.
About This Guide
Data Sources
: In-house validation reports (n=37 mirror assemblies), UN ECE R46 regulation, SAE J985 standard, ASTM D1003-20, ISO 13468-1:2019, product technical documentation from Jingyi Optoelectronics.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and industrial precision measurement.
Disclosure
: Jingyi Optoelectronics manufactures rearview mirror reflectance testing systems. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: October 2026