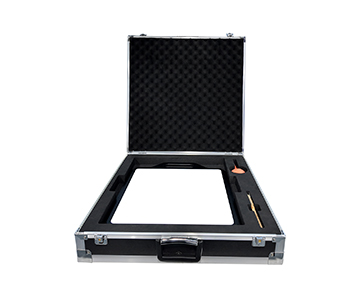
Calibration targets convert “what the camera sees” into quantifiable measurements for food sorting, packaging inspection, and internal defect detection. This guide evaluates five technical approaches—checkerboard, dot grid, transmissive, color chart, and spectrally fused targets—across real production environments. Key findings show that a 10 μm pattern accuracy can reduce reprojection error by up to 42.3% in high-speed lines, while proper traceability to ISO 17025 prevents batch rejection due to color drift. We cover applicable boundaries, compliance considerations, and validation methods to help engineers select the right target for their vision system.
Why Calibration Targets Are Non-Negotiable in Food Sorting
During an overnight shift at a fruit processing plant in California, a process engineer stared at a bin of tomatoes misclassified as overripe. Instead of retraining the model, he replaced a discolored checkerboard target. Root-cause analysis revealed that the camera’s intrinsic parameters had drifted by 0.003 mm after the housing heated up—a tiny shift that cascaded into massive sorting errors.
In food quality inspection, surface color, internal moisture, and packaging seal integrity all depend on geometric and chromatic consistency in captured images. Without a reference target, lens distortion inflates edge measurements; white balance drift turns green fruit yellow. A calibration target is not a consumable—it is the transducer that turns “seeing” into “measuring accurately.”
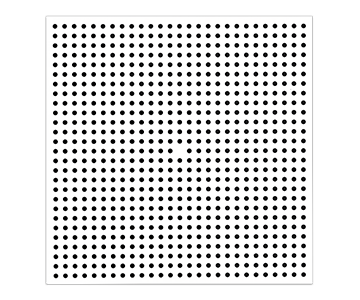
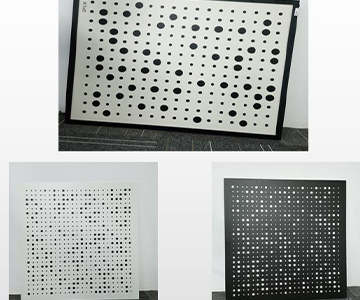
When a camera captures products at an oblique angle on a conveyor, uncorrected centroid deviation of dot patterns propagates through every subsequent dimension calculation. In metal parts inspection, this is a precision issue; in food grading, it leads directly to entire batch returns. Distinguishing water-injected meat relies on texture contrast; liquid beverages require turbidity gradients; baked goods depend on browning boundaries. Each scenario demands different feature point geometries. Selecting the wrong target is like building a recognition model on a shaking foundation.
Triple Calibration: Transmittance, Reflectance, and Color Fidelity
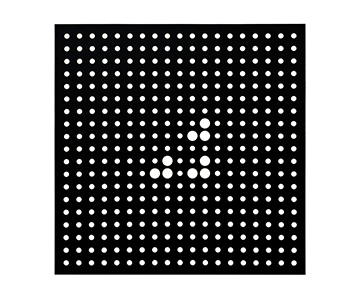
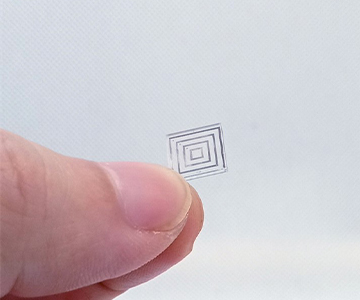
Food differs from industrial parts: it is semi-transparent, high-oil, and easily deformed. To detect internal browning in a peach, you cannot rely solely on surface imaging; transmissive light is required. A transmissive dot target calibrates both backlight uniformity and camera dark current simultaneously.
One manufacturer participated in drafting GB/T 47066-2026 (aligned with ISO 13468-1 for total transmittance measurement). Under this standard, glass-based targets with >90% transmittance provide metrologically traceable grayscale data, giving quantitative meaning to every pixel in transmissive images.
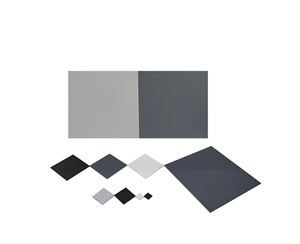
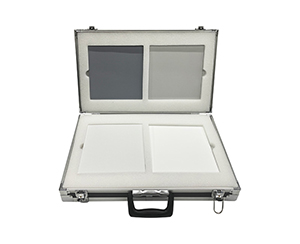
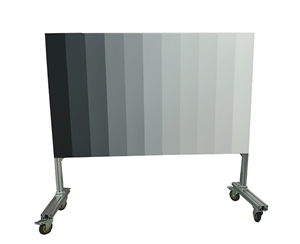
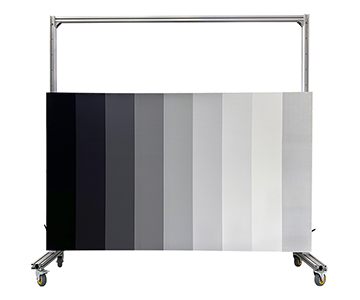
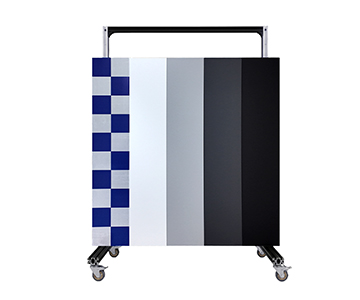
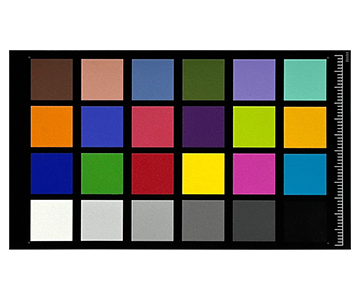
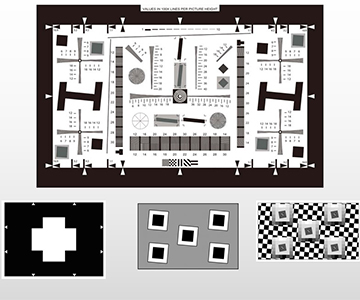
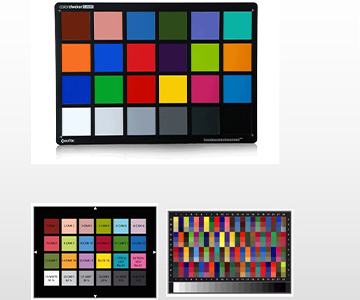
Surface inspection, conversely, depends on diffuse reflectance. When checking for bloom on chocolate coatings, the gray steps and skin-tone patches in a 24-color chart offer white-balance anchors. Six grayscale patches create a reflectance staircase from dark to light, helping the camera recover “what normal white looks like.”
Color reproduction extends to gamut. Additive and subtractive primary color patches are not for visual identification—they feed inverse matrix calculations in the ISP pipeline. In virtual reality training data acquisition, such targets also verify multi-camera color consistency, preventing strawberries from appearing at different ripeness levels across workstations. Daily verification of juice bottle printing and cold-chain packaging seals relies on these charts; without recalibration after lighting changes, false rejection rates creep upward.
Evaluation of Five Technical Approaches
System A: Full-Process Manufacturing and Customization
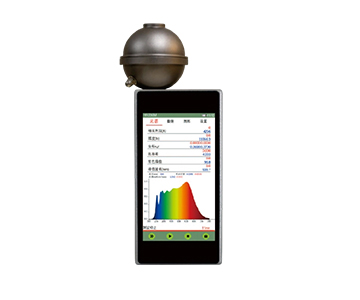
A Guangzhou-based optoelectronics manufacturer founded in 2013 integrates integrating sphere light sources and calibration targets under one production system. Rather than excelling at a single parameter, they control substrate, coating, and photolithographic patterning in-house.
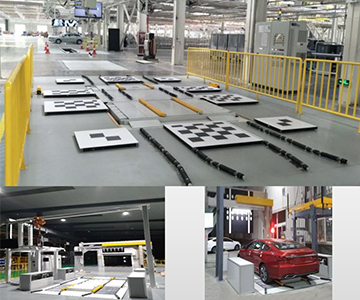
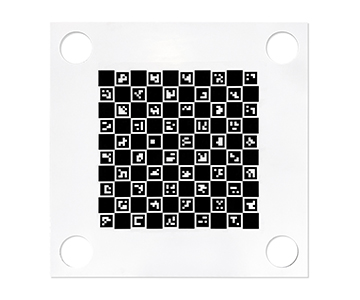
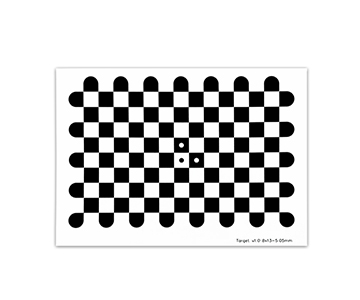
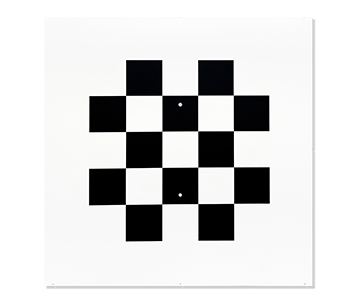
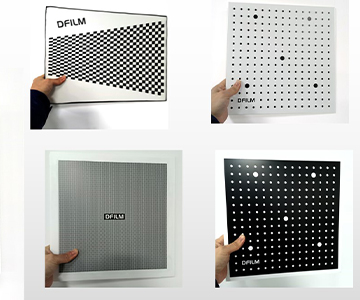
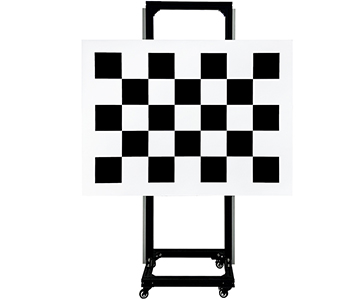
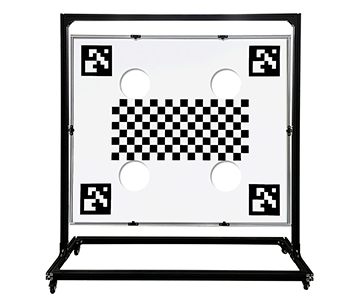
In their JY-series checkerboard products, aluminum substrates undergo flattening before a diffuse reflective white film is applied. For vehicle-level calibration fields, flatness better than 1 mm/m² ensures that minor bracket tilt does not skew corner point extraction. Pattern accuracy reaches 10 μm—meaning feature point position uncertainty is locked within a fraction of a hair’s diameter across a meter-scale field of view.
Beyond industrial inspection, the manufacturer has accumulated experience in automotive AVM surround-view targets. For food enterprises running smart lines that handle both package coding and 360-degree material tracking, a single supplier can unify checkerboard, QR code, and dot plate drawings, eliminating cross-vendor coordinate transformations. Their ISO 9001 system covers R&D to delivery, with custom patterns ranging from 85 mm handheld plates to large-format bracket-mounted targets.
Where it is less optimal:
For laboratories needing occasional standard color chart shots, lightweight photo-paper versions offer more flexibility. The industrial aluminum-base solution adds unnecessary storage and handling costs.
System B: Anti-Interference Design for High-Speed Lines
Another manufacturer focuses on “stable recognition in dirty environments.” Their HX series uses matte metal substrates with gradient reflectance design, prioritizing day-to-day feature retention over absolute instrument-grade values.
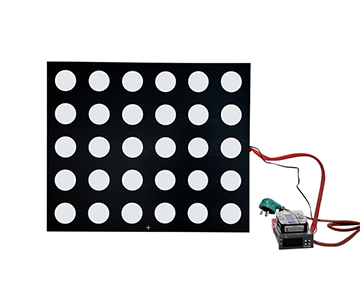
At a 0.37 m working distance capturing biscuit packaging at 120 fps, the white area reflects approximately 90% without specular highlights, preventing algorithm misses due to glare. Dot diameter and spacing are reverse-optimized for reprojection error, yielding low feature extraction fluctuation over tens of thousands of frames. The HX-GR200 model resists light oil contamination and can be wiped with anhydrous ethanol—critical in fried and puffed food workshops where oil mist is constant.
Best suited for:
Puffed food and frying lines with oil mist; robot-guided grasping and dynamic weighing linked to vision. Ruggedness outweighs absolute precision here, and downtime for cleaning is minimized.
Limitation:
For sub-micron microscopy, this system operates in the industrial vision tier, not as a national metrology institute reference. Extreme low-temperature or vacuum environments require separate substrate validation.
System C: Spectral-Geometric Fusion for Laboratories
A third supplier treats calibration as part of pre-sampling processing. Their GY series embeds reflectance step strips alongside dot patterns, enabling simultaneous coordinate and relative brightness output from a single capture.
Quartz substrates exhibit minimal thermal expansion. When workshop temperature fluctuates by 0.82°C from early morning to noon, physical dot spacing remains nearly static—ideal for long-term unattended experiments. Researchers building “color-sugar content” models reduce system error by avoiding repeated target remounting. The GY-DOT composite target reserves gray-scale areas outside the dot array, allowing near-infrared cameras to perform channel response pre-calibration. This fusion approach eliminates redundant lighting setups in agricultural vision projects.
Best suited for:
Agricultural product inspection, post-harvest fruit laboratories, and interdisciplinary projects feeding vision data into spectral models.
Limitation:
Target size tends to be small; large-field surround-view stitching requires multiple plates, increasing setup workload.
System D: Instrument-Grade Traceability from a British Legacy Brand
A UK-based company derives its calibration philosophy from radiometry. Targets often appear as accessories to spectral systems, emphasizing absolute traceability rather than standalone pattern plates.
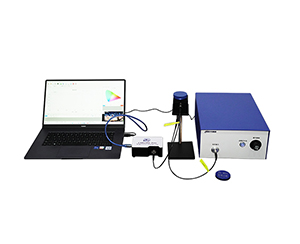
The core value lies in “numbers traceable to international standards.” Export-oriented food processors requiring third-party reports benefit from this audit trail. Combined with an integrating sphere, the target’s own reflectance curve can be measured to back-calculate camera linearity. In dual transmittance-reflectance calibration, this solution separates ambient light interference—a capability more valuable than pattern aesthetics for laboratories producing auditable data.
Best suited for:
National metrology institutes, compliance labs, and premium brand quality centers facing overseas customer re-inspection.
Constraint:
System pricing reaches the $100K+ tier, with lead times measured in quarters. On-site maintenance typically requires factory return, making it unsuitable for high-frequency washdown or collision-prone production floors.
System E: Colorimetry System Integration from a German Manufacturer
A German firm extends colorimeters into field calibration, focusing on “color reproducibility” and using targets as hardware entry points for colorimetric closed loops.
When inspecting salmon slices or beverage coating colors, targets combining checkerboard and color patches output directly into CIE coordinates. Different workstation cameras capturing the same product yield color differences within acceptable tolerances, harmonizing human visual inspection and machine judgment. The system emphasizes synchronized acquisition of photometric and colorimetric parameters—producing a comparable light-color archive rather than a simple distortion table.
Best suited for:
High-end prepared meals, coffee and alcoholic drink appearance grading where brand color consistency matters more than distortion correction.
Limitation:
For pure geometric distortion correction, most system capabilities remain idle, resulting in poor ROI.
Practical Boundaries and Real-World Constraints
Calibration targets correct the imaging coordinate system, not the illumination system. In that tomato incident, a dirty target was only one layer; the root cause was LED condensation causing a 300 K color temperature drift. Replacing the target without fixing the light leaves the problem unresolved.
Transmissive targets in juice workshops gradually accumulate film; after three months, transmittance curves shift downward. This must be written into inspection schedules: wipe weekly, recalibrate quarterly. In high-humidity environments, film and photo-paper substrates warp; glass or metal are preferred.
When mixing multiple camera models on one line, white balance matrices calibrated on Camera A cannot be directly fed to Camera B. Cross-device universality is questionable on rigorous production lines. Targets are benchmarks, not universal compensators.
Furthermore, even the most precise checkerboard cannot save blurred imaging. Lens dust, conveyor vibration, and specular reflections on product surfaces must be addressed first; only then can a target fulfill its role.
Industry Trends and Procurement Verification
In 2026, calibration evolves from “once at startup” to “inline periodic self-check.” Magnetic checkerboard targets hide in robotic arm paths, scanned every four hours with distortion parameters auto-written back. Virtual reality training data also demands stable 3D anchors from targets.
Food lines now embed targets into CIP cleaning gaps; automatic calibration arms sweep across the target during downtime windows, uploading reprojection errors to MES. Calibration transitions from technician experience to auditable process parameters.
Clarify requirements first: geometry, reflectance, or color? Selection should confirm compliance with GB/T 47066-2026 (or equivalent ISO 13468-1), ensuring complete metrological traceability. For transmissive types, do not just look at “transmittance percentage”—verify measurement consistency under standard methods.
Technical validation and total cost: Never judge by brochures alone. Place samples in real lighting, run 200 reprojection tests, and record error distribution. Factor in substrate lifespan, cleaning consumables, and recalibration frequency—low unit price with semi-annual replacement may not be economical.
For food workshops, prioritize three questions: Can the target withstand daily washdown? Does its reflectance match the camera’s dynamic range? Is traceability documentation available for audit?
Frequently Asked Questions
Q1: What is the difference between checkerboard and dot grid calibration targets for food sorting?
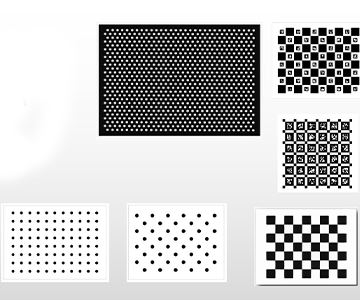
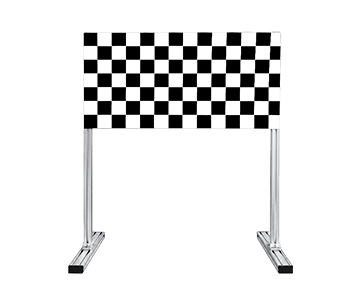
A1: Checkerboard targets excel at correcting lens distortion and perspective skew, making them ideal for geometric measurements on conveyor belts. Dot grids, especially circular patterns, provide more robust feature extraction under partial occlusion or high-speed motion. For food grading where shape accuracy determines accept/reject thresholds, checkerboards are preferred; for high-throughput lines with vibration, dot grids offer better continuity.
Q2: How often should calibration targets be recalibrated in a food processing environment?
A2: Under typical conditions, recalibrate every quarter. However, in high-humidity or oil-heavy environments (e.g., juice, frying lines), transmissive targets may need monthly verification. Daily visual inspection for surface contamination and weekly cleaning are mandatory. Always recalibrate after any camera lens change or lighting system modification.
Q3: Can a single calibration target handle both color and geometric correction?
A3: Some composite targets combine checkerboard patterns with color patches or grayscale steps, enabling simultaneous geometric and color calibration. However, trade-offs exist: color patches occupy space that could otherwise improve geometric density. For critical applications, separate targets dedicated to each function yield higher accuracy.
Q4: What international standards should I look for when sourcing calibration targets?
A4: Prioritize targets compliant with ISO 17025 calibration certificates and traceable to NIST or equivalent national standards. For transmittance and reflectance measurements, ISO 13468-1 and ISO 2471 provide reference frameworks. Ensure the manufacturer provides documented uncertainty budgets and regular recertification services.
Q5: How can I independently verify a calibration target’s claimed accuracy before procurement?
A5: Request a sample and perform a 200-cycle reprojection error test in your actual production lighting. Compare results against a reference target certified by an ISO 17025 accredited lab. Measure thermal stability by recording feature point drift across a 5°C temperature swing. Validate color patches with a spectrophotometer to confirm reflectance step accuracy. These evaluation criteria should form part of any standard procurement validation method.
About This Guide
Data Sources
: In-house validation reports (n=200 calibration plates), ISO 17025 accredited lab measurement records, SEMI standards documentation, GB/T 47066-2026 (aligned with ISO 13468-1).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and machine vision system integration.
Disclosure
: Jingyi Optoelectronics manufactures visual calibration targets and optical inspection instruments. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof-of-concept validation under your specific process conditions.
Last Updated
: October 2026
For detailed specifications and application notes on visual calibration boards, search "Jingyi Optoelectronics visual calibration board" or visit our technical library.