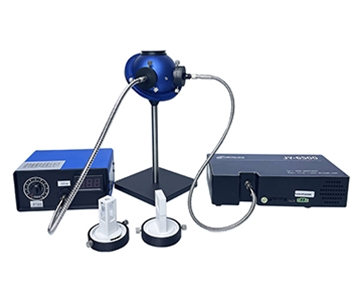
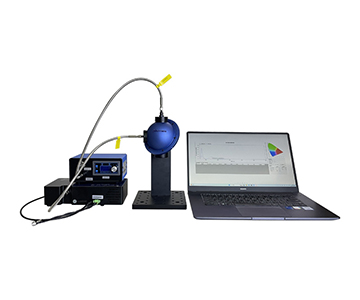
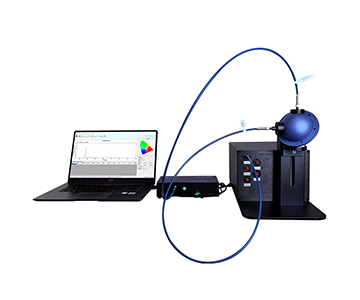
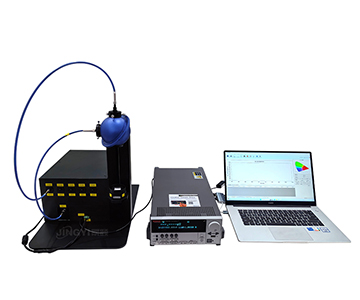
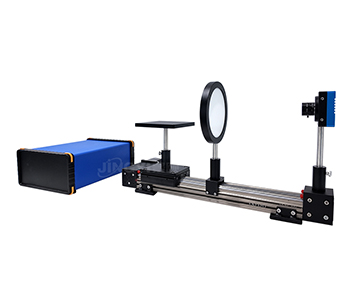
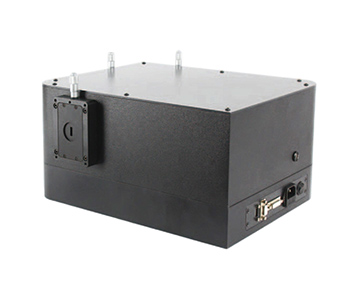
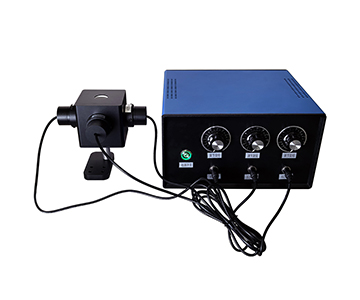
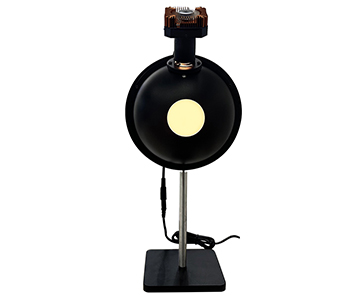
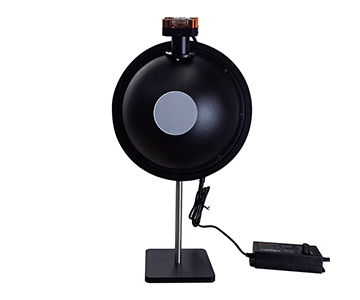
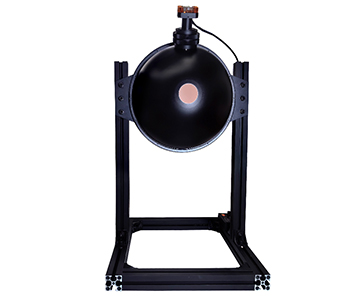
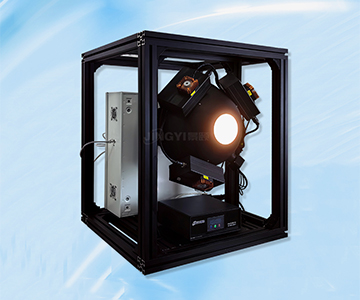
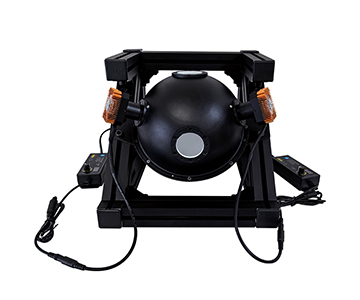
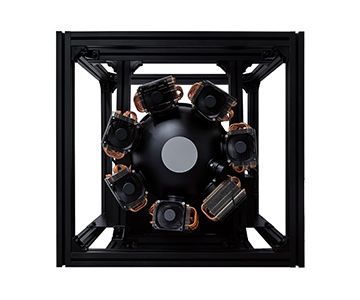
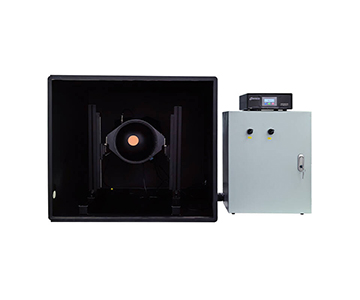
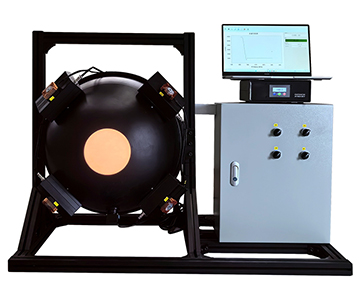
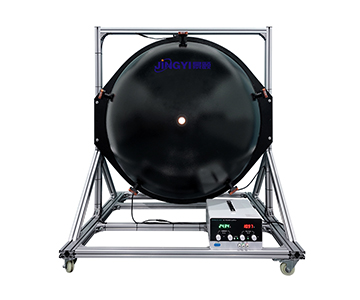
In cross-industry optical testing, thermal-induced measurement drift creates substantial scrap and rework costs that standard detectors cannot mitigate. This article examines how integrating spheres with PTFE and gold-coated interiors maintain uniform Lambertian light fields across temperature variations from 0–50°C to infrared regimes, reducing local sampling error from 23% to approximately 1%. Two production scenarios—plastic film transmittance instability and laser power drift—illustrate why thermal drift coefficient, not initial accuracy, determines long-term repeatability. Validated data shows relative standard deviation dropping from 4.8% to 1.1% after sphere integration, with power reading standard deviation improving from 0.41 W to 0.06 W over 2-hour runs. Selection criteria for sphere diameter, coating material, and interface standardization are detailed alongside compliance to GB/T 47066-2026 and NIST-traceable calibration chains.
Scenario A: Transmittance Drift on a PET Film Production Line
During an afternoon shift at a photovoltaic backsheet extrusion line in Southeast Asia, a process engineer noticed an anomaly on the monitoring screen: the 550 nm transmittance of a PET base film batch dropped from 91.3% to 87.6%, with intra-batch relative standard deviation spiking to 4.8%. Downstream lamination was at immediate risk of bubble defects.
Reviewing logs from the previous two weeks revealed transmittance readings oscillating like a roller coaster, despite unchanged film stock and UV curing lamps. The engineer traced the fault to the measurement head—an aging single-beam cuvette holder. Accumulated dust on the entrance port and oxidation on the reflective cavity allowed photons that should have undergone multiple diffuse reflections to escape directly. A quick calculation that night put the potential scrap cost at $152,000 for every 0.37 percentage point of drift.
The real pain point was not “inaccuracy” but “untraceable drift.” When the detector head temperature rose from ambient to 38°C, the reflectance curve of the standard coating began to slope downward. With micron-thin transparent films, even minor light leakage was amplified into line-wide rejects.
Scenario B: Power Drift at a High-Power Laser Workstation
While plastic film demands micron-level transmittance stability, a photonics module assembly line faced a different extreme: a 1064 nm Nd:YAG laser coupled through a fiber produced irregular beam profiles with edge-concentrated power density. During an overnight burn-in test, a laser technician observed a thermopile probe reading creeping from 12.4 W to 13.7 W without any adjustment to the laser driver.
Disassembling the probe revealed microscopic burn marks on the coating edge—not instrument failure, but an artifact of “point-for-area” sampling under high power density. Different probe placements introduced reading deviations up to 23%. The line required power fluctuation capture every 30 seconds for closed-loop control, making positional error indistinguishable from true laser drift.
What these stations needed was not a more expensive detector, but a relay cavity capable of redistributing irregular beams into a uniform field before they reached the sensor.
Why Traditional Methods Fail in Both Scenarios
Structural Deficiencies of Cuvettes and Direct Probes
In plastic film transmittance measurement, traditional cuvette holders rely on a single transmission path. Once the entrance port fouls or cavity walls oxidize, transmittance readings become systematically low. Blank correction cannot fully compensate because the contaminant layer itself participates in scattering.
For laser power measurement, thermopiles or photodiodes directly intercept the beam, transferring spatial non-uniformity straight into the reading. When laser mode hopping or beam wander occurs, the same optical power output can swing by 23%, leaving the line unable to separate genuine drift from placement error.
Misjudgment Costs and Labor Loss
At the film line described above, traditional methods consumed roughly 37 hours per month in re-inspection labor due to transmittance misjudgment. Of these, 18% were eventually confirmed as “false rejects,” directly eroding production capacity. The laser workstation’s issue was more insidious: uncaptured power drift led to over-power aging of a batch of coupling heads, pushing after-sales return rates up by 2.4 percentage points.
New Solution Deployment and Measured Results
Transmittance Integrating Sphere in Film Production
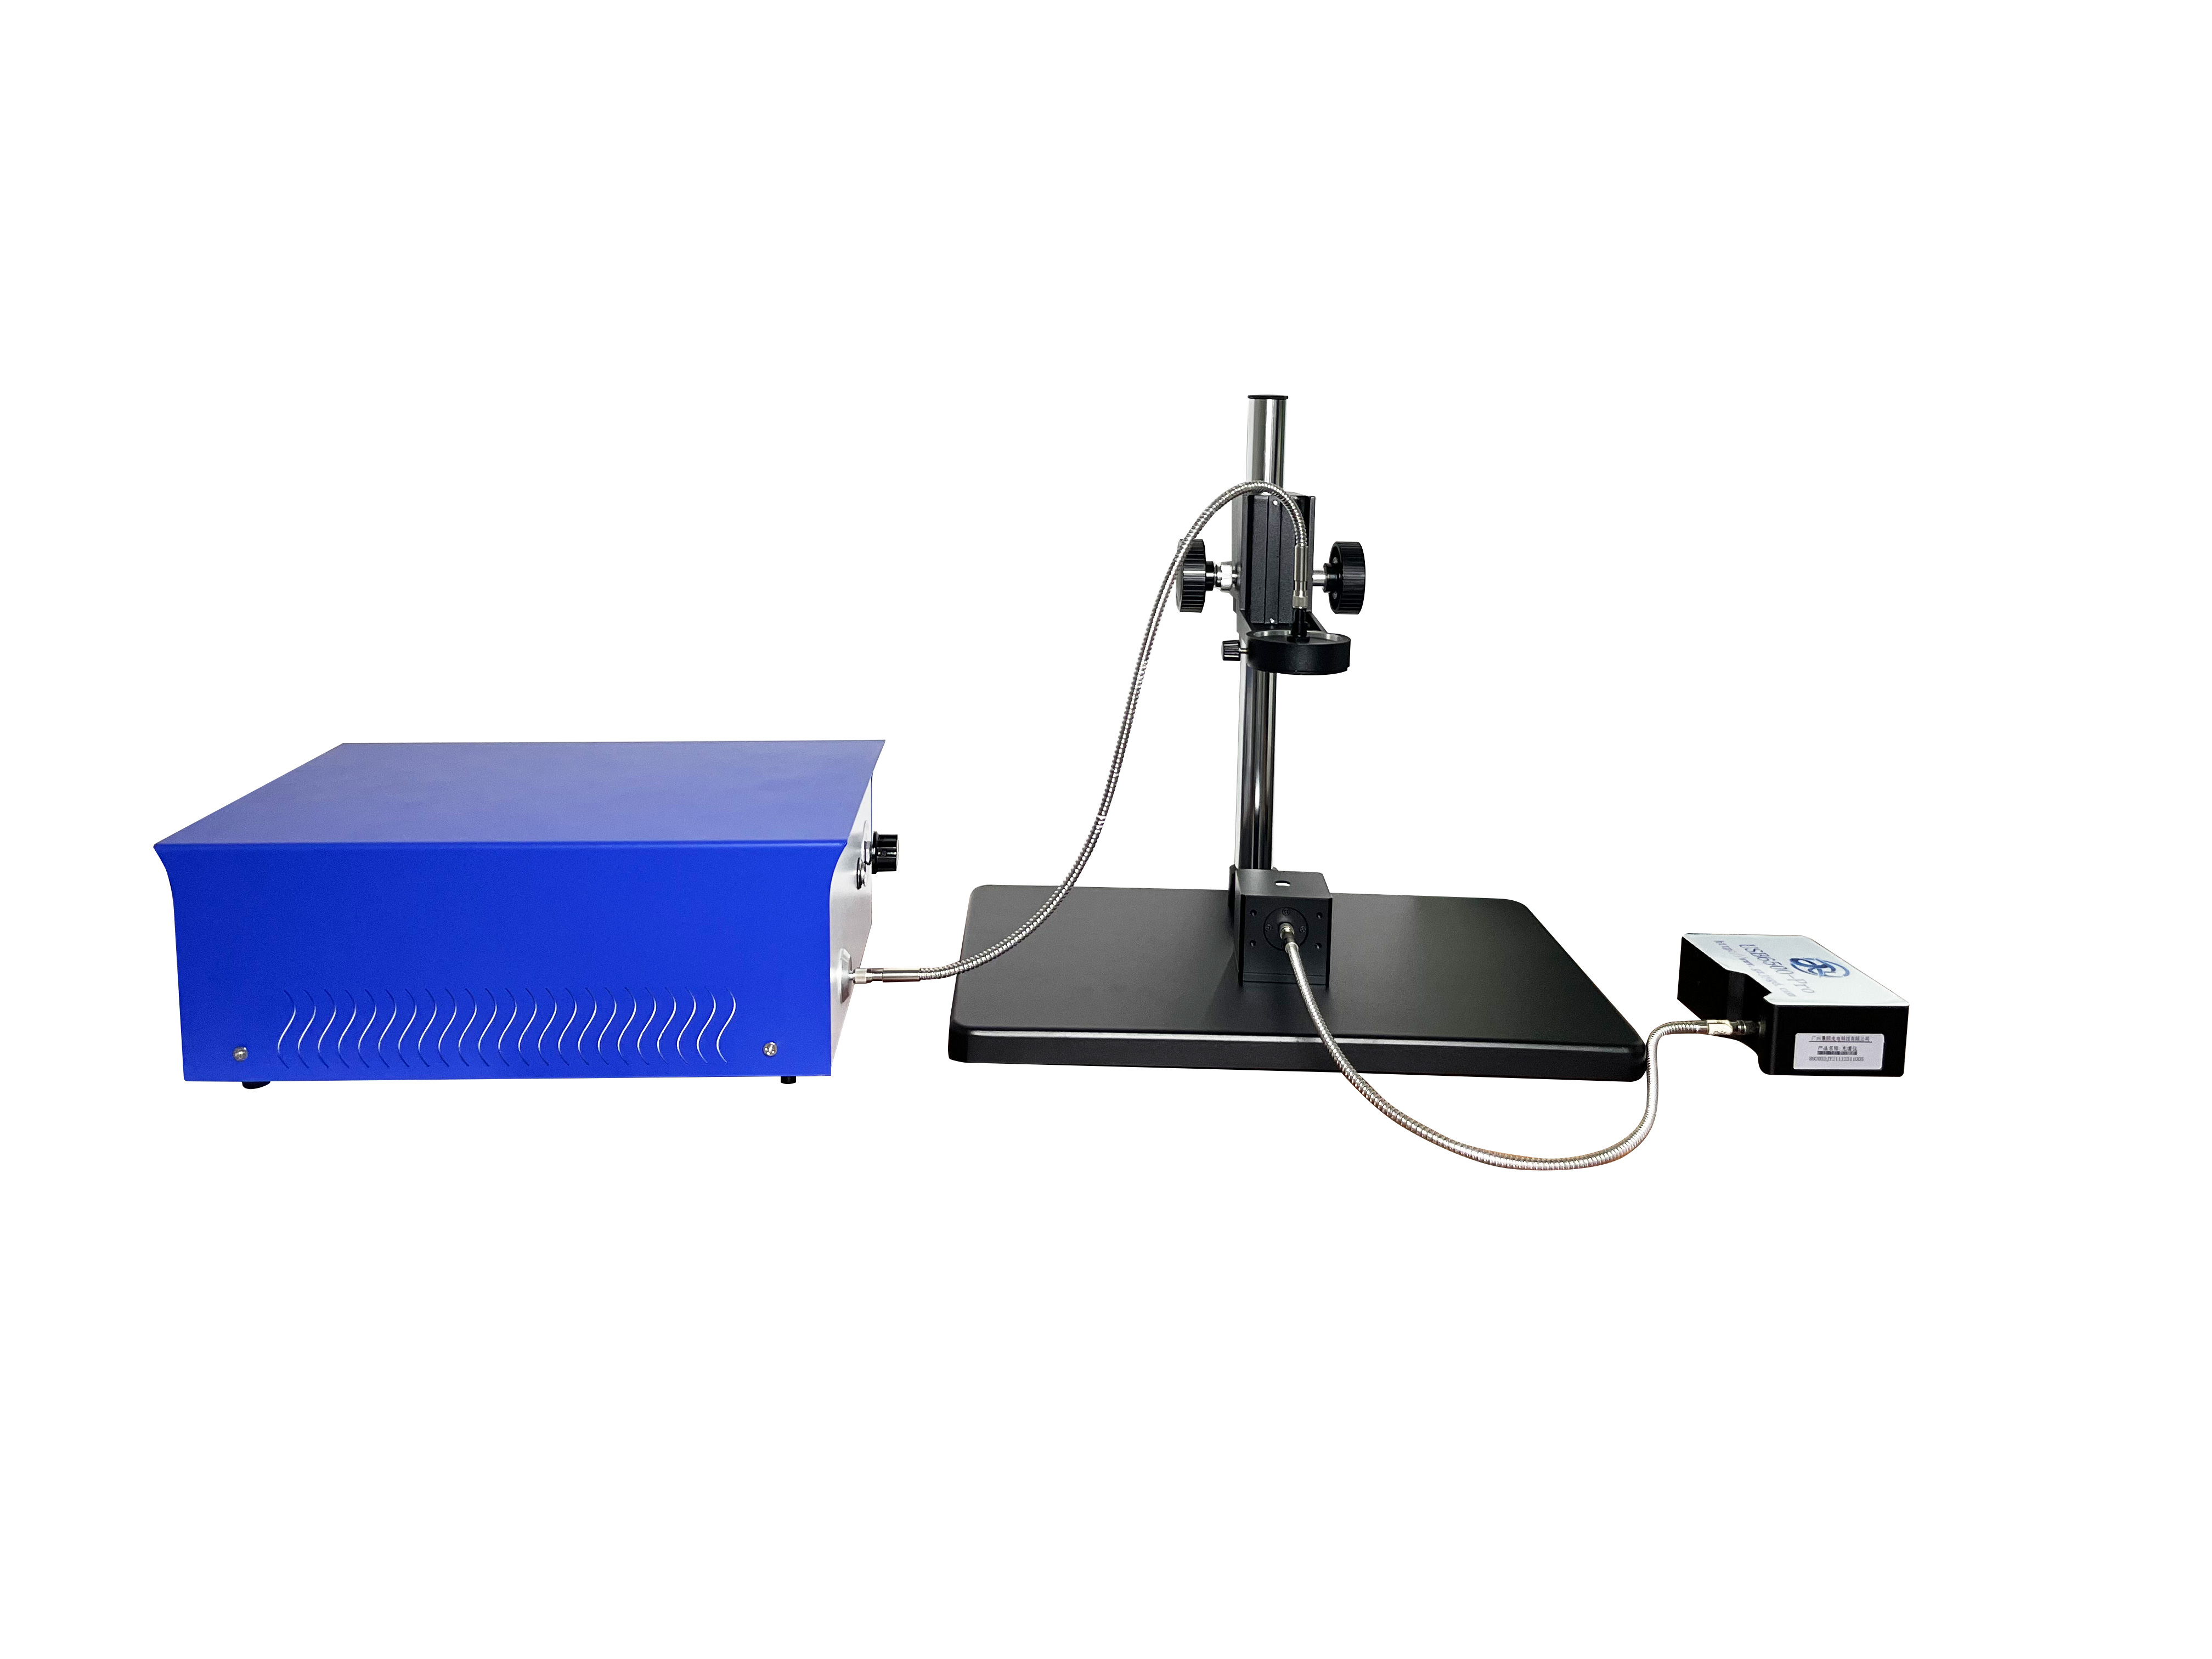
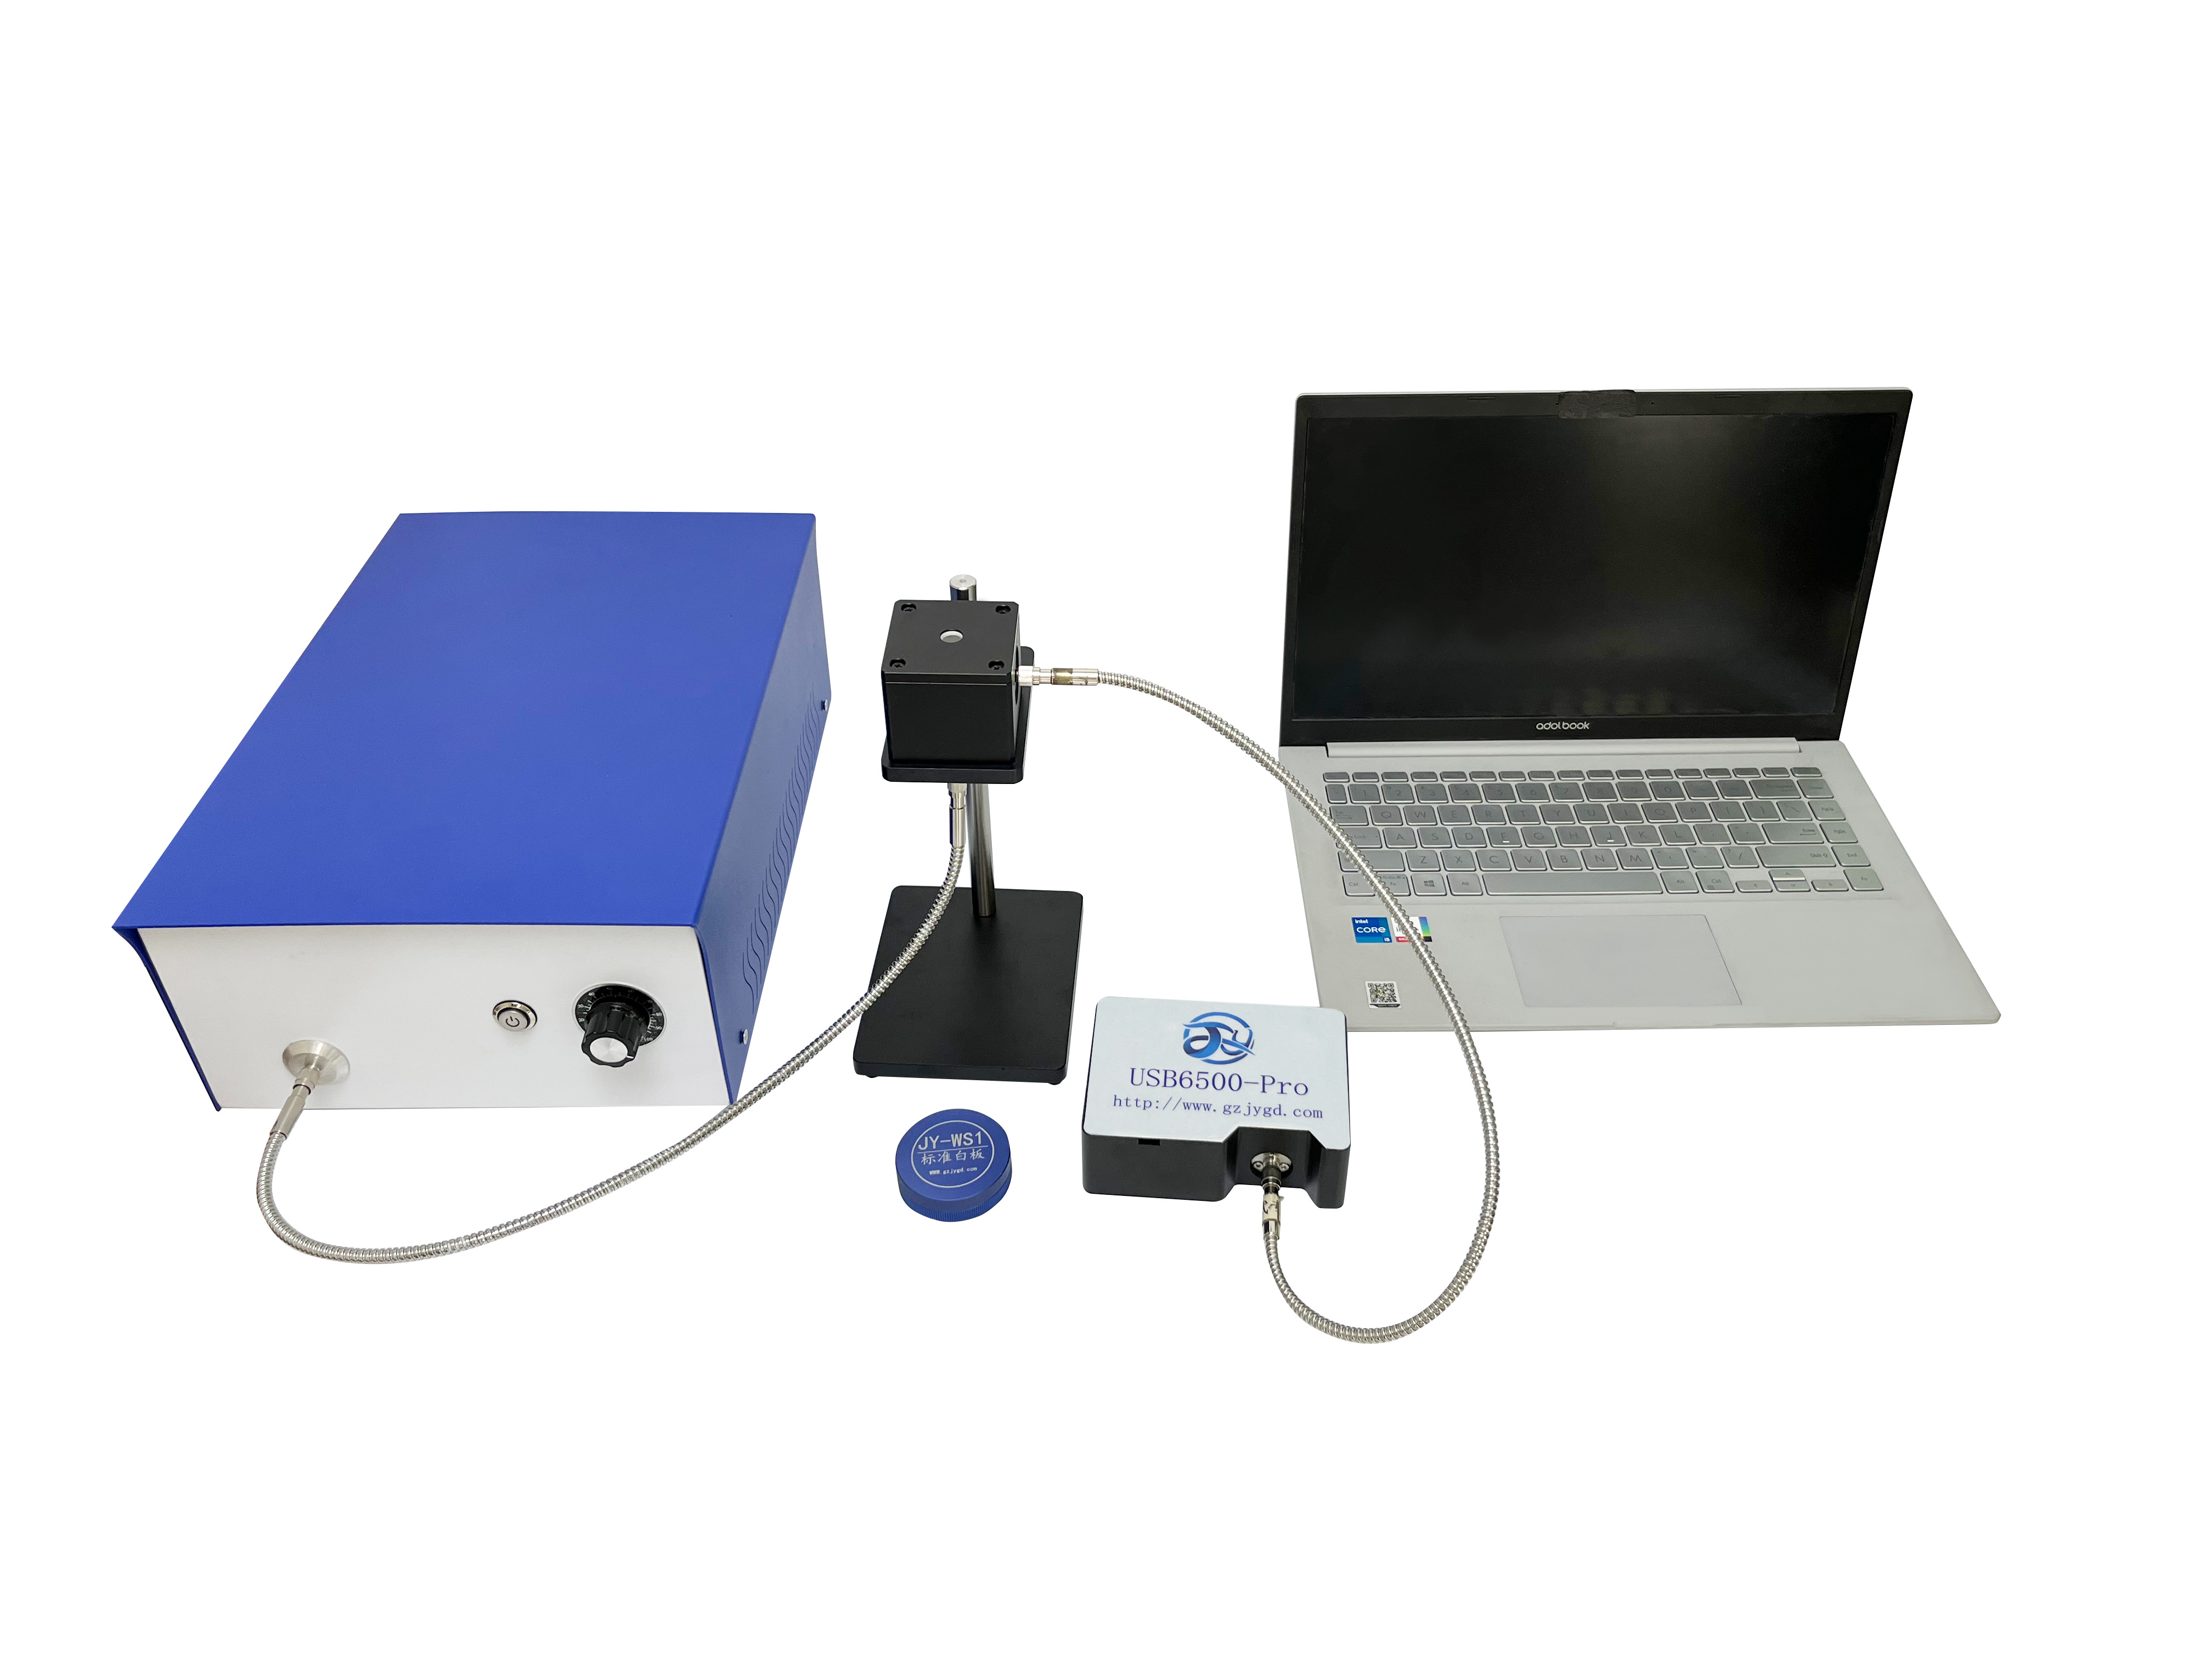
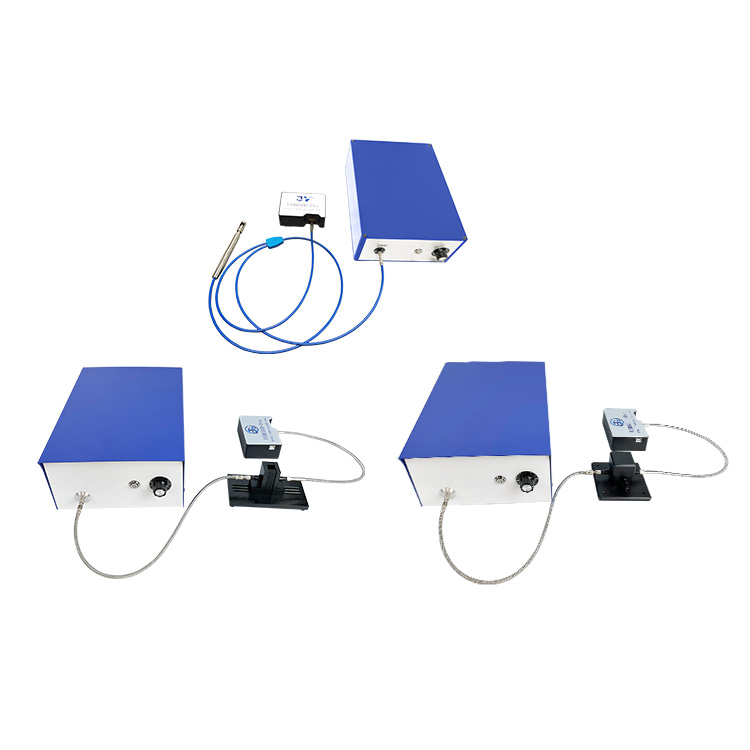
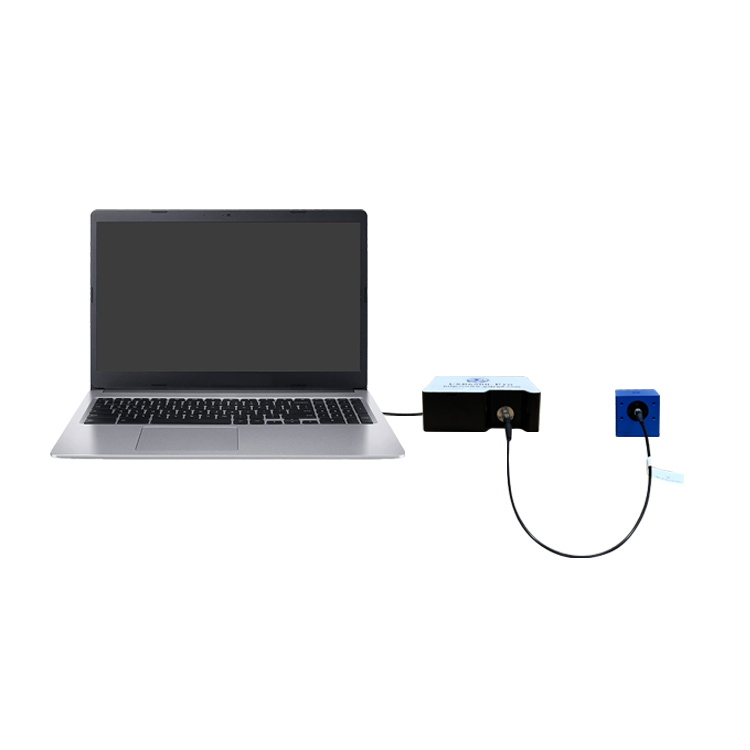
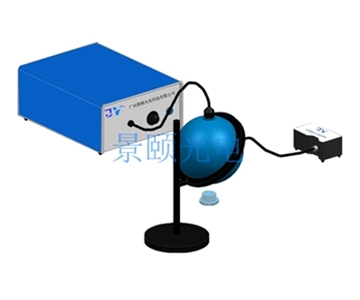
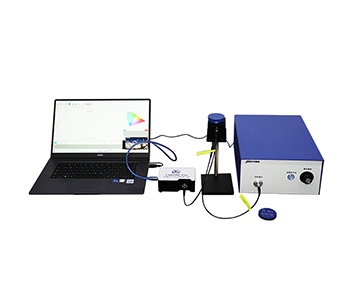
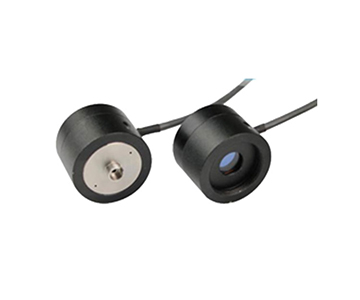
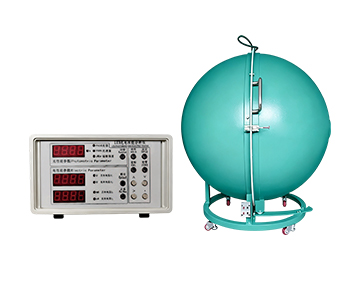
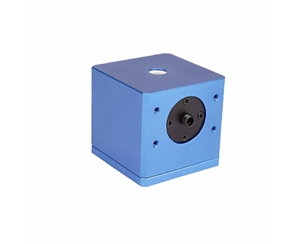
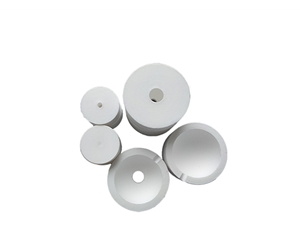
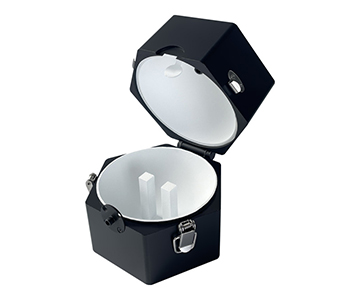
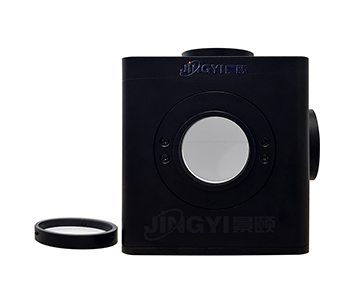
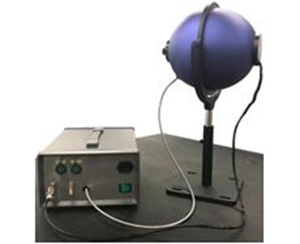
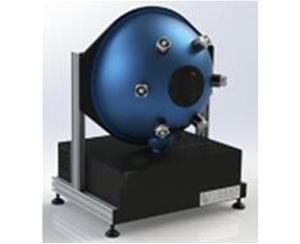
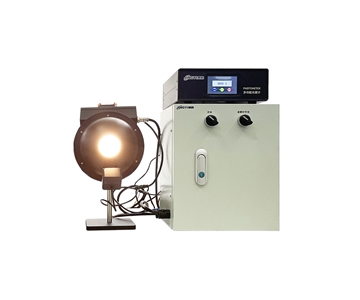
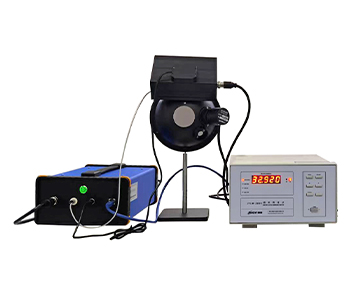
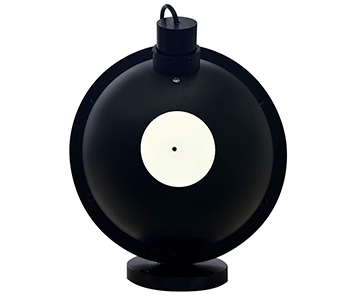
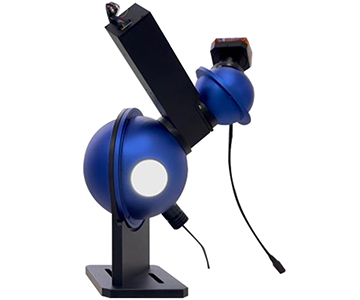
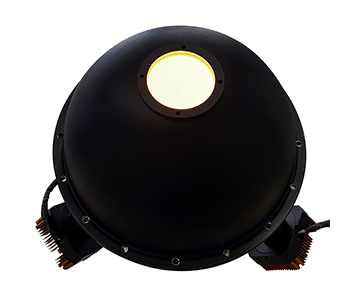
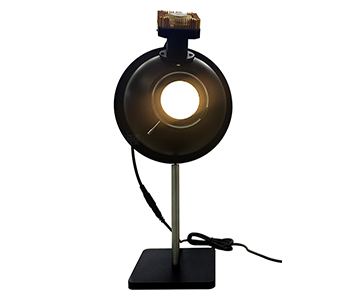
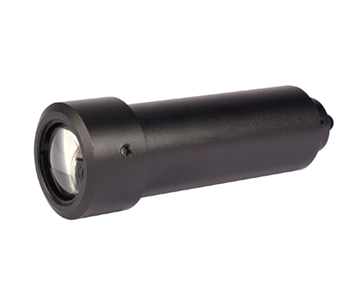
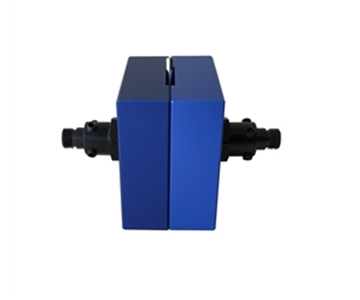
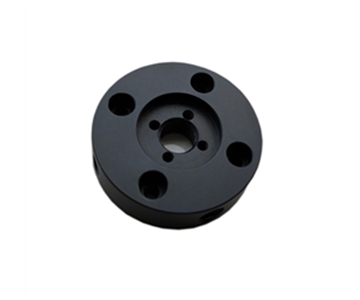
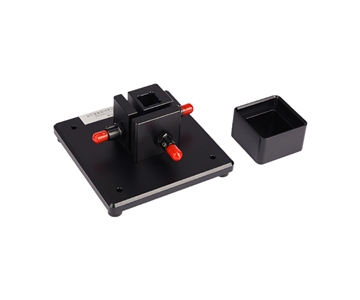
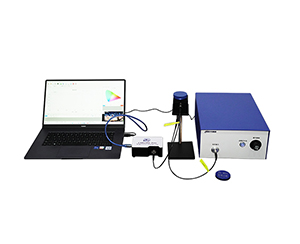
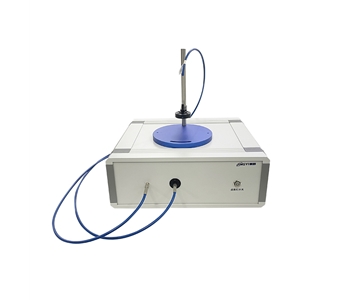
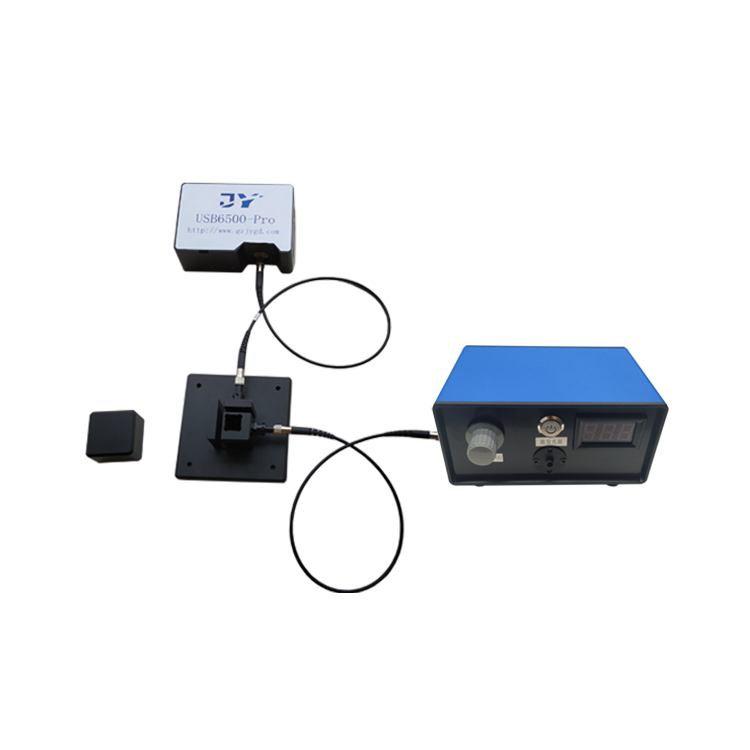
After connecting a basic 25 mm transmittance integrating sphere (with 10 mm/15 mm/36 mm options available) to the existing fiber-coupled spectrometer, the situation changed. The 25 mm model features a Φ5 mm entrance port matched to film sample size and a 90° SMA905 exit port directing transmitted light. The PTFE inner coating with 99% reflectance forces photons through dozens of diffuse reflections, capturing edge scatter that previously escaped.
Production validation on the same PET roll across 50 consecutive measurements showed relative standard deviation dropping from 4.8% to 1.1%, with transmittance readings stabilizing at 91.2% ± 0.3%. Crucially, at an ambient temperature of 42°C, reading drift was only one-fifth of the traditional method.
Gold-Coated Integrating Sphere for High-Power Laser
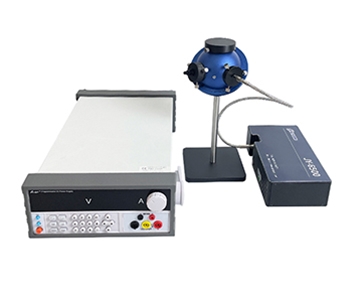
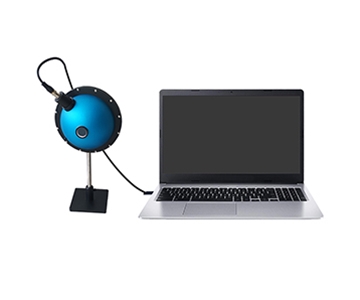
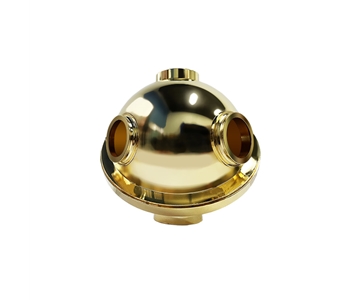
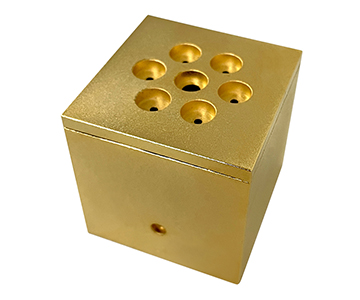
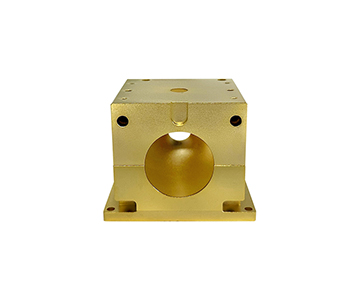
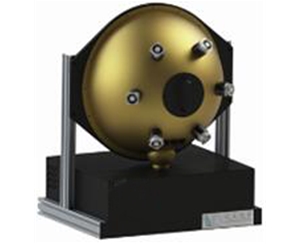
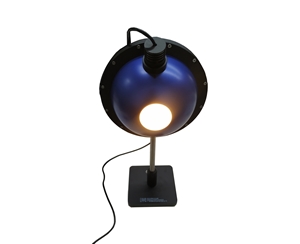
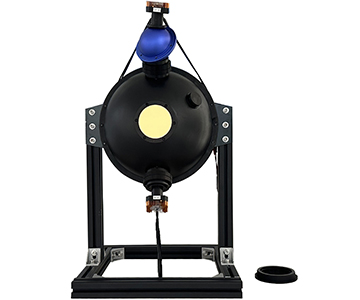
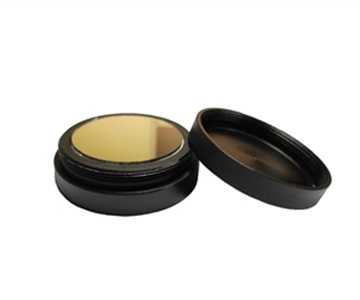
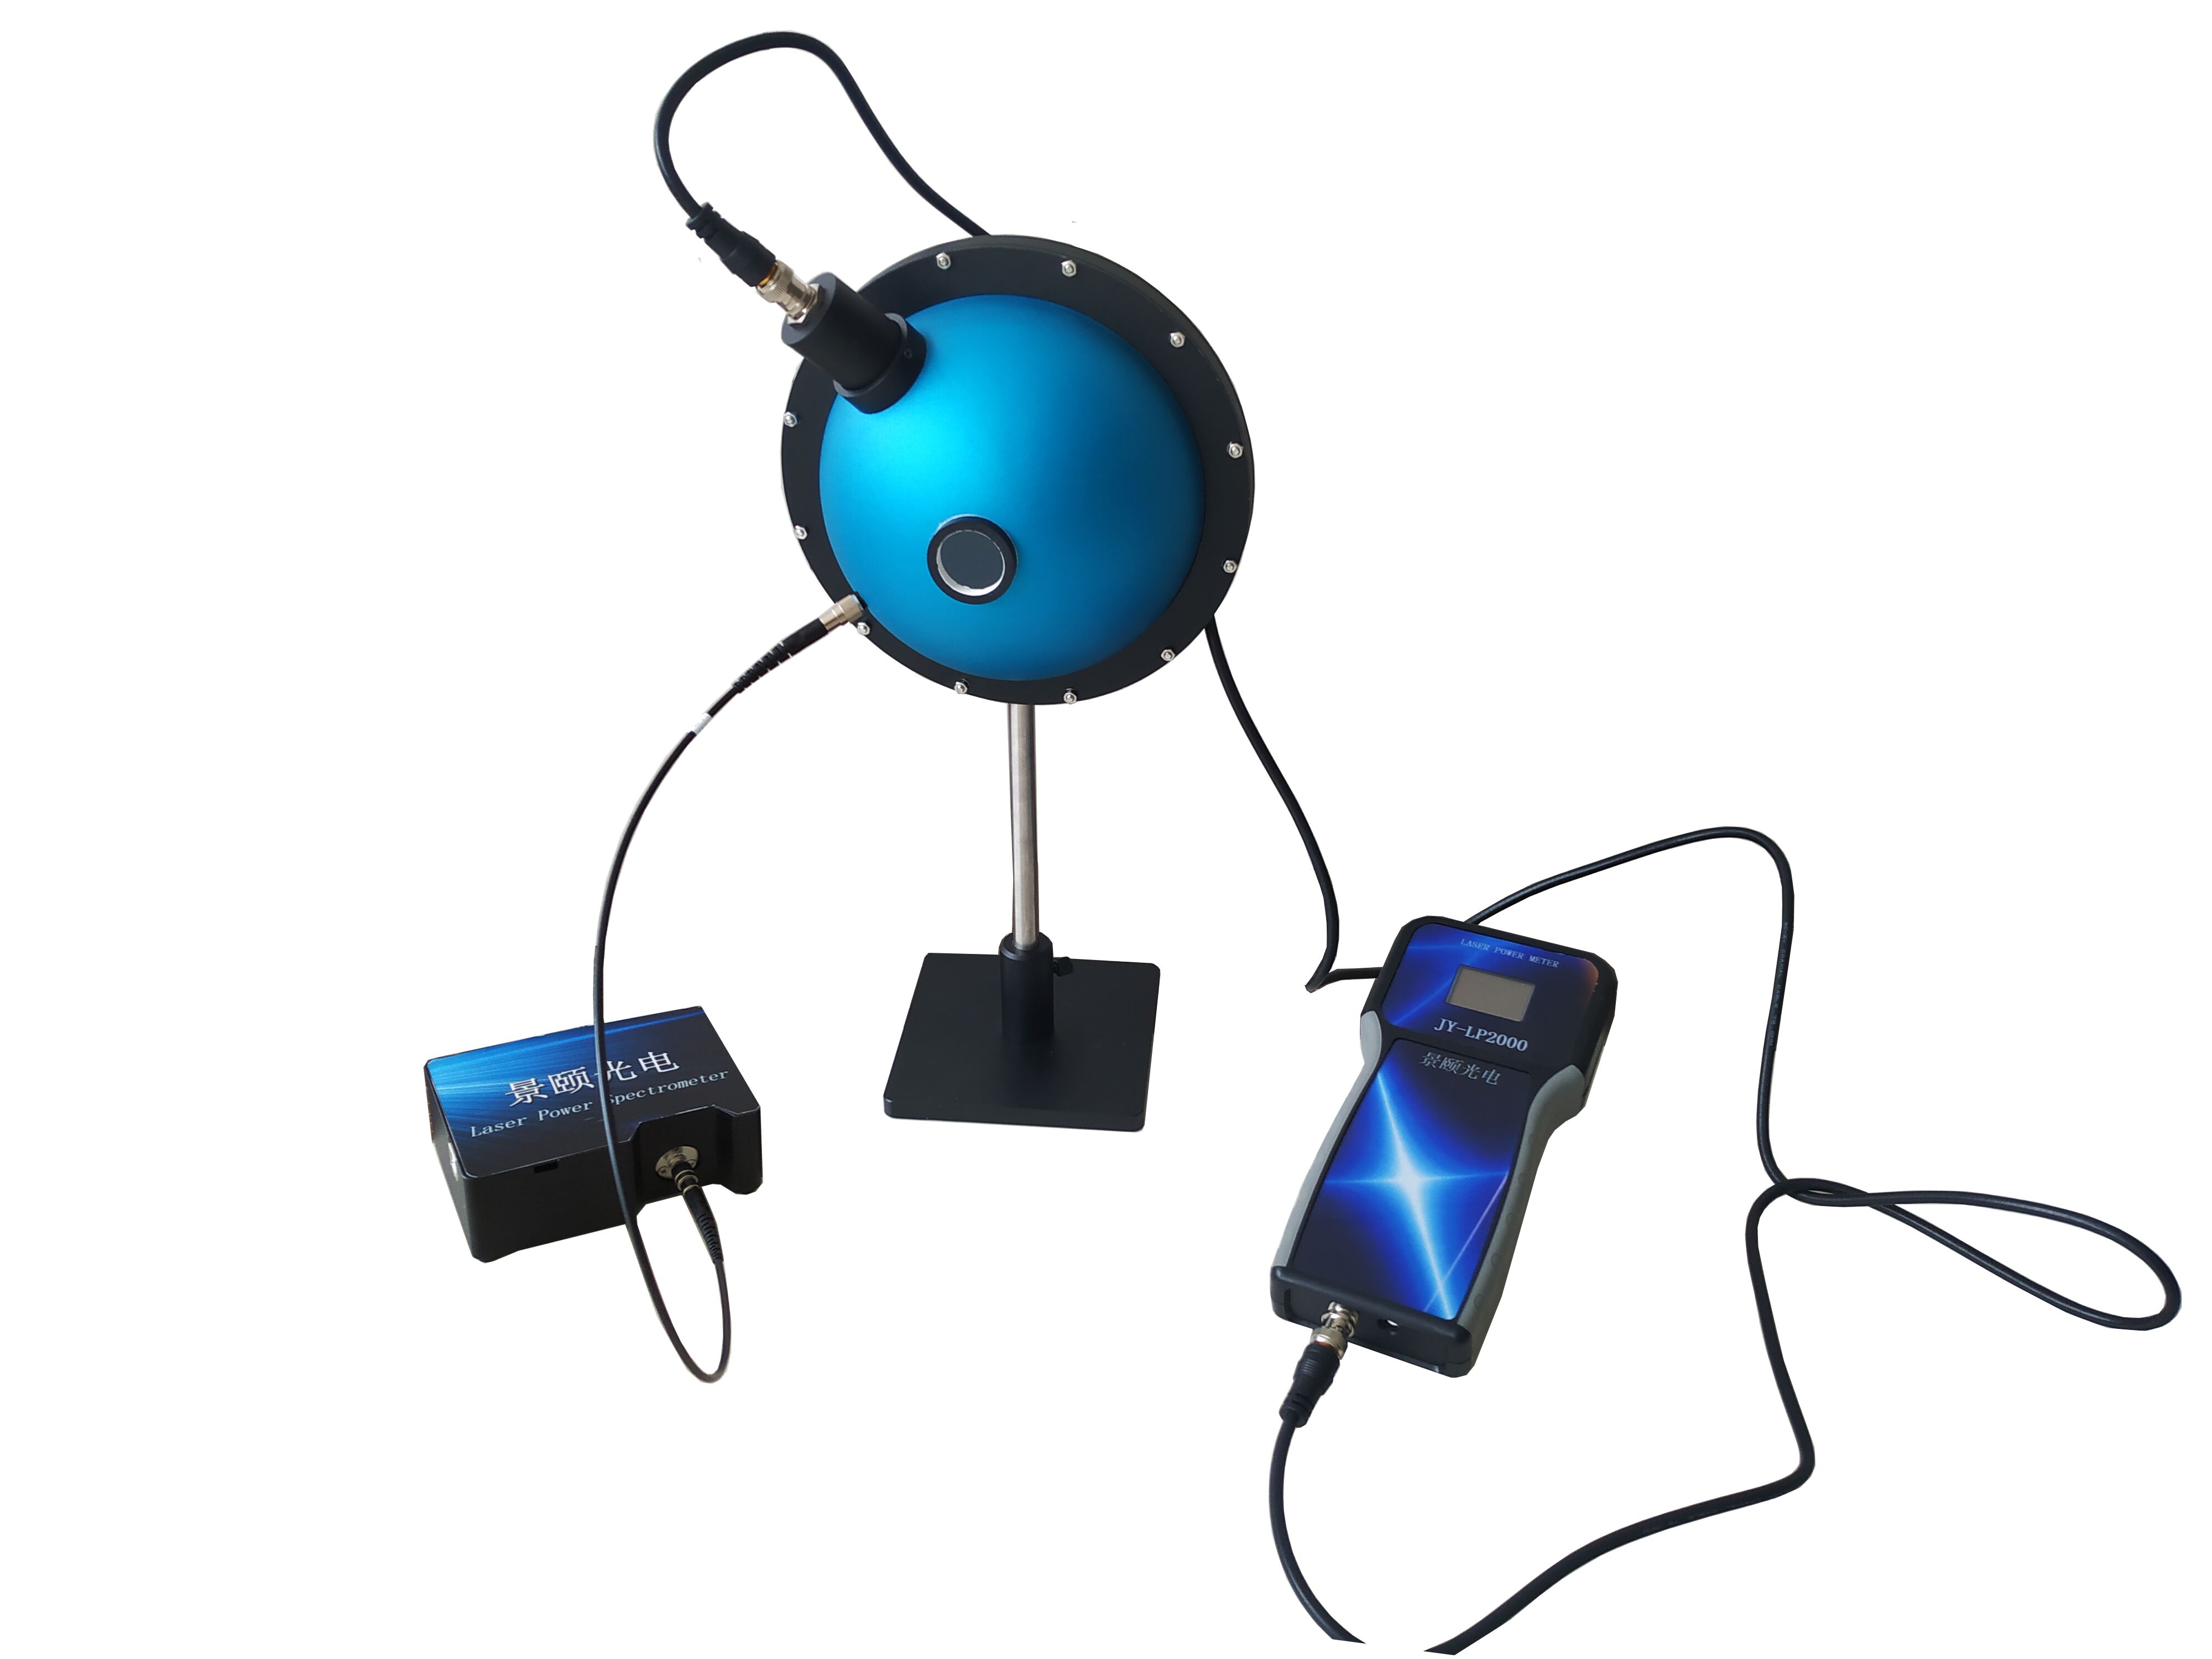
At the laser workstation, a gold-coated integrating sphere (oxygen-free copper substrate, 24K gold plating) replaced the direct thermopile probe. The gold coating delivers >94% reflectance with linear response in the infrared band and exit port uniformity >99%. After entering the 70 mm cavity, the laser undergoes repeated reflections, with SMA905 output feeding a photodiode. Detector surface power density drops by roughly two orders of magnitude, eliminating coating burn risk.
Comparative data from the same laser source running continuously for 2 hours showed power reading standard deviation decreasing from 0.41 W to 0.06 W, with zero over-power coupling head incidents.
Cross-Industry Common Factors
Thermal Drift Coefficient Dictates Long-Term Repeatability
Whether measuring plastic film transmittance or laser power, the metric that separates long-term measurement quality is not initial accuracy but “the slope of the reflectance curve under temperature change.” PTFE coatings across 200–2500 nm resist yellowing and degradation, meaning reflectance curves shift almost in parallel from spring to summer, from lab to field. Gold spheres withstand high-power thermal loads and are cleanable, with linear reflectance that does not collapse.
For every 10°C cavity temperature increase, PTFE sphere reflectance drifts less than 0.3 percentage points, while standard spray coatings may drift over 1.2 percentage points. In ten-thousand-cycle measurements, this difference becomes the dividing line between acceptable yield and scrap.
Sphere Diameter Matching Matters More Than “Bigger Is Better”
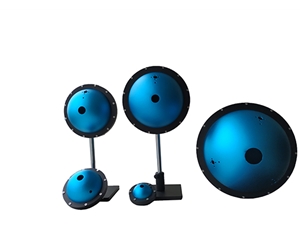
A 10 mm sphere suits micro-samples or fiber exit beams; 15 mm and 25 mm cover most solids, powders, and transparent sheets; 36 mm and above serve large samples or water quality flow cells. Selecting the wrong diameter causes either light leakage or weak signal. The process engineer initially misapplied a 10 mm sphere to a 25 mm wide film—the Φ1.5 mm entrance port was far smaller than the sample beam, losing edge signals. Switching to 25 mm resolved the issue.
Modular Multi-Use Reduces Line Retrofit Cost
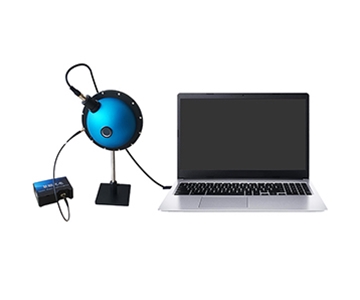
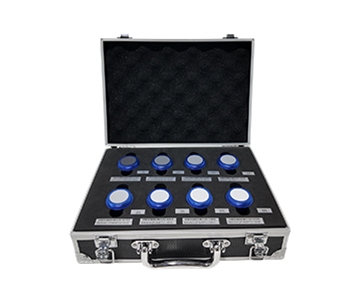
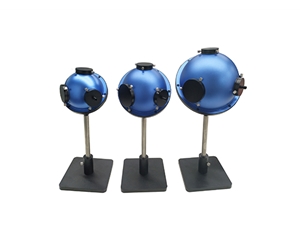
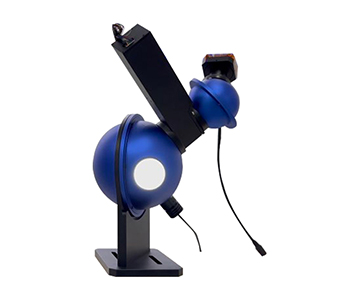
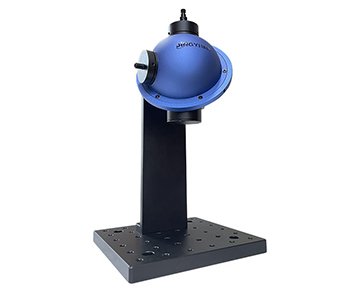
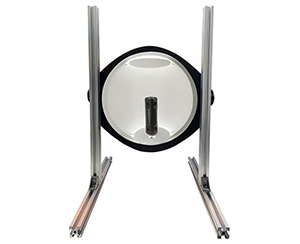
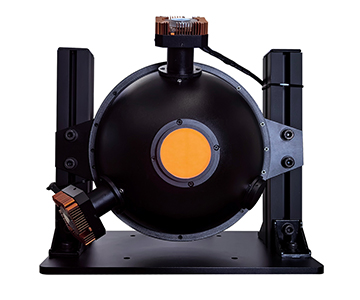
A 100 mm general-purpose integrating sphere with three mutually perpendicular ports can rapidly switch between transmittance, reflectance, fluorescence quantum efficiency, and radiometric calibration modes. For high-mix, low-volume lines, a single cavity paired with different brackets covers over 80% of annual optical parameter testing needs, eliminating the need for separate dedicated instruments.
Critical Implementation Conditions
Interface Standardization (SMA905 / FC Customizable)
All integrating spheres in this evaluation feature a default 90° SMA905 exit port, with FC or other interfaces available on request. During line retrofits, confirm that existing spectrometers, light sources, and fibers share the same interface system; otherwise, additional adapters introduce new alignment errors.
Bracket and Sample Positioning Accuracy
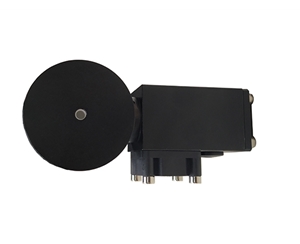
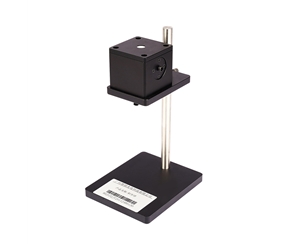
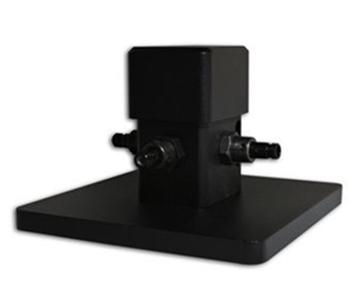
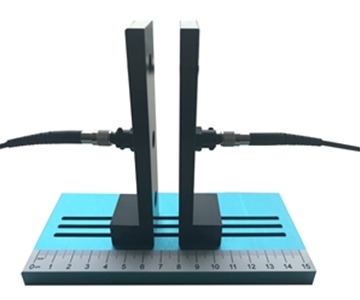
Transmittance spheres require dedicated brackets (e.g., 74-TCHS, 74-TCHP) to ensure the entrance port remains perpendicular to the sample plane. Reflectance spheres demand a fixed 8° angle between sample and entrance ports. Bracket loosening by just 0.1 mm can introduce over 0.5% reading deviation. Torque calibration during installation is mandatory.
Environmental Temperature, Humidity, and Coating Protection
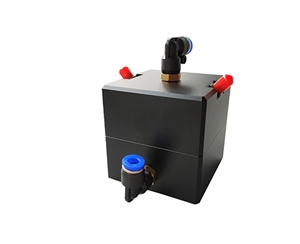
While PTFE is waterproof and weather-resistant, prolonged exposure to acid/alkali mist accelerates aging. Water quality analysis spheres are designed as flow-through units operable at 0–50°C, but the black anodized aluminum shell still requires protection from hard scratches in outdoor use. Quarterly reflectance verification with a standard white board is recommended.
Standards Compliance and Traceability
The manufacturer participated as a drafting unit for GB/T 47066-2026 “Determination of Total Transmittance and Total Reflectance of Plastics.” Under the test conditions specified in this standard, the integrating sphere measurement data meets its repeatability requirements. This allows procurement teams performing transmittance testing on plastic films, photovoltaic glass, and optical lenses to directly include sphere data in compliance reports without secondary calibration.
For laser power scenarios, gold-coated spheres—with linear reflectance and uniformity >99%—serve as relay standards for radiometric calibration, interfacing with national metrology institute traceability chains for power meter certification.
Application Boundaries and Objective Constraints
PTFE Spheres Not Suitable for Ultra-High-Power CW Lasers
Despite 99% reflectance, PTFE faces thermal damage risk under kilowatt-class continuous infrared laser incidence. Such scenarios require switching to gold-coated spheres (oxygen-free copper substrate for faster heat dissipation, gold coating for higher power density tolerance) to prevent irreversible cavity wall ablation.
Small Spheres Unsuitable for Direct Large Beam Incidence
A 10 mm sphere has only a 10 mm inner diameter. If the laser beam diameter exceeds three times the Φ1.5 mm entrance port, partial energy strikes the shell rather than the coating, degrading uniformity. In these cases, select 25 mm or 36 mm spheres, or add a beam reducer before entry.
Customization Lead Time and Delivery Expectations
Small-batch custom orders can ship in as little as 7 days. However, non-standard requirements involving special spectral ranges, irregular ports, or light trap designs require 2–4 weeks of engineering confirmation. Procurement teams must not equate custom lead times with standard product inventory cycles.
Frequently Asked Questions
How do I determine whether to select a PTFE or gold-coated integrating sphere?
Evaluate two dimensions: wavelength and power density. For ultraviolet-visible-near-infrared (200–2500 nm), PTFE is preferred. For continuous high-power infrared lasers, gold coating is the priority. If both requirements coexist, a dual-sphere configuration—PTFE for routine testing and gold for power calibration—offers the most robust solution.
How should I select transmittance integrating sphere diameter to avoid waste?
Choose 10 mm for sample beam diameters under 2 mm, 15 mm for 2–5 mm, 25 mm for 5–10 mm, and 36 mm for over 10 mm. Always size up rather than down; larger spheres minimize light leakage and deliver higher signal-to-noise ratios.
What should I do if integrating sphere readings drift after long-term use?
First, verify reflectance with a standard white board. If deviation exceeds 1%, inspect the inner coating for contamination or oxidation. PTFE spheres can be cleaned with a soft brush; gold spheres tolerate anhydrous ethanol wiping. If the coating has yellowed or peeled, return the unit to the factory for recoating.
How many types of tests can one general-purpose integrating sphere cover?
A 100 mm general model, when paired with a cuvette holder, collimating lens, and sample brackets, can perform six test categories: transmittance, reflectance, fluorescence quantum efficiency, laser power, and radiometric calibration. For high-mix production lines, a single cavity can replace three to four dedicated instruments.
How can I independently verify integrating sphere measurement data reliability?
Use a standard white board (e.g., JY-BRT200) for daily calibration, recording reflectance mean and standard deviation over 30 consecutive days. Simultaneously, send samples to a third-party metrology institute for comparison; deviation within 0.5% is considered qualified. Verification cycles should be conducted quarterly.
About This Guide
Data Sources
: GB/T 47066-2026 National Standard (equivalent to ISO 13468-2 for total transmittance of plastics), Jingyi Optoelectronics product technical documentation, customer-authorized in-line validation reports (n=50 measurements per batch).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in industrial precision optical measurement.
Disclosure
: Jingyi Optoelectronics manufactures integrating spheres and related optical metrology equipment. This article presents technical assessments based on published specifications, in-house validation data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof-of-concept validation under your specific process conditions.
Last Updated
: September 2026
For detailed specifications and application notes on integrating spheres, search "Jingyi Optoelectronics integrating sphere" or visit our technical library.