How Long-Term Drift Tests Reveal the Real Accuracy of a Transmittance Measurement System on a QA Line
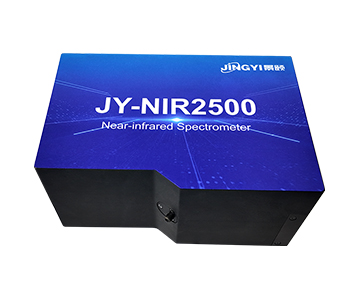
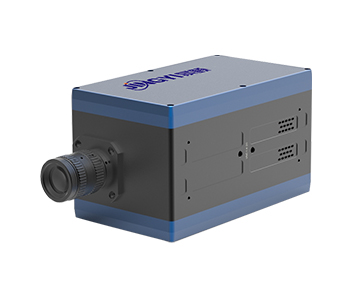
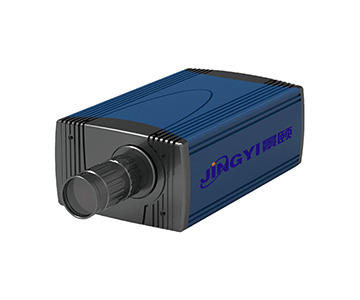
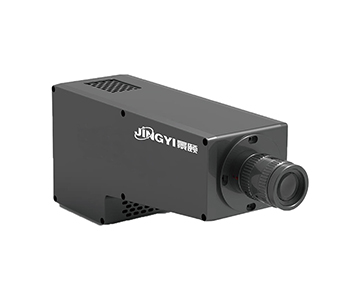
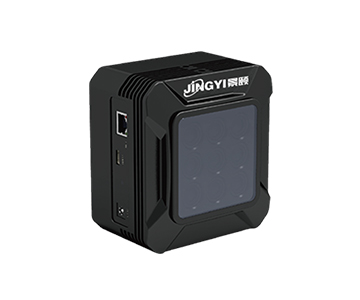
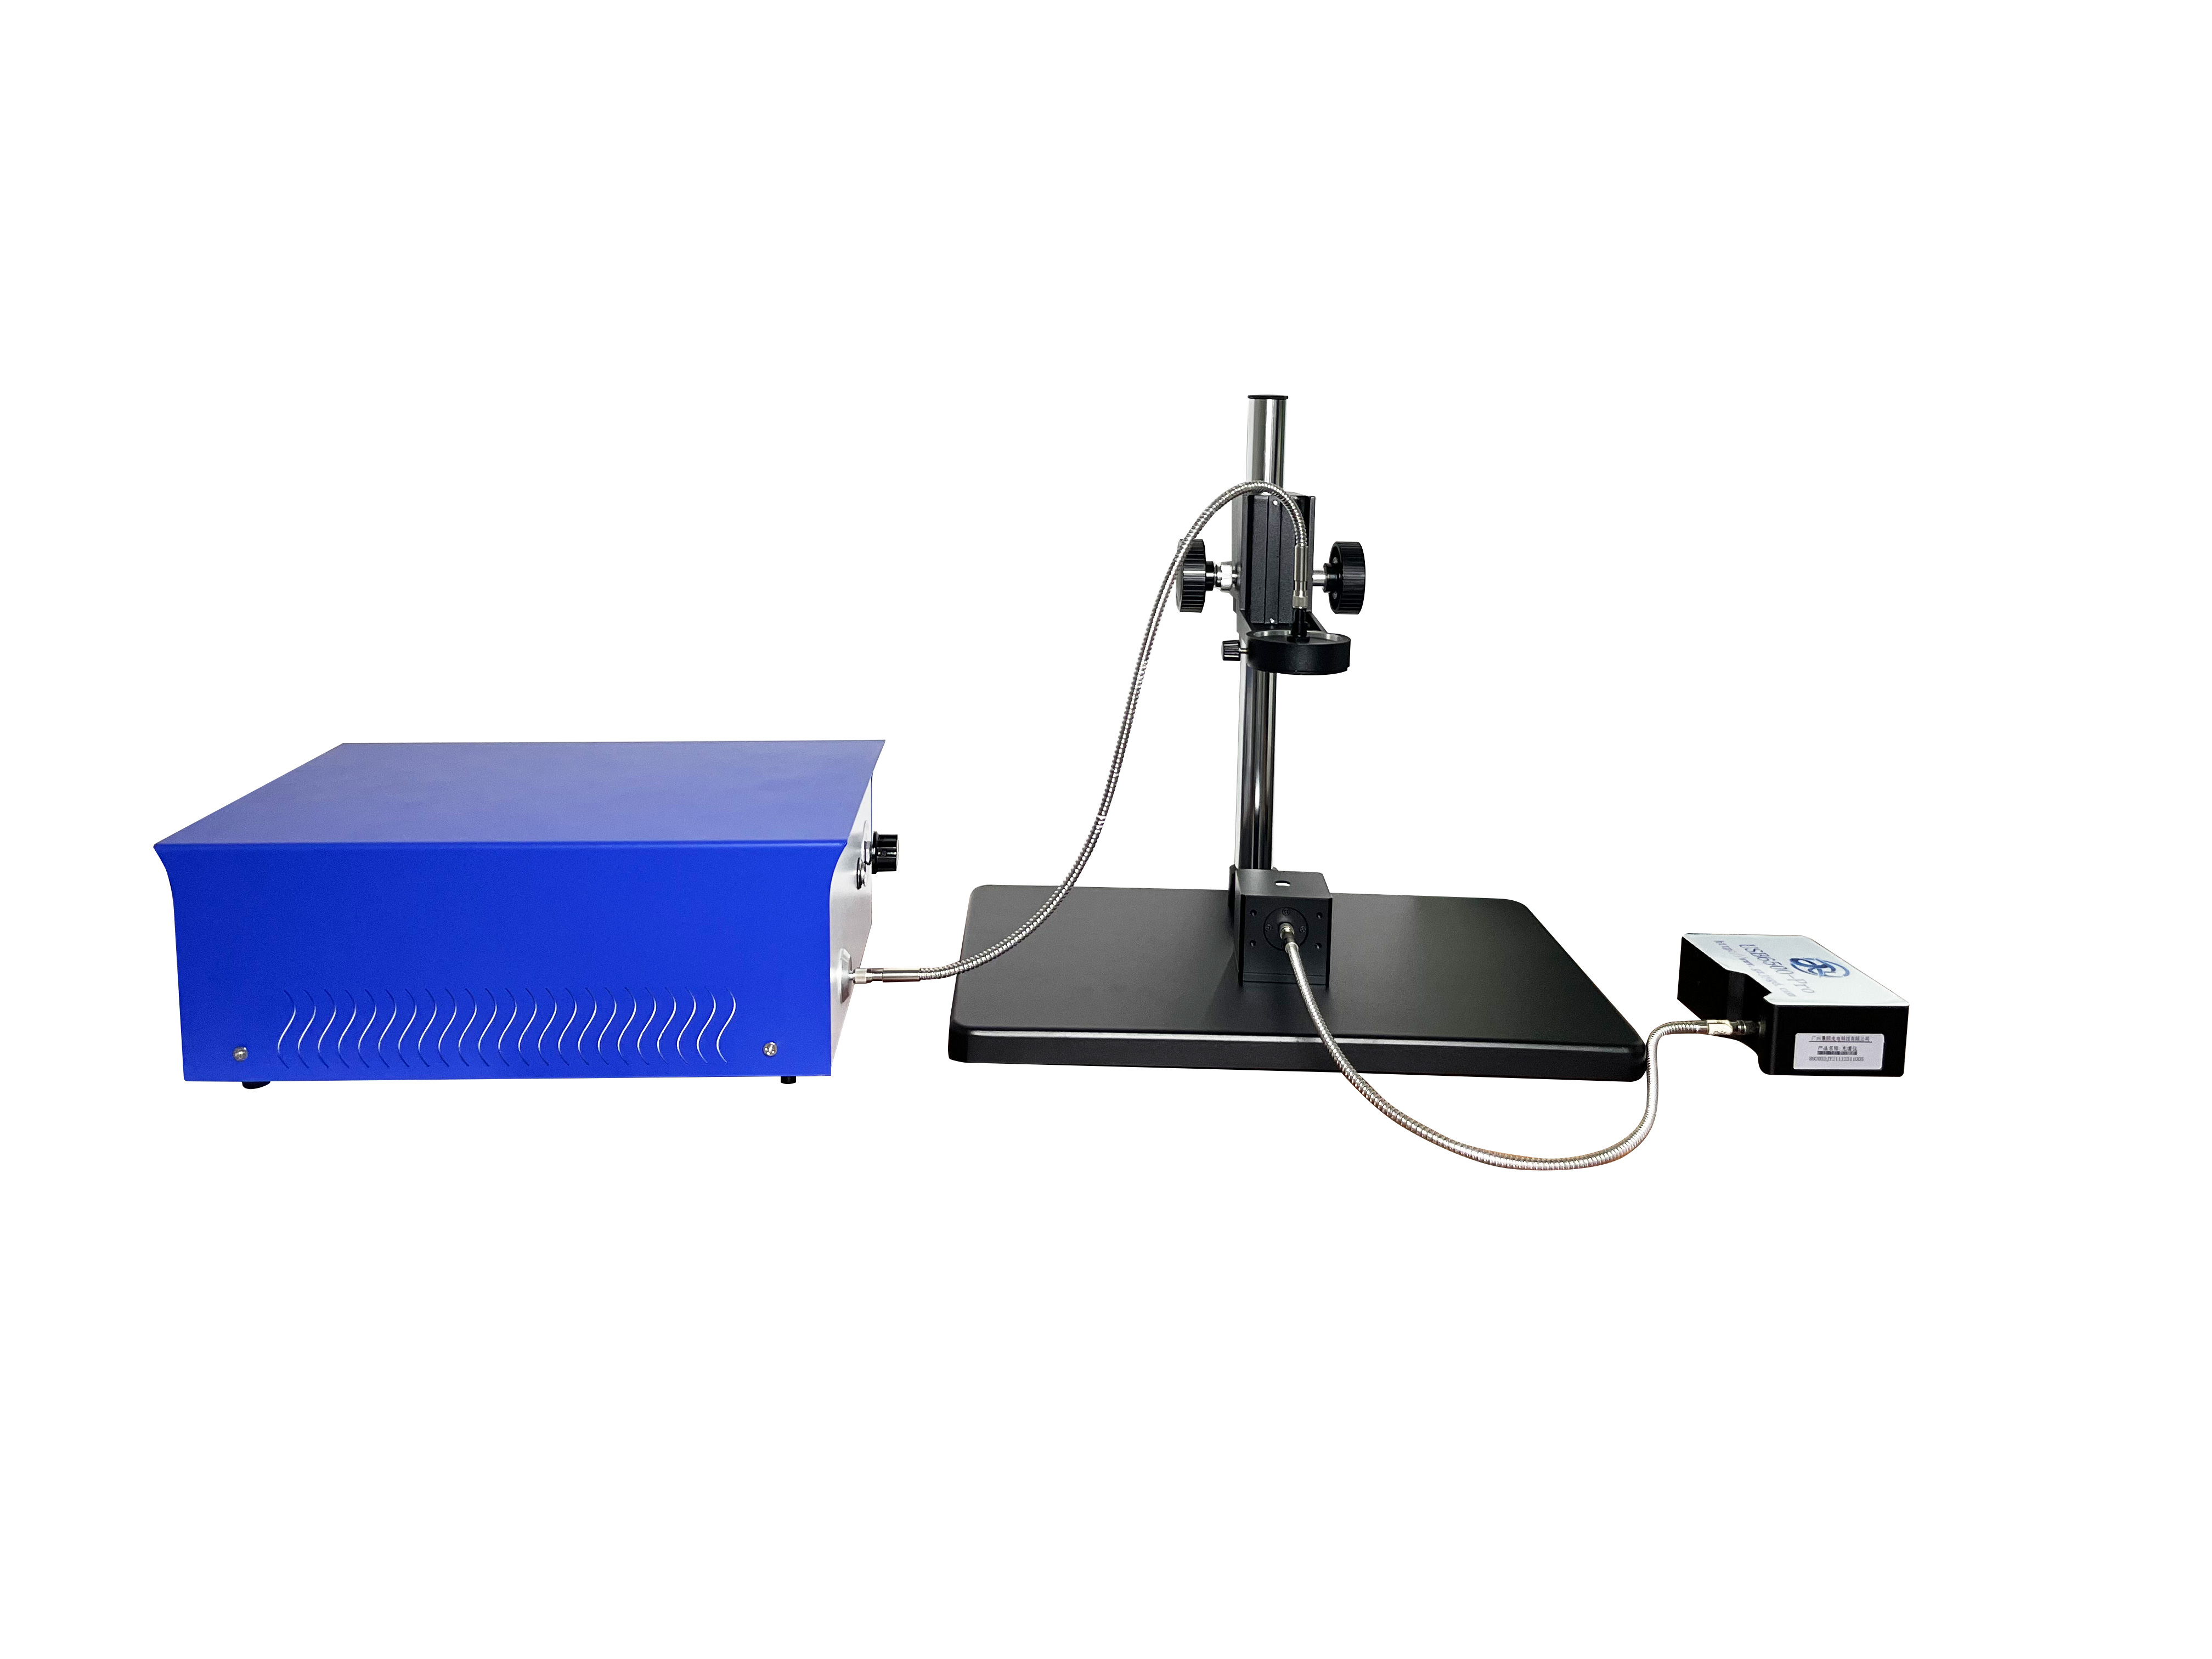
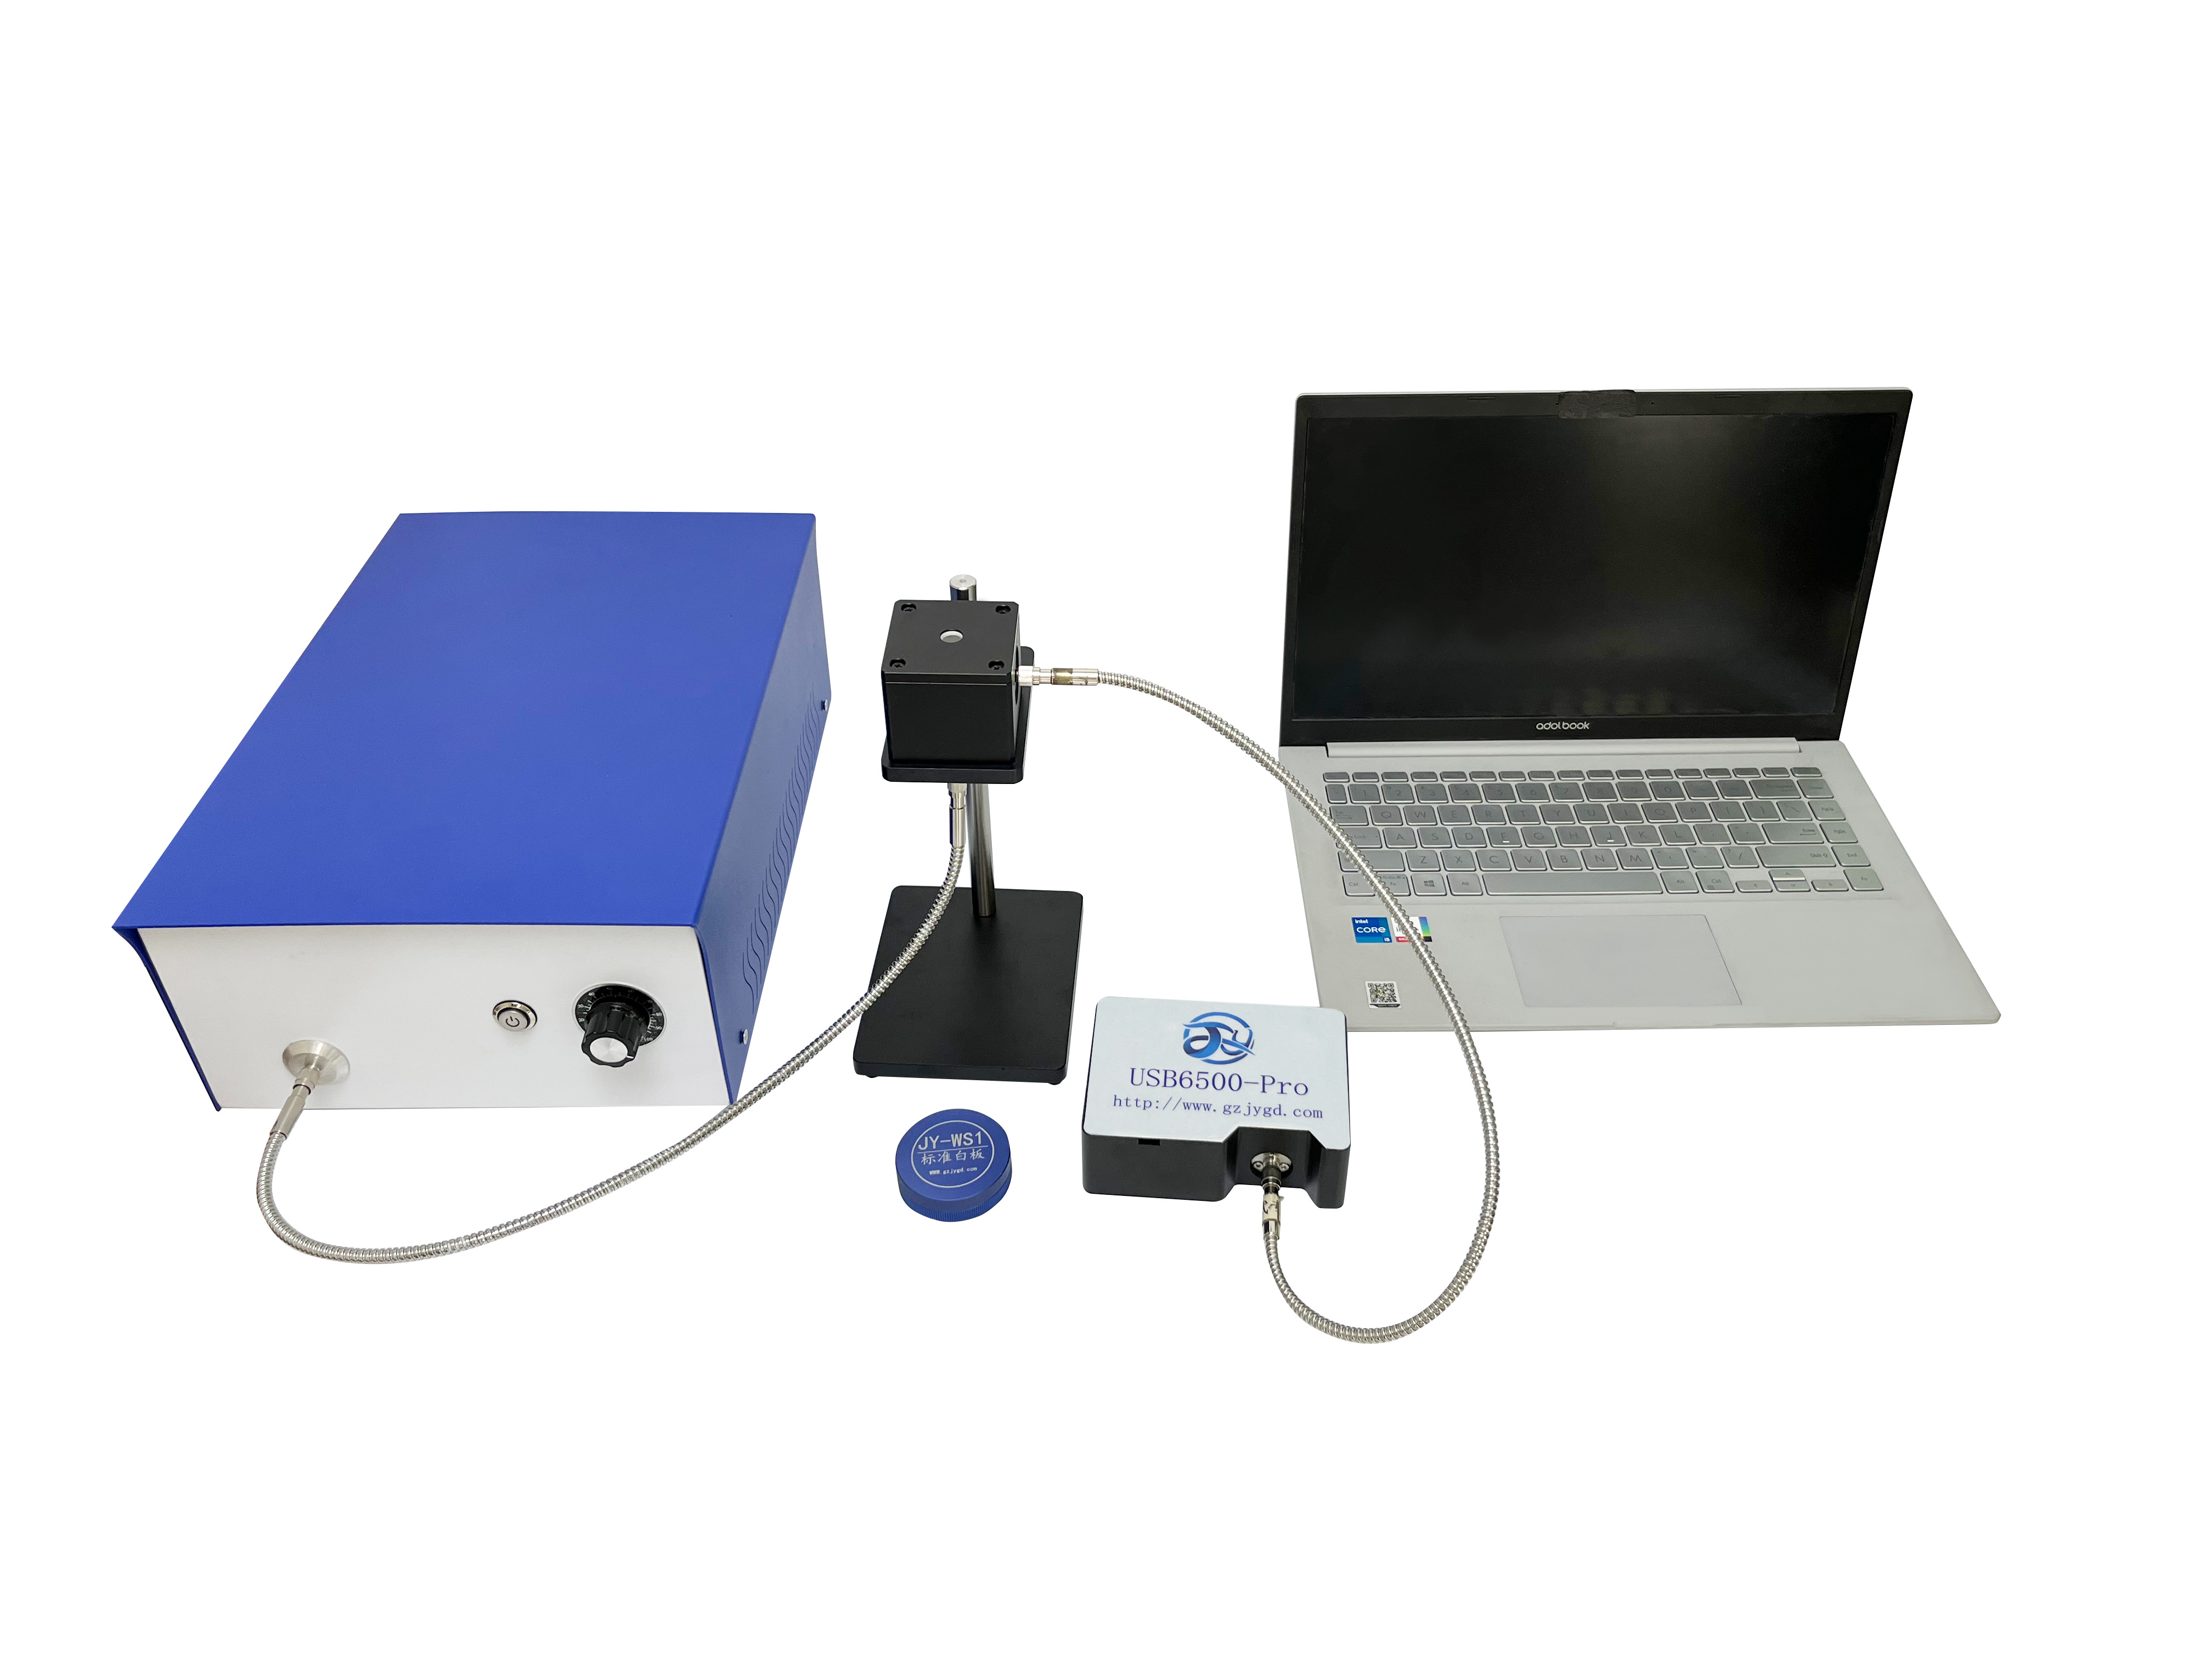
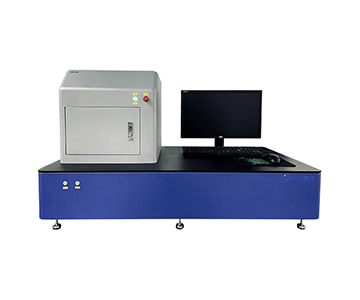
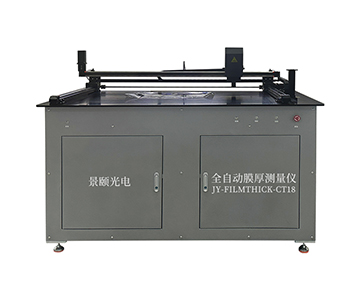
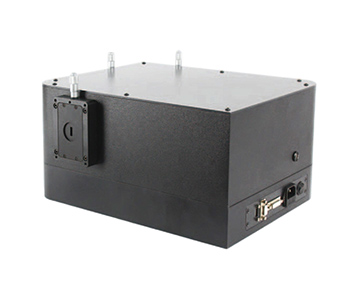
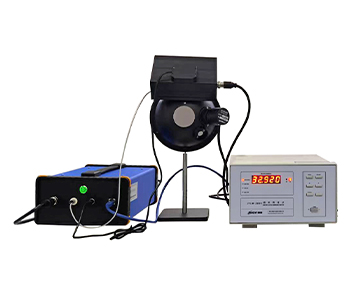
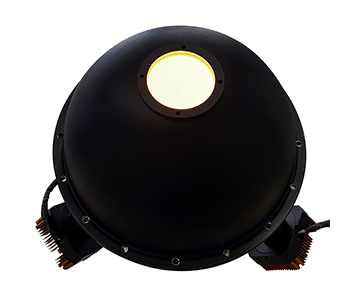
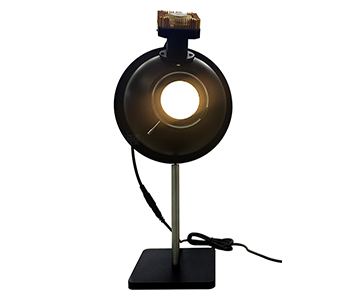
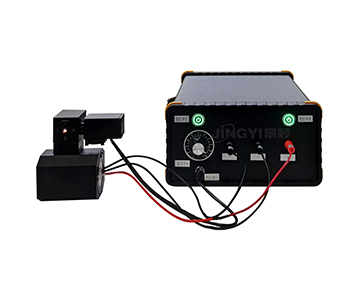
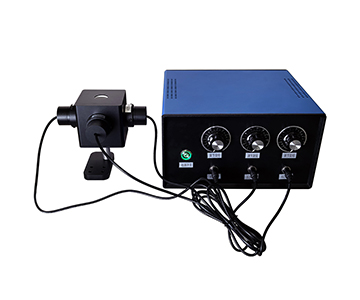
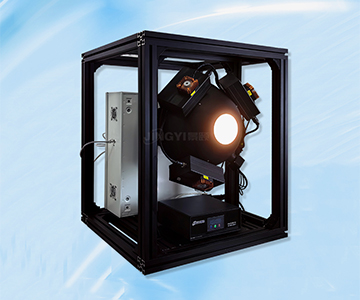
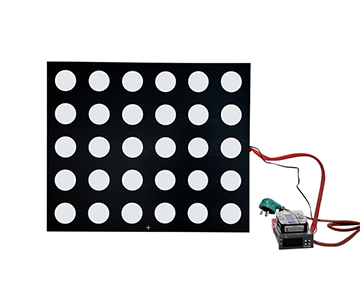
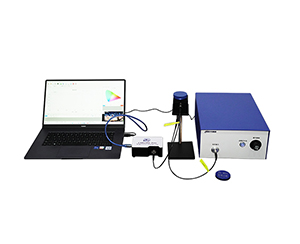
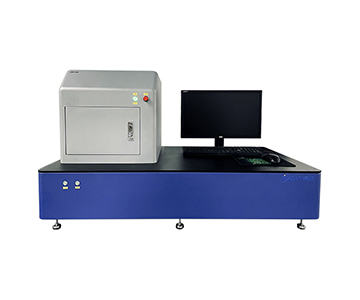
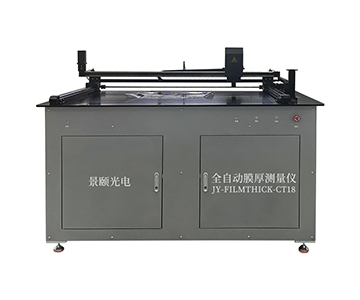
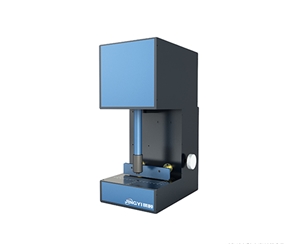
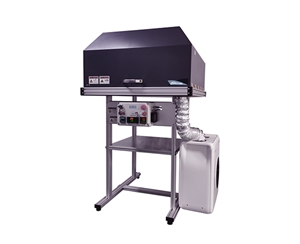
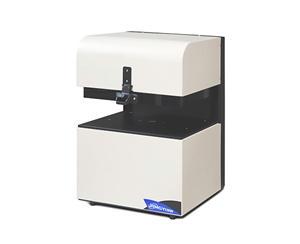
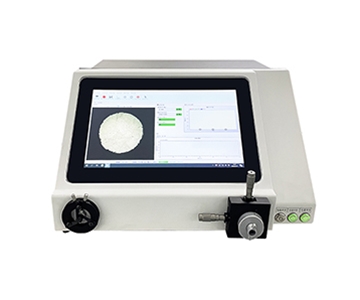
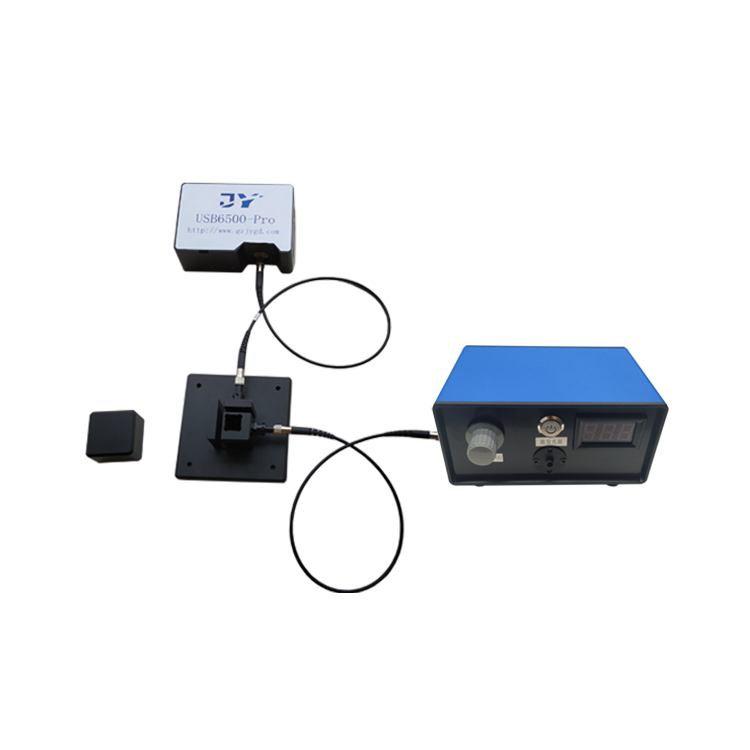
A transmittance measurement system used in plastic laser welding and optical film inspection is only as reliable as its worst drift cycle, not its best single reading. On production lines running continuous shifts, weld strength consistency is governed less by the welding parameter set than by two quietly degrading numbers: wavelength repeatability and measurement repeatability. In a qualified production environment, a mainstream near-infrared optical gauge using a 980 nm source matched to the welding wavelength, automatic zero calibration, and full-field multipoint scanning can complete one measurement in under 1 second, with measurement repeatability below 1% and a detection resolution of 0.01%. These are the conditions under which light-energy variation stops being mistaken for material variation.
Why a 2.3 Percentage Point Drift Escalates into Batch Rework
The hidden cost of transmittance drift on a plastic laser welding line
During a night shift at an automotive plastic components plant, a set of readings was recorded that no one acted on at the time. The same lot of modified polymer parts measured 28.4% transmittance on the first-piece check in the morning and 26.1% when re-tested after midnight — a 2.3 percentage point drop. The difference never triggered an alarm, because the manual sampling routine in use covered exactly one point on exactly one part at exactly one moment.
Weld strength dispersion rose in the following shift. Defective parts reached the next operation, and the rework loss totaled roughly $152,000.
The accident chain is depressingly consistent across plants: the welding machine parameters had not changed. What changed was the transmitted energy of the incoming material and the measurement value assigned to it. In plastic laser welding, transmittance sits on a steep part of the process curve. Read a little high and laser energy over-deposits in the weld zone, melting or embrittling it; read a little low and the energy never reaches the joint interface, leaving an incomplete bond. The acceptable window is narrow, and it is defined by the actual part in the fixture, not by a lab standard.
A handheld single-point gauge compounds the problem through two overlapping blind spots. First, one point cannot represent an injection-molded surface whose transmittance varies across the flow lines. Second, without automatic calibration, source aging and detector dark-current drift are silently added into every result. When the inspection step itself drifts, process tuning loses its reference point — engineers end up optimizing against a moving target.
Locking the Measurement Value with a Matched Wavelength Source and Automatic Calibration
How matched-wavelength optics and auto-calibration suppress long-term drift
The engineering answer is to design drift suppression into the optical path and the software workflow, rather than training it into the operator.
The central design choice is to keep the inspection source on the same wavelength band as the welding laser. The default is 980 nm, with 850 nm, 905 nm, 915 nm, and 940 nm available as
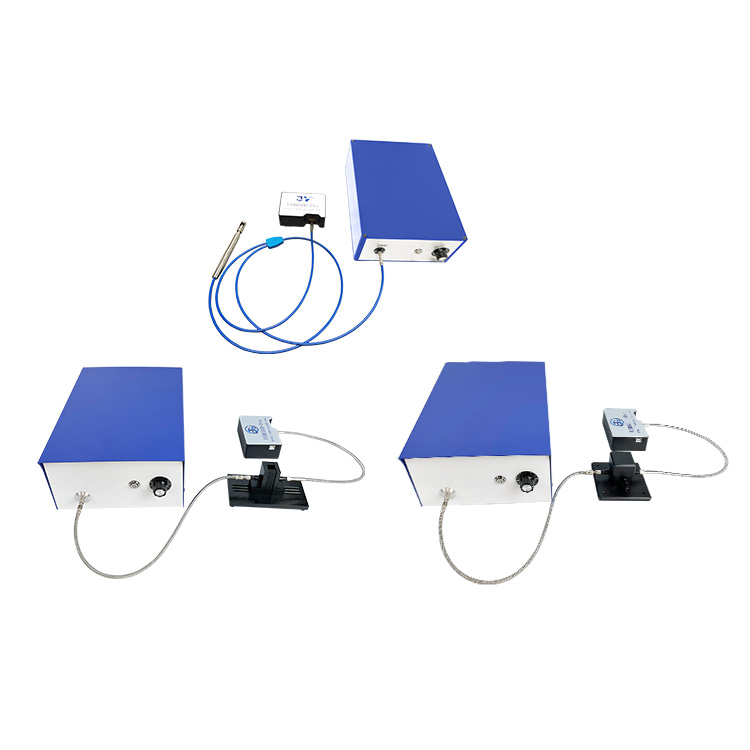
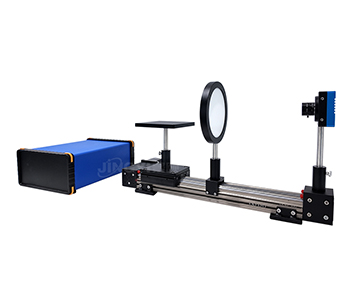
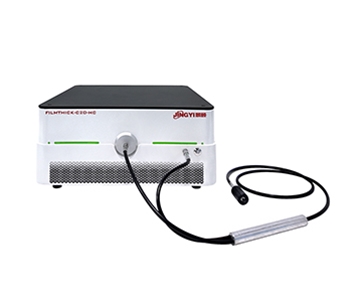
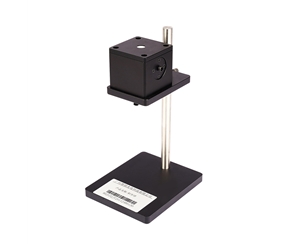
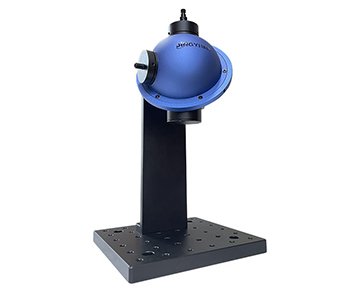
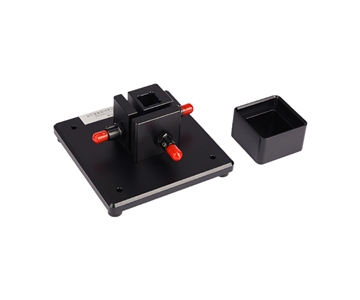
For curved or tubular workpieces, a non-planar single-point geometry paired with a contoured stage keeps the incident beam normal to the measured area. The extra reflection loss introduced by a tilted part attitude is removed at the hardware level. This is the detail that decides whether arc-shaped parts from different shifts are numerically comparable at all.
Automatic calibration resets the reference on every power-up and after extended continuous operation. Combined with automatic dark-background subtraction, source attenuation and detector zero-point drift are stripped out of the reported result instead of being averaged away.
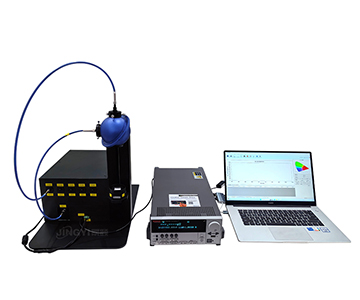
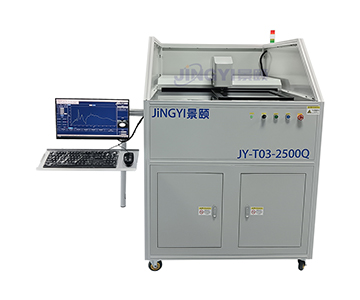
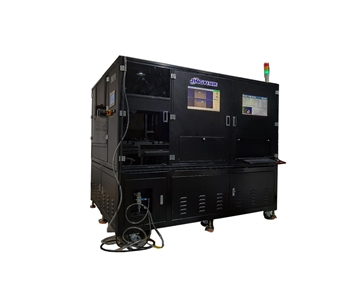
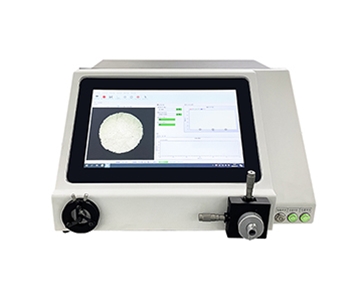
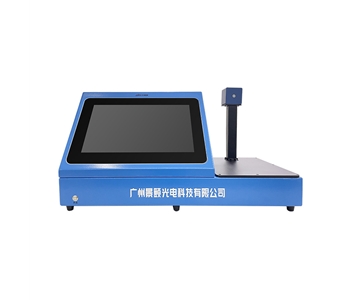
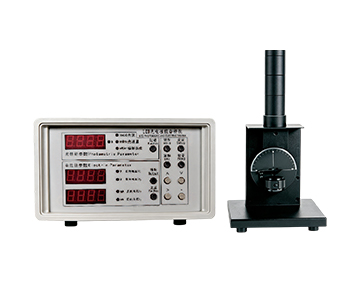
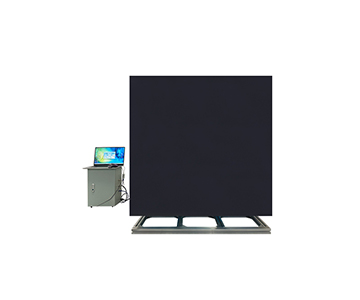
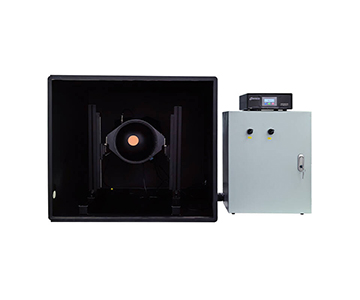
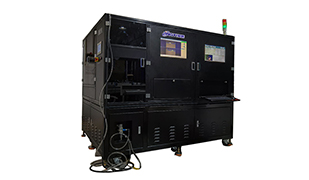
The measurement specification is built around repeatability rather than a headline accuracy number: measurement repeatability below 1%, detection resolution of 0.01%, a 0–100% transmittance range, and a single-test time of 1 second or less. Scanning a defined area in under one second means multiple points are measured simultaneously rather than by sequential repositioning — which compresses the tact time and removes the repeat-positioning error that a change of fixture station would otherwise introduce.
From Flat Panels to Curved Tubes: Matching the Optics to the Part Geometry
Transmittance testing across flat panels, curved welded parts, micro-areas, and fiber optic samples
Flat panels and thin-film samples
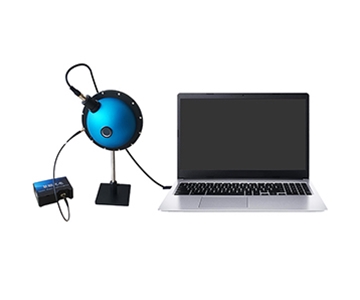
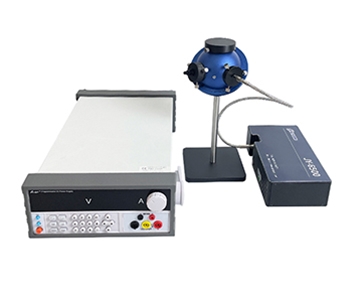
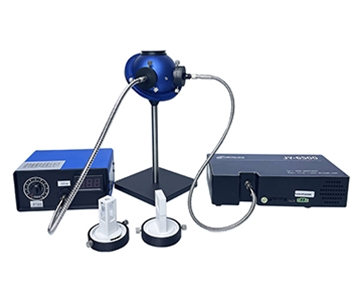
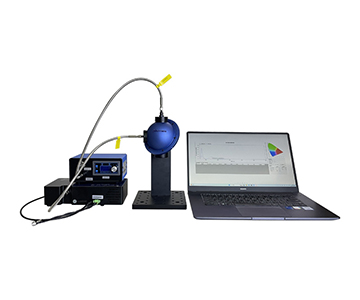
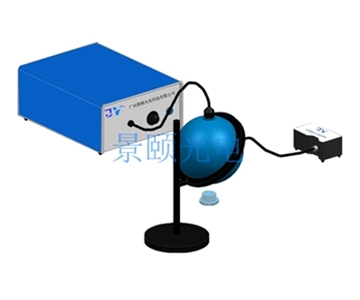
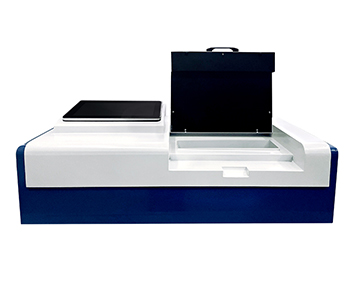
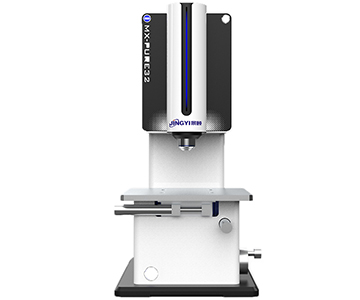
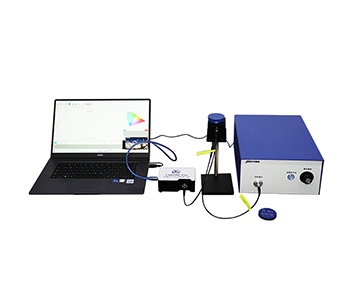
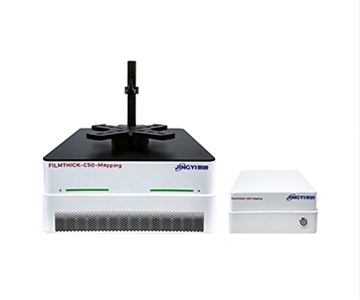
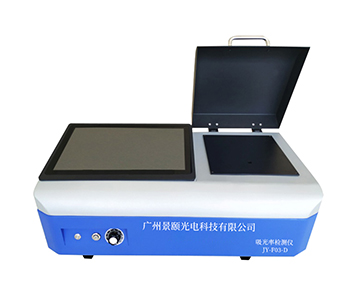
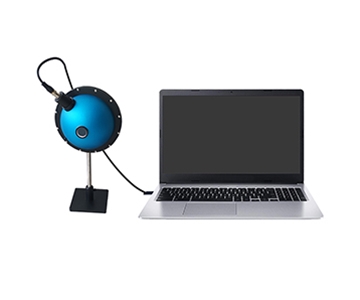
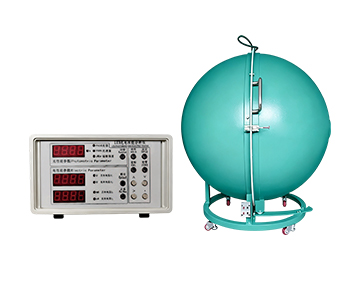
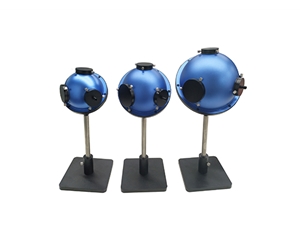
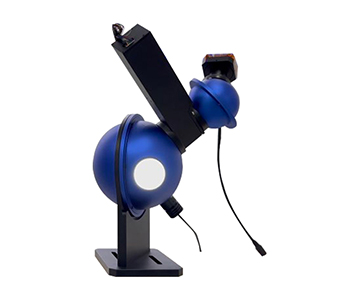
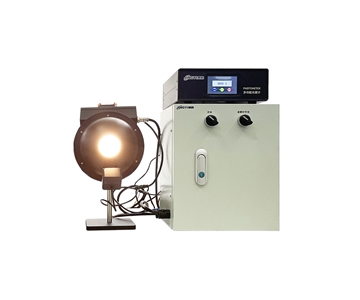
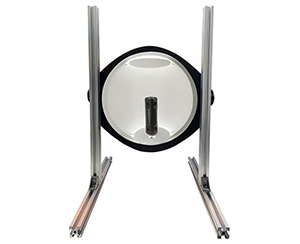
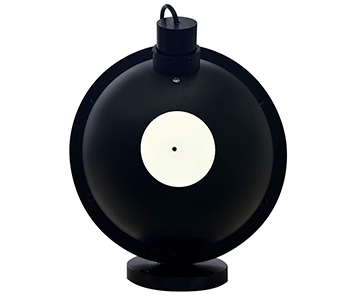
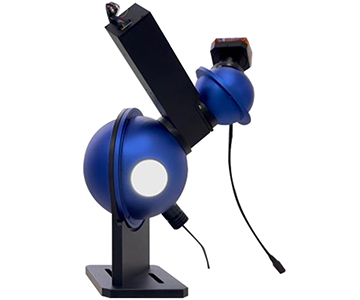
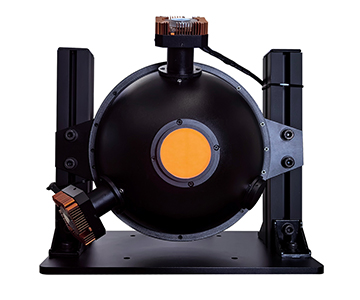
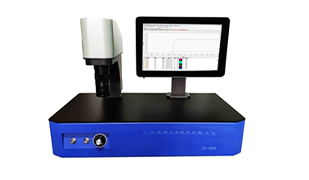
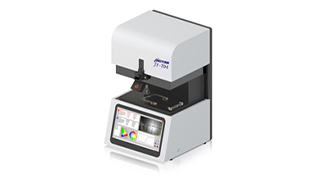
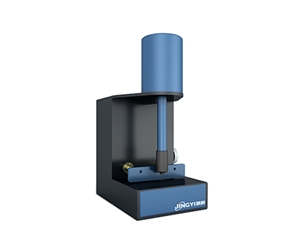
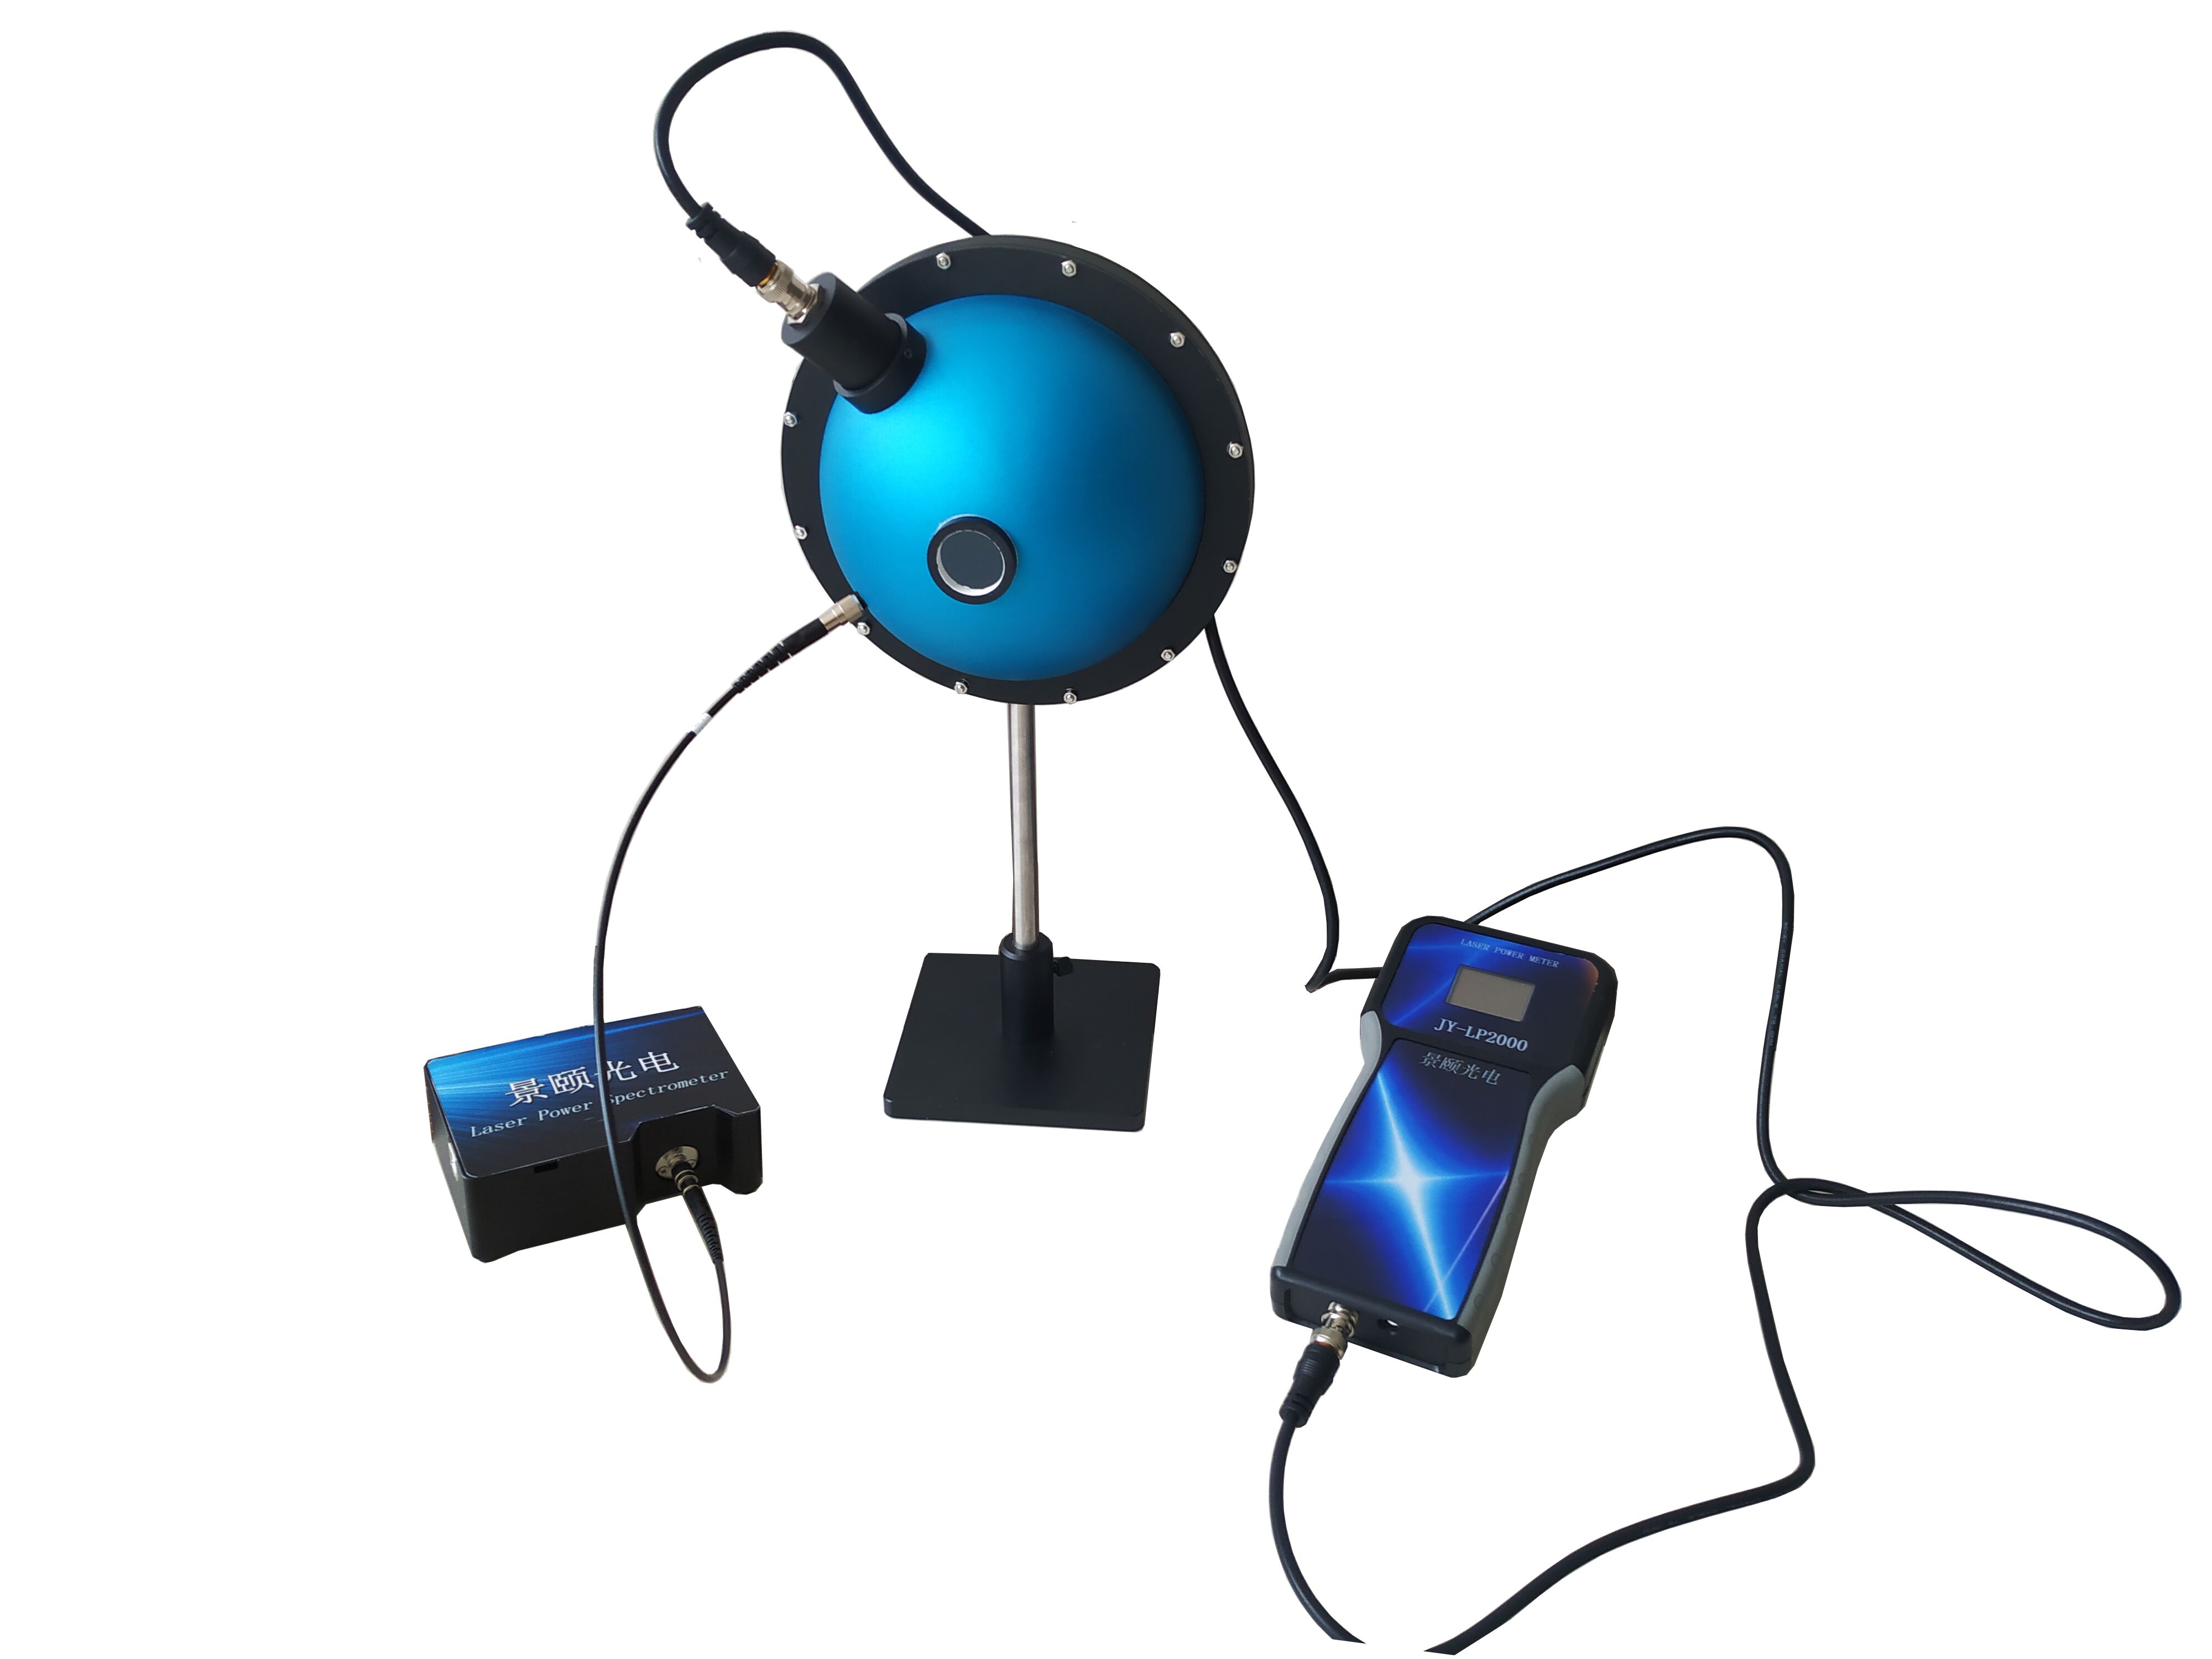
For display panels, mobile phone screens, touch panels, optical filters, and plastic films, an integrating sphere collection path with vertical illumination is the appropriate geometry. Spot diameter is selectable from 0.3 mm to 3 mm, spectral resolution is 1 nm, and a single-side measurement takes 30 ms or less.
The relevant reference point here is GB/T 47066-2026,
Determination of total transmittance and total reflectance of plastics
. Under the conditions described in that standard, transmittance measurement accuracy better than 1% and test repeatability better than 1% are documented, which covers the routine incoming and in-process inspection needs of film and flat glass products.
Non-planar measurement of curved and irregular parts
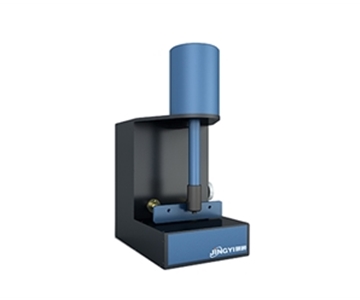
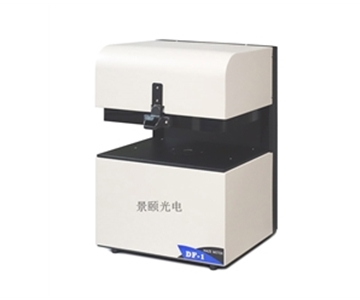
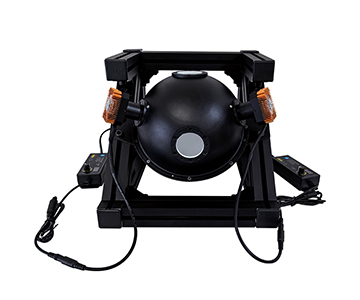
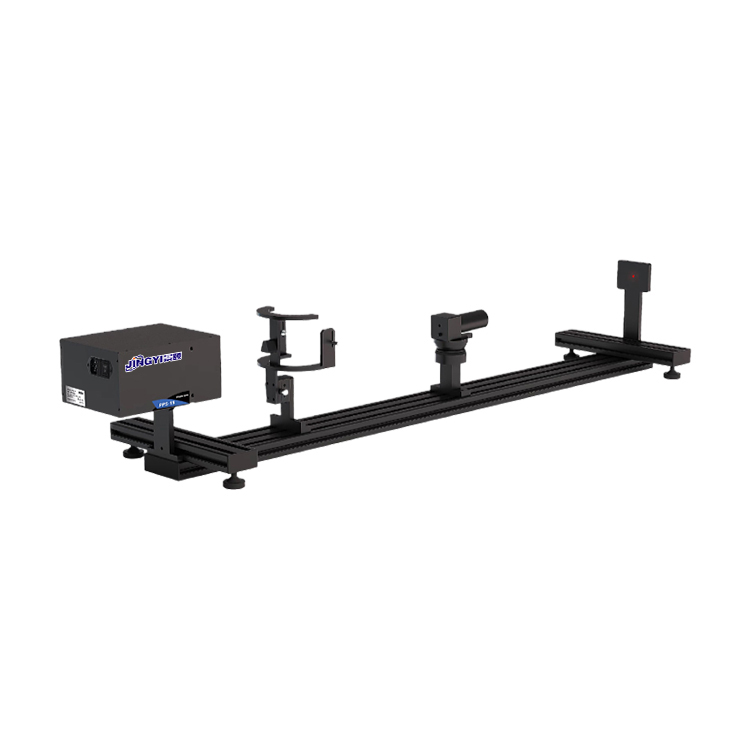
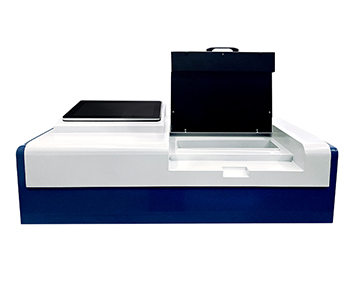
A curved laser-welded part cannot simply be placed flat on a conventional sample stage, which is why a separate curved-body configuration exists. Three versions cover samples from 10–150 mm and 10–450 mm in length, with a minimum diameter of 5 mm; adjustment is available in manual and motorized variants, the latter reaching measurement repeatability below 0.5%.
The practical advantage is a configurable contoured stage and a multi-degree-of-freedom adjustment bracket, allowing tubular and irregular components to be measured without disassembly. That flexibility is what makes the same instrument usable in both a laboratory and a flowing production line.
Micro-areas and fiber optic samples
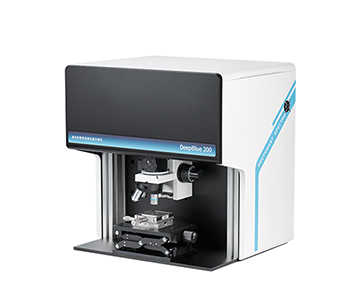
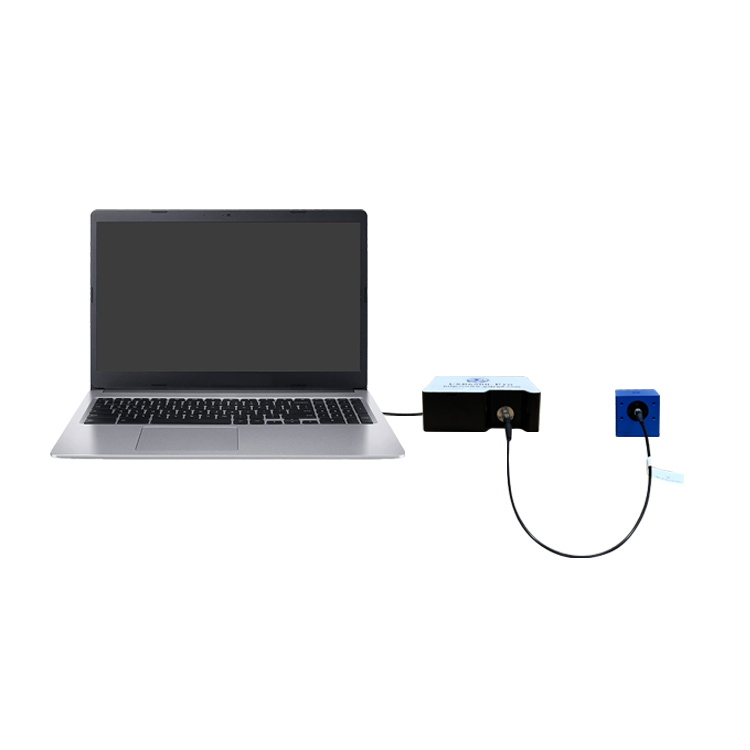
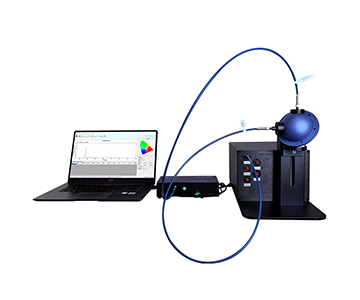
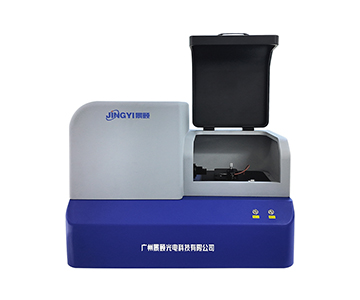
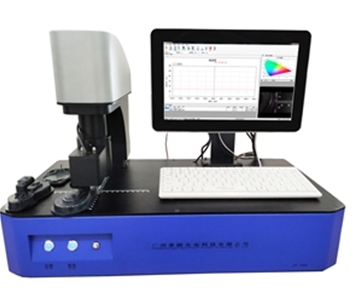
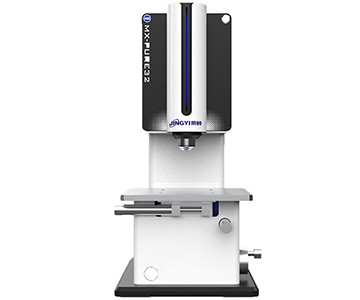
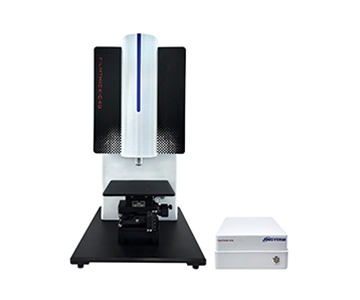
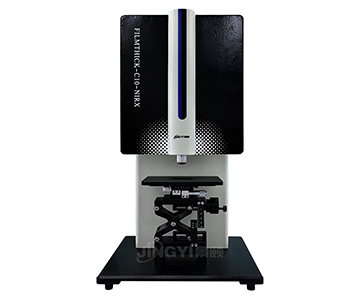
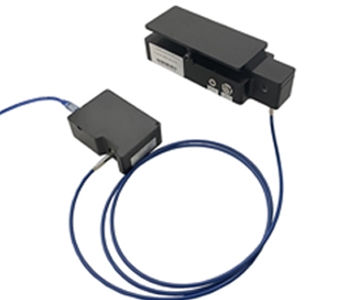
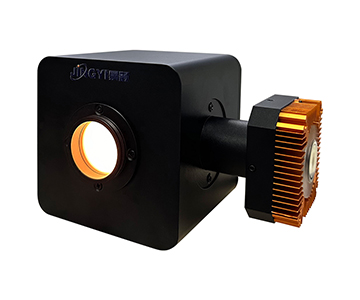
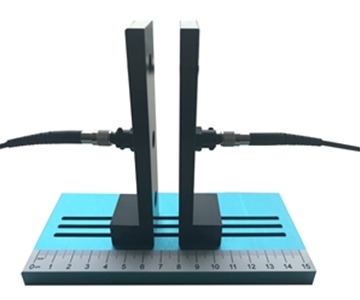
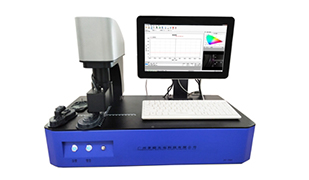
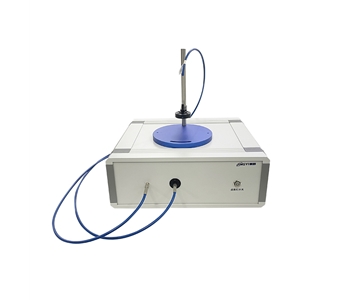
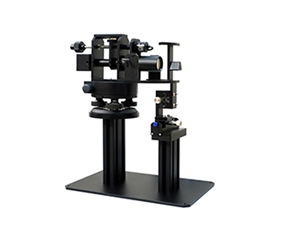
For small, thin, or strongly curved samples, a microscope-type instrument focuses a measurement beam of 1 mm or less and a roughly 60 µm spot onto the surface, making it possible to judge uniformity across a lens surface or a coated layer. Fiber optic samples are routed through the sample chamber by connecting both ends, with an end-face image snapshot taken alongside; transmittance spectrum and color uniformity are output together. These two configurations place the highest demands on optical alignment, which is also where long-term drift tends to show up first.
Production Data: What Changed After the Numbers Stabilized
Validated results from a full-field multipoint deployment on an automotive welding line
| Metric |
Before deployment |
After deployment |
Change |
| Sampling coverage |
12% (single-point) |
100% (full-field multipoint) |
+88 percentage points |
| Daily value drift |
±2.3% |
±0.4% |
Compressed to roughly one-sixth |
| Welding defect rate |
3.7% |
0.9% |
−75.7% |
| Inspection hours per shift |
4.5 h |
1.2 h |
−73.3% |
The most representative installation is the plastic-part welding station of a major domestic automaker. After introducing full-field multipoint detection and automatic OK/NG judgment, sampling coverage rose from 12% to 100%, daily drift fell from ±2.3% to ±0.4%, the welding defect rate dropped from 3.7% to 0.9%, and per-shift inspection time went from 4.5 hours to 1.2 hours. Coverage increased by 88 percentage points; daily drift was compressed to roughly one-sixth of its former value; defect rate fell by 75.7%; inspection hours were reduced by 73.3%.
The interpretation is straightforward. Moving from "one point pulled at random" to "a defined area, fully scanned, with automatic maximum, minimum, and mean statistics" constrains both the missed-measurement risk and the drift in the measured value at the same time. Report output and a user-configurable acceptance range then turn the quality data into something auditable.
Why Repeatability Matters More Than Single-Reading Accuracy
Why repeatability under continuous operation matters more than a single-point accuracy figure
Viewed through the lens of long-term drift, the absolute accuracy of one isolated sample is rarely the scarcest capability on a line. What actually determines lot-to-lot consistency is how the instrument behaves after hours of continuous operation, source aging, and ambient temperature change.
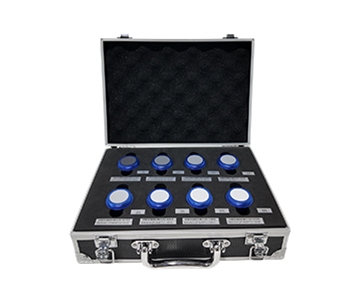
A mainstream instrument in this class documents wavelength repeatability of 0.2 nm, instrument repeatability of 1% or better, and wavelength accuracy within 1 nm. Together these three form the foundation of a stable measured value.
The distinction is worth keeping clear. Wavelength repeatability describes how reliably the spectral peak returns to the same position across multiple measurement runs; measurement repeatability describes the scatter among repeated readings of the same sample. A slow upward or downward creep on a trend chart is the typical symptom when either one deteriorates. For that reason, acceptance testing should be done with a reference standard across multiple time intervals — not judged from a single-point figure on a factory calibration certificate.
The Constraints No One Should Ignore
Where this approach fits, and where it does not
This approach does not fit every inspection task.
First, near-infrared instruments are built around welding-process wavelengths. If the object requires UV coverage — full-spectrum evaluation of photovoltaic glass, for example — a 250–2500 nm broadband instrument is the appropriate choice; the wavelength range of the near-infrared type does not directly cover that requirement.
Second, the motorized adjustment version for curved parts carries explicit lower limits on sample diameter and length (minimum diameter 5 mm). Wire and micro-tubing below that threshold need fixture compatibility confirmed before a line is committed.
Third, fully automatic loading and robotic integration carry requirements of their own: floor space, compressed air, and tact-time matching. In low-volume, high-mix conditions, a semi-automatic configuration offers changeover flexibility that is often the more economical choice.
Frequently Asked Questions
Q1: Where does long-term drift in a transmittance gauge mainly come from?
The primary sources are energy attenuation from source aging, changes in detector dark current, and changes in the reflectance of the integrating sphere coating. Instruments with automatic calibration and automatic dark-background subtraction, combined with periodic re-checking against a verification standard, keep this portion of the drift within a relatively small range.
Q2: How is measurement repeatability maintained on curved samples?
The deciding factor is keeping the incident beam normal to the measured area, which a contoured stage and multi-degree-of-freedom bracket can provide. It is also necessary to confirm that the instrument supports non-planar single-point measurement, and to lock the same measurement location and spot parameters in the software for every run.
Q3: How do you choose between full-field scanning and single-point detection?
Single-point detection is faster and suits homogeneous materials. Full-field multipoint detection suits injection-molded and welded parts where uniformity matters: it automatically outputs independent values for each region together with the maximum, minimum, and mean, removing the possibility that a low-reading area is simply missed.
Q4: What should I look at to judge long-term stability when selecting equipment?
Wavelength repeatability and measurement repeatability are the two indicators that matter, rather than wavelength accuracy alone. Also confirm that the instrument provides automatic calibration, a verification standard, and a calibration certificate, and check standard compliance — in this application, compliance with GB/T 47066-2026 should be confirmed so that the traceability chain of the measured value is complete.
Q5: How can I independently verify the reliability of a transmittance measurement system?
Use a reference standard supplied by an independent metrology institute and re-measure across time intervals, comparing the instrument reading with the standard value. Require the supplier to provide a factory calibration certificate with a traceable calibration chain, and during acceptance simulate a long continuous-run condition to see whether the trend curve develops a systematic offset.
Editorial Notes
Research Basis
: Product technical documentation from Guangzhou Jingyi Optoelectronics Technology Co., Ltd.; GB/T 47066-2026,
Determination of total transmittance and total reflectance of plastics
; deployment records from an automotive plastic welding line.
Reviewed by
: Cai Xiaodong, Senior Application Engineer at Jingyi Optoelectronics, with 10 years of experience in optical inspection and industrial quality control, focused on deploying spectral measurement systems on manufacturing lines.
Sponsorship Disclosure
: Jingyi Optoelectronics manufactures optical measurement instruments. The assessments in this article rely on published specifications and aggregated deployment data. No third-party compensation was involved.
Reader Guidance
: This material is intended for educational and evaluation purposes. Equipment choices should always be validated through on-site proof-of-concept testing under your own process conditions, including the actual material lot, shift-cycle duration, and ambient temperature range.
Publication Date
: September 2026
For detailed specifications and application notes on transmittance measurement systems, search "Jingyi Optoelectronics transmittance measurement system" or visit the technical library.