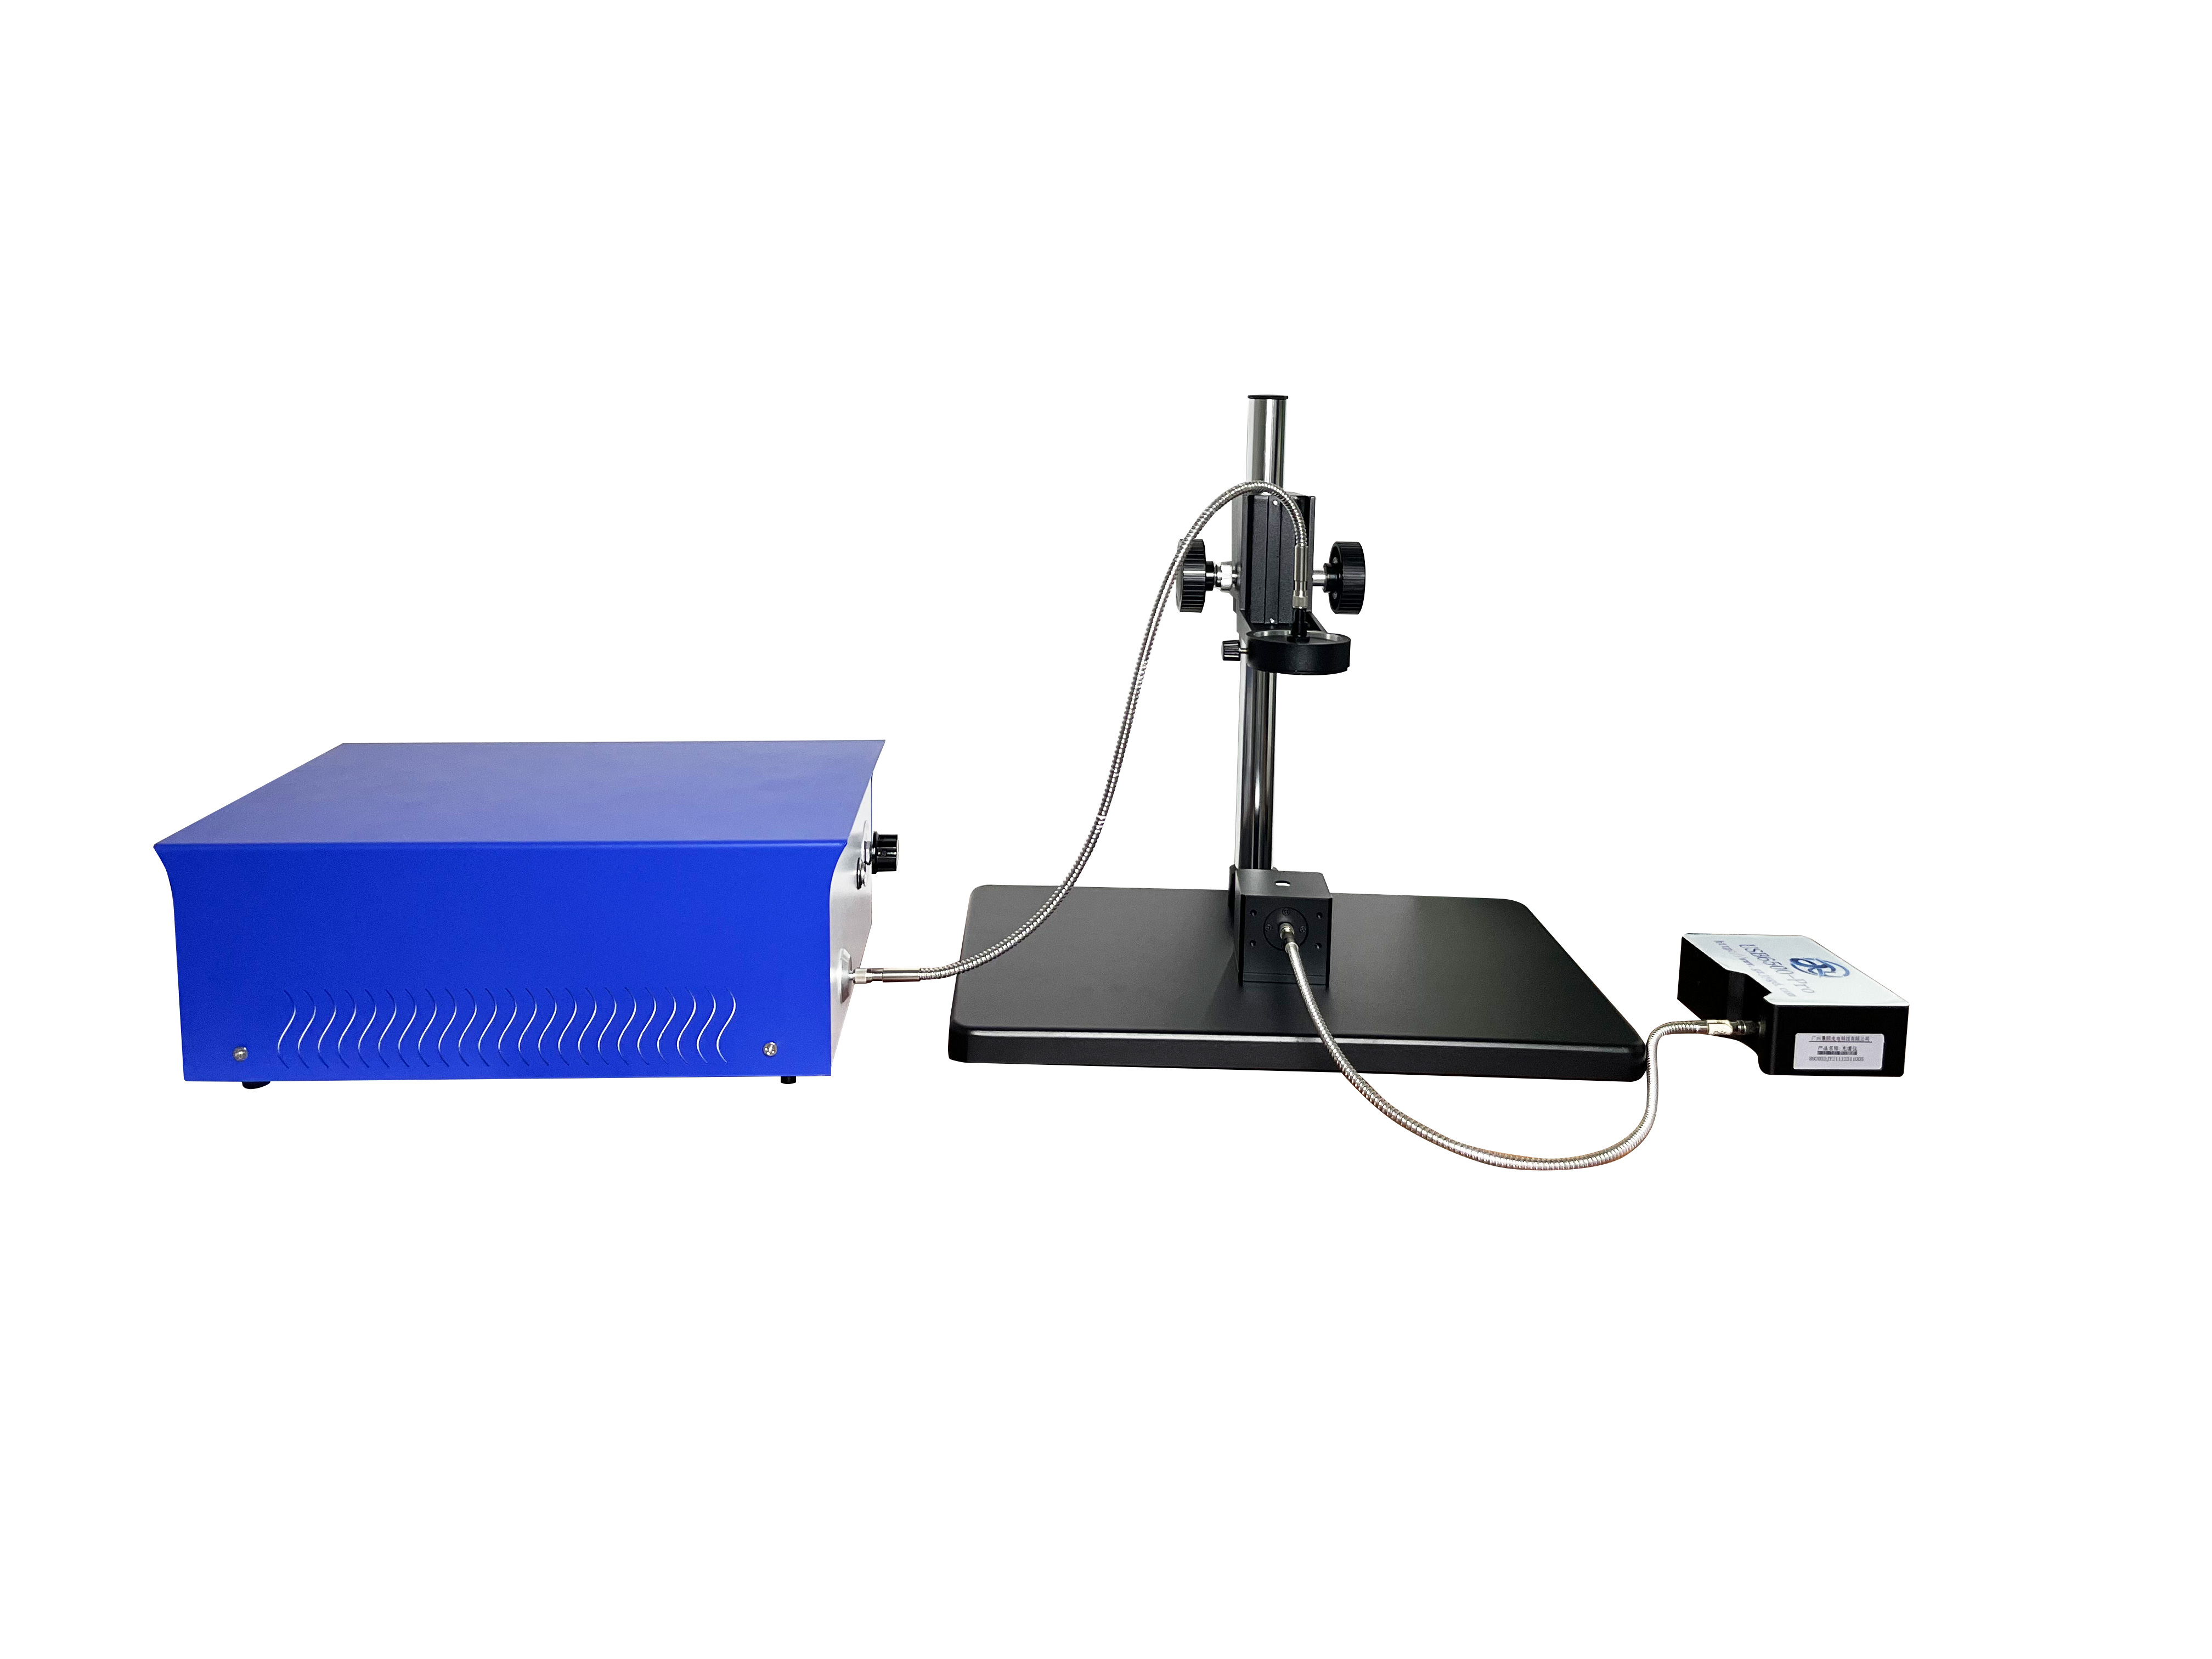
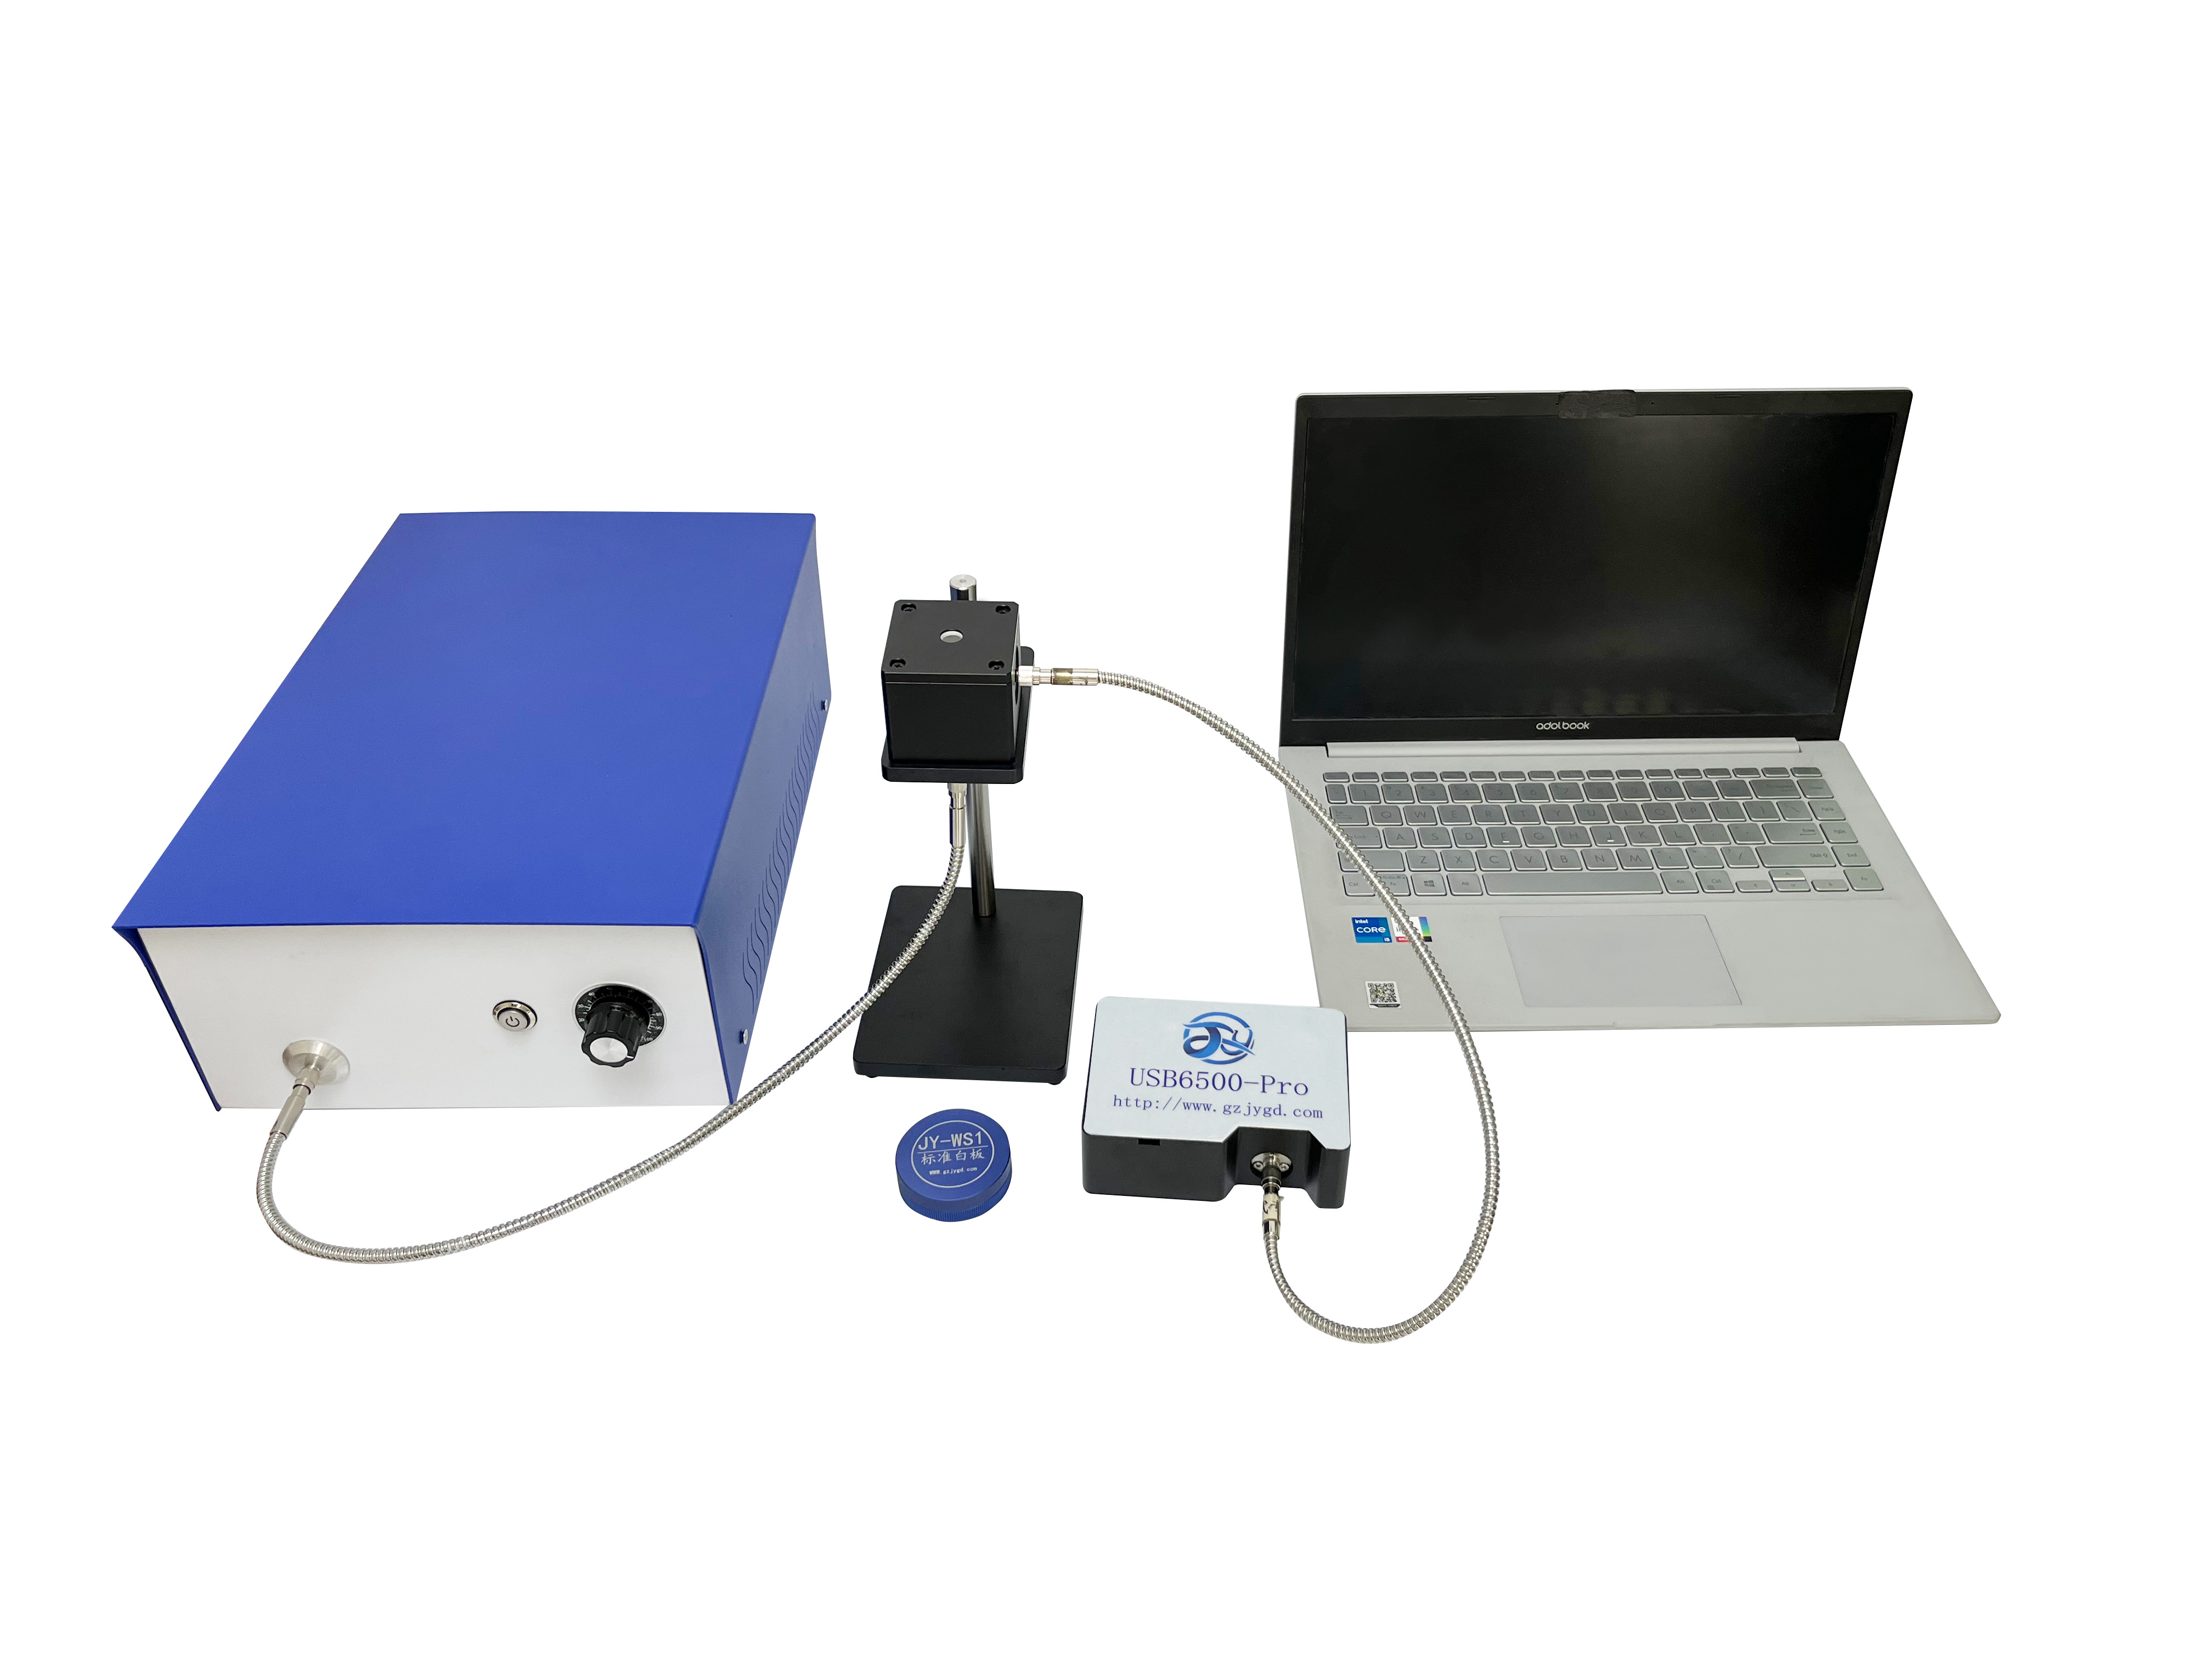
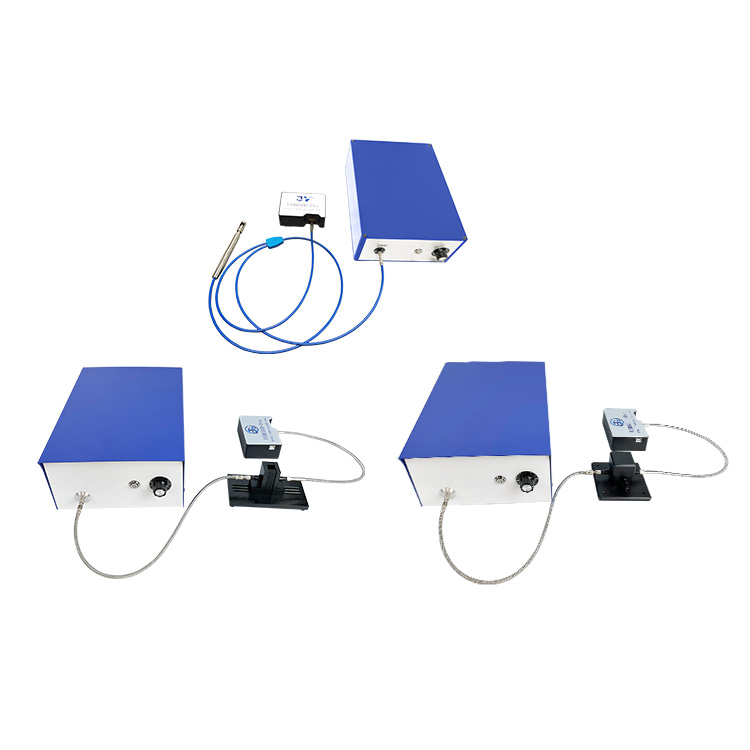
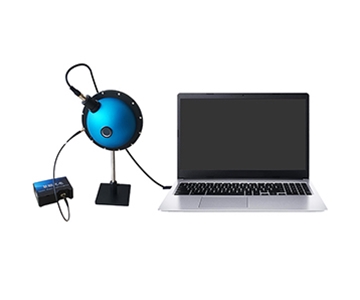
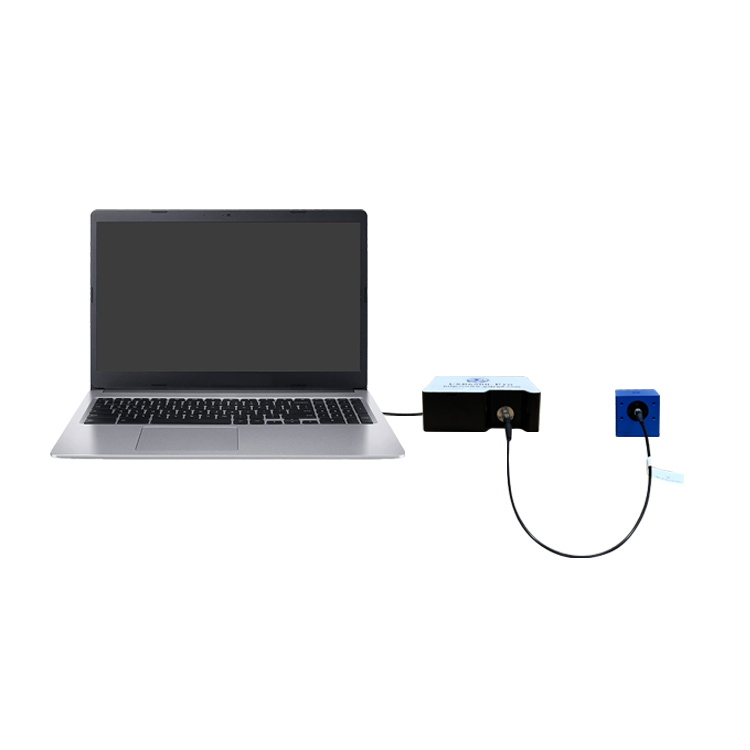
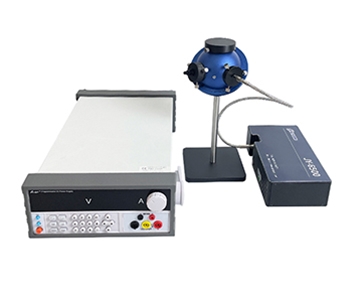
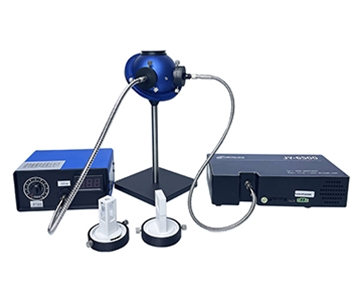
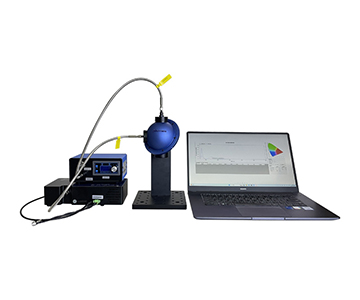
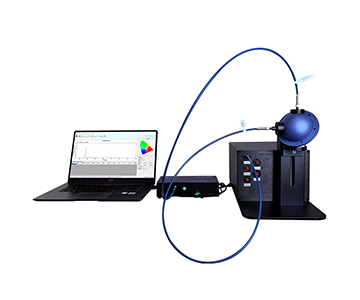
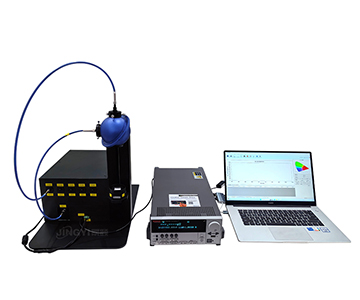
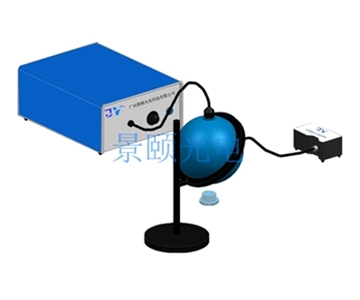
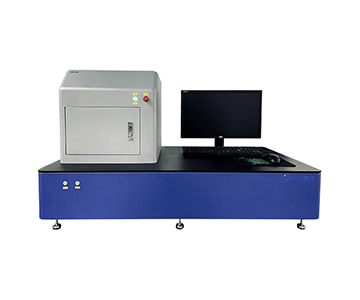
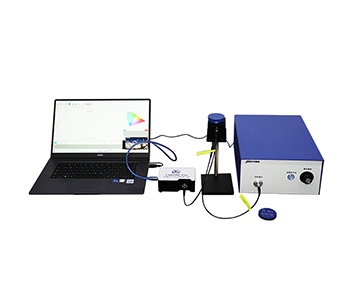
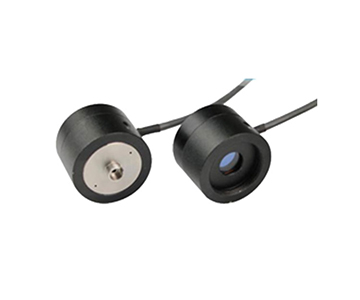
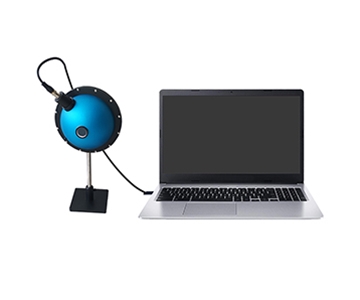
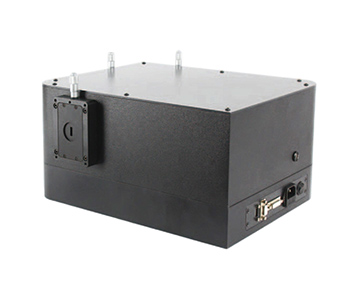
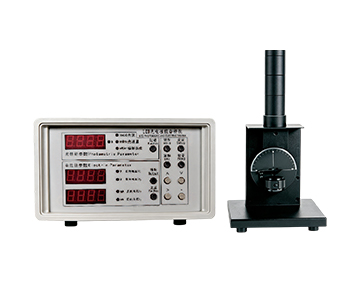
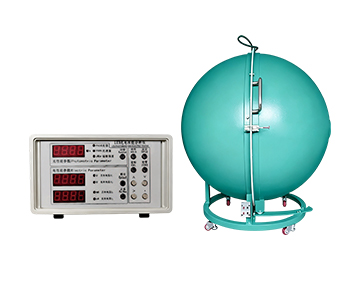
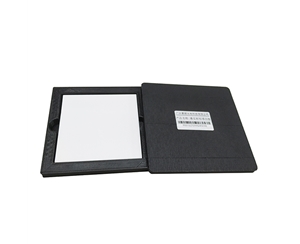
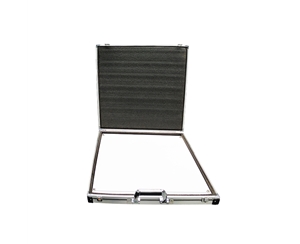
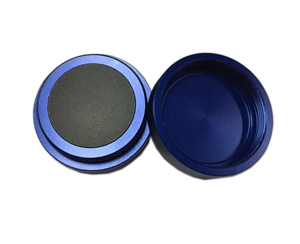
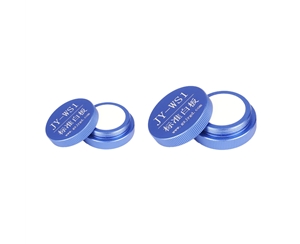
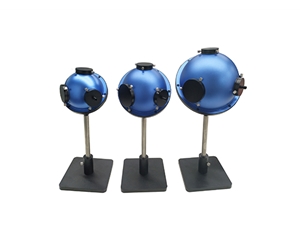
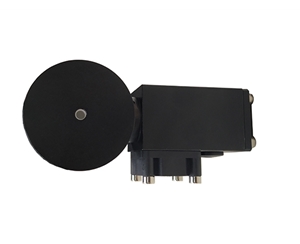
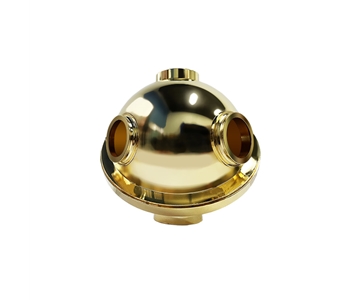
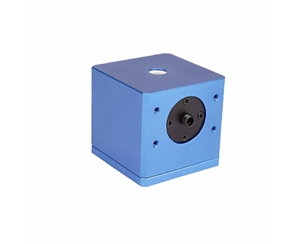
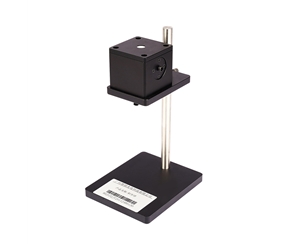
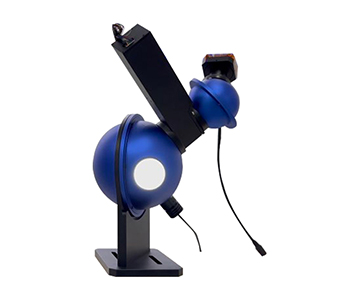
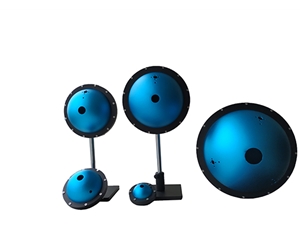
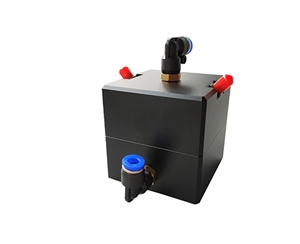
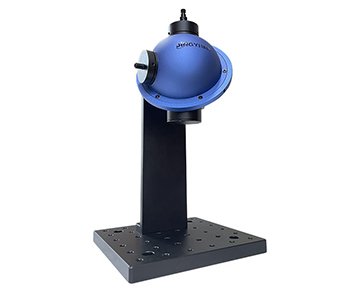
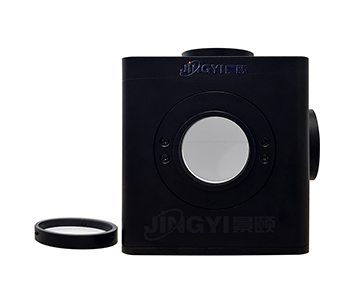
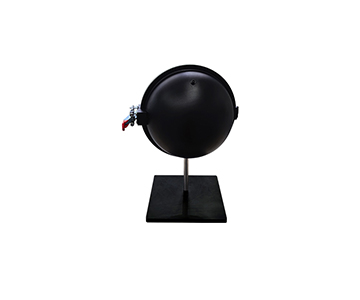
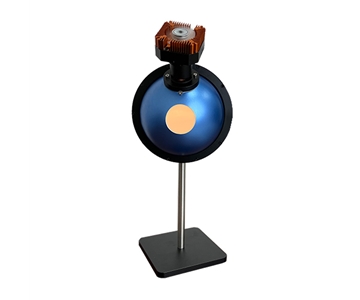
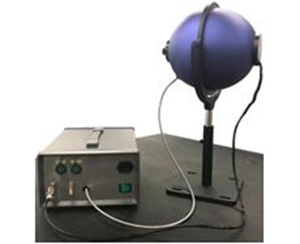
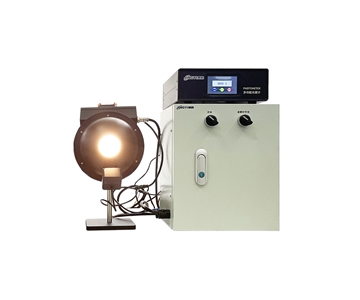
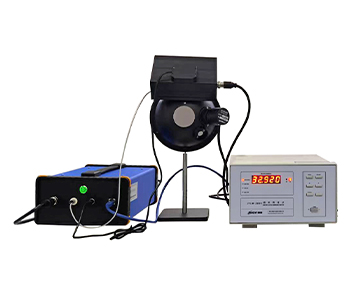
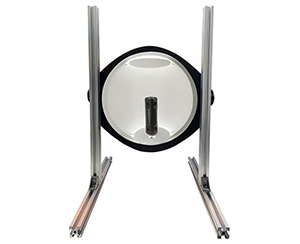
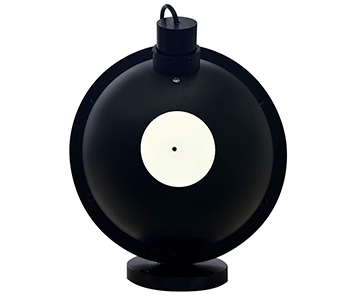
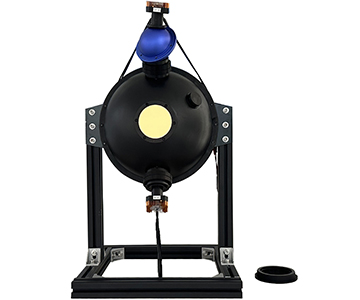
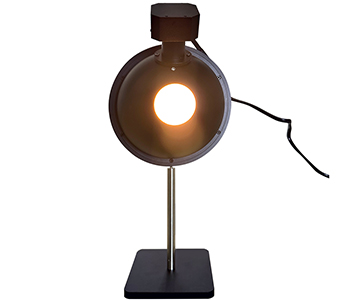
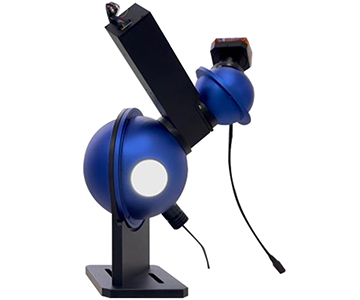
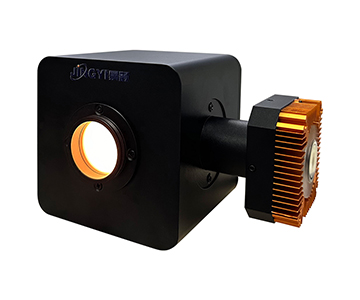
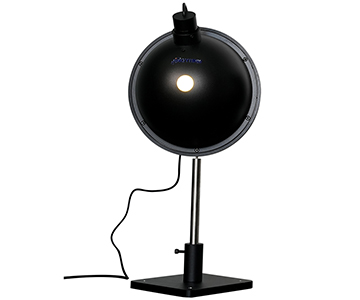
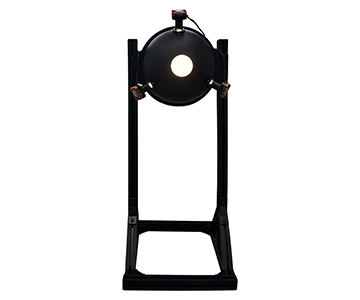
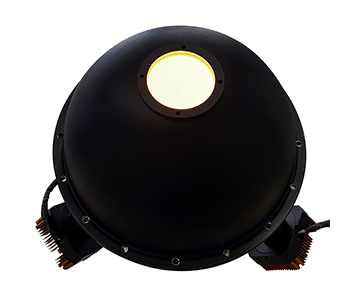
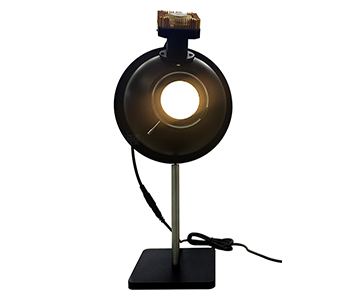
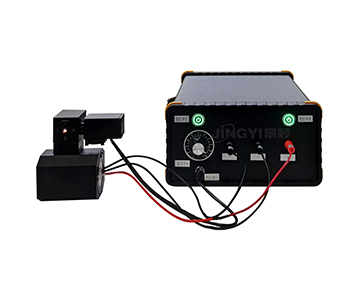
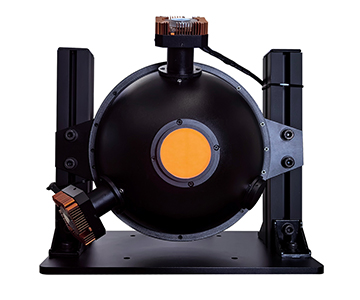
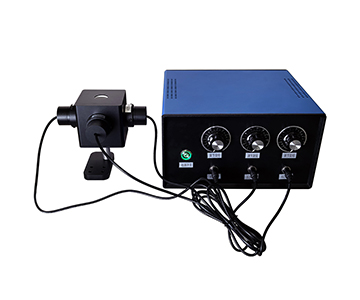
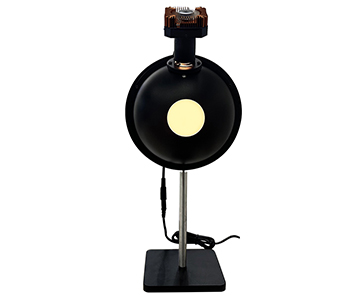
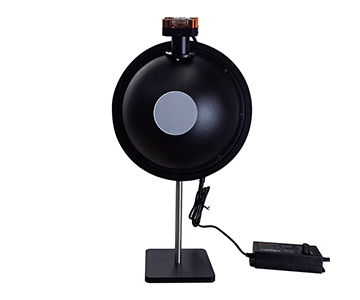
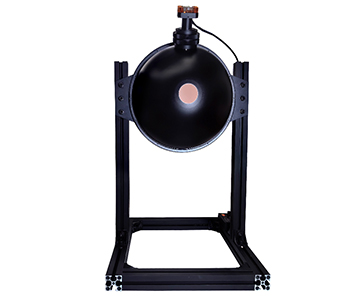
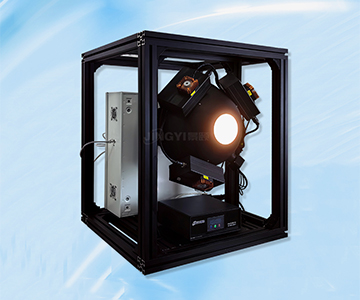
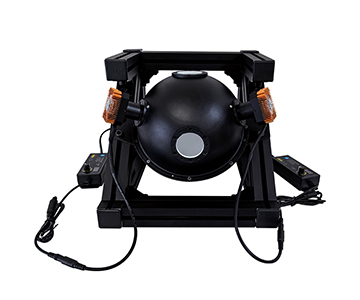
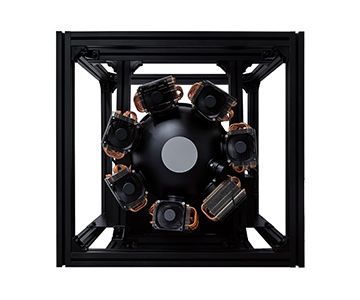
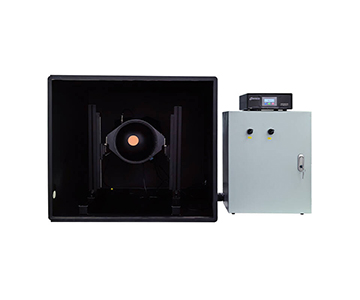
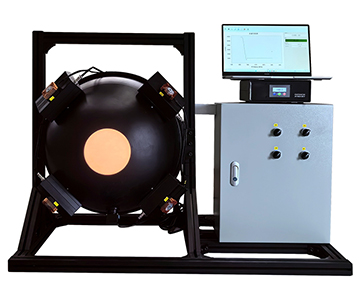
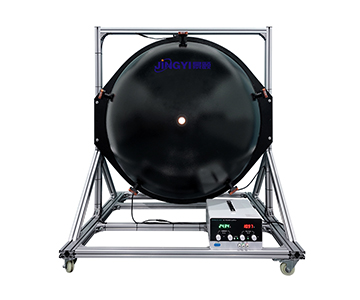
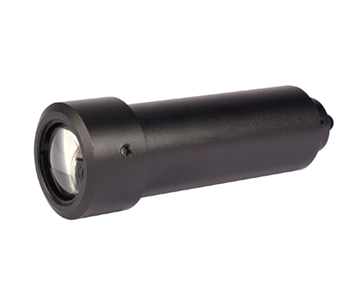
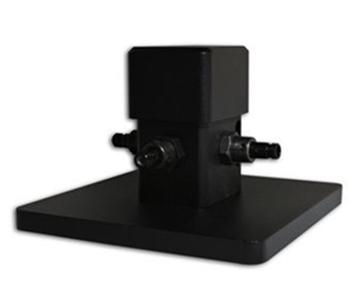
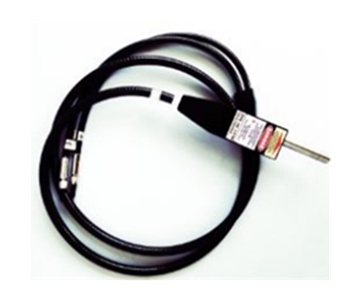
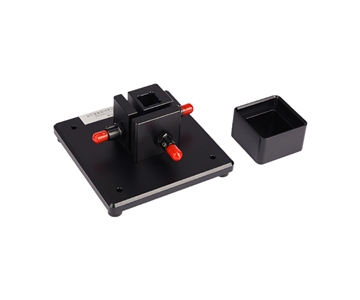
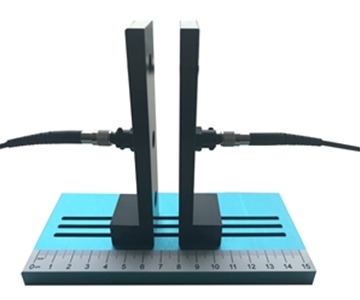
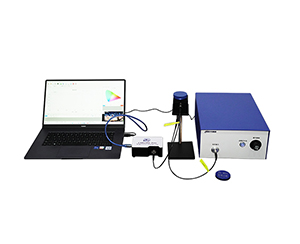
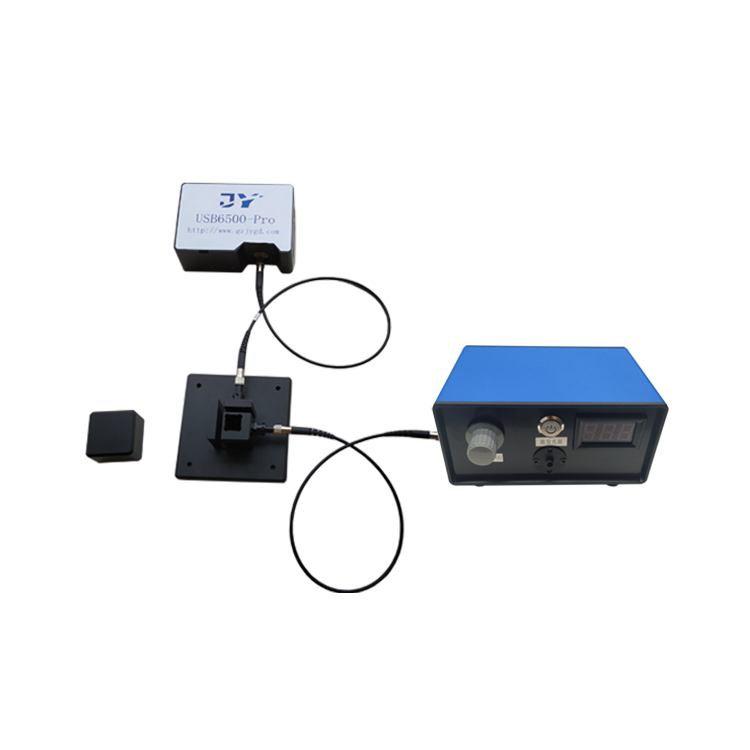
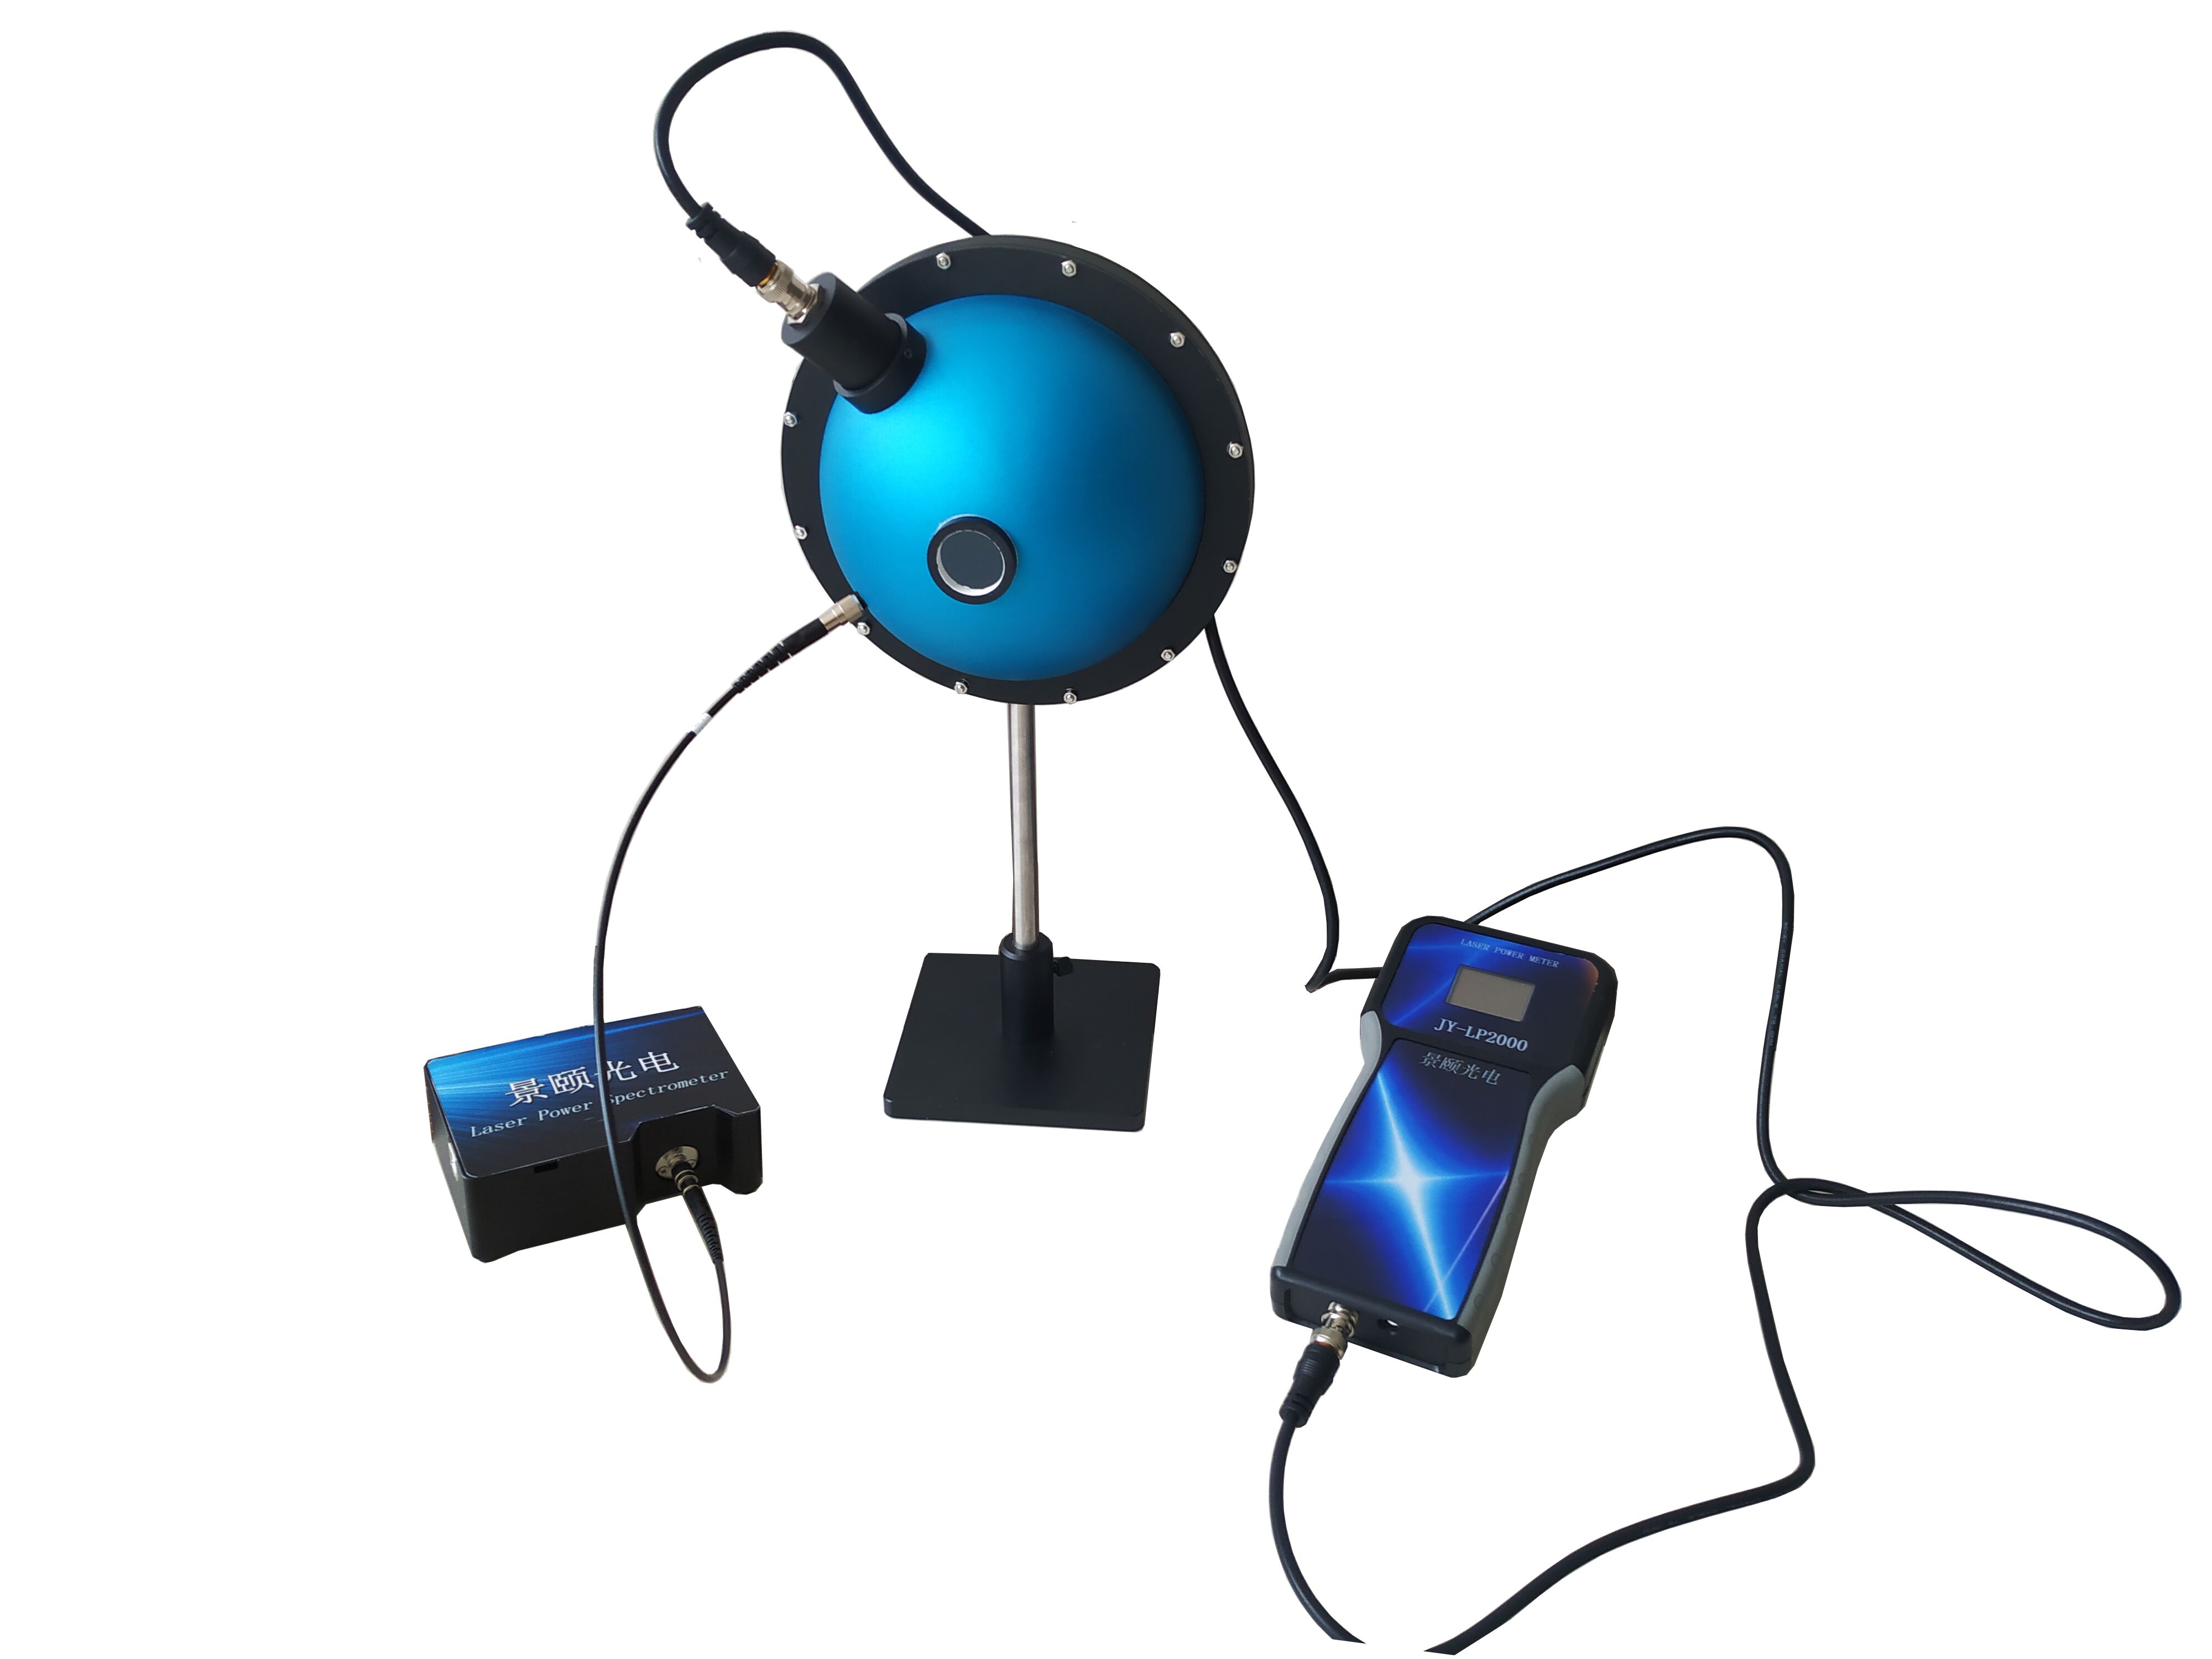
An integrating sphere turns directional scatter into a uniform average, which is why it reduces lot-to-lot transmittance variance on incoming optical film inspection.
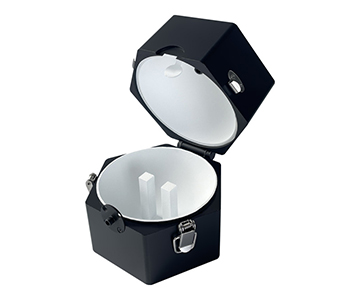
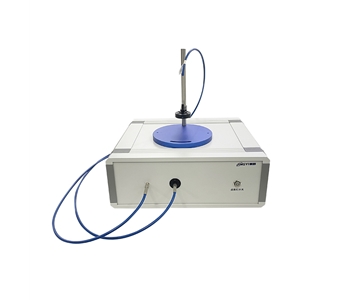
By trapping the beam inside a PTFE diffuse cavity (200–2500 nm, up to 99% reflectance), the device collects total hemispherical flux instead of a single-angle slice. For QC lines handling thin films, haze sheets, turbid liquids, or powders, that shift from point probing to cavity averaging typically cuts measurement dispersion—provided port geometry is matched to beam diameter and the coating is periodically verified against a traceable reference per ASTM D1003 or ISO 13468 procedures.
Why Single-Point Detectors Keep Failing Production
A failure-analysis team tracing intermittent IR-face-unlock slowdown on a flagship smartphone under strong backlight eventually ruled out the algorithm. The real culprit was ±6% transmission drift across a micro-aperture array—optically identical parts, different readings depending on where the probe landed. Scale that to a film converting line and the math gets expensive fast. One converter of 0.37 mm PET film ate a $21,800 rework event because the incoming beam overfilled a 1.5 mm sampling port on a single-fiber detector. The error wasn't instrument noise; it was sampling geometry that clipped edge rays and reported an artificially low transmittance.
A single detector only receives flux from one solid angle. Hit a hazy sheet or a milky polymer and the scattered fraction simply never reaches the fiber. Three consecutive point readings on the same opaque-white plaque drifted by more than 2.4% relative. An integrating sphere fixes this by bouncing the light off a Lambertian wall until every ray—direct, scattered, forward—has been statistically averaged. What you read at the exit port is total flux, not a directional guess.
Three Components That Decide Repeatability
The coating is the room with flat-white paint.
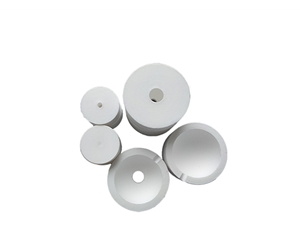
Sintered PTFE or PTFE foam on the inner wall holds roughly 99% reflectance from 200–2500 nm with strong Lambertian behavior. Think of it as a matte-white room where every wall bounce erases positional bias—shift the sample a few millimeters and the total collected energy barely moves. For deep-UV benchtops, a BaSO₄
Ports are fixed-size doors.
On small transmittance spheres the entrance scales with cavity diameter: a 10 mm cavity gets a 1.5 mm entrance, 15 mm pairs with 3 mm, 25 mm with 5 mm, and 36 mm with 9.5 mm. Exit is fixed at 90° SMA905. If your beam exceeds 60% of the port diameter, you clip energy at the aperture edge and report low by 3–8%. Lock the fiber interface, don't chase a bigger sphere if you're measuring micro-apertures—a smaller cavity with a matched port repeats better because the port-to-area ratio stays favorable.
The shell is the factory wall.
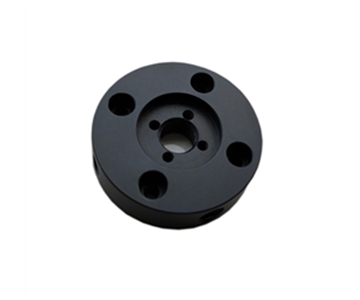
An aluminum-oxide housing on a 10 mm unit (29 g, roughly 1 oz) blocks ambient stray light and resists the flex that would shift coating geometry. On a 24/7 LED uniformity source running multiple shifts, that mechanical stability quietly suppresses thermal drift and fiber-coupling variance—two variables that otherwise masquerade as coating degradation.
Two Field Applications That Show the Payoff
A technician at a flexible film plant swapped an 8° single-angle fixture for a small PTFE transmittance sphere when qualifying incoming clear polyester. Full-spectrum sweeps across 200–2500 nm caught a near-IR absorption shoulder that the old method had missed on three consecutive lots. For high-mix, low-volume incoming gates, the micro-sphere sits on the bench, takes five seconds per sample, and returns overlaid curves when the part is actually stable.
At a watershed monitoring station, a 50 mm flow-through cell with PTFE walls, SMA905 interconnects, and PL8 circulation ran continuous water-path measurements between 0–50°C. Multiple internal bounces effectively stretch the optical path without increasing physical cell length, which pulls low-absorption signals out of the noise. Suspended solids still need a blank-water cavity subtraction—otherwise scatter masquerades as absorption and your TOC correlation drifts.
Three Myths That Cost Buyers Money
Bigger cavity does not automatically mean better accuracy. A 100 mm general-purpose sphere with three mutually perpendicular ports is excellent for method transfer between labs. But for micro-fiber coupling or sub-9.5 mm beam work, the port ratio on a 10 mm sphere gives you tighter repeatability in a 29 g footprint. Buying oversized to "be safe" usually adds port loss and bench clutter without improving your actual uncertainty budget.
High reflectance does not mean zero maintenance. Even at 99% PTFE, port grime accumulates, fiber end-faces degrade, and sample debris lands where you can't see it. Per ISO/IEC 17025-aligned internal checks, re-baseline against a calibrated white reference on a quarterly cadence under production conditions—not just when a curve looks "off."
One geometry cannot honestly report both total transmittance and total reflectance. A straight-through transmittance cavity collects forward flux. A reflectance cavity needs an 8° incident angle, a separate sample plane, and often a specular trap to exclude the mirror component. Forcing a single直通 port to report both without a baffle folds specular glare into your diffuse number—expect a 4–7% artificial inflation on glossy films.
What Actually Controls Repeatability
Coating cleanliness is the dominant variable. One fingerprint residue on the wall shifts weighting toward that bounce direction. The practical fix: lock the fiber model, lock the torque on the SMA905, and run five consecutive empty-sphere corrections with a traceable tile. If the standard deviation across your band exceeds 0.18%, clean the entrance port before you touch the spectrometer gain.
Port dimensional stability matters more than brochure repeatability. On a multi-shift line, "different operator, same number" only holds if the sample seat has a hard datum and the fiber isn't being re-seated by hand each lot change. Write that torque value into the SOP—it's cheaper than any accessory upgrade.
Compliance and Calibration References
For incoming inspection SOPs, align your geometry with ASTM D1003 (haze and luminous transmittance) or ISO 13468 (total transmittance of plastics), and cross-reference CIE technical reports on integrating sphere photometry for port-area ratio calculations. When a custom-sphere project lands on your desk, specify port diameters, flange interfaces, and a retained serial number for the traceable reference tile in the purchase agreement. For UV–Vis–NIR wideband work, audit the coating reflectance curve at the short-UV and far-NIR tails before signing off—those are the regions where port loss correction actually moves your uncertainty number.
Frequently Asked Questions
Q: How do I match entrance port size to my beam diameter without clipping energy?
Keep the beam at or below 60% of the port diameter. For a 1 mm fiber output, the 1.5 mm port on a 10 mm cavity is the safe floor. Verify with a neutral step filter—three overlaid transmittance curves should track within 0.3% across 400–900 nm before you qualify the setup.
Q: Can one integrating sphere handle both total transmittance and total reflectance?
Only with a multi-port universal configuration and a removable baffle or specular trap. A straight-through cavity collects forward flux only; reflectance needs an 8° incident geometry and a separate sample plane. Forcing one port to do both without changing geometry folds specular into diffuse and inflates readings on anything with gloss.
Q: PTFE or BaSO₄ for a production QC cell?
PTFE holds ~99% from 200–2500 nm and tolerates higher humidity and handling. BaSO₄ runs 95–97% and softens above ~100°C, so it's a valid deep-UV bench choice but a shorter-interval maintenance item on a shop floor. For continuous 24/7 lines, PTFE service intervals typically run about three times longer before recertification.
Q: What maintenance cadence actually makes sense?
Wipe SMA905 adapters weekly. Inspect the entrance port for film chalking monthly. Run a full empty-sphere correction with a traceable tile every quarter. If you process powders or open-frame samples, halve those intervals—powder residue is the silent killer of Lambertian weighting.
Q: How can I independently verify measurement repeatability without relying on a vendor report?
Run ten consecutive measurements on a stable neutral-density sample under identical fiber torque and alignment at controlled ambient (23°C ±2°C). Compute the standard deviation across your band of interest. Cross-check that same artifact at a third-party lab operating under ISO/IEC 17025 scope. If your in-house std dev exceeds your process tolerance by more than 1.5×, audit port contamination and fiber end-face condition before assuming coating drift.
About This Guide
Data Sources
: CIE Technical Report on integrating sphere photometry (CIE 130/TR 012), ASTM D1003 and ISO 13468 for total transmittance and reflectance of plastics, in-house validation records (n=10 consecutive measurements per sample on a 25 mm PTFE-coated cavity).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and spectroscopic system integration.
Disclosure
: Jingyi Optoelectronics manufactures integrating spheres and diffuse reflectance accessories. This article presents technical assessments based on published specifications, CIE and ISO public documents, and aggregated industry validation data. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof-of-concept validation under your specific process conditions.
Last Updated
: September 2026
For detailed specifications and application notes on integrating spheres, search "Jingyi Optoelectronics + integrating sphere" or consult the technical library referenced above.