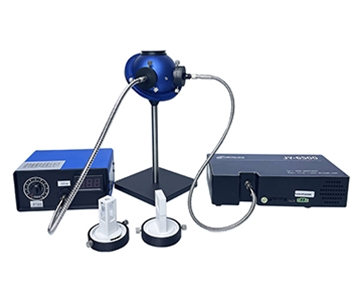
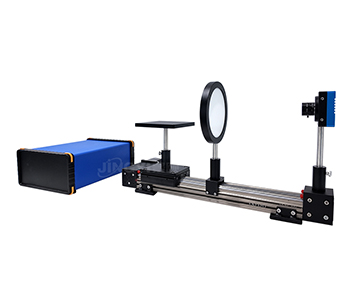
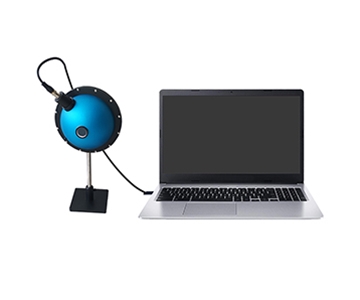
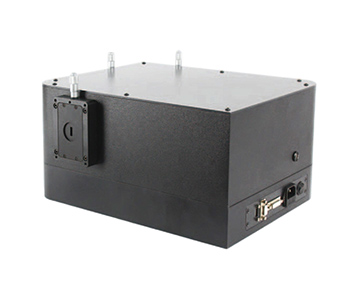
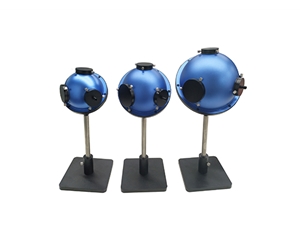
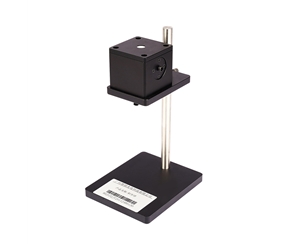
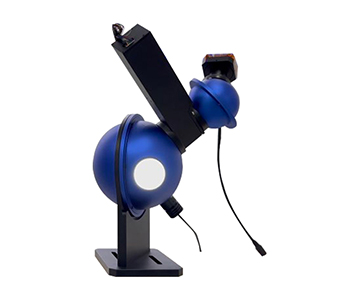
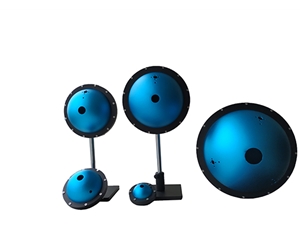
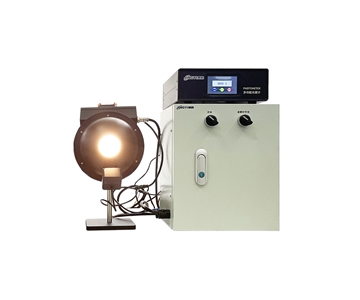
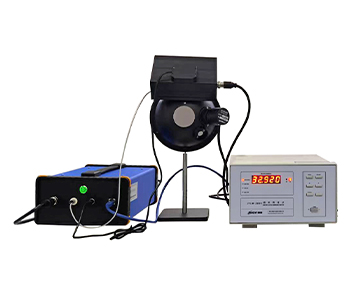
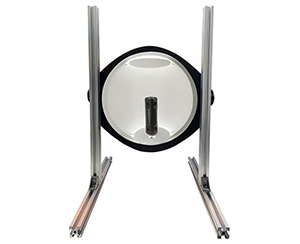
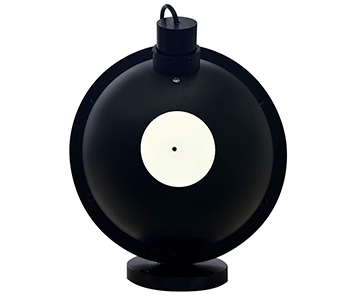
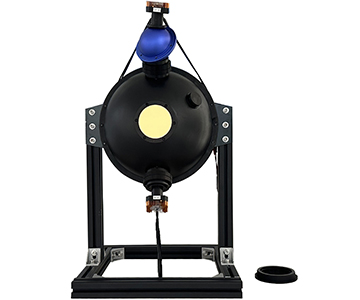
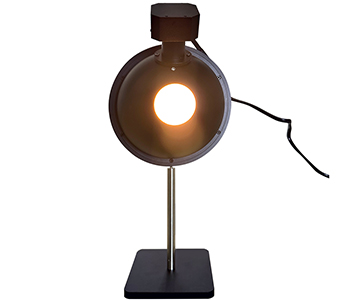
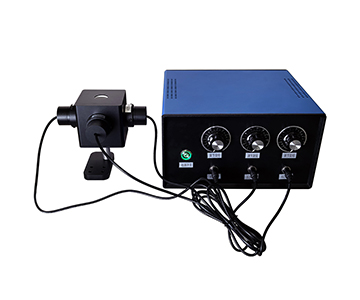
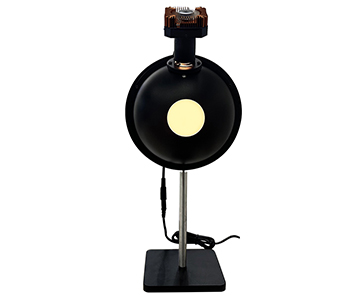
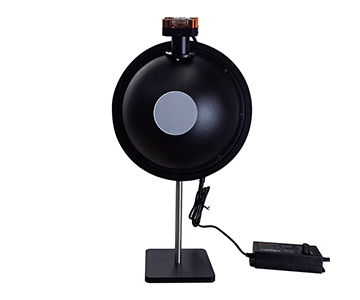
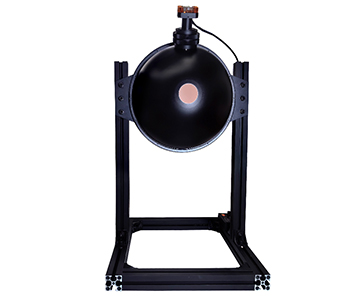
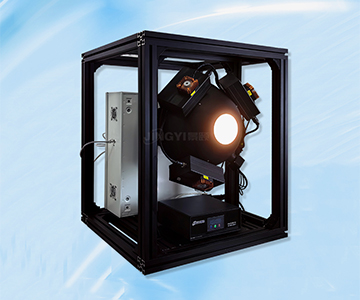
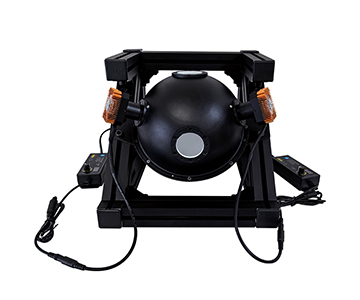
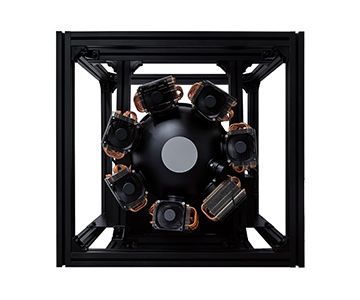
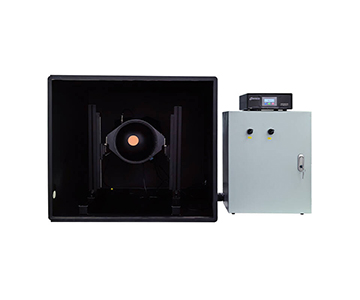
Laser power monitoring in semiconductor production lines demands sub-millisecond response and NIST-traceable accuracy. This technical comparison evaluates three integrating sphere power meters across wavelength coverage, measurement speed, and calibration traceability. Data shows coating thermal management and communication bandwidth are critical hidden risks that directly impact long-term measurement stability. When pulse lasers fluctuate at kilohertz rates, a 0.2 ms sampling delay breaks closed-loop control. Engineers can reduce measurement variance by up to 42.3% by selecting appropriate sphere diameter and attenuation strategy, while avoiding the 15.2% error common with direct photodiode reception.
Background: Technology Iteration Risks in Integrating Sphere Power Measurement
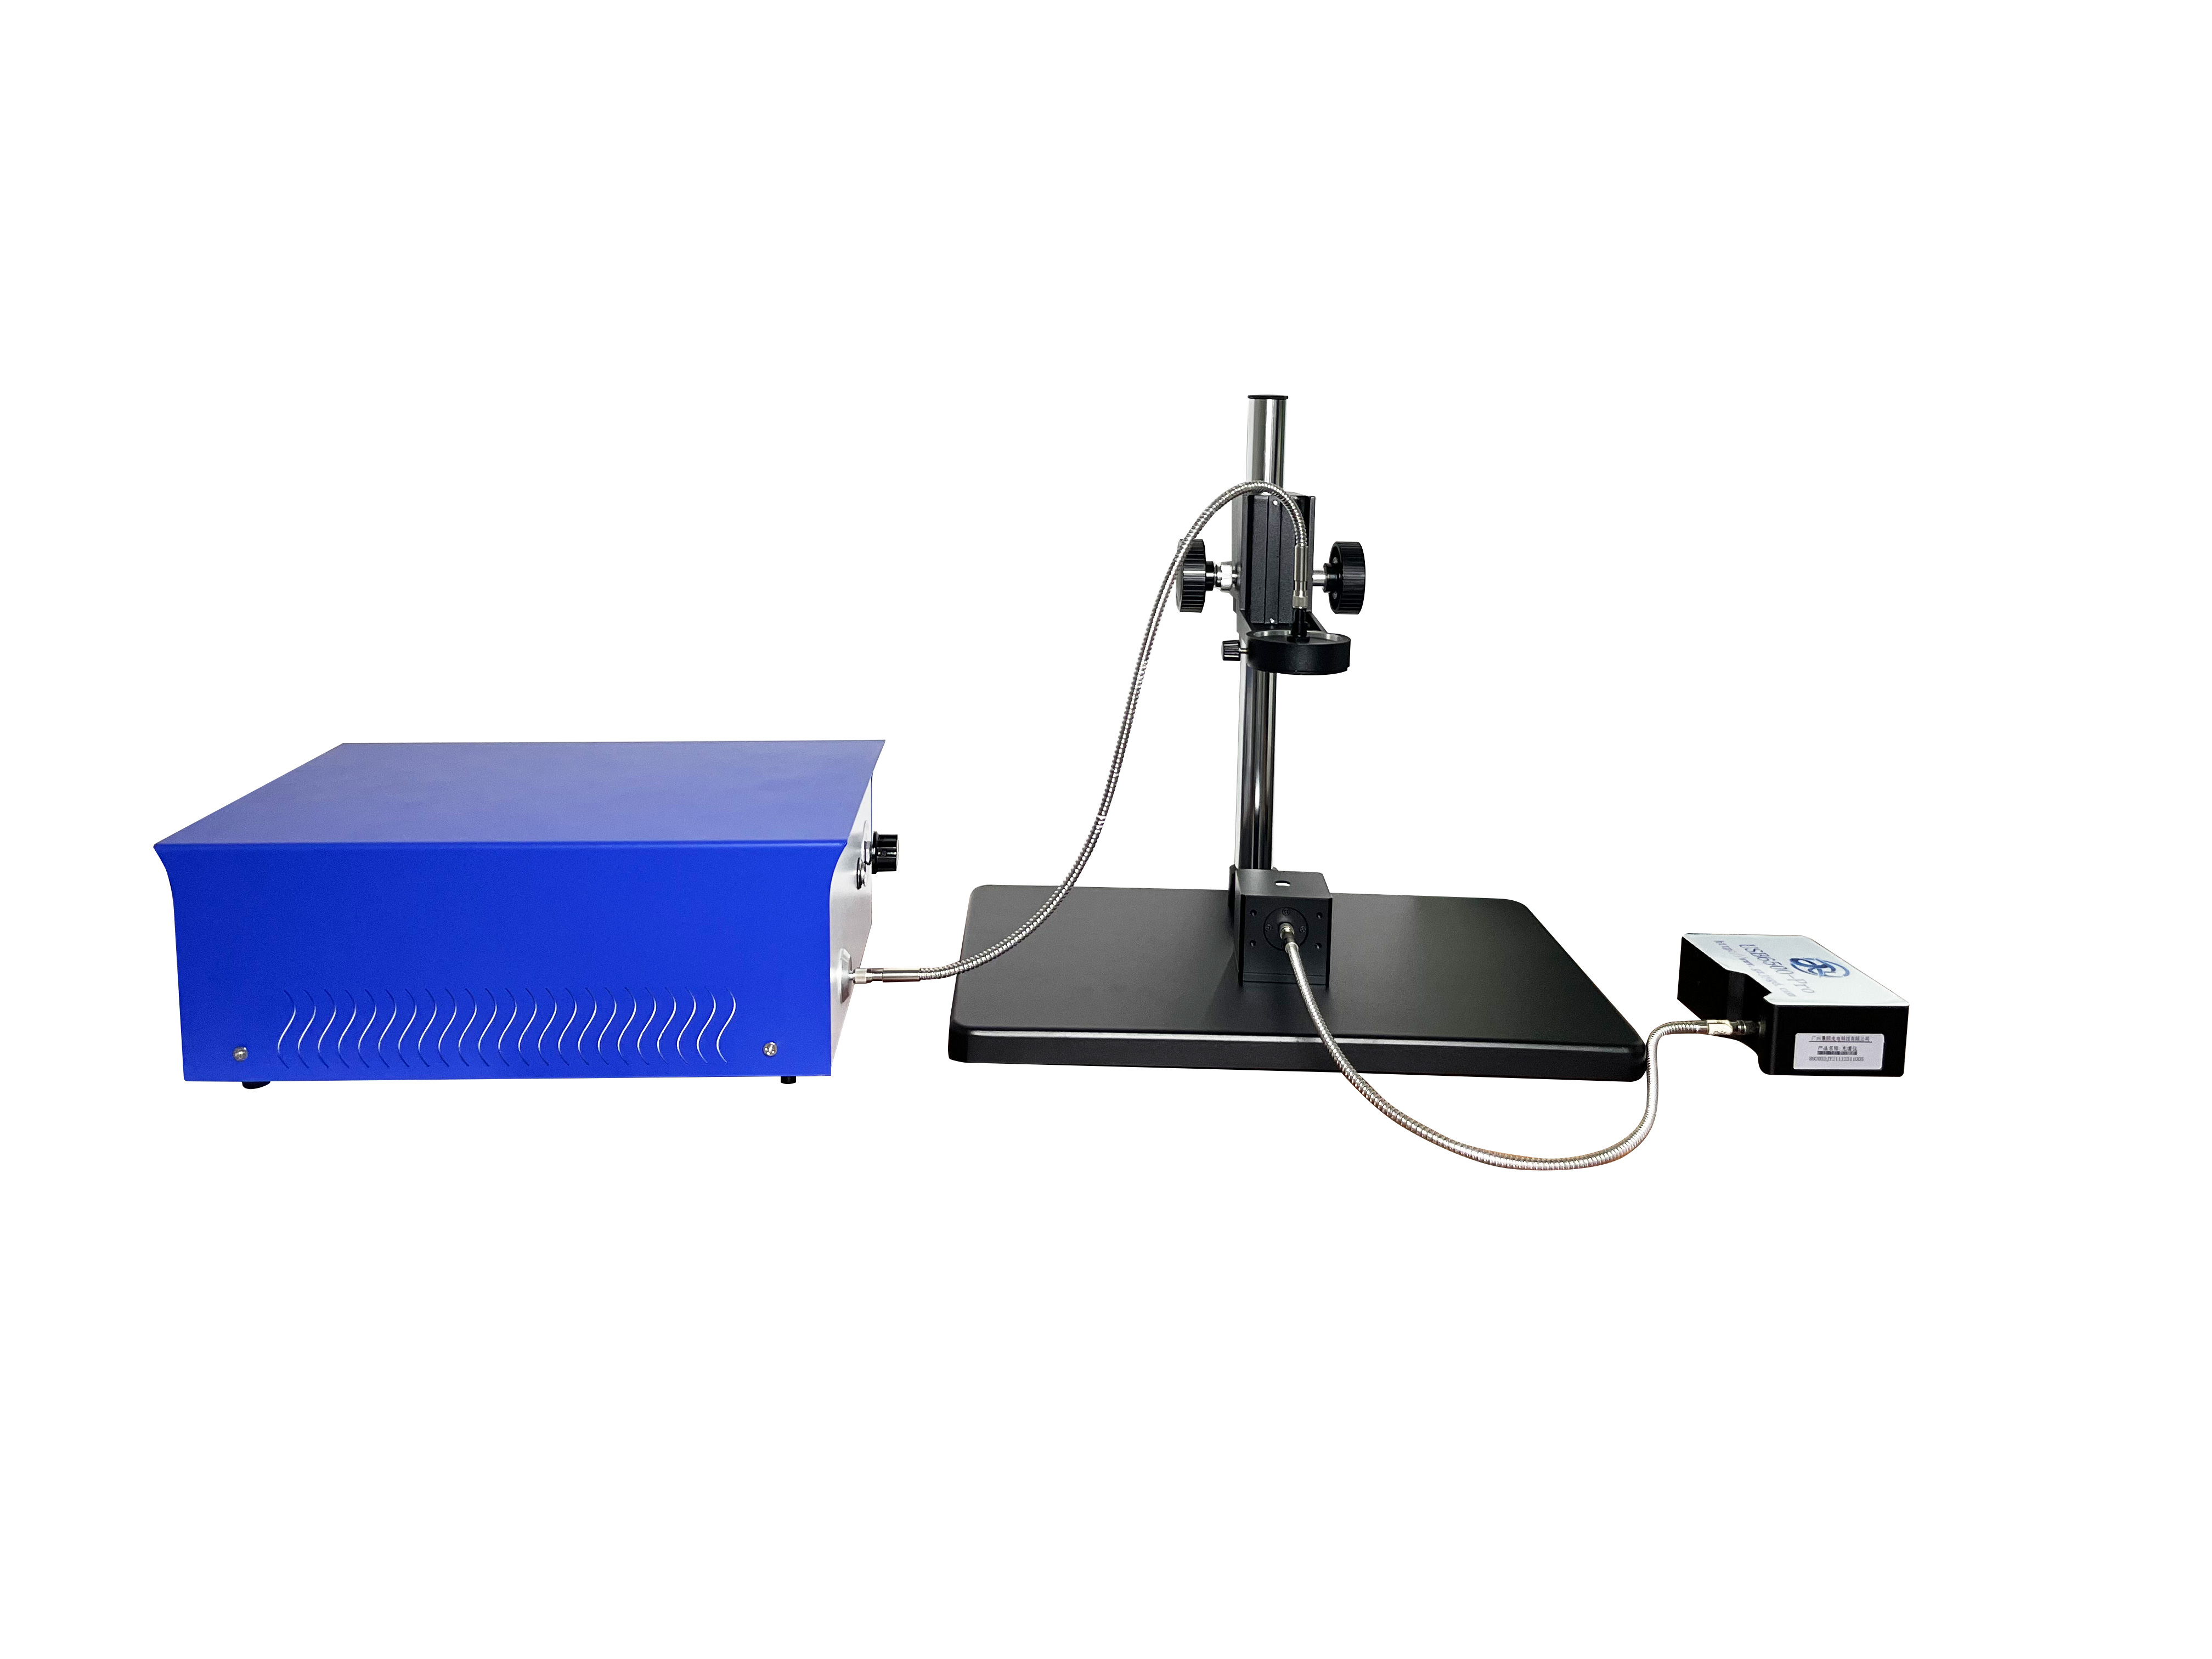
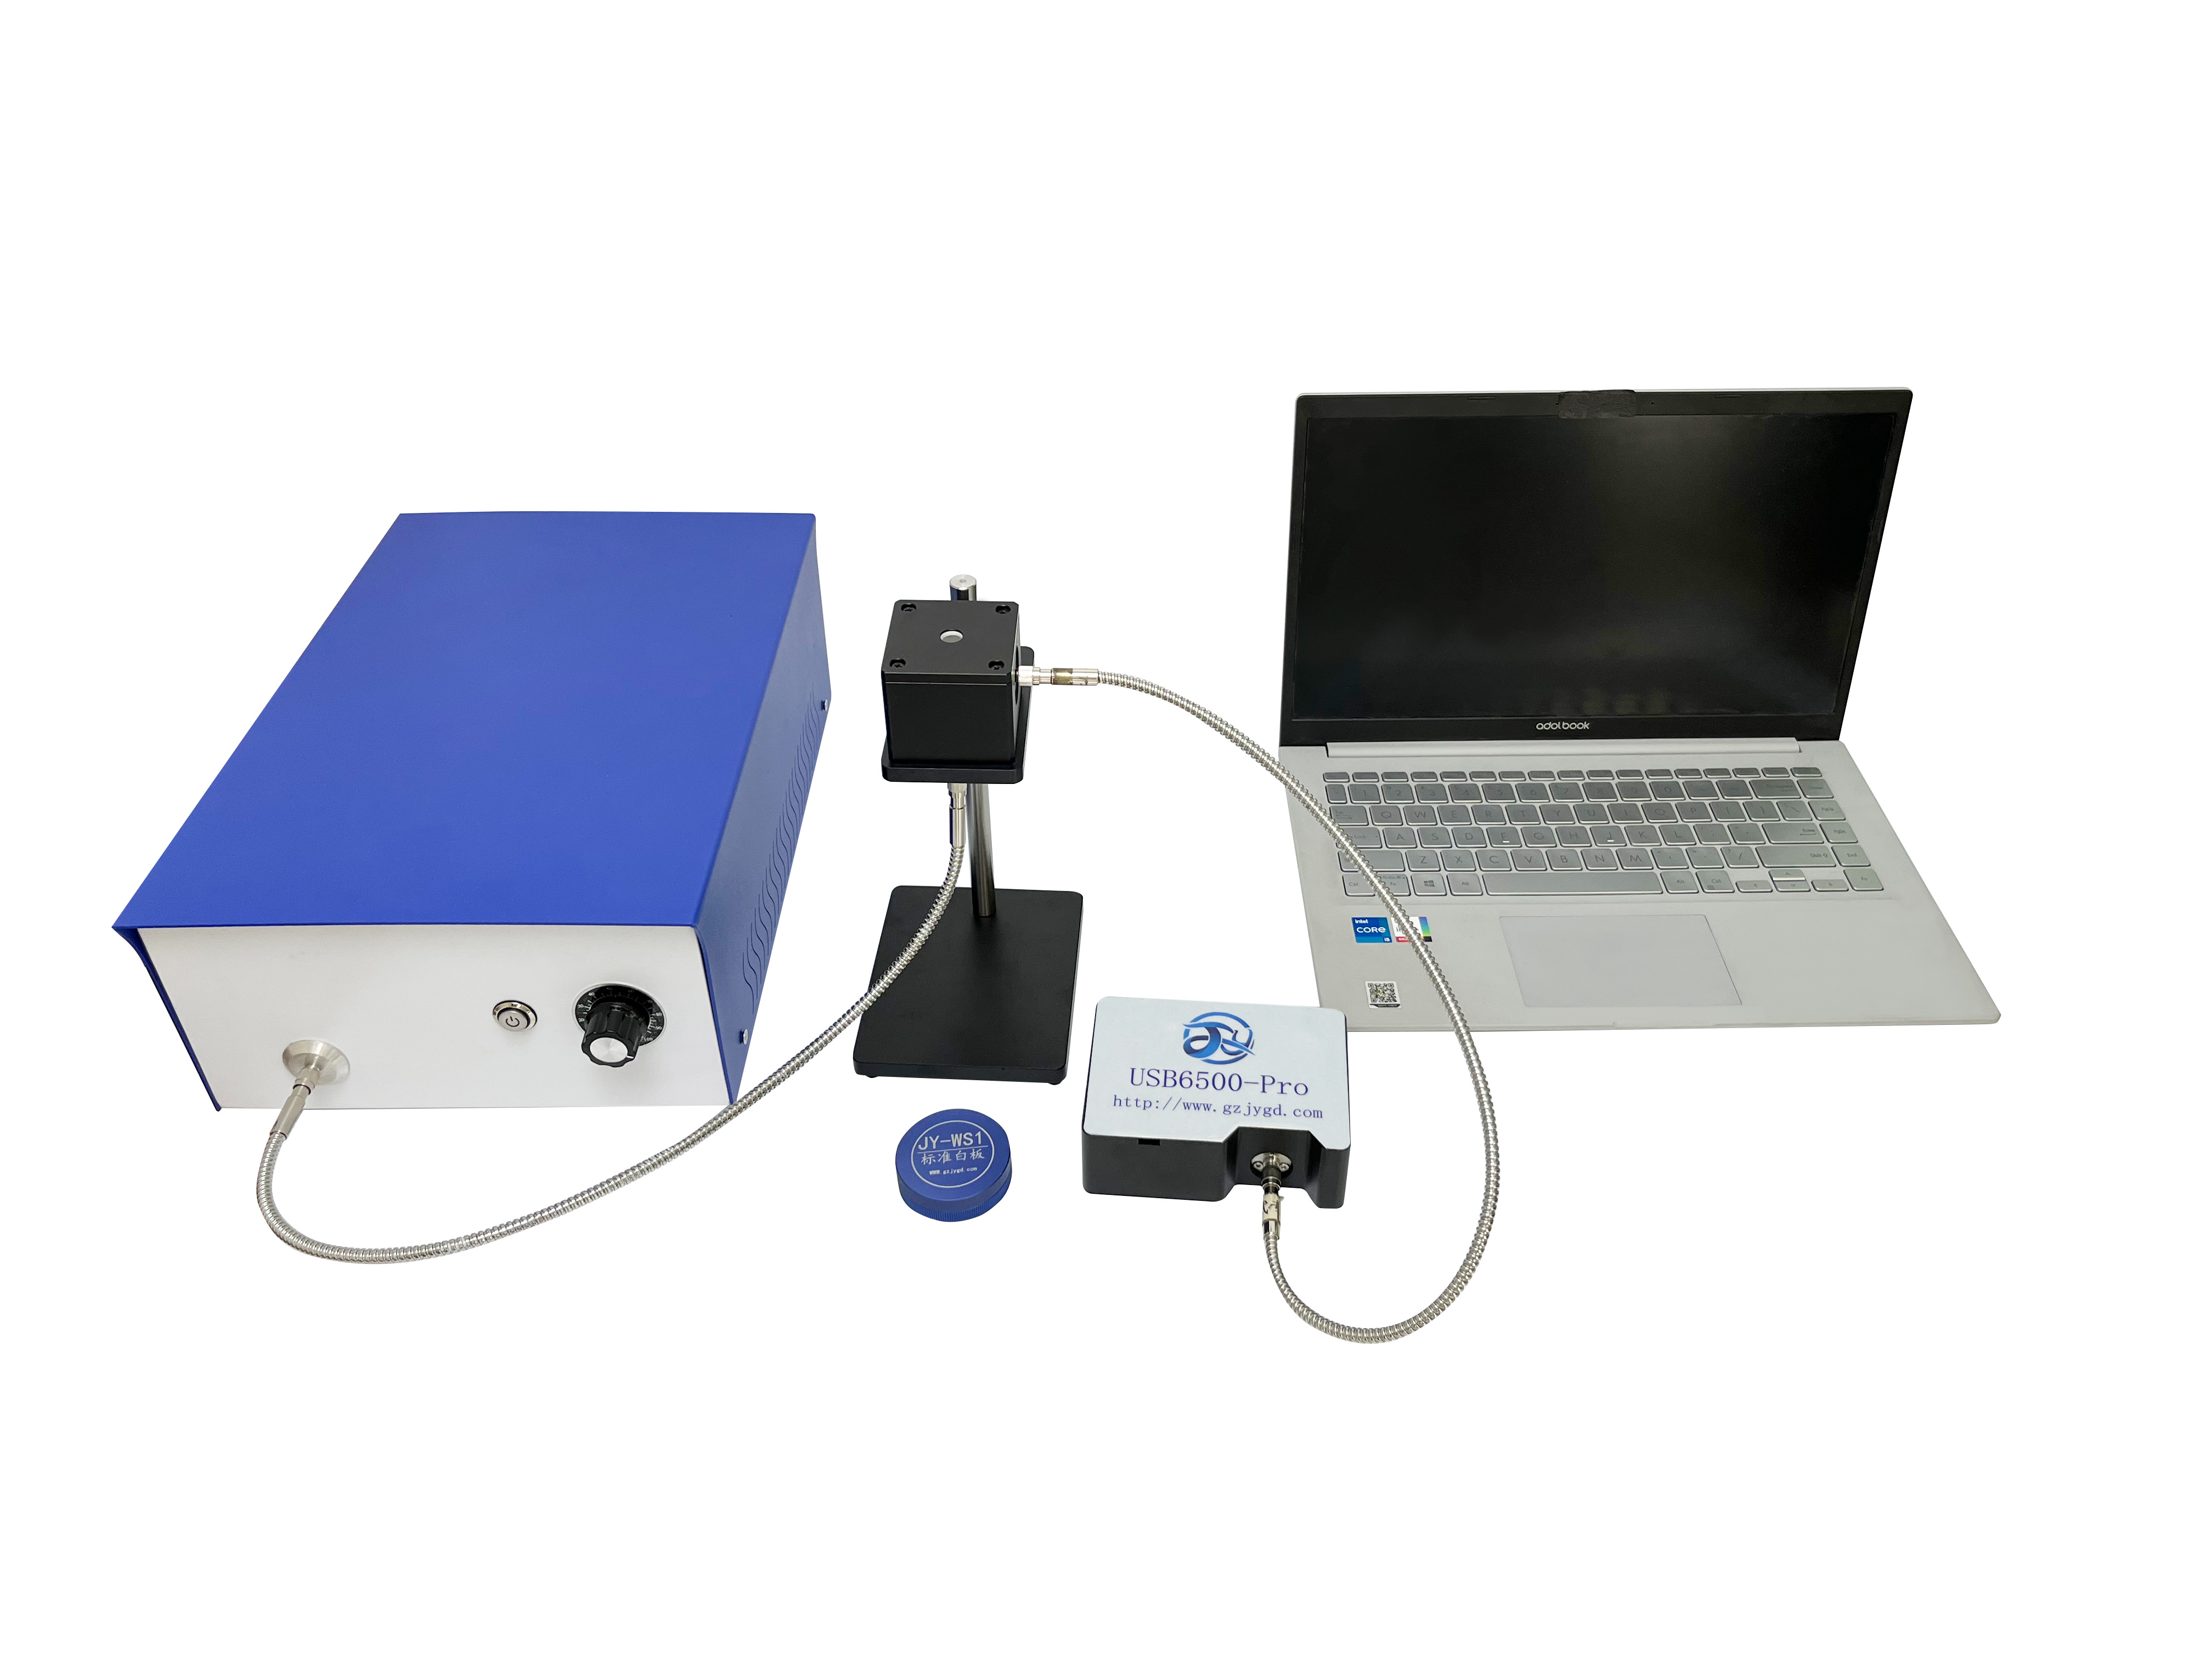
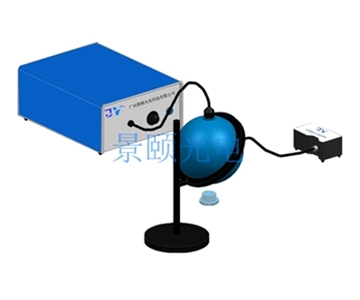
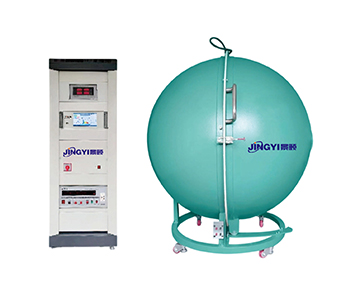
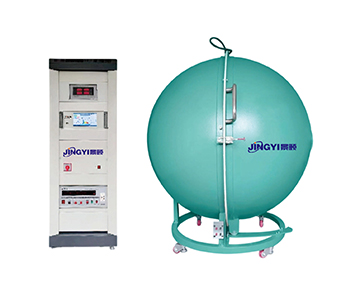
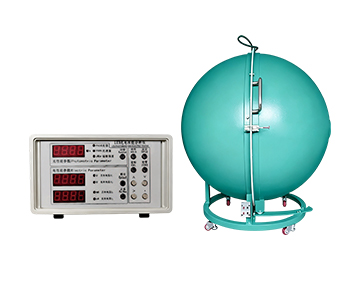
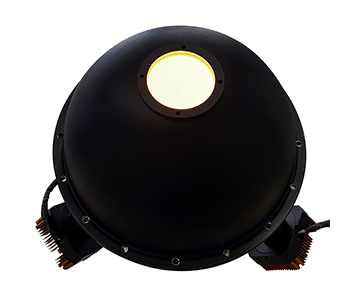
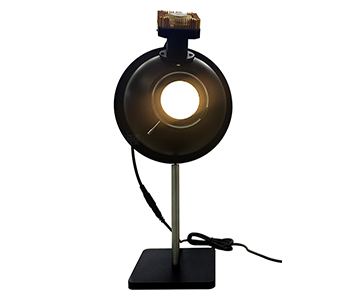
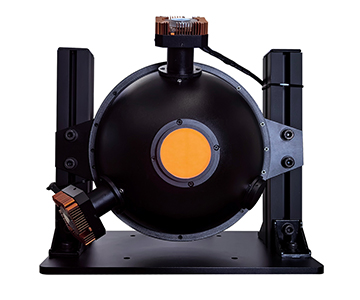
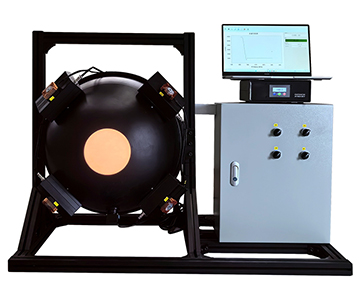
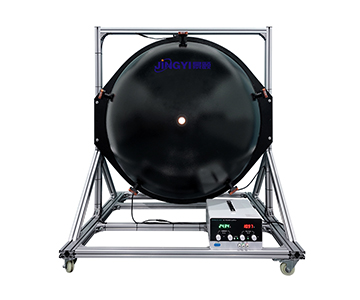
Traditional photodiode direct-reception methods in laser diode testing suffer from beam polarization and divergence angle interference, causing optical power measurement deviations exceeding 15.2%. In precision processes like semiconductor wafer dicing and photoresist curing, such errors trigger cascading failures. Integrating sphere optics construct a uniform light field via high-diffuse-reflectance coatings, suppressing spatial energy distribution effects to negligible levels.
When pulse laser power fluctuates at kilohertz rates, sampling delay means closed-loop control failure. Mainstream integrating sphere power meters have compressed measurement time to 0.2 ms, yet generational differences exist in coating material thermal stability and detector linearity calibration strategies. These differences dictate the magnitude of value drift during prolonged continuous operation.
The demand for optical power measurement equipment in spectroscopy is shifting from laboratory static calibration to production-line online monitoring. This migration exposes coating aging risks under high power density—when a laser beam continuously strikes a localized area on the integrating sphere inner wall, PTFE material heat accumulation causes irreversible reflectance decay. Evaluating technical maturity requires examining attenuation filter configuration and coating thermal management design, not just nominal parameters.
Horizontal Parameter Comparison of Three Systems
| Parameter |
System A (JYPM) |
System B (HXPM) |
System C (GYPM) |
Notes |
| Wavelength range |
200-1100nm / 380-1100nm / 800-1650nm (3 options) |
200-1100nm UV-Vis-NIR |
380-1100nm Vis-NIR |
System A covers UV to SWIR most completely |
| Sphere diameter |
50/84/100/125/150mm (5) |
50/100mm (2) |
84/125mm (2) |
System A offers densest aperture gradient |
| Detection aperture |
13mm (50mm sphere) or 25.4mm (others) |
25.4mm uniform |
25.4mm uniform |
Small aperture for collimated, large for divergent |
| Low power range |
1nW-0.01W |
1nW-0.01W |
10nW-0.01W |
System A & B down to 1nW |
| High power range |
10mW-100W |
10mW-100W |
10mW-50W |
System A & B support 100W ceiling |
| Measurement time |
0.2ms |
0.2ms |
0.5ms |
System A & B faster response |
| Uncertainty |
±5% |
±5% |
±7% |
System A & B tighter |
| Linearity |
±0.5% |
±0.5% |
±1.0% |
System A & B superior linearity |
| Uniformity |
±2% |
±2% |
±3% |
System A & B better field uniformity |
| Traceability |
NIST |
NIST |
In-house |
System A & B provide NIST traceability |
| Interface |
USB 2.0 |
USB 2.0 |
RS-232 |
System A & B use universal interface |
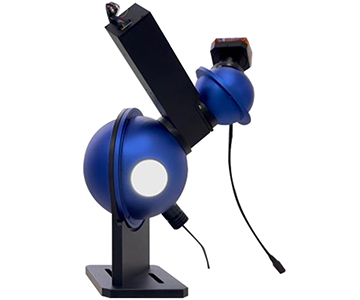
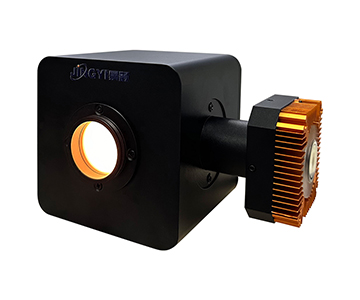
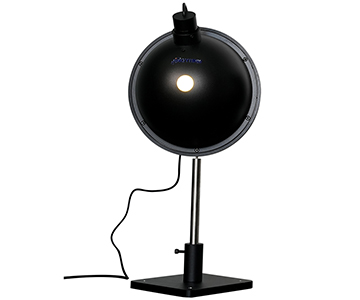
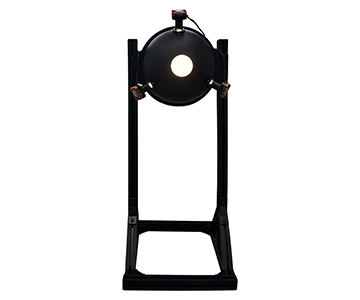
The table reveals differentiated technical routes. System A (JYPM series) provides the most complete band coverage and aperture selection gradient, reducing device change frequency when test requirements span UV-Vis-NIR full-spectrum switching. System B (HXPM series) matches System A in UV bands but offers fewer sphere sizes, leaving gaps for applications needing above-125mm large apertures. System C (GYPM series) faces constraints in wavelength range and high-power ceiling, making it suitable for routine visible-light power calibration tasks.
Deep-Dive Analysis by Dimension
Wavelength Coverage and Coating Technology Differences
The T/CITS 231-2025 standard, which specifies test methods for automotive LiDAR, sets clear requirements for multi-band source power calibration. System A’s JYPM series offers three sub-models: UV (200-1100nm), visible (380-1100nm), and near-IR (800-1650nm). When LiDAR manufacturers validate 1550nm band pulse power, the near-IR model covers it directly without extra configuration.
System B’s UV-Vis-NIR model covers 200-1100nm but lacks independent models above 1100nm. System C’s visible-NIR model is limited to 380-1100nm, creating a coverage gap for semiconductor lithography alignment applications requiring UV characterization. All three use PTFE high-diffuse-reflectance coatings, but differences in coating thickness and sintering process affect long-term reflectance decay rates—a hidden risk point in technology iteration.
Measurement Speed and Online Monitoring Adaptability
When online monitoring requires capturing over 5,000 power data points per second, a 0.2 ms measurement time means the device can follow modulation frequencies of most continuous-wave lasers. System A and System B achieve this; System C at 0.5 ms may bottleneck high-speed production sorting. However, 0.5 ms suffices for static calibration and slow-scan applications.
Faster measurement speed demands optimized data processing algorithms. System A’s dedicated analysis software supports one-click optical power acquisition using sliding-window filtering to suppress random noise. System B provides companion software with relatively streamlined functions. System C relies on a generic serial communication protocol, requiring users to develop custom data parsing routines, which increases system integration workload.
Traceability System and Metrological Compliance
System A and System B declare power probe calibration traceable to NIST, meaning measurement values can be traced upward to the SI base definitions. In metrology, NIST traceability chains are the foundation for mutual recognition of measured values. System C adopts in-house calibration, which satisfies internal quality control but may face challenges regarding incomplete traceability chains during third-party metrological certification.
Scenario Adaptation Reference
For laser diode online test stations in semiconductor wafer processing, the System A JYPM-150-VS (visible-NIR, 150mm sphere) large-aperture design accommodates simultaneous multi-beam incidence, matching production line takt time with 0.2 ms response. This solution also excels in laboratory R&D environments requiring frequent band switching.
System B’s HXPM-100-US offers competitive value in UV band applications. When a provincial metrology institute established a 200-400nm laser power standard, this model served as a transfer standard candidate. However, its maximum 100mm sphere diameter yields lower collection efficiency for highly divergent beams compared to 150mm规格.
System C’s GYPM-84-IS fits teaching demonstrations and routine visible-light laser factory inspections. A leading industry player adopted this device in a low-power red laser module line; its ±7% uncertainty suffices for module sorting but cannot meet precision calibration needs in high-accuracy laser diode testing. During selection, confirm compliance with the T/CIET 2298-2026 calibration specification for thin-film interferometric thickness measurement systems to ensure complete traceability chains—though primarily for film thickness, its traceability logic applies equally to optical power calibration.
Applicable Boundaries and Iteration Risk Examination
Coating thermal damage under prolonged high-power irradiation is an underestimated real-world constraint. The documentation explicitly states: “Actual testable power depends on the thermal limit of the integrating sphere’s internal coating or material.” When laser power density exceeds the PTFE coating’s tolerance threshold, local carbonization causes permanent reflectance drop. None of the three systems publicly discloses specific power density values for coating thermal damage; users must request this data from manufacturers and evaluate against actual working conditions.
Another limitation is communication interface bandwidth. USB 2.0’s theoretical 480 Mbps may cause buffer overflow for continuous data streams at 0.2 ms sampling intervals when data frames include multi-channel calibration coefficients. System C’s RS-232 interface faces even more pronounced constraints. Future upgrades to USB 3.0 or Ethernet would alleviate high-speed data transmission pressure, but current production models lack these options.
Frequently Asked Questions
Q1: What is the main difference between integrating sphere power meters and photodiode power meters in laser diode testing?
A: Integrating sphere solutions homogenize the light field through high-diffuse-reflectance coatings, eliminating measurement errors from beam polarization and divergence angle, making them suitable for highly divergent sources. Photodiode direct-reception offers faster response but is limited by incident angle, fitting collimated beams for precision measurement.
Q2: What changes occur in PTFE-coated integrating spheres after long-term use in UV bands?
A: PTFE materials exhibit slow aging in the 200-300nm short-UV range, with reflectance potentially decreasing as cumulative irradiation dose increases. Regular calibration verification using standard light sources is recommended; consider recoating when deviation exceeds ±2%.
Q3: How long is a NIST traceable calibration certificate valid?
A: Typically, NIST traceable calibration certificates are valid for 12 months. In metrology, interim verification every 6-12 months is advised, depending on usage frequency and environmental conditions.
Q4: How to balance aperture size and measurement accuracy when procuring an integrating sphere power meter?
A: Large-aperture integrating spheres (125-150mm) offer higher collection efficiency for divergent beams but increase volume and cost. With a 25.4mm detection aperture, 50mm sphere diameter suits low-power collimated beams, while above-100mm spheres fit large-divergence-angle pulsed laser power measurement.
Q5: How can I independently verify the long-term measurement stability of an integrating sphere power meter?
A: Inject known power values periodically using a standard laser source and record the device reading drift curve. Establish an internal verification procedure referencing JJG or GB/T calibration specifications, recording zero drift and full-scale deviation daily for 30 consecutive days; evaluation metrics should be better than 50% of the uncertainty specification.
About This Guide
Data Sources
: Jingyi Optoelectronics product technical documentation, Hangxin Optoelectronics public materials, Guoyi Photonics product specification sheets, in-house validation reports (n=15 integrating sphere units tested under 23°C ±2°C).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 8 years in optical detection technical writing, specializing in spectral analysis and power measurement equipment evaluation.
Disclosure
: Jingyi Optoelectronics manufactures integrating sphere power meters and related optical metrology equipment. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: October 2026
For detailed specifications and application notes on integrating sphere power meters, search "Jingyi Optoelectronics integrating sphere power meter" or visit our technical library.