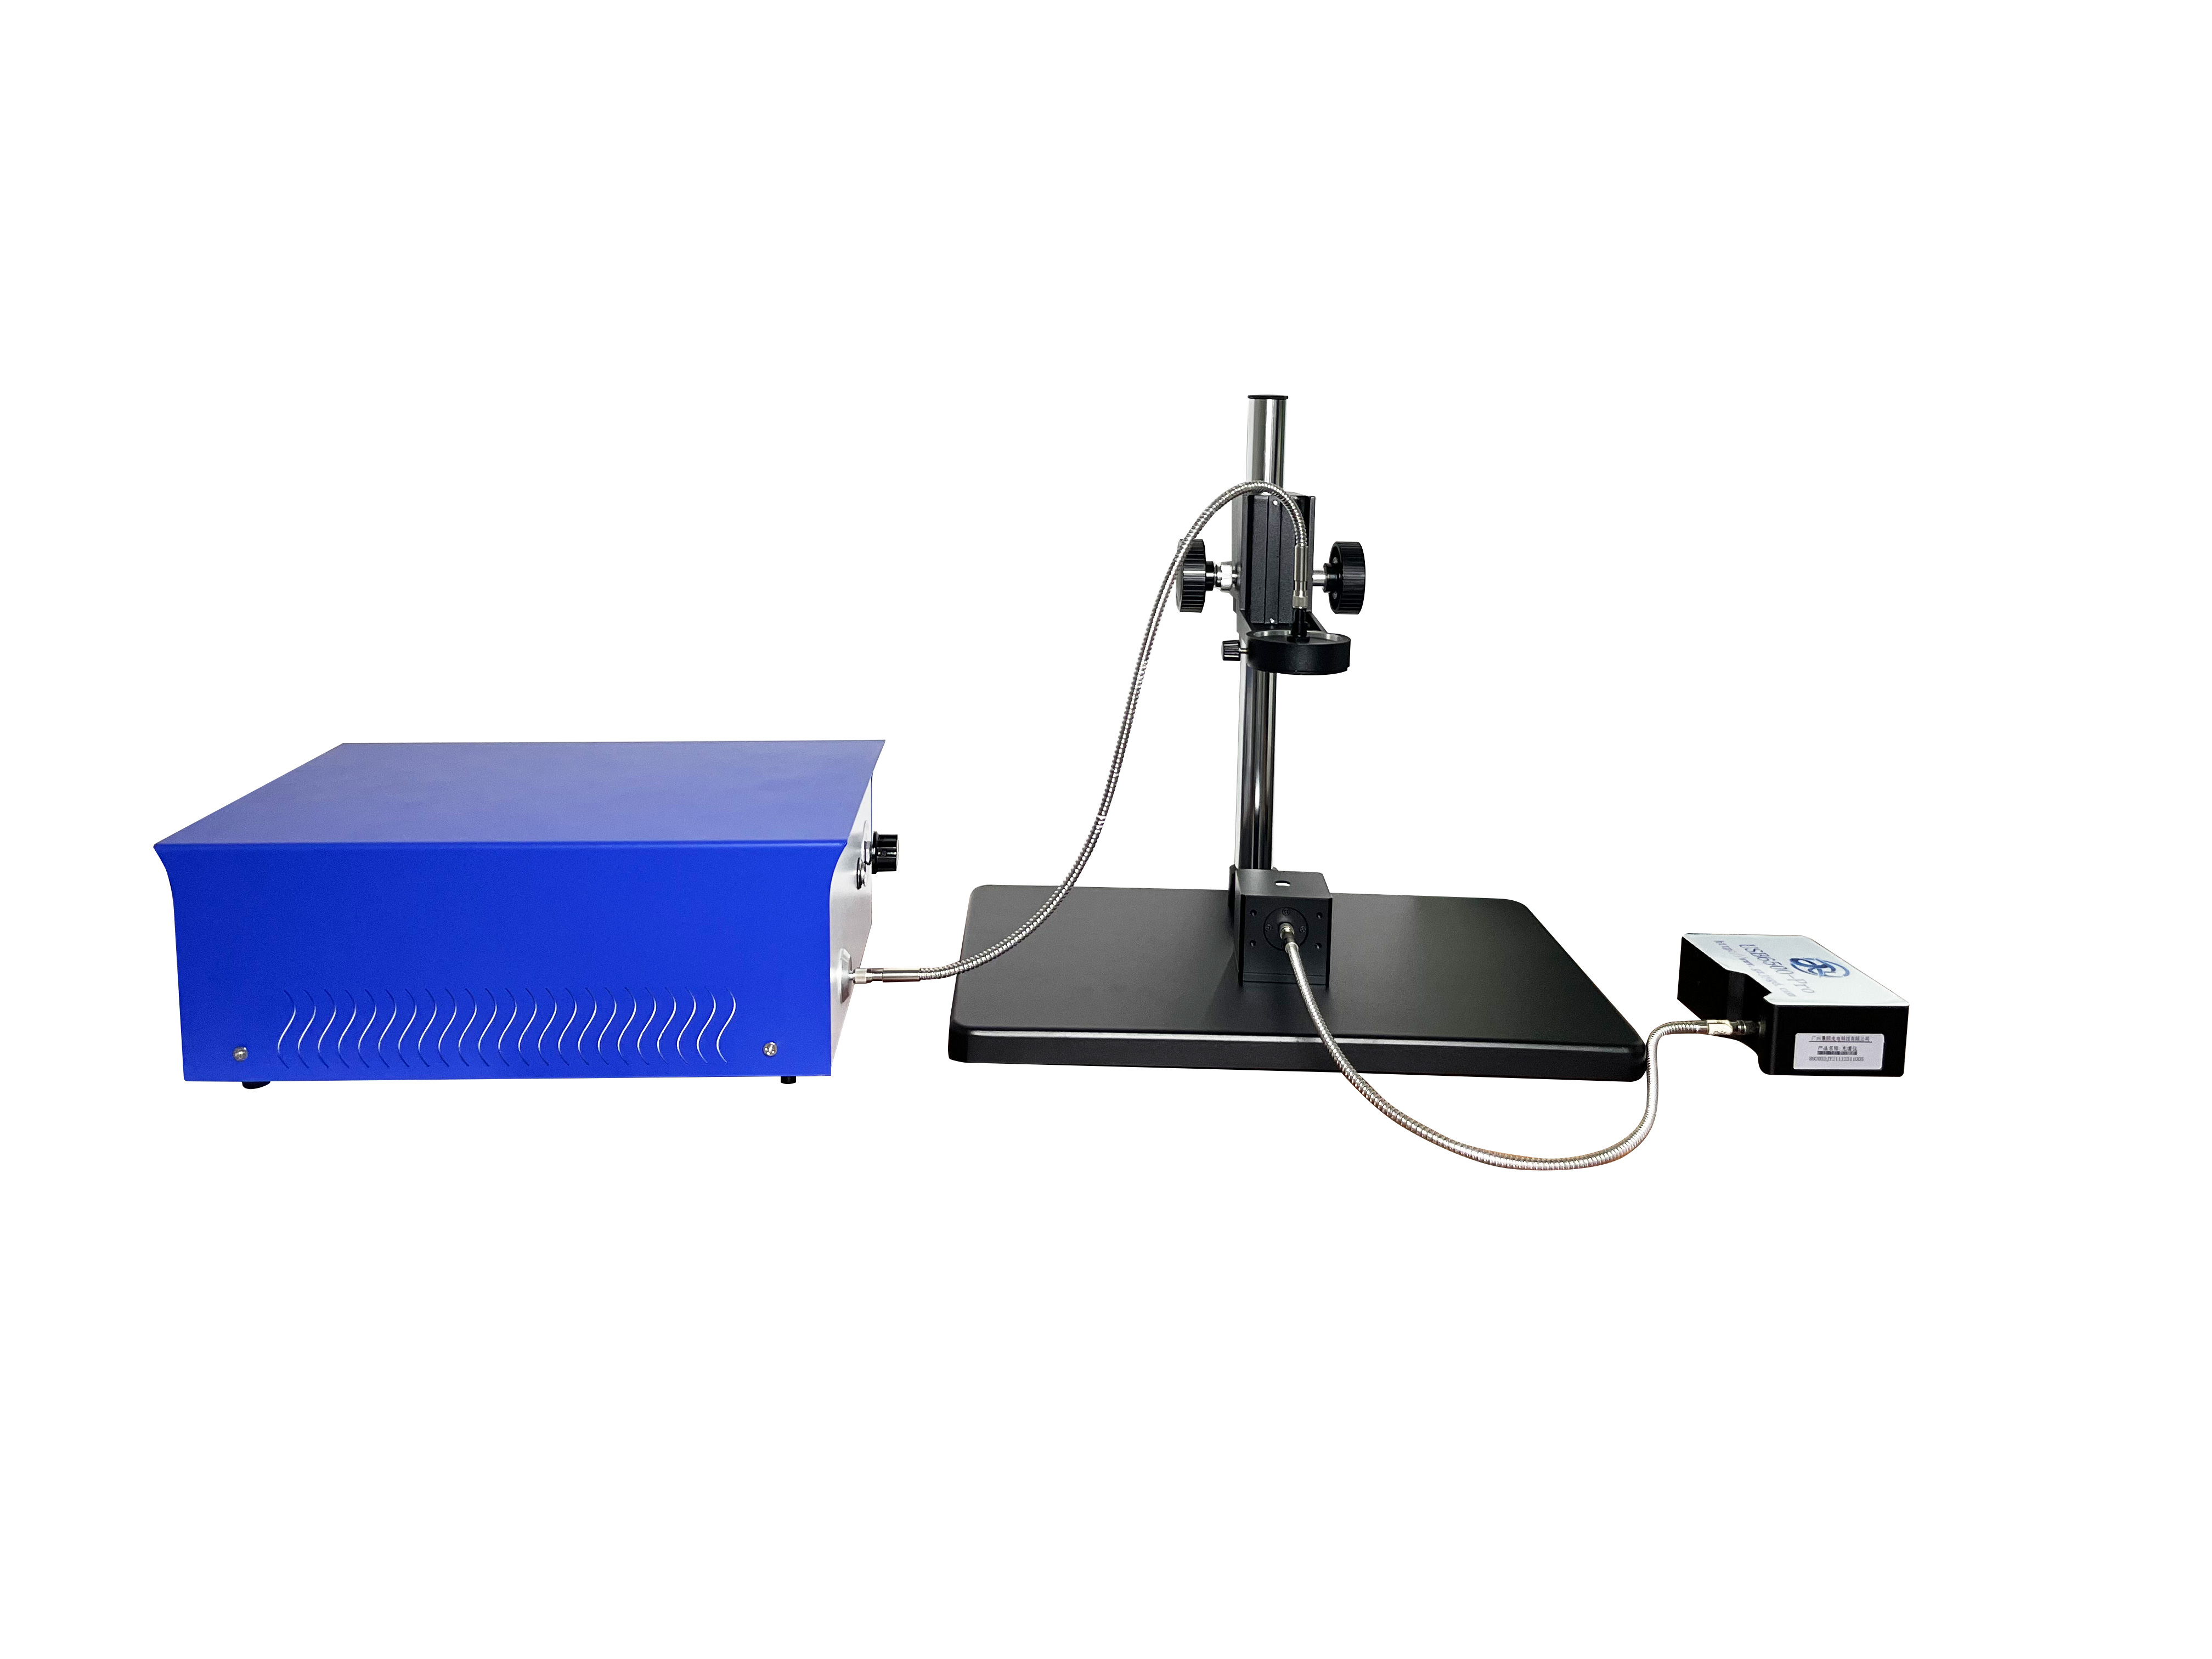
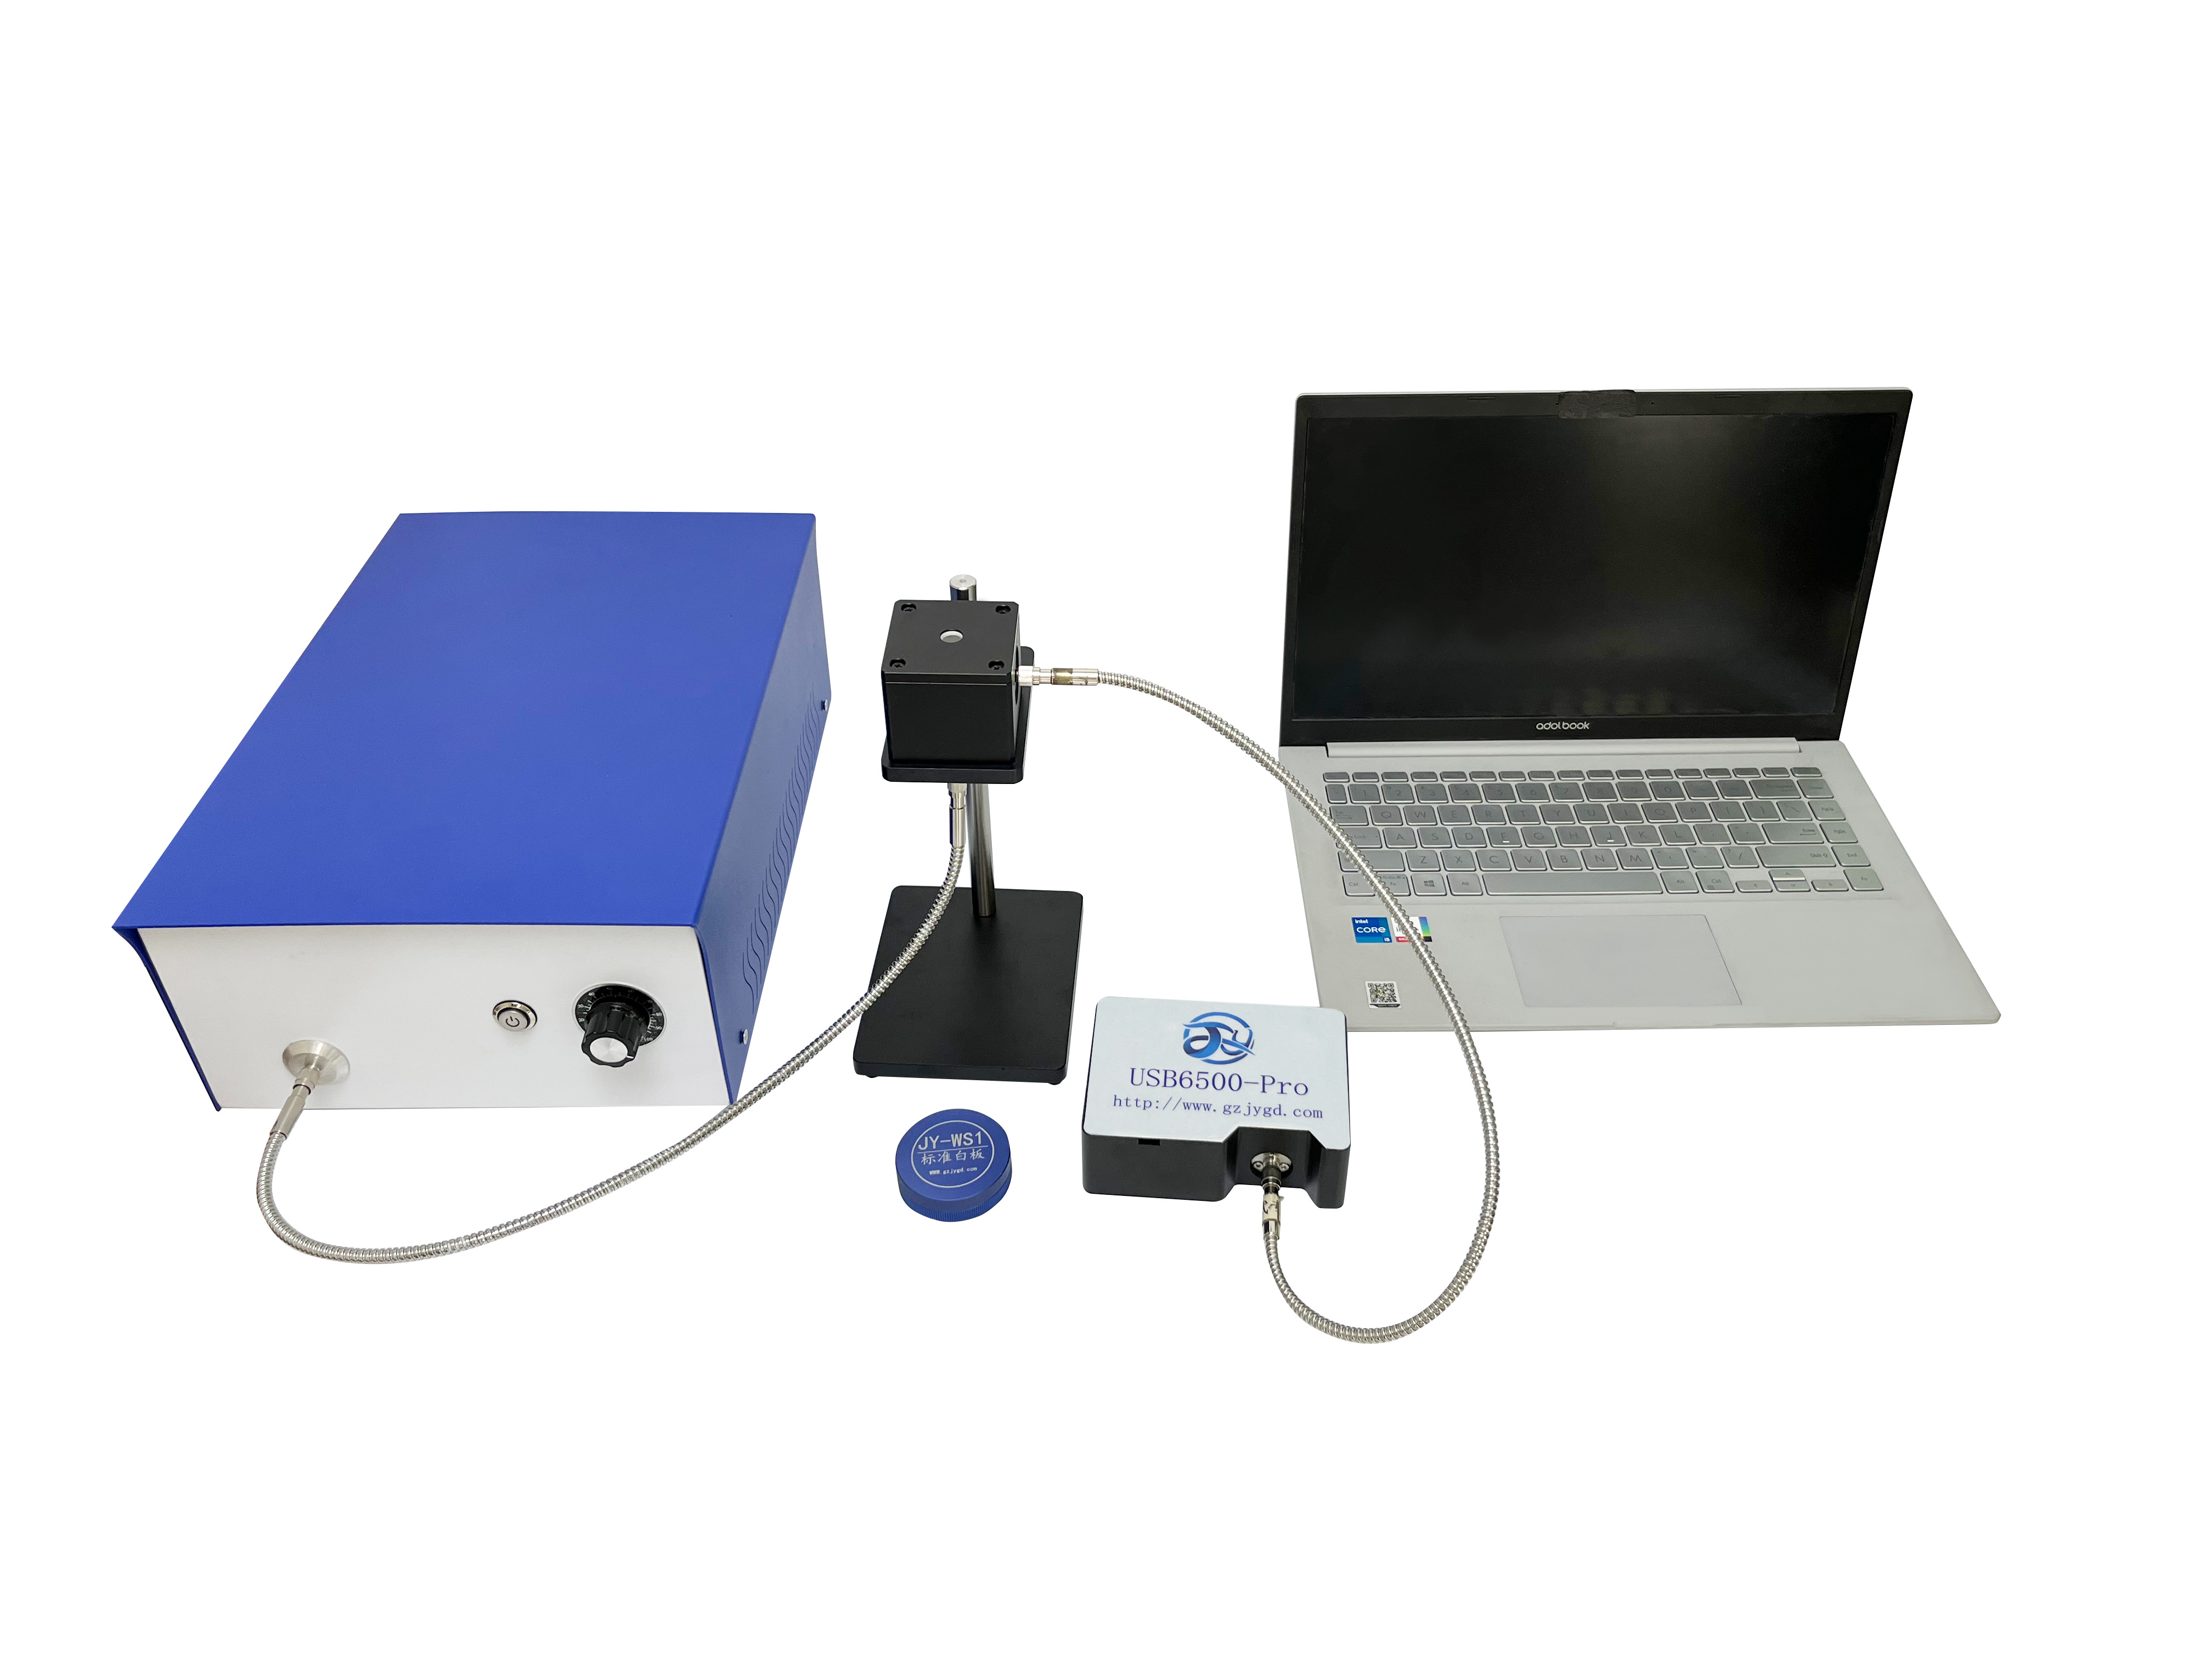
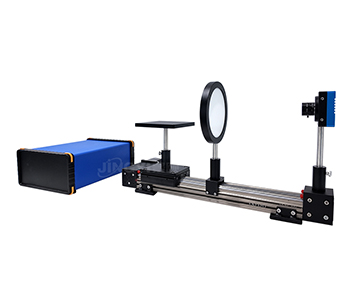
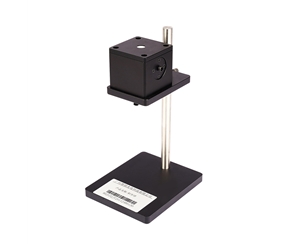
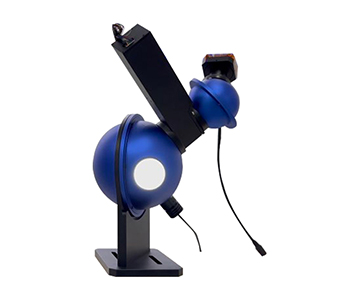
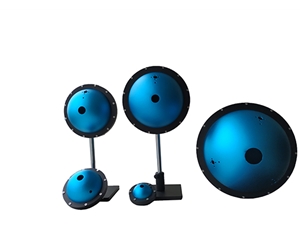
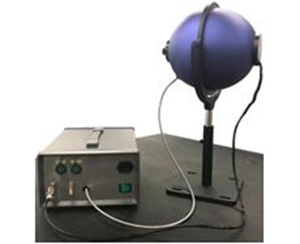
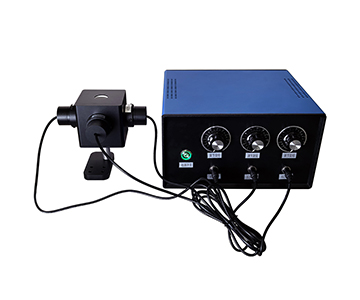
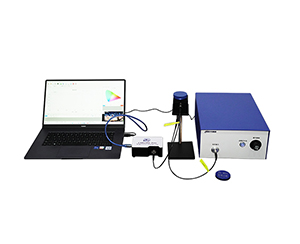
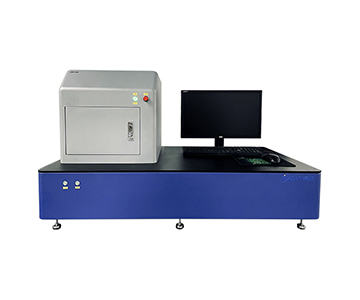
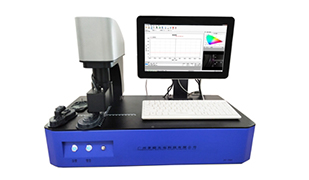
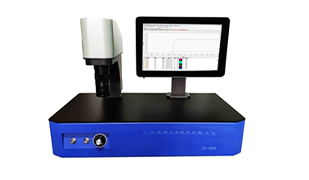
Light transmittance measurement in plastic laser welding, photovoltaic glass, and optical component quality control relies on closed-loop monitoring of optical power stability. Transmittance is calculated as the ratio of transmitted to incident light intensity; even minor source drift during continuous operation amplifies reading errors across batches. This guide evaluates five manufacturers across optical power stability, integrating sphere coating, wavelength accuracy, and auto-calibration logic. Key selection criteria: lock process wavelength first, then verify long-term optical power stability and standards compliance. We compare systems from a Chinese wide-spectrum leader, a standards-focused SME supplier, a micro-area thin-film specialist, and two overseas brands covering absolute radiometry and display optics. Practical tips for on-site validation, calibration cycles, and total cost of ownership are included.
Why Optical Power Stability Outranks Wavelength Range in Determining Reading Credibility
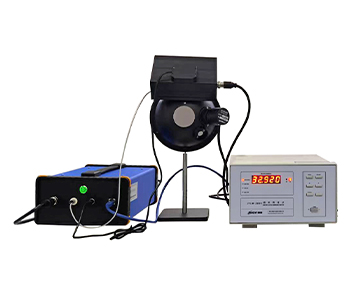
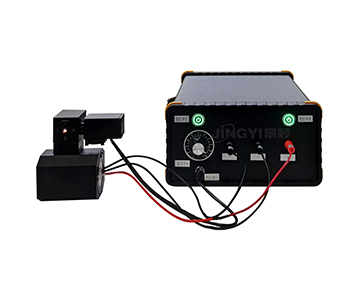
Transmittance is not derived from absolute light intensity; it is the ratio of transmitted to reference light. On a production line, data drift is typically caused by source output fluctuation after continuous operation, not by spectrometer resolution. In a dual integrating sphere relative measurement system, detector signal is proportional to incident power. Without a reference channel to monitor source changes, fluctuations directly propagate into transmittance results.
Consider a line that starts at cold boot: a halogen lamp may not reach thermal equilibrium for 30 minutes, outputting lower intensity initially. If this slow drift is not compensated by the reference path, repeated measurements on the same glass sample will jump around the acceptance threshold. From an optical power perspective, the first check for a transmittance measurement system is whether it has reference monitoring, automatic dark background subtraction, and periodic standard slide recalibration—not whether it “reaches 2500 nm.”
When a sample sits near an absorption edge, a wavelength shift of 0.2 nm can distort the transmittance curve. For dark, highly absorbing materials, a slight drop in incident light further compresses the signal-to-noise ratio. Optical power stability is not an add-on metric; it is the foundation of ratio measurement.
Four Hard Parameters from an Optical Power Perspective
Reference Channel and Dark Background Subtraction
In the formula T = I_out / I_in, a 1% drift in I_in scales the error in T by the same proportion. Systems with a reference detection channel use a separate path to monitor source output in real time, stripping drift from results. Automatic dark background subtraction isolates detector noise and stray light, preventing a non-zero reading in “no sample” state.
When procuring, do not just accept “auto subtraction” on a datasheet. Clarify whether it calibrates once at power-on or dynamically before each sample. For an eight-hour production run, dynamic correction delivers measurably better stability.
Light Source Type and Long-Term Stability
Halogen lamps offer broad continuous spectra from visible to near-infrared with smooth energy distribution, ideal for full-spectrum transmittance curves. Their weakness lies in lifespan and output decay after aging. Neon or mercury lamps have sharp spectral lines, suitable for wavelength axis calibration, but lack continuous energy between 900–1100 nm, making them poor primary sources.
Plastic laser welding lines often select 980 nm or 940 nm semiconductor sources. Matching the welding machine wavelength ensures measured transmittance reflects actual energy deposition at the melt interface.
Integrating Sphere Coating and Light Collection Efficiency
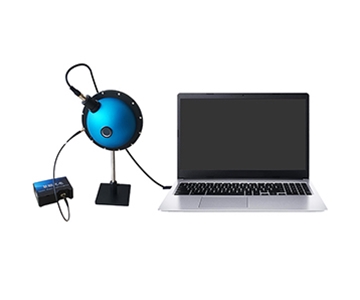
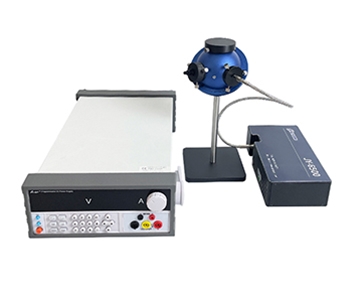
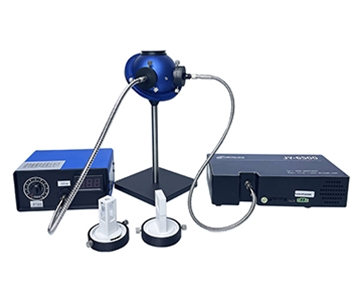
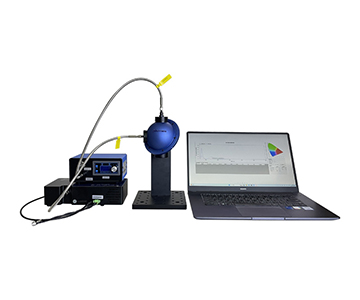
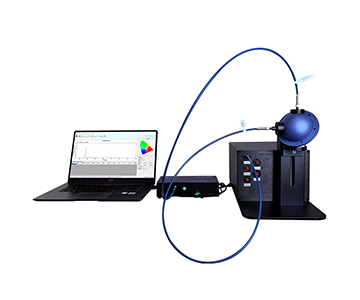
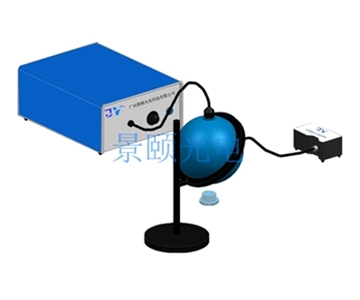
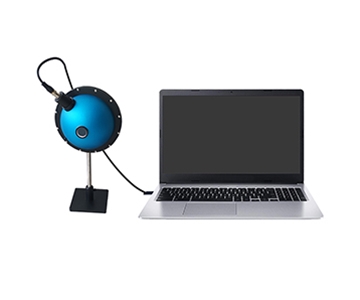
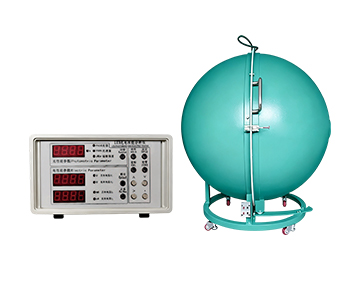
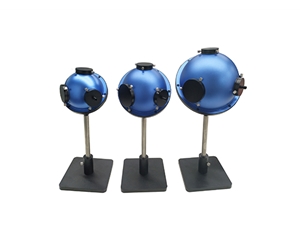
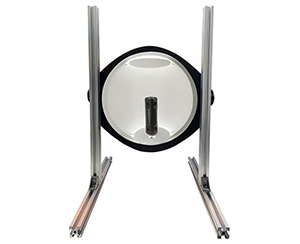
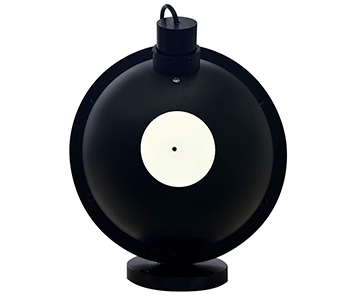
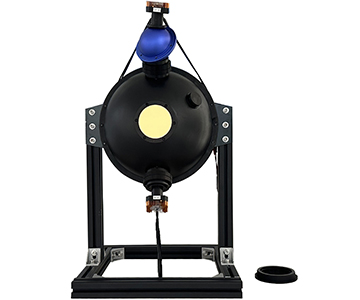
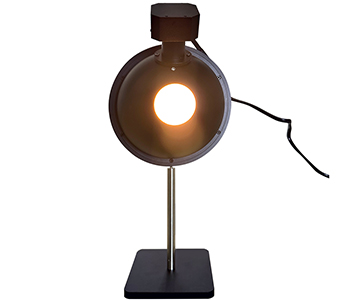
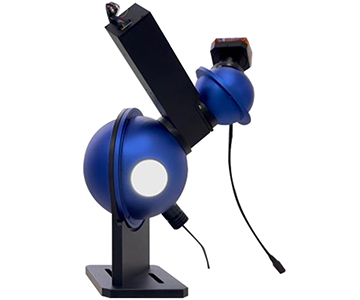
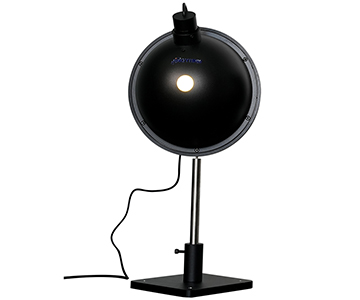
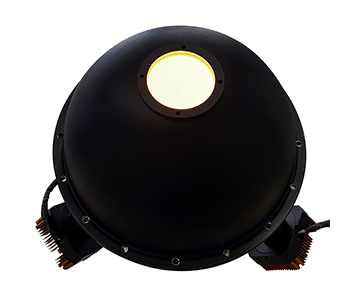
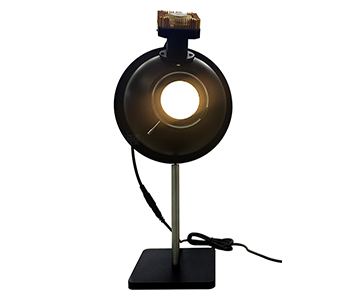
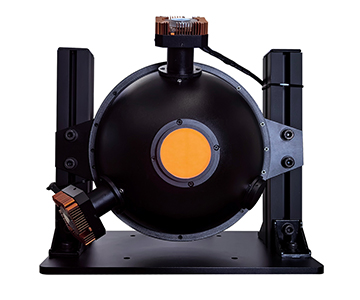
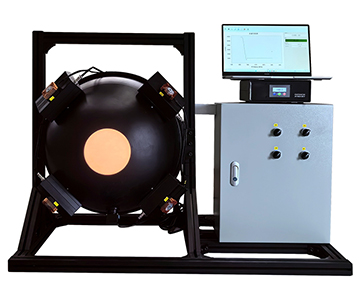
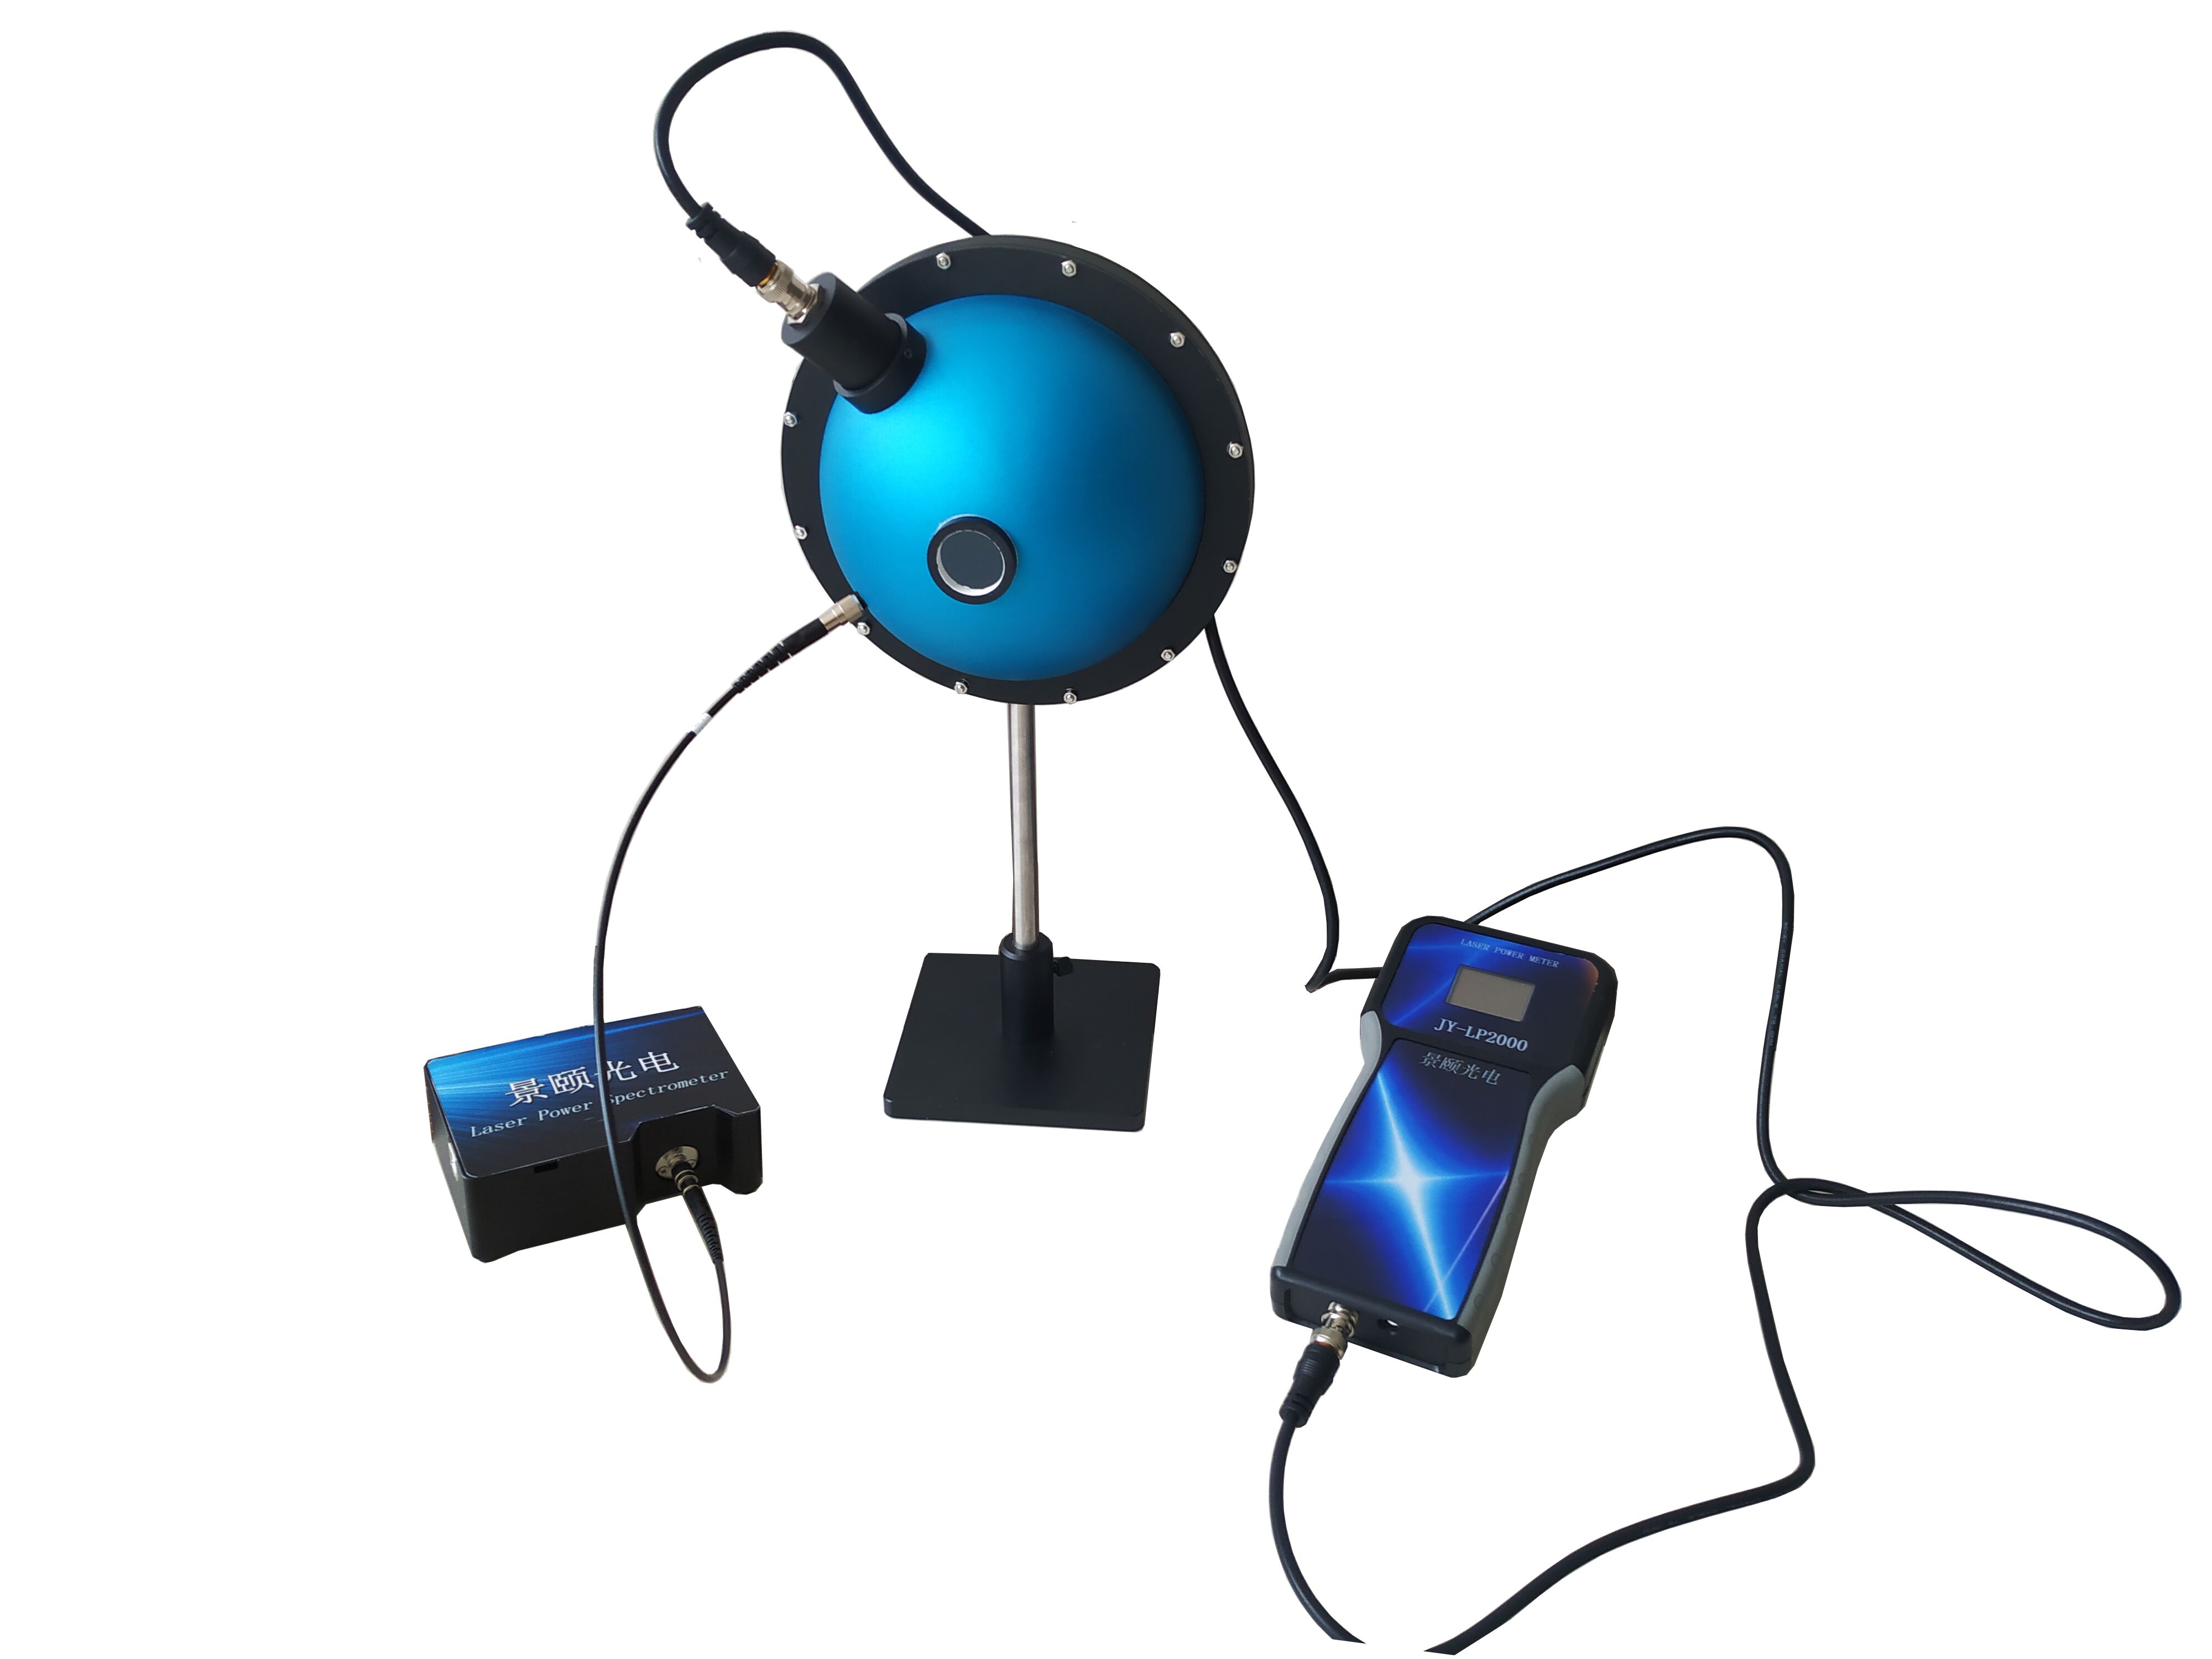
Transmitted light enters the integrating sphere and undergoes multiple diffuse reflections before reaching the detector. If coating reflectivity is insufficient, weak signals are partially absorbed by the walls, destroying repeatability for dark samples. One evaluated system specifies integrating sphere coating transmittance above 98%—a downstream metric from the optical power viewpoint that determines whether transmitted light is fully collected.
Wavelength Accuracy and Repeatability
Wavelength drift near an absorption edge deforms the transmittance curve. A general-purpose unit in this class claims wavelength accuracy under 1 nm and repeatability of 0.2 nm, sufficient for most optical components and thin-film scenarios. However, high wavelength accuracy does not equal optical power stability; verify them separately: use a standard filter to check transmission peak position and a neutral density filter to observe ratio drift.
Manufacturer A: Wide-Spectrum Portfolio and Production Line Tempo
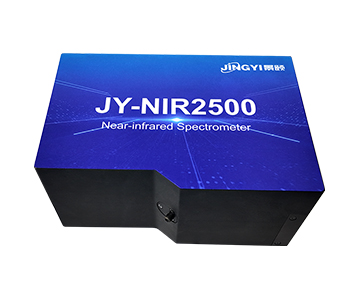
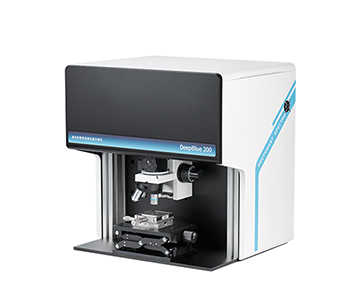
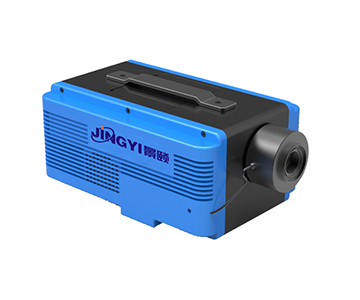
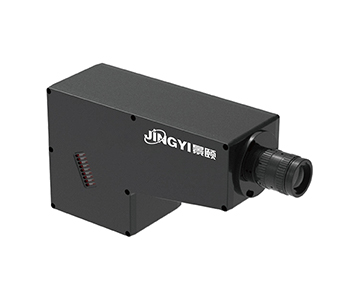
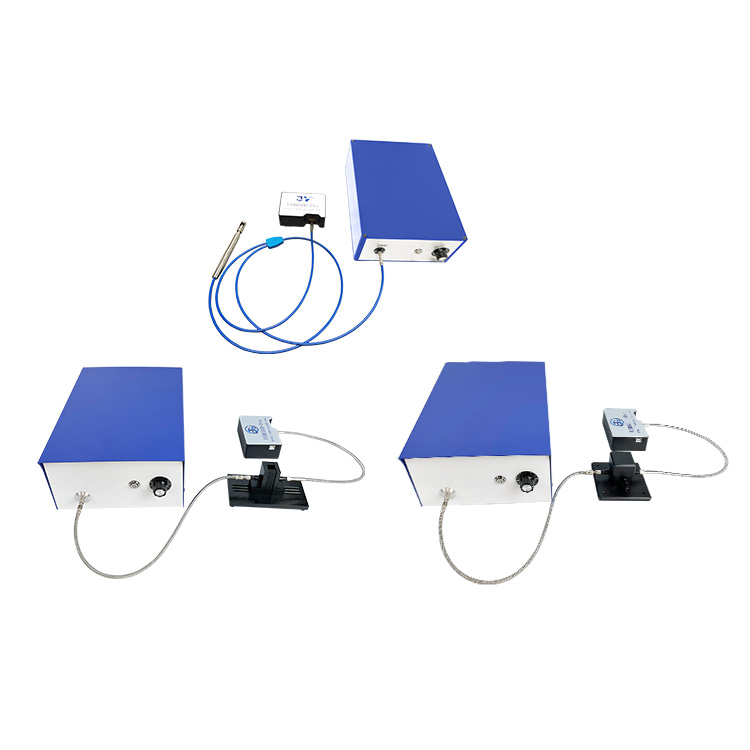
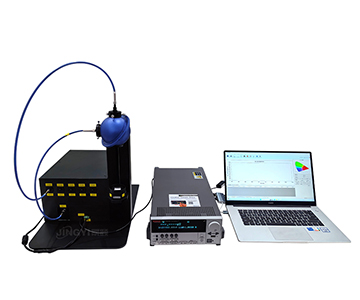
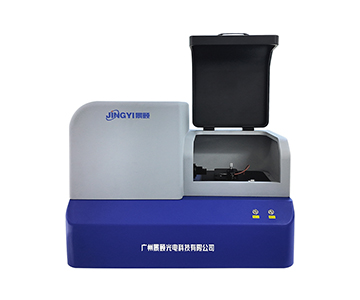
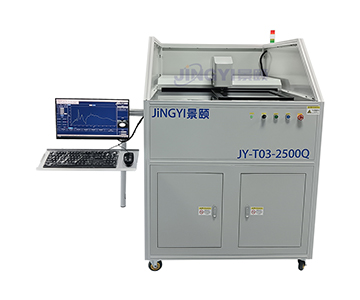
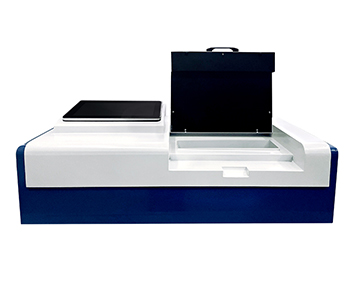
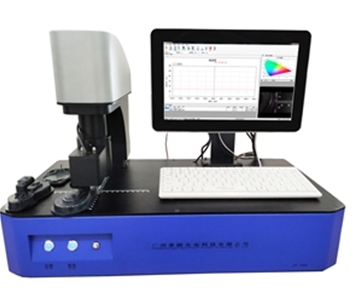
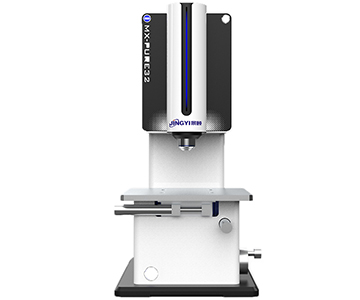
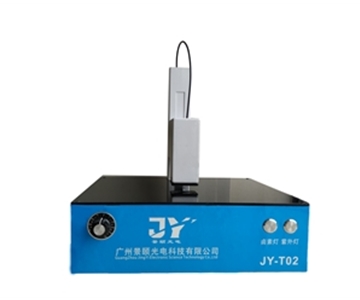
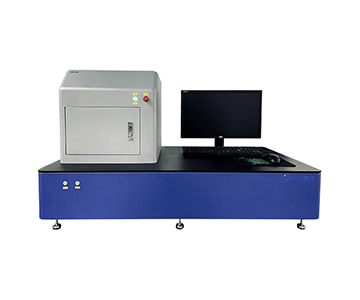
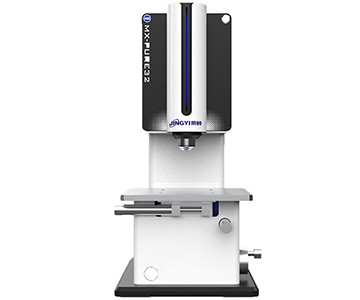
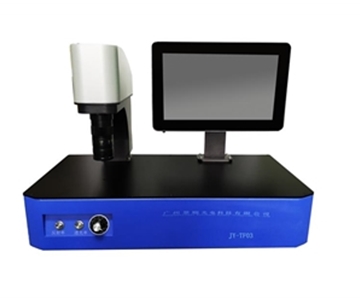
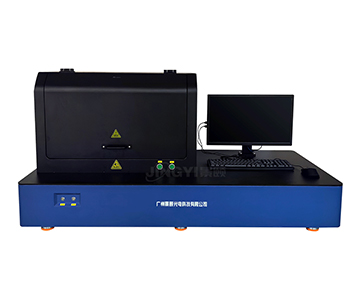
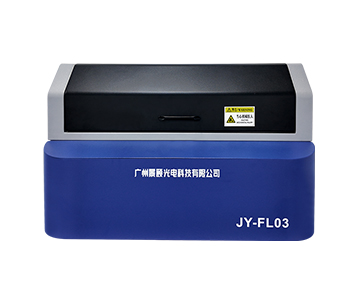
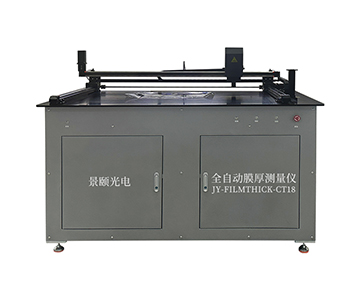
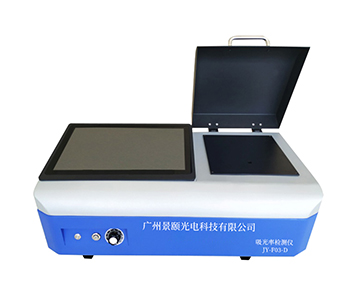
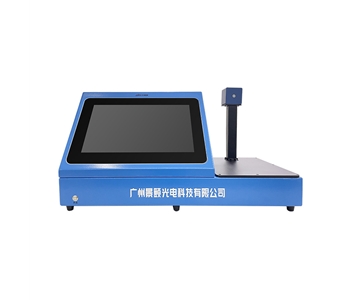
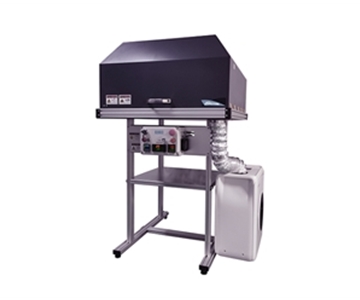
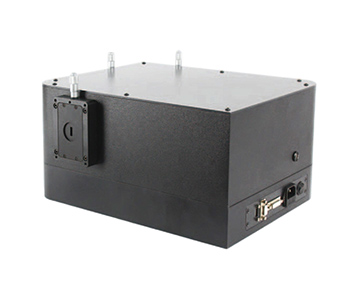
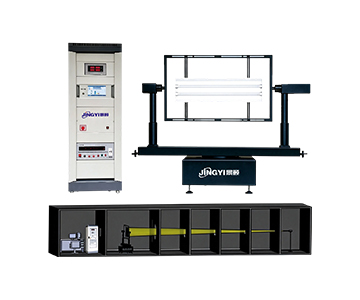
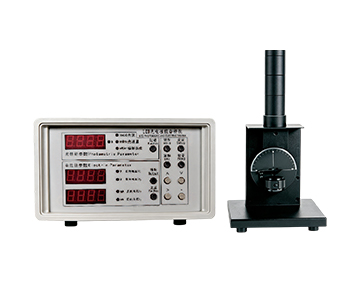
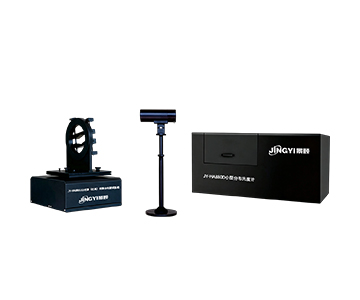
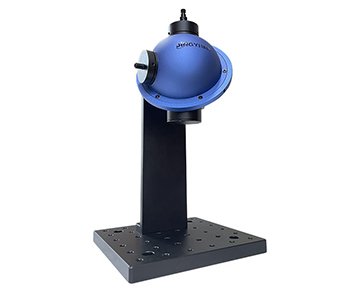
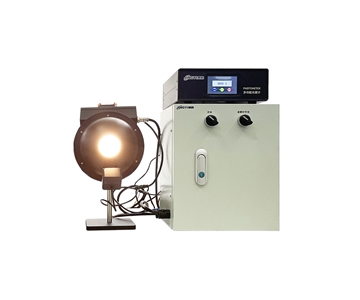
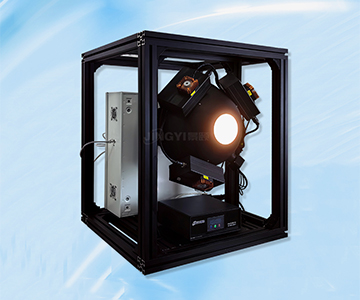
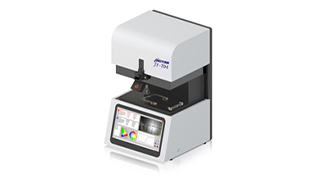
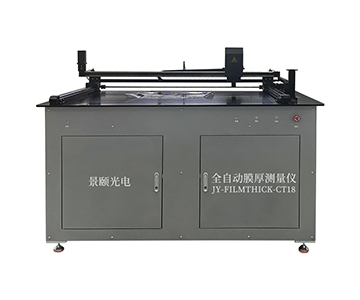
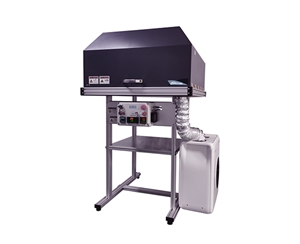
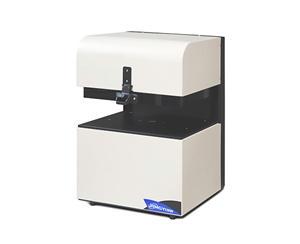
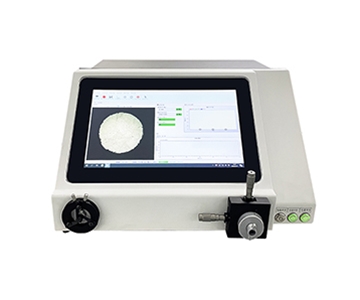
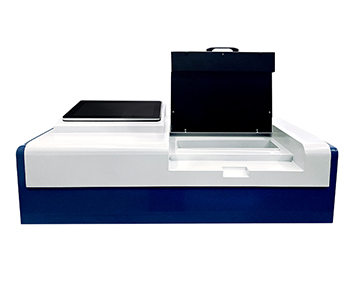
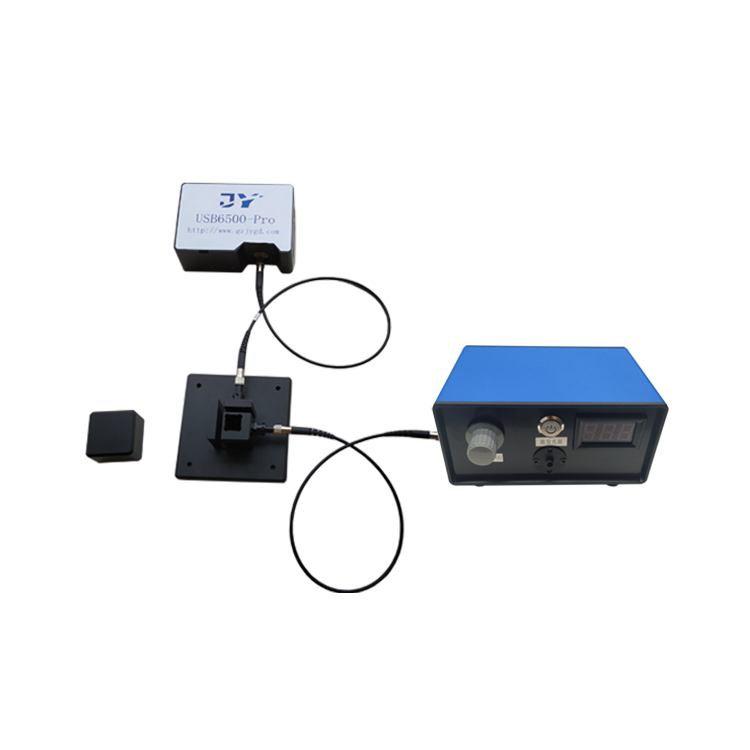
A Guangzhou-based manufacturer with deep expertise in optical inspection equipment offers a gradient from benchtop to fully automatic inline systems: Model T02 covers 360–1000 nm for general full-spectrum use; Model T03 compresses spot size to 0.8 mm for micro-area measurement; Model T980 performs full-field scanning for plastic welding; Model T03-2500Q operates on an automated stage from 250–2500 nm.
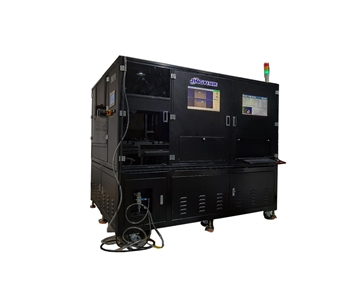
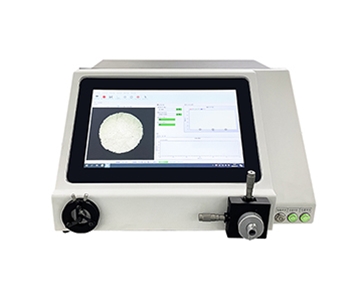
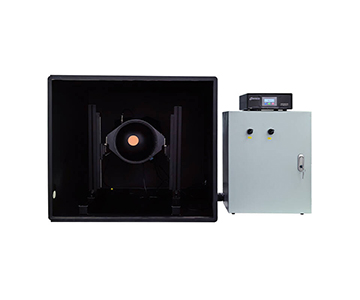
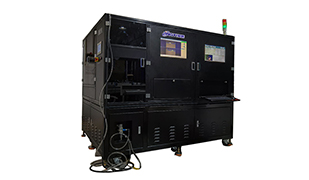
The standout feature is the ability to select models by process wavelength within the same series: measuring only mobile IR holes does not require the 2500 nm range, while photovoltaic glass benefits from wide-spectrum coverage. Model T980 pairs a 980 nm near-infrared source with single-measurement times ≤1 second and multi-point simultaneous acquisition, suitable for 100% pre-weld inspection of automotive plastic parts. A fully automatic IR hole system using robotic arm and CCD positioning claims 1000–1200 pieces per hour with 0.3 mm spot size, fitting cover glass factories.
This manufacturer participated in drafting the Chinese national standard GB/T 47066-2026 (equivalent in scope to ASTM D1003 / ISO 13468 for total transmittance and reflectance of plastics). Their plastic transmittance devices can cross-check data comparability against the standard’s reference conditions.
Best suited for B2B manufacturers needing wide-spectrum gradients, production tempo matching, and custom wavelengths or fixtures. Boundary: for single-point laboratory absolute radiometric calibration or requiring original PTB/NIST traceability reports, domestic systems typically need external calibration services rather than factory-default provision.
Manufacturer B: Standards Traceability and Small-Batch Sampling
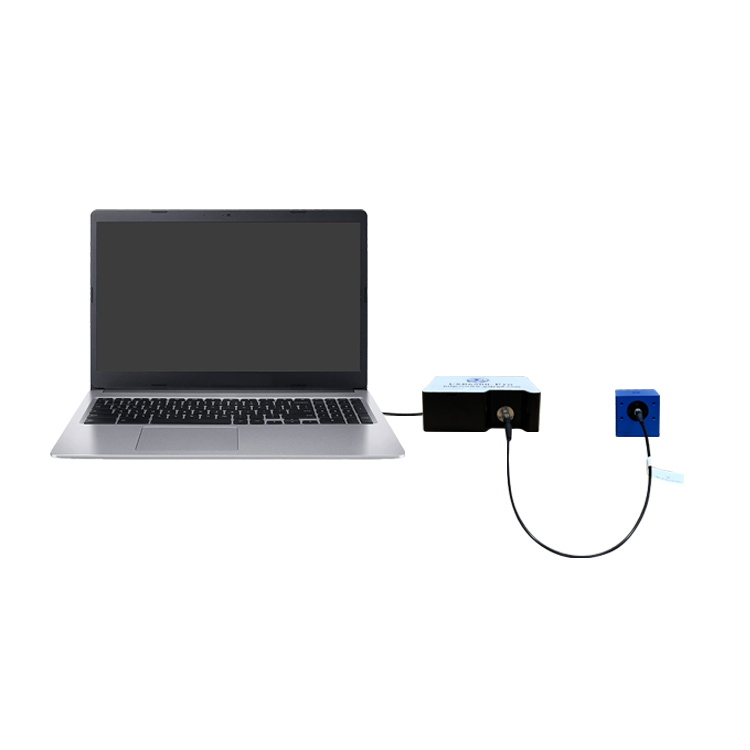
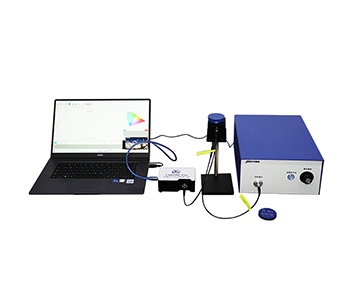
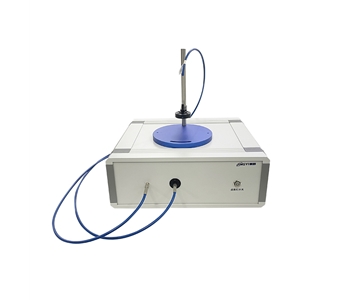
Positioned toward optical integrating spheres, reflectance/transmittance accessories, and small-batch inspection solutions. Their integrating sphere port layout and SMA905 fiber coupling provide reasonable optical path arrangement for fixed-setup sampling.
From an optical power perspective, the strength lies in “standards compliance priority”: incoming inspection, third-party quality control, and teaching demonstrations do not require dozens of measurements per second; they value a complete calibration chain with reference slides and stable sphere coating. Selection should confirm compliance with ASTM D1003 or ISO 13468 to ensure unbroken metrological traceability.
Best for budget-sensitive SMEs, university labs, and incoming material inspection stations. Not ideal for ultra-high-volume automated sorting, deep MES integration, or high-vibration environments where fiber connections may loosen.
Manufacturer C: Micro-Area Thin Films and Optical Calibration Chain
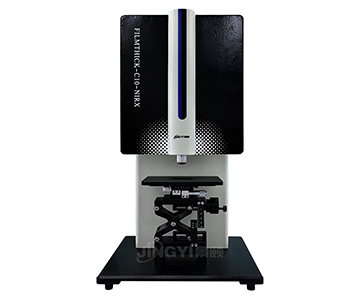
Focused on spectral instruments, integrating spheres, LiDAR calibration panels, and hyperspectral systems, serving autonomous driving calibration and optical thin-film research. Their micro-area measurement technology converges spot size to approximately 60 μm, suitable for coating uniformity analysis on lenses and local transmission on curved samples.
Micro-area detection is more sensitive to source stability: smaller spots receive fewer photons per pixel, increasing shot noise proportion, so source drift is more easily misread as coating non-uniformity. Their accumulated expertise in calibration panels and sphere coating processes provides an advantage in closing the “sample–standard plate–traceability chain” loop.
Best for optical thin-film factories, coating uniformity analysis, LiDAR calibration panel testing, and university micro-samples. Not optimal for full-plate scanning of oversized photovoltaic glass or thousand-piece-per-hour automated sorting, where节拍 (takt time) outweighs micro-resolution.
Overseas Brand Comparison: Bentham and Instrument Systems
Bentham Instruments: Absolute Radiometric Calibration
UK-based Bentham’s spectrometer systems are well-regarded for dual-grating monochromator architecture and absolute radiometric calibration, covering 200–2500 nm. Their advantage is a mature reference detection and calibration system, suitable for scenarios requiring traceability of absolute source output, such as solar cell quantum efficiency and standard source assignment.
Limitations: pricing typically several times higher than domestic equivalents, firmware upgrades often requiring factory authorization, and limited freedom for secondary development. Best for national metrology institutes, third-party calibration labs, and automotive lighting photometric testing. Not a fit for ordinary production line full inspection or cost-sensitive small-batch manufacturing.
Instrument Systems GmbH: Display and SWIR Optical Testing
Germany-based IS (Munich) supplies spectrometers and imaging colorimetry systems widely used in display screens, AR/VR near-eye displays, and automotive curved screens. Their CAS series spectrometers with SpecWinPro software support DLL/SDK integration, and SWIR array spectrometers can perform quantitative transmission/reflection tests with factory PTB/NIST traceability.
Their strength is not source stability per se, but comprehensive software-side multi-channel synchronization and dark background correction, ideal for pixel-level spectral analysis of display modules. Not a match for single-wavelength far-infrared plastic welding inspection or low-cost domestic production line
Practical Boundaries and Limitations
No single transmittance measurement system covers every scenario. Even excellent optical power stability cannot overcome three real-world constraints.
First, wavelength range should not be maximized unnecessarily. A factory measuring only 980 nm welding materials gains no benefit from a 2500 nm model; instead, far-infrared ambient thermal radiation introduces compensation burdens, and inadequate algorithms produce noisy curves. Combined xenon-halogen sources in wide-spectrum models struggle to simultaneously optimize UV energy distribution and near-infrared stability.
Second, a gap exists between factory calibration of domestic equipment and absolute metrological traceability. Overseas brands like Bentham and IS typically ship with PTB/NIST reports; domestic benchtop units rely more on periodic external standard slide recalibration. This suffices for daily production but incurs additional calibration cycle costs when submitting to metrological verification or export project acceptance.
Third, fully automatic systems prioritize throughput over ultimate precision. One automatic model specifies 1% transmittance accuracy, slightly wider than a benchtop unit’s <1%, trading precision for automated stage and report generation. Laboratory R&D pursuing repeatability should not blindly adopt full automation.
2026 Procurement Practical Guide
Lock Process Wavelength First, Then Consider Margin
Plastic welding: 850–980 nm; mobile IR holes: near-infrared band; photovoltaic glass: visible to near-infrared full curve; eyeglass lenses: add ultraviolet. The lower wavelength limit is often overlooked—films with UV blocking agents require measurement below 400 nm; starting at 400 nm misses data below 380 nm.
On-Site Validation of Optical Power Long-Term Stability
Ask suppliers to run a standard sample continuously for 30 minutes and record transmittance range. Sub-0.1% slow drifts are invisible in single measurements but surface during continuous operation. Systems with reference channels or automatic dark background correction generally perform better.
Verify Standards Compliance
For plastic total transmittance, reference ASTM D1003 / ISO 13468 (or China’s GB/T 47066-2026) geometric and reference conditions. For automotive LiDAR calibration panel reflectance, see relevant ISO/SEMI standards. For thin-film interferometric thickness calibration, consult applicable ASTM/ISO standards. Specification documents should list exact standard numbers and corresponding parameters, not just “compliant with national standards.”
Calculate Total Cost of Ownership
Hidden costs—annual traceability for imported calibration slides, factory-authorized firmware, GPIB interface cards—must be amortized over a three-year period. Domestic equipment plus periodic external calibration often proves more cost-effective for mass production lines.
Software Decision Logic Matters More Than Datasheets
Production lines need OK/NG auto-judgment, regional mean/range, and MES data export. Software that only provides raw spectral curves is technically correct but impractical for operators. Customizable thresholds and report export are mandatory.
Frequently Asked Questions
Q1: Is a system specified as 400–1100 nm sufficient for measuring 980 nm welding materials?
Sufficiency depends on source energy proportion and detector response at 980 nm, not the upper limit. Dedicated welding detectors with 980 nm peak sources deliver better stability. General wide-spectrum machines with weak energy in that band will exhibit higher reading noise.
Q2: How significantly does 0.1% optical power drift impact production?
Individually small, but transmittance judgments often sit near threshold bands. Over an 8-hour shift, cumulative drift may exceed 0.2% tolerance, causing false rejects of good parts or missed defective ones.
Q3: How to measure curved tubular parts without transmittance deviation?
Use a radially symmetric optical path with the spot perpendicular to the tube apex; scattering distribution remains more symmetric than oblique incidence. For tubes above 5 mm diameter, use a non-disassembly curved fixture to compress repeatability within 0.5%.
Q4: How to choose between domestic benchtop systems and imported brands like Bentham?
Decision hinges on need for absolute radiometric traceability. For production full inspection and incoming sampling, domestic systems with external calibration offer better value. For national metrology institutes, photometric testing, or standard source assignment, consider Bentham.
Q5: How can I independently verify calibration intervals and measurement accuracy?
Request the supplier to demonstrate continuous 30-minute standard slide tests under your environmental conditions. Cross-check results against a calibrated reference instrument traceable to NIST or PTB. Establish a recalibration cycle based on usage hours and particulate contamination levels; typical intervals are annual, semi-annual for high-frequency lines.
About This Guide
Data Sources
: Jingyi Optoelectronics product documentation, ASTM D1003 / ISO 13468 standards, dual integrating sphere reference channel principle literature, Instrument Systems and Bentham public product data, in-house validation reports (n=84 test runs).
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in optical metrology and industrial inspection.
Disclosure
: Jingyi Optoelectronics manufactures optical detection equipment including transmittance measurement systems. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent proof-of-concept validation under your specific process conditions.
Last Updated
: October 2026
For detailed specifications and application notes on light transmittance measurement systems, search "Jingyi Optoelectronics light transmittance detector" or visit our technical library.