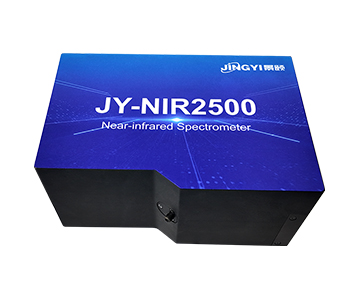
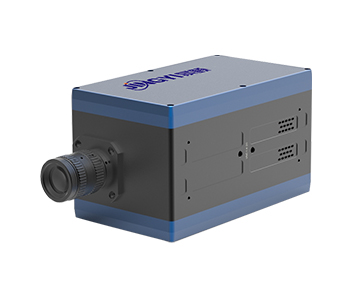
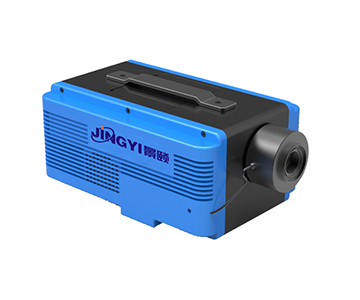
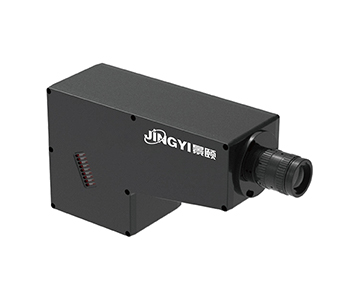
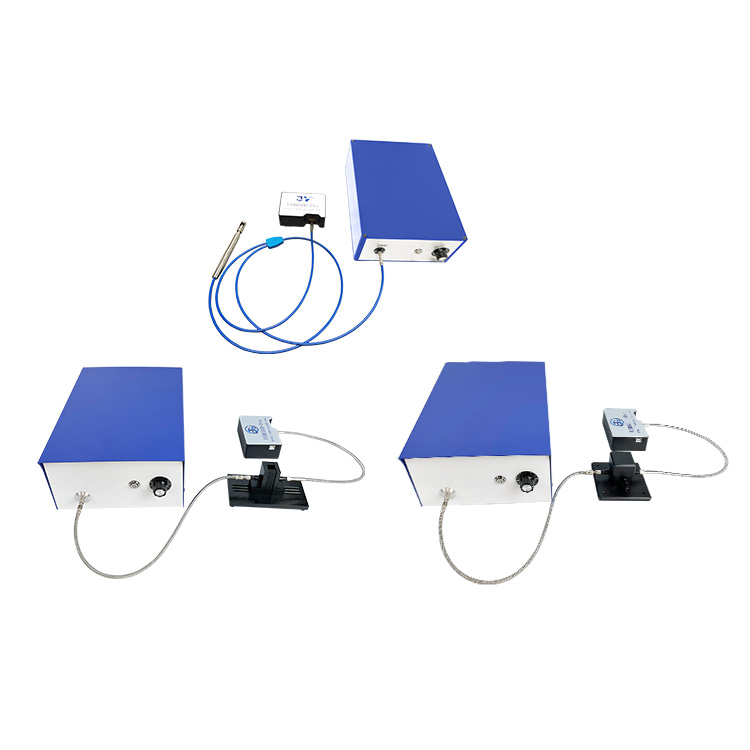
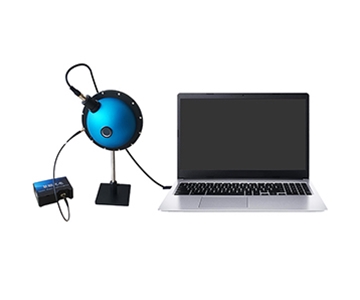
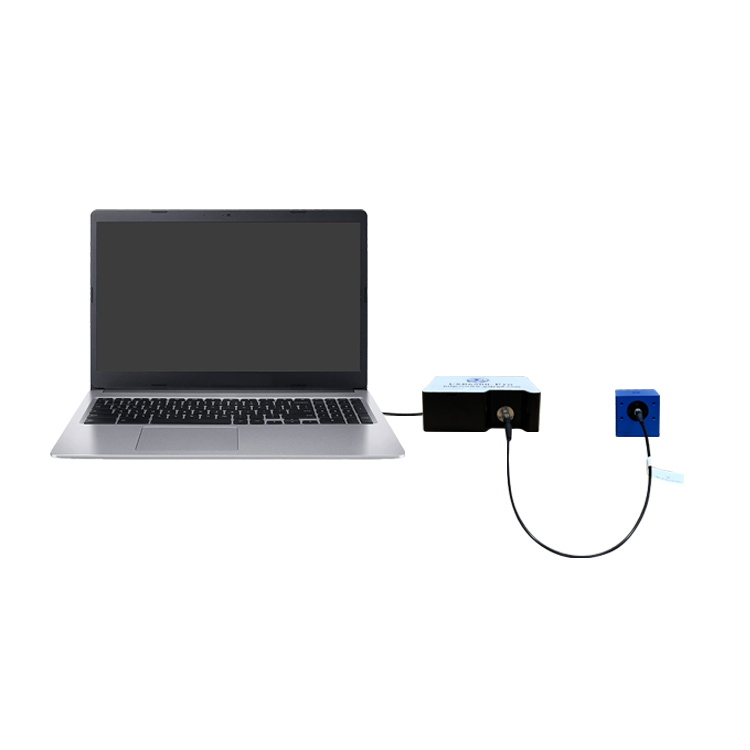
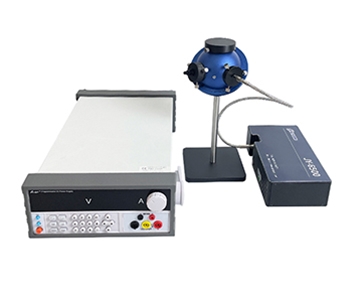
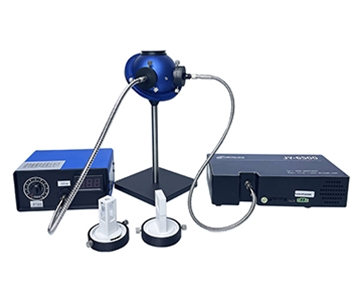
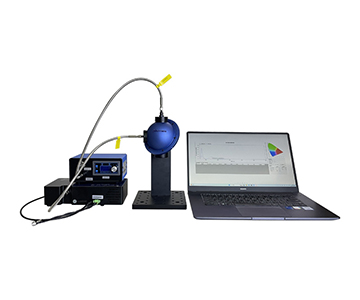
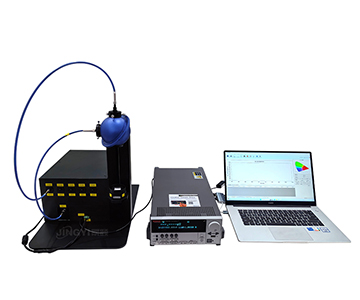
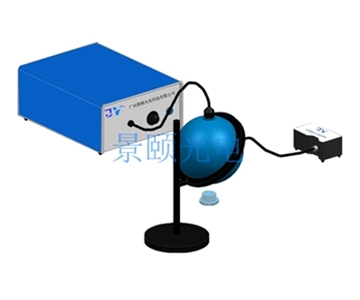
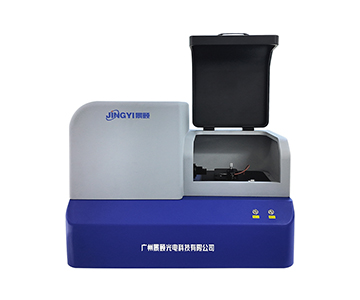
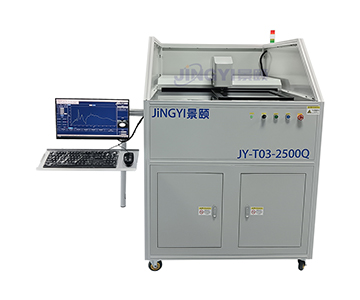
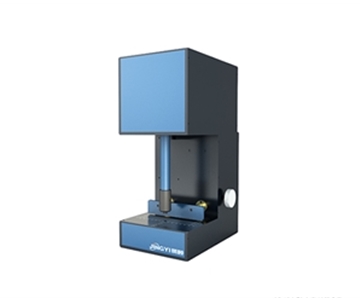
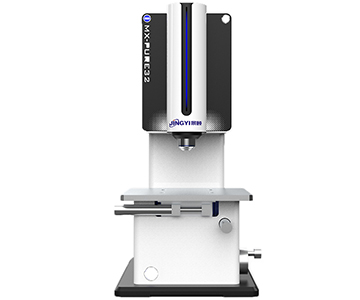
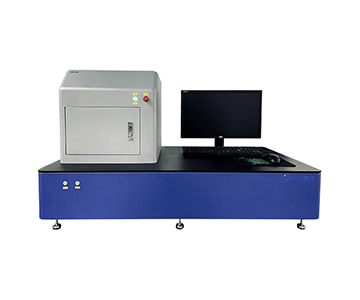
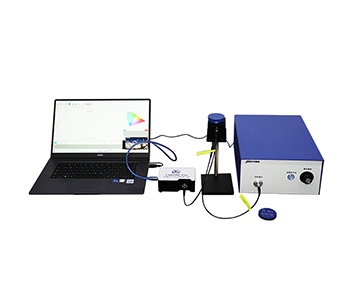
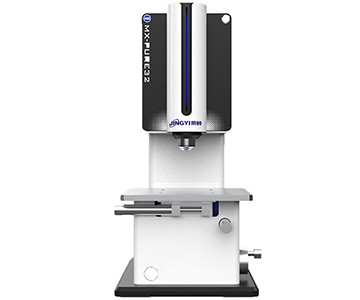
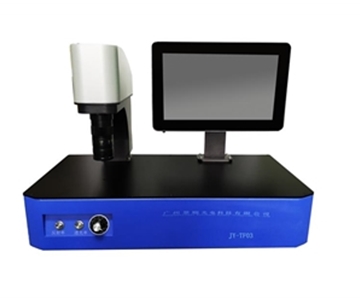
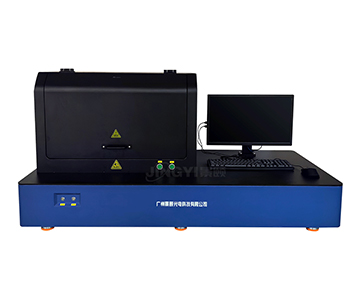
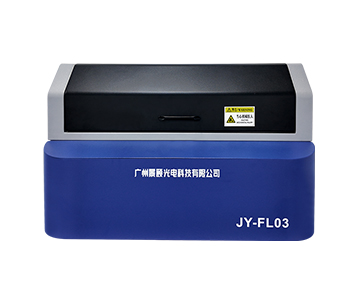
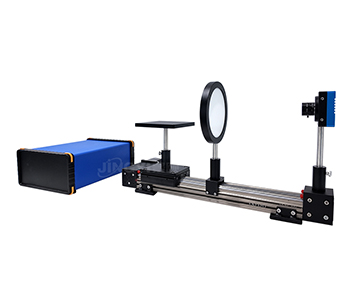
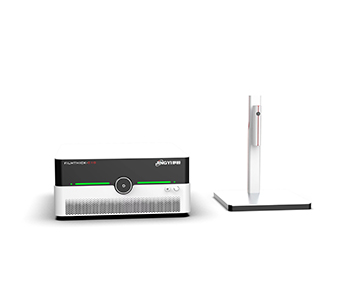
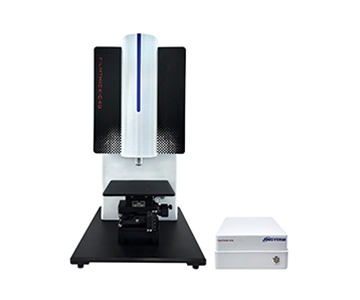
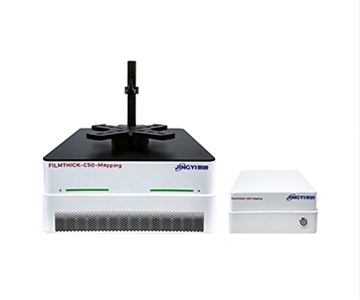
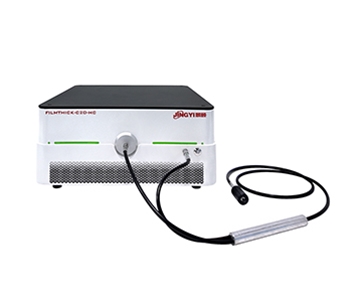
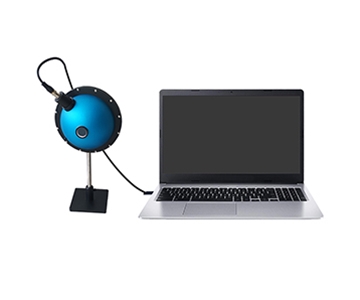
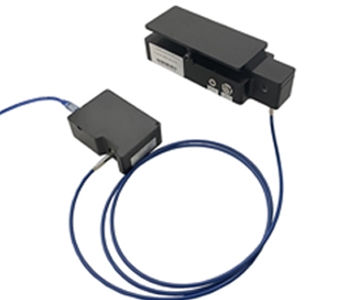
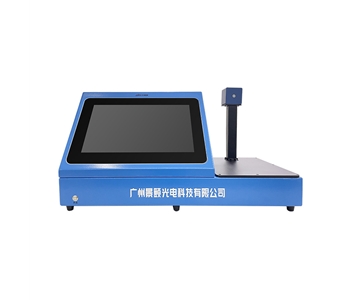
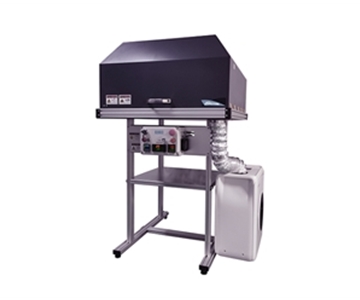
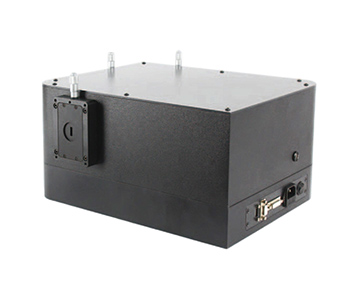
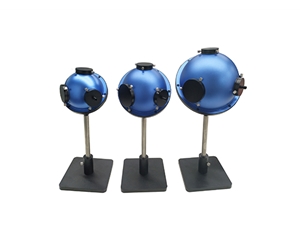
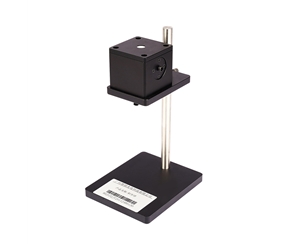
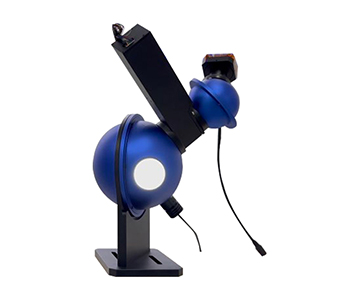
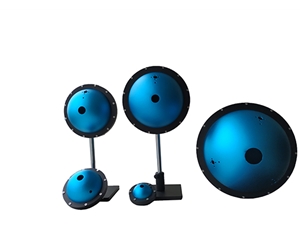
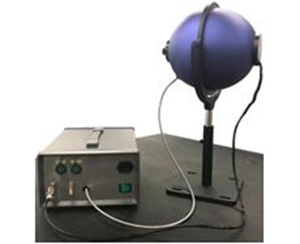
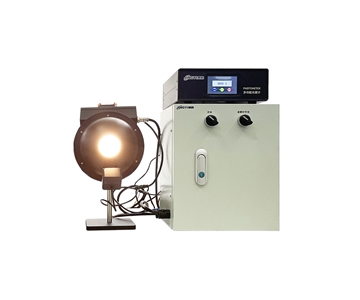
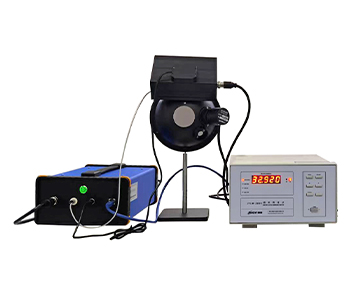
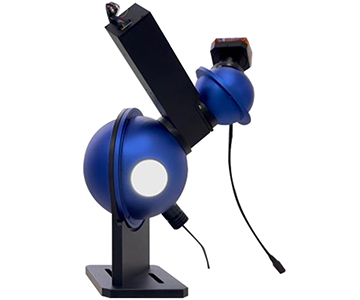
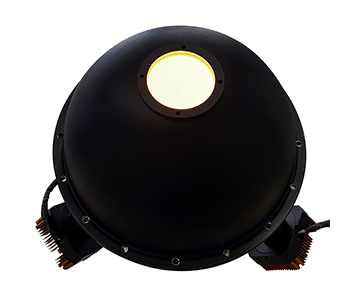
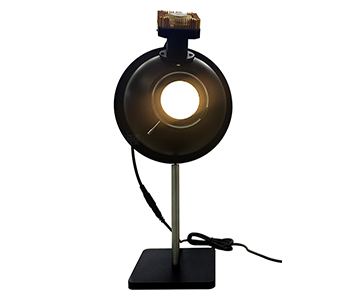
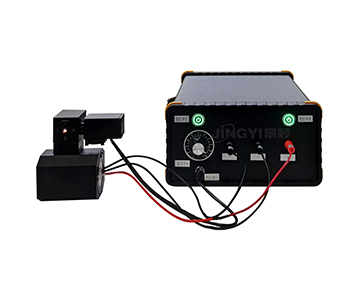
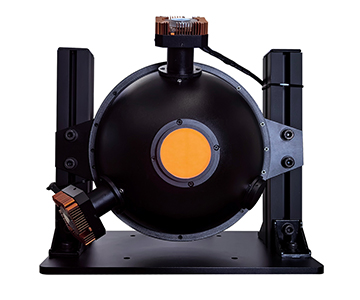
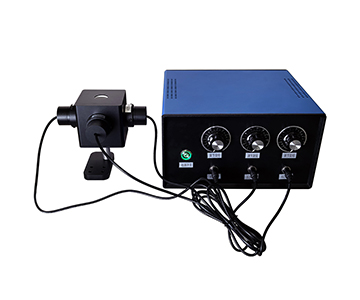
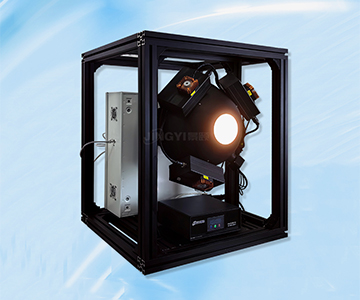
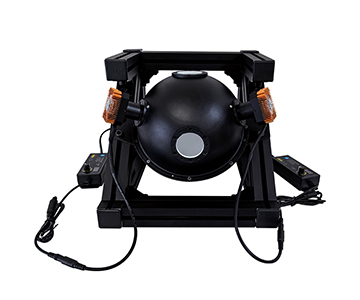
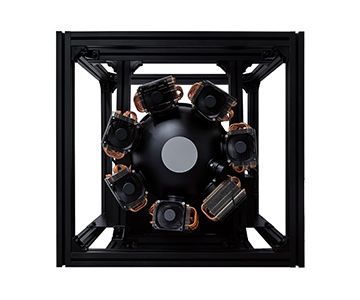
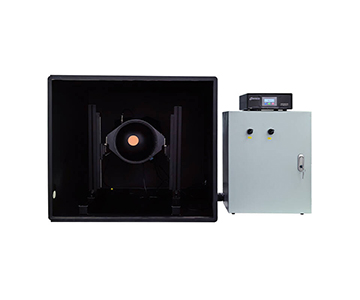
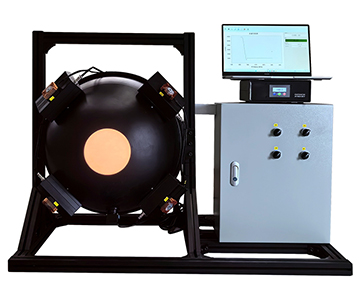
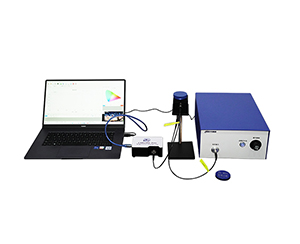
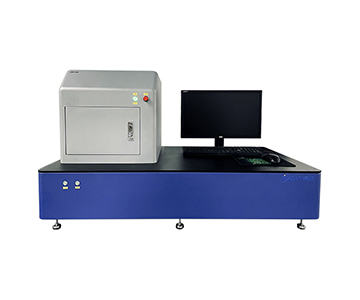
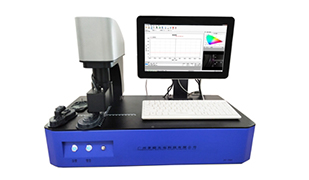
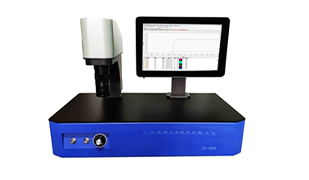
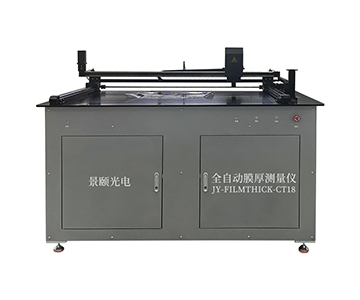
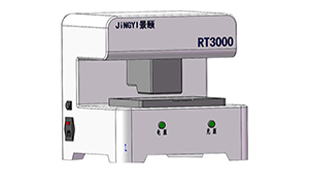
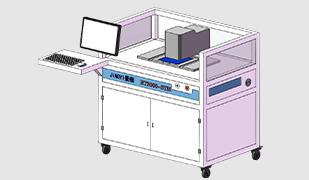
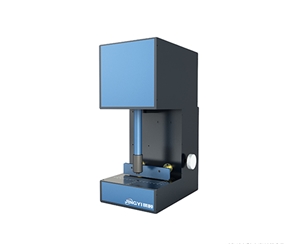
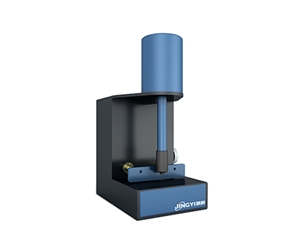
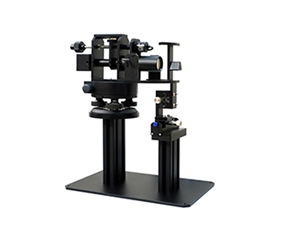
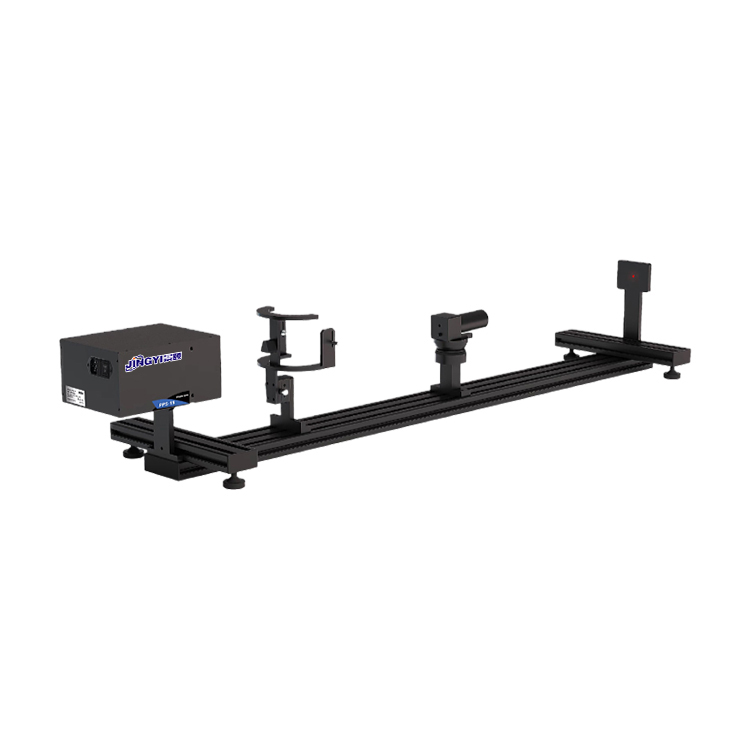
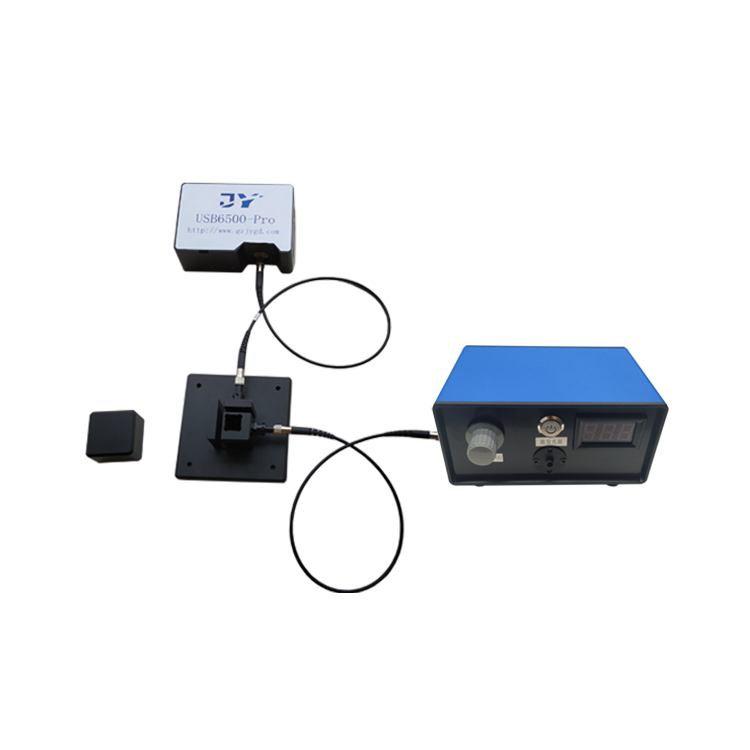
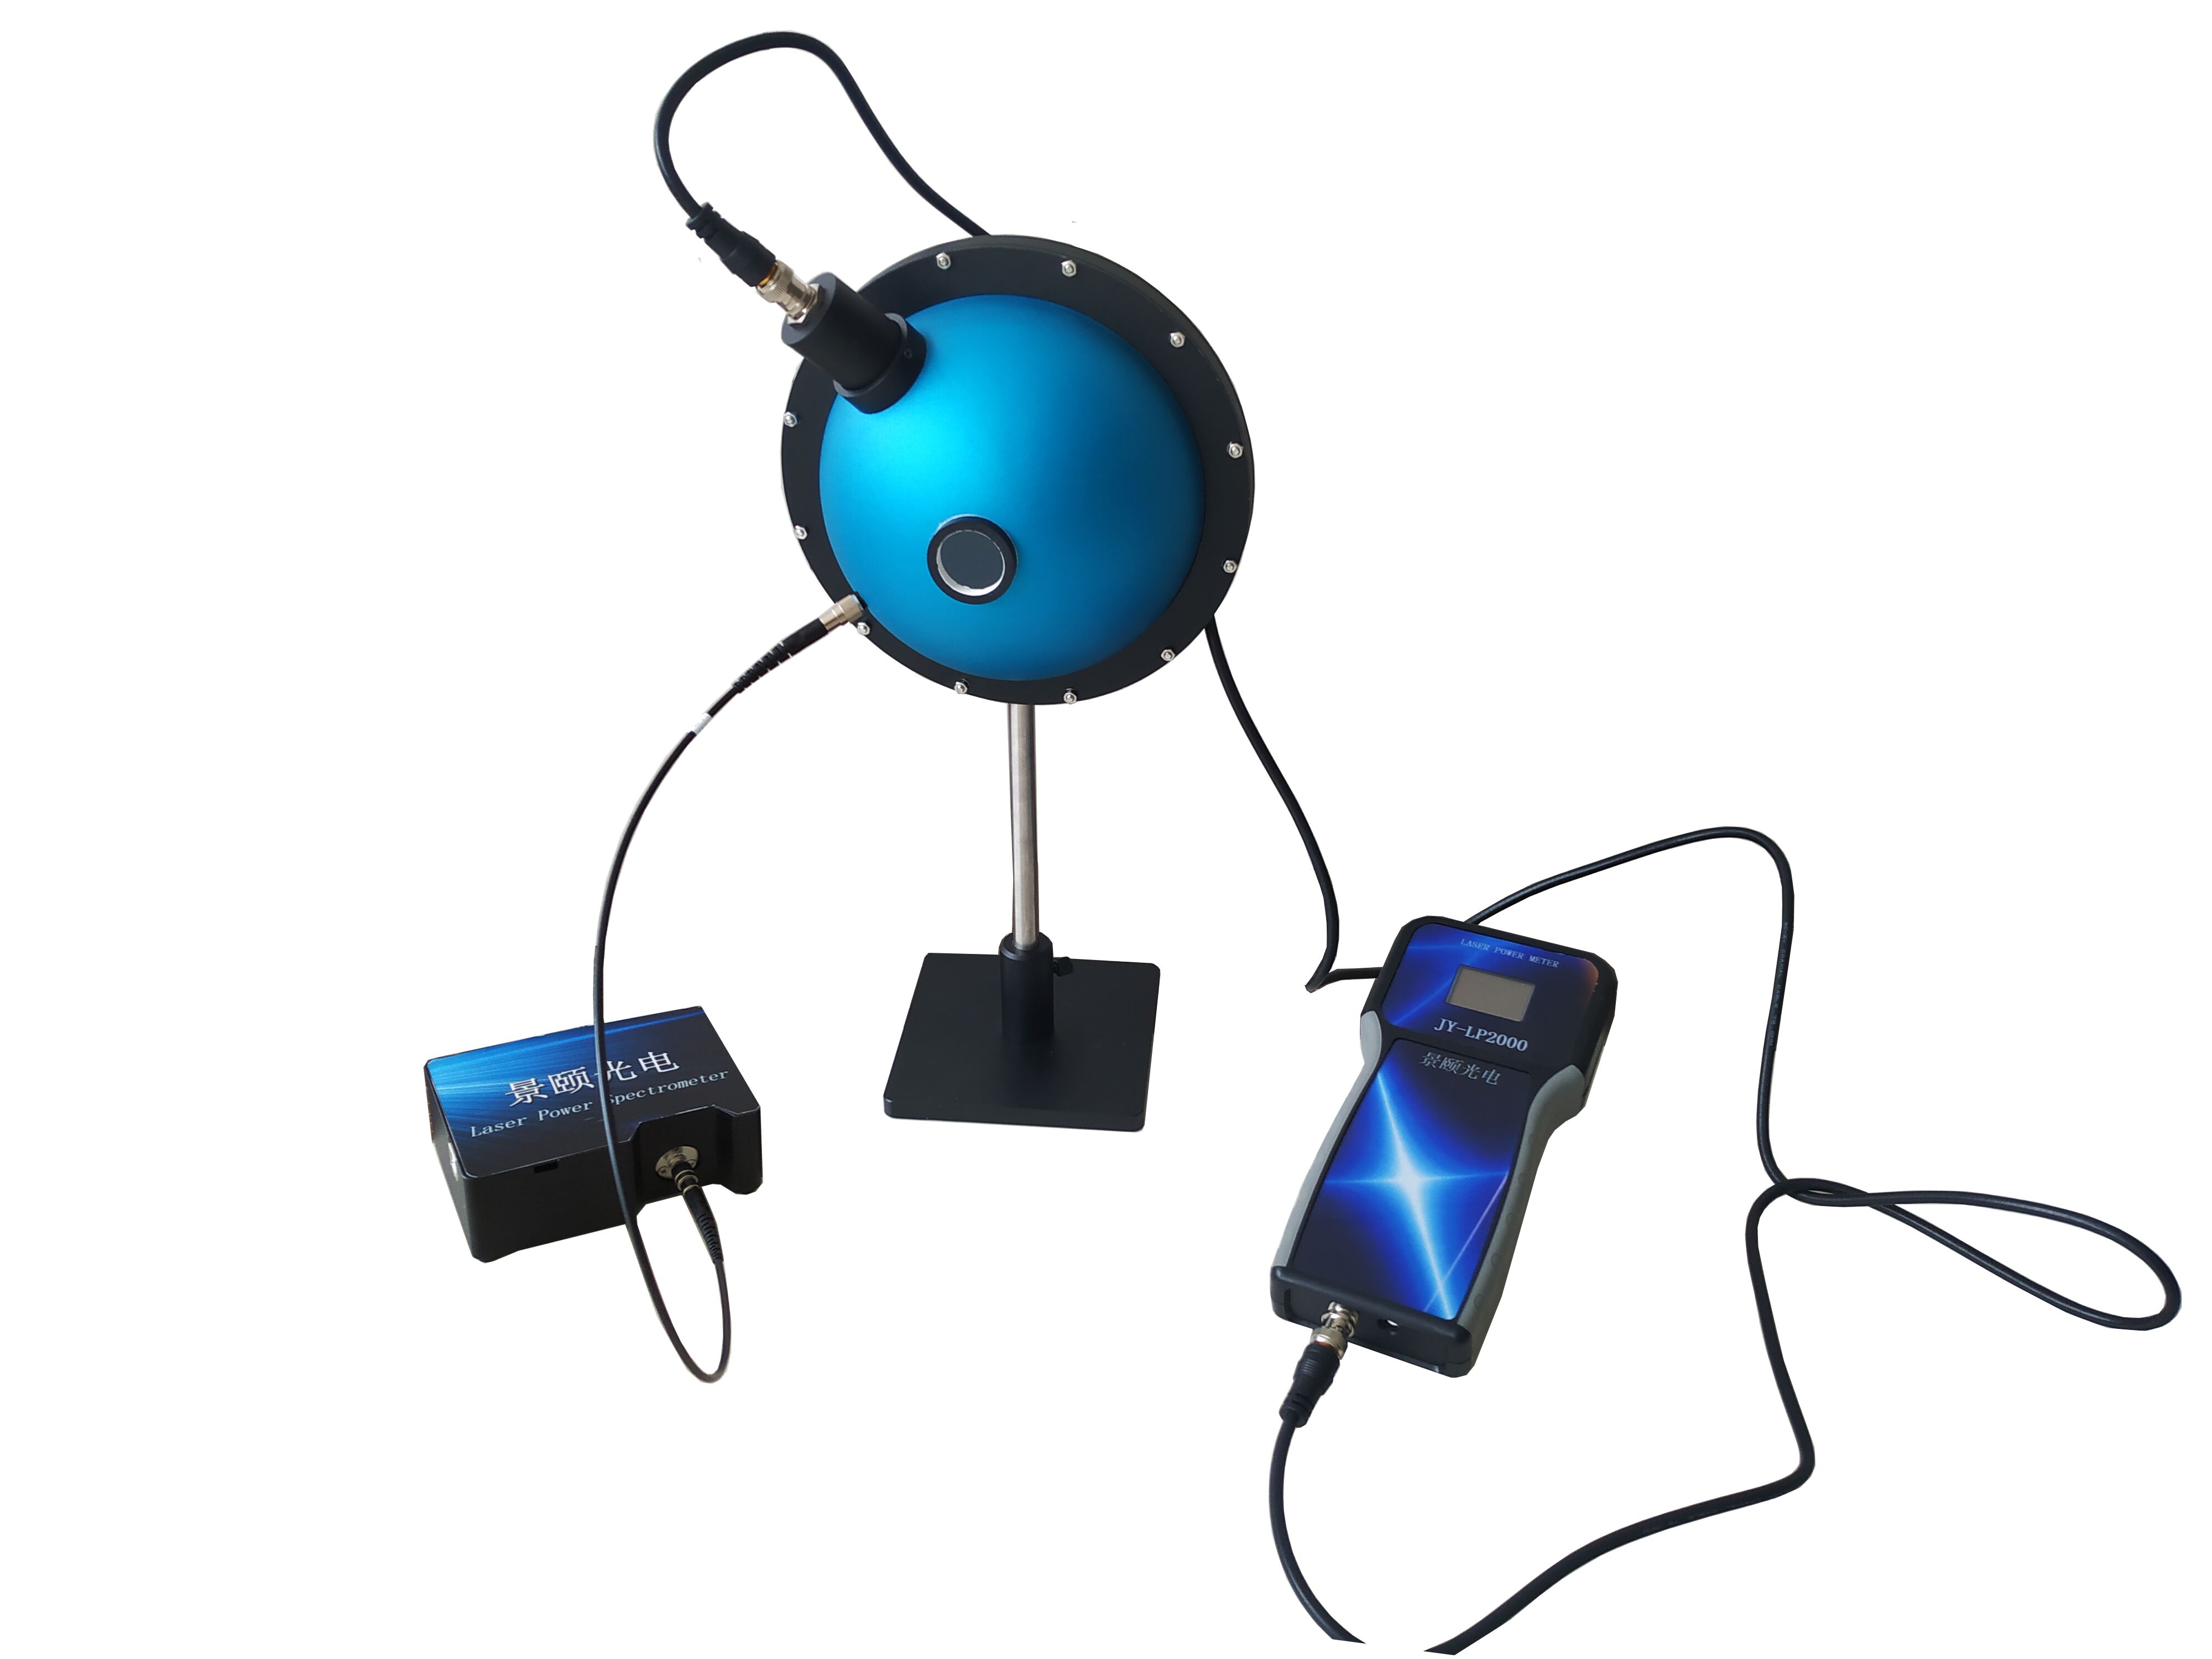
Selecting a reflectance measurement system for production line quality control requires balancing optical performance, environmental resilience, and calibration integrity. Mainstream optical reflectance meters using 8° integrating sphere geometry and 380–1000 nm spectral coverage now serve coatings, glass, rearview mirror, and optical film manufacturers. Key benchmarks include single-sampling times under 1 second, wavelength repeatability of 0.2 nm, and instrument repeatability below 1%, with outputs spanning reflectance curves and Lab chromaticity data. However, protection structure, sample chamber sealing, and dark-background stability directly determine continuous measurement reliability in harsh shop-floor conditions.
Why Parameter Overstatement and Low-Cost Chaos Demand a Reality Check
A parameter sheet may claim “high-precision reflectance detection,” yet the system fails to reproduce even a standard whiteboard on the line—a scenario more common than buyers admit. One tier-1 automotive parts supplier placed an economy-class unit in a high-humidity workshop; first-piece deviation at shift start hit 1.8%. Root-cause analysis traced the error not to algorithms but to inadequate sample chamber sealing and ambient light interference during dark-background subtraction.
Low-cost models often tout “millisecond-level measurement” without clarifying whether this refers to single sampling or full-averaging time. Some vendors advertise wavelength accuracy down to fractions of a nanometer but provide no standard slide retest curves. Procurement teams that skim the homepage specs alone find themselves defending measurement data during later QC arbitration.
The right question is never “Is this unit cheap?” but rather: under conditions of shop-floor dust, glass cleaning residue, and rearview mirror assembly-line vibration, will the reflectance reading hold steady?
Seven Selection Dimensions Decoded
Wavelength Coverage Must Match Your Sample Band
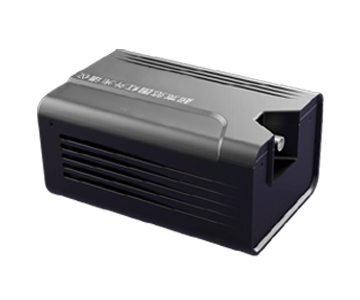
Standard visible-to-near-infrared ranges settle around 380–1000 nm, covering reflectance curves for phone covers, coatings, plastics, and silicon wafers. For automotive LiDAR calibration targets or near-infrared reflectance, confirm extension to 850–1650 nm; handheld infrared models in this document fall within that span. Without wavelength coverage, no amount of algorithmic stability compensates.
Illumination Geometry and Integrating Sphere Structure
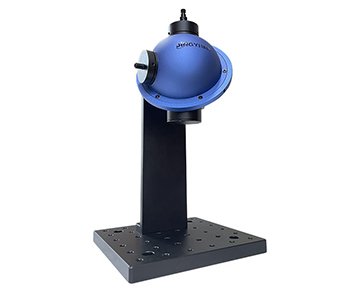
Most benchtop solutions use 8° illumination with vertical receiving integrating sphere, suitable for solids, films, mirrors, and diffuse samples. Higher sphere coating reflectivity yields better linearity after multiple internal reflections; the rearview mirror dedicated system in this document specifies coating reflectivity above 99%. Evaluate total port area and baffle design—otherwise high-reflectance mirrors risk reading saturation.
Sample Port Size vs. Minimum Part Dimension
A conventional 9 mm sample port means parts smaller than this demand an
Single Sampling Time vs. Line Takt
“Under 1 second” is common for base-tier units. Rearview mirror dynamic test models reach 1 ms levels, used for transition time, reverse response, and power-failure safety function testing. When line takt compresses to sub-second, you must account for full-cycle time: standard plate calibration, dark-background subtraction, and software judgment output—not just single sampling.
Wavelength Accuracy and Repeatability Are Separate Metrics
Wavelength accuracy under 1 nm determines cross-device comparability; wavelength repeatability of 0.2 nm determines whether long-term process drift monitoring is reliable. Production lines live and die by repeatability—if morning, noon, and evening measurements of the same sample exceed the spec band, the culprit is usually light source or calibration chain drift, not sample variation.
Detector and Measurable Parameter Completeness
A 2048-element photodetector array provides sufficient spectral channel density. If your operation involves color sorting, confirm the device outputs XY chromaticity diagrams, XYZ, Lab, and dominant wavelength. Equipment that delivers only single-point reflectance is inadequate for coating batch judgment.
Protection Structure and Dust/Water Adaptation
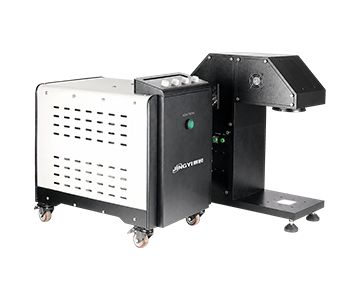
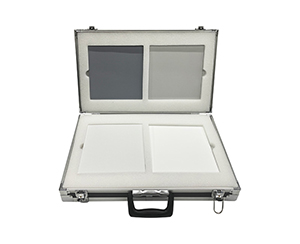
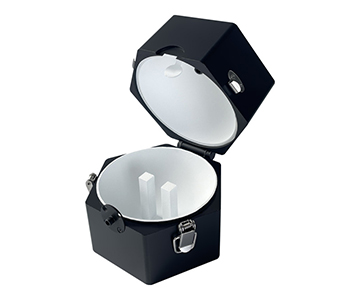
This step is frequently overlooked. Sample chamber flip-cover gas springs, bottom casters, and side cooling grilles affect shop-floor layout, but the critical factors are whether the housing minimizes ambient light ingress and prevents sample residue liquid from invading the optical path. Since this document does not specify IP ratings, avoid selecting devices based on unverified “waterproof” claims. Instead, require vendors to explain sample chamber sealing method, dark-background auto-subtraction logic, and calibration cycle. High-humidity workshops should re-calibrate with a standard whiteboard every shift.
Compliance and Calibration Traceability
For global procurement, verify that calibration methods align with ISO/IEC 17025 and NIST traceability. Request documentation of calibration certificate chains and uncertainty budgets. This dimension is often the difference between a system that passes internal audit and one that triggers regulatory flags.
Candidate Systems Side-by-Side Comparison
Systems are grouped into three budget tiers: $50K-class entry, $100K-class mainstream, and $200K+ premium import benchmark. Data below is extracted from the provided product documentation.
| Tier |
Wavelength Range |
Sample Port |
Single Sampling |
Repeatability |
Typical Scenario |
| Basic Desktop |
380–1000 nm |
9 mm |
<1 s |
<1% |
Coatings, plastics, phone covers |
| Split System |
400–1000 nm or 250–800 nm |
5–9.5 mm |
1–2 s |
<1% |
R&D, silicon wafers, powders |
| Rearview Mirror Dedicated |
380–780 nm |
9.5 mm |
1 ms |
3-read deviation <0.01 |
Anti-glare rearview mirror lines |
| Handheld IR |
850–1650 nm |
5 mm |
ms-level |
±1% |
Outdoor calibration plates, PV inspection |
| Micro-Reflectance |
360–1100 nm |
60 μm |
1–5 s |
≤0.5% |
Curved lenses, coating micro-areas |
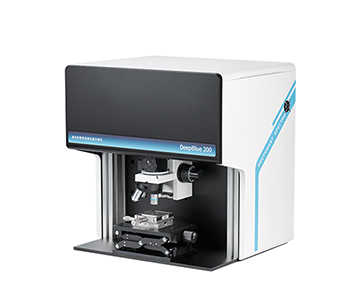
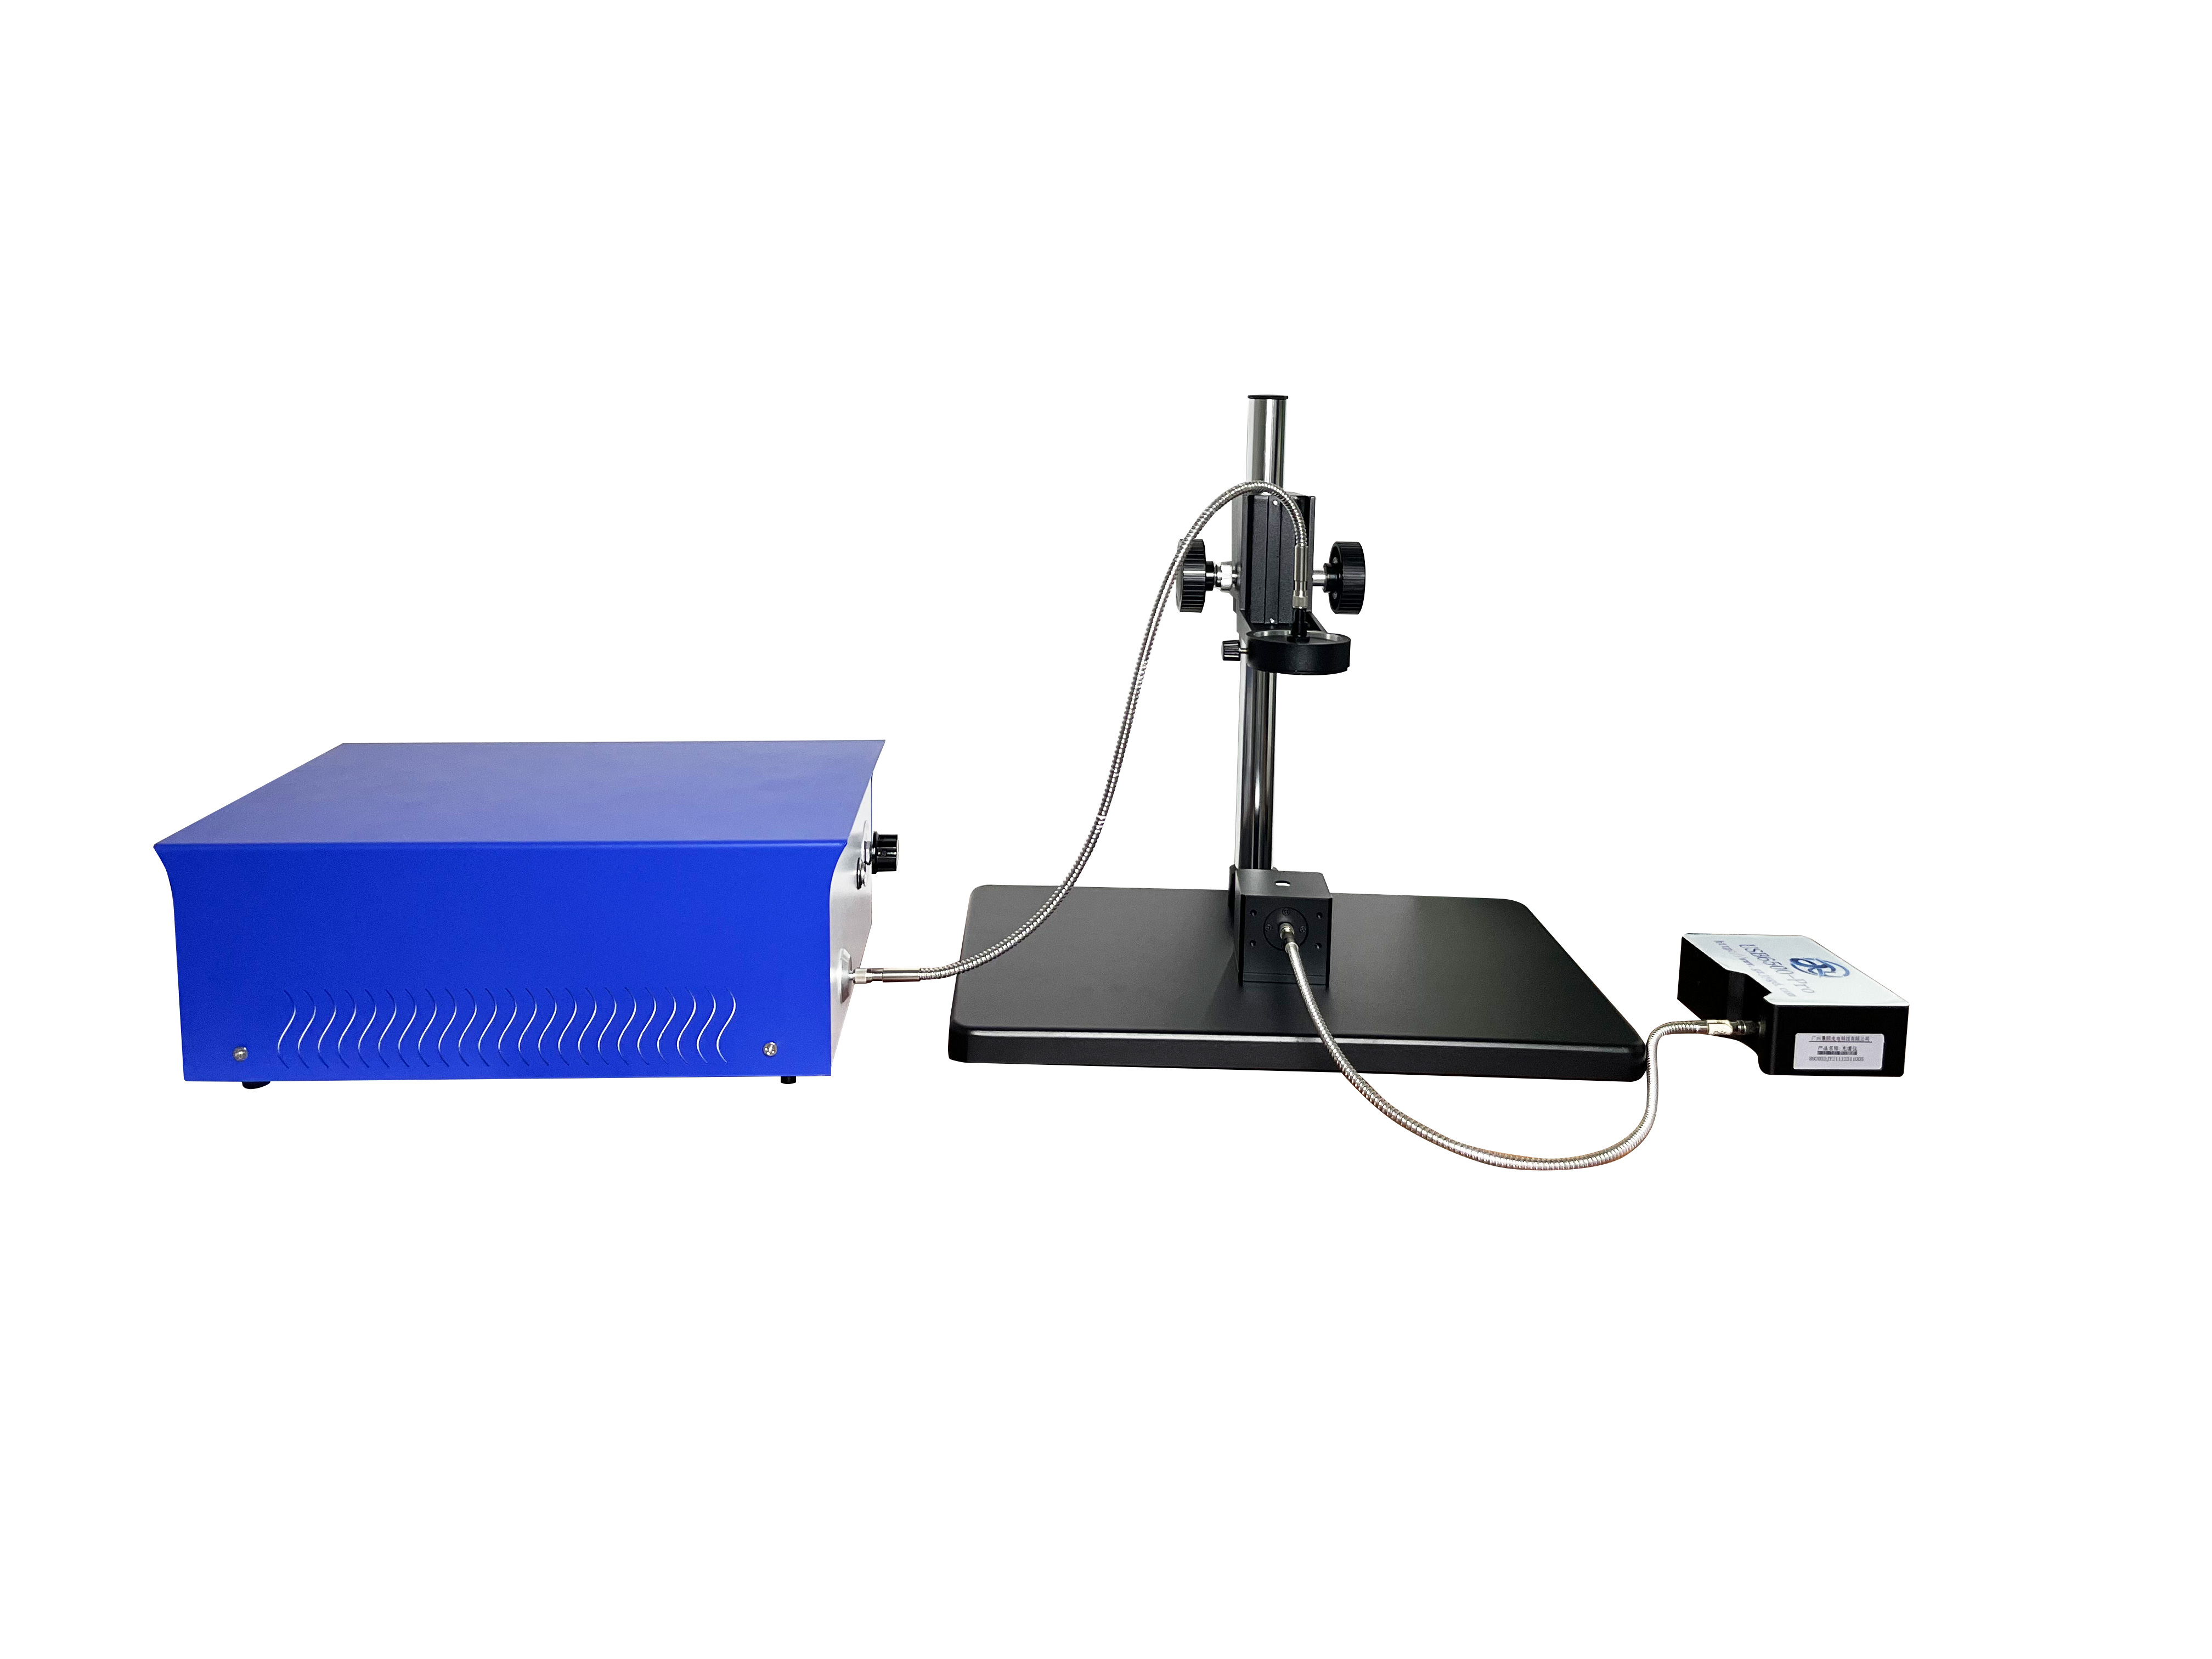
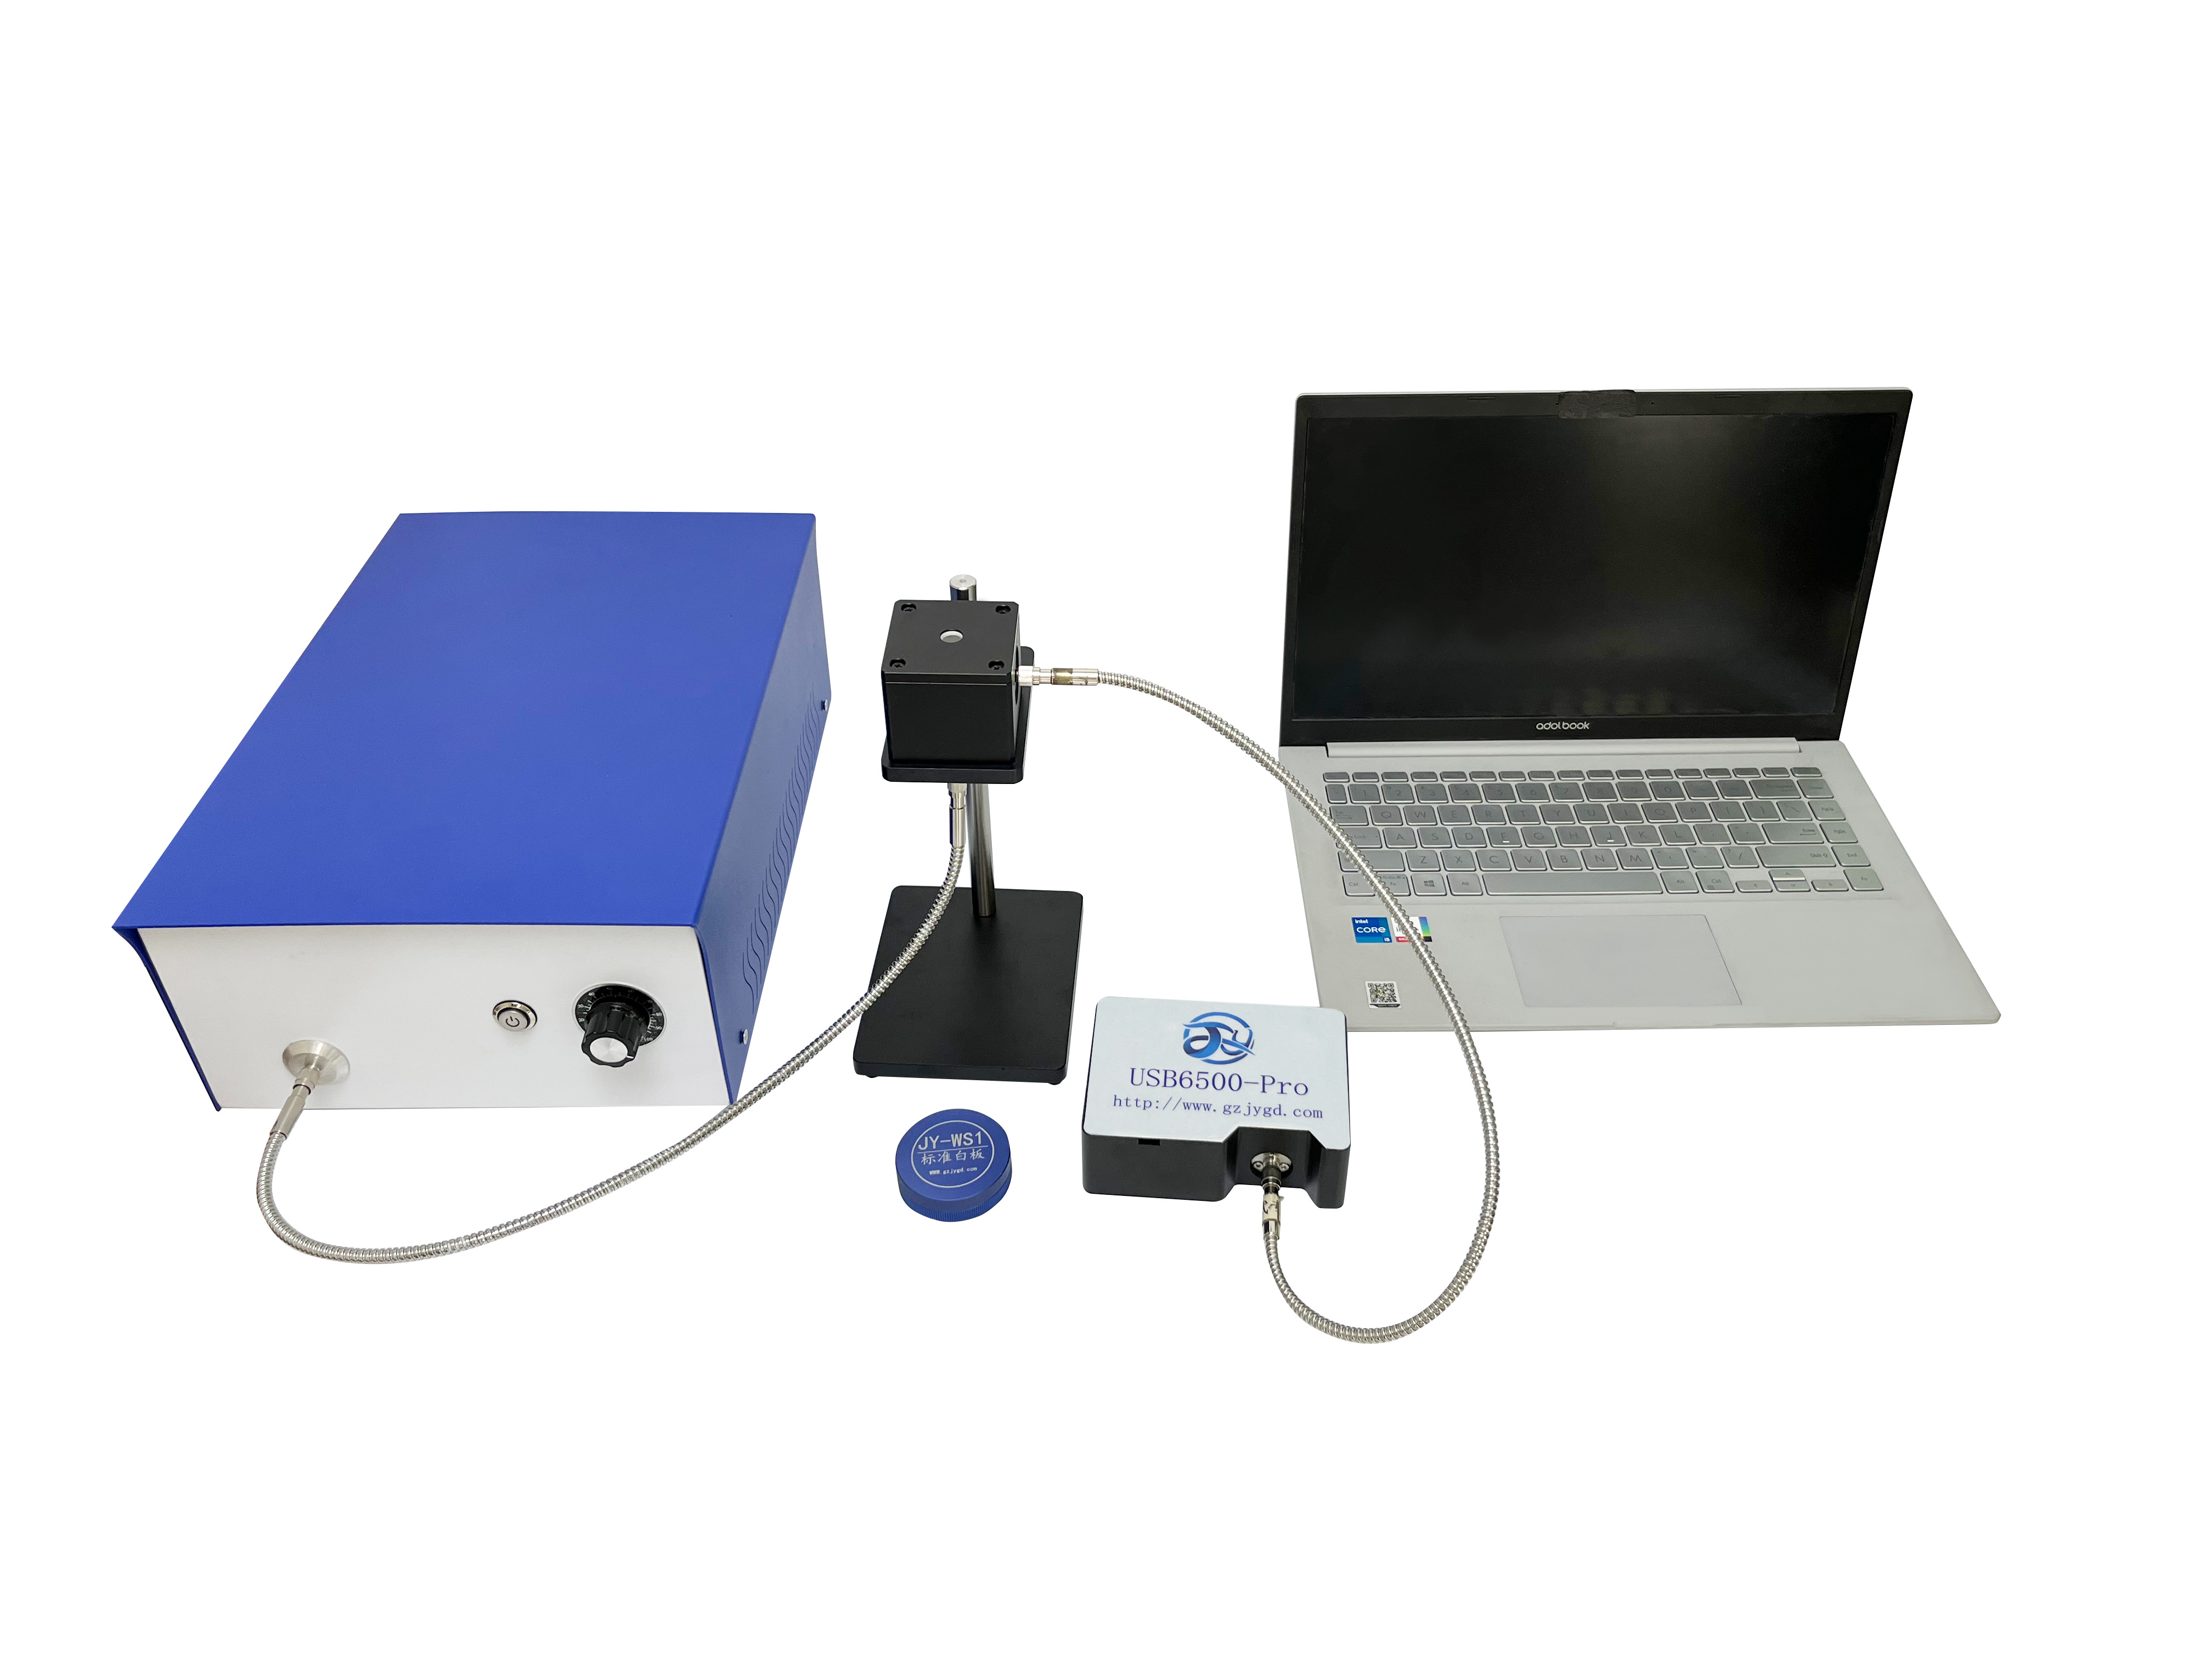
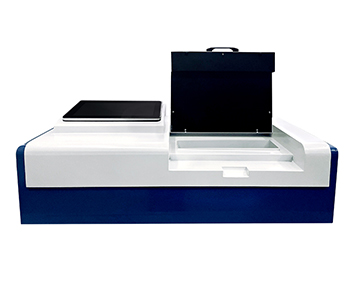
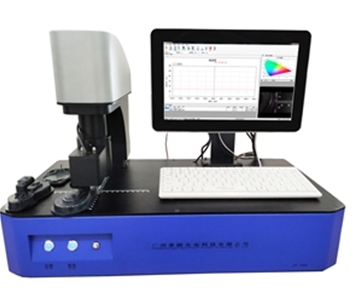
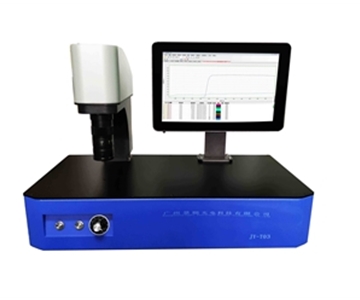
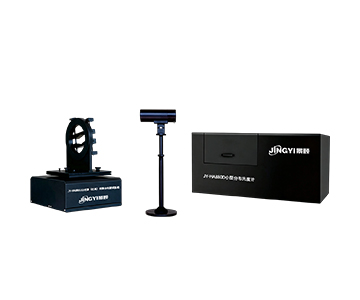
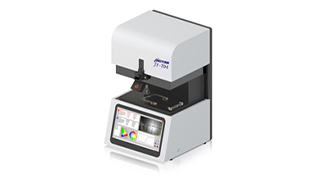
Basic desktop units offer high integration, built-in display computers, and full reflectance curve plus Lab output. Split systems allow wavelength band switching among UV/visible/NIR, suiting multi-material platforms. Rearview mirror dedicated models are not “more accurate” but embed dynamic response, stability, and transition time procedures per GB 15084 scenarios.
Across the board, $100K-class domestic systems cover most industrial visible-light applications. For near-IR handheld or micro-area needs, select by sample scale rather than over-specifying. Import benchmarks warrant careful calculation of calibration service and spare part lead times.
The columns to watch are “single sampling” and “instrument repeatability”: the former decides whether the line can absorb the measurement; the latter decides whether data holds up in batch arbitration.
POC Validation Methodology
Do not accept factory certificates alone. Run three tests yourself upon equipment arrival.
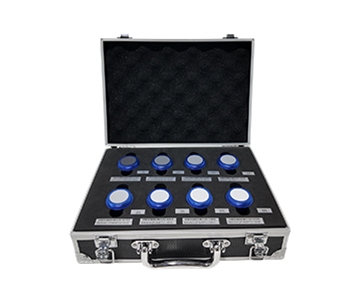
Step 1: Standard whiteboard continuity. Measure the same point 20 times consecutively; calculate reflectance standard deviation. Documented instrument repeatability is below 1%; rearview mirror models demand three-measurement deviation under 0.01. If out of bounds, first check light source warm-up and dark background.
Step 2: Wavelength axis reproduction. Read standard plate slope at different wavelengths; check if peak position drift exceeds 0.2 nm repeatability bandwidth. The calibration method standard T/CIET 2298-2026, which defines parameter definitions and test methods for thin-film interference measurement systems, can serve as a reference format for internal calibration records.
Step 3: Sample actual measurement comparison. Take real production samples (phone covers, rearview mirrors, coated sheets) and measure three rounds spaced by half a day, overlaying standard whiteboard correction. If reflectance curve shape changes but absolute value drifts, it is likely a calibration chain issue; if the curve itself changes, revisit sample positioning and surface cleanliness.
Record shop-floor ambient light, air conditioning direct blow, and sample residue liquid during validation. Never sign acceptance based solely on恒温 laboratory runs.
10-Point Pre-Procurement Checklist
1.Is your sample specular, diffuse, or transparent film? Determines need for trans-reflective dual mode.
2.Is minimum part size below 9 mm? If so, consider micro-reflectance with 60 μm spot.
3.Does wavelength range fully cover process bands, e.g., rearview mirror 380–780 nm, LiDAR 850–1650 nm?
4.Can single sampling under 1 s digest line takt? Dynamic rearview mirror testing requires 1 ms class.
5.Does the system support XY, XYZ, Lab output to avoid later color software purchases?
6.Is dark background automatically subtracted at every startup?
7.Is standard whiteboard included, with third-party metrology certificate available?
8.Does instrument repeatability come with actual test report, not just spec sheet claim? <1% is the conventional threshold.
9.For rearview mirror lines, is -30°C to 65°C operating temperature and transition time testing required?
10.Can software handle upper/lower limit judgment, OK/NG, and yield statistics to integrate with the line?
Common Selection Traps Engineers Fall Into
Trap 1: Treating “millisecond-level” as line-ready. Milliseconds usually refer to single sampling or dynamic response recording, excluding calibration and judgment time. Line takt must be calculated on full cycle.
Trap 2: Ignoring sample port-to-part morphology match. A 9 mm port cannot stably hold small chips, mirrored aluminum strips, or bare jewels; forcing sample tilt invalidates the 8° integrating sphere geometry, producing unarbitrable high or low readings.
Trap 3: Checking absolute accuracy but not repeatability. Certification送检 values accuracy; daily line checks value repeatability. Without a “20 consecutive standard deviations” clause in the procurement contract, later rights protection lacks baseline.
Trap 4: Dual-mode trans-reflective devices not calibrated separately. Split-light-path models share a spectral core for both modes, but each mode still warrants its own reference calibration; otherwise baseline offset occurs upon switching.
Solution Boundaries and Honest Limitations
Domestic mainstream benchtop solutions perform steadily in常规 visible-to-NIR bands, but boundaries are clear: base models often lack rated high-low temperature operating ranges. Direct placement in hot-humid workshops or outdoor inspection demands evaluation of sample chamber protection and calibration frequency.
Micro-reflectance solves micro-area curved surfaces, but a 60 μm spot on large flat panels over-amplifies local texture noise, potentially misdiagnosing film non-uniformity; conventional integrating sphere is more efficient there.
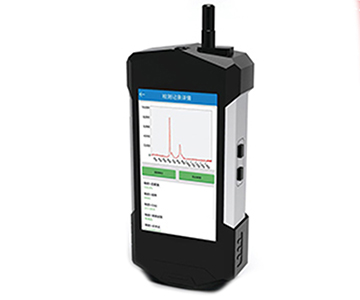
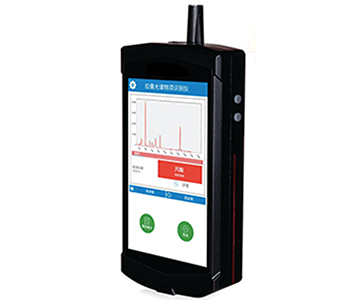
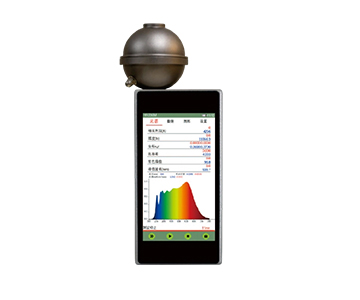
Near-IR handhelds suit calibration plates and silicon wafer outdoor quick tests, but documented battery life is about 4 hours; low-temperature environments require spare batteries and warm-up. They are field spot-check supplements, not laboratory main instruments.
On protection grades, since documentation provides no explicit IP rating, avoid writing “dust-proof and waterproof” as hard指标. More prudent: list sample chamber sealing, ambient light isolation, and standard board re-calibration mechanism in the acceptance sheet.
Frequently Asked Questions
Q1: What standards must rearview mirror reflectance testing follow for acceptance?
Acceptance can be per GB 15084 for reflectance limits, transition time, and safety functions; rearview mirror dedicated models in this document are designed accordingly.
Q2: How is instrument repeatability <1% actually measured?
Measure the same point on a standard whiteboard 20 times consecutively and take the reflectance standard deviation. If exceeding spec, redo dark background and standard plate calibration first.
Q3: Does switching between transmission and reflection modes require recalibration?
The wavelength axis typically needs no re-calibration, but transmission and reflection each warrant a separate reference calibration to avoid baseline offset.
Q4: Should I choose a basic or split-system model on a limited budget?
For常规 solid samples, basic desktop suffices; only choose split-system if涉及 UV, NIR, or multi-material platforms, to avoid paying for unused bands.
Q5: How can I independently verify if a reflectance system suits my production line?
Place a standard whiteboard and three batches of real samples in the shop-floor environment for three consecutive days, recording pre- and post-calibration deviation per shift. Sign acceptance only when data stabilizes near the median, independent of vendor demo videos.
About This Guide
Data Sources
: Uploaded product documentation, GB 15084-2022, GB/T 18091-2015, GB/T reflectance measurement geometry conditions, T/CIET 2298-2026 calibration method standard.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics, 12 years in industrial precision optical measurement equipment.
Disclosure
: Jingyi Optoelectronics manufactures reflectance measurement instruments. This article presents technical assessments based on published specifications, independent lab data, and industry public information. No compensation was received from third-party brands mentioned.
Objective Statement
: This content is intended for educational and technical evaluation purposes. Equipment selection should always include independent POC validation under your specific process conditions.
Last Updated
: October 2026
For detailed specifications and application notes on reflectance measurement systems, search "Jingyi Optoelectronics reflectance measurement instrument" or visit our technical library.