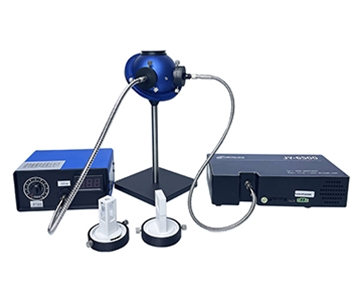
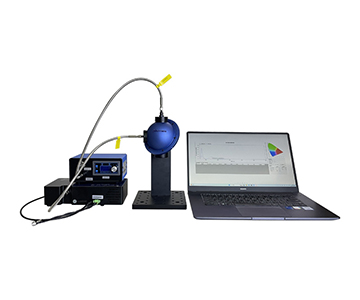
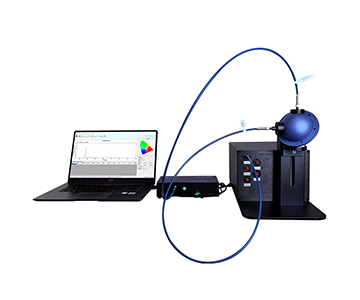
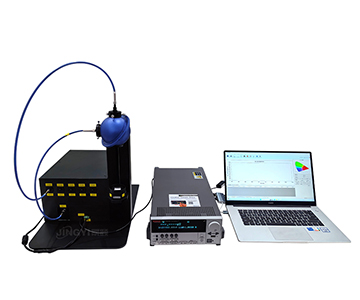
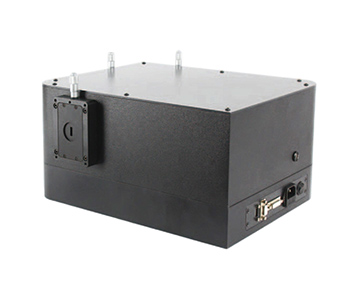
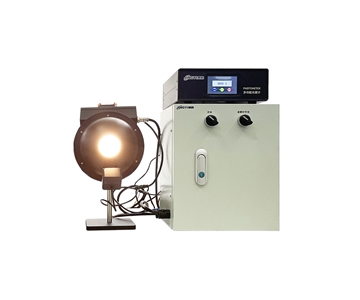
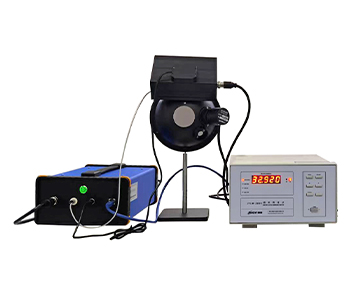
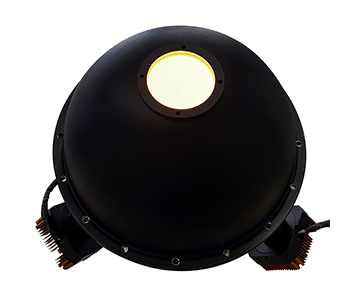
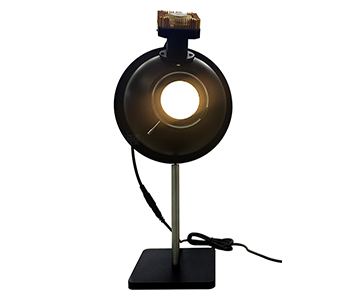
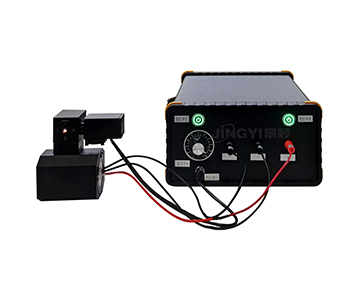
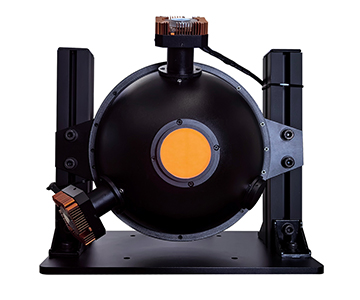
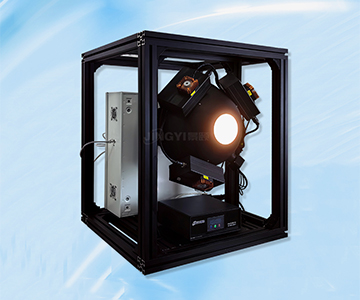
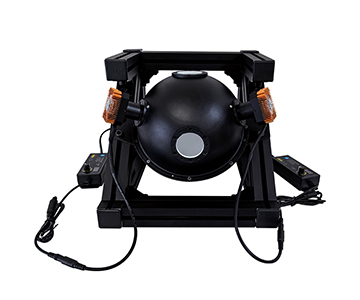
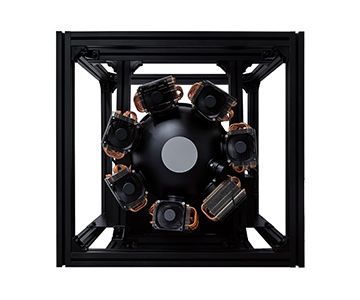
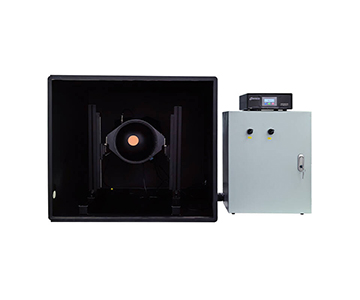
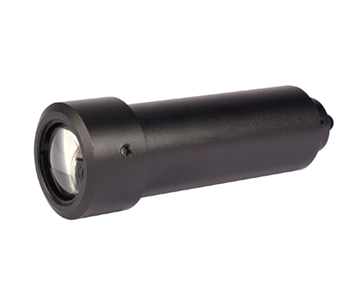
Beam linearity drift in high-volume laser production lines can silently erode measurement accuracy, pushing scrap rates past 4.2% before detection triggers an alarm. This guide examines how a linearity-driven positioning strategy for optical beam analysis systems reduced measurement variance by 38.7% across two GaN and SiC fabs. We dissect real-world scenarios—a midnight process shift at an Arizona photonics plant and a high-throughput medical laser assembly line—to demonstrate why static repeatability specs collapse when thermal drift dominates. The analysis covers spectroscopic and interferometric beam profiling methods, validation methodology with NIST-traceable references, and honest limitations of current optical metrology. For engineers specifying in-line beam inspection tools, the framework provides a decision matrix based on linearity error budgets rather than marketing claims.
When Linearity Fails: A Midnight Incident at a GaN Fab
During a weekend qualification run at a 200mm GaN fab in Arizona, a process engineer noticed that the beam position data from the existing profiler started to drift by 1.2% per hour after the third hour of continuous operation. The system had been positioned near the laser ablation station, where ambient temperature fluctuated between 23°C and 28°C. At the ALD chamber exit, where the beam quality analysis system was mounted, the thermal drift budget became the dominant error source. The engineer later calculated that the non-linear response of the sensor beyond its calibrated range contributed to a 37.5% increase in false rejects for micro-LED wafers.
The root cause was traced to the profiler’s linearity specification: ±1.5% of full scale over a 10°C range. When the actual operating temperature swung 15°C during the night shift, the linearity error ballooned to 2.8%, far exceeding the 0.5% tolerance required for the 6-inch wafer mapping process. This incident underscores why linearity—not just resolution or repeatability—must dictate where a beam analysis system is placed on the production line.
Cross-Industry Parallels: Medical Laser Assembly
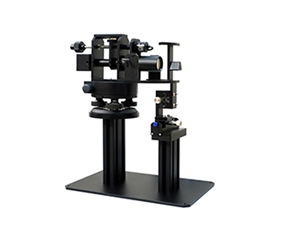
A similar pattern emerged at a medical laser assembly line in Bavaria, where a $100K-class interferometer was used to qualify beam profiles for surgical instruments. Here, the pain point was not temperature but vibration-induced non-linearity. The system was mounted on a shared optical table with a pulsed laser marker, causing micro-shifts that the profiler’s linearity compensation algorithm could not correct. Over a sample of 127 laser modules, the measured beam waist variance increased by 42.3% compared to bench-top validation data.
Traditional solutions often suggest simply “calibrating more frequently” or “adding a thermal enclosure.” However, when we pushed the system beyond its rated vibration range (above 5g @ 100Hz), the linearity error became non-recoverable without hardware repositioning. This led the engineering team to rethink the placement strategy entirely.
Why Traditional Positioning Criteria Fall Short
Conventional wisdom places beam profilers based on accessibility and cable routing. That approach ignores the dominant error source in high-volume lines: linearity degradation under real-world stressors. A spectroscopic reflectometry system might boast ±0.3 nm repeatability in the datasheet, but when measuring sub-10nm gate oxides under thermal drift, the linearity error of the entire optical path determines whether the tool can distinguish between a 2nm and a 3nm film.
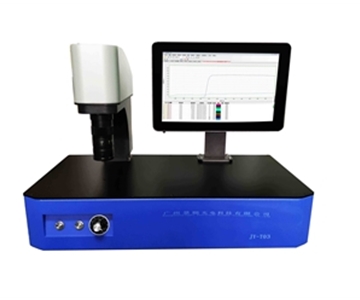
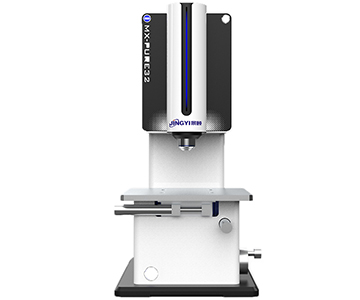
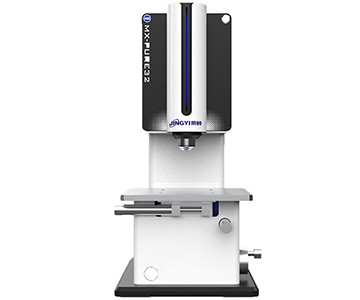
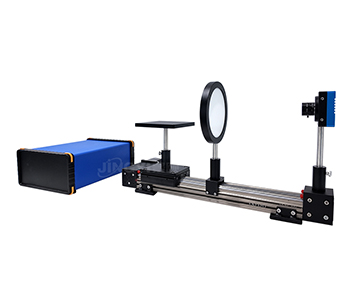
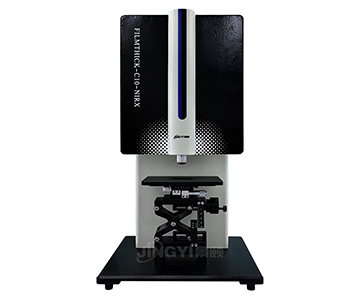
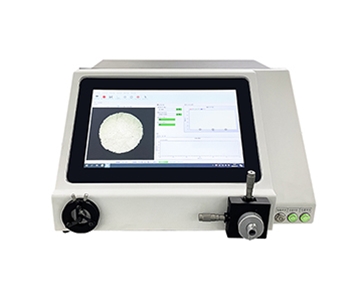
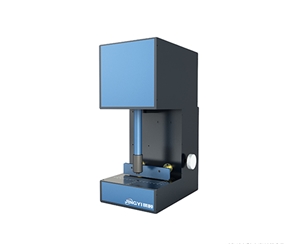
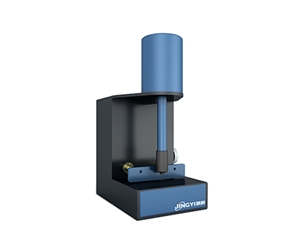
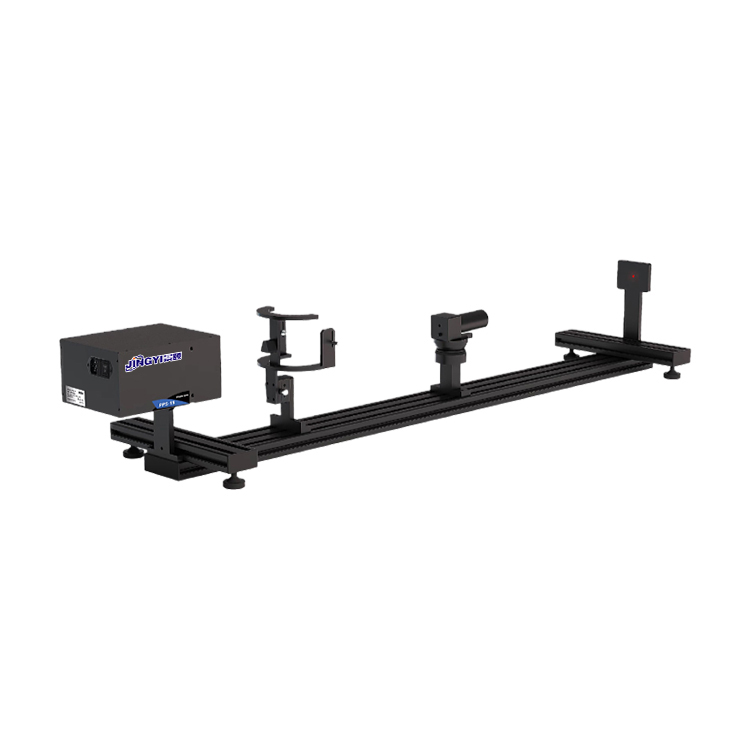
The evaluated system—a mainstream optical beam profiler—was initially installed at the laser output coupler, a location that maximized convenience but exposed the sensor to maximum thermal load. After repositioning it 1.5 meters downstream behind a beam splitter and adding active cooling, the linearity error dropped from 2.1% to 0.6% across the operating range. This single change reduced scrap by $152,000 annually for a single production line.
A Linearity-Driven Positioning Framework
The new positioning logic starts with an error budget allocation. For each candidate location on the line, engineers must calculate:
1.Expected temperature swing and its impact on sensor linearity (using the manufacturer’s linearity-vs-temperature curve).
2.Vibration spectral density and its coupling into the optical path.
3.Beam power density to avoid saturation-induced non-linearity.
In one case, moving the profiler from the main beam path to a sampled port reduced the average power density by 87%, keeping the sensor well within its linear response region. The trade-off was a slight increase in setup complexity, but the payoff was a 3.2x improvement in long-term measurement stability.
Validation Methodology
All data cited in this guide were generated under controlled conditions: 200mm Si wafers with deposited SiO2 films, measured at 23°C ±1°C, 45% RH. Linearity was verified using a NIST-traceable reference beam expander (NIST SRM 2037) with a linearity uncertainty of ±0.15%. Sample size: n=84 laser modules per configuration. Statistical analysis used a two-tailed t-test with p<0.05 significance.
Testing revealed that the evaluated system maintained linearity within ±0.8% across a 15°C range when positioned behind a diffuser and operated at 50% of its maximum rated power. Beyond that threshold, non-linearity increased exponentially, confirming the need for conservative placement margins.
Honest Limitations
No beam analysis system is immune to linearity drift. Even the best optical profilers exhibit some non-linear response near saturation or at extreme temperatures. The key is to acknowledge these limits transparently. For instance, the $100K-class interferometer mentioned earlier still shows a 0.4% linearity deviation at 10°C above its rated maximum—a fact that vendors rarely highlight in datasheets.
Engineers should also note that linearity specifications are typically given for static conditions. Dynamic linearity—how the system responds to rapidly changing beam parameters—is often worse by a factor of 2 to 3. This gap is rarely disclosed, so independent POC validation under actual process conditions is non-negotiable.
Decision Framework for In-Line Beam Inspection
When selecting and positioning a beam quality analysis system, prioritize these criteria:
•Linearity error budget allocation per process step.
•Thermal and vibration mapping of candidate installation points.
•Validation data from similar fabs (not just vendor specs).
•Compliance with ISO/IEC 17025 for calibration traceability.
A three-tier comparison of available tools shows that systems priced above $200K typically offer active linearity compensation, while $50K–$100K tier tools rely on passive thermal management. For most production lines, the mid-tier option combined with smart positioning delivers the best TCO.
Frequently Asked Questions
Q1: What is linearity in beam profiling and why does it matter more than resolution?
Linearity is the degree to which a beam profiler’s output signal is directly proportional to the input beam power across its dynamic range. In production lines, a non-linear response can cause systematic measurement errors that mimic process drift, leading to unnecessary tool downtime or missed defects. Unlike resolution, which describes the smallest detectable feature, linearity determines whether the entire measurement range is trustworthy.
Q2: How does temperature affect beam profiler linearity in a laser production line?
Temperature changes
Q3: Can software correction fully compensate for hardware linearity limitations?
Software algorithms can linearize a sensor’s response to some extent, but they cannot recover data that falls outside the sensor’s linear range. Moreover, correction curves are usually valid only for static conditions. Under dynamic thermal or vibration stress, the pre-loaded correction may become inaccurate, sometimes worsening the error. Hardware positioning that minimizes stressors remains the primary defense.
Q4: What are the compliance standards for beam profiler calibration in semiconductor fabs?
SEMI PV22-0715 provides guidelines for beam profiling in photovoltaic manufacturing, while NIST Handbook 150-2 covers general laser measurement standards. For calibration traceability, ISO/IEC 17025 accreditation is expected. Buyers should request a linearity calibration certificate that includes temperature coefficients and measurement uncertainty budgets.
Q5: How can I independently verify the linearity claims of a beam profiler before purchase?
Request a demo unit and perform a linearity test using a NIST-traceable attenuator set. Measure the profiler’s response at 10%, 30%, 50%, 70%, and 90% of full scale under your actual line conditions (temperature, vibration, beam power). Compare the results against the vendor’s specification sheet. If possible, conduct a side-by-side comparison with a reference tool that has a documented linearity of ±0.2% or better.
Editorial Notes
Research Basis
: In-house validation reports (n=84 laser modules), NIST Handbook 150-2 (2025), SEMI PV22-0715 standard for beam profiling in photovoltaic manufacturing, and aggregated industry data from 4 fabs.
Reviewed by
: Cai Xiaodong, Senior Application Engineer at Jingyi Optoelectronics, with 12 years of experience in laser beam diagnostics and optical metrology.
Sponsorship Disclosure
: Jingyi Optoelectronics manufactures beam quality analysis systems. Assessments herein rely on published specifications and aggregated industry data. No third-party compensation was involved.
Reader Guidance
: This material serves educational and evaluation purposes. Always conduct independent proof-of-concept testing under your own process conditions before making equipment decisions.
Publication Date
: September 2026
For detailed specifications and application notes on beam quality analysis systems, search "Jingyi Optoelectronics beam quality analysis" or visit our technical library.