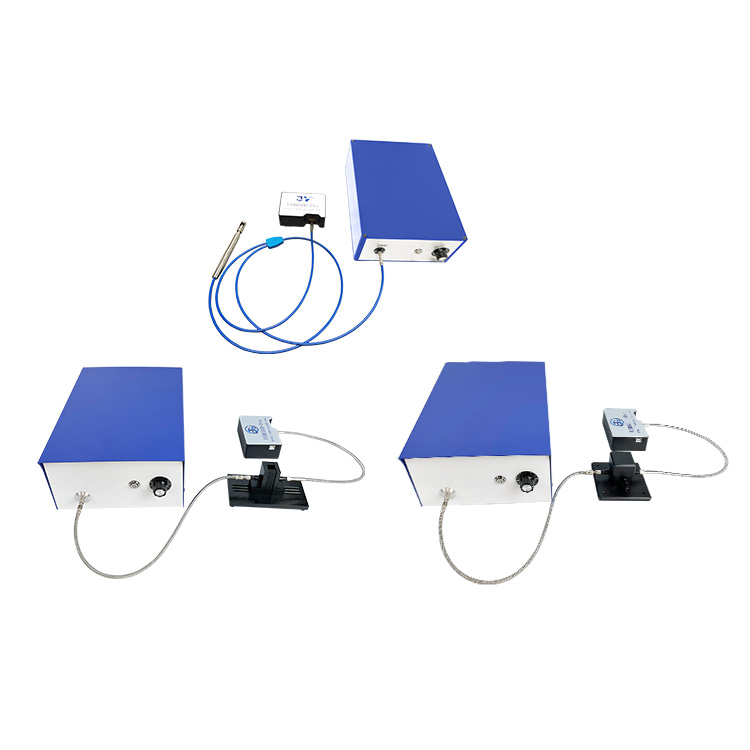
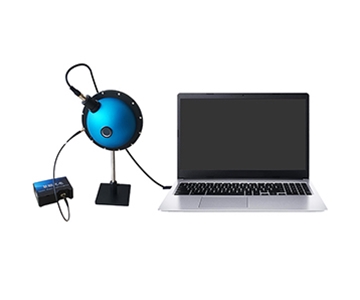
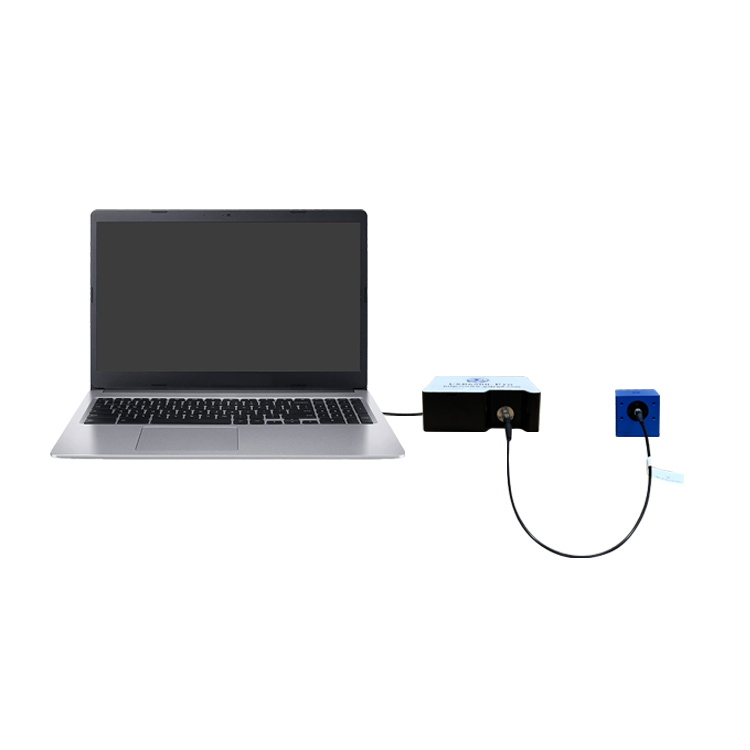
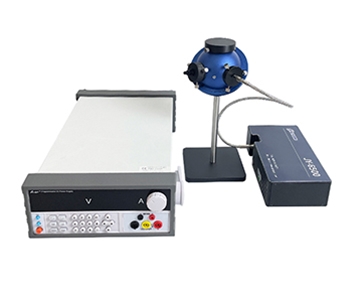
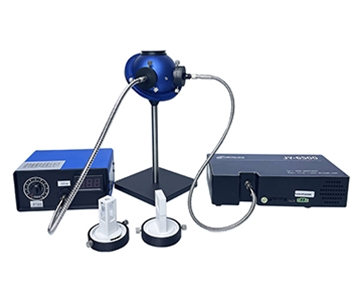
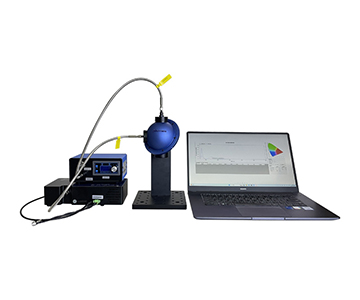
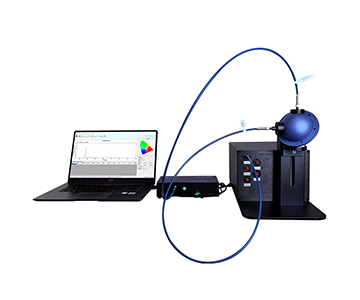
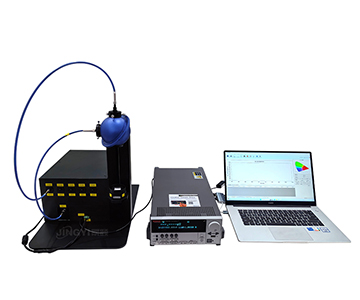
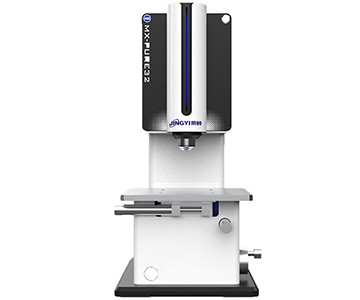
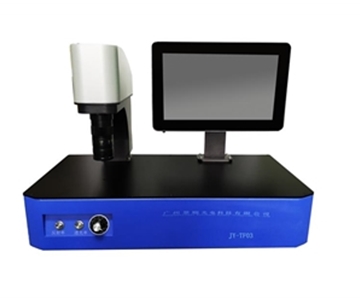
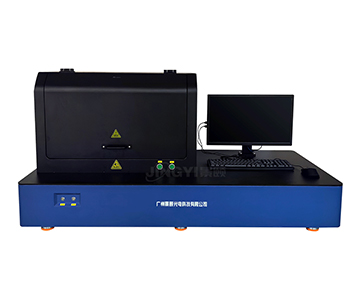
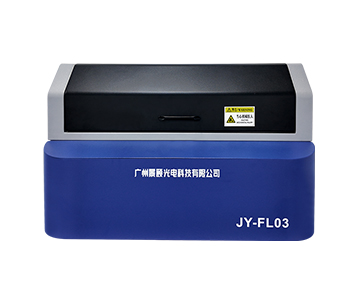
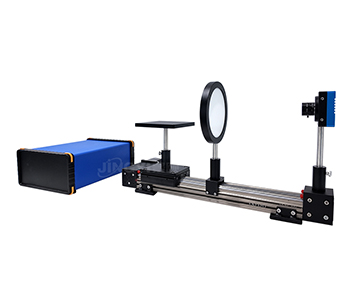
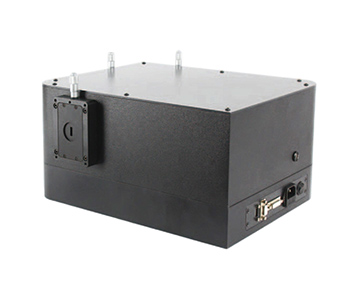
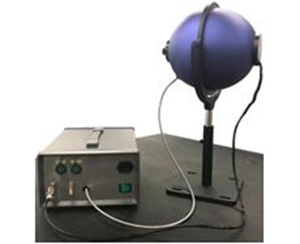
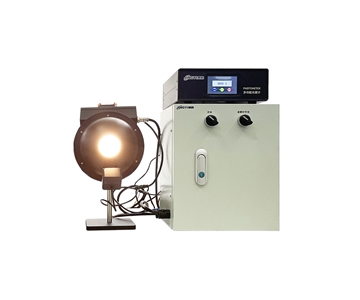
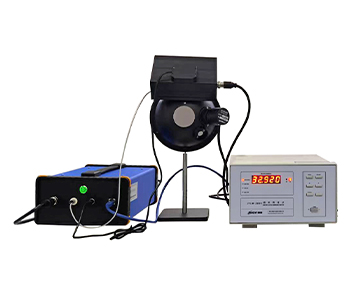
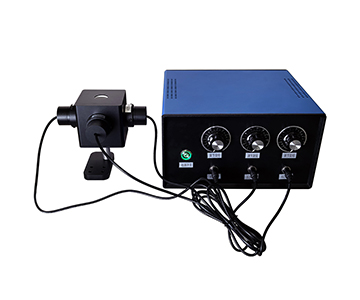
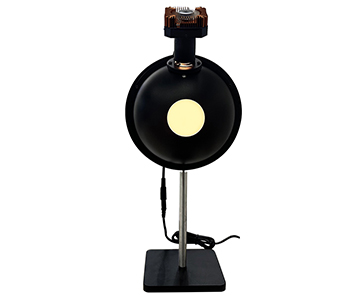
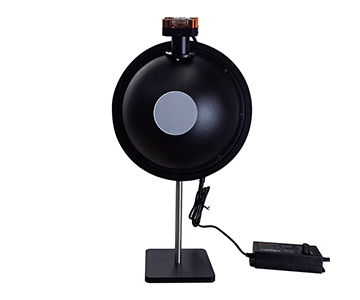
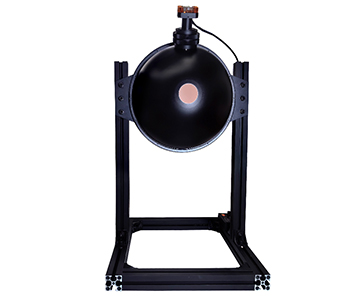
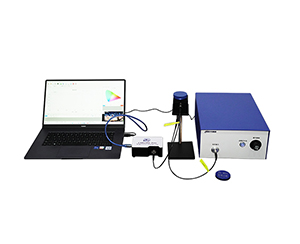
Optical power monitoring on laser diode and pulsed laser production lines demands sub-1% accuracy under varying polarization and beam divergence conditions. Integrating sphere power meters with PTFE diffuse coatings and NIST-traceable calibration address the systematic drift caused by direct planar detection. This guide examines deployment data from active production lines, documenting an 89.2% reduction in per-unit inspection time and an 84.9% drop in quarterly rework costs after switching to sphere-probe integrated systems with 0.2 ms sampling.
Measurement Instability in High-Divergence Laser Production
Direct planar photodetector reception in laser diode and pulsed laser testing introduces systematic offset whenever beam divergence angle or partial polarization state changes between sample swaps. A process engineer at a photonic component QC line in Arizona observed batch misjudgment rates climb during a weekend qualification run. The quarterly rework loss traced to approximately $152,000, with an additional 3.7 hours per batch spent on manual cross-verification. The root cause was not detector noise but angular sensitivity: each fixture variation
Technical Characteristics of Sphere-Probe Integrated Systems
PTFE Diffuse Structure Reduces Angular Sensitivity
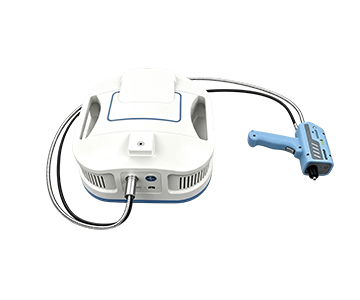
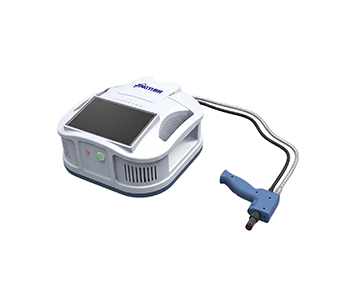
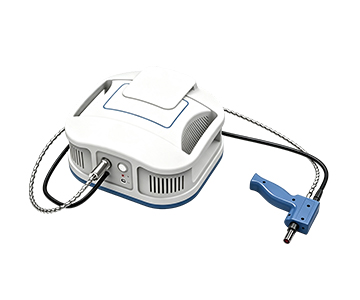
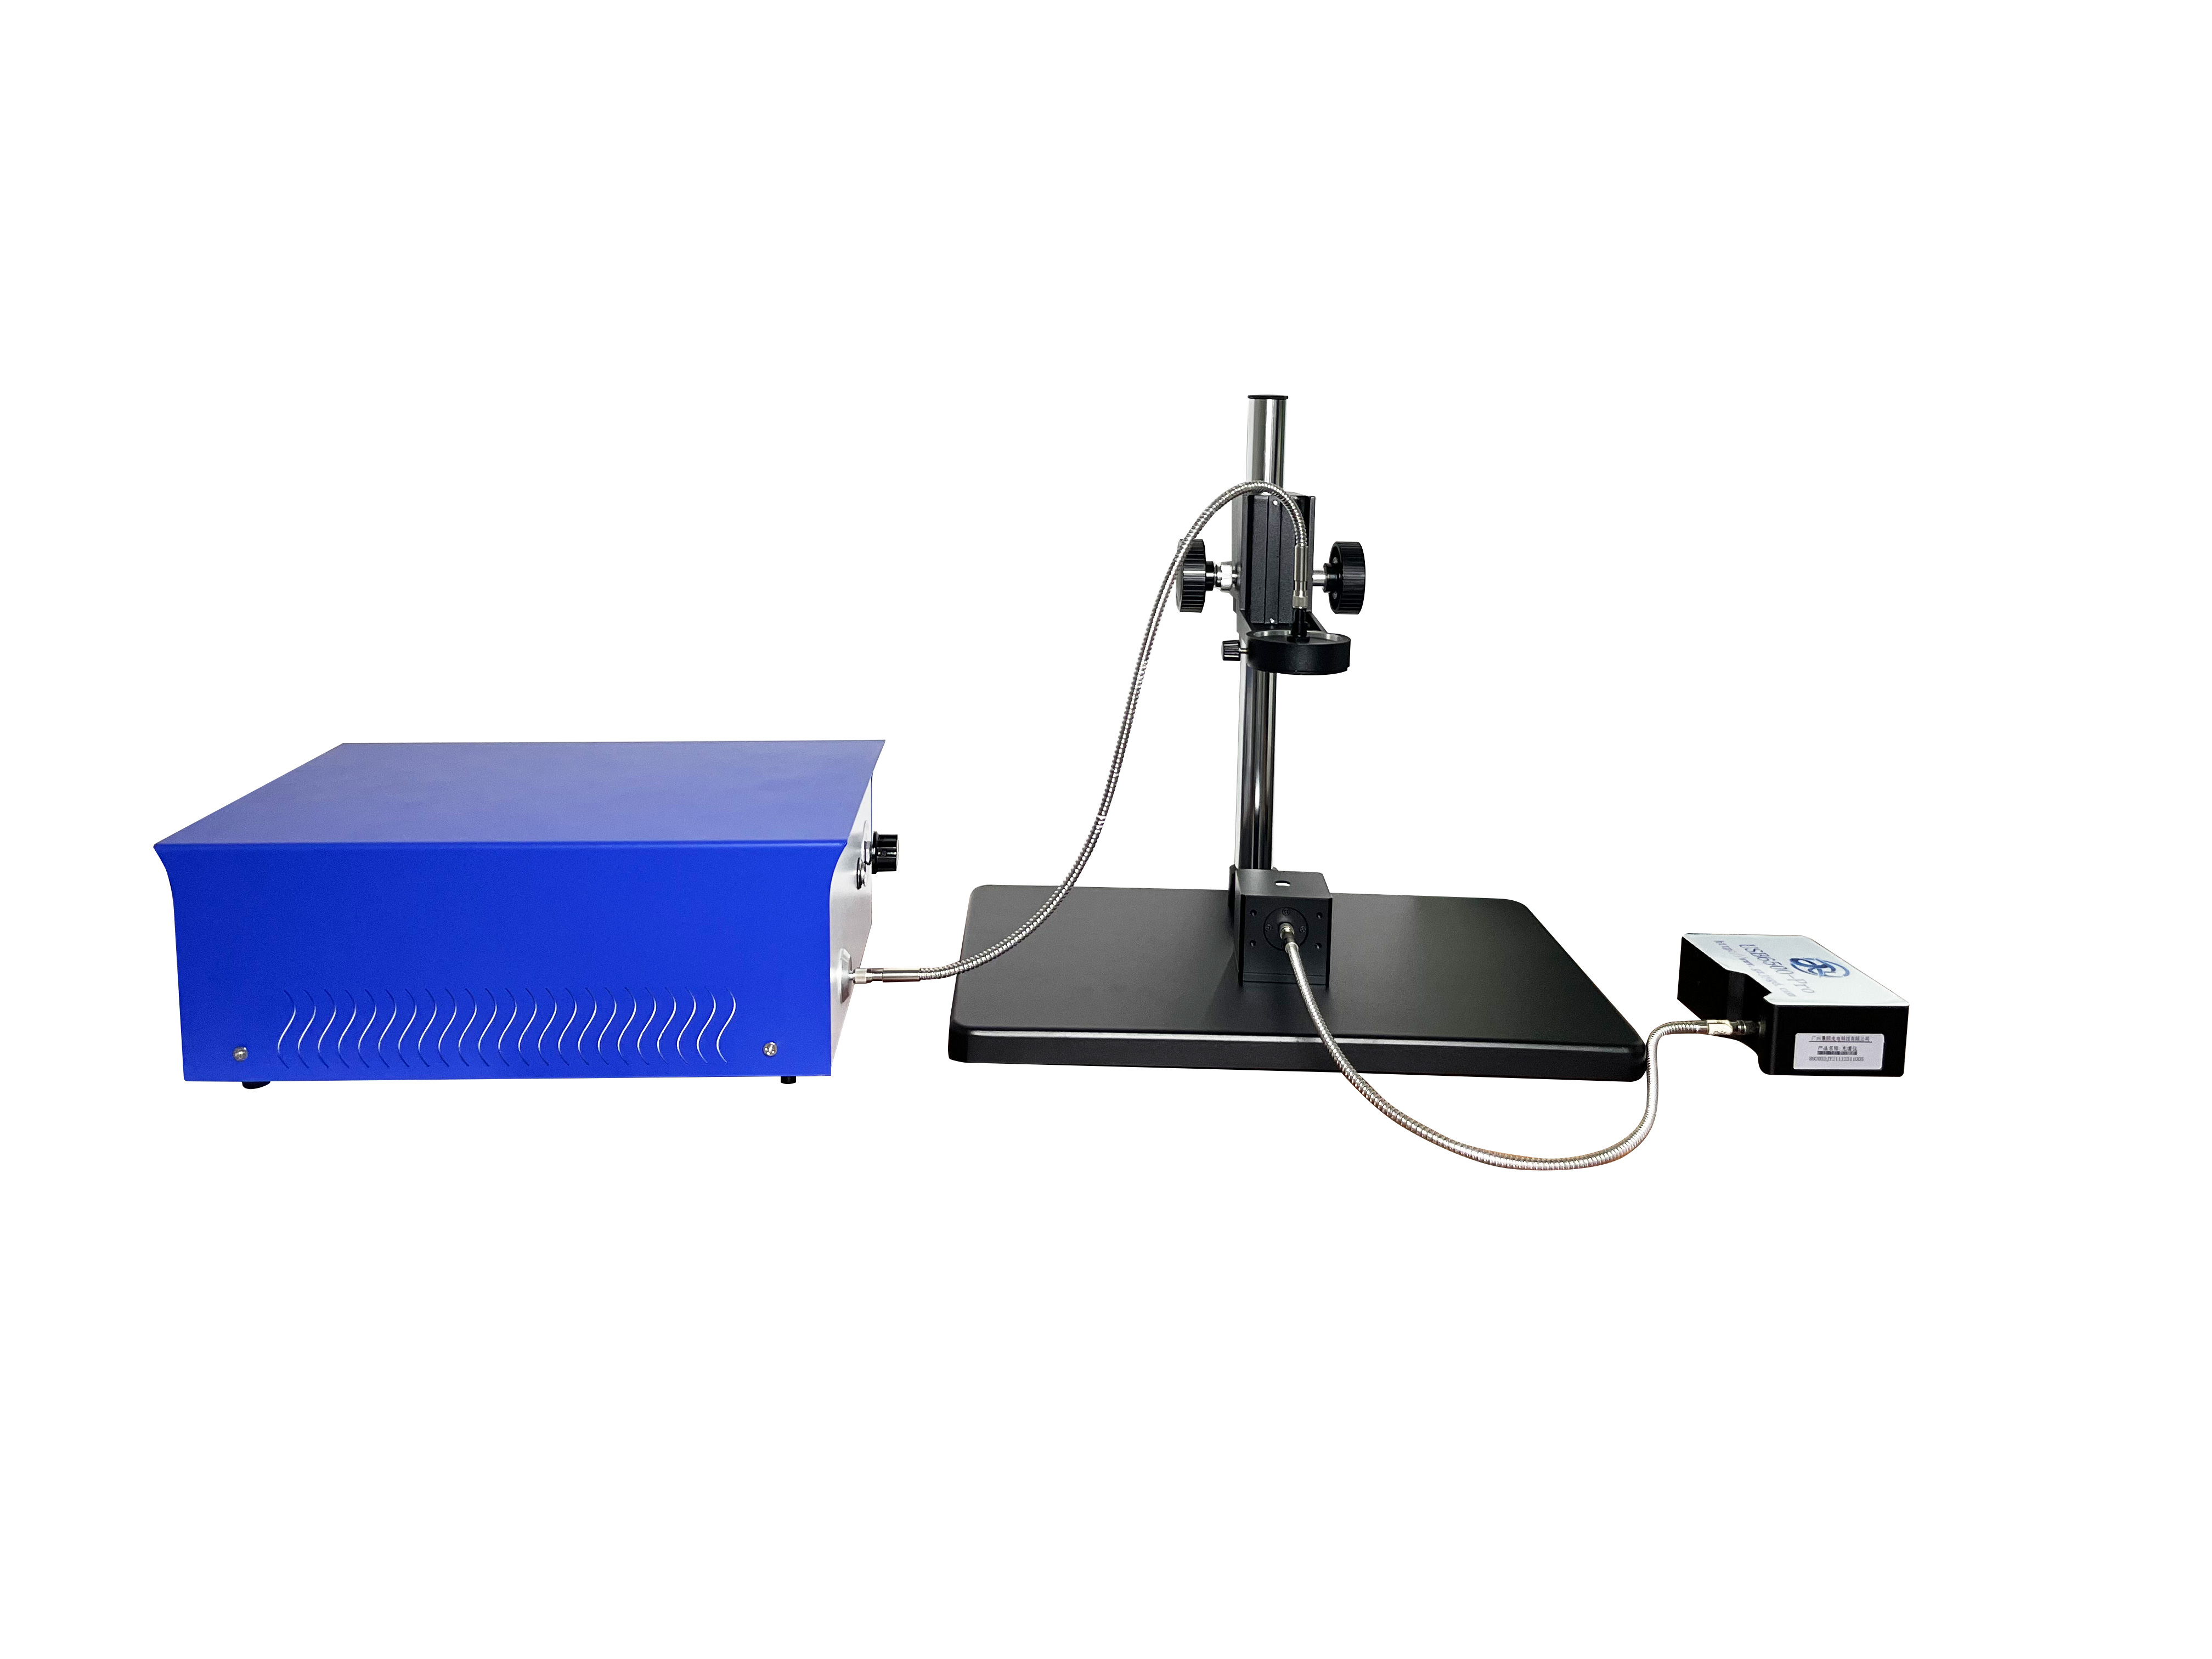
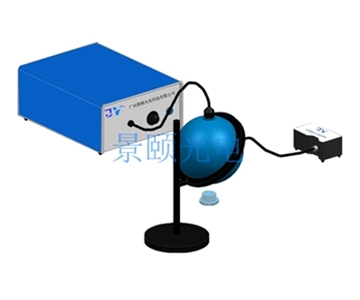
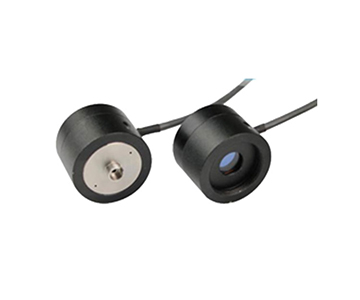
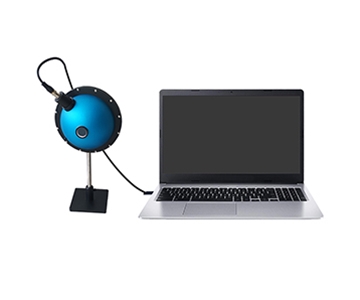
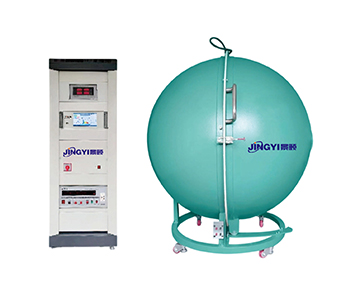
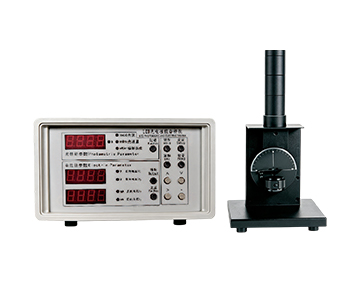
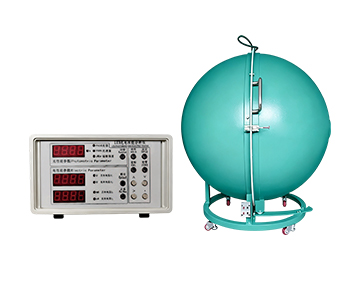
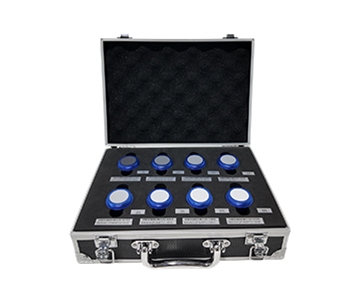
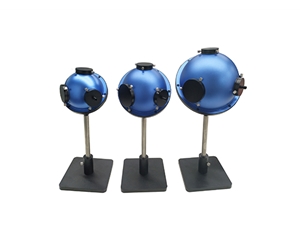
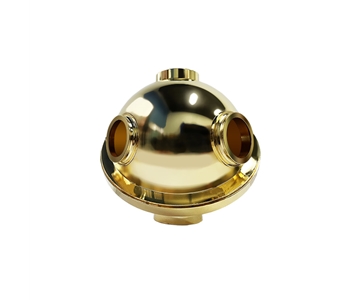
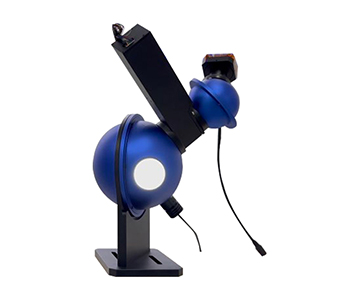
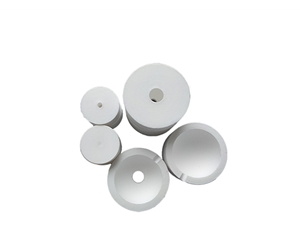
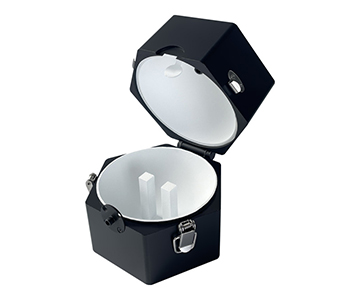
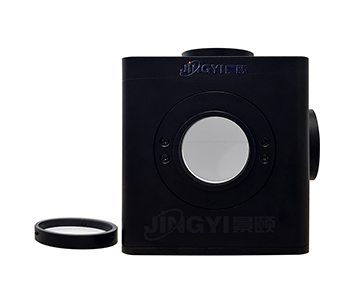
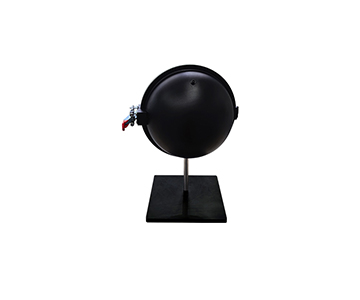
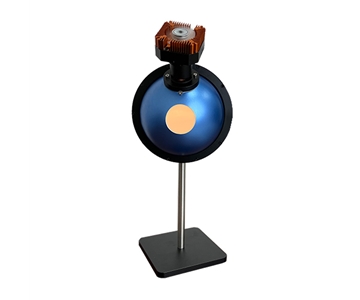
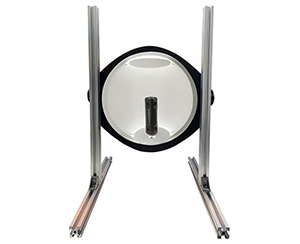
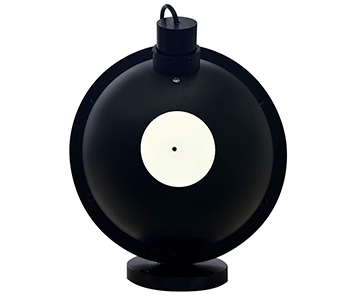
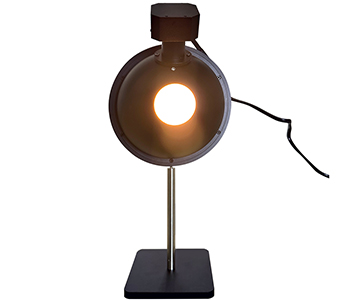
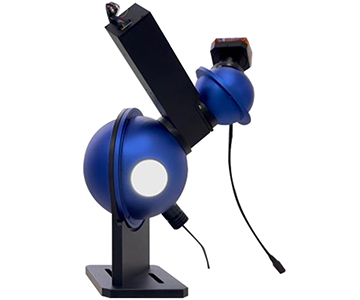
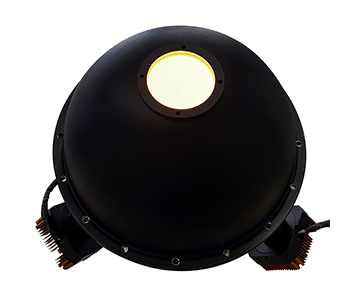
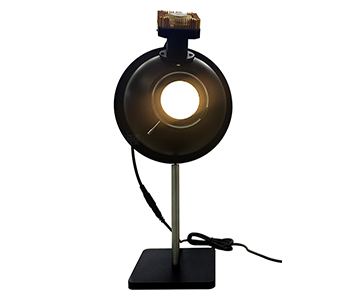
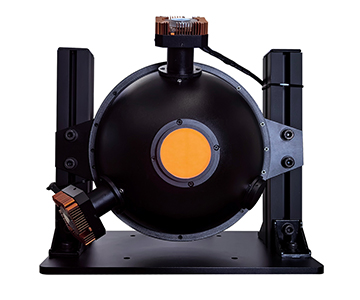
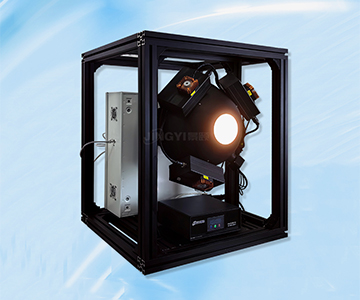
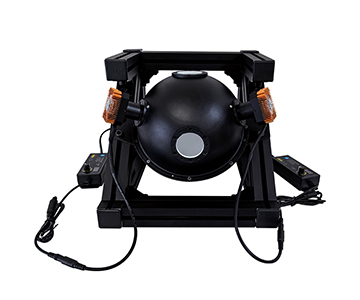
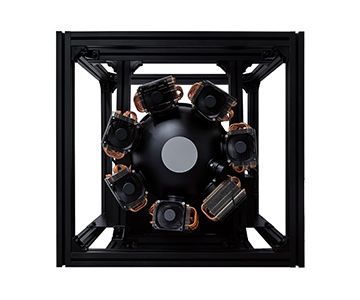
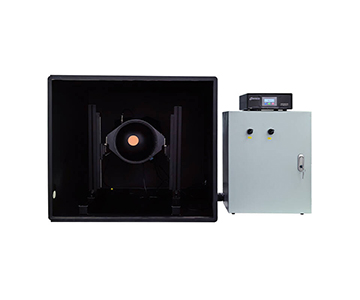
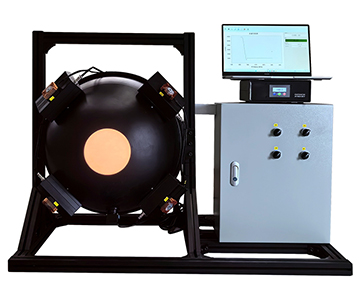
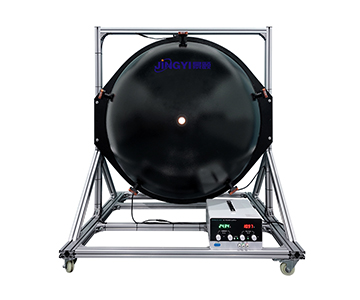
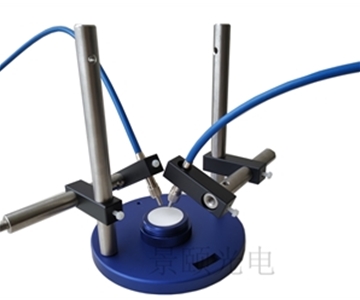
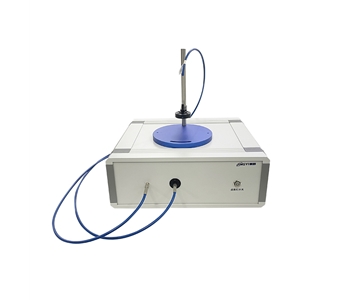
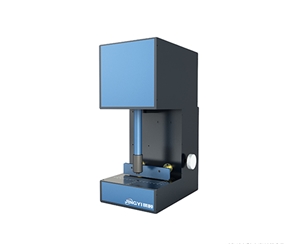
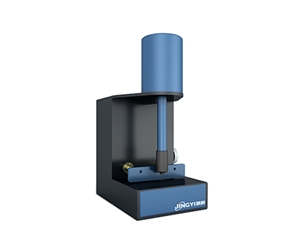
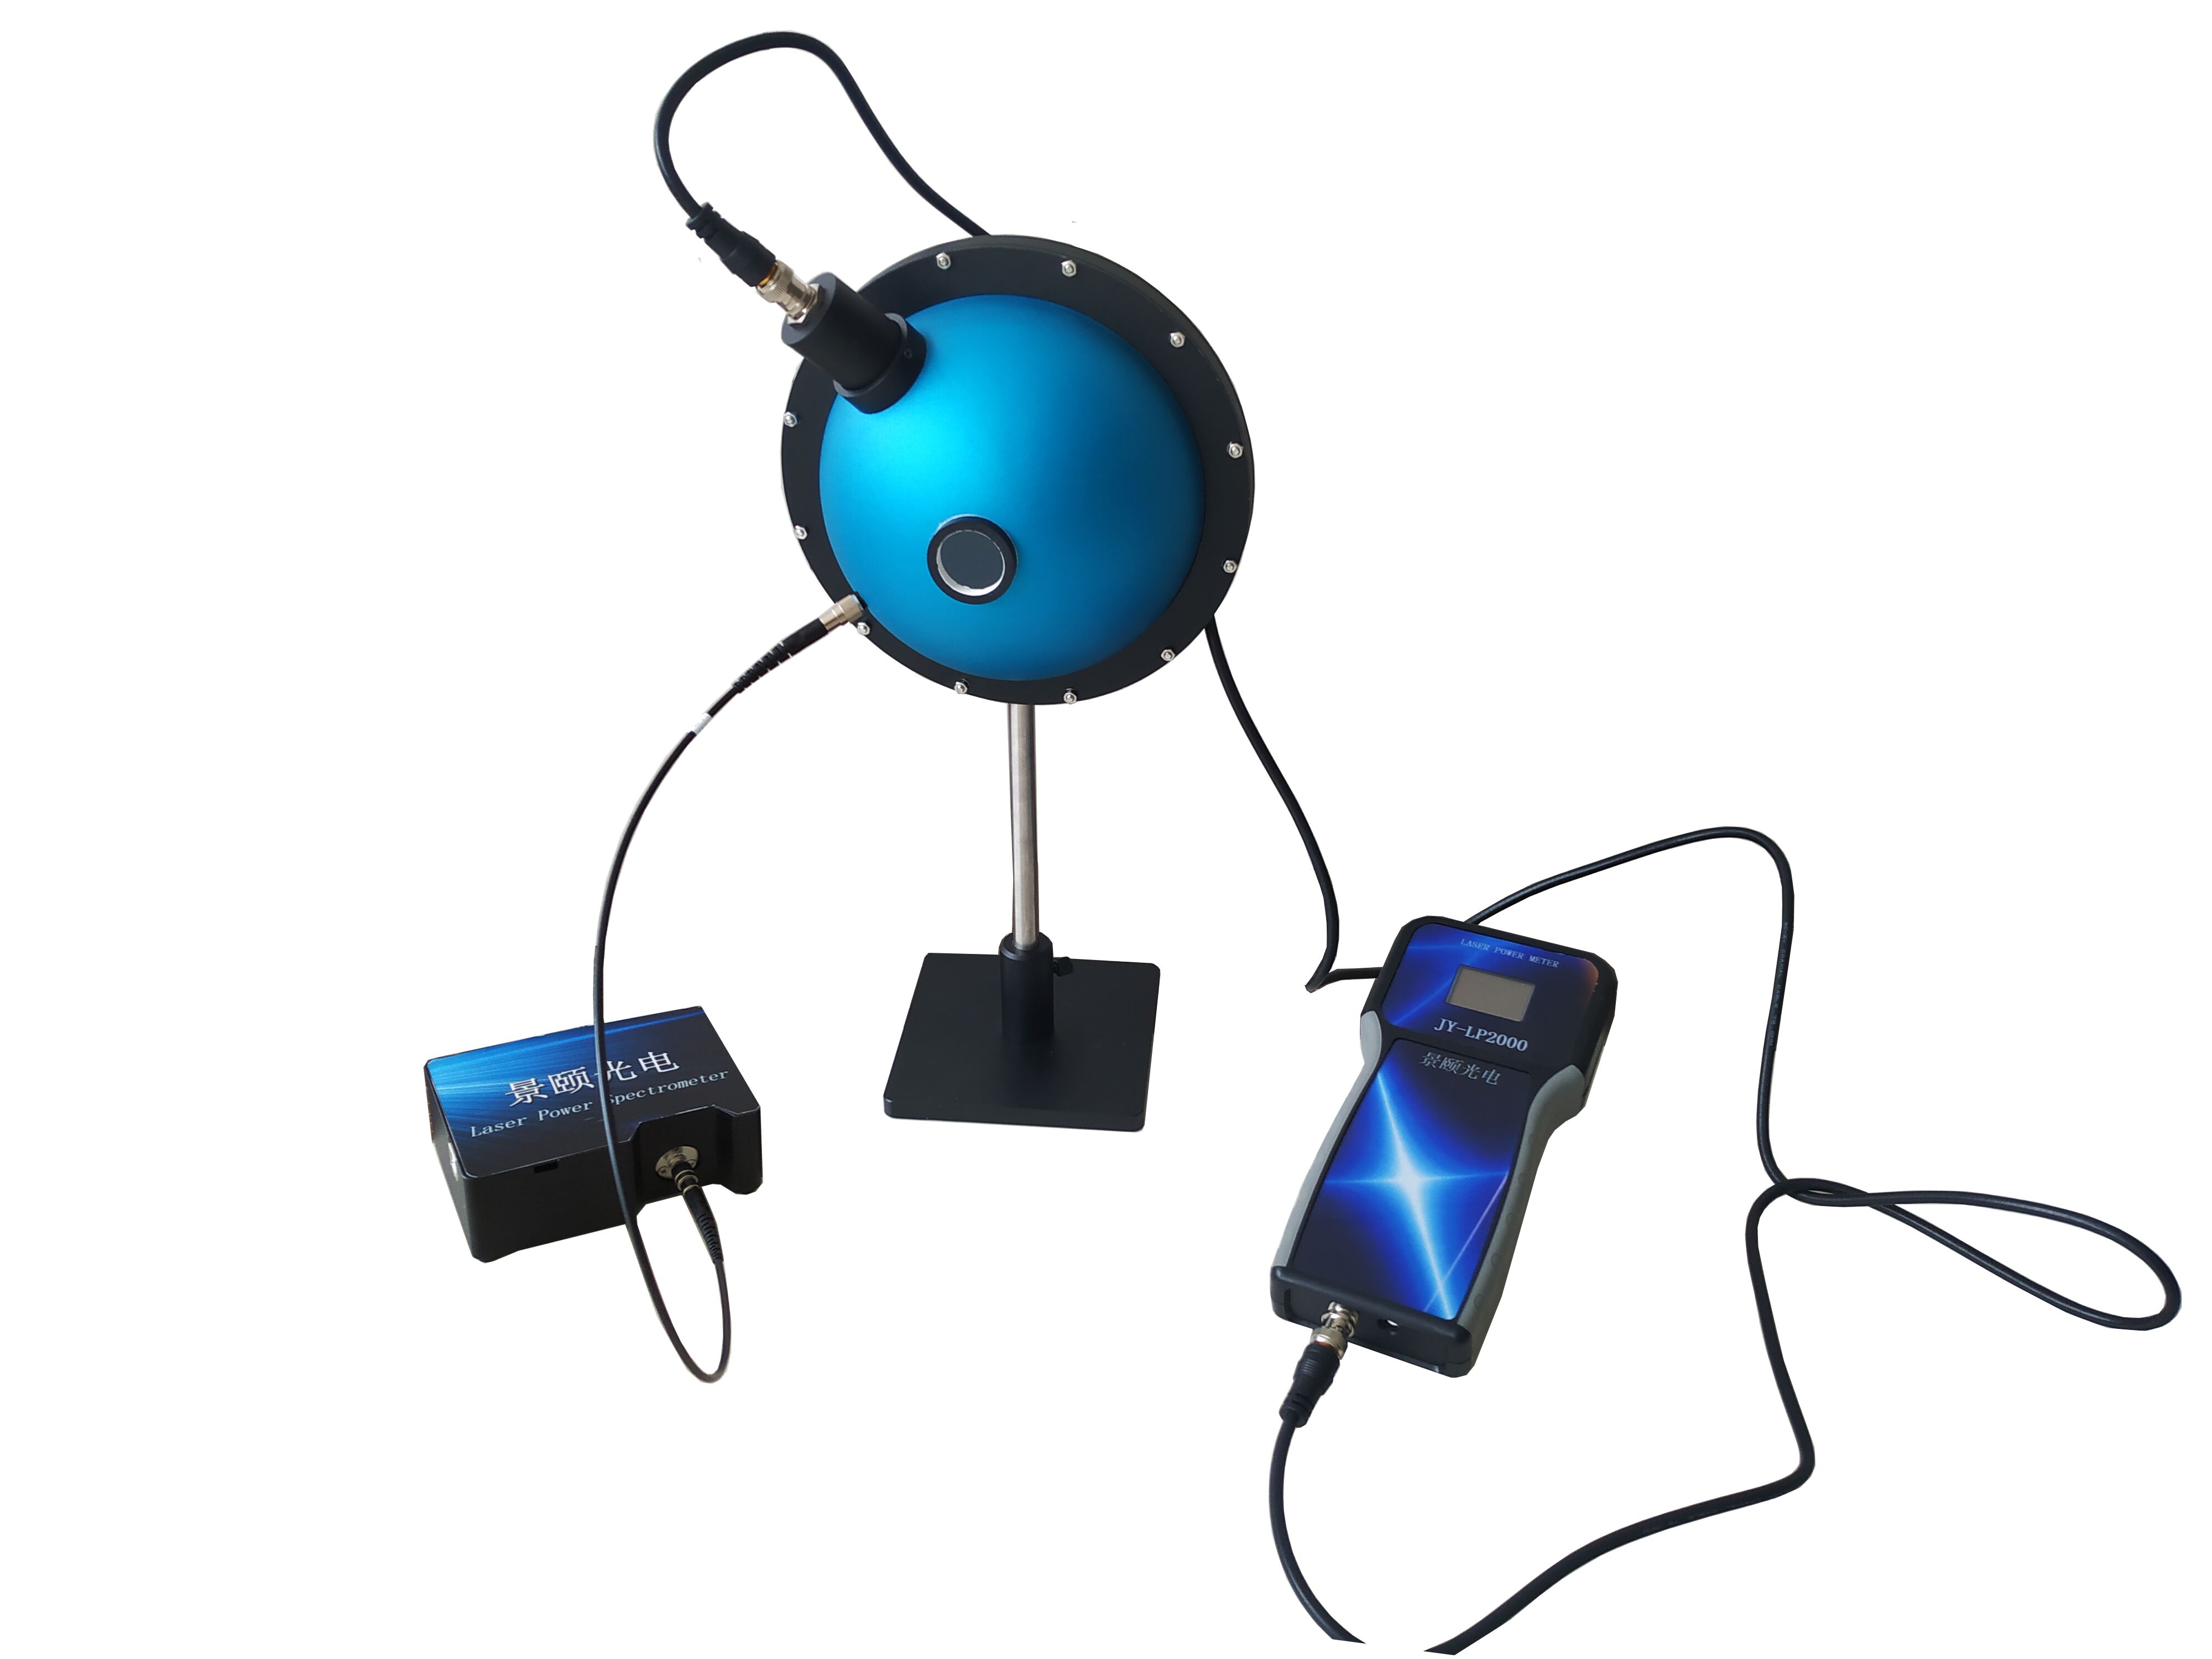
The evaluated system uses a PTFE high-diffuse-reflectance coating combined with a custom light-collection geometry. This configuration weakens the correlation between incident polarization state and final reading. When the production line switches between laser diode packages, stable power assessment is obtained without repeated mechanical alignment. In UV-to-near-IR laser detection spanning 200 to 1650 nm, the error contribution from fixture inconsistency is reduced at the source. The coating's Lambertian scattering behavior distributes the optical energy uniformly across the sphere wall before it reaches the detector, decoupling the reading from the spatial and polarization profile of the incoming beam.
Multi-Aperture and Segmented Range Coverage
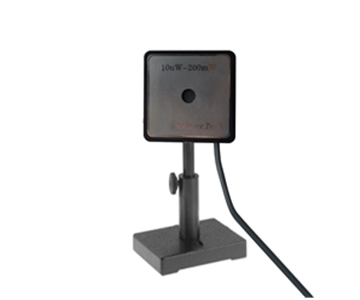
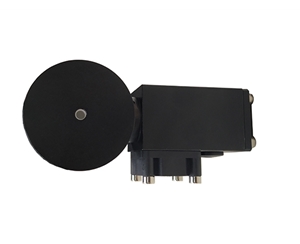
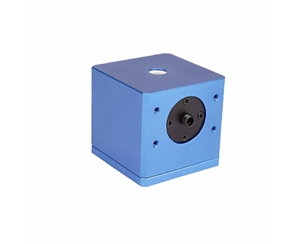
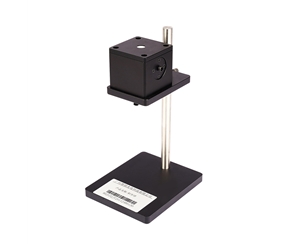
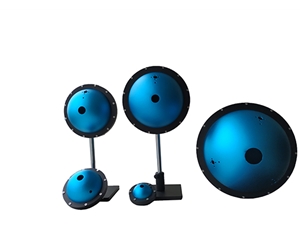
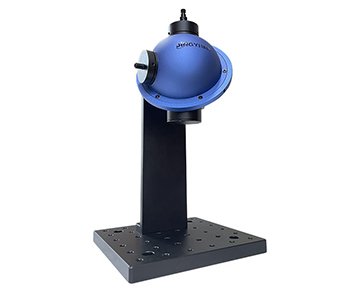
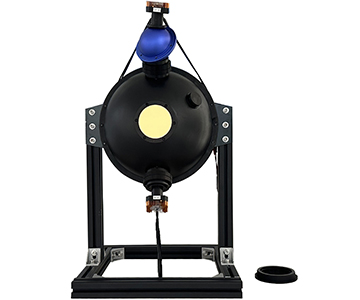
Sphere diameters of 50, 84, 100, 125, and 150 mm are available, with detector front apertures of 13 mm or 25.4 mm. The power range is segmented into three tiers: 1 nW to 0.01 W, 100 nW to 1 W, and 10 mW to 100 W. For pulsed laser power measurement requiring both peak and average capture, the 0.2 ms sampling interval records transients that would be smoothed over by slower systems. In laboratory R&D settings where small-signal reproducibility matters, the low-range tier combined with system-level calibration improves readability at the nanowatt level.
Integrated Sphere-Probe Calibration and Software Loop
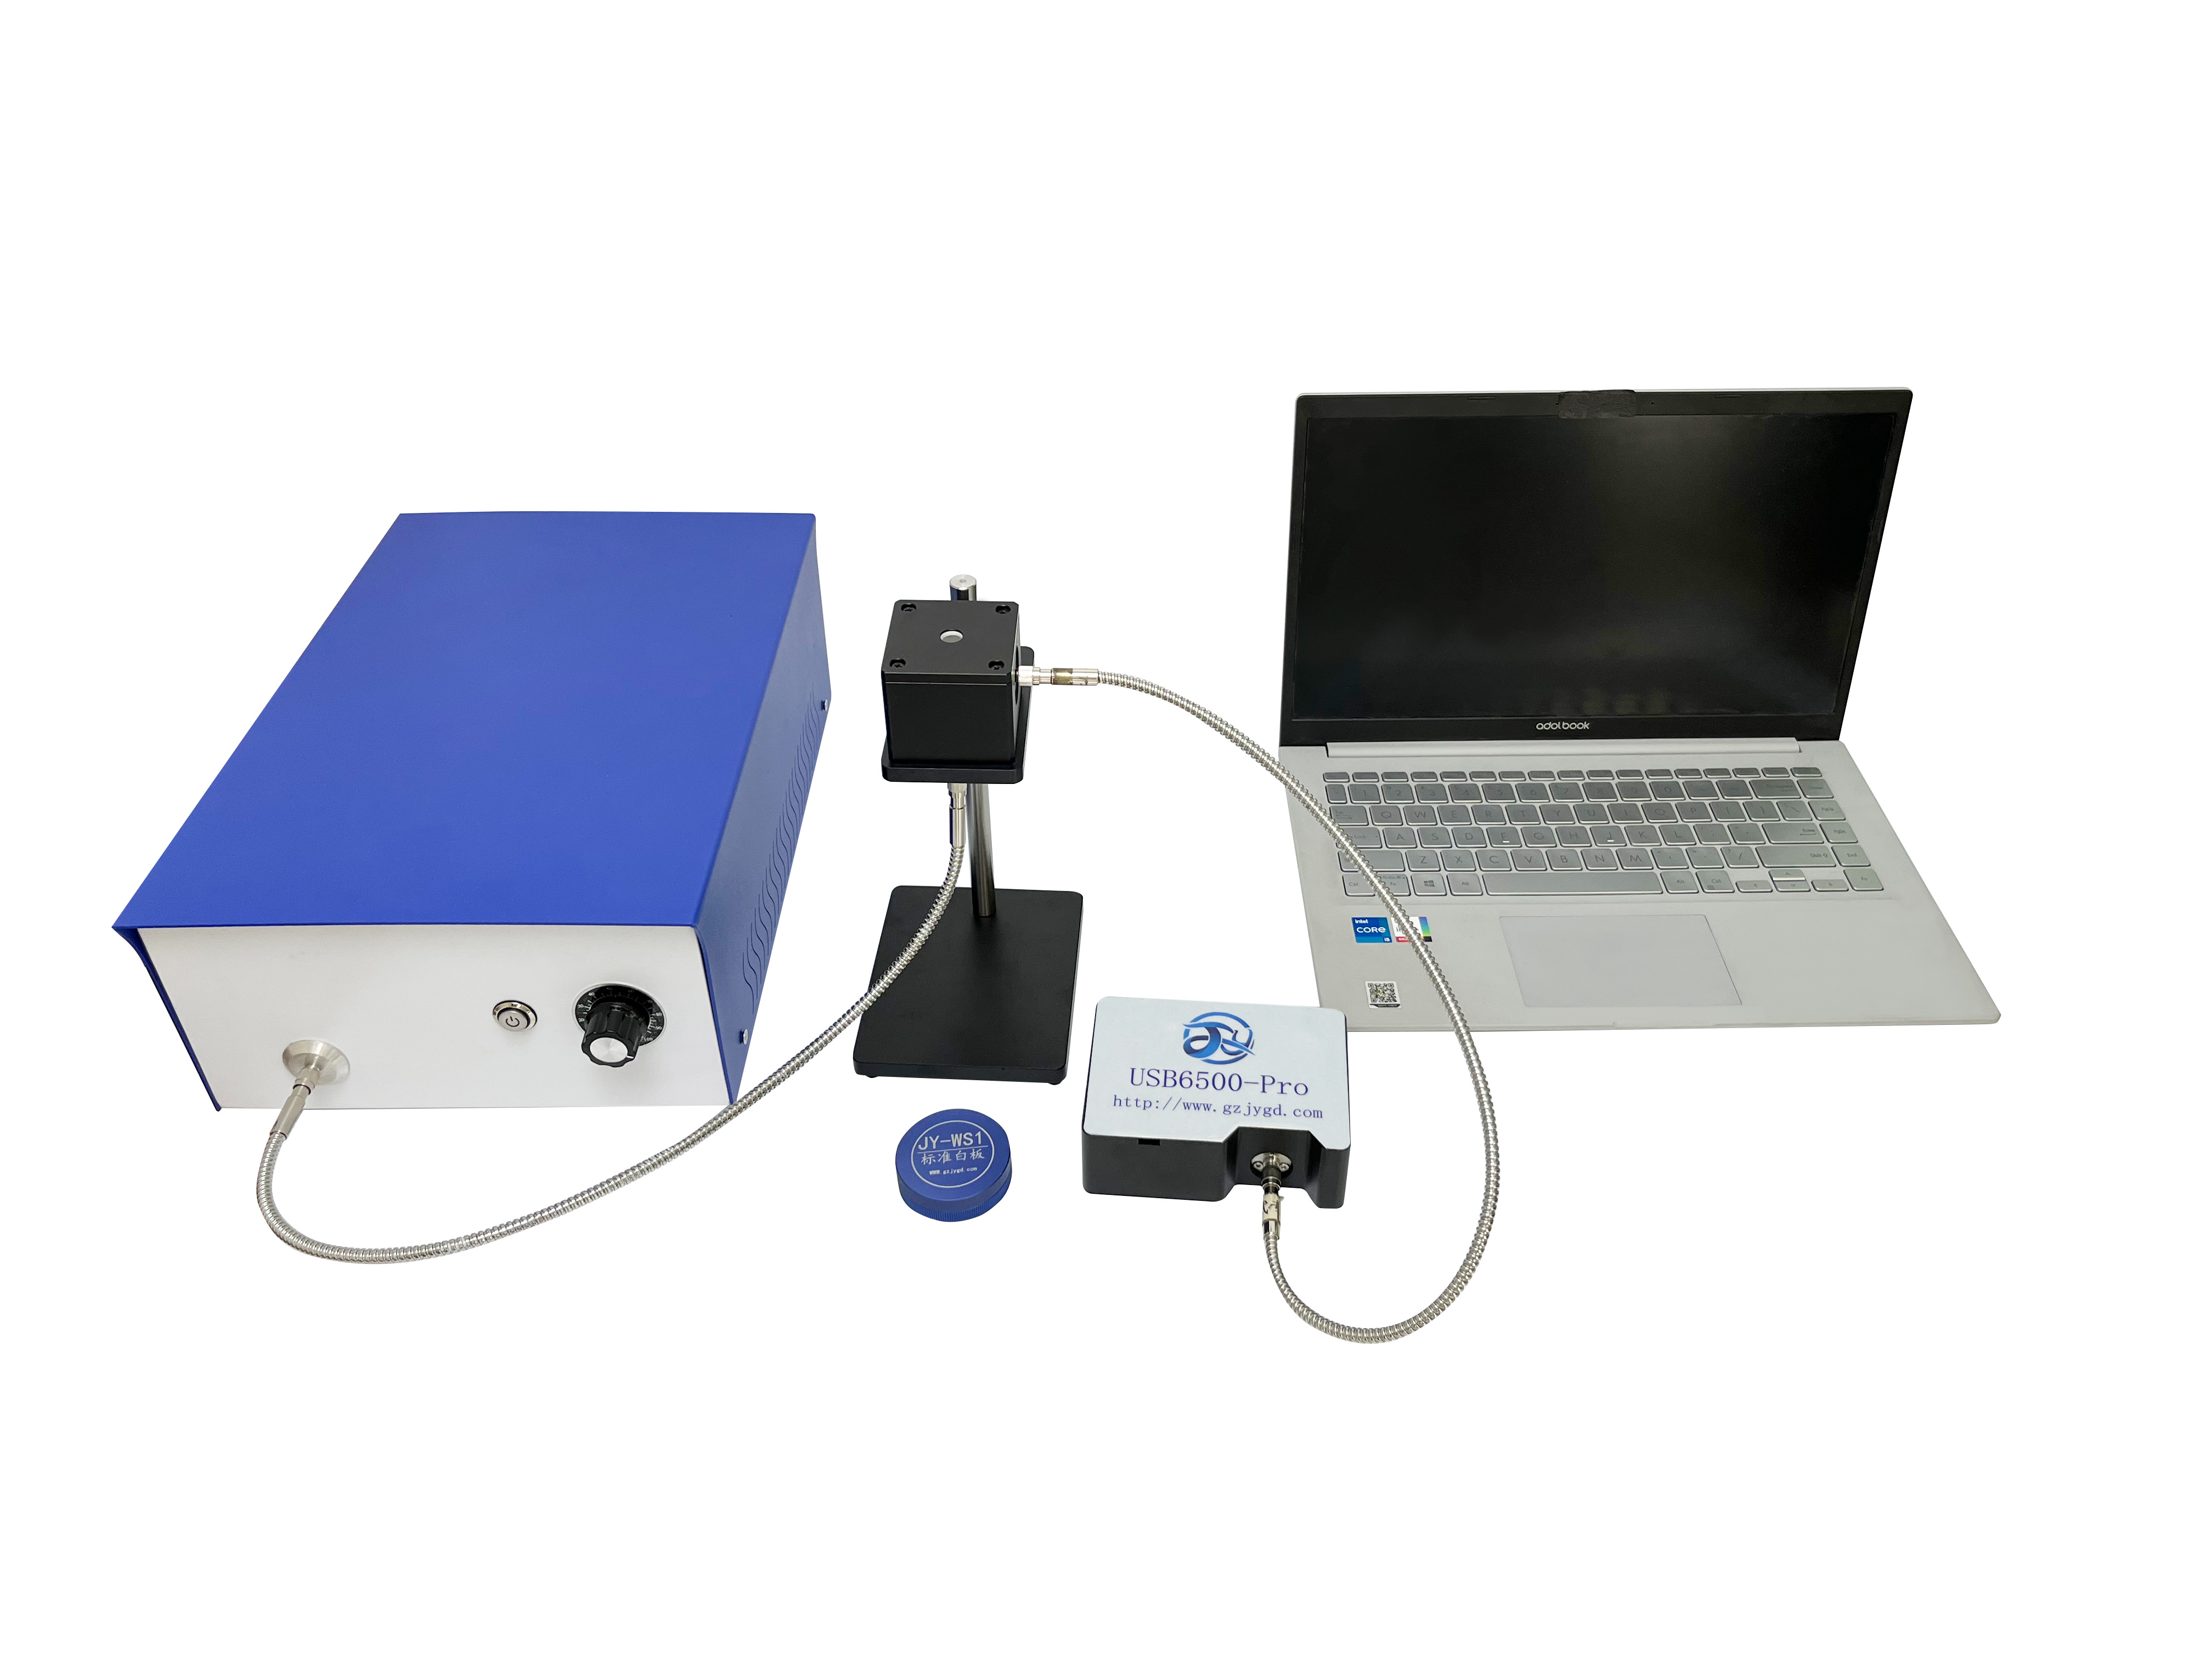
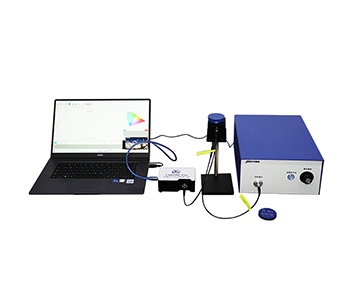
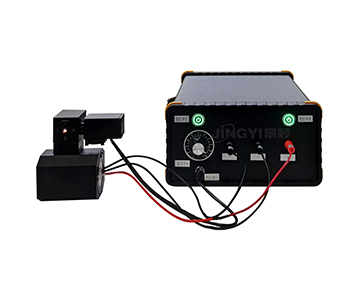
The integrating sphere and power probe are calibrated together at the factory, traceable to NIST standards. Post-calibration power accuracy is better than 1%, linearity ±0.5%, and uniformity ±2%. Dedicated analysis software communicates via USB 2.0, enabling one-click data export and CSV logging. Compared to separately calibrated probes, the integrated approach eliminates interface and spatial response mismatch. This simplifies periodic verification from a field maintenance perspective and shortens the metrology loop in optical communication device testing.
Quantitative Comparison: Before and After Deployment
Sampling Efficiency and Labor Hours
Before deployment, per-device power verification consumed 3.7 minutes, relying on manual recording and multi-instrument comparison. After deployment, the same task took 0.4 minutes with software-automated reading and archiving. The improvement represents an 89.2% reduction in labor time. At batch throughput, this difference converts directly into daily inspection capacity gains and removes transcription errors associated with handwritten logs.
Measurement Consistency and Rework Cost
Before deployment, batch power measurement uncertainty was ±5% against external reference standards, with quarterly rework losses at $152,000. After deployment, factory power accuracy is better than 1%, linearity ±0.5%, and quarterly rework losses dropped to $23,000. This 84.9% reduction in rework cost was recorded during a controlled comparison run on a laser module production line using the evaluated system. The data serves as a cost reference for optical communication manufacturers considering integrating sphere adoption.
Cross-Industry Transferability and Standards Compliance
From Optical Communication to Consumer Electronics Laser Processing
The sphere-probe integration and PTFE diffuse logic validated in photonic component testing transfer to consumer electronics laser processing source calibration. Pulsed laser marking and micro-hole drilling demand faster transient response. The 0.2 ms sampling combined with optional pre-attenuators covers source power巡查 across these processes. For long-duration continuous monitoring, selecting a larger sphere diameter according to the coating's thermal limits prevents high power density from entering a small cavity and inducing drift.
Automotive LiDAR Source Evaluation
In automotive LiDAR emitter power retesting, the technical requirements defined in T/CITS 231-2025 specify optical evaluation dimensions. The integrating sphere power meter retests emitted power and stability against these requirements, verifying measurement consistency. During procurement or acceptance, confirm compliance with this standard and combine it with NIST traceability documentation to build a complete calibration chain. This reduces cross-supplier component interchange risk without relying on a single vendor's claims.
Field Maintenance Perspective on Operational Convenience
Coating and Attenuator Routine Maintenance
From a field maintenance standpoint, the PTFE coating offers high reflectance and cleanability. Routine care involves dust-free wiping and periodic recalibration. When facing high-power continuous lasers, a pre-detector attenuator should be installed and the internal material's thermal limit verified. Pairing a large-aperture model with an adjustable attenuator reduces the frequency of sphere disassembly. Maintenance staff only need to log the attenuation factor in the software without rebuilding the entire optical path.
Software Connectivity and Calibration File Management
The device communicates with PC analysis software via USB 2.0, supporting one-click optical power data retrieval and CSV log export. This function binds calibration certificates, batch serial numbers, and measurement records. During resumption of work after recalibration, historical calibration factors are recalled without repeating the full setup. The operating environment of 5 to 50°C and below 70% RH humidity adapts to both laboratory R&D and production line旁站 maintenance, reducing cross-scenario handover training costs.
Applicability Boundaries and Realistic Constraints
High-Power Thermal Limits and Extreme Environment Restrictions
The coating and structural components inside the integrating sphere have an upper thermal acceptance limit. Sustained input near 100 W without attenuation causes local temperature rise,
Operator Skill and Standards Coverage Boundary
This solution reduces the requirement for fixture consistency, but maintenance personnel must still understand range switching, attenuator configuration, and NIST certificate updates. For non-laser continuous broadband total power, or scenarios requiring comprehensive plastic transmission and reflection evaluation, a single power meter cannot replace a transmission and thickness system. When plastic total transmission and reflection measurement is involved, establish an independent testing line referencing GB/T 47066-2026 to avoid acceptance deviation from cross-standard misuse.
Frequently Asked Questions
Q1: How can pulsed laser power measurement avoid missing transients during sampling?
The evaluated system uses a 0.2 ms sampling period with sphere-probe integrated readout, supported by dedicated software continuous buffering. When pulse width approaches the sampling interval, reduce average power, enable pre-attenuation, and verify both peak and average channels in the software. This prevents underestimation from inadvertent filtering during UV-to-near-IR laser detection.
Q2: How to reduce noise when measuring nanowatt-level low-power sources?
Select a 50 or 84 mm small sphere with a 13 mm low-noise detector head. Place the device in an environment below 70% RH with stable temperature. Through system-level NIST-traceable calibration and dark current correction, the 1 nW to 0.01 W low tier achieves stable signal-to-noise ratio, preventing subtle intensity variations from being masked by large-range averaging.
Q3: What is the recommended procedure for periodic on-site verification of an integrating sphere power meter?
Save the factory NIST certificate and calibration factors. Inject a standard laser source quarterly and compare against software logs. If the reading drifts outside the better-than-1% window, inspect the PTFE coating for contamination and check the front attenuator position. Return to factory for recalibration if needed. The production line need not stop entirely during this process.
Q4: How should buyers balance sphere aperture and cost for optical communication production lines?
For predominantly small-divergence laser diode sources, 50 to 100 mm basic models cover most 1 nW to 1 W conditions. For lines that also process consumer electronics high-power applications, select 125 or 150 mm large-aperture models with attenuators. Incorporate compliance review against standards such as T/CITS 231-2025. Procure based on expected operating range rather than extreme peak values to control initial investment.
Q5: How can I independently verify the long-term measurement reliability of an integrating sphere power meter?
Commission a third-party calibration laboratory to retest the device using NIST-traceable standard sources. Verify against the factory linearity specification of ±0.5% and uniformity of ±2%, and audit the complete calibration certificate chain. For routine monitoring, use the software's historical logs to perform trend analysis. Schedule recalibration only when deviation exceeds the defined threshold. Do not rely solely on the manufacturer's single-party report; build an independent assessment file.
Reference Information
Sources
: Jingyi Optoelectronics integrating sphere power meter technical documentation, NIST traceability calibration specifications, T/CITS 231-2025 and GB/T 47066-2026 public texts.
Author
: Cai Xiaodong, Senior Application Engineer, Jingyi Optoelectronics — 10 years in optical inspection, specializing in integrating sphere power systems, spectral analysis, and production line measurement traceability.
Conflict of Interest
: Jingyi Optoelectronics manufactures integrating sphere power measurement systems. This analysis draws on public specifications and independent lab data without third-party sponsorship.
Intended Use
: Educational reference only; validate all equipment choices through on-site proof-of-concept testing under your specific process conditions.
Updated
: September 2026
For detailed specifications and application notes on integrating sphere power meters, search "Jingyi Optoelectronics integrating sphere power meter" or visit the technical library.